
shaft machining · hillsborough, new jersey
Home / Custom Shaft Manufacturing
Custom shaft manufacturing has been at the centre of this shop for three generations, starting in the polymer extrusion industry and growing from there. We make high-precision shafts for demanding drives — large industrial drive shafts through to fine splined and stepped components — at scales and tolerances most job shops cannot reach. Those shafts go into aerospace and defense work, high-torque polymer processing lines, and heavy industry generally.
Work usually starts with reverse engineering, which is what you need when the OEM prints for a piece of legacy machinery no longer exist. From there: material sourcing in high-grade alloys, stainless and exotics; CNC turning and 5-axis milling for splines, keyways and stepped diameters; grinding on every precision diameter for surface finish; and a final inspection for alignment and concentricity on the Keyence portable CMM. Then it ships, anywhere in North America. Most shaft work here is built to print from the customer’s drawing.
Most shaft enquiries describe the machine, not the shaft. That is fine — tell us what it drives and send the print, and we will take it from there.
Pump shafts — centrifugal and positive-displacement pump shafts, turned and ground on the seal and bearing diameters, in stainless where the fluid calls for it.
Blower and fan shafts — long, straight shafts for high-volume blowers and industrial fans, where runout decides how long the bearings last.
Gearbox and drive shafts — input, output and intermediate shafts for industrial reducers, splined or keyed, ground on the bearing journals. Often made here alongside a gearbox rebuild.
Extruder shafts and screws — drive shafts, feed screw repair, flight re-cutting and straightening for single and twin-screw lines.
Mixer and agitator shafts — long shafts with keyed or flanged ends, machined for the seal and the coupling.
Ball mill pinion and drive shafts — pinion shaft blanks with their journals and keyways, drive shafts and countershafts, and honed trunnion liners and bearing sleeves for mid-size mills.
Rotor and motor shafts — replacement rotor shafts measured off the old one and made new.
Rolls and rollers — journaled rolls and roller shafts for converting, film and process lines.
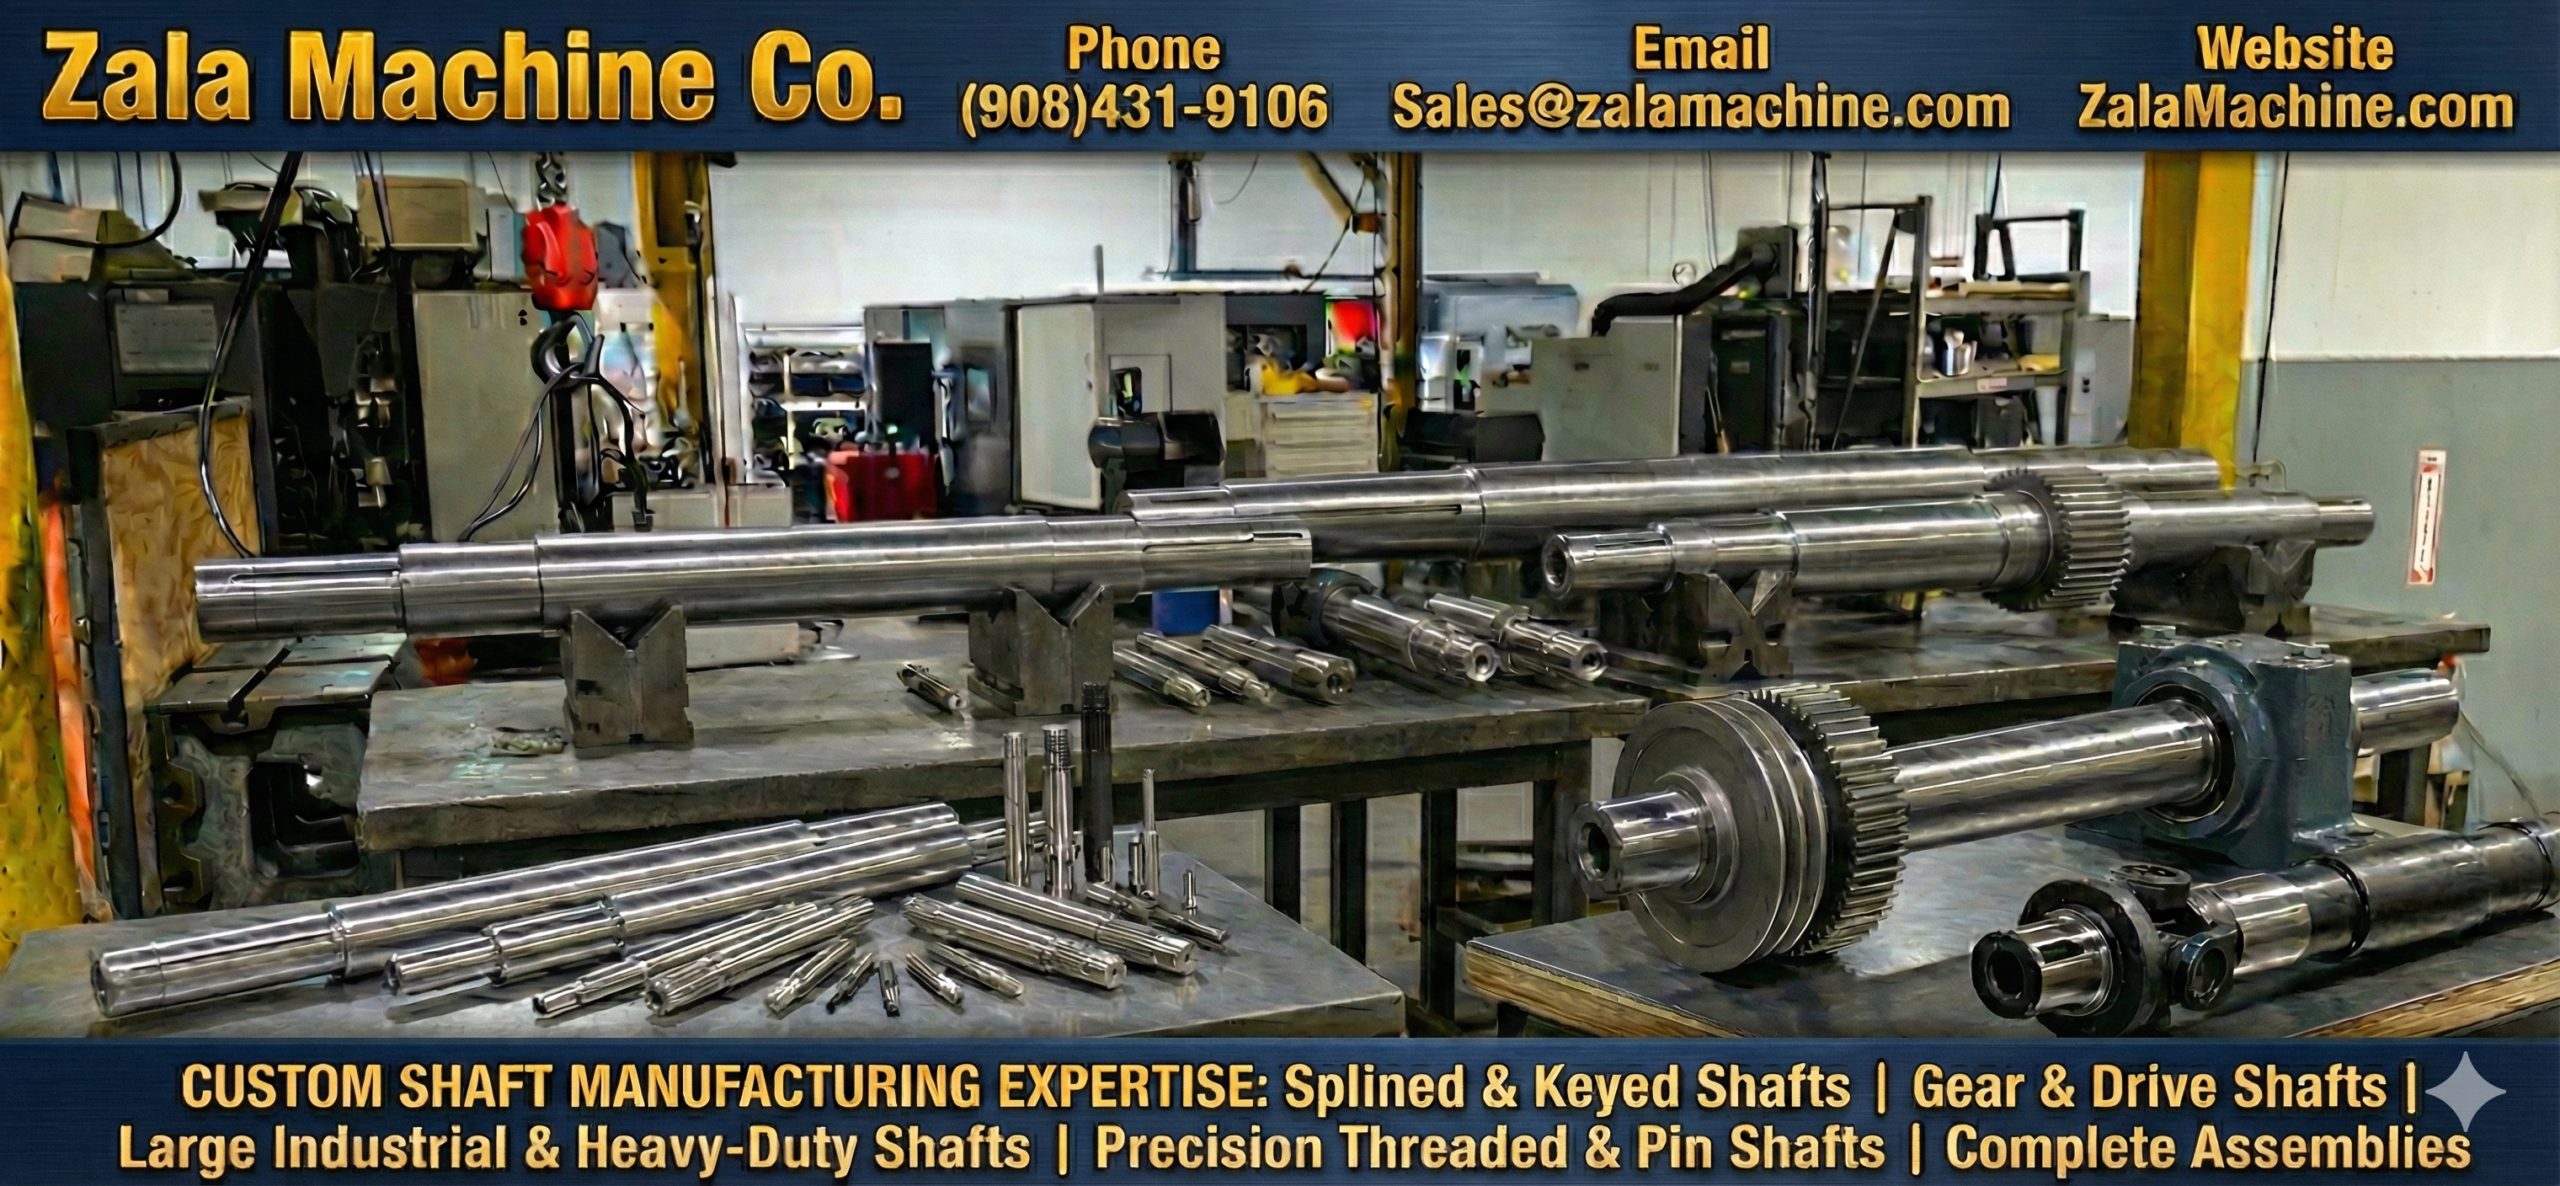
Splined, keyed, stepped and large industrial shafts made in this shop.
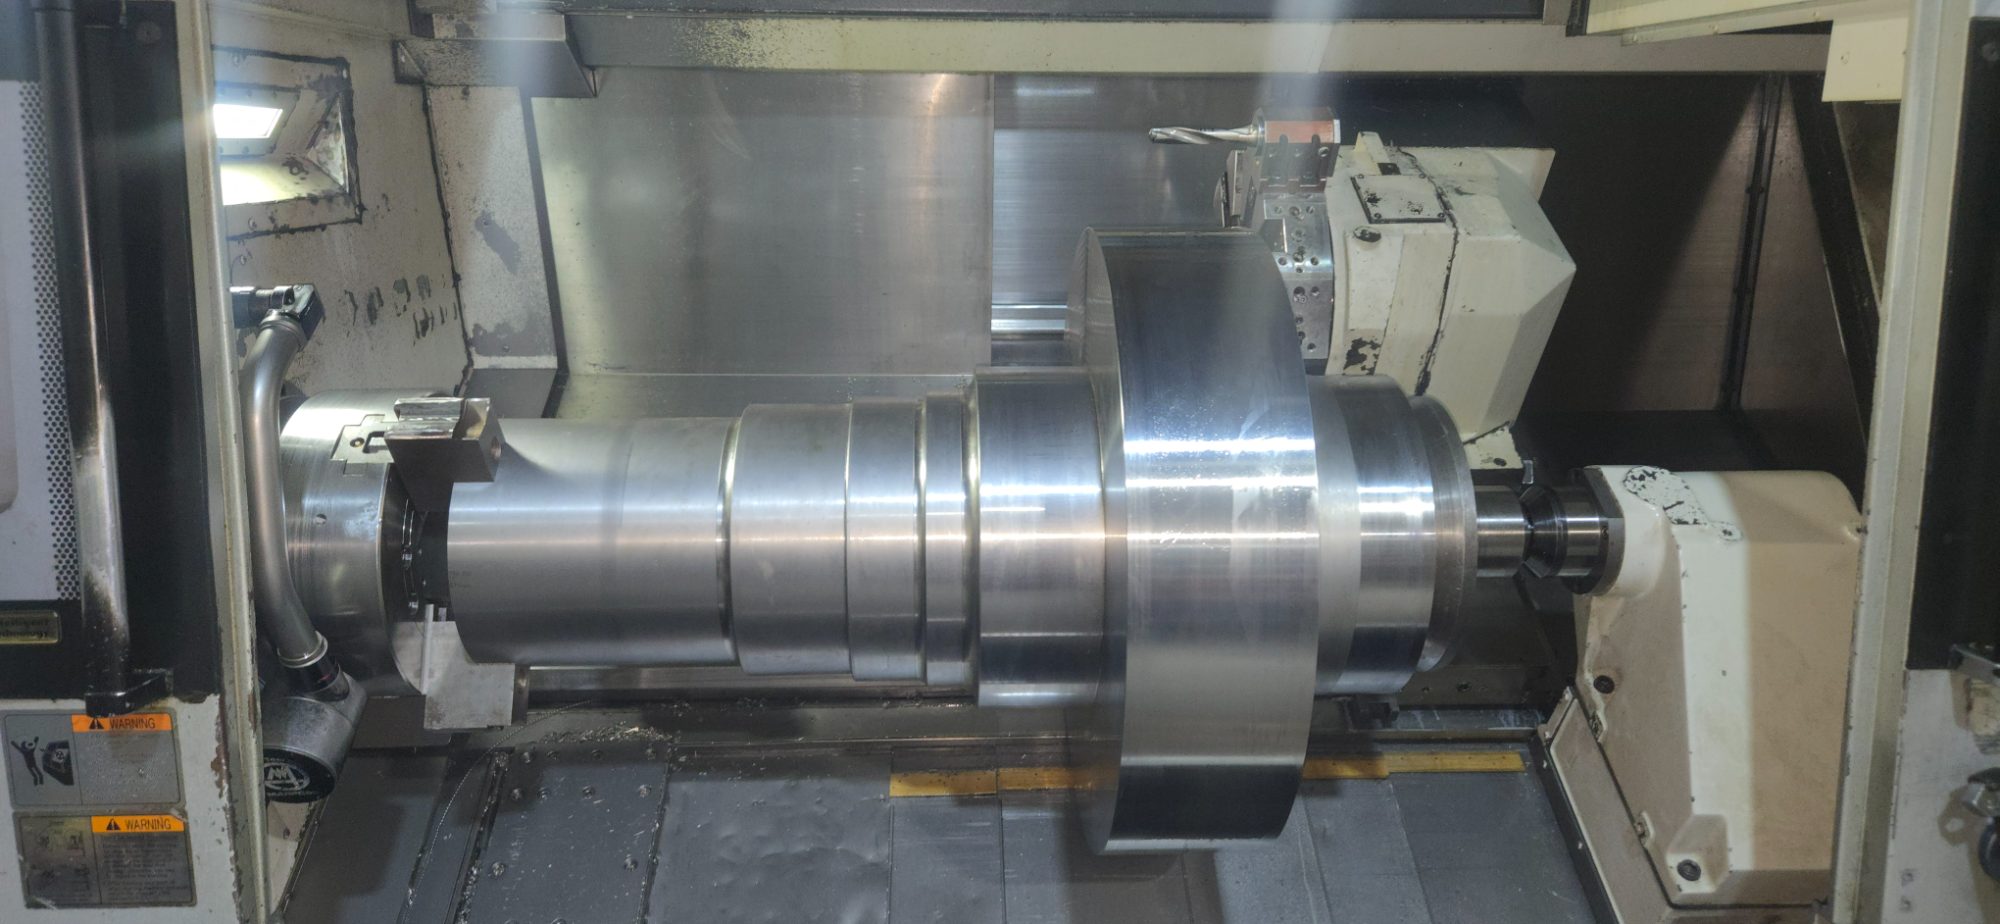
Large-diameter thrust shaft for a gearbox, turned on the CNC lathe.

Stepped drive shaft with multiple diameters, machined to print.
Custom shafts manufactured at Zala Machine Co. — splined, stepped, keyed and hollow-bore shafts turned and milled to print for industrial drives and gearboxes.
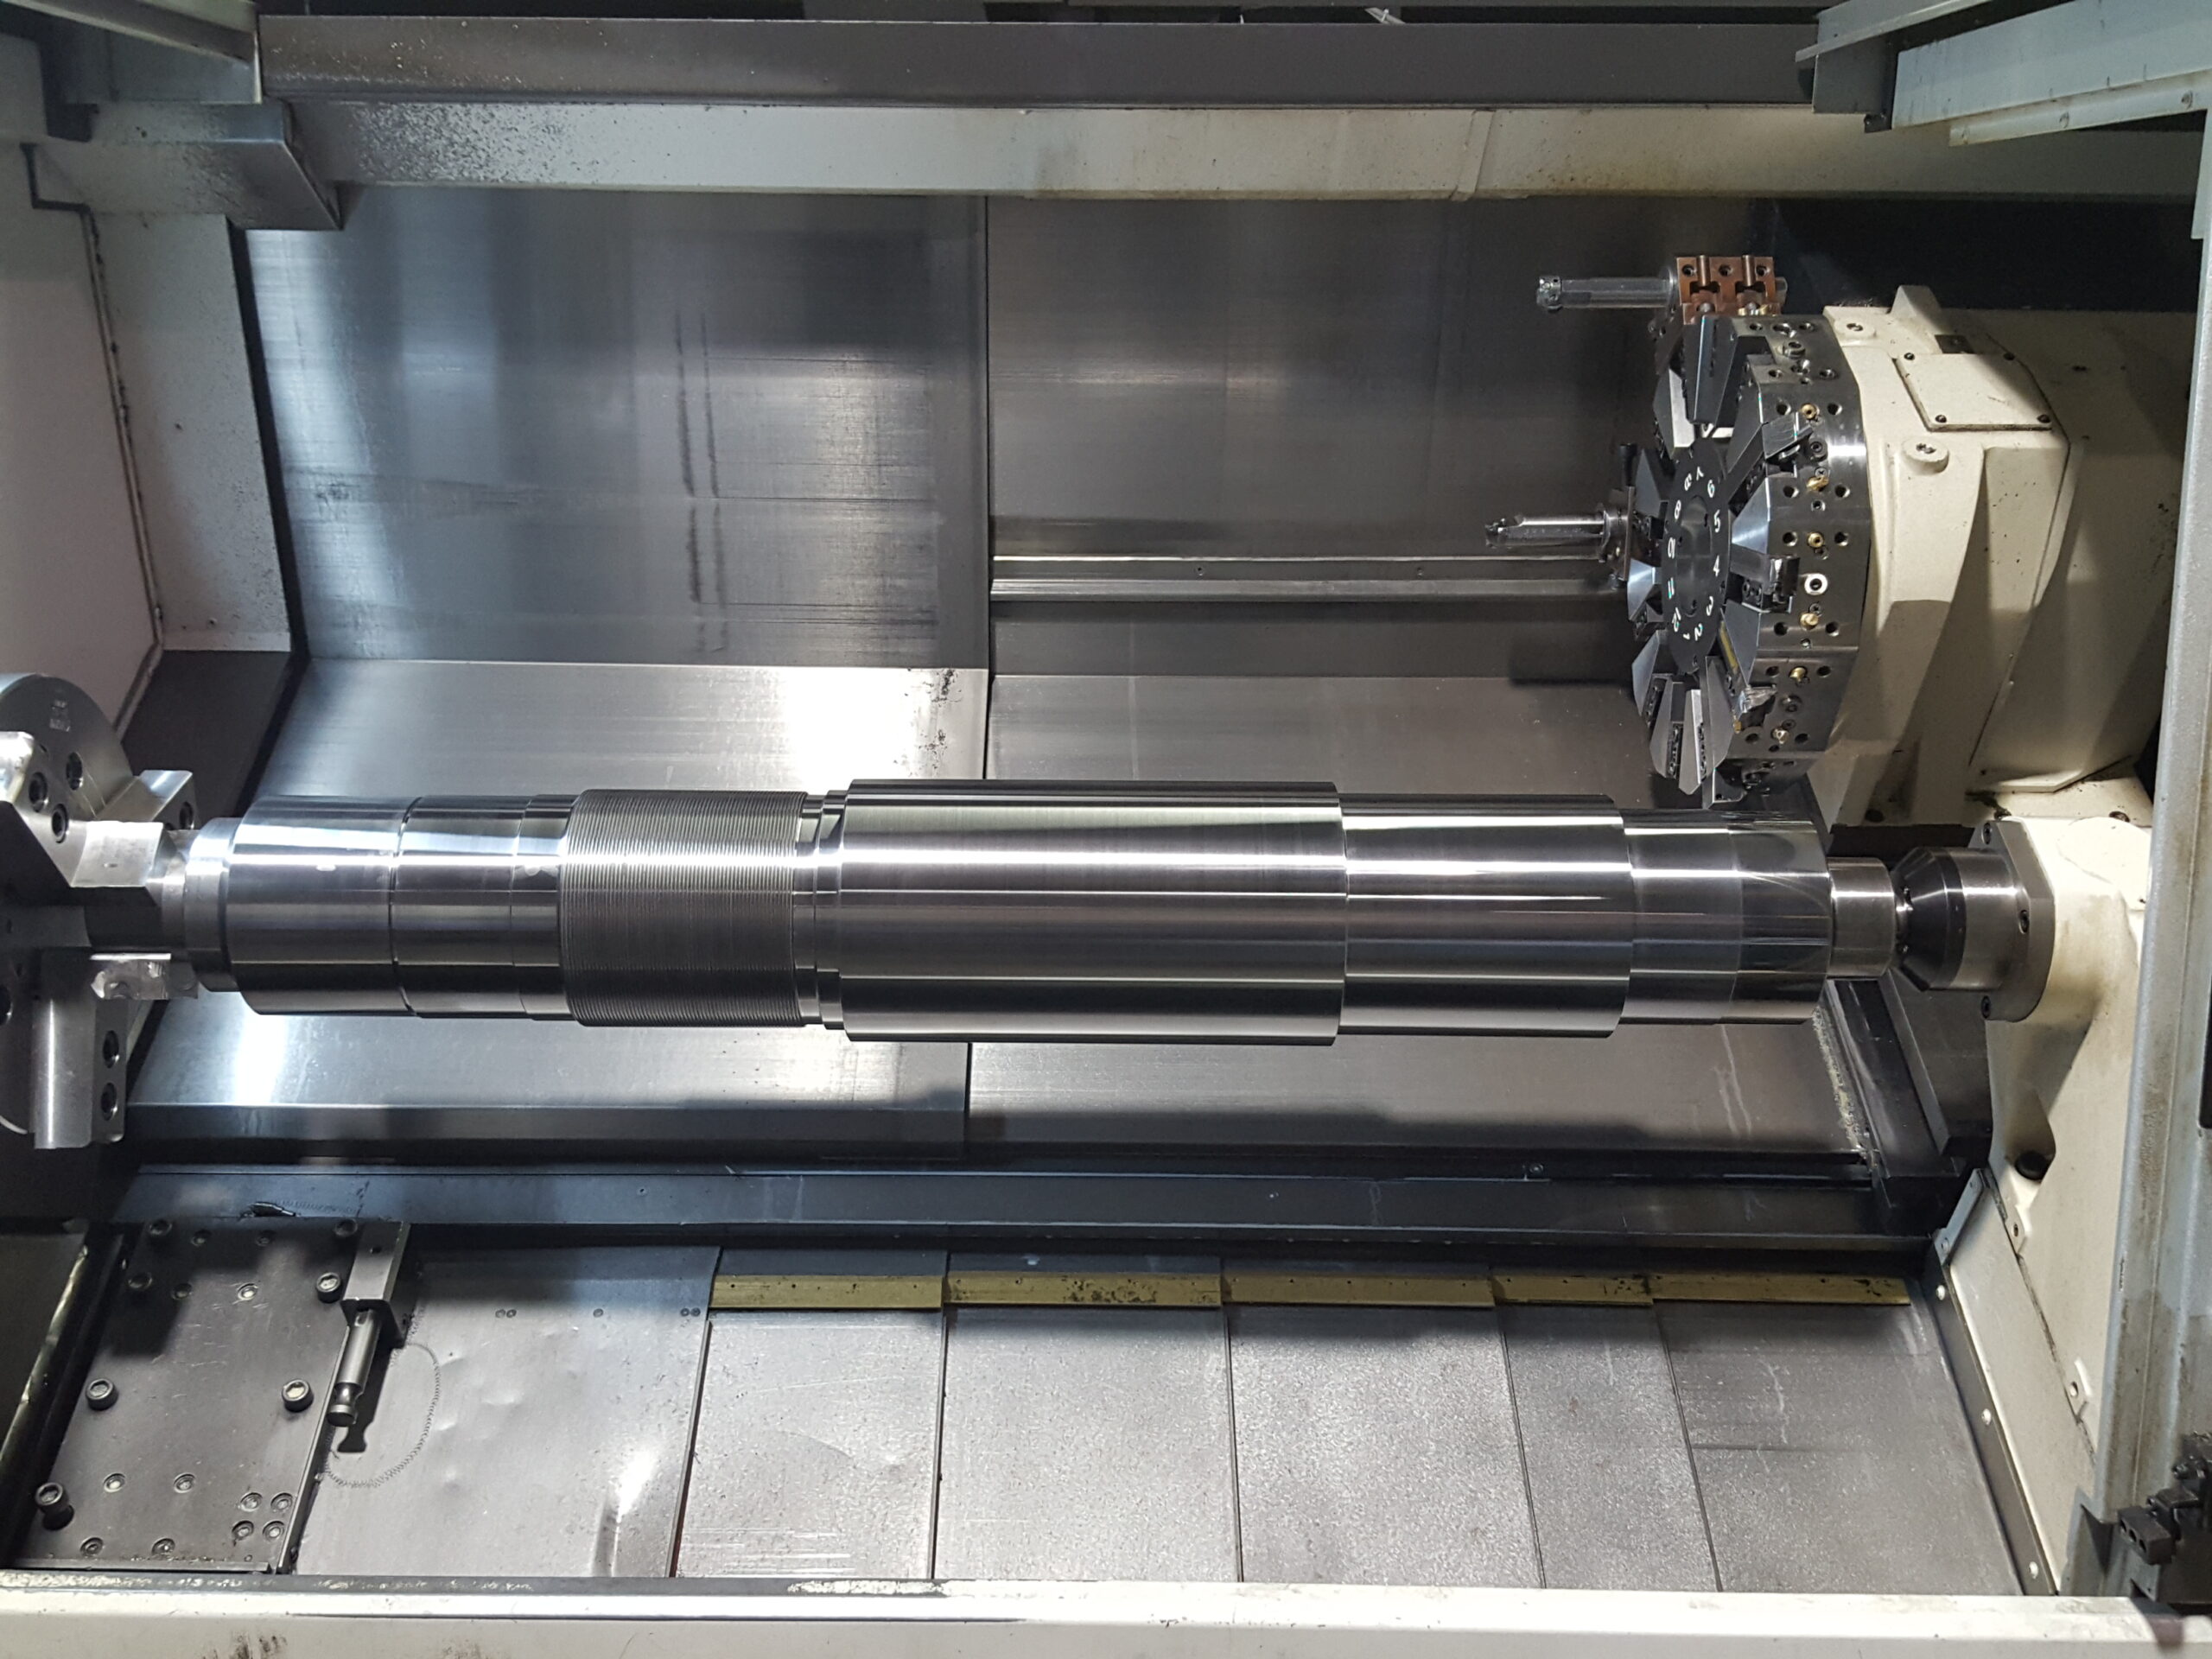
Long component set up on the CNC lathe bed.
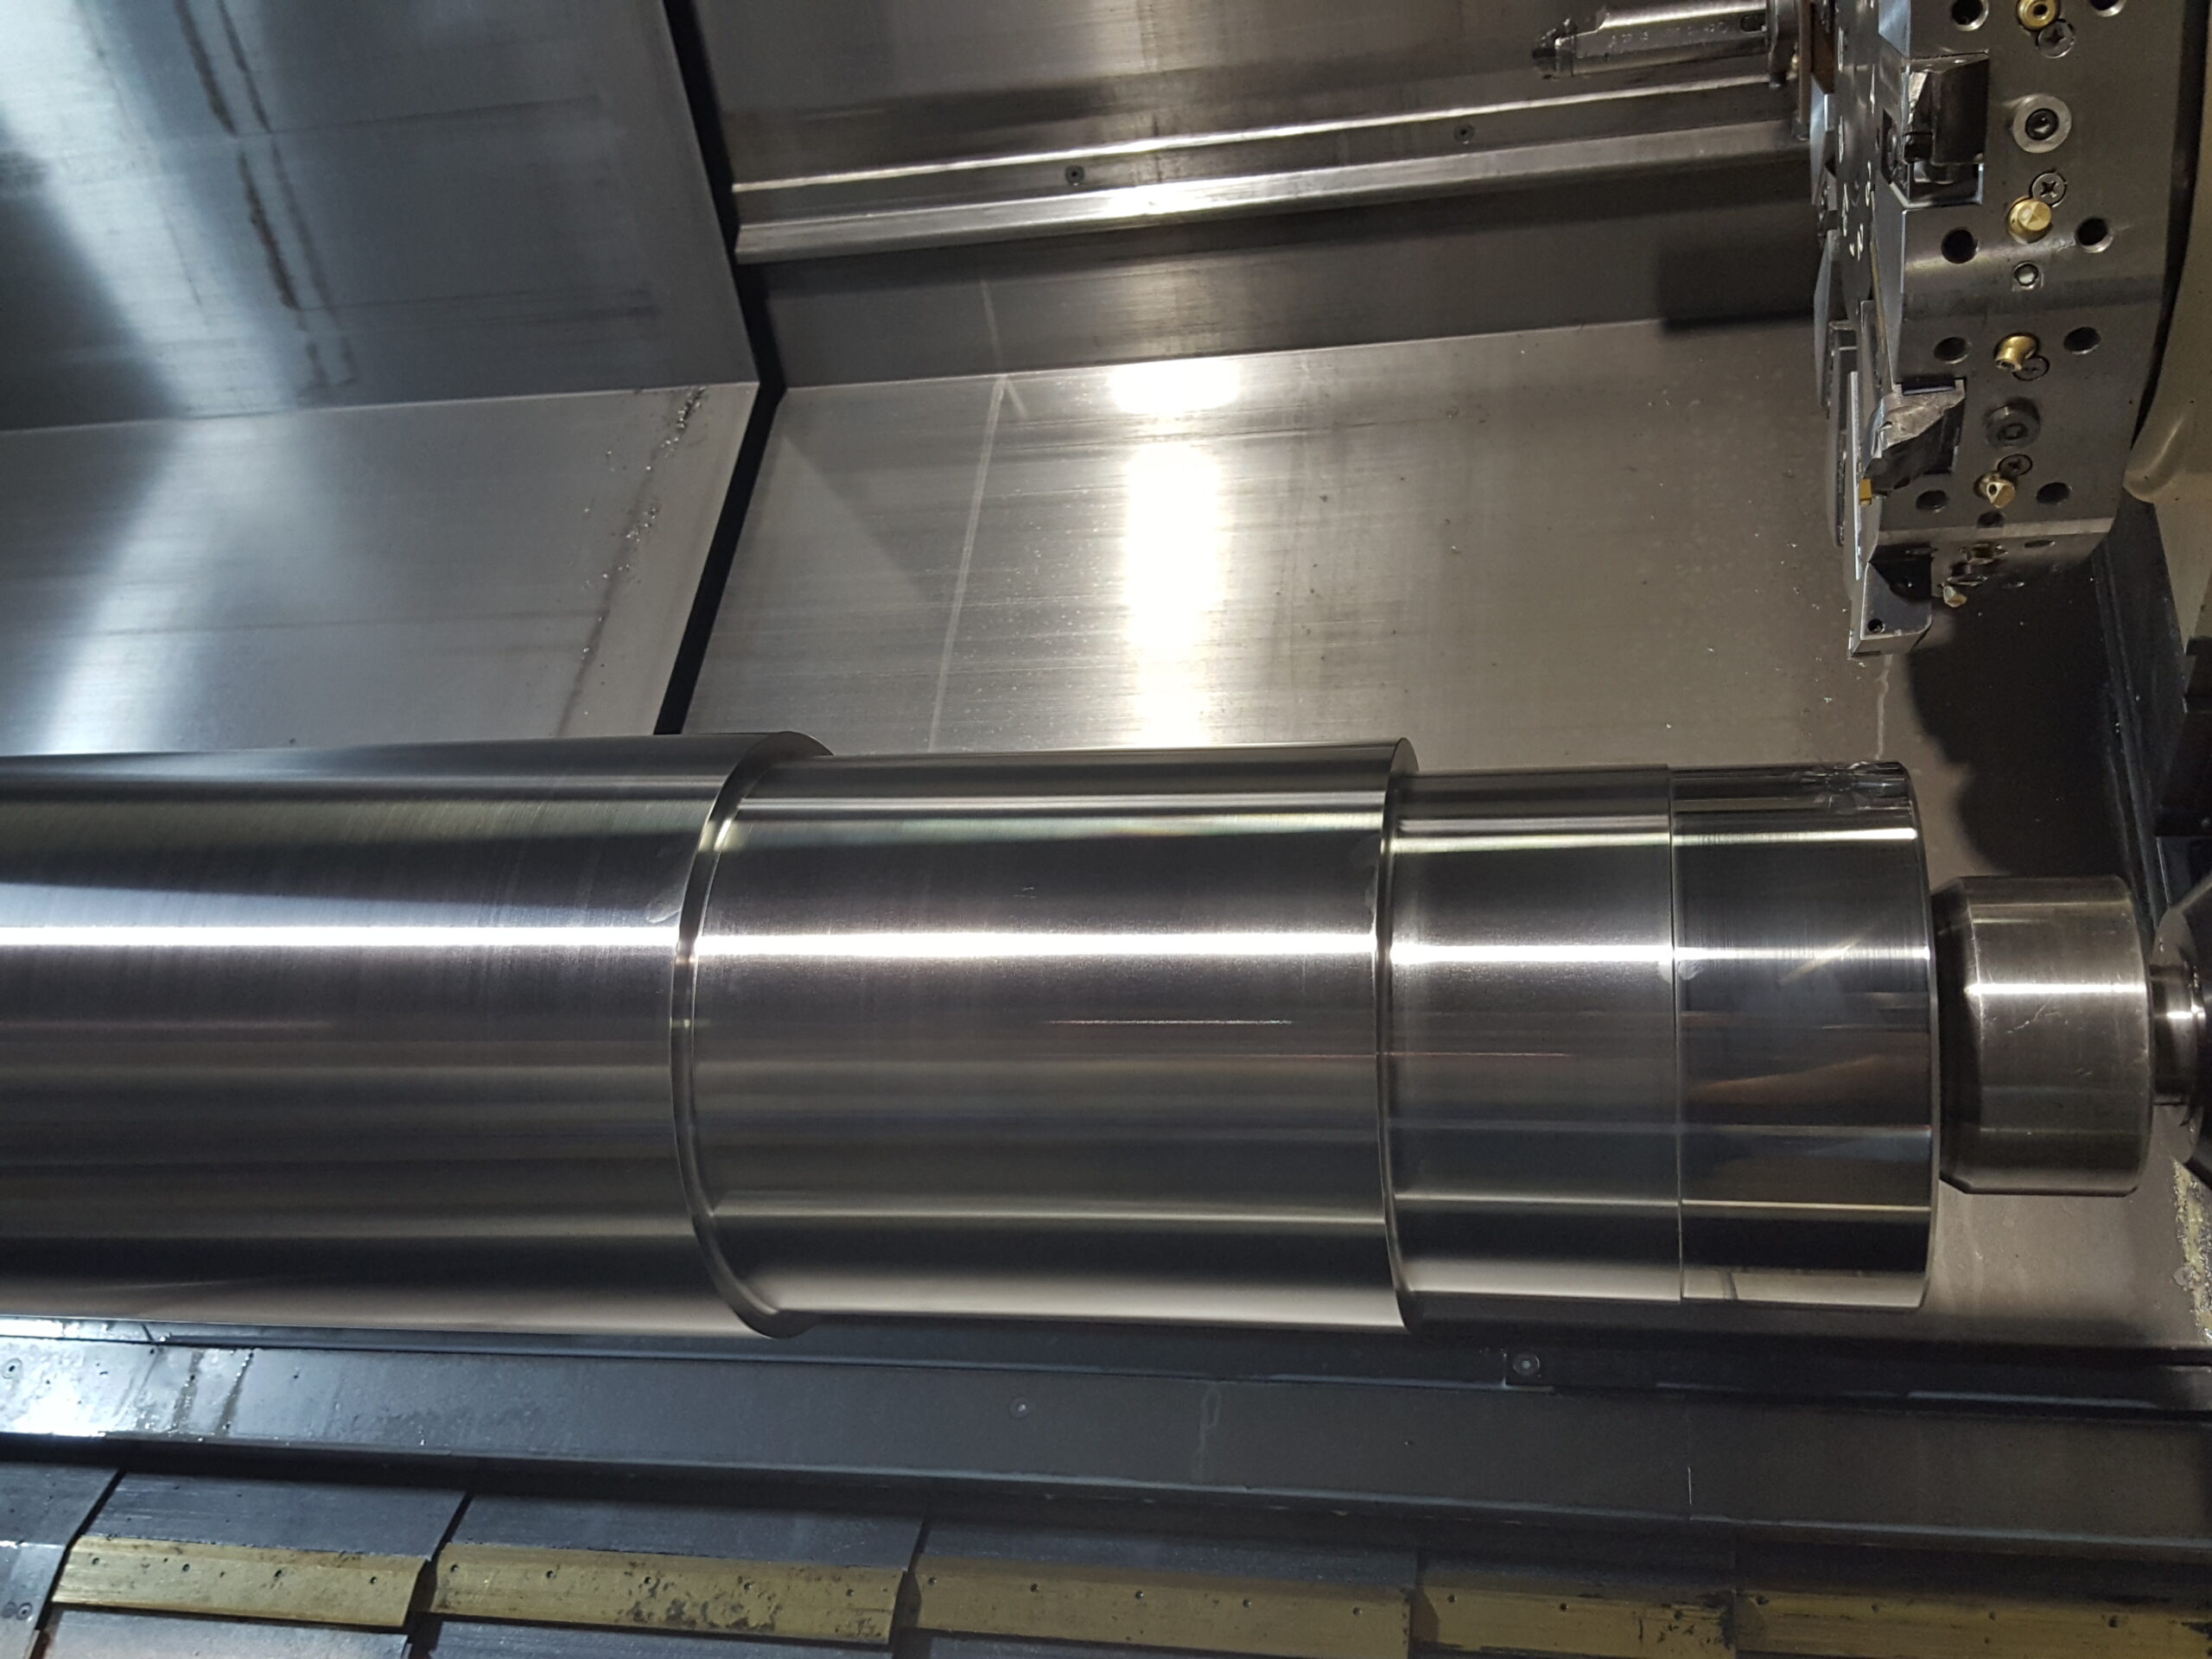
Multi-diameter shaft resting on the lathe bed.
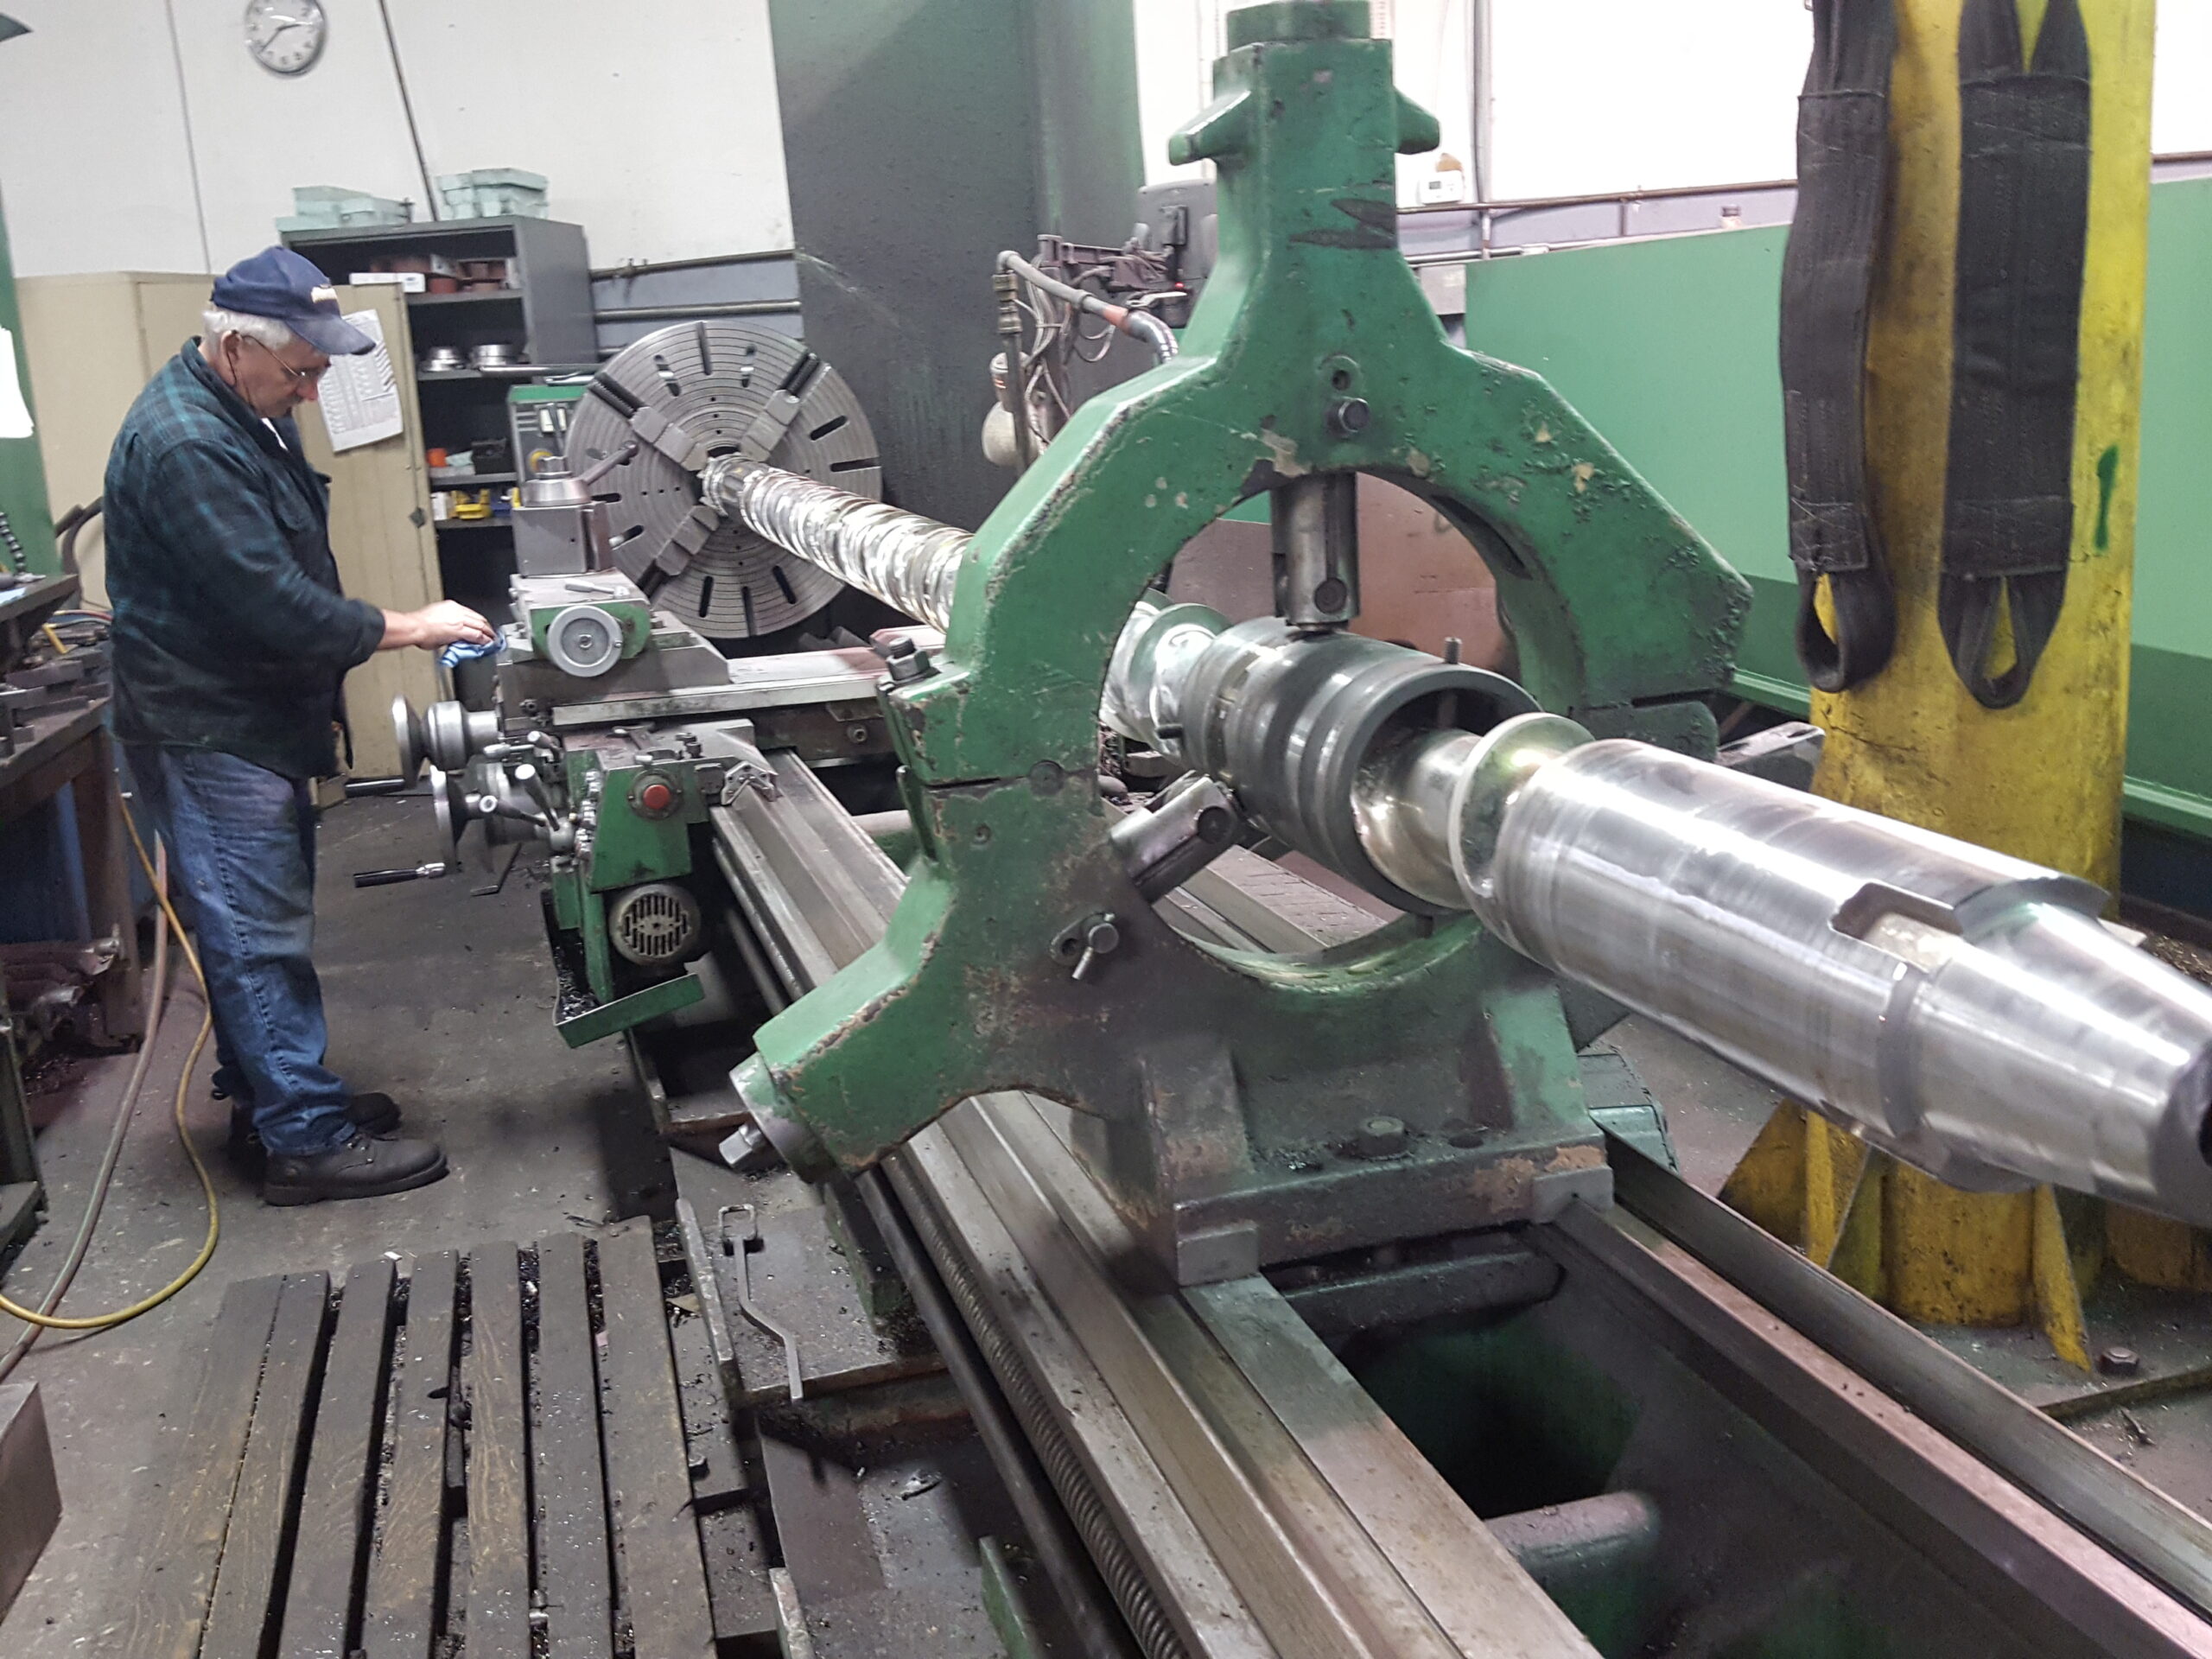
Setting up a long shaft on the large lathe.
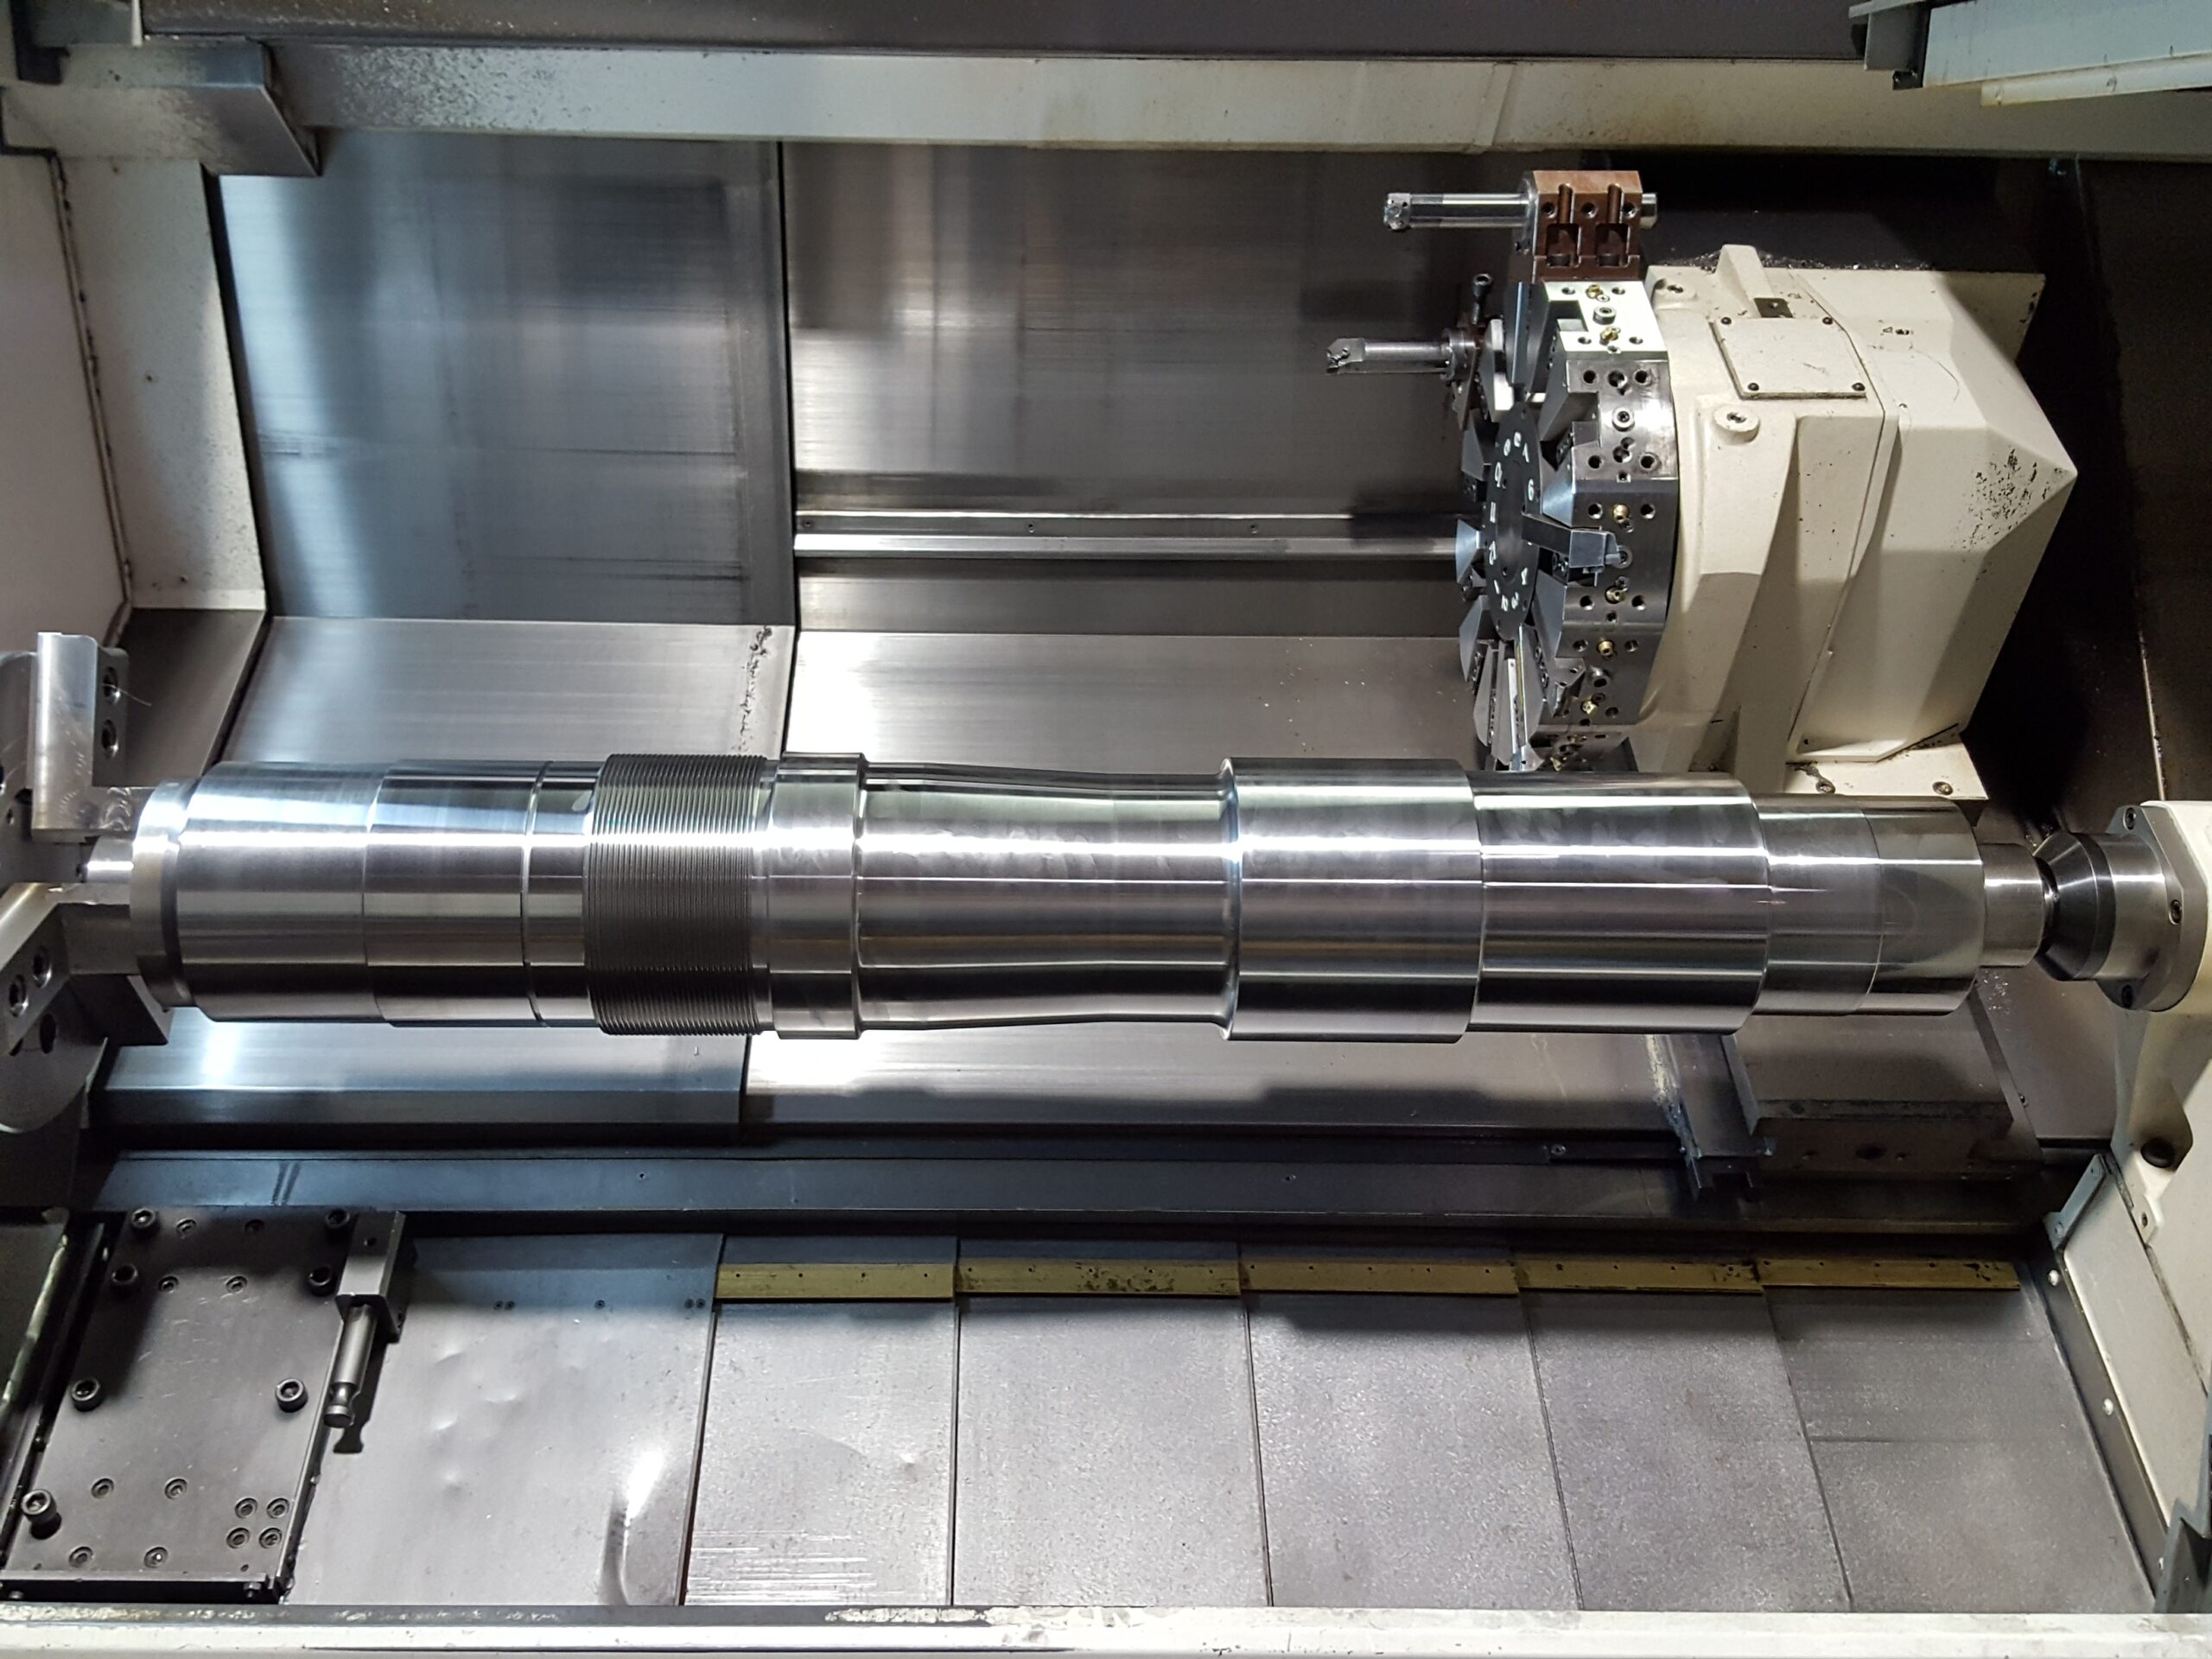
Machined industrial shaft on the lathe bed.
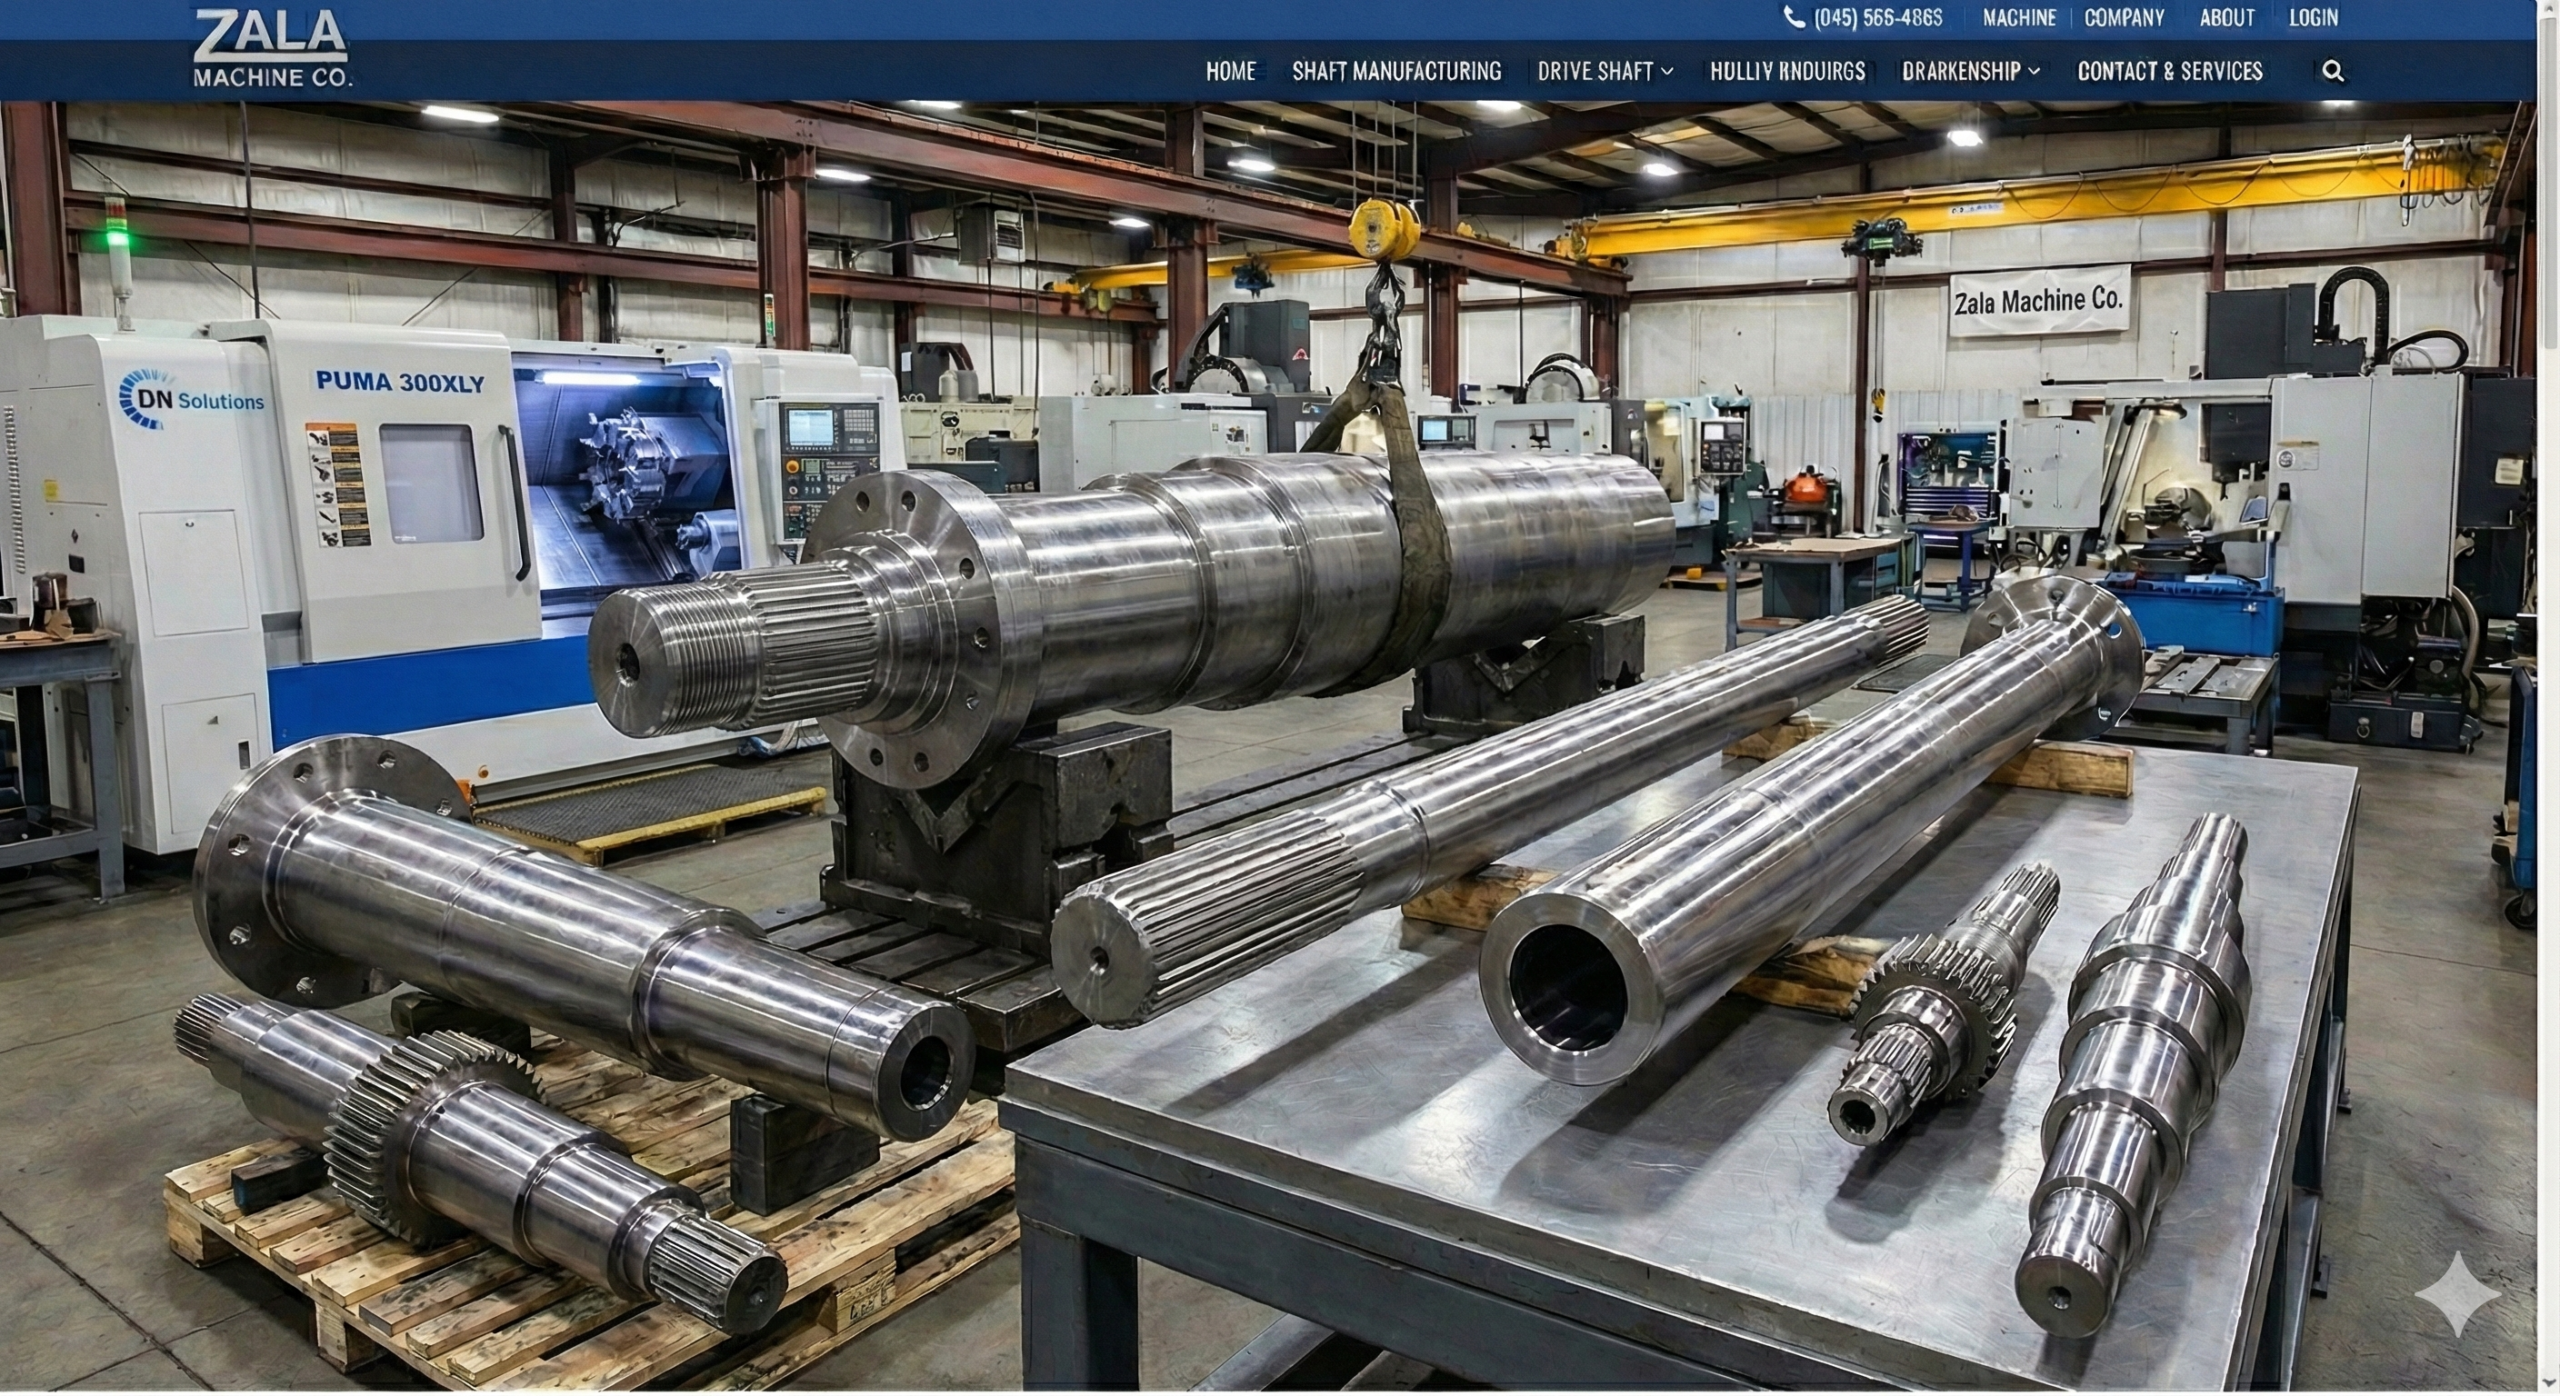
Flanged, splined and hollow-bore shafts.
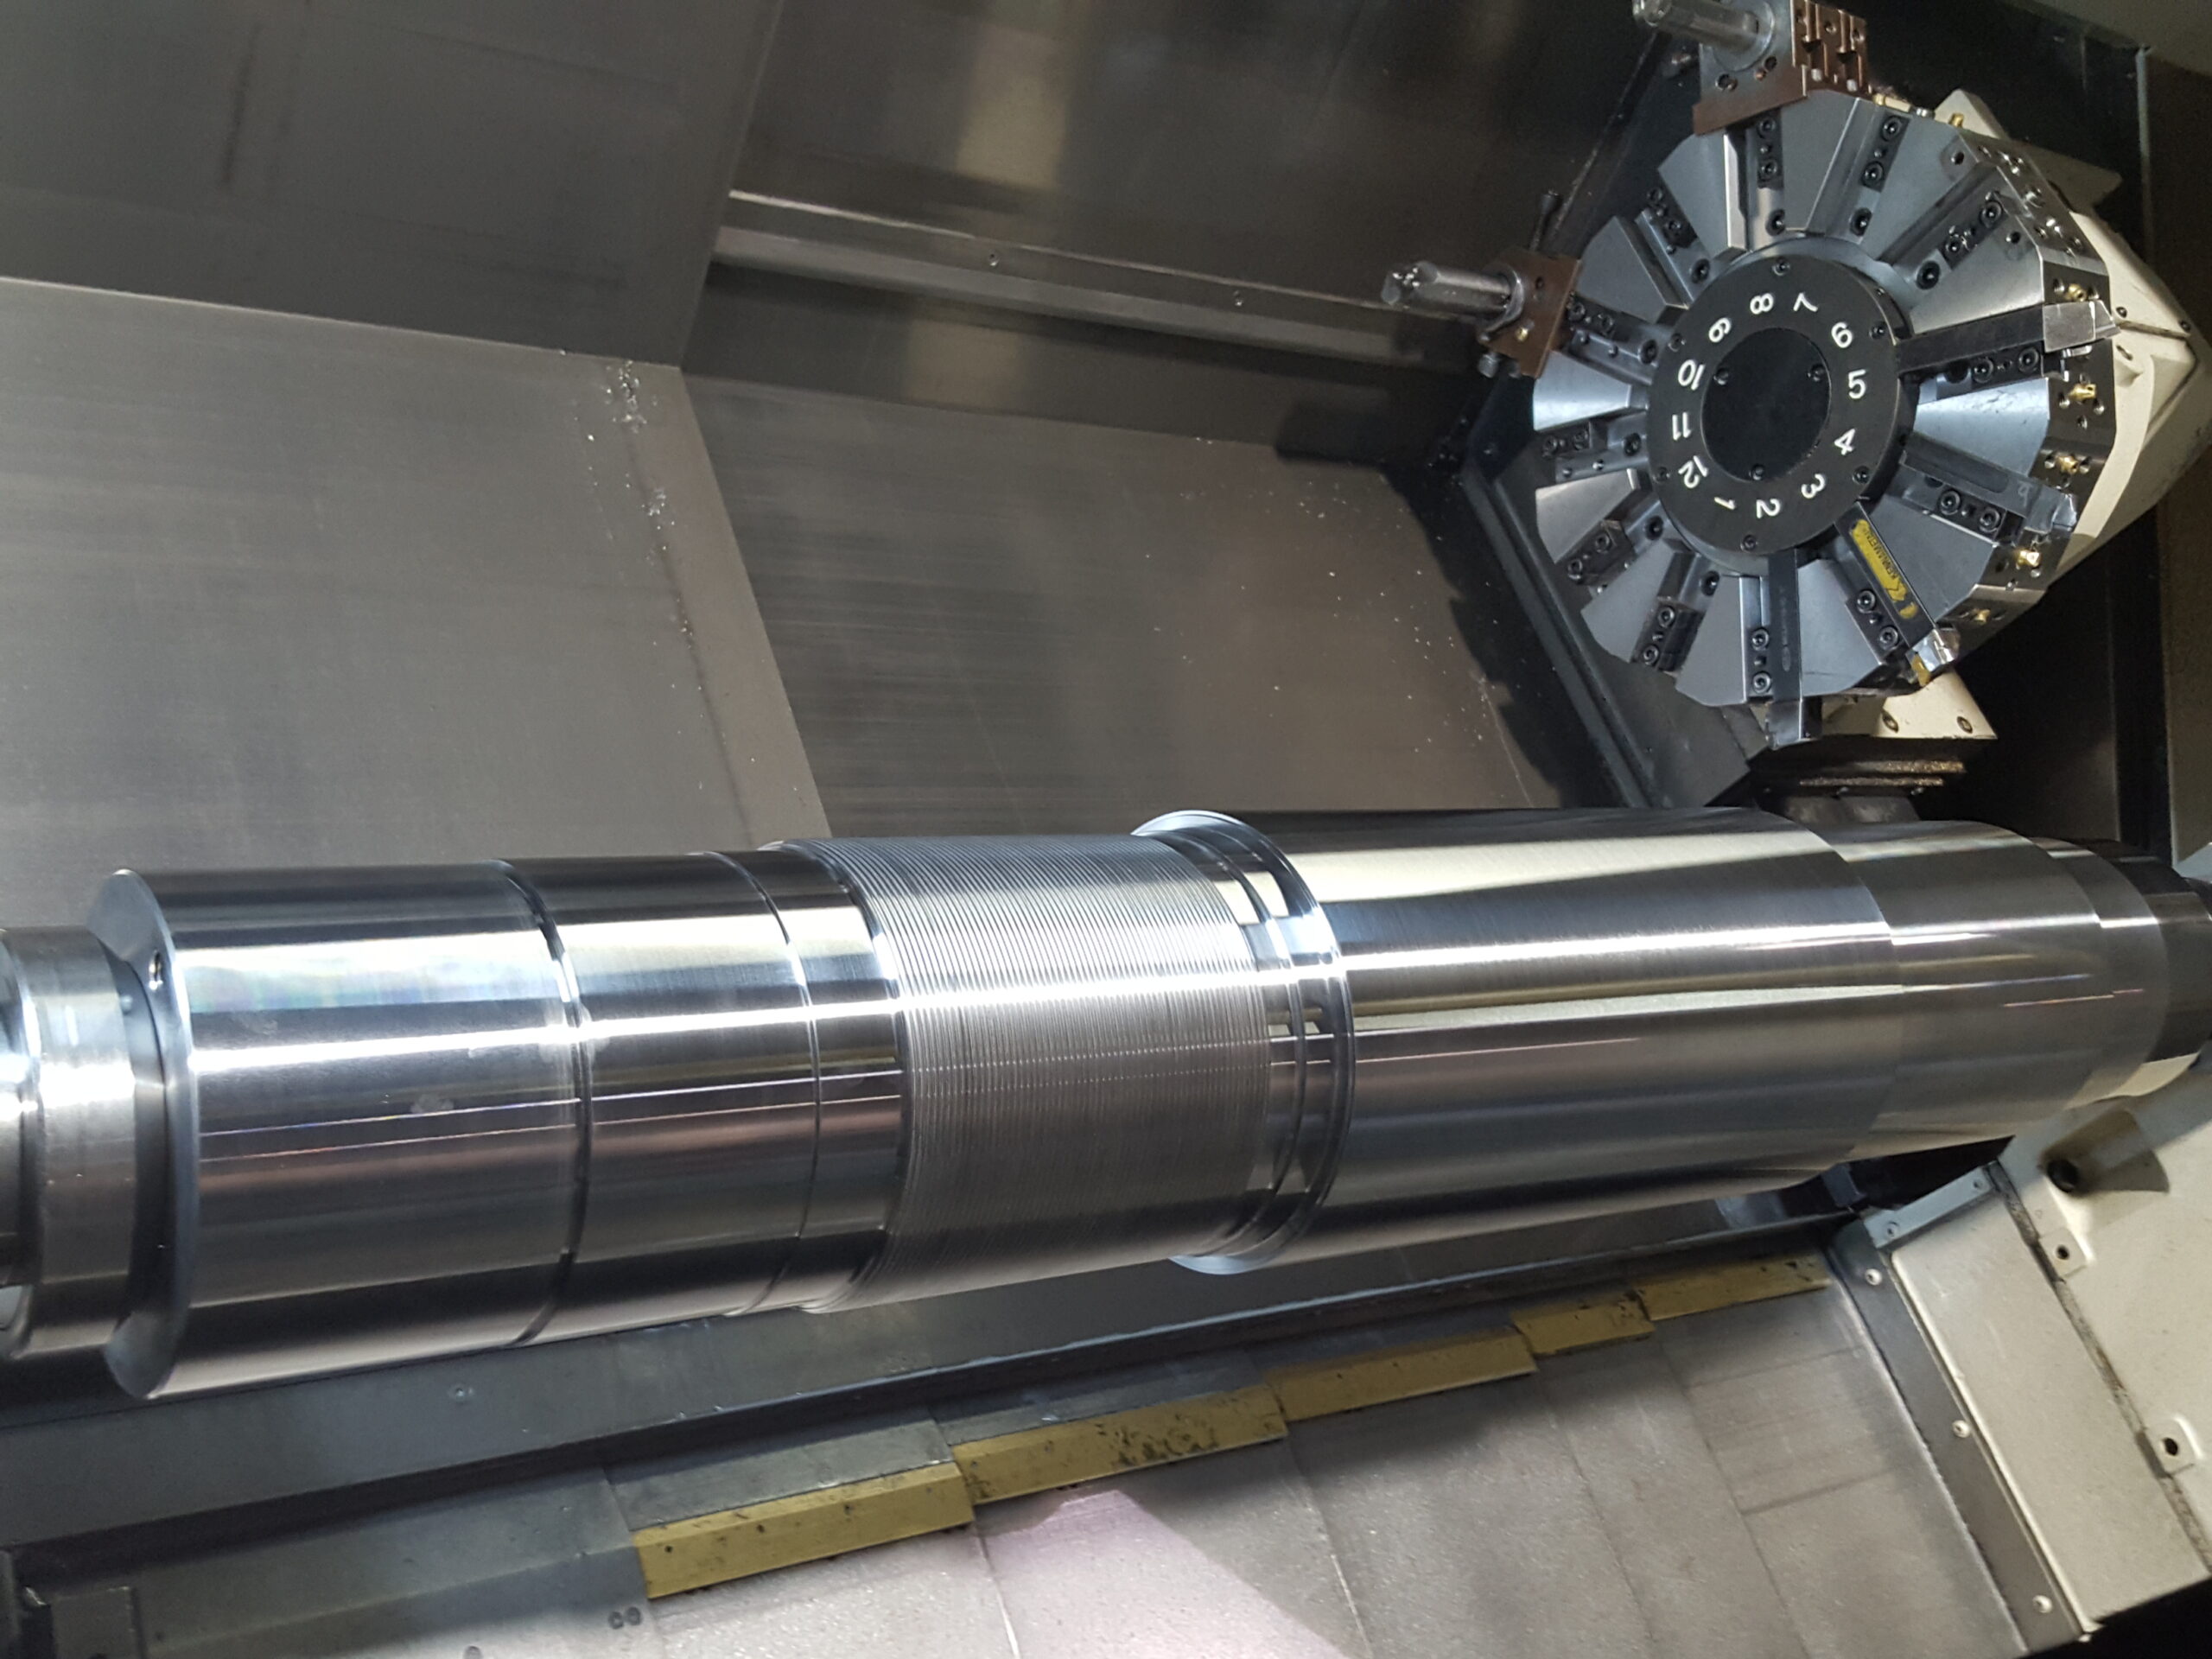
Long splined drive shaft after CNC turning.
Four kinds of shaft make up most of the work. Each can be made to your print or measured off the old part.
Shafts for single and twin-screw extruders, held to tight tolerances on length, diameter and straightness for torque transfer and alignment. We reverse engineer and machine new splined, geared, drive and thrust shafts for the gearboxes that come through our gearbox repair work.
Engineered for heavy industrial use, our drive shafts are machined to handle high rotational loads with minimal vibration.
Internal and external splines and keyways machined here, on the Mori Seiki NTX2000. For geared shafts we machine the blank and our gear-cutting partner cuts the teeth.
Shafts with deep-hole bores for coolant passages, weight reduction or internal components. Gundrilling and honing are both in house, so a through-bored shaft stays in one building from bar to finished part.
CNC turning to 28″ diameter on the Okuma LB4000EX and to 83″ long on the Doosan Puma 300XLY, with manual turning between centres to 170″ on the Poreba.
CNC milling and 5-axis milling for keyways, splines, flats, cross holes and complex shaft ends.
Gundrilling and honing for through bores and finished IDs.
Grinding on bearing seats and seal diameters. All of it in house.
4140 HT, 15-5 PH and other stainless steels, Inconel 718, titanium and bronze, among others. Material test reports are supplied on request, and you can supply the bar yourself if you prefer.
Heat treating, nitriding and plating go to our outside vendors. The shaft comes back here to be finished and inspected.
Every shaft is checked before it ships, by hand and on our Keyence XM-5000 portable CMM.
On CNC we turn to 28″ diameter by 60″ long on the Okuma LB4000EX, and to 14″ diameter by 83″ long on the Doosan Puma 300XLY, which is our longest CNC lathe. On the manual machines we go to 32″ diameter by 170″ between centres, and to 60″ diameter on the vertical turret lathes. Deep-hole work runs to 4″ diameter and 96″ deep.
Grinding to 14″ × 60″. The full machine list is on our facility list.
On CNC we turn to 28″ diameter by 60″ long on the Okuma LB4000EX, and to 14″ diameter by 83″ long on the Doosan Puma 300XLY, which is our longest CNC lathe. On the manual machines we go to 32″ diameter by 170″ between centres, and to 60″ diameter on the vertical turret lathes. Deep-hole work runs to 4″ diameter and 96″ deep.
Most of what leaves this shop is made to a customer’s print. Send a PDF, DWG, DXF, IGES or STEP file with quantities and we come back with a price and a lead time. There is no minimum order, and production runs go into the thousands.
One-off and prototype shafts are welcome too. See our research and prototype machining page.
Yes. Bring us the worn or broken one. We measure every feature by hand and on a Keyence XM-5000 portable CMM, work out the correct dimension rather than copying the wear, and machine the new shaft from that.
4140 HT, 15-5 PH and other stainless steels, Inconel 718, titanium and bronze, among others. Material test reports are supplied on request, and you can supply the bar yourself if you prefer.
Shaft grinding is done in house, on every precision diameter, for surface finish and for the fits that matter. Finish is verified on a profilometer.
Splines and keyways are machined here, on the Mori Seiki NTX2000 five-axis mill-turn, and we are taking on more of that work. Gear teeth are cut by our gear-cutting partner from blanks we machine — bore, keyways and journals — with the schedule for the whole job held by us.
Yes. Gundrilling to 4″ diameter and 96″ deep for coolant passages, weight reduction or internal components, honed afterwards where the bore finish matters. Both are in house.
It depends on the shaft and the material. Most emergency work is finished in one to two days, and our fastest was a stainless replacement shaft in two hours with the customer’s driver waiting at the shop. Scheduled work is quoted with a date we are confident we can meet.
Yes. Pump shafts, high-volume blower and fan shafts, mixer and agitator shafts, and ball mill pinion and drive shafts are all shaft work, and shaft work is what this shop does most. Send the print, or the old shaft if there is no print, and tell us what it drives.
Shafts are part of most jobs in this shop. These pages cover the work around them.
When the success of your equipment depends on the integrity of a single shaft, precision is the only option. A machinist here will review your drawing and come back to you on material, method and lead time. If a shaft has already failed and the line is down, say so when you send it — emergency machining runs on an expedited schedule.
Call the shop or email sales@zalamachine.com, or use the quote form below.