Home / CNC Milling

Most of the milling in this shop is one of two things: a part that has to come off the machine right the first time, or a part that is too big for a lot of shops to hold. We run three vertical machining centres in Hillsborough, New Jersey, and the largest gives 157″ of travel in X — a mill that will take a weldment or a base plate other job shops turn down.
Vertical milling is the core of it, 3-axis and 4-axis, in steel, stainless, aluminium, 4140, titanium and Inconel. Tolerances under .001″ are standard work and we hold ±.0005″ where the print calls for it. Single replacement parts, small batches and production runs all run through the same department.
| Zayer horizontal / vertical | 157″ × 40″ × 70″ travel — our largest milling envelope |
| Okuma Millac VMC | 60″ × 30″ × 30″ travel, with 4th axis |
| Okuma Genos 560V | 40″ × 20″ × 20″ travel, full 4-axis |
| Part size | from 2″ up to 157″ long |
| Tolerance | under .001″ as standard, ±.0005″ where the print calls for it |
| Materials | aluminium, 300 and 400 series stainless, 15-5 PH and 17-4 PH, 4140 and 4340, titanium, Inconel, industrial plastics |
| Lifting | to 10 tons |
| Finishing in house | bore honing, shaft grinding, welding and polishing |
A milled part behaves differently in every material, and most of what runs here is not aluminium.
Aluminium — brackets, housings and lightweight industrial parts, cut fast and held flat.
Stainless — 300 and 400 series, plus 15-5 PH and 17-4 PH, for food, pharmaceutical and marine work.
Alloy steel — 4140 and 4340, including hard milling after heat treat where the part has to stay dimensionally stable.
Titanium and Inconel — rigid setups and the right feeds, for the parts that punish tooling.
Industrial plastics — polymer extrusion components, insulators and custom bushings.
Milling is rarely the whole job. A milled part usually needs a bore honed, a journal ground, a weldment finished or a shaft turned, and all of that happens in the same building. The part does not travel between shops and it does not lose its reference between operations.
That matters most on repair and replacement work. When a gearbox housing needs a new bearing bore, or the OEM quotes months on a plate that is holding up a line, we machine it here from steel we already have on the floor. Every part is checked against the print before it ships — Keyence portable CMM, micrometers, bore gauges and depth mics.
Milled parts leave Hillsborough for plants right across the state — Bridgewater, Somerville, Flemington, Edison, Piscataway and Trenton, and the industrial corridor through Newark, Elizabeth, Jersey City and Paterson — as well as eastern Pennsylvania, New York and New England. Customers in Somerset, Hunterdon, Middlesex and Mercer counties regularly drop parts off and collect them by hand. Further out, parts go by truck across the United States, Canada and Mexico.
Prototype, one-off replacement, small batch or production run — the same machines and the same inspection. Tell us the quantity with the drawing and we will quote it.
Travel x-40″, y-20″, z-20″.
A great fast machine capable of heavy-duty, precise milling in all materials, with full 4-axis capabilities.
Travel x-60″, y-30″, z-30″, with 4th axis.
Great for Complex Precise Milling.
Travel x-157″, y-40″, z-70″.
Large Precision CNC Milling.
From 2″ up to 157″ long. The Zayer gives 157″ × 40″ × 70″ of travel, the Okuma Millac 60″ × 30″ × 30″ with a 4th axis, and the Genos 560V 40″ × 20″ × 20″. We lift to 10 tons, so a large weldment or base plate is no obstacle.
Under .001″ is standard work, and we hold ±.0005″ where the print calls for it. Every part is checked against the drawing before it ships — Keyence portable CMM, micrometers, bore gauges and depth mics.
Yes. The Genos 560V runs full 4-axis and the Millac has a 4th axis, which is what lets us machine features around the circumference of a part — off-centre drilling, slotting and milling on shafts and cylindrical work. For simultaneous 5-axis work, see our 5-axis milling page.
Aluminium, 300 and 400 series stainless, 15-5 PH and 17-4 PH, 4140 and 4340 alloy steel including hard milling after heat treat, titanium, Inconel, and industrial plastics.
No. We mill single replacement parts and one-off prototypes as well as production runs. Tell us the quantity with the drawing and we will quote it.
Yes, and most parts need it. Bore honing, shaft grinding, welding and polishing all happen in this building, so the part is not shipped between shops between operations.
Yes. We weld and then machine — frames, bases and large plates get their flats, bores and hole patterns cut after welding, so the finished faces run true rather than following wherever the weld pulled.
Hillsborough, New Jersey, in Somerset County — an easy drive from Bridgewater, Somerville, Flemington, Edison, Piscataway and Trenton, and from the corridor through Newark, Elizabeth, Jersey City and Paterson. Milled parts also go by truck across the United States, Canada and Mexico.

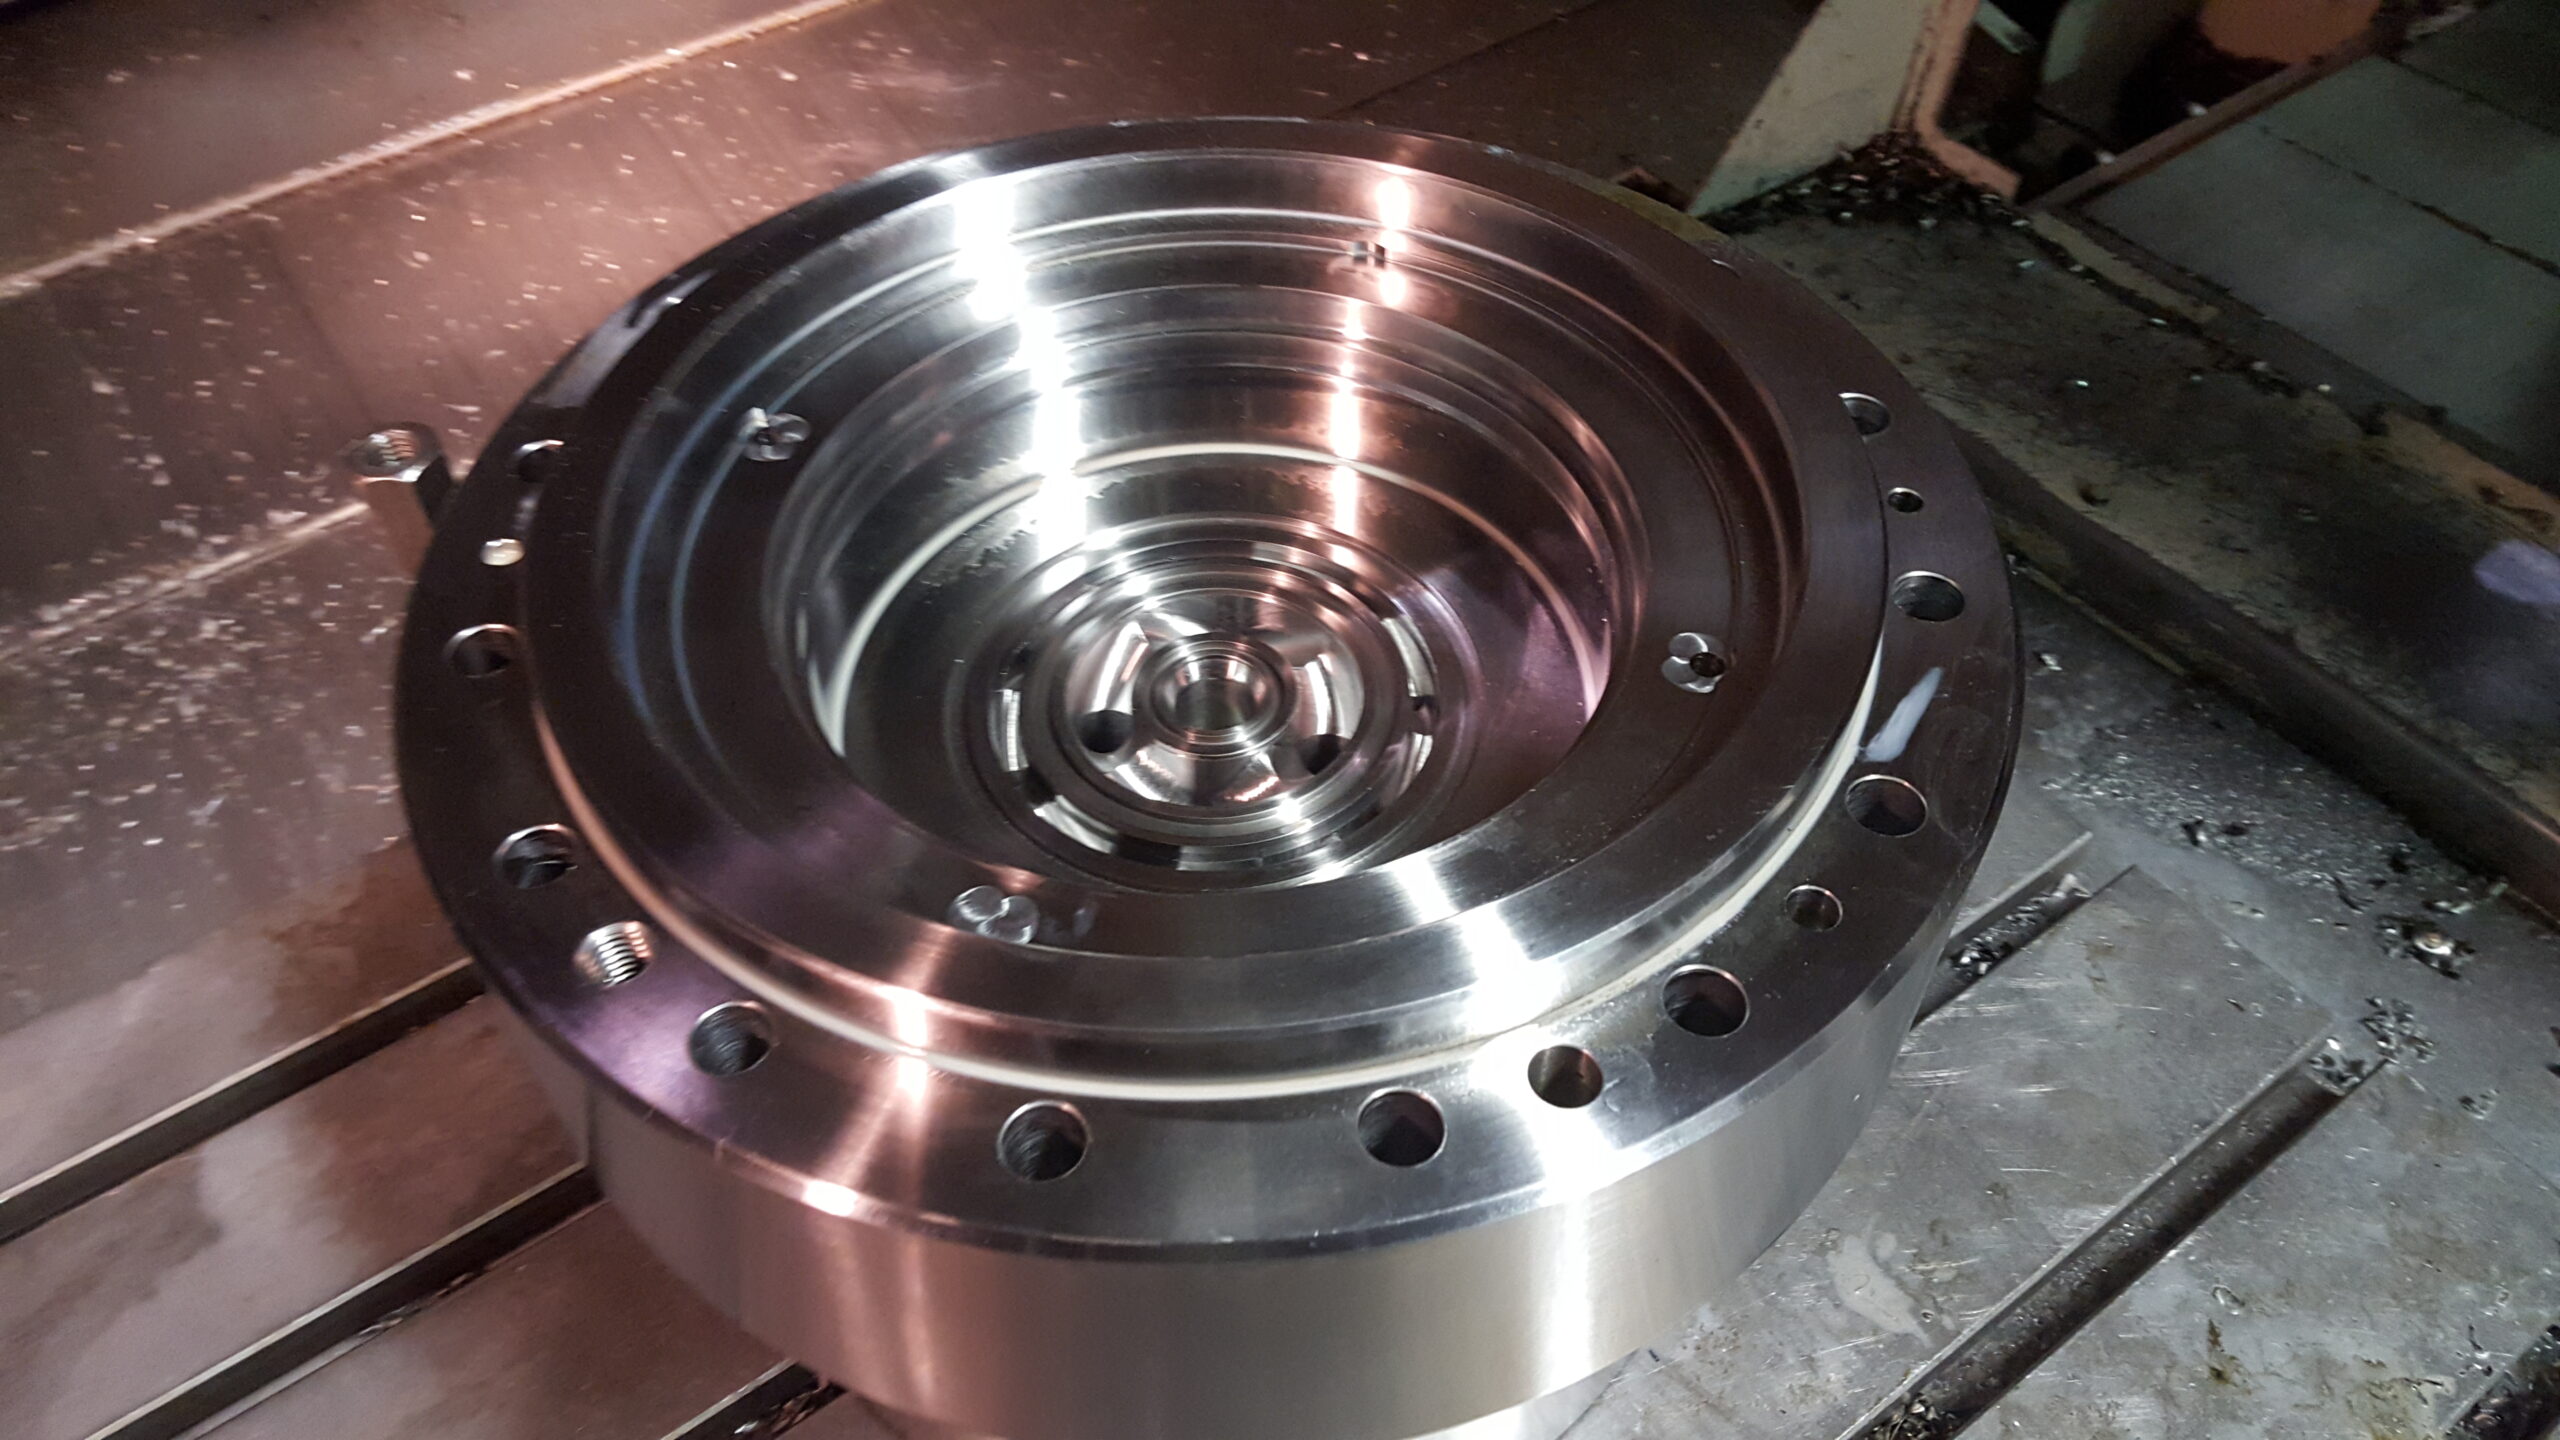
Travels to 157″ x 40″ x 70″ on the Zayer, 60″ x 30″ x 30″ with a 4th axis on the Okuma Millac, and 40″ x 20″ x 20″ on the Genos 560V. Manifold blocks, sealing faces, gear rings, bolted plates and weldment finishing, in steel, stainless, aluminium and Inconel.
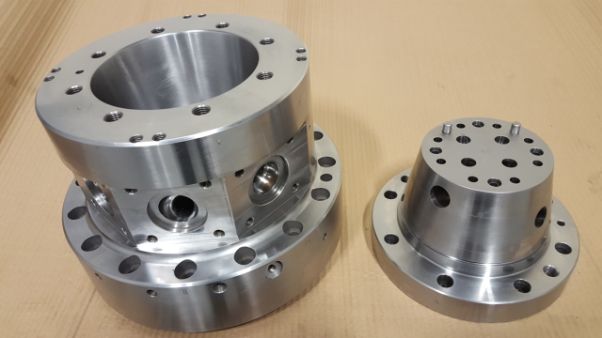
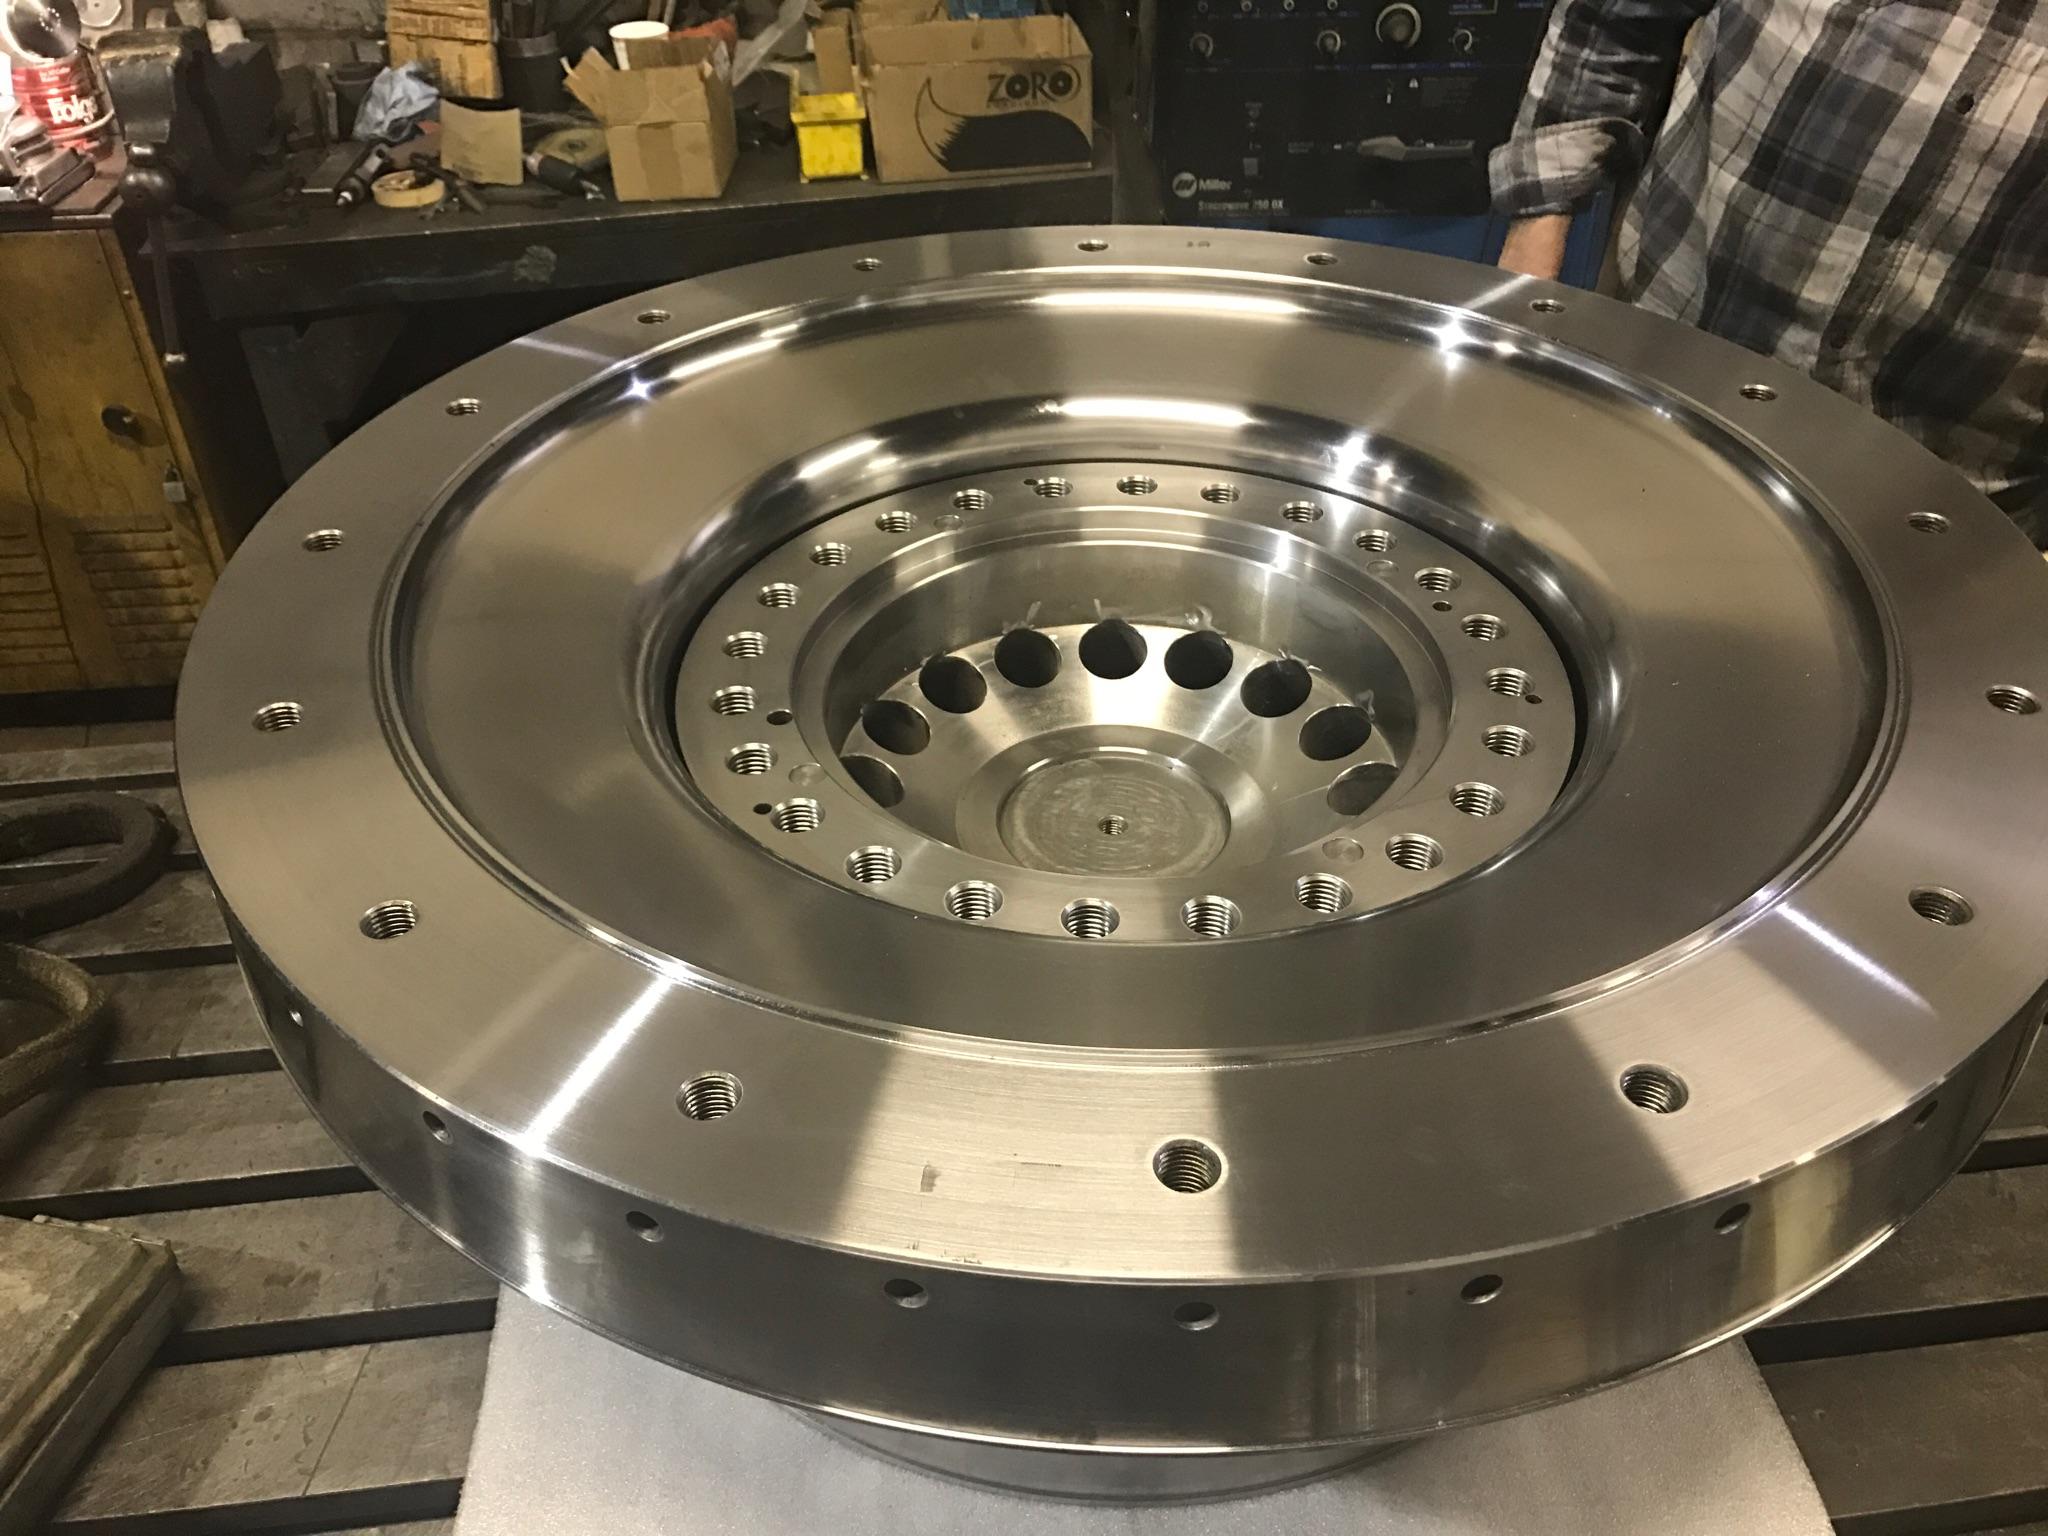
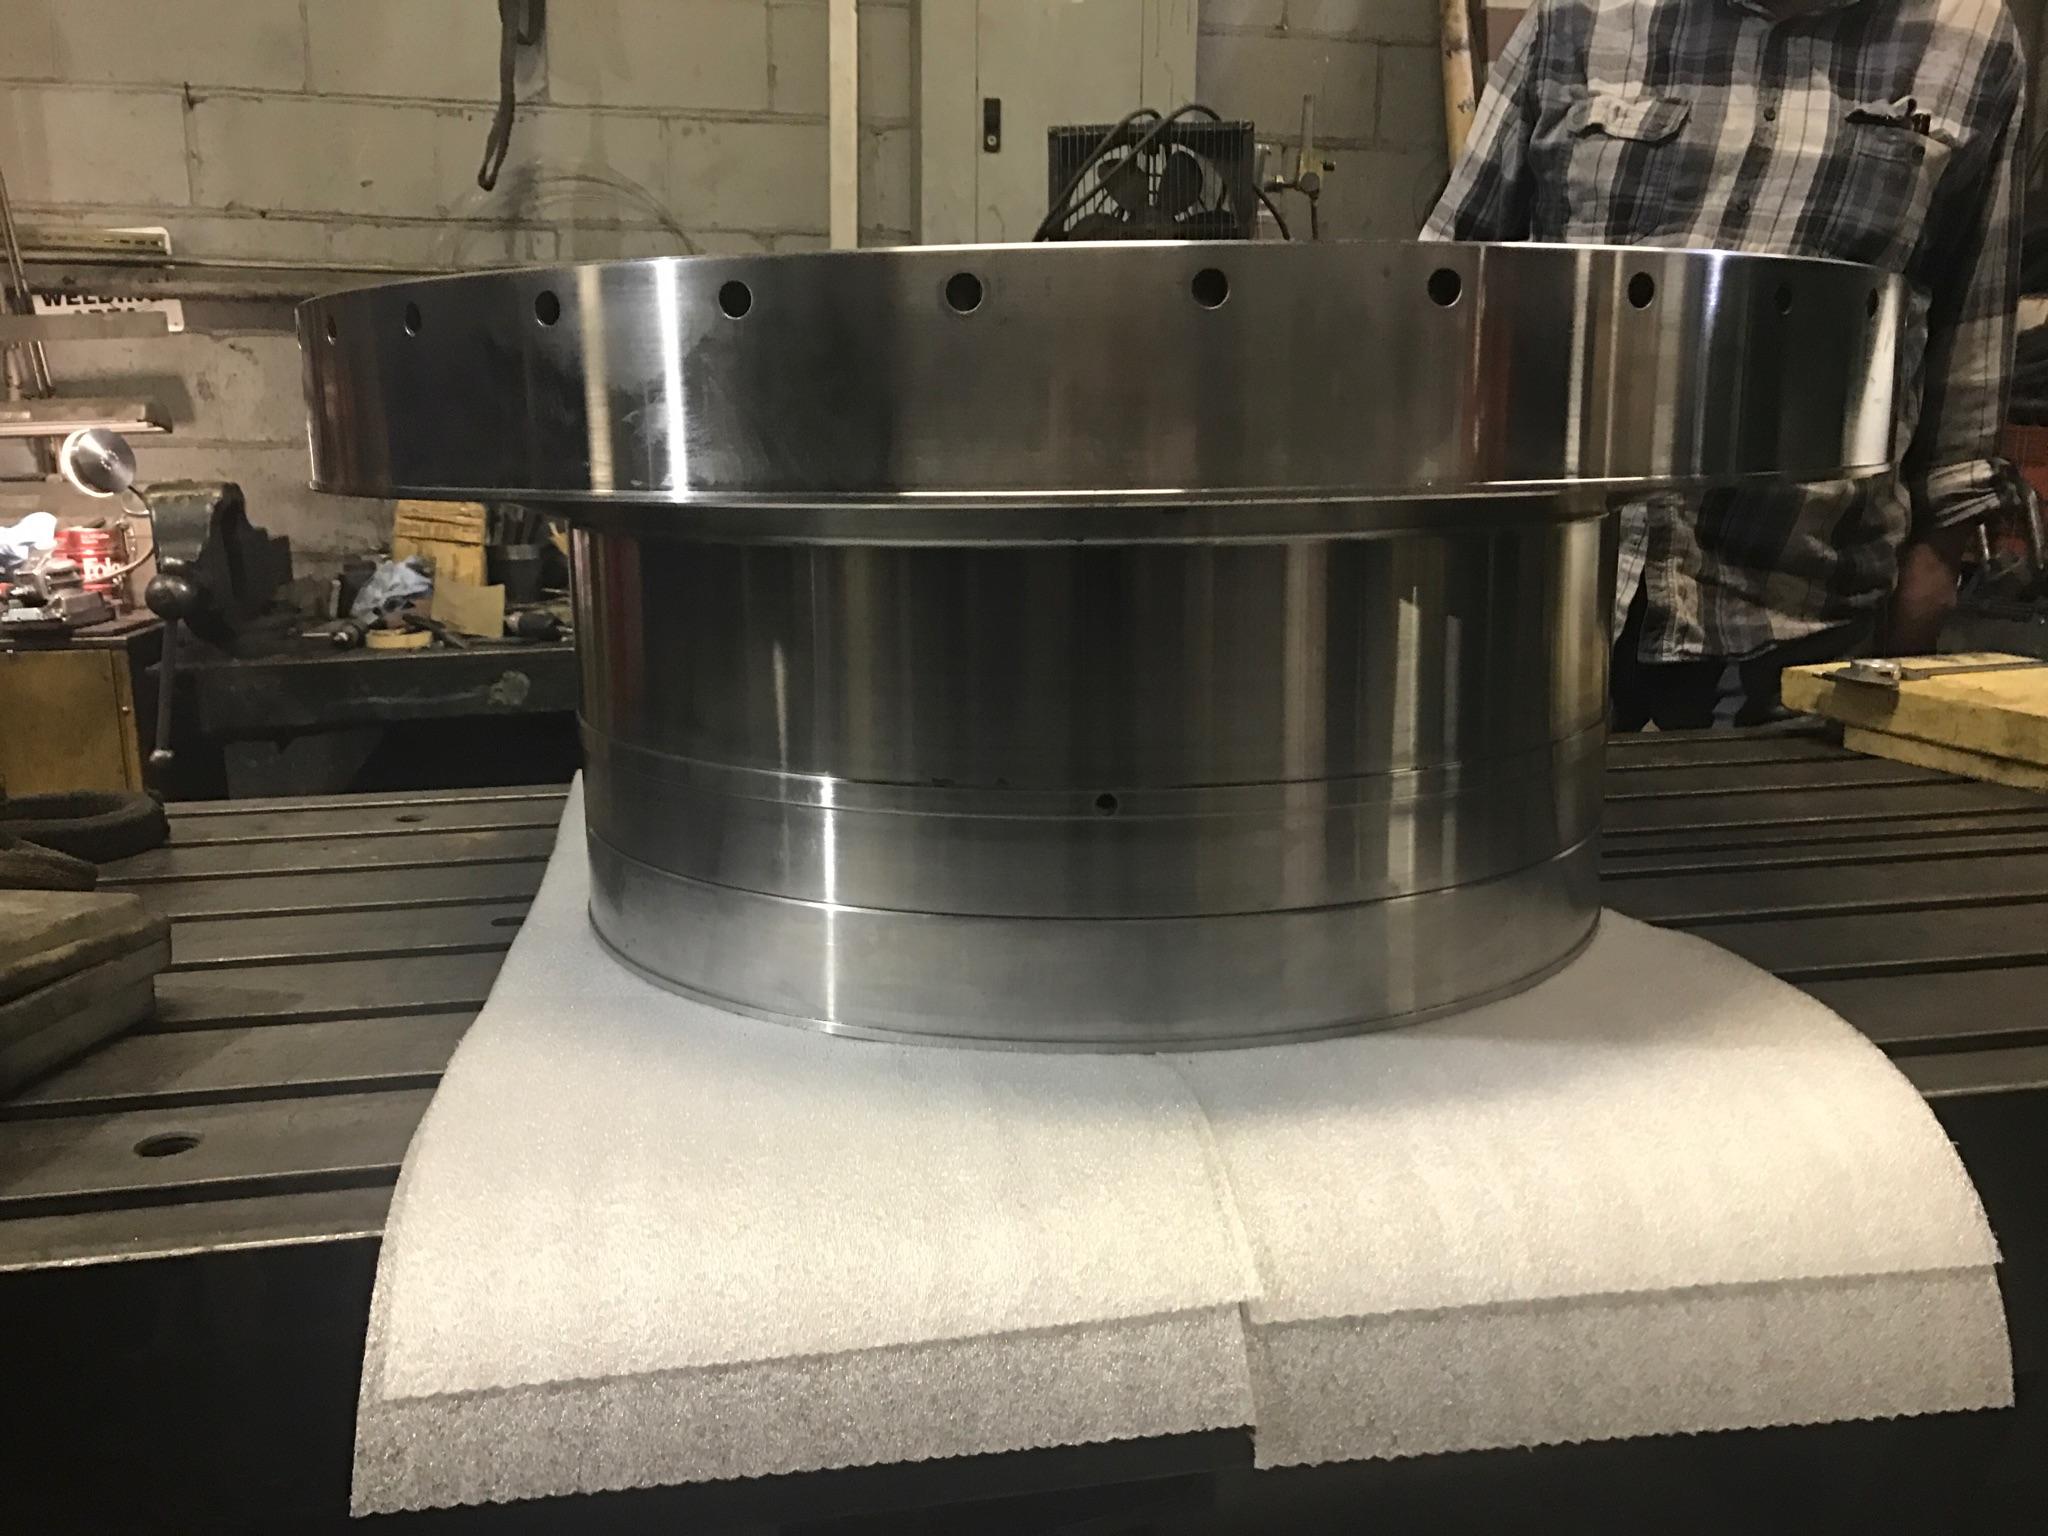
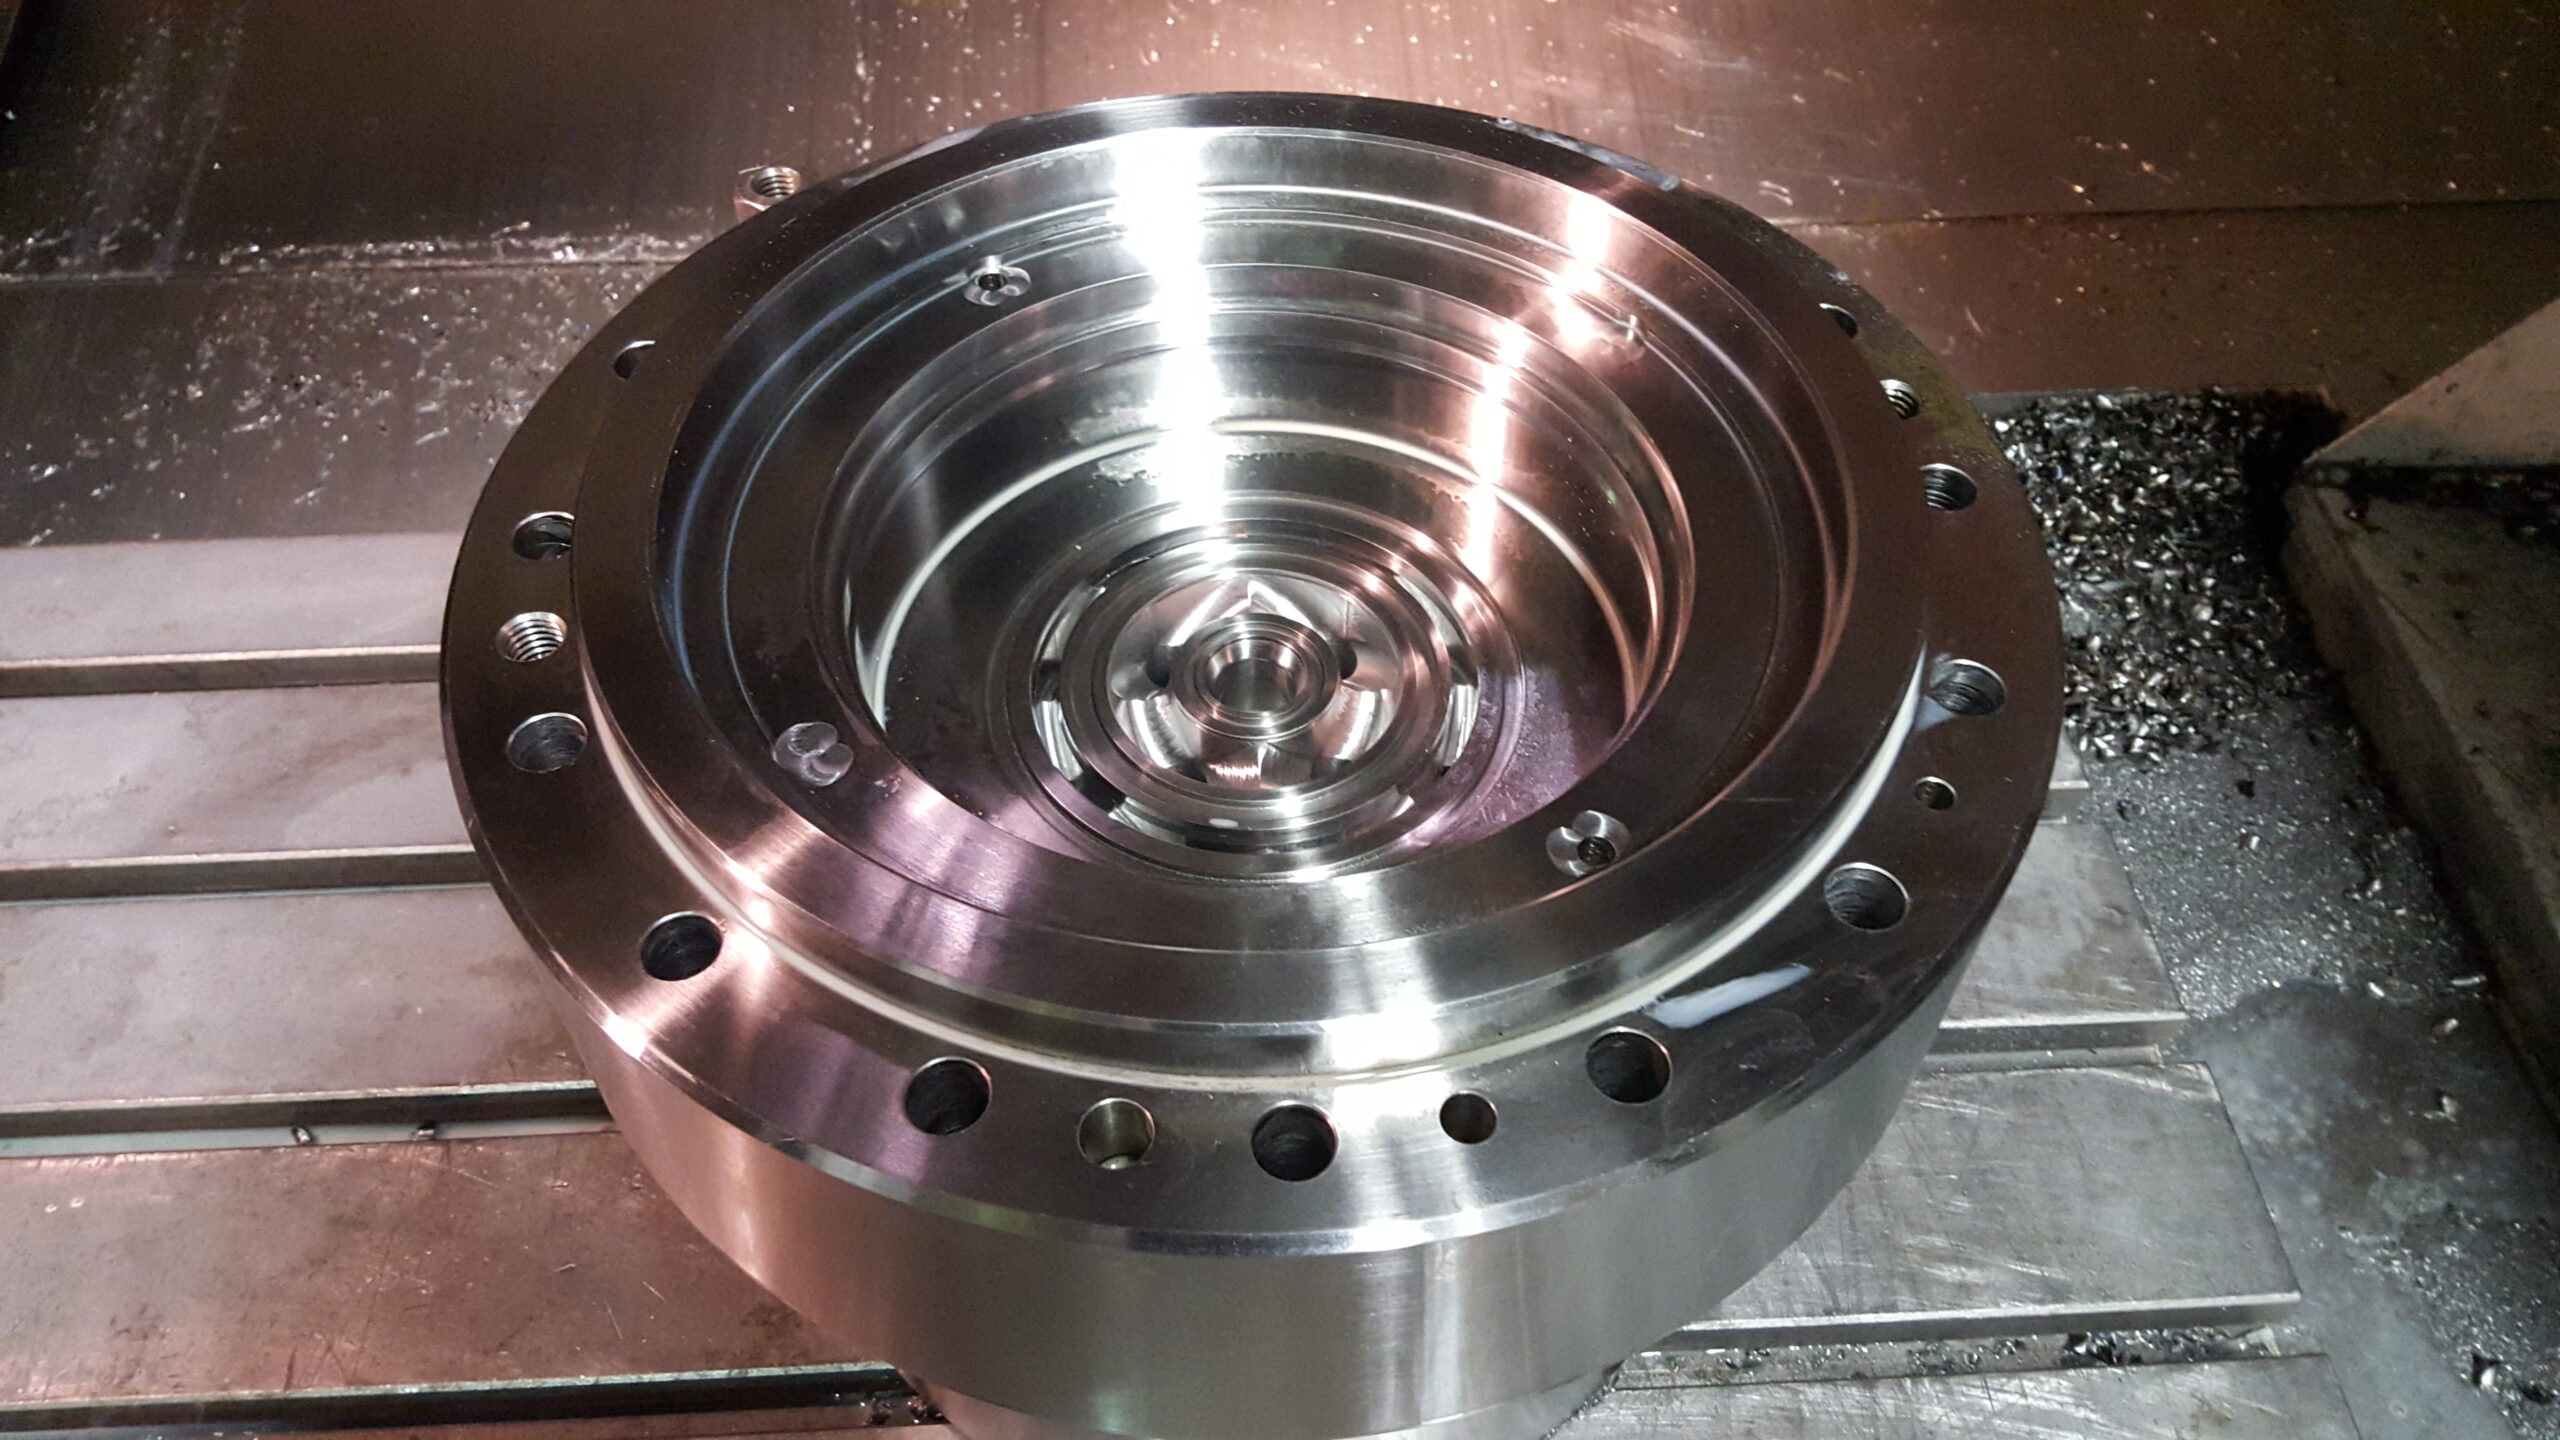
Milled components from our New Jersey machine shop — manifold blocks, sealing faces, gear rings and large bolted plates cut on our vertical and 4-axis machining centres.