
Research & prototype machining
Home / Research & Prototype Machining
Our research and prototype machining serves university labs, research laboratories, fusion research groups and R&D teams with parts that don’t fit a catalog. We build one-offs, prototypes and test assemblies to your print, and you work directly with the machinists making your part.
Research work is rarely routine. The quantity is small, the material is unusual and the tolerances matter. That is the kind of work we like.
We have built camera cage assemblies from Invar for a university research group. We have machined magnetic test assemblies for fusion laboratories. We have produced solid copper rails for a company developing fusion energy. We have also completed smaller projects for other universities and research labs.
Most of these jobs started as a drawing and a phone call. Some started as a sketch. We work through the details with you before we cut metal.
Many research shops cannot handle large or heavy components. We turn parts up to 60″ in diameter and 170″ long. We mill up to 157″ and lift up to 10 tons. The same machinists handle a palm-sized fixture and a long copper rail.
There is no sales desk between you and the person making your part. Questions about material, critical features and how the part will be used are settled before we cut metal, so the first part comes off right. If the design changes partway through, you tell the machinist directly.
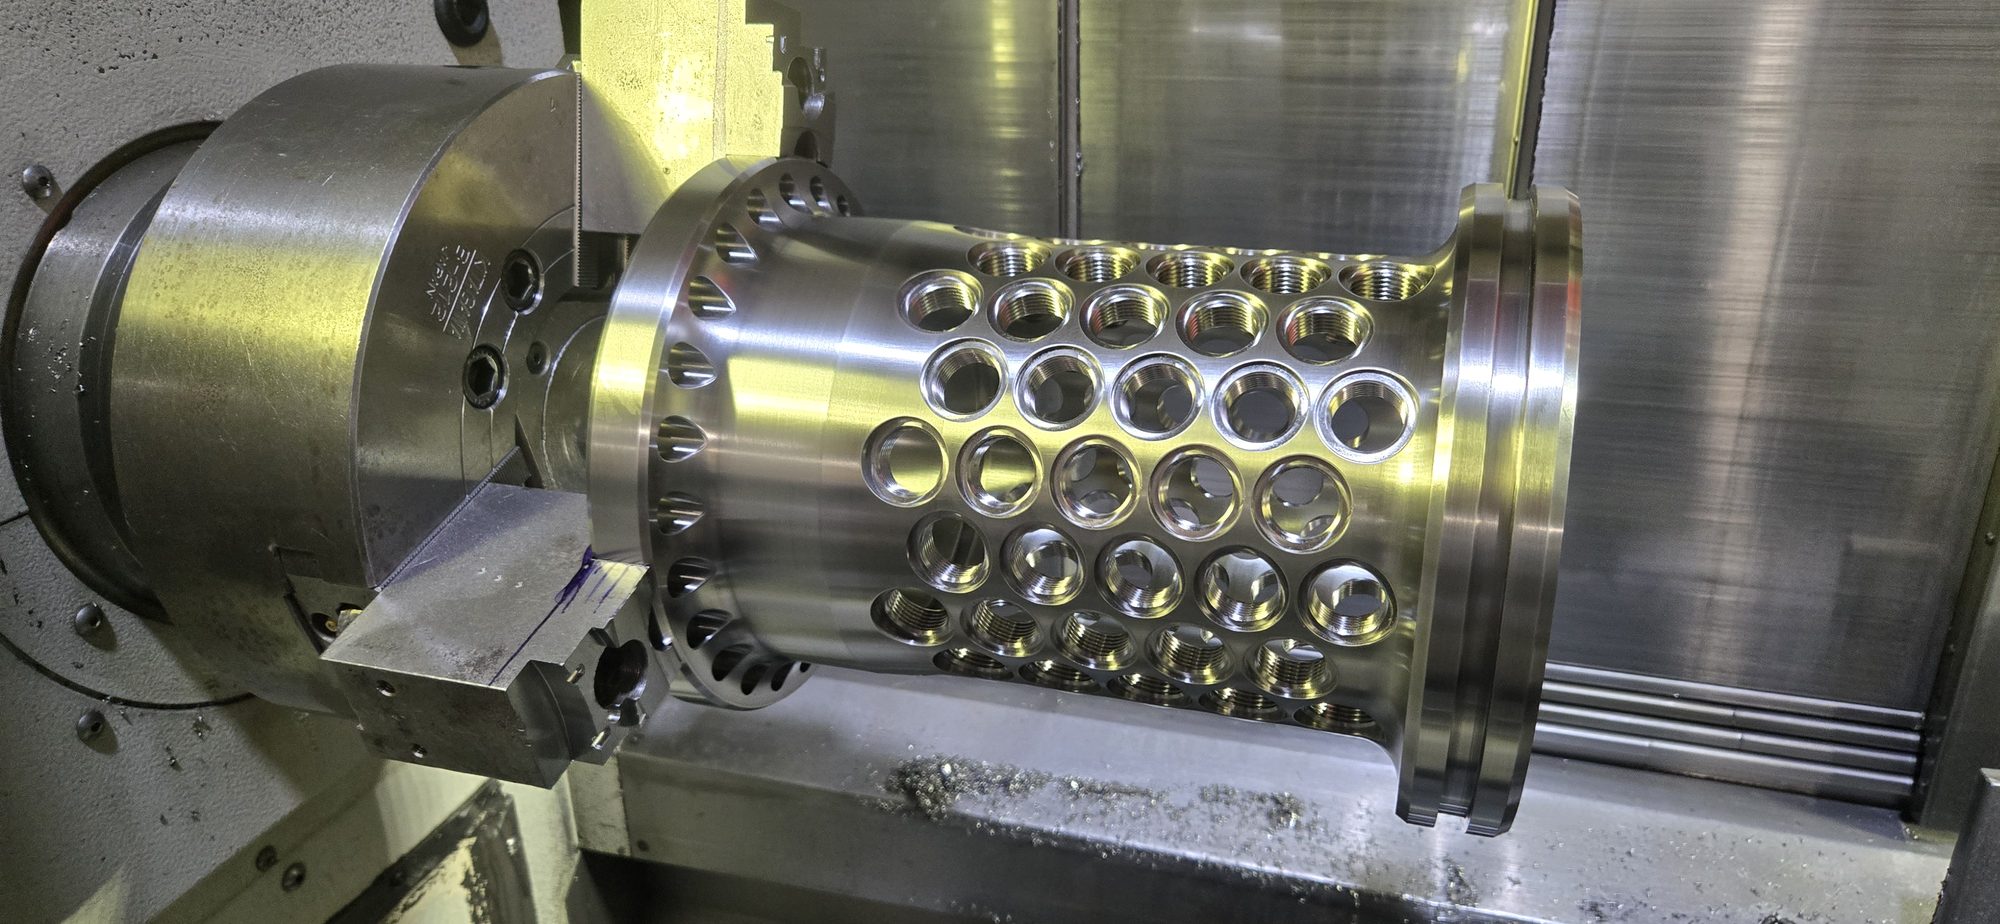
Titanium prototype cylinder in the CNC lathe, rows of radial holes drilled through the wall.

A long shaft carried in the steady rest to hold it true over its length.
One-off parts machined in Hillsborough, New Jersey. More photos and videos are in our gallery.
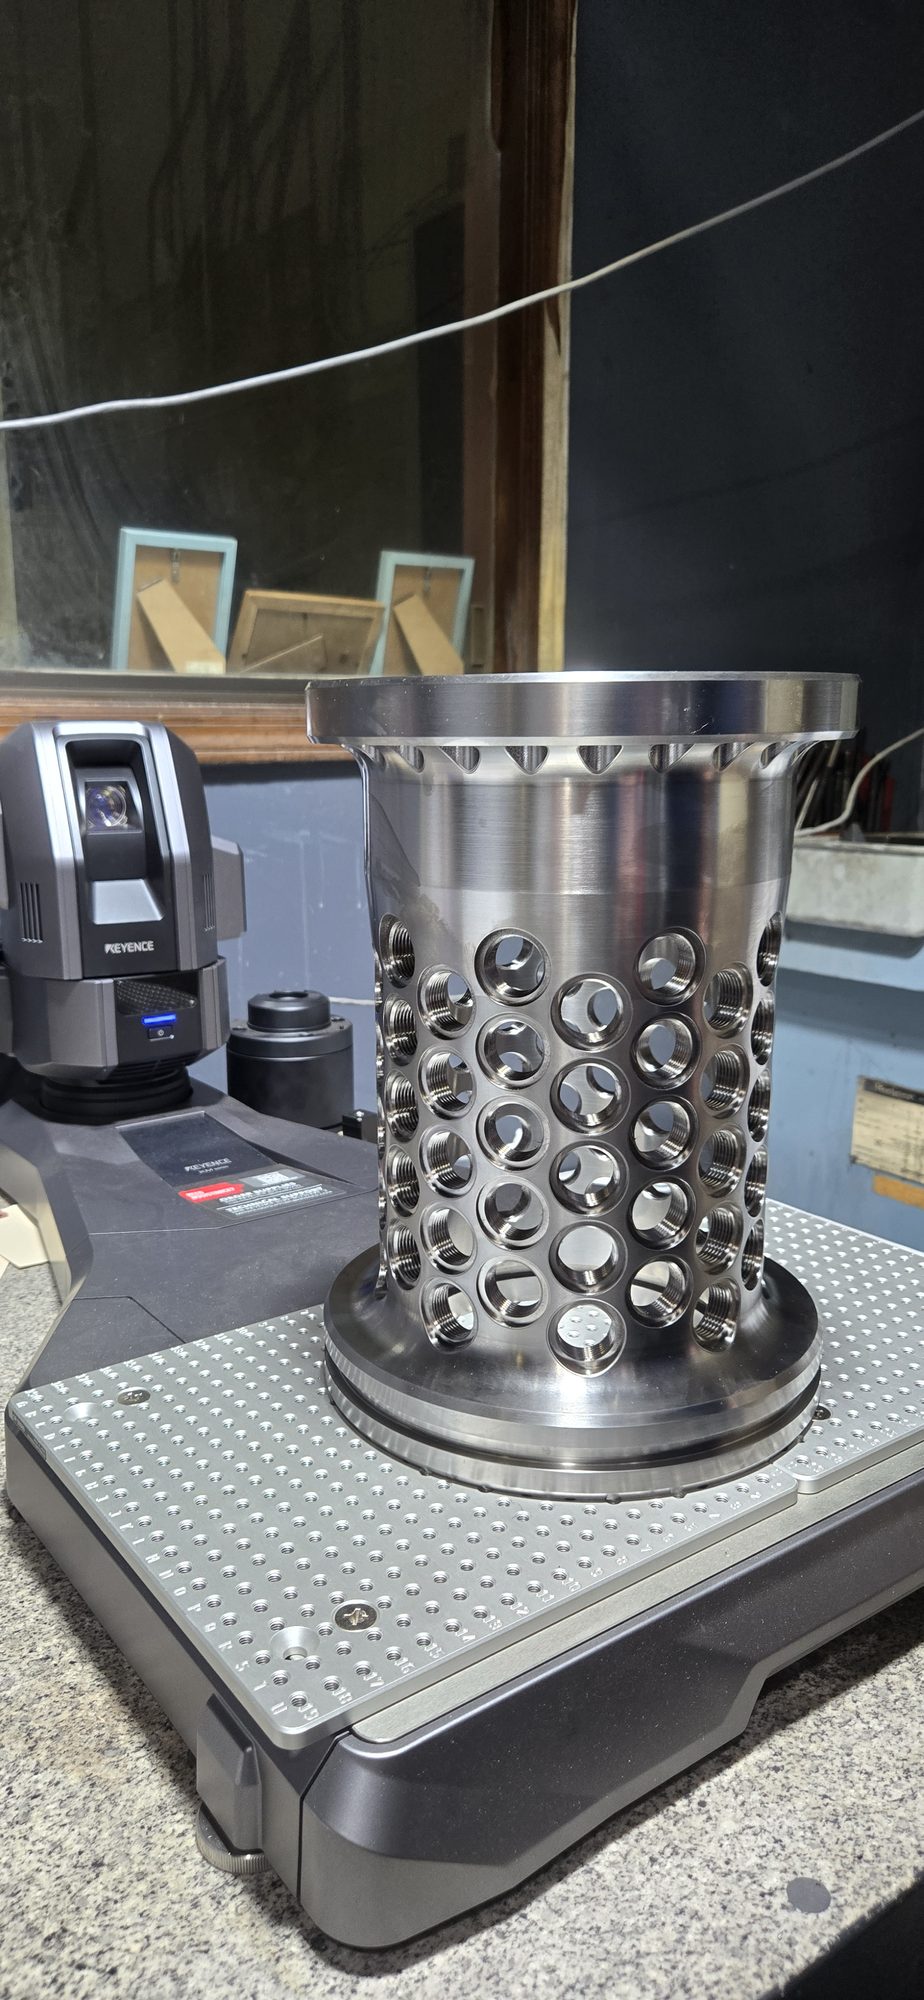
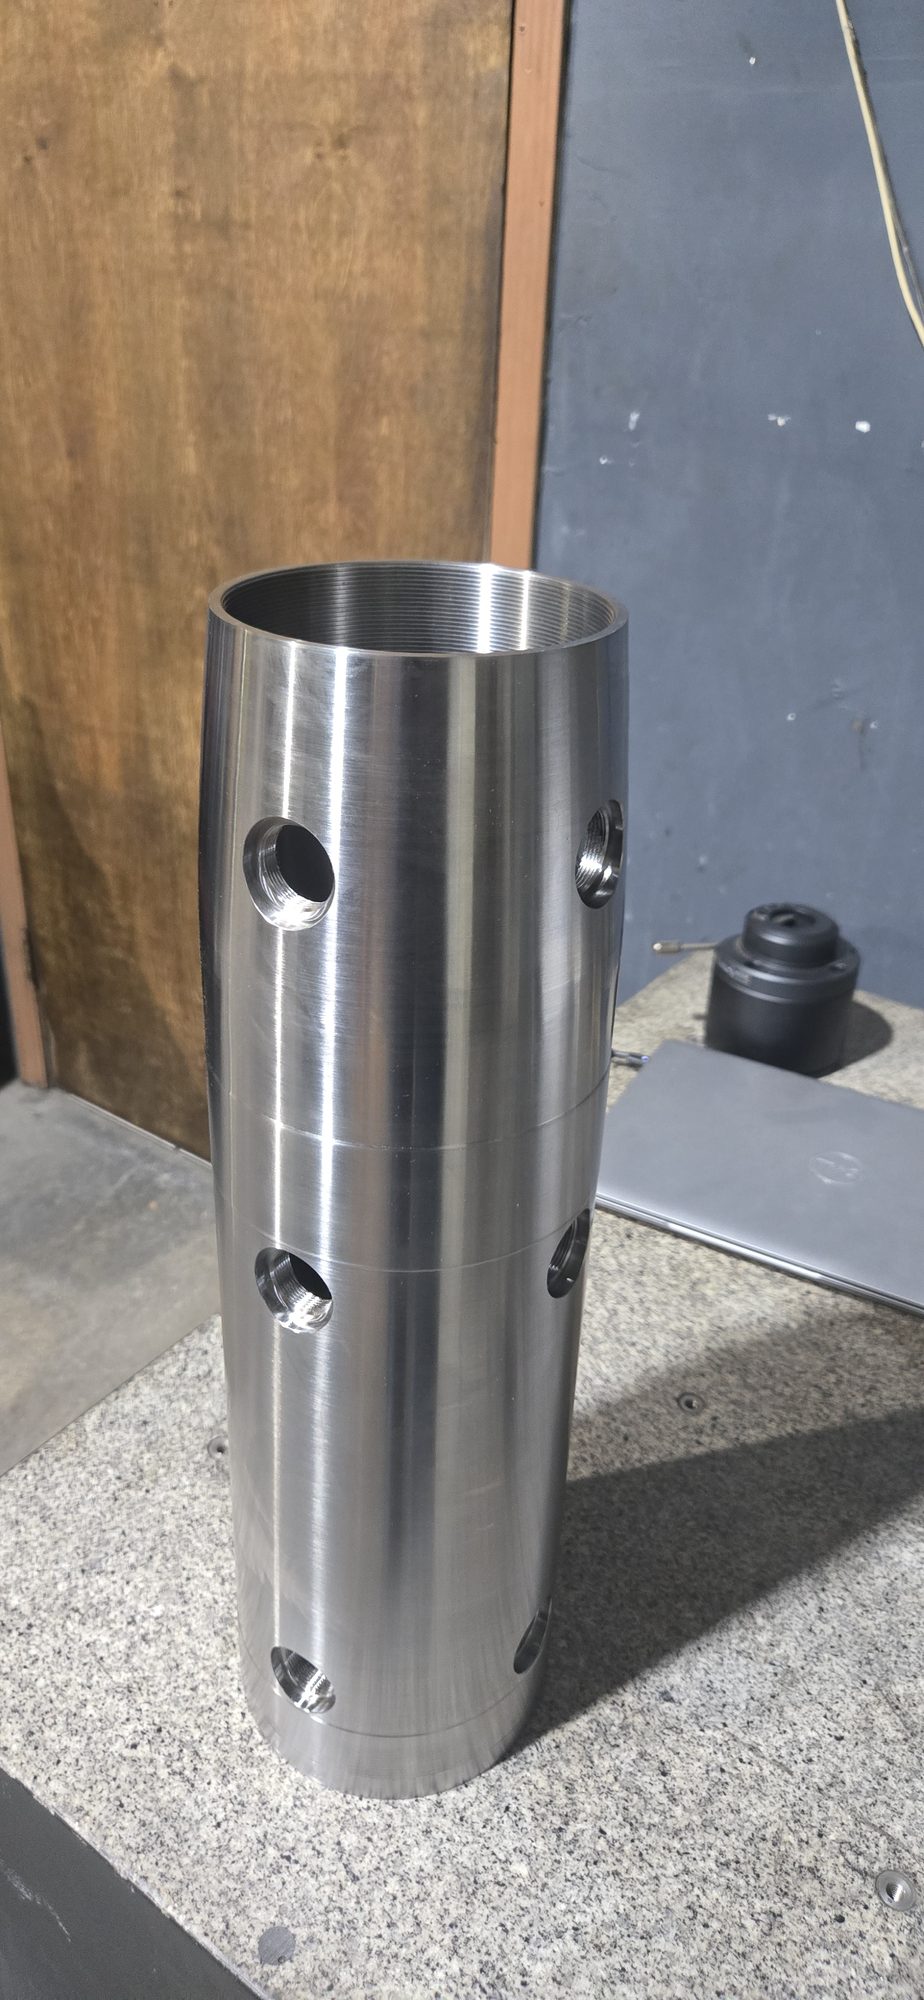
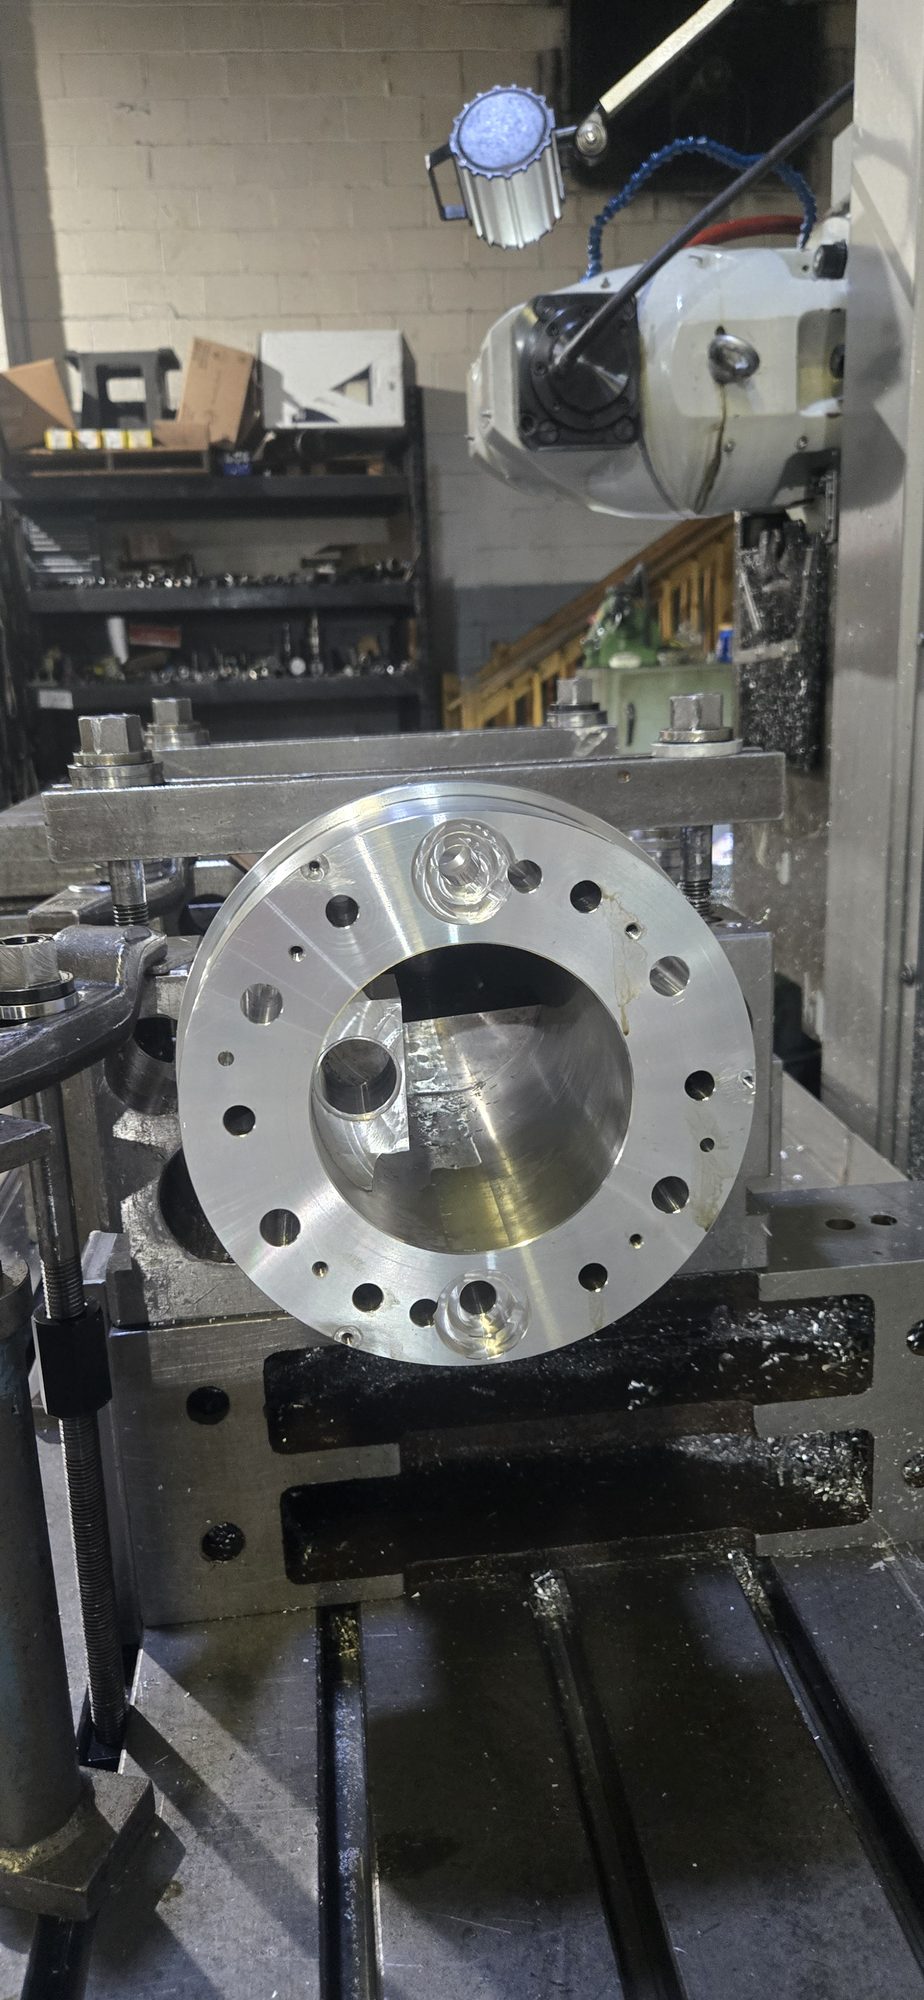
Five steps from a drawing or a sketch to a part on your bench.
A STEP file, a PDF or a hand sketch is a fine place to start.
We ask about material, critical features and how the part will be used.
You get a clear price and lead time. Purchase orders are welcome.
Critical dimensions are checked before the part ships.
Parts go out by freight or courier, or you can pick them up in Hillsborough.
Research parts are often made from materials that fight back. We machine the full range, and we will tell you plainly if a material or a feature needs a different approach.
Invar and specialty alloys. Invar is chosen for its low thermal expansion. It is tough and gummy to cut, and it work-hardens quickly, so holding size takes the right tooling and patience.
Copper, brass and bronze. Copper is soft and prone to burrs. Keeping it flat, clean and true over long lengths takes care at every setup. Brass and bronze go into bushings, wear parts and fittings.
Stainless steels. 300 and 400 series, 15-5 PH and 17-4 PH, for clean and corrosive environments.
Carbon and alloy steels. 1018 and 1020, 4140, 4140 HT and 4340, including machining after heat treat. Tool steels as well.
Titanium and nickel alloys. Titanium and Inconel, with rigid setups and the right feeds for alloys that punish tooling.
Aluminum. Brackets, housings, fixtures and prototype blocks, cut fast and held to size.
Cast iron and plastics. Cast iron for bases and housings, and engineering plastics for insulators, fixtures and prototype parts.
Material certs are supplied on request. If your material is not on this list, call us and we will talk it through.
We accept purchase orders and university purchasing cards. We can provide a W-9 and complete your supplier registration.
We sign NDAs, and we don’t publish customer names or project details. Material certs and inspection reports come on request.
From a palm-sized fixture to a long copper rail.
| Quantities | one-offs, prototypes and small runs |
| Vertical turning | to 60″ diameter |
| Horizontal turning | 32″ × 170″ between centres |
| CNC turning | 28″ × 60″; 14″ × 83″ |
| 5-axis mill-turn | 24″ × 60″ |
| Milling | 157″ × 40″ × 70″ |
| Lifting | to 10 tons |
| Materials | Invar, copper, brass, bronze, 300 and 400 series stainless, 15-5 PH, 17-4 PH, carbon, alloy and tool steels (1018 to 4140 HT and 4340), titanium, Inconel, aluminum, cast iron, plastics |
| Files | STEP, PDF or a hand sketch |
Yes. Single prototypes and small runs are a normal part of our work.
Yes. We will work with you to turn it into a part we can make.
Yes. We don’t publish customer names or project details, and we’ll sign your NDA.
Yes. We accept purchase orders and university purchasing cards. We can provide a W-9 and complete your supplier registration.
Yes. Startups and private R&D teams are welcome too.
Yes. We have built Invar camera cage assemblies and solid copper rails. Both take the right tooling and care at every setup.
We turn to 60″ diameter and 170″ between centres, mill to 157″, and lift to 10 tons.
The services a prototype usually draws on.
Send us the drawing. We’ll call you back to talk through it.