
gundrilling · hillsborough, new jersey
Home / Gundrilling Services
Our gun drilling services cover holes from 5/16″ to 4″ diameter and up to 96″ deep, on a machine dedicated to gundrilling. Four inches is a large hole for a gun drill. It is the size where many shops stop and send the work out.
Gundrilling is a discipline of its own. What sets the work here apart is what happens either side of the hole. The same shop turns, mills, five-axis machines, hones and grinds the part, so a gundrilled component leaves finished rather than half-made. Send raw bar, a casting, or a part that only needs the hole. We take it from wherever it starts.
This is the work we are set up for. A melt pipe is a gundrilling job before it is anything else. So is a long-neck elbow: the neck has to be drilled deep and straight, then honed so the polymer moves through without a step or a dead spot. We have made melt pipes and elbows for the major extruder OEMs for years, and we still do. Extruder barrels are gun drilled here too. Hollow shafts run the same way: drilled on centre, honed to finish, and turned and ground on the outside without leaving the building.
Not every deep hole needs the gundrill. Our CNC lathes and mills run through-coolant carbide drills on high-pressure coolant, so deep holes can be drilled on any of them, as long as the part fits the machine. That is how the holes go into our extruder breaker plates: down to 1mm diameter and up to 30 times the diameter deep.
The same approach handles flat work. Mold base drilling runs on our CNC mills, with holes up to 20″ deep put in by through-coolant carbide drills on high-pressure coolant. Tube sheets get the same treatment: full hole patterns drilled, bored and counterbored on the CNC machines, with the turning and milling around them done in the same building. Send the print with the hole schedule and we will come back with a price and a date.
Gundrilling makes the hole. Honing brings it to size, roundness and finish. Both happen here. Our honing runs to 26″ diameter and 120″ long, so a long bore never leaves the building between operations.
The shop is in Hillsborough, in Somerset County, New Jersey. We gun drill for plants across New Jersey, New York and Pennsylvania, from the Newark and Elizabeth corridor down to Trenton and Philadelphia. Deep-hole parts travel well on a truck, so we take work from further out too.
A look around the shop floor in Hillsborough. Click to play.
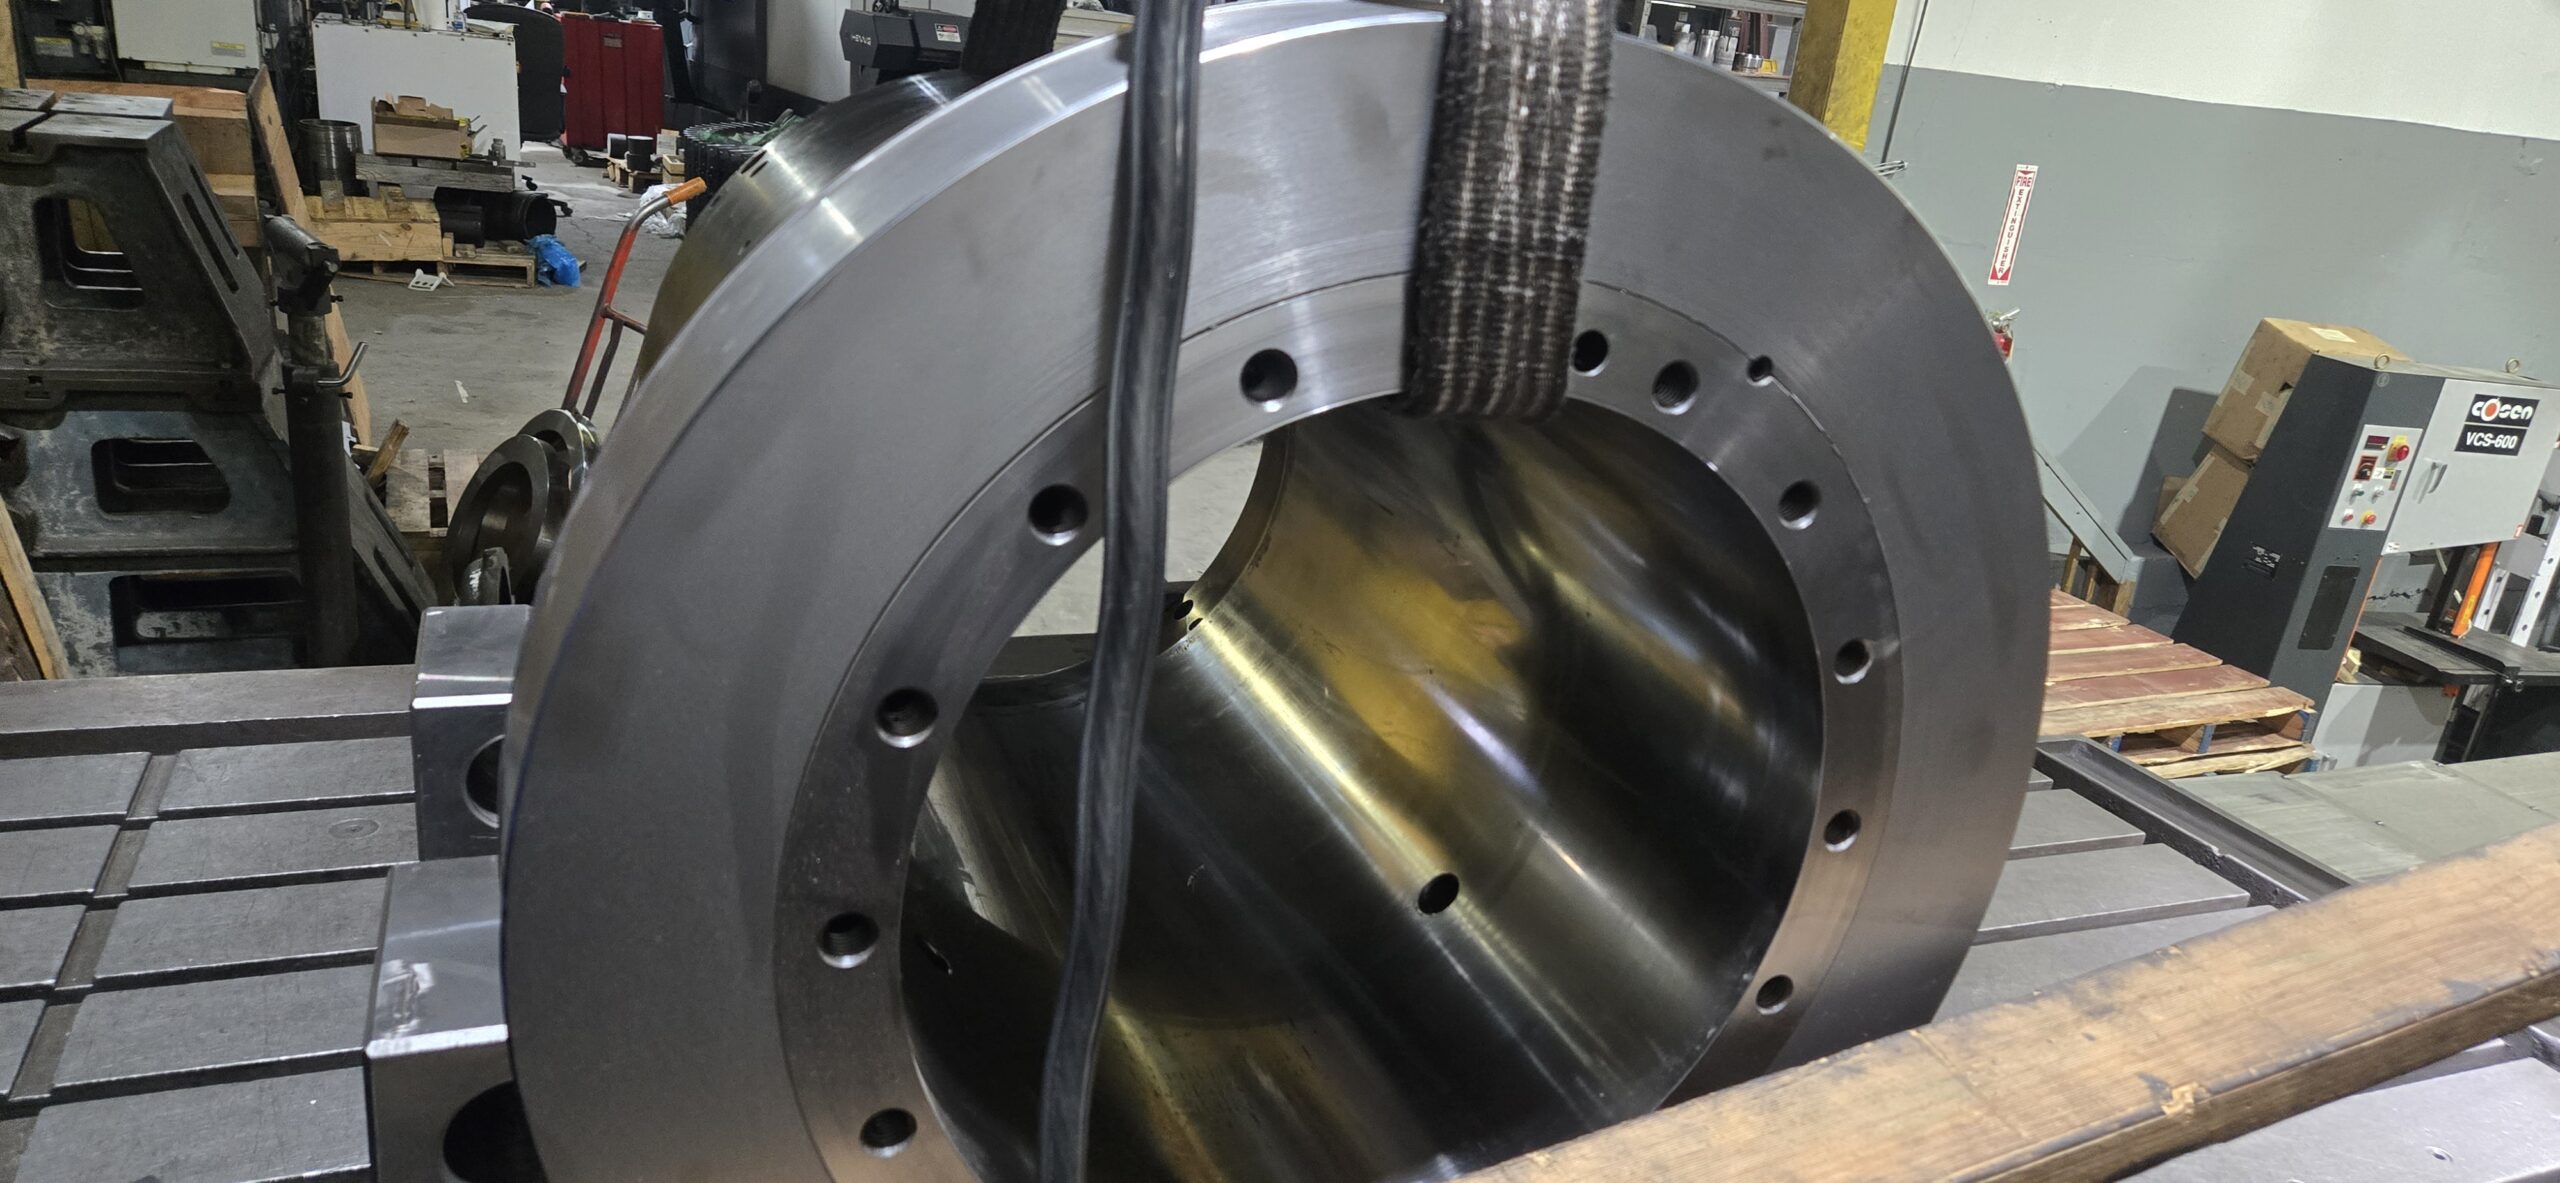
Large bore and flange face machined on a heavy body.
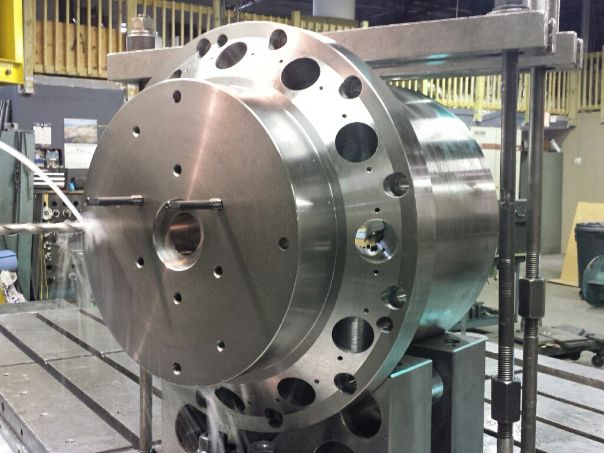
Die housing set up on the machine for deep boring.
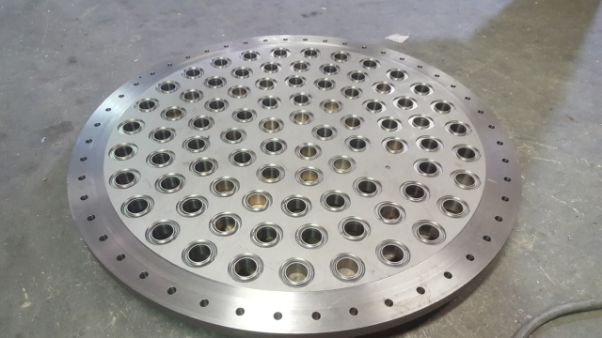
Tube sheet with a bored and counterbored hole pattern, drilled on the CNC.
Most of our gun drilling is round work drilled on centre, where the bore has to stay true to the outside diameter.
Drilled deep and straight, then honed so the polymer transfers without a step. More on melt pipes and elbows.
Drilled on centre, then turned and ground on the outside, with the bore concentric to the diameter.
Holes to 4″ diameter and up to 96″ deep on the gundrill, where a twist drill would wander long before the bottom.
Mold base drilling up to 20″ deep on our CNC mills, with high-pressure through-coolant drills.
Hole patterns drilled, bored and counterbored on our CNC machines.
Extrusion parts with deep bores and five-axis features. More on breaker plates.
Holding a deep hole on centre depends as much on the setup as on the drill. Because the turning, milling and grinding happen here, the workpiece is prepared, drilled and finished without leaving the building or losing its reference.
CNC turning and milling: stock prepared and features cut on our lathes and mills, to 28″ diameter on the Okuma LB4000EX.
Five-axis machining: complex outside geometry cut in one setup on the Mori Seiki NTX2000, held true to the bore.
On-centre gundrilling: the difficult bores for rotary parts, drilled straight over long depths.
Precision grinding: shaft grinding in house on every precision diameter, with finish checked on a profilometer.
Gundrilled parts from this shop go into polymer extrusion lines — feed blocks, adapters and melt pipes that need a deep bore, five-axis work and a good internal finish. They go into aerospace and defense work; Zala Machine Co. is ITAR registered. And they go into industrial drive systems, as gundrilled shafts and cylinders that arrive ready to assemble.
One shop owns the part: from material through final inspection, the quality of the whole component is ours, not split across three vendors.
Parts that spin: much of our work is rotating components, where the bore and the outside diameter have to stay concentric.
Close to you: the shop is in Hillsborough, New Jersey, and we gundrill for customers across NJ, NY and PA.
Gun drilling, deep hole drilling and honing, with the turning and milling around them.
| Gundrilling | 5/16″ to 4″ diameter, up to 96″ deep |
| Deep hole drilling on CNC | Through-coolant carbide drills on high-pressure coolant, on any machine the part fits. Holes down to 1mm at up to 30 × diameter |
| Mold base drilling | Up to 20″ deep on our CNC mills |
| Honing | .060″ to 26″ diameter, up to 120″ long |
| CNC turning | 28″ diameter × 60″ long (Okuma LB4000EX); 14″ × 83″ long (Doosan Puma 300XLY) |
| Manual turning | 32″ diameter × 170″ between centres (Poreba) |
| 5-axis | Mori Seiki NTX2000 mill-turn |
| Materials | Carbon and alloy steels including 4140 HT, stainless such as 15-5 PH, Inconel 718, titanium and bronze |
The shop is in Hillsborough, New Jersey, in Somerset County. Most gundrilling comes from plants across New Jersey, New York and Pennsylvania, and from the industrial corridor through Newark, Elizabeth, Jersey City and Paterson.
Deep-hole parts travel well, so we take work from beyond the tri-state too. Send the print and the part.
From 5/16″ to 4″ diameter, and up to 96″ deep, on a machine dedicated to gundrilling.
A gundrill is a single-flute tool fed with high-pressure coolant through its centre, which flushes the chips back out along the flute. That is what lets it go deep and stay straight. A twist drill wanders long before it gets there. Any hole much beyond about ten times its own diameter wants gundrilling.
Straight enough for rotary parts, which is the hardest case — the bore has to stay concentric with the outside diameter over the whole length. Because we turn, drill and grind the part in the same shop, the workpiece keeps its reference from one operation to the next.
Yes, and it is often the right answer. Gundrilling makes the hole; honing brings it to size, roundness and finish. Both are here, so the part does not travel. Our honing runs to 26″ diameter and 120″ long.
Extruder melt pipes, elbows, barrels and feed blocks, hydraulic and high-pressure tubes, gundrilled and hollow shafts, die housings, and rotary components that need a coolant passage or weight taken out of the middle. On our CNC mills we also drill mold bases up to 20″ deep and tube sheets with full hole patterns.
The same through-coolant deep hole drilling puts the holes in our extruder breaker plates, down to 1mm and up to 30 times the hole diameter deep.
Carbon and alloy steels including 4140 HT, stainless such as 15-5 PH, Inconel 718, titanium and bronze.
Yes. Send the part and the print. We can also take it the other way — raw bar or a casting in, finished component out.
Hillsborough, New Jersey, in Somerset County. We gundrill for plants across New Jersey, New York and Pennsylvania, and take deep-hole work from further out — tubes and shafts travel well on a truck.
A gundrilled part is usually turned, milled, honed or ground here as well. These pages cover that work.
Whether it is a gundrilled shaft with five-axis features or a high-pressure extruder melt pipe, the whole job runs here. Send the print and we will come back with a price and a date.
Call the shop or email sales@zalamachine.com, or use the quote form below.