
cnc milling · hillsborough, new jersey
Home / CNC Milling
Our vertical CNC milling services run in Hillsborough, New Jersey, on three CNC machining centres. The largest, a Zayer, gives 157″ of travel in X, 40″ in Y and 70″ in Z. That takes a weldment, a base plate or a long frame that many job shops turn down. Tolerances under .001″ are standard work, and we hold ±.0005″ where the print calls for it.
Large plates, frames, bases and housings go on the Zayer. We lift to 10 tons in the shop, so a heavy part is set up and indicated properly rather than worked around. Long parts are cut in one setup where the travel allows it, so the features stay in true relation end to end.
The Okuma Millac takes 60″ × 30″ × 30″ with a 4th axis, and the Okuma Genos 560V runs full 4-axis at 40″ × 20″ × 20″. The 4th axis lets us machine features around a part: off-centre holes, slots and flats on shafts and cylindrical work. For simultaneous 5-axis work, see our 5-axis milling page.
Every CNC machine here has a high-pressure coolant pump, so deep holes are drilled on the mills with through-coolant tooling. Mold base drilling runs up to 20″ deep. Longer bores go to our gun drilling department.
A lot of the milling here is repair work. When a gearbox housing needs a new bearing bore, or a plate is holding up a line, we machine it from steel already on the floor. Where there is no drawing, we reverse engineer the worn part first. Single parts, small batches and production runs all run through the same department.
Milled parts leave Hillsborough for plants across New Jersey: Bridgewater, Somerville, Flemington, Edison, Piscataway and Trenton, and the industrial corridor through Newark, Elizabeth, Jersey City and Paterson. Customers in Somerset, Hunterdon, Middlesex and Mercer counties often drop parts off and collect them by hand. Further out, parts ship by truck to eastern Pennsylvania, New York, and across the United States, Canada and Mexico.
CNC milling on the shop floor. Click to play.
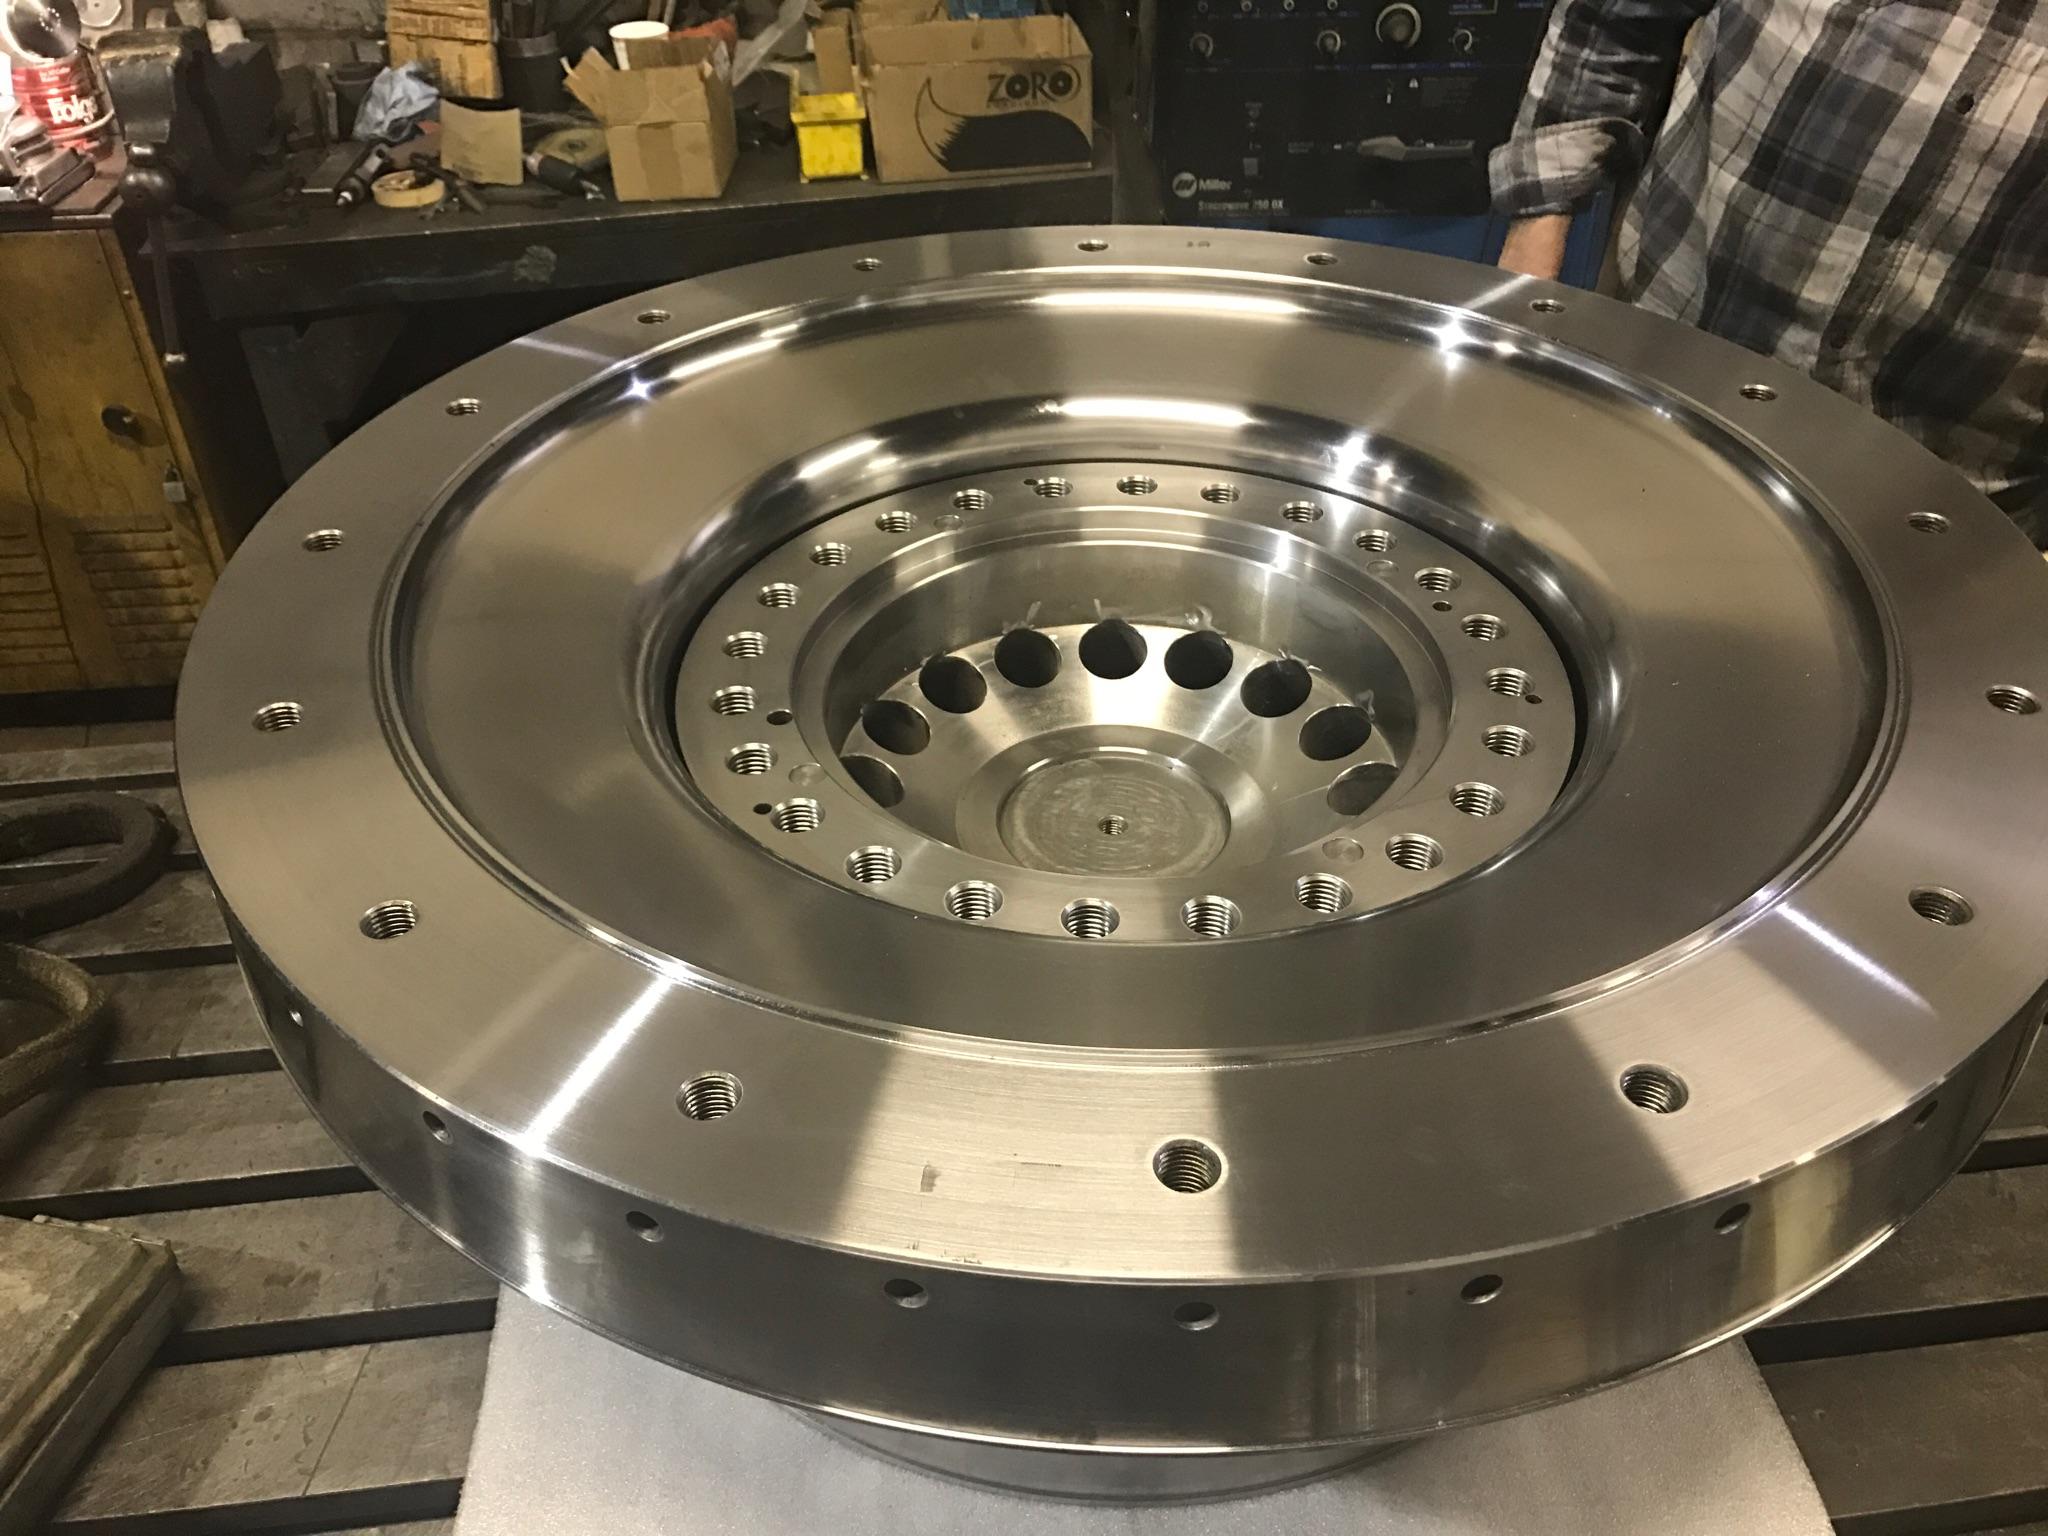
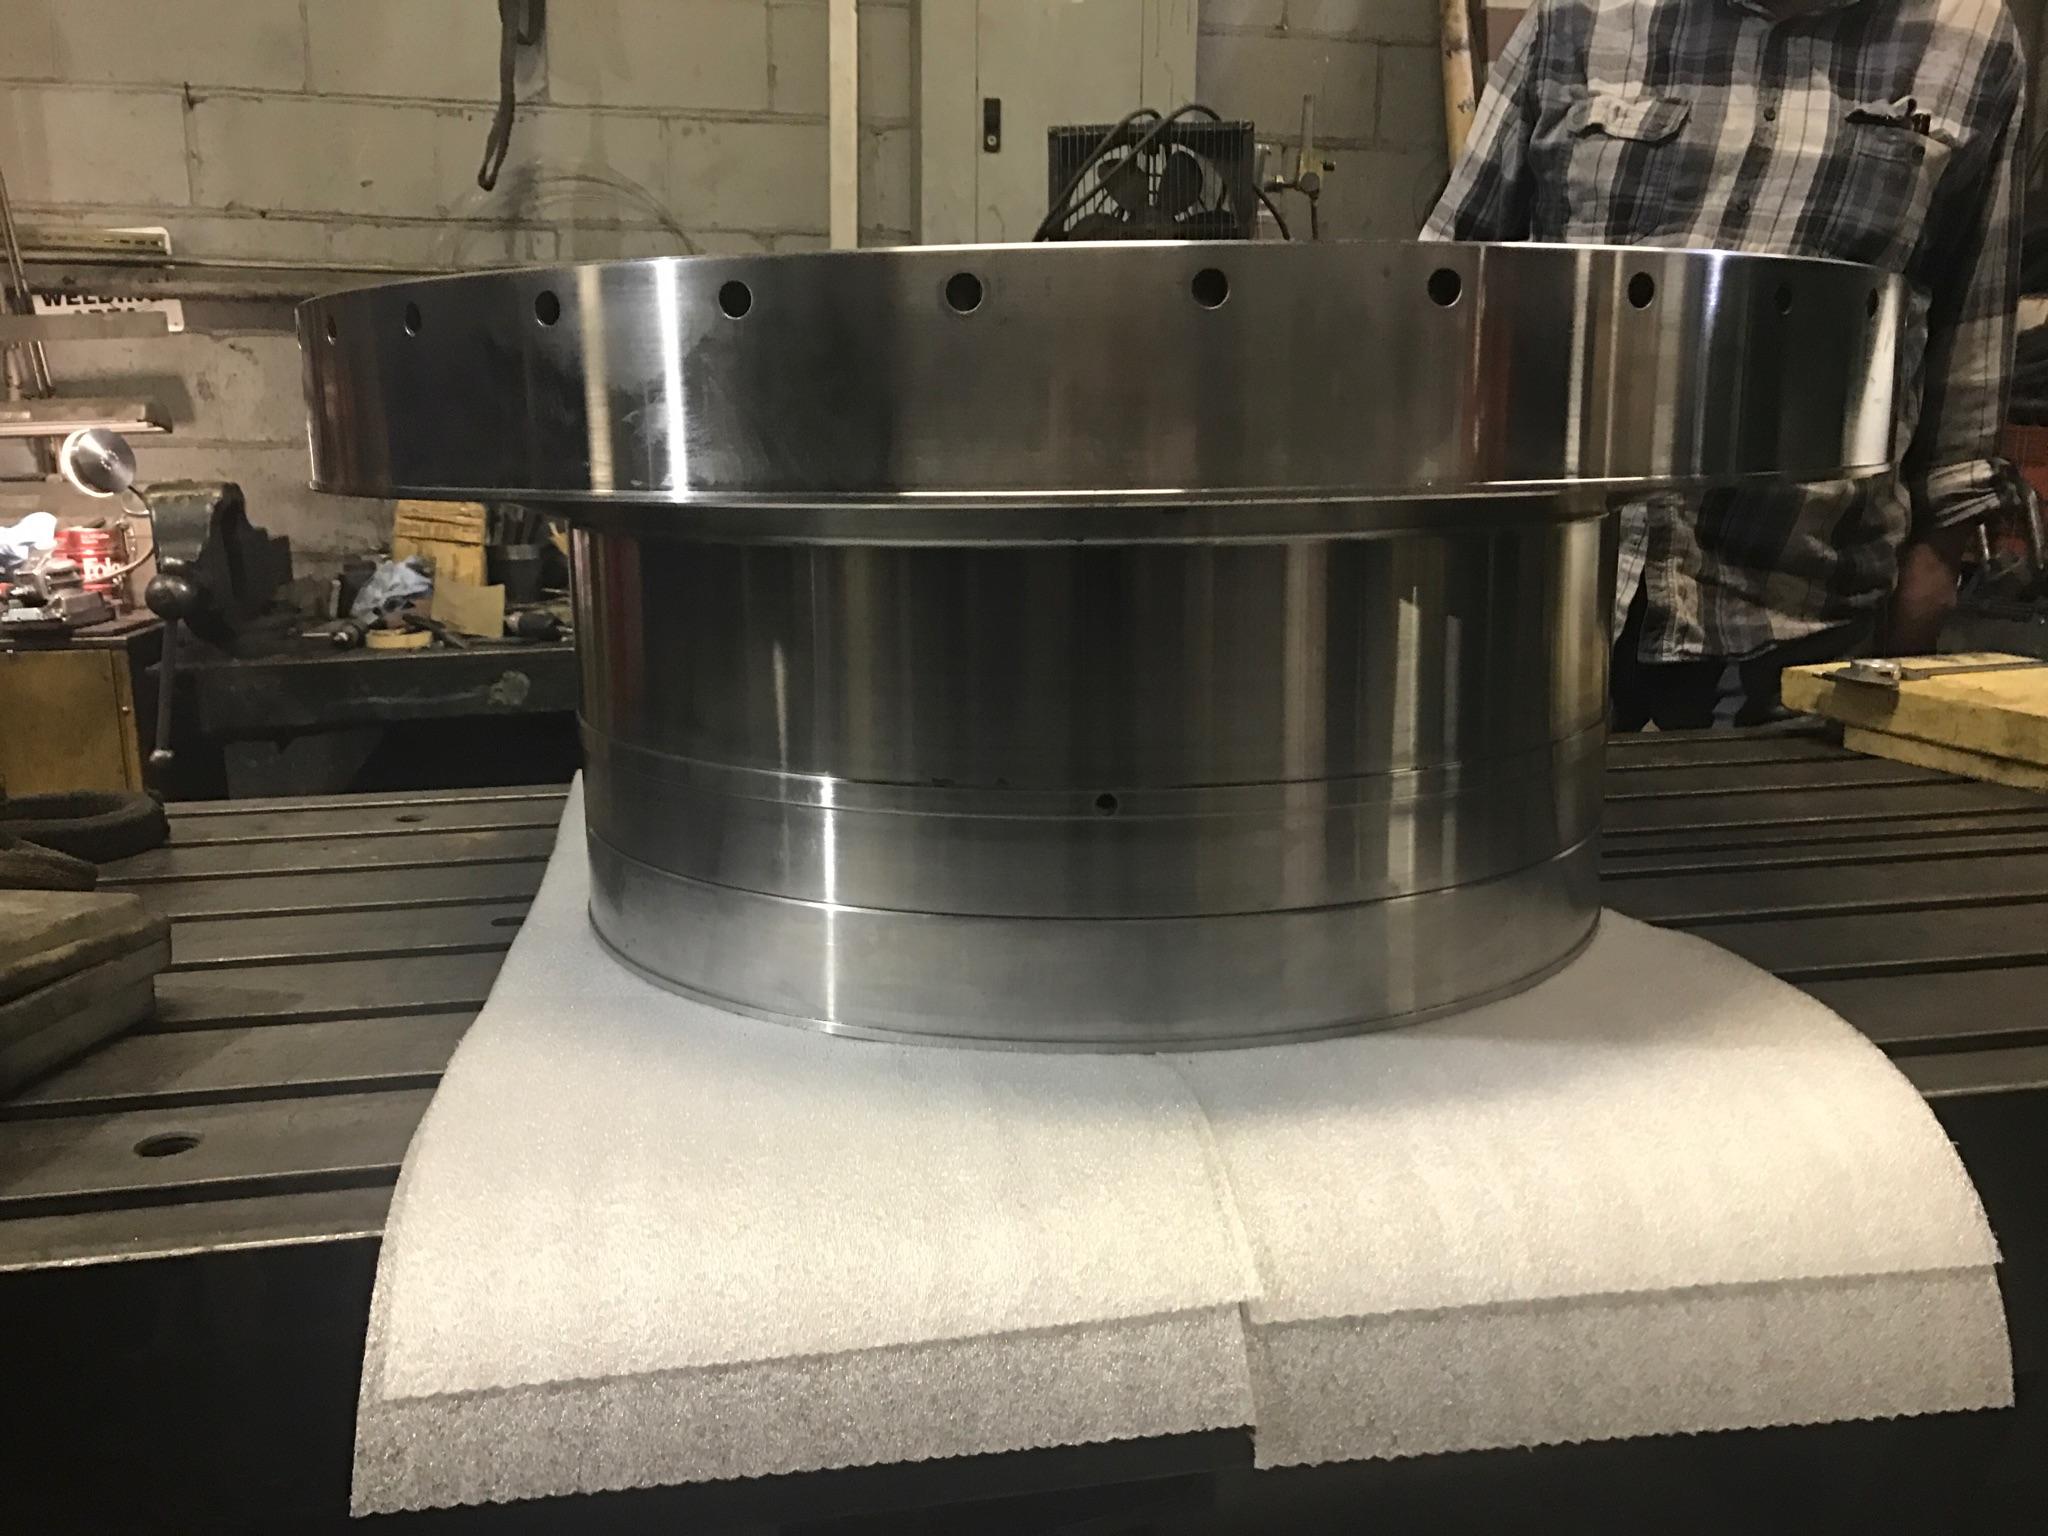
Flanged plate with an internal gear ring, after machining.
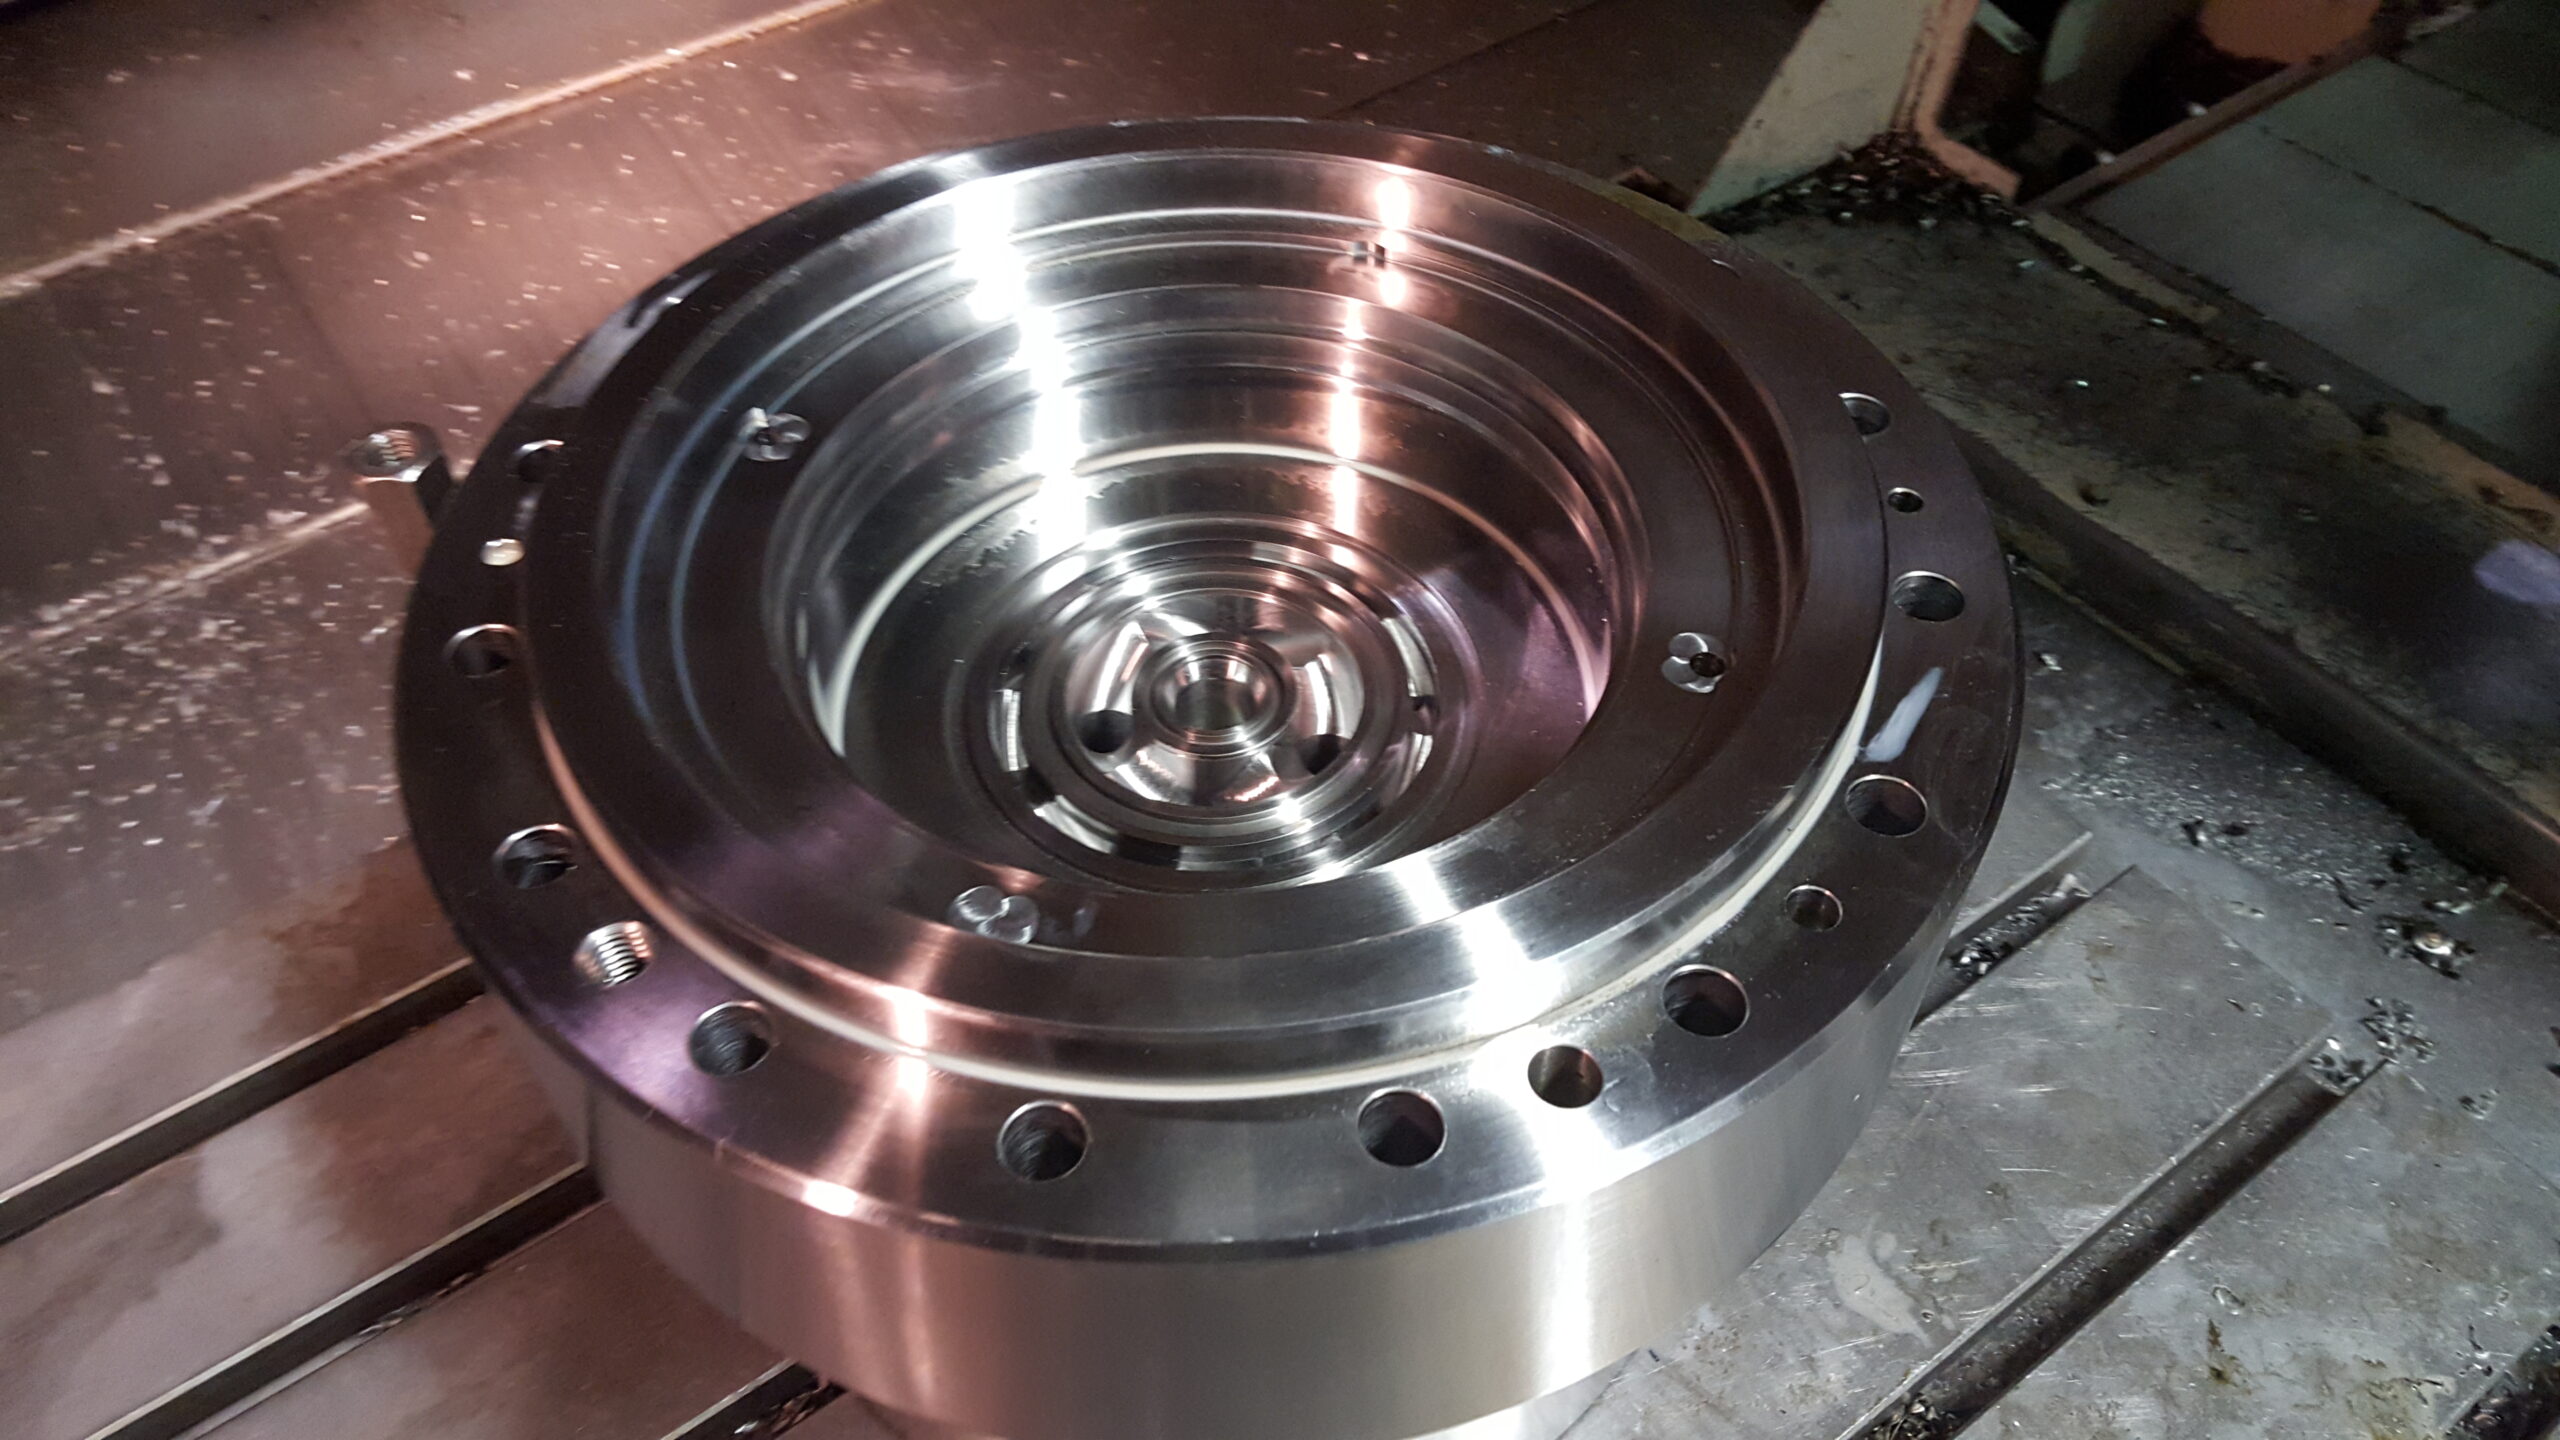
Sealing face with concentric grooves and drilled bolt holes.
Milled parts from our machining centres in Hillsborough, New Jersey: manifold blocks, sealing faces and plates, cut to print. More photos and videos are in our gallery.
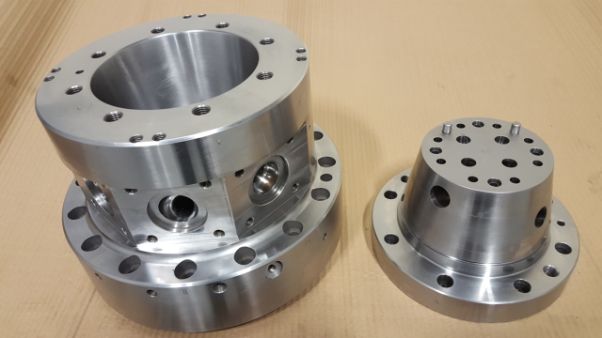
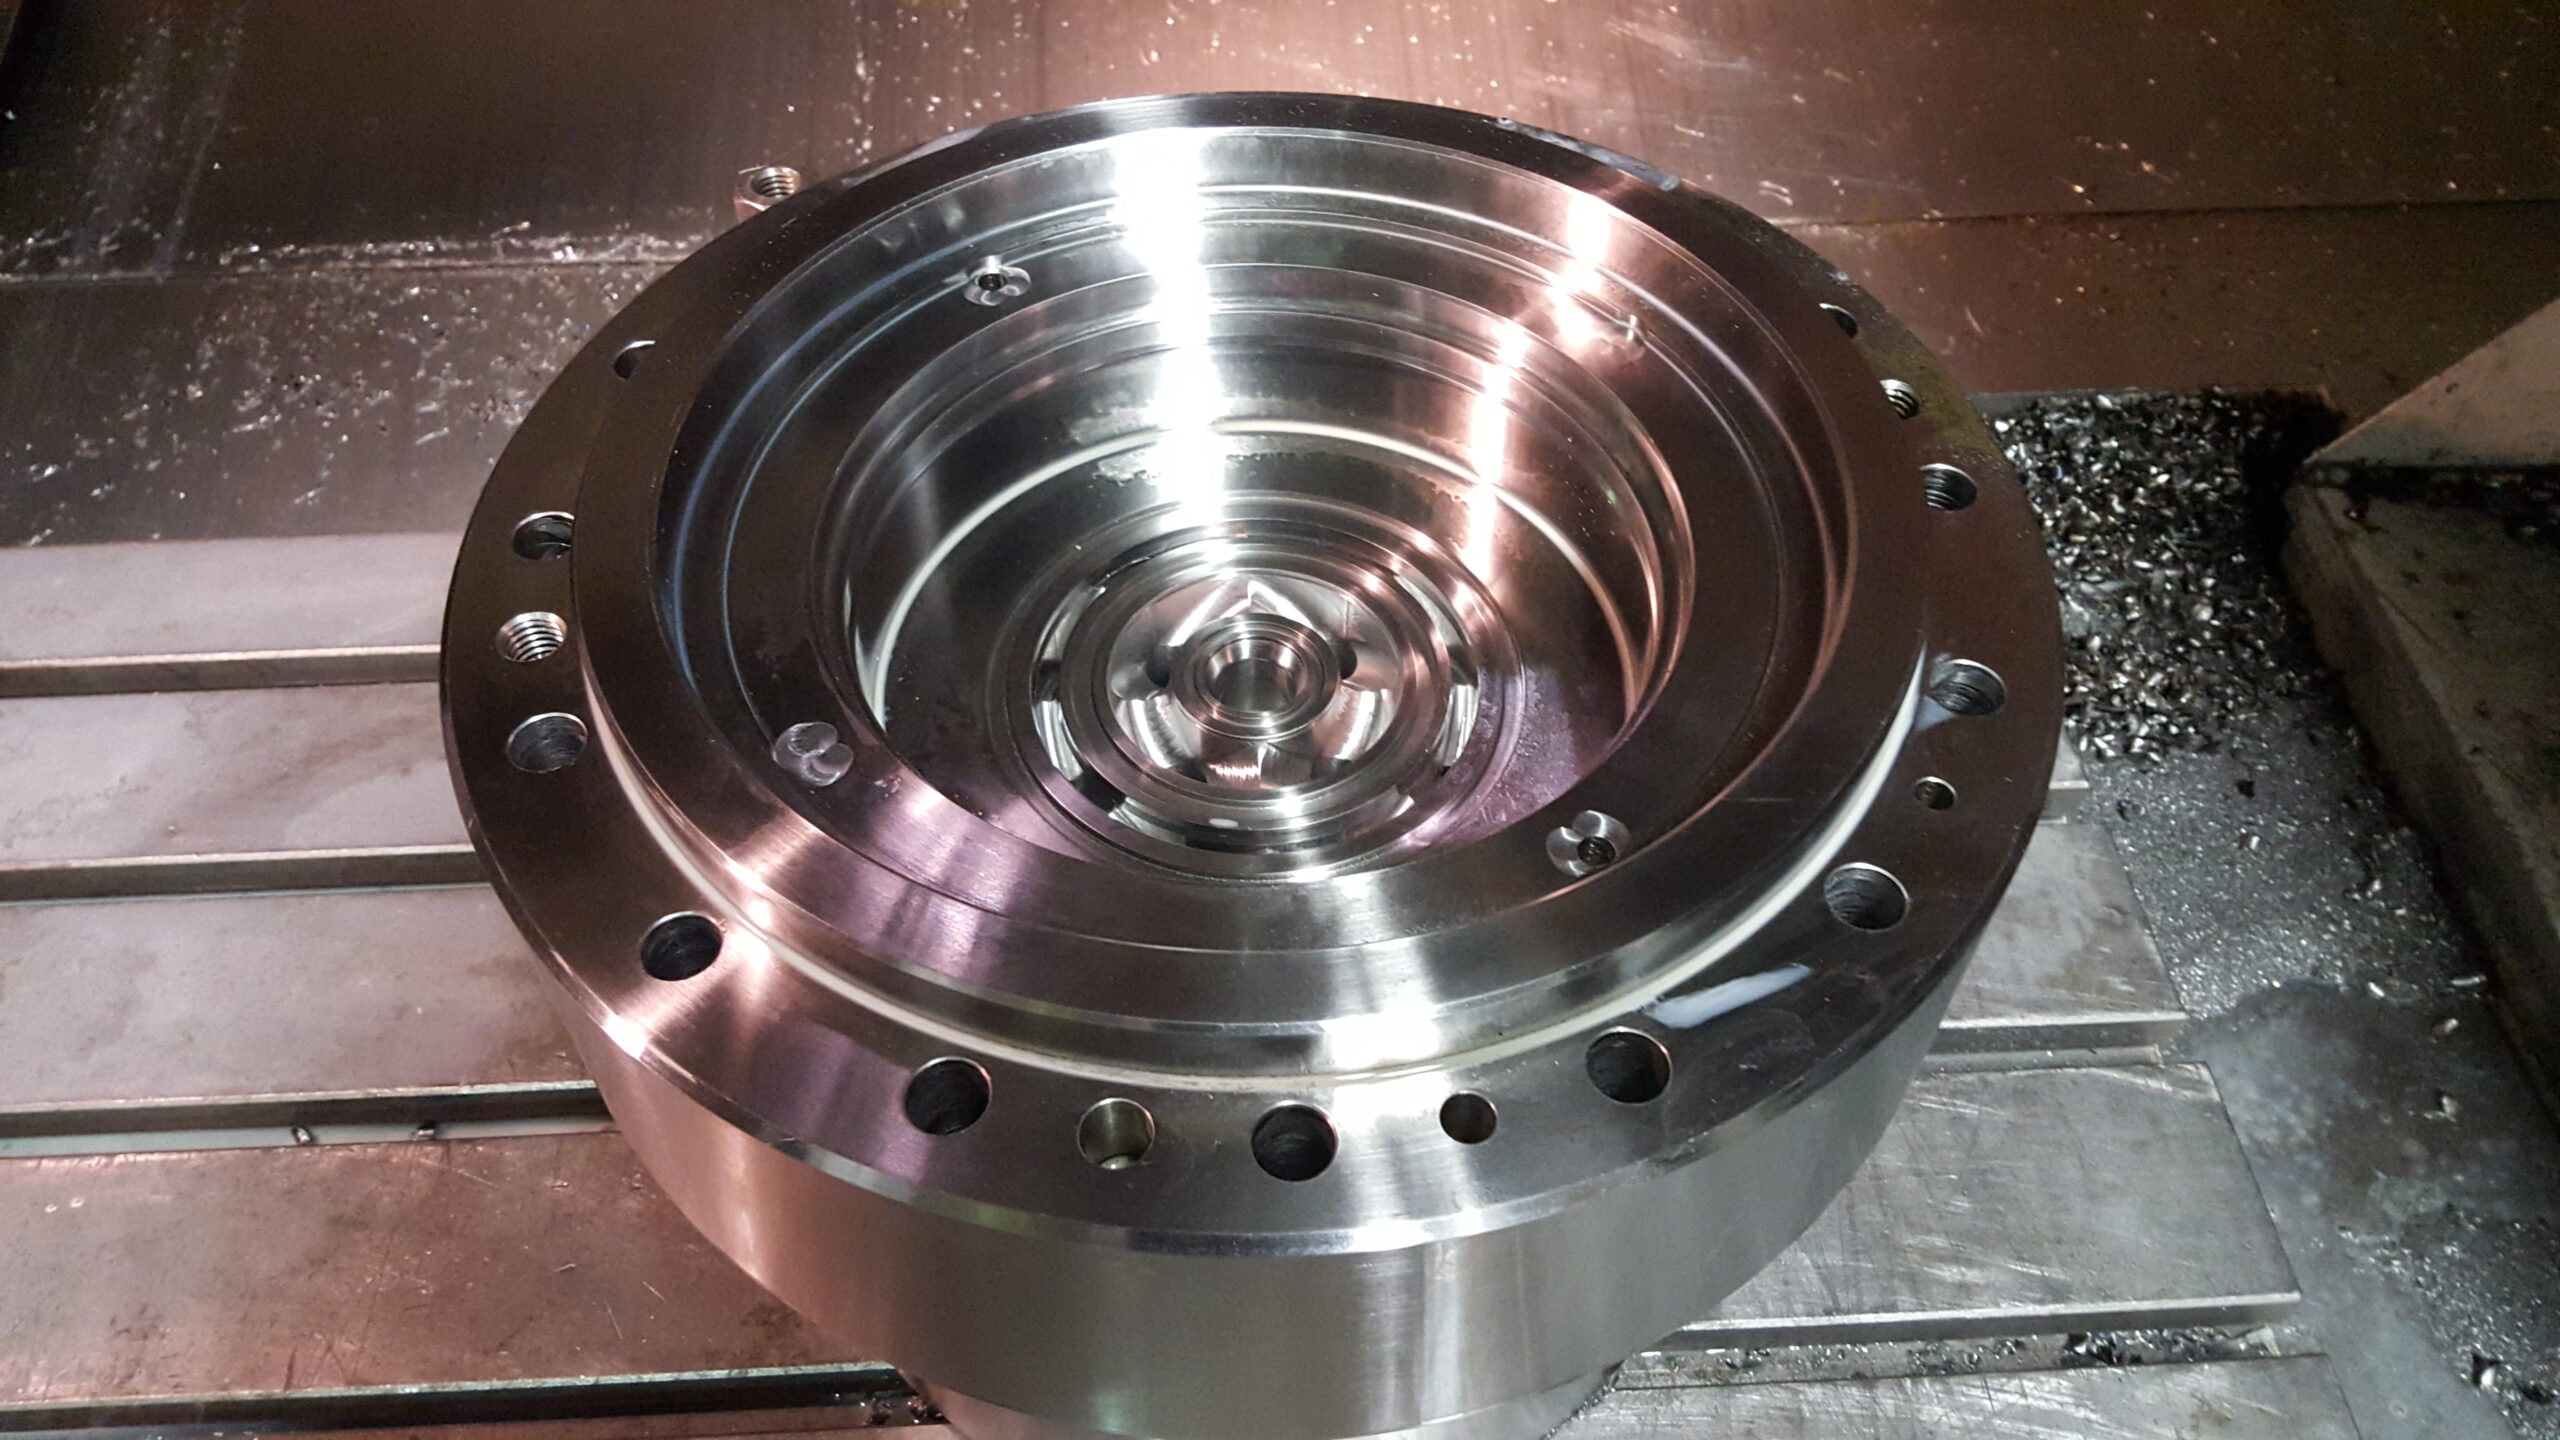
Three CNC machining centres, from a fast 4-axis machine to the largest envelope in the shop. Prototype, one-off, small batch or production run, the same machines and the same inspection.
Travel 157″ × 40″ × 70″. The largest milling envelope in the shop, for plates, frames, bases and weldments.
Travel 60″ × 30″ × 30″, with a 4th axis. The heavy-duty workhorse for complex, precise milling.
Travel 40″ × 20″ × 20″, full 4-axis. Fast, rigid and precise in every material.
Manifold blocks and valve bodies. Cross-drilled bores, ports and sealing faces held to print.
Plates, bases and frames. Bolted plates, machine bases and weldments with their flats, bores and hole patterns cut after welding. See large fabrication.
Gearbox and extruder parts. Housings, gear rings, adapters and mounting plates, often alongside a gearbox rebuild or extruder components.
Sealing faces and rings. Concentric seal grooves, bolt circles and large rings machined flat and true.
Most of what runs here is not aluminium. Alloy steel, 4140 and 4340, including hard milling after heat treat where the part has to stay dimensionally stable. Stainless in the 300 and 400 series, 15-5 PH and 17-4 PH, for food, pharmaceutical and marine work. Titanium and Inconel, with rigid setups and the right feeds. Aluminium, brass, bronze and industrial plastics for housings, insulators and custom bushings.
Milling is rarely the whole job. A milled part usually needs a bore honed, a journal ground, a weldment finished or a shaft turned. All of that happens in the same building, so the part does not travel between shops or lose its reference between operations.
Bores go to bore honing when the finish or size calls for it, and turned features run on our CNC lathes.
Every part is checked against the print before it ships, with a Keyence portable CMM, micrometers, bore gauges and depth mics.
The machining centres, the drilling and the finishing around them.
| Zayer horizontal / vertical | 157″ × 40″ × 70″ travel — our largest milling envelope |
| Okuma Millac VMC | 60″ × 30″ × 30″ travel, with 4th axis |
| Okuma Genos 560V | 40″ × 20″ × 20″ travel, full 4-axis |
| Part size | from 2″ up to 157″ long |
| Tolerance | under .001″ as standard, ±.0005″ where the print calls for it |
| Materials | aluminium, 300 and 400 series stainless, 15-5 PH and 17-4 PH, 4140 and 4340, titanium, Inconel, industrial plastics |
| Lifting | to 10 tons |
| Finishing in house | bore honing, shaft grinding, welding and polishing |
| Deep hole drilling | high-pressure through-coolant on every CNC; mold base drilling to 20″ deep |
From 2″ up to 157″ long. The Zayer gives 157″ × 40″ × 70″ of travel, the Okuma Millac 60″ × 30″ × 30″ with a 4th axis, and the Genos 560V 40″ × 20″ × 20″. We lift to 10 tons, so a large weldment or base plate is no obstacle.
Under .001″ is standard work, and we hold ±.0005″ where the print calls for it. Every part is checked against the drawing before it ships — Keyence portable CMM, micrometers, bore gauges and depth mics.
Yes. The Genos 560V runs full 4-axis and the Millac has a 4th axis, which is what lets us machine features around the circumference of a part — off-centre drilling, slotting and milling on shafts and cylindrical work. For simultaneous 5-axis work, see our 5-axis milling page.
Aluminium, 300 and 400 series stainless, 15-5 PH and 17-4 PH, 4140 and 4340 alloy steel including hard milling after heat treat, titanium, Inconel, and industrial plastics.
No. We mill single replacement parts and one-off prototypes as well as production runs. Tell us the quantity with the drawing and we will quote it.
Yes, and most parts need it. Bore honing, shaft grinding, welding and polishing all happen in this building, so the part is not shipped between shops between operations.
Yes. We weld and then machine — frames, bases and large plates get their flats, bores and hole patterns cut after welding, so the finished faces run true rather than following wherever the weld pulled.
Hillsborough, New Jersey, in Somerset County — an easy drive from Bridgewater, Somerville, Flemington, Edison, Piscataway and Trenton, and from the corridor through Newark, Elizabeth, Jersey City and Paterson. Milled parts also go by truck across the United States, Canada and Mexico.
Milled parts are often turned, drilled, honed or welded before they ship. These are the services that sit alongside the mills.
Send the print, the material and the quantity, and we will quote it. Call the shop or email sales@zalamachine.com, or use the quote form below.