Machine Shop Gallery

Work from the floor at Zala Machine Co. in Hillsborough, New Jersey — precision CNC turning, milling, boring and honing on extrusion tooling, shafts and heavy industrial components. Every part shown here was machined in house.

Swipe through every photo. Tap one to see it full size.

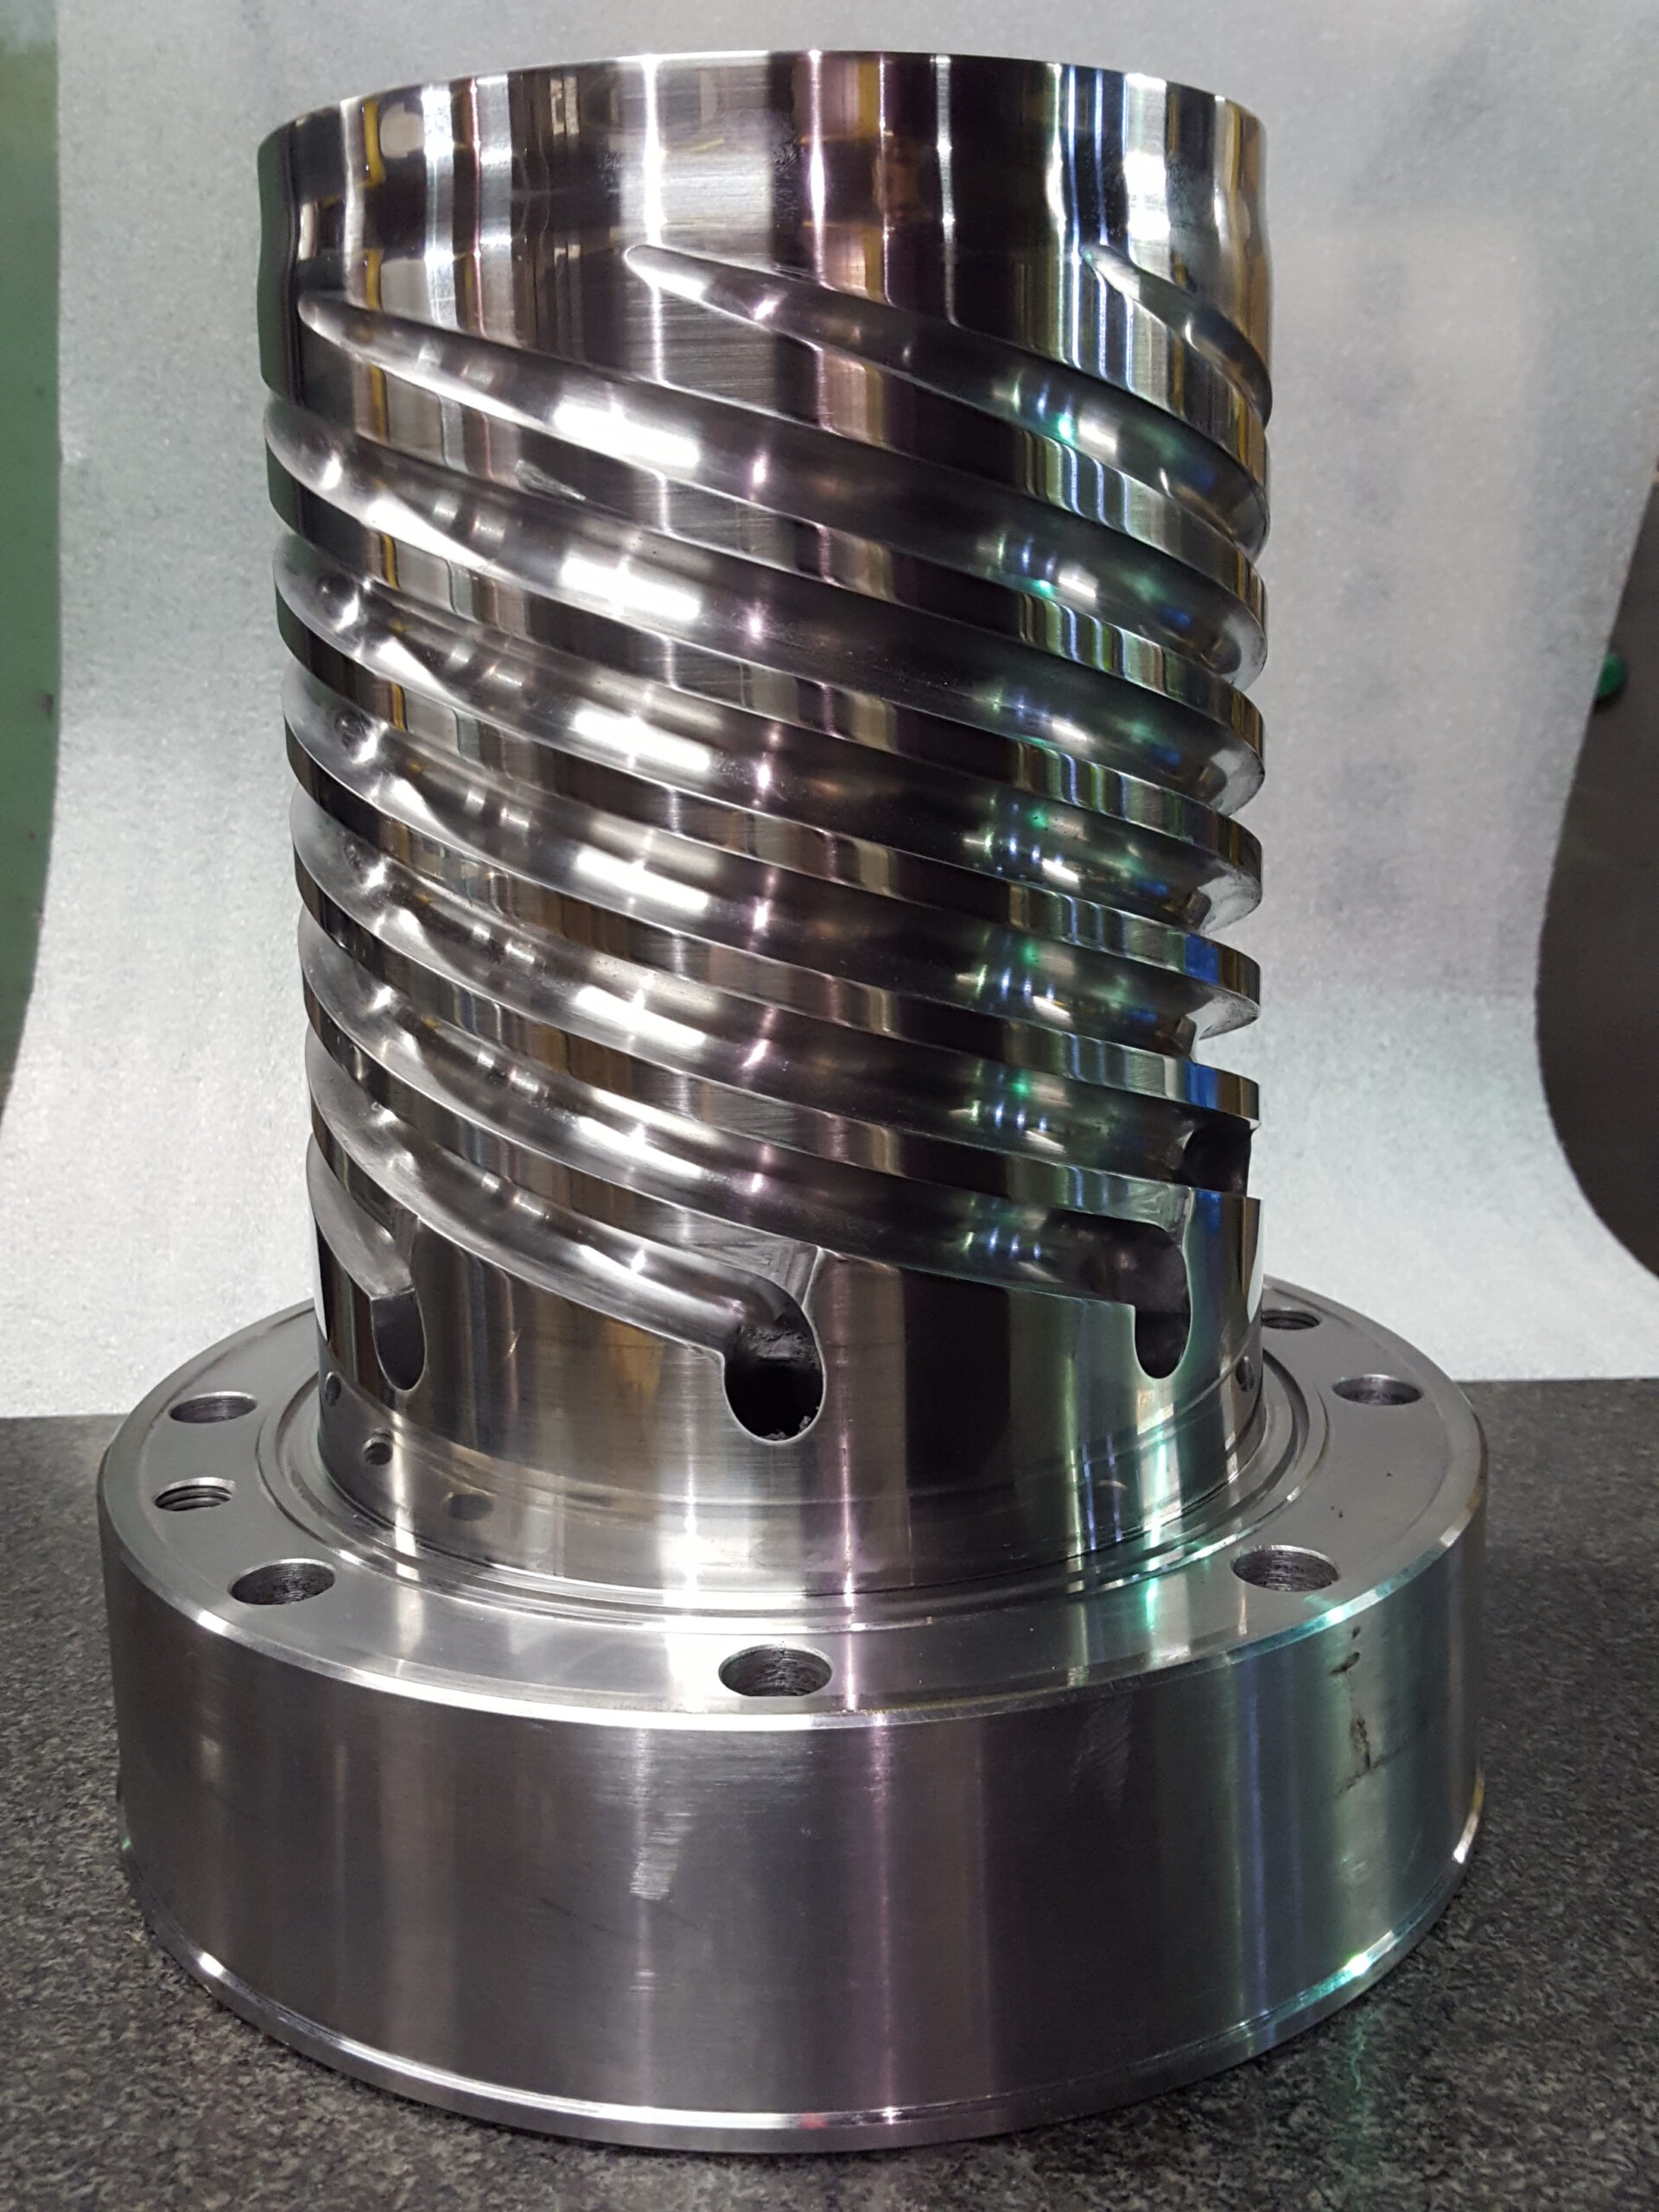
Finished spiral mandrel with helical flow channels and mounting flange
Blown film dies: Finished spiral mandrel with helical flow channels
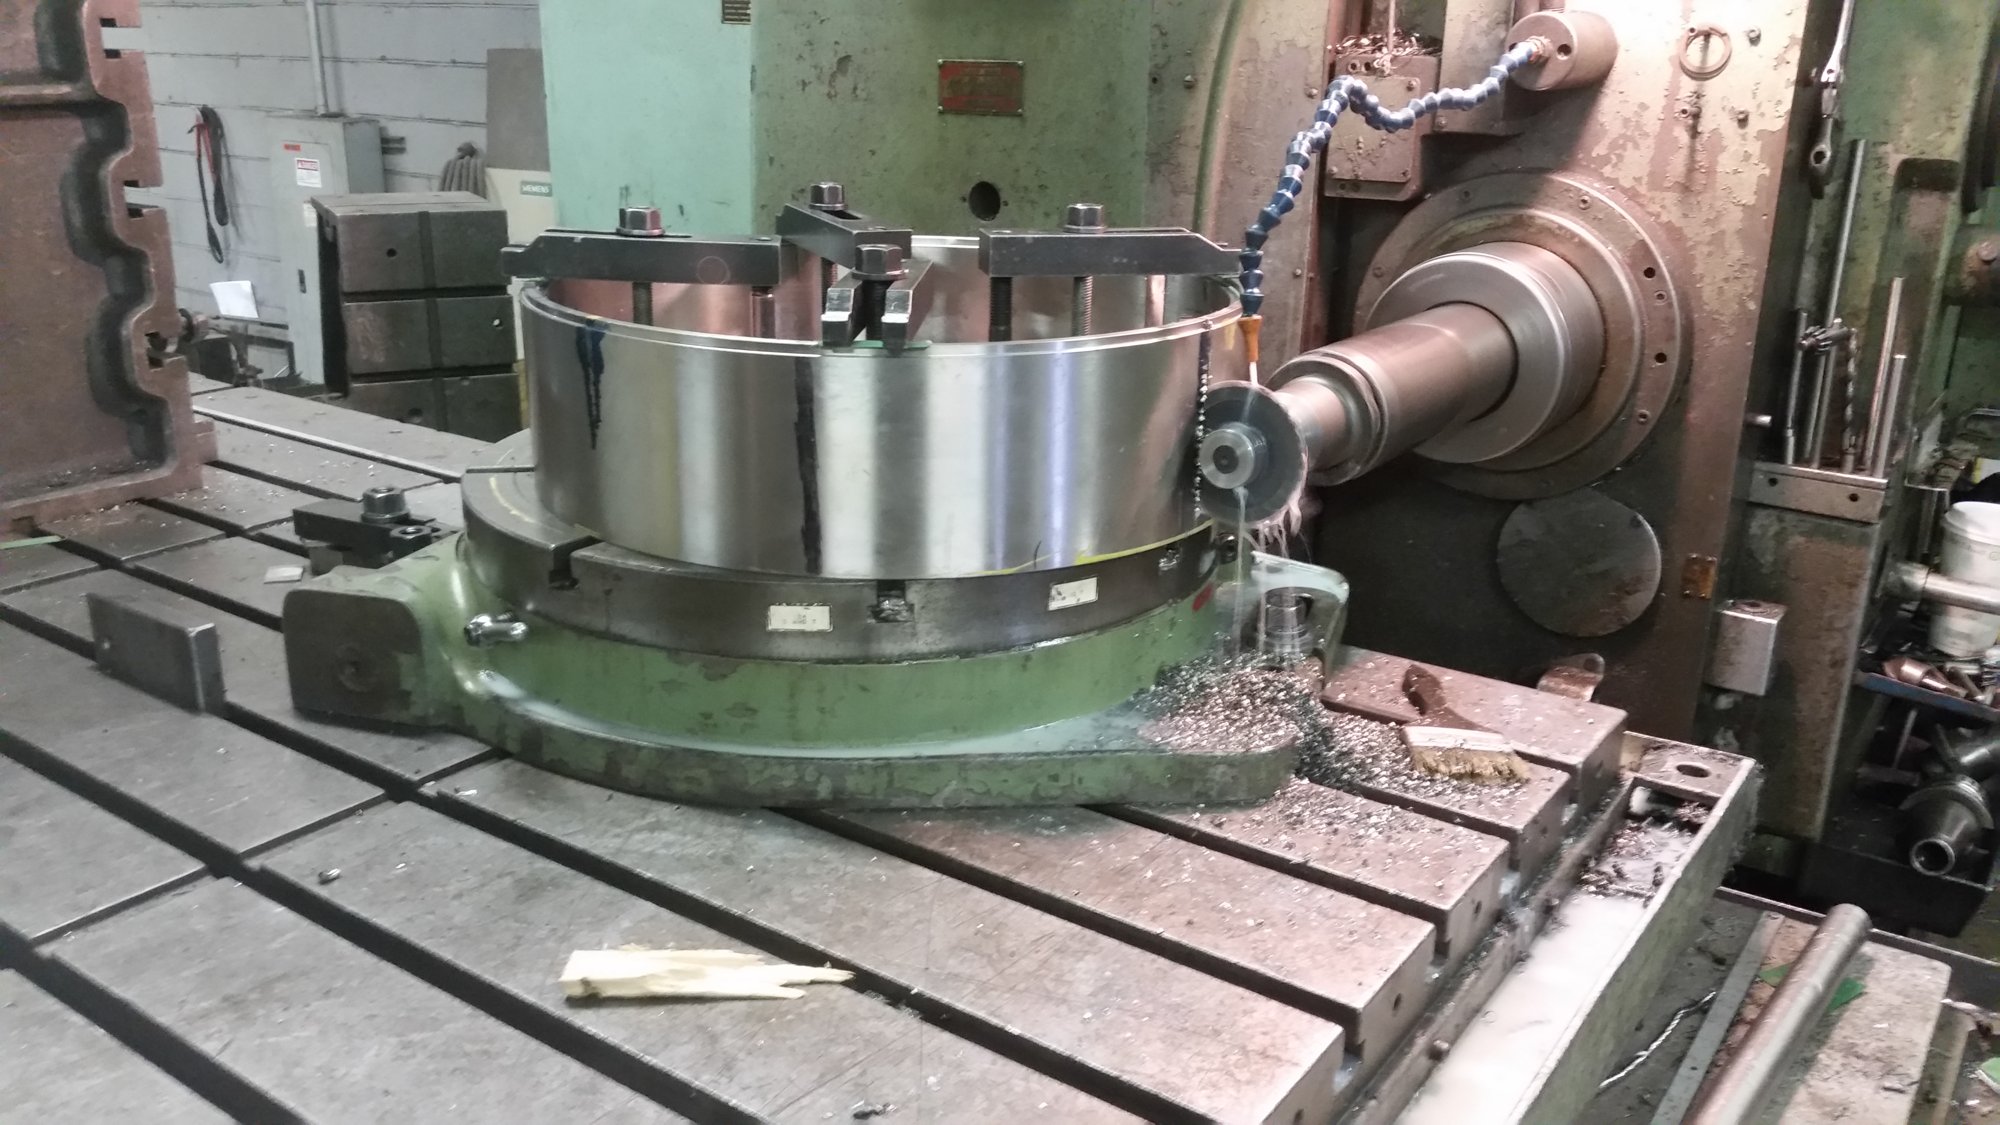
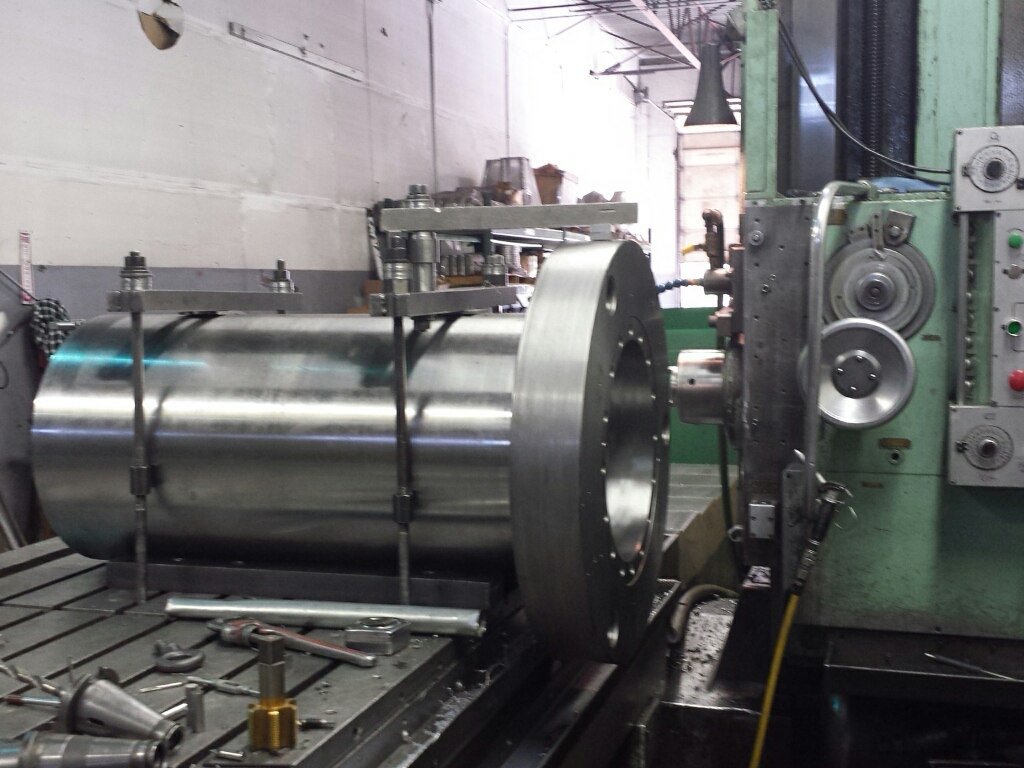
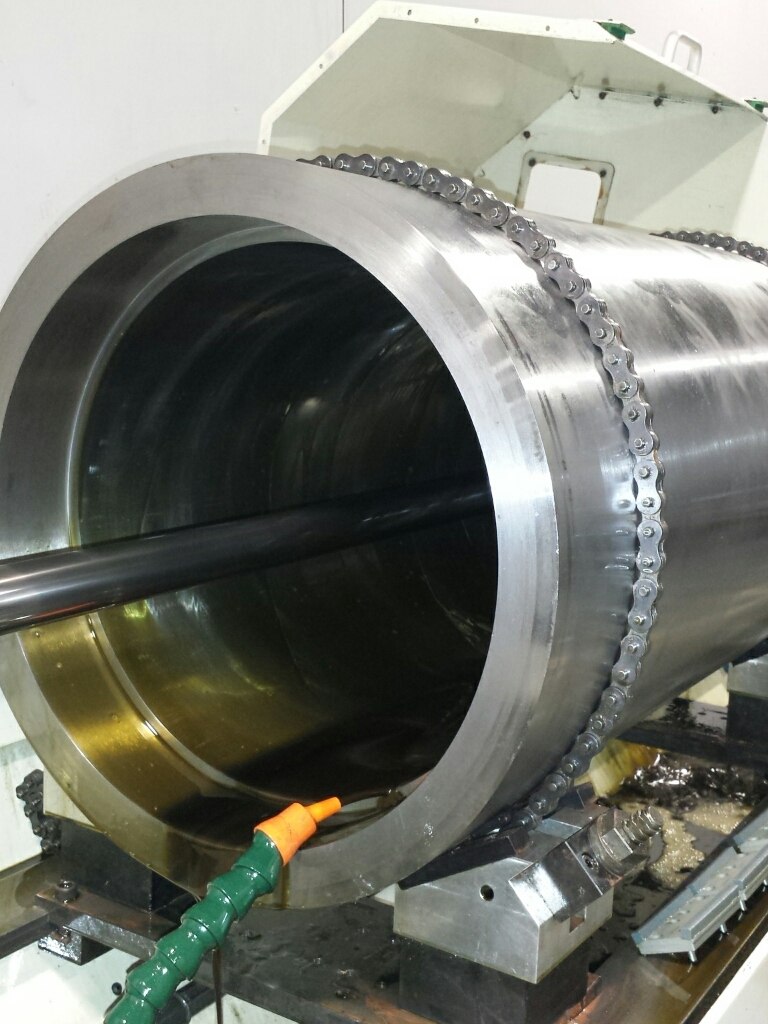
Large steel ring clamped on the horizontal boring mill's rotary table, boring bar engaged
Large machining: Large ring on the horizontal boring mill's rotary table
Production run of machined stainless cylinders lined up, every bore finished to the same size
Turning and production: A production run of stainless cylinders, all alike
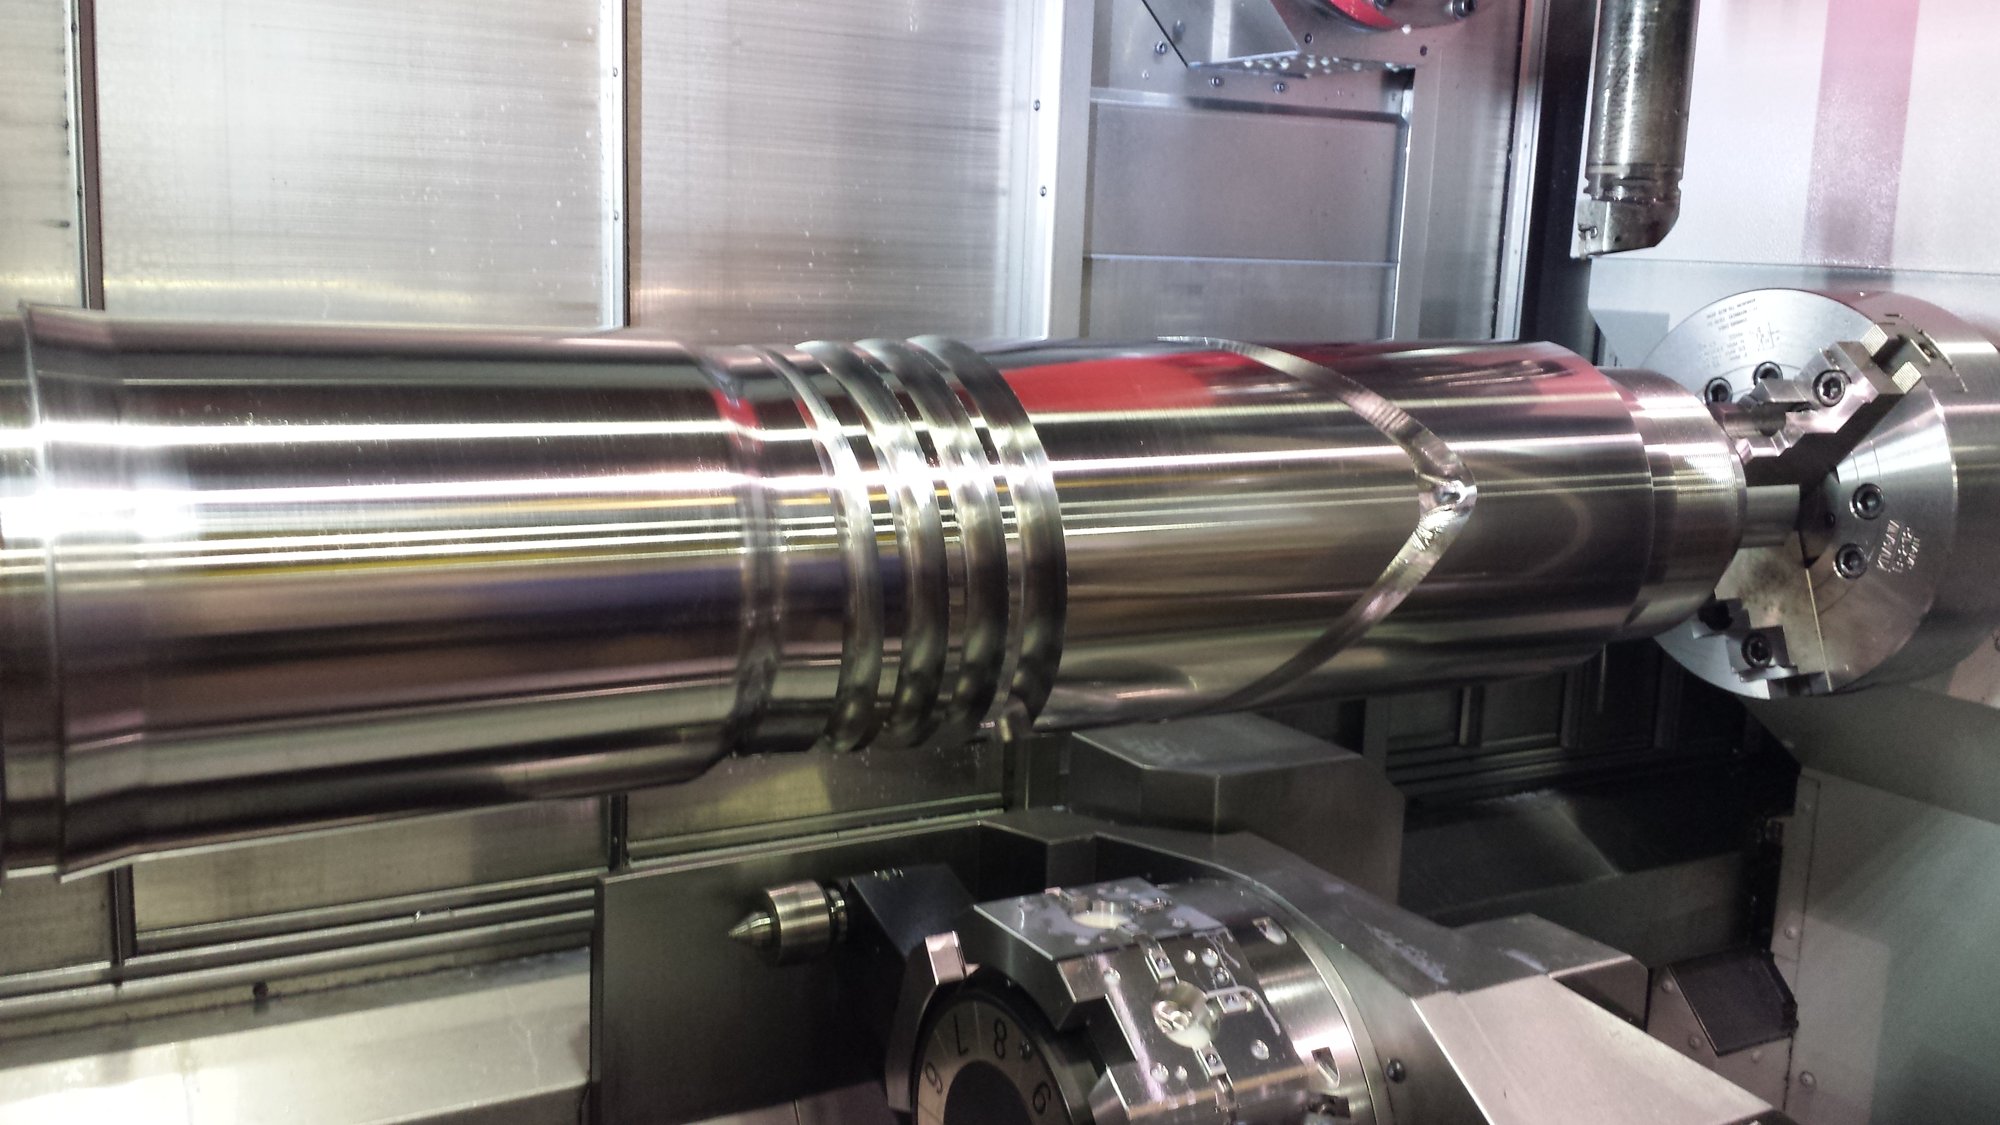
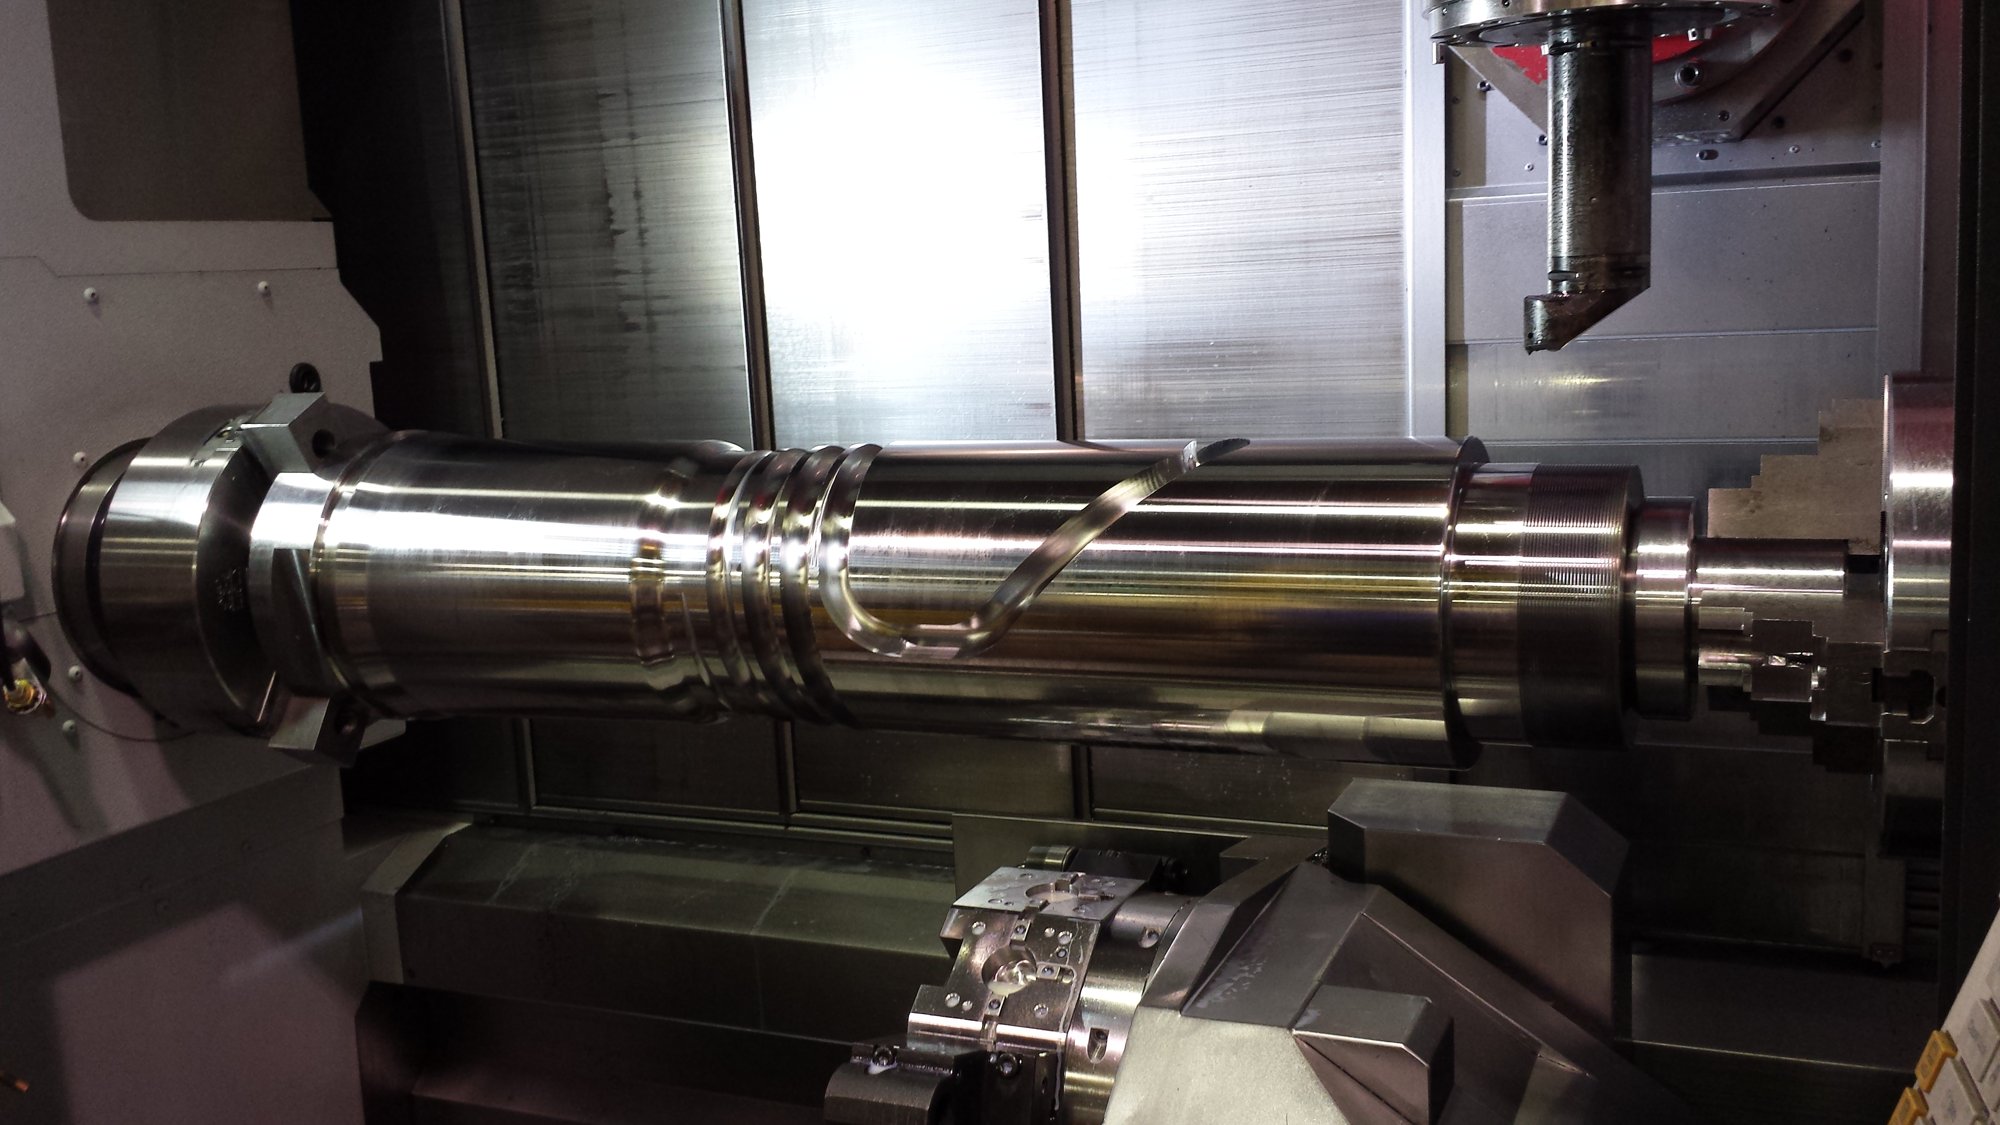
Extruder screw running in the CNC mill-turn, helical flights and mixing section cut on one setup
Extruder parts: Extruder screw running in the CNC mill-turn
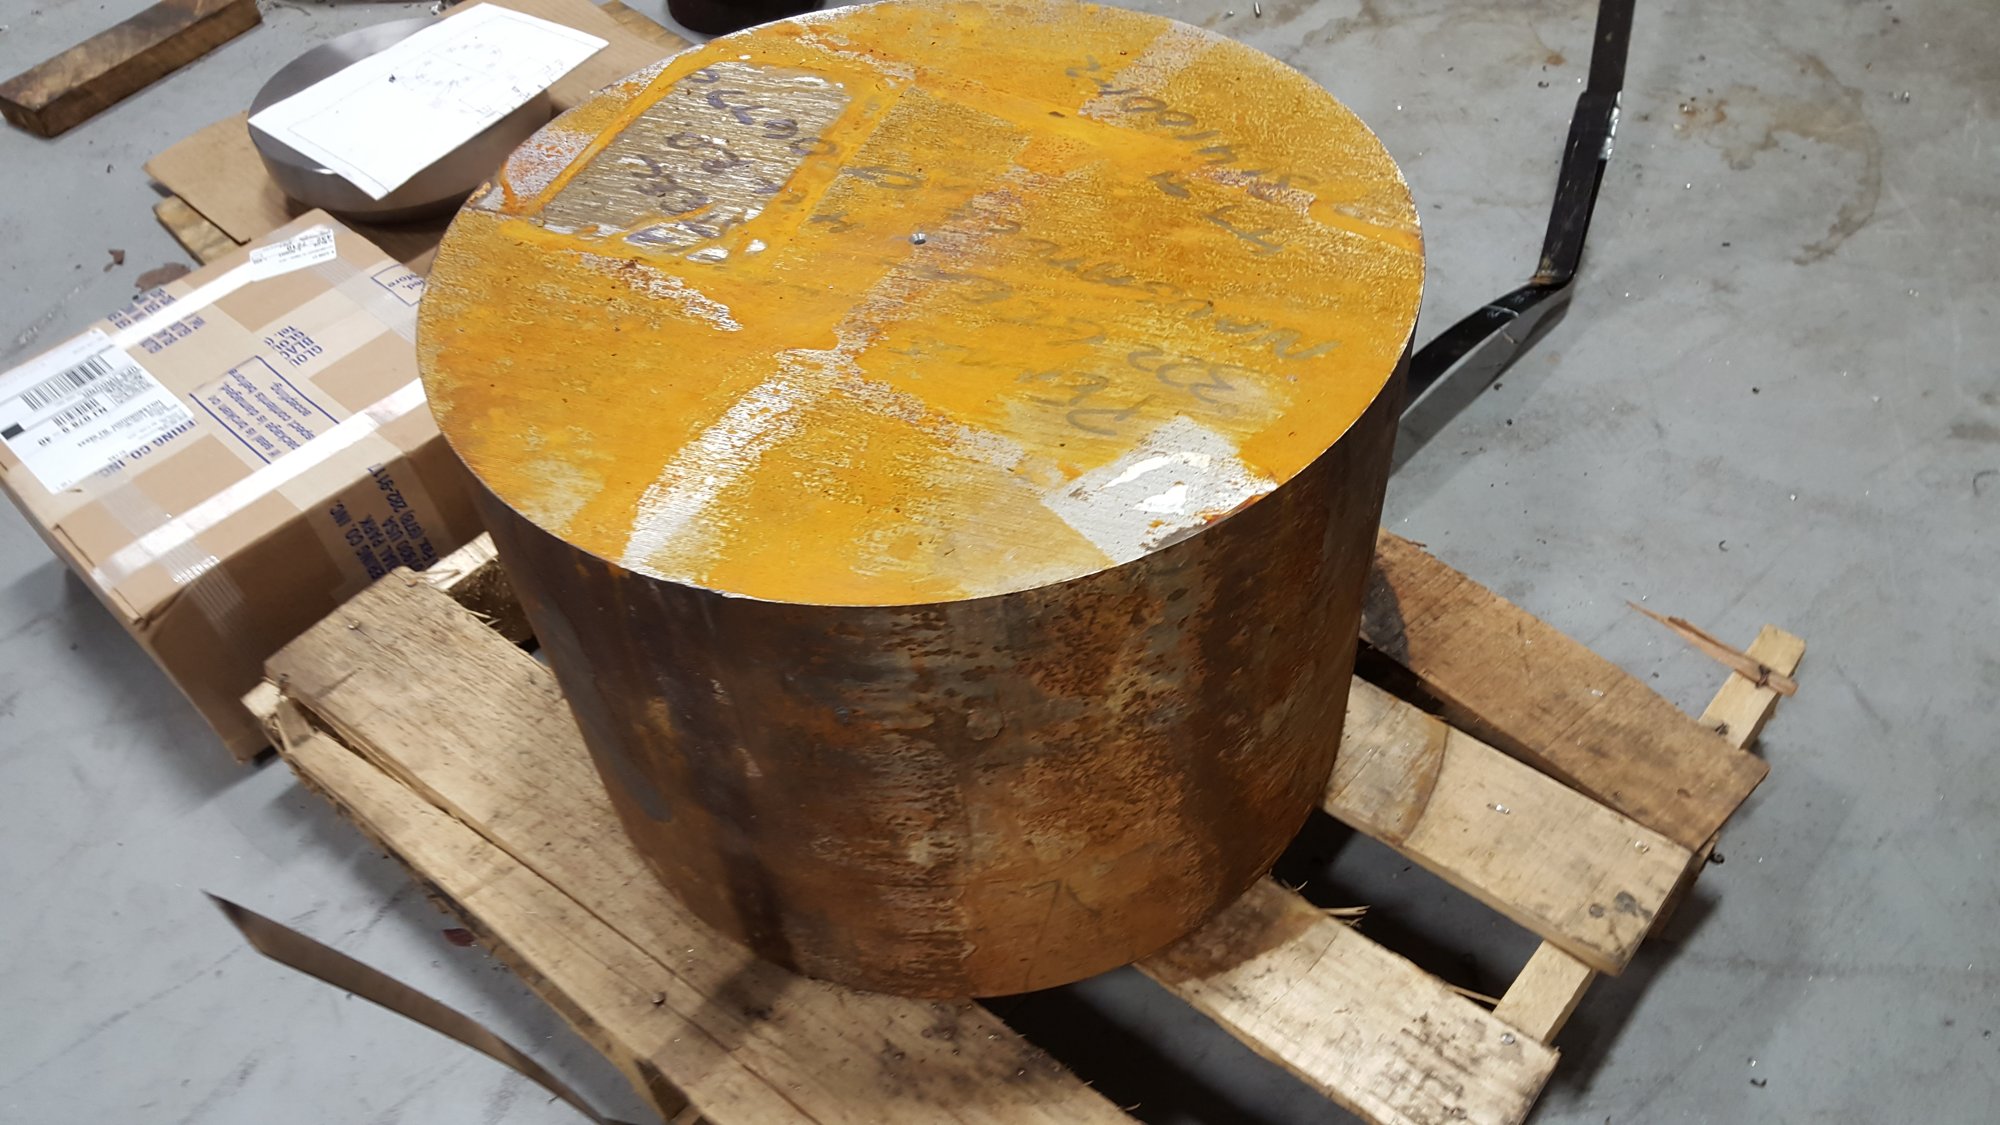
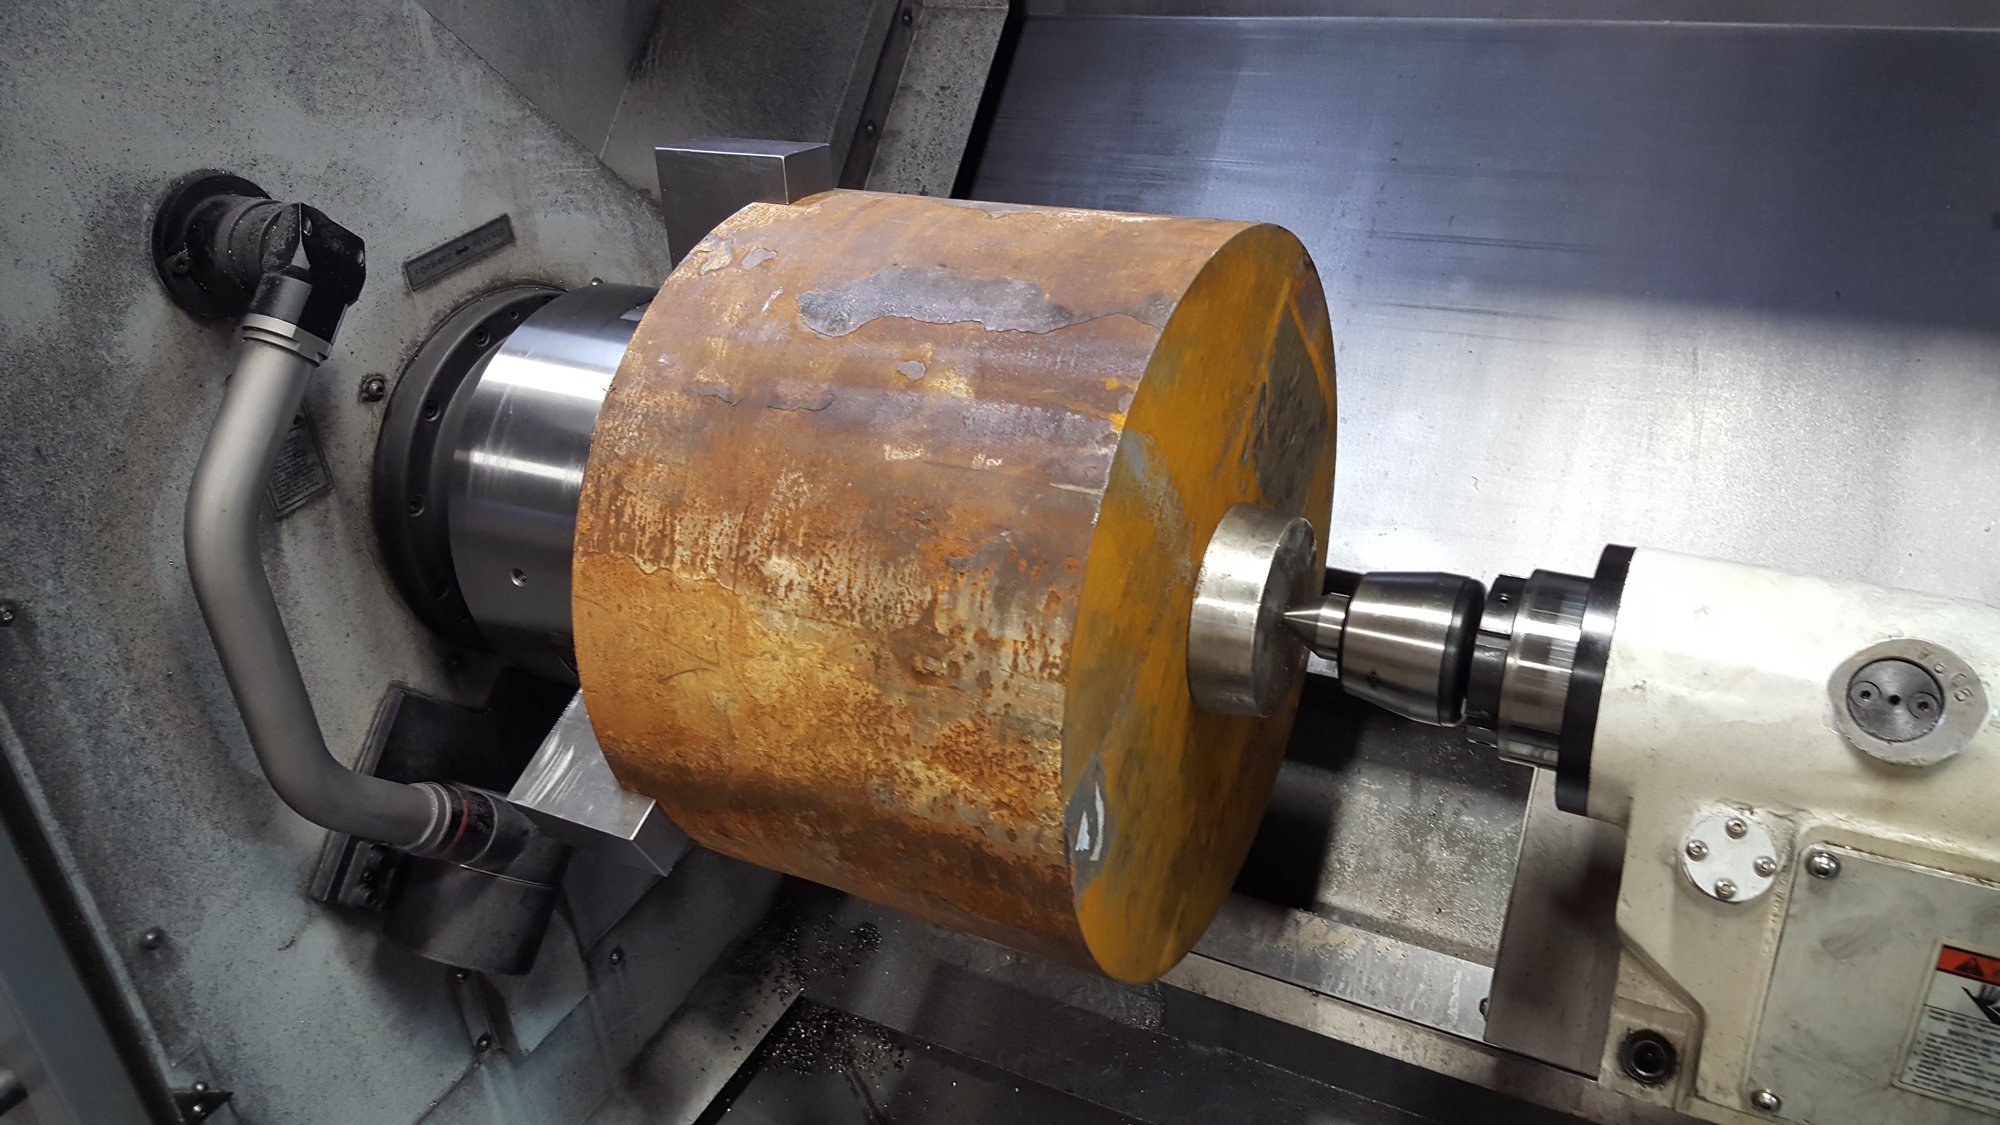
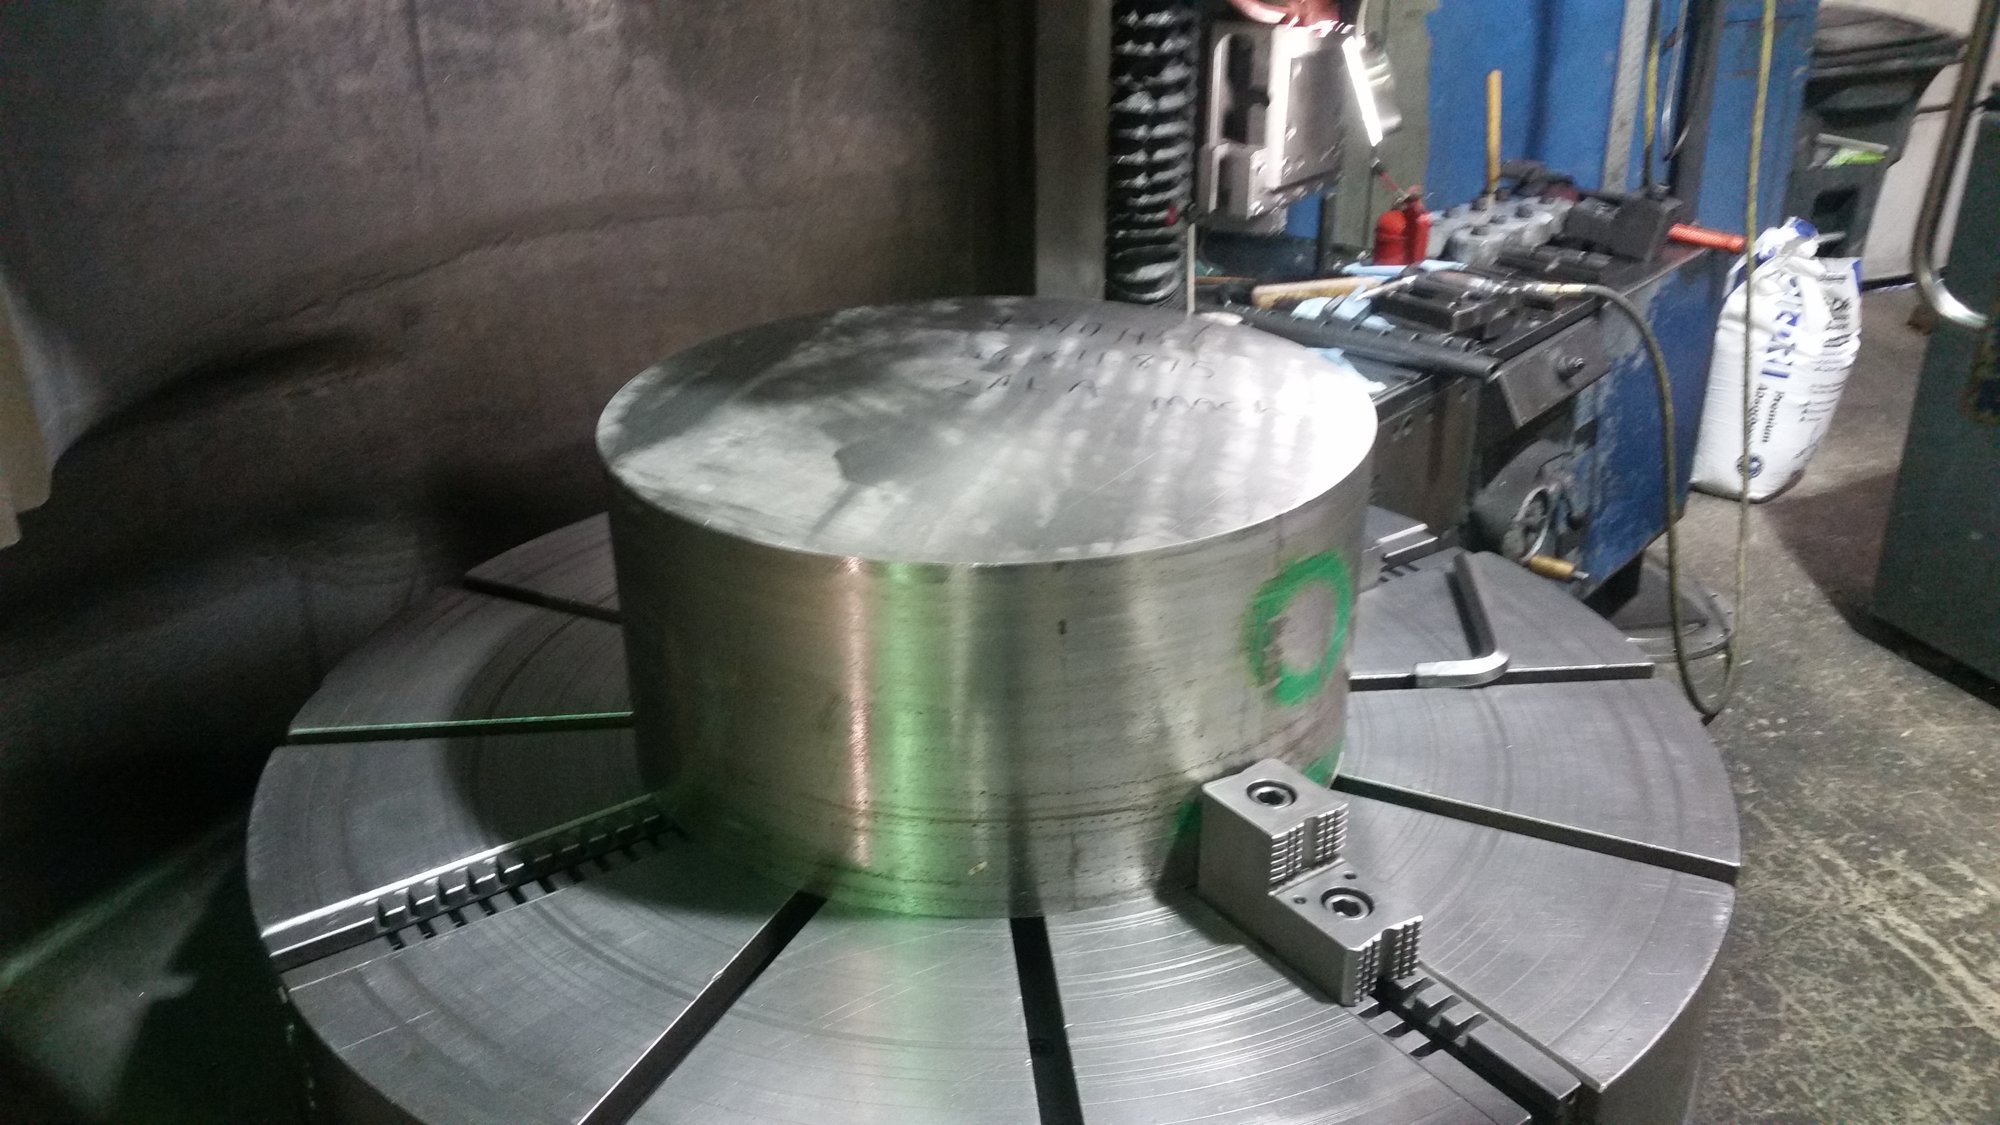
Round steel billet on the pallet, the starting stock for a three-layer blown film die block
One die, start to finish (1 of 10): The billet arrives — round steel stock on the pallet
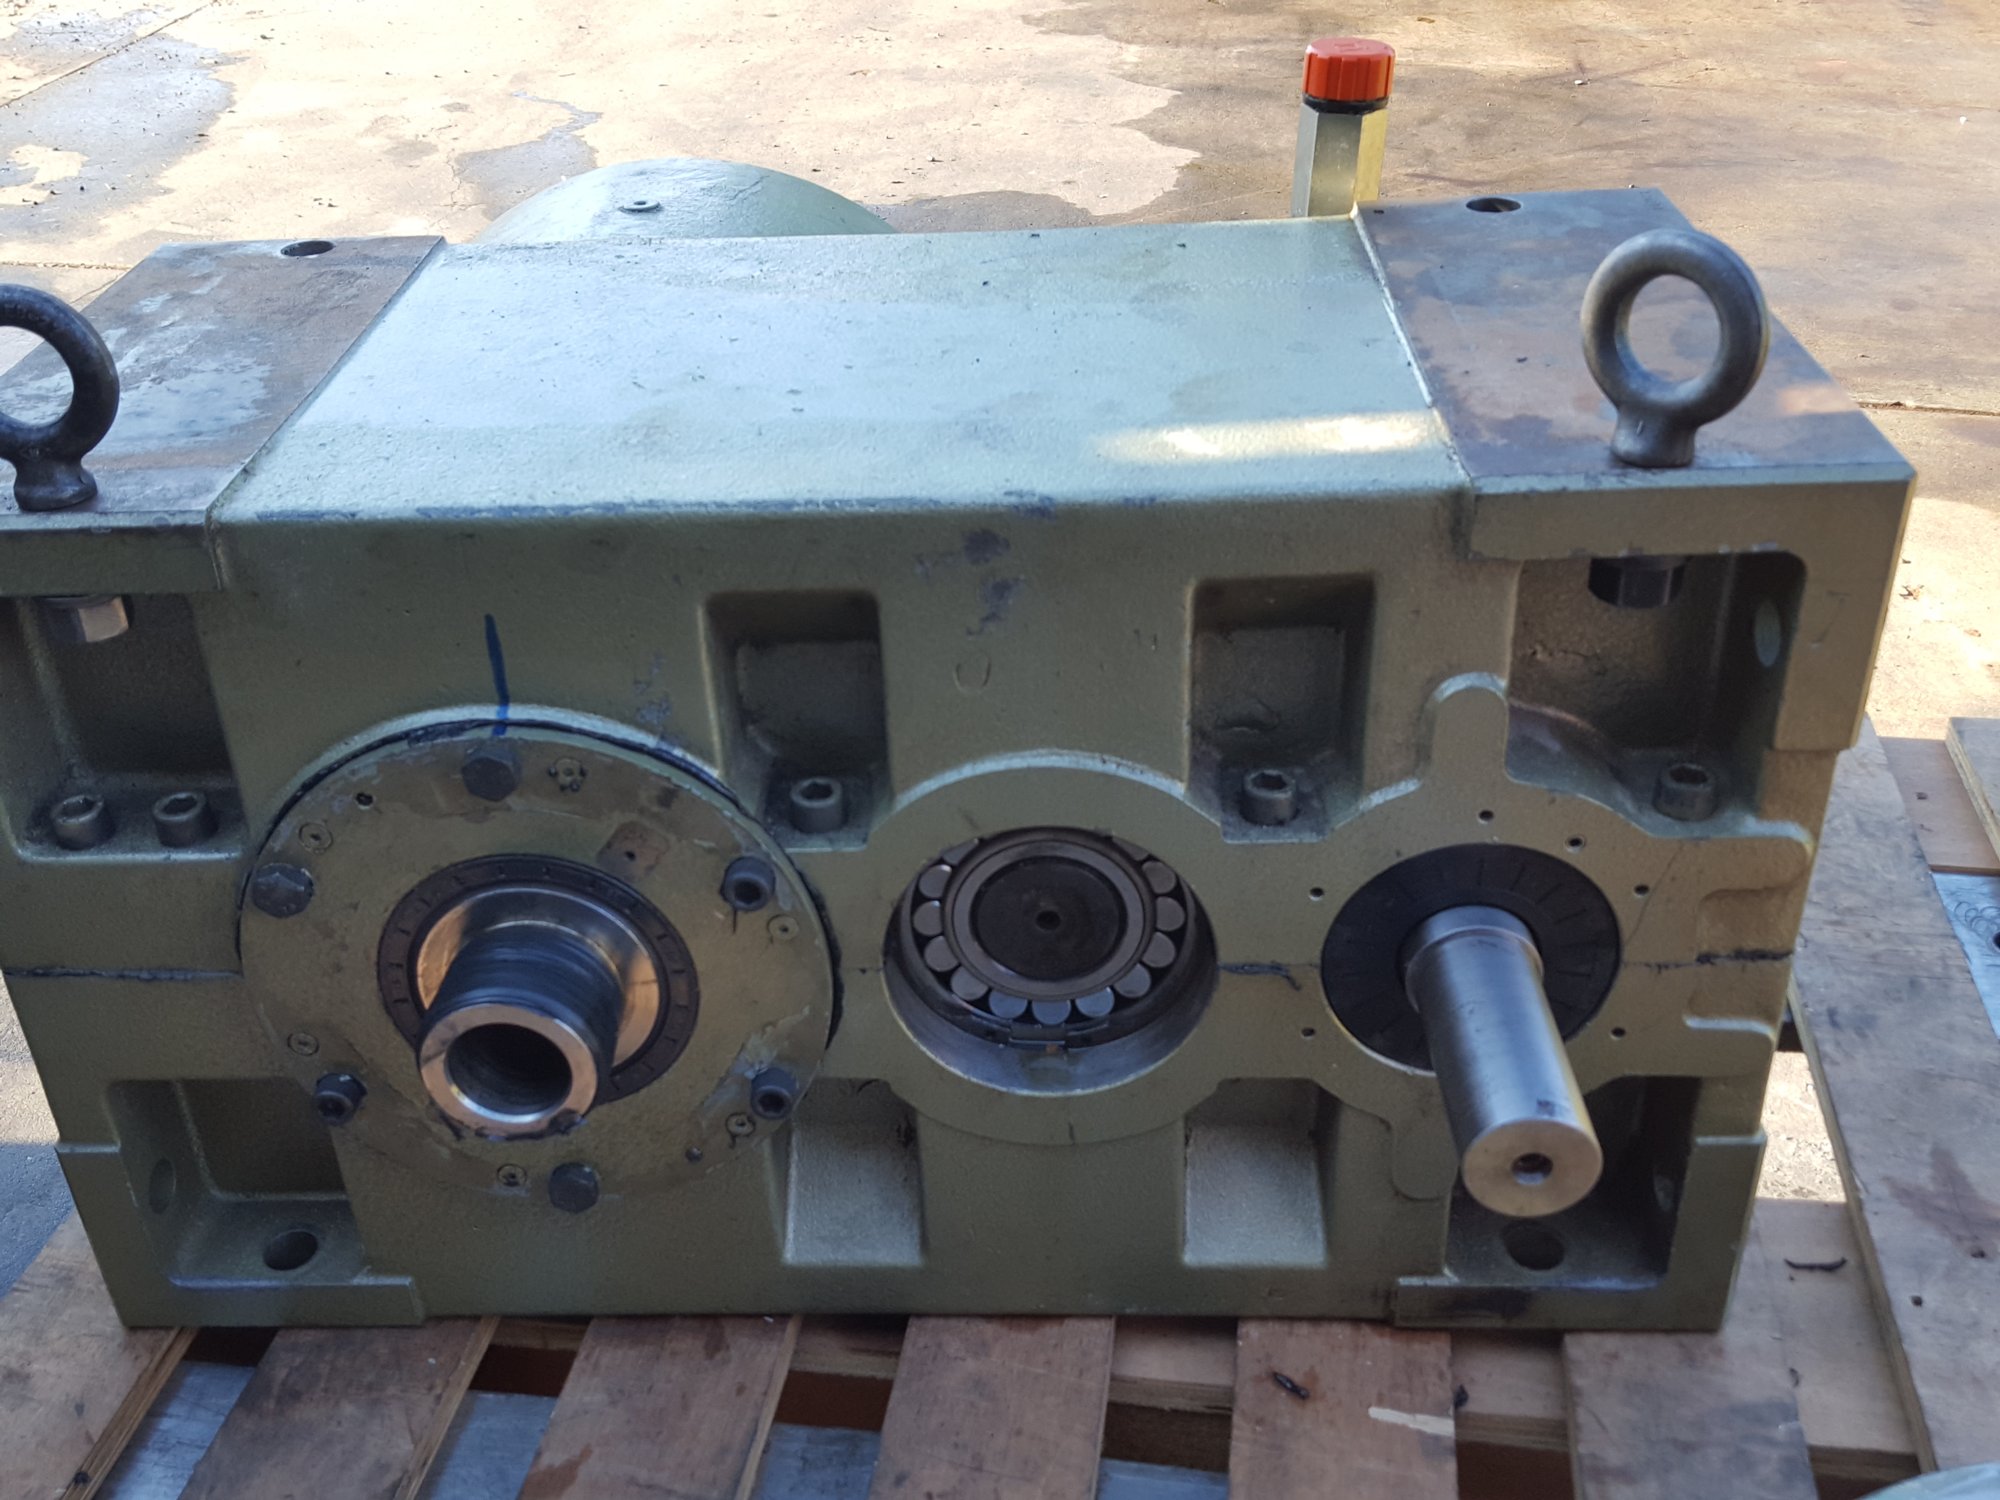
Twin-screw extruder gearbox opened for inspection, showing the helical gear train and bearings in the housing
Gearbox repair: Twin-screw extruder gearbox opened for inspection
Large stepped extrusion die body machined from solid steel
Blown film dies: Large stepped die body machined from solid steel
Fabricated machine base weldment clamped on the horizontal boring mill, bores opened up after welding
Fabrication and shipping: Welded machine base, bores opened up after welding
CAM model of a die plate on screen, toolpaths laid out around the bolt circle before cutting
The shop: CAM model of a die plate, toolpaths laid out
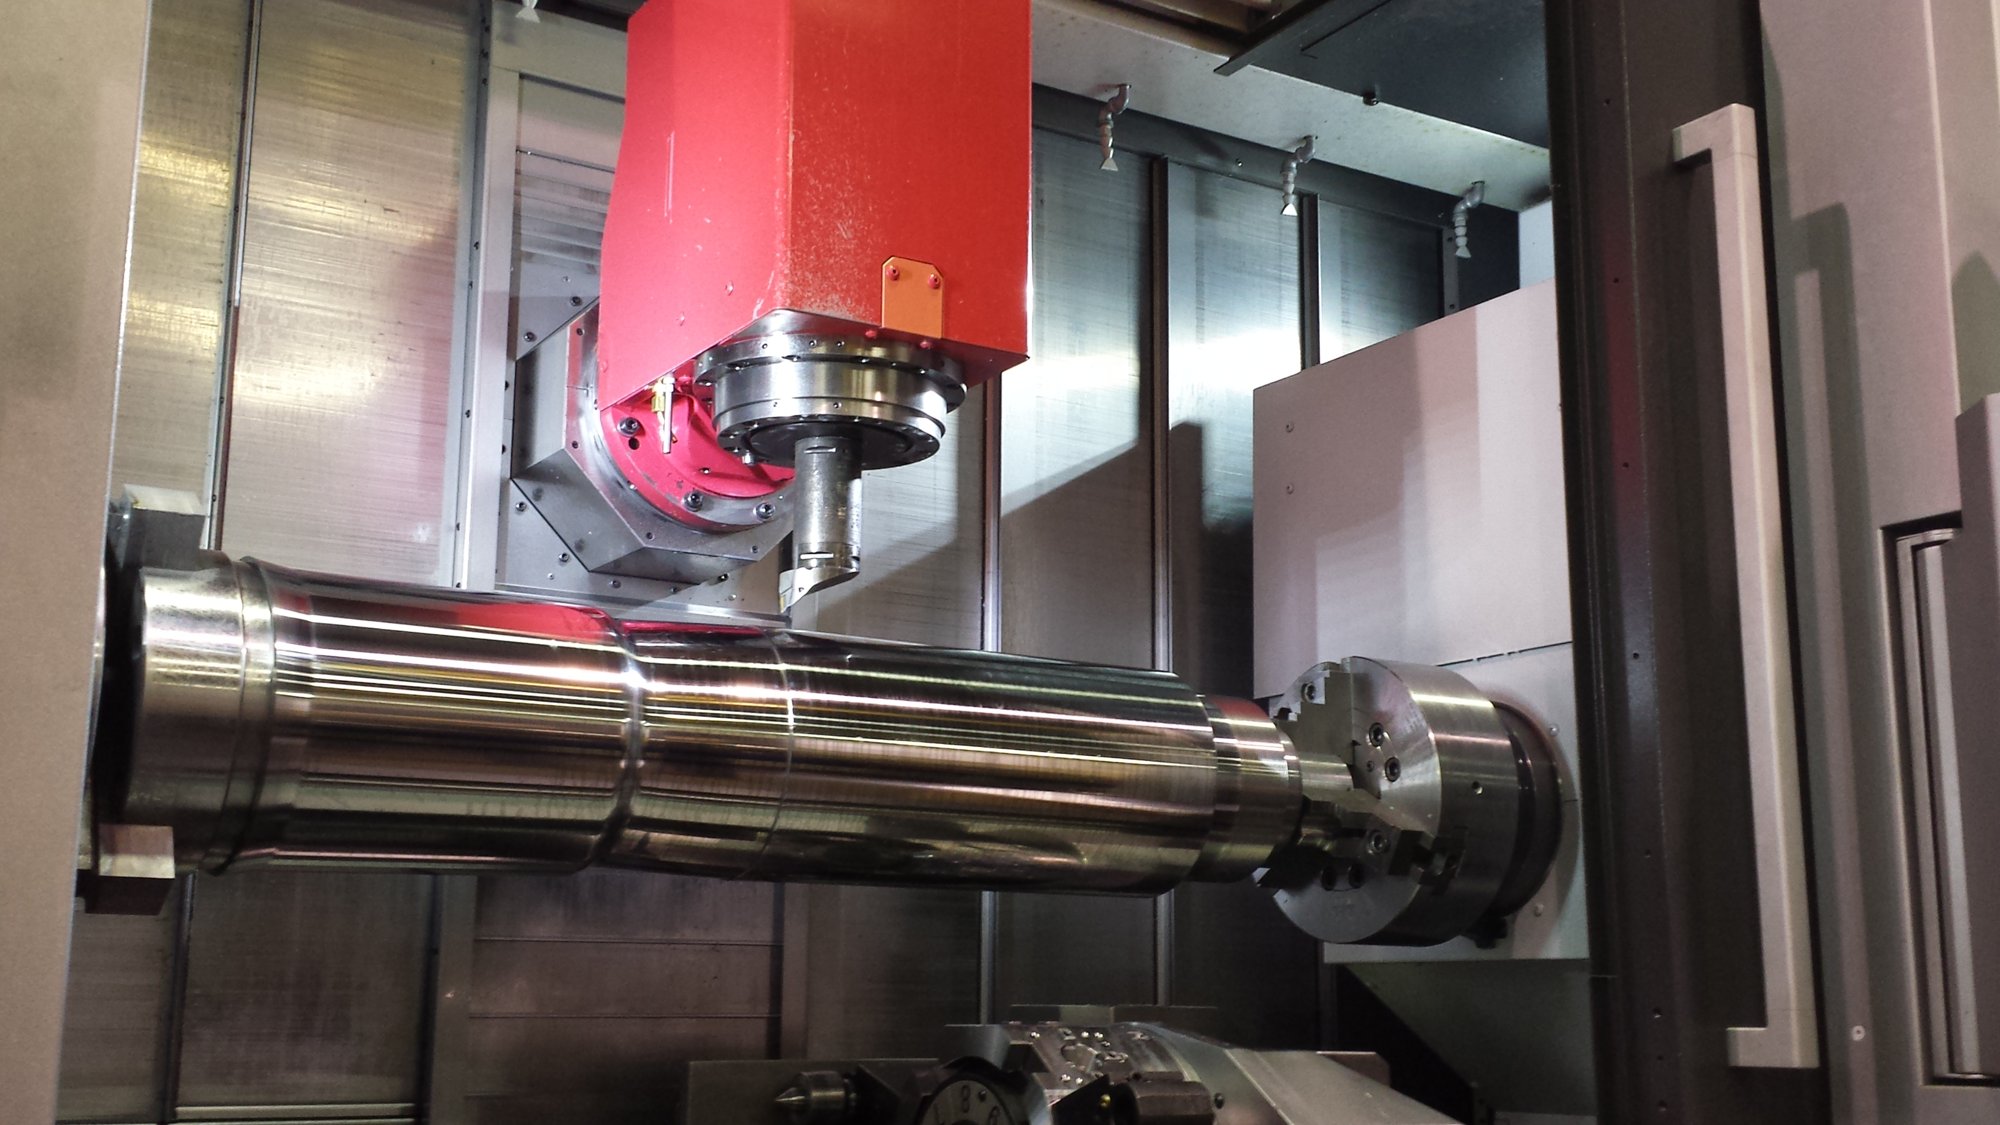
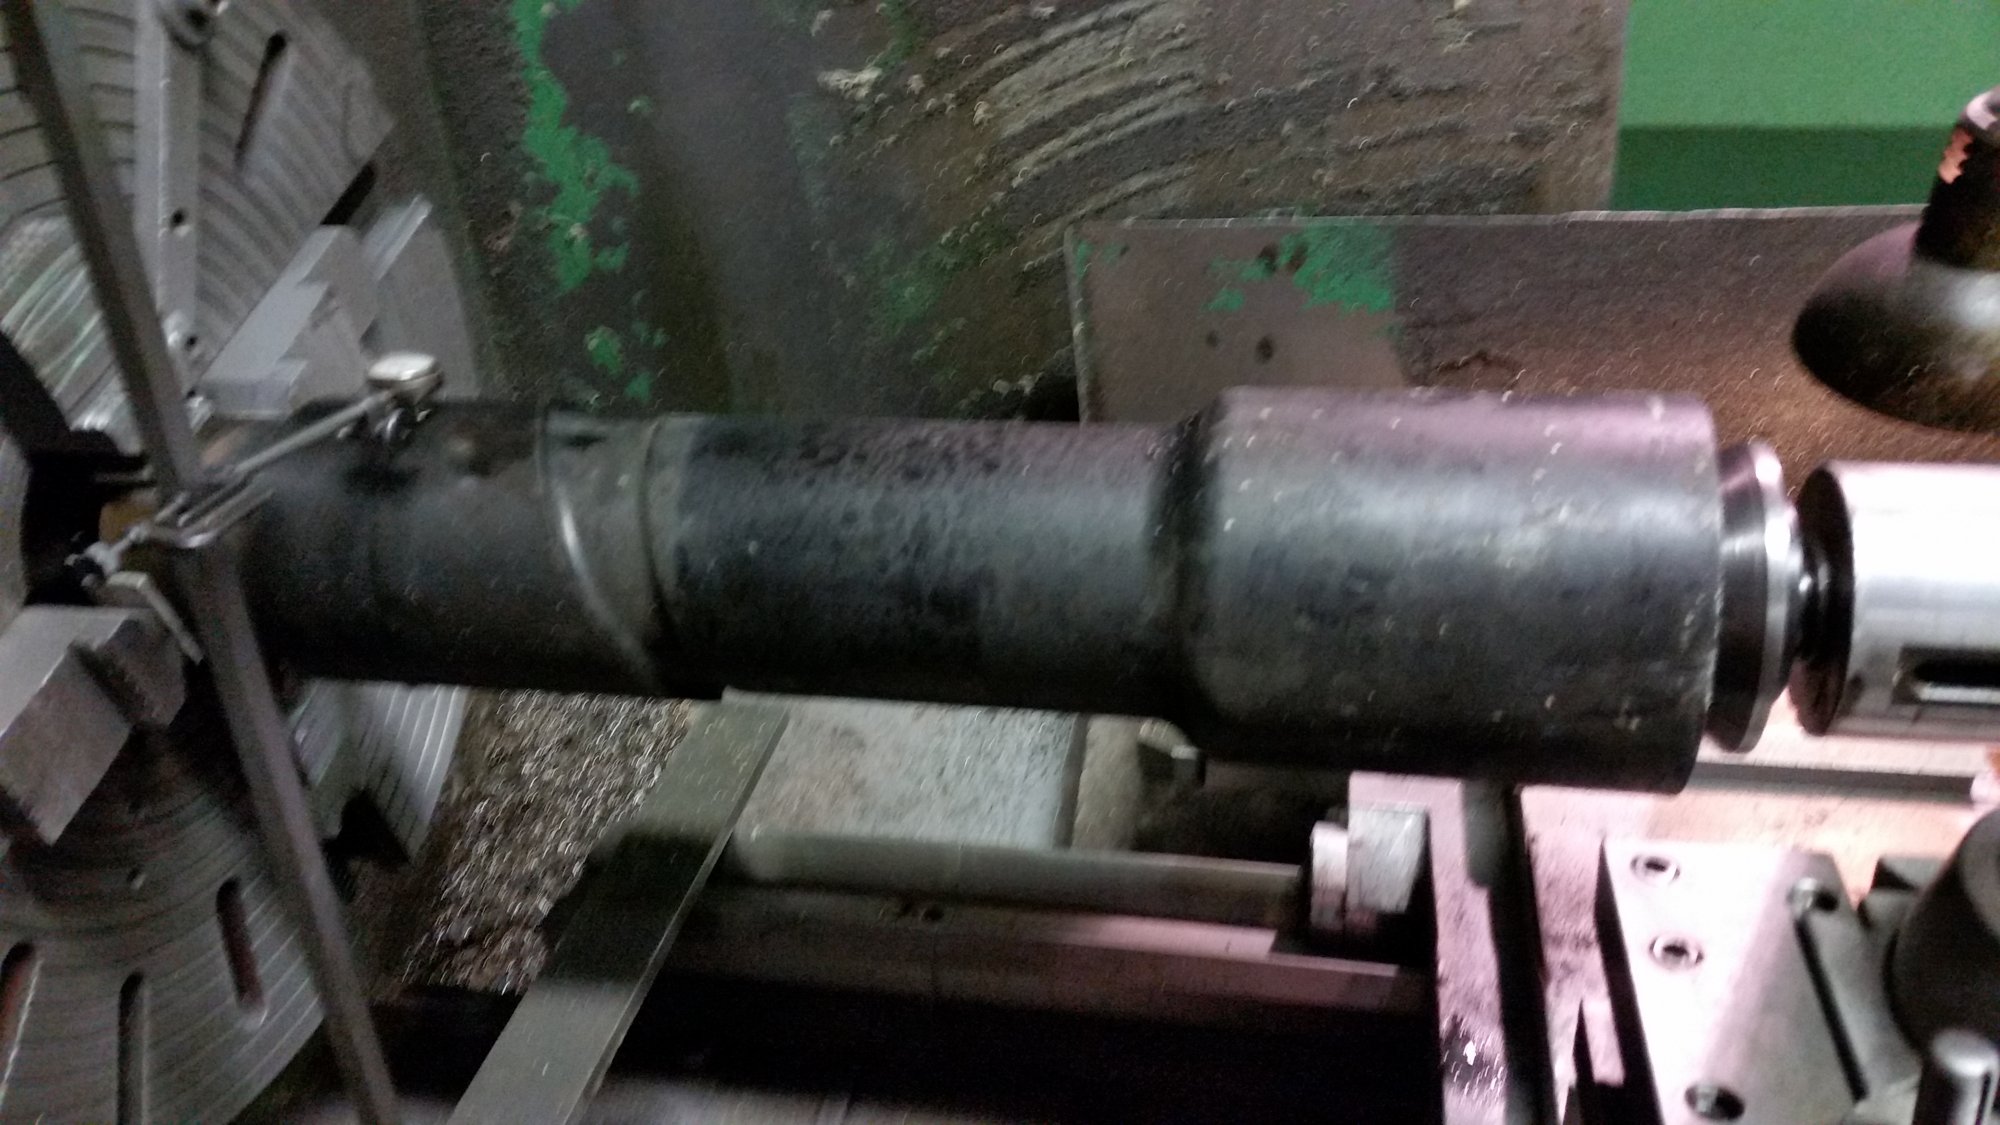
Large stepped shaft in the CNC lathe with its keyway milled, supported between chuck and tailstock
Shaft machining: Large stepped shaft with its keyway milled
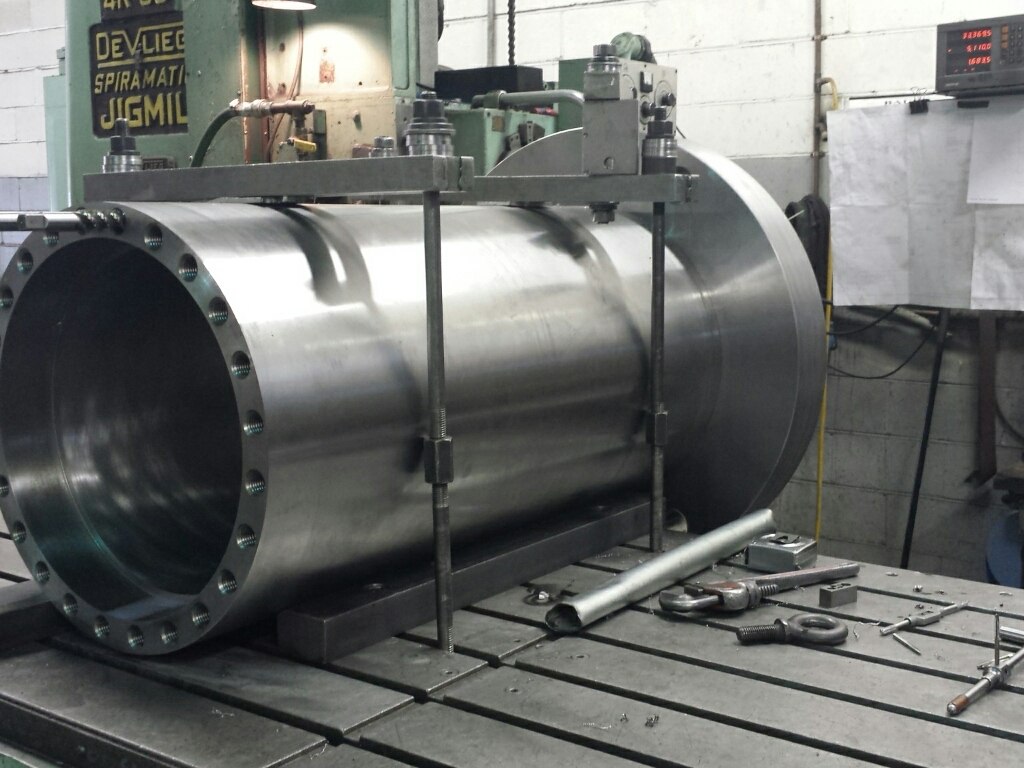
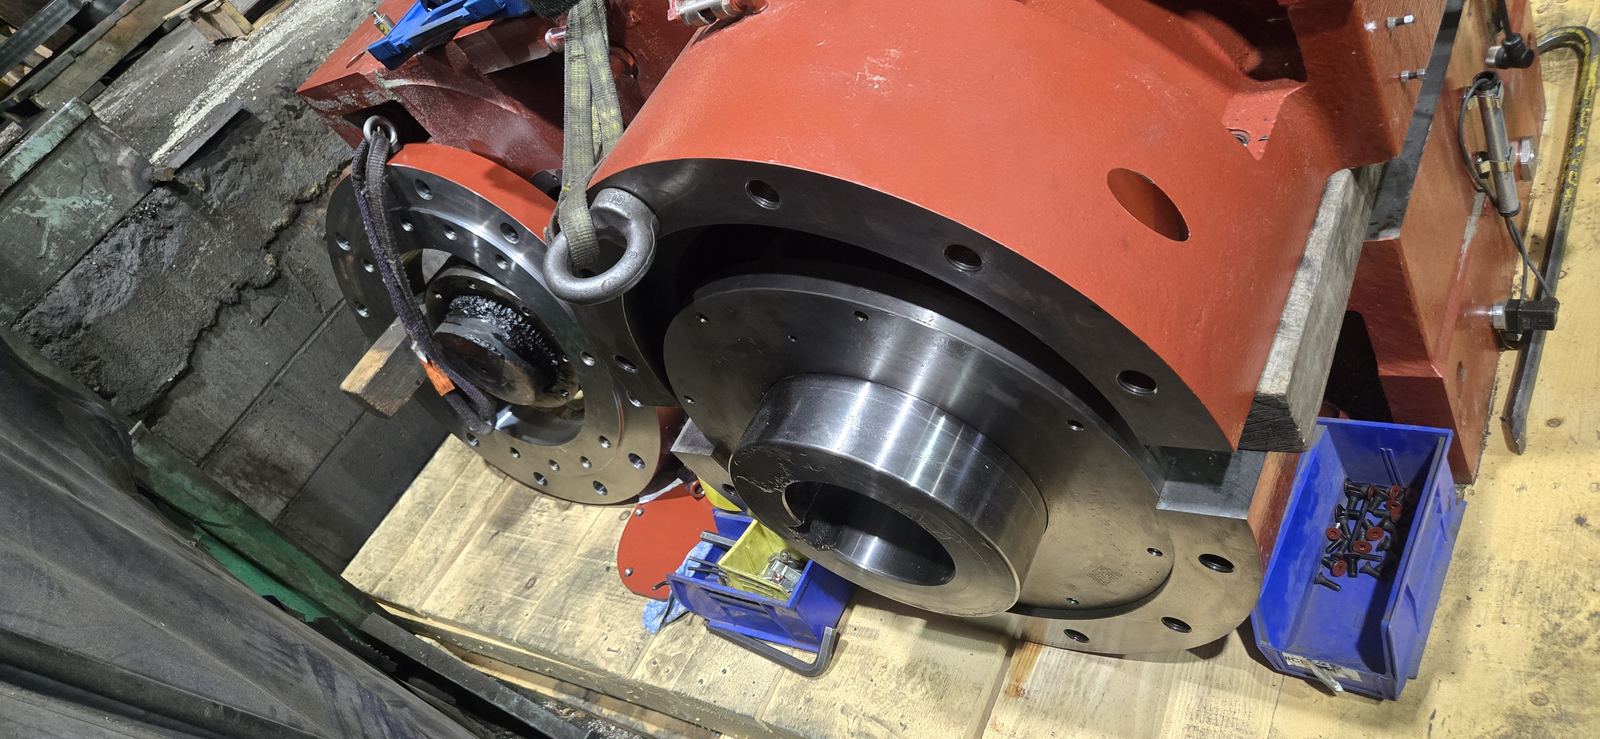
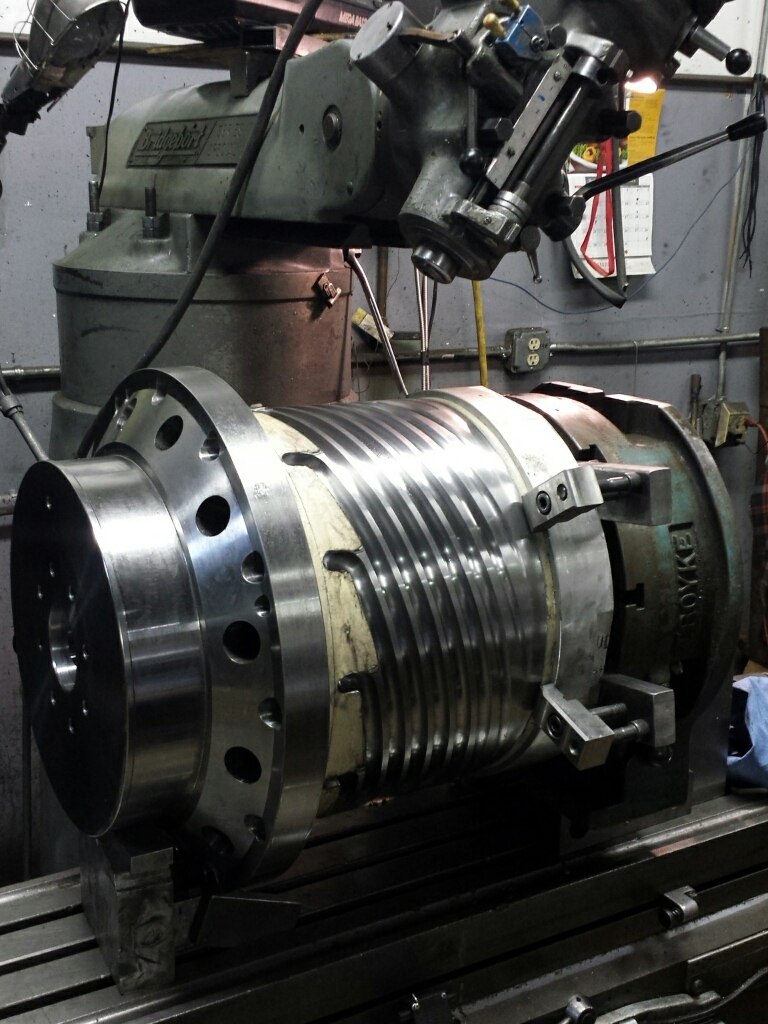
Large cylinder housing clamped on the DeVlieg jig mill, open bore and bolted flange to the front
Large machining: Cylinder housing clamped on the DeVlieg jig mill
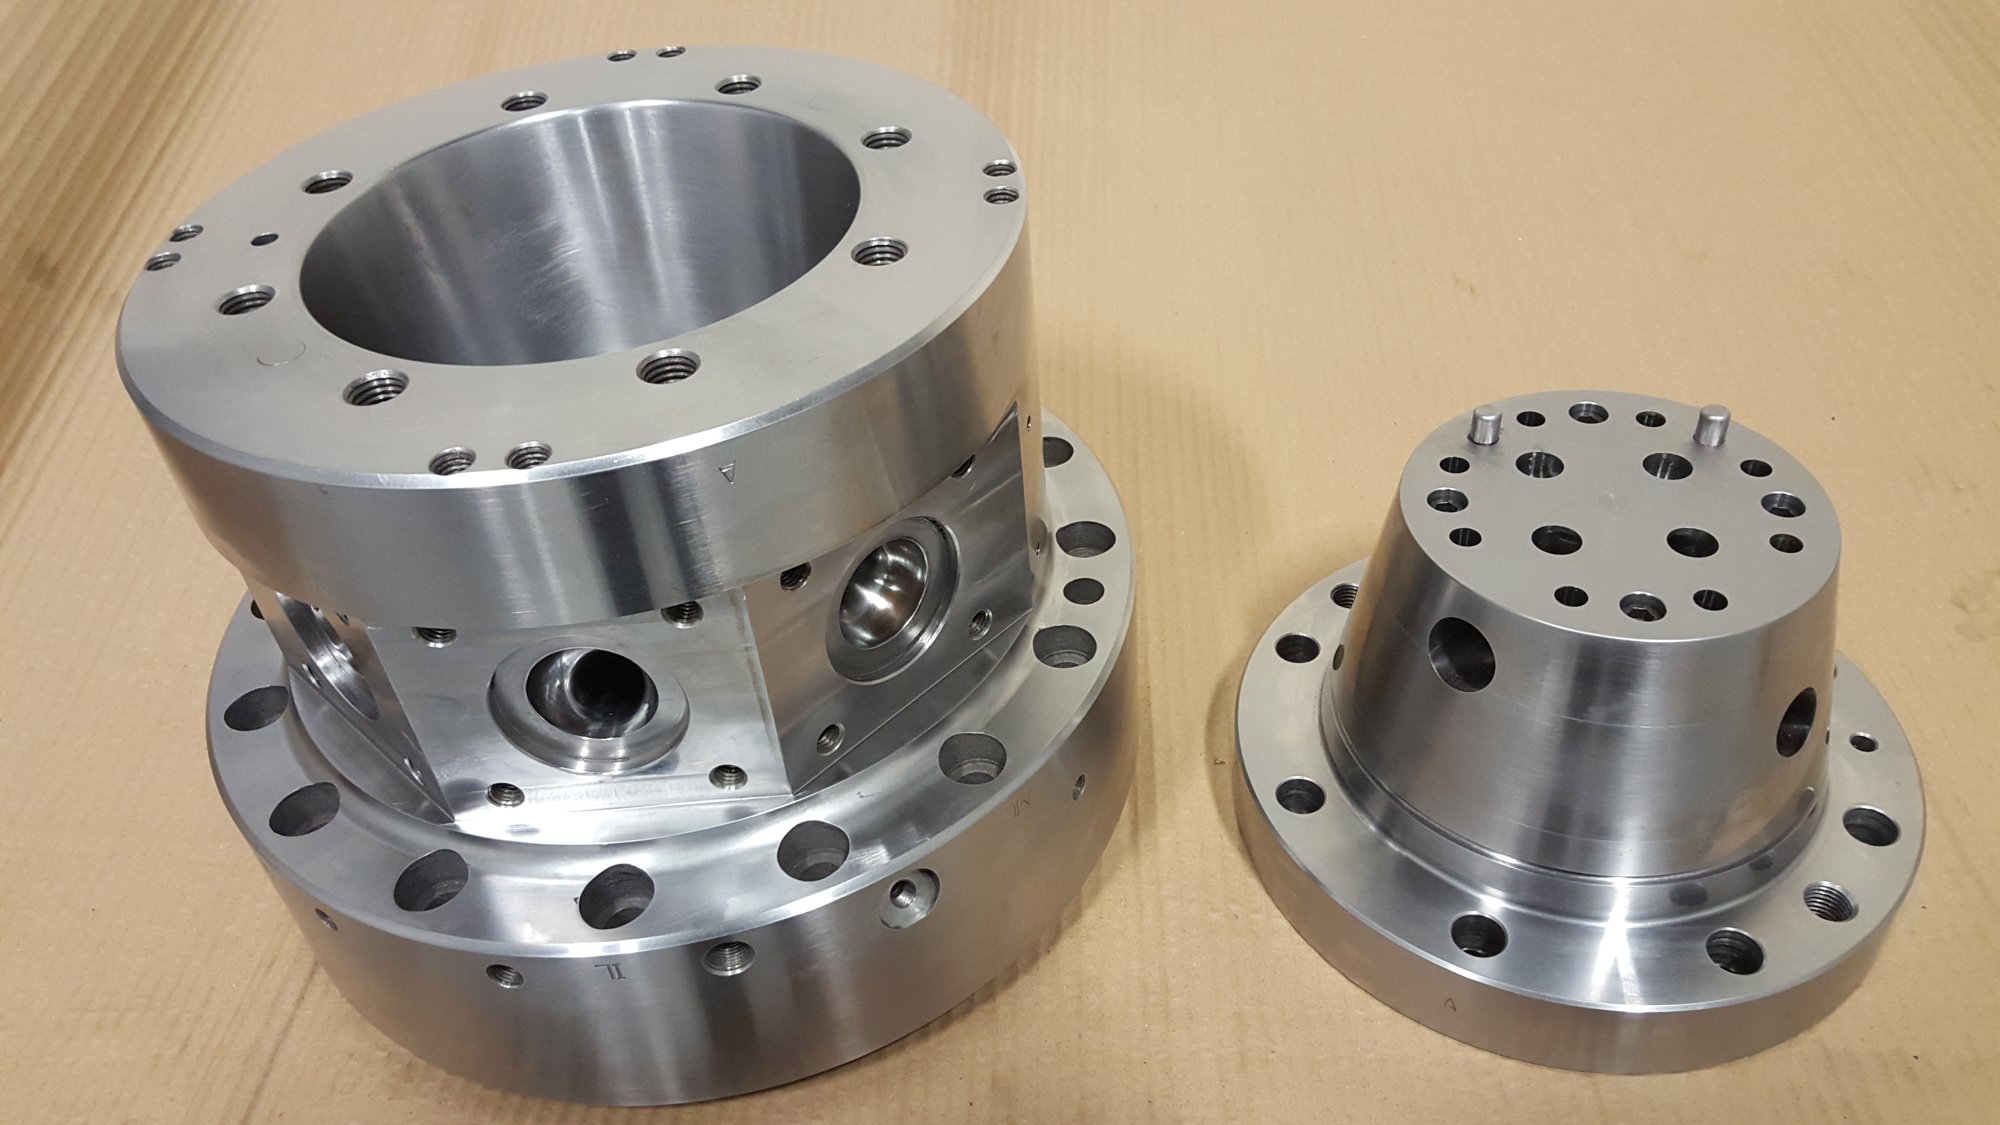
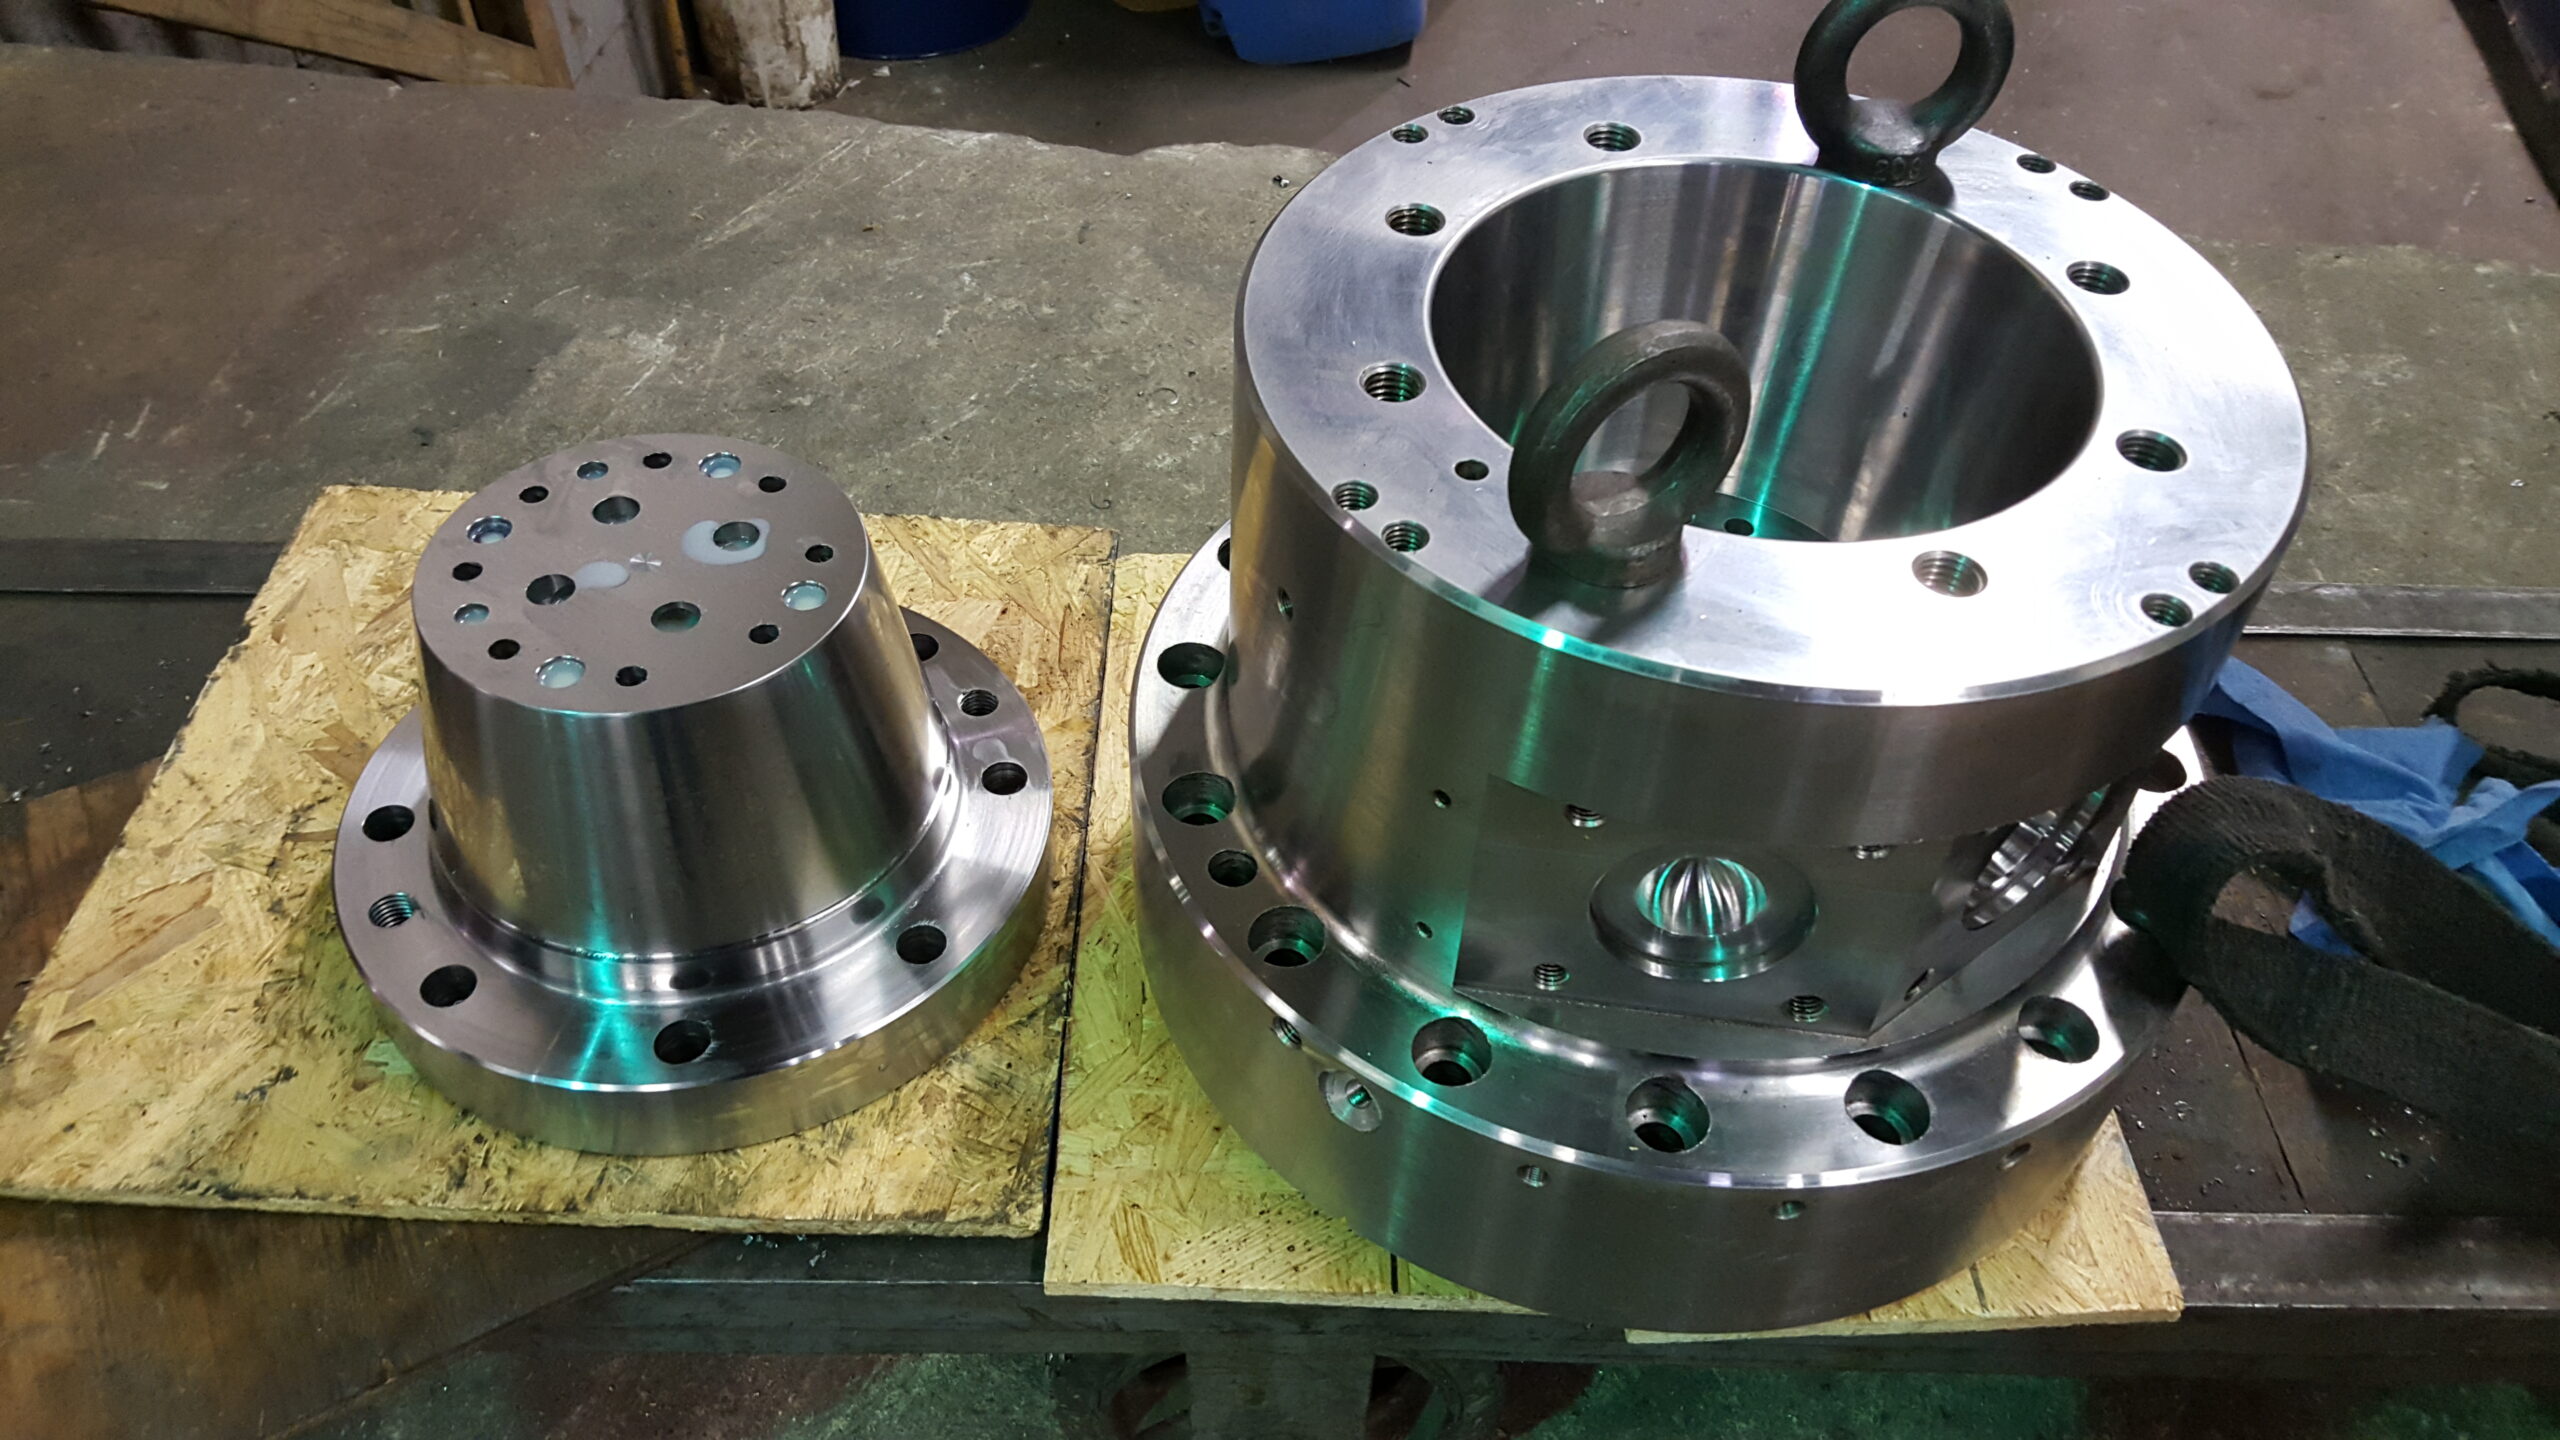
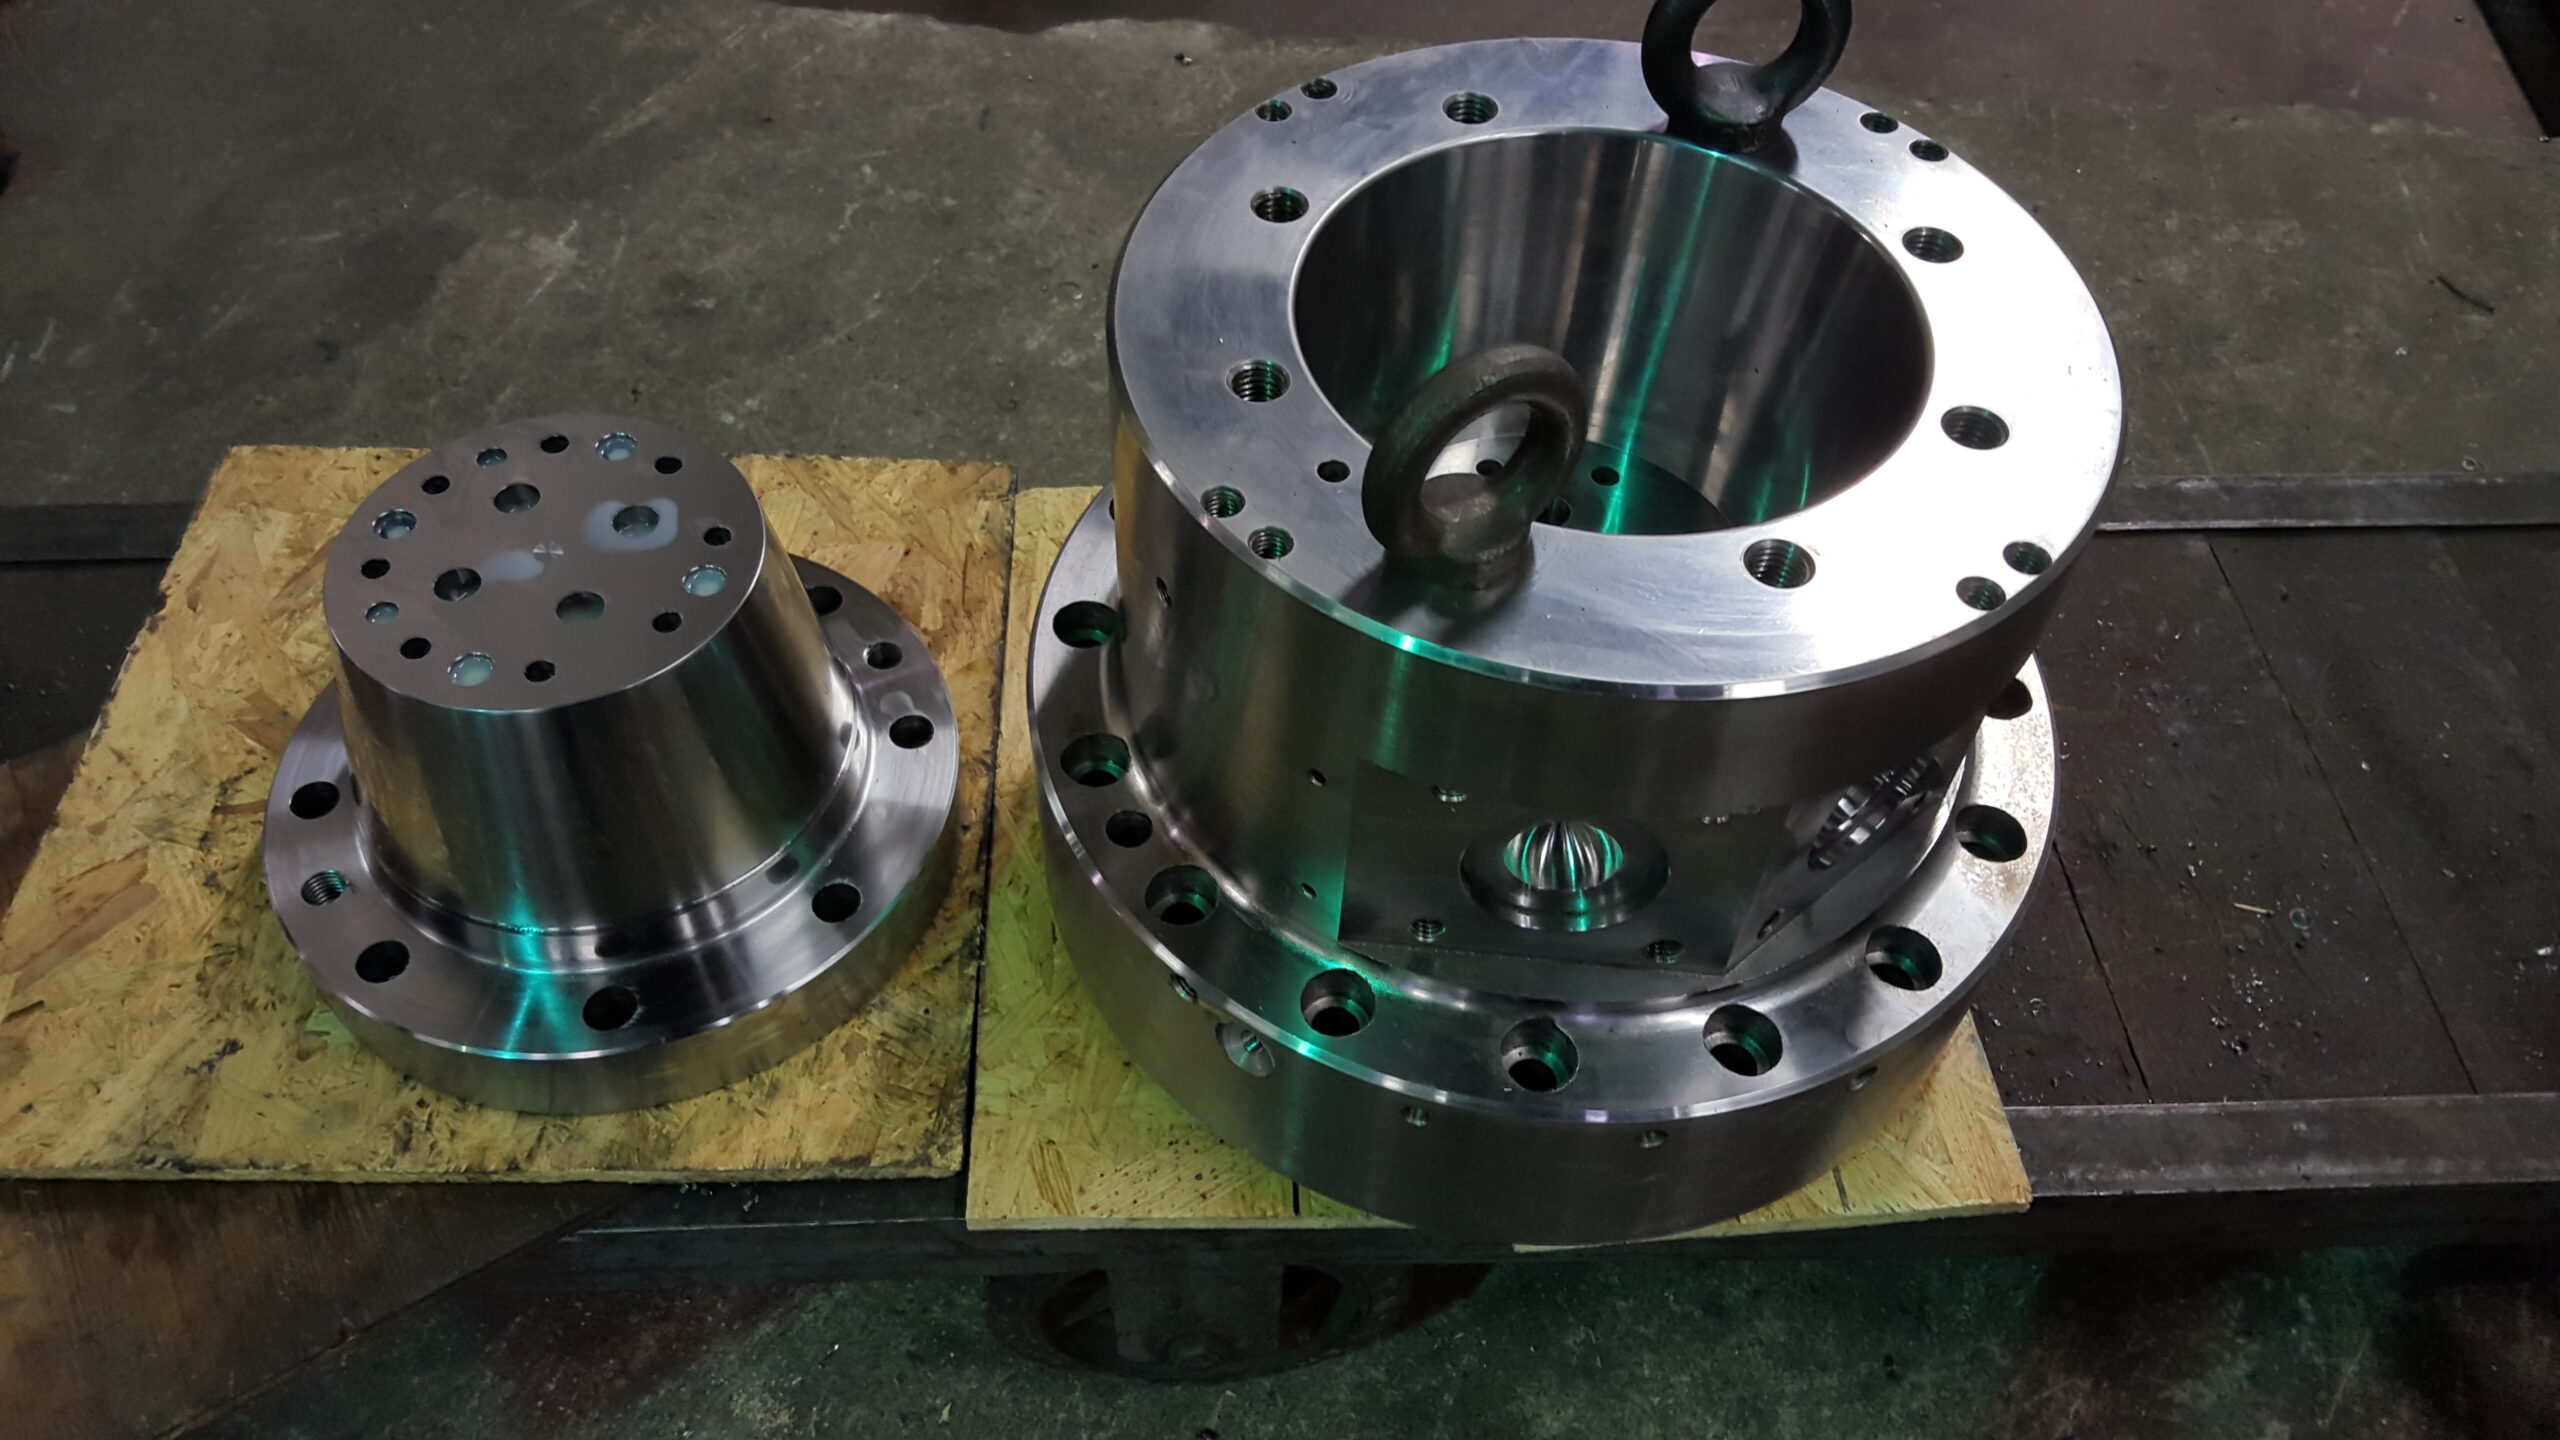
Two finished multi-layer blown film die components side by side, side ports and drilled port face
Blown film dies: Two die components, side ports and drilled port face
Four CNC-turned shafts from one run, coarse threads and milled keyways, finished on the bench
Turning and production: Four turned shafts from one run, threads and keyways
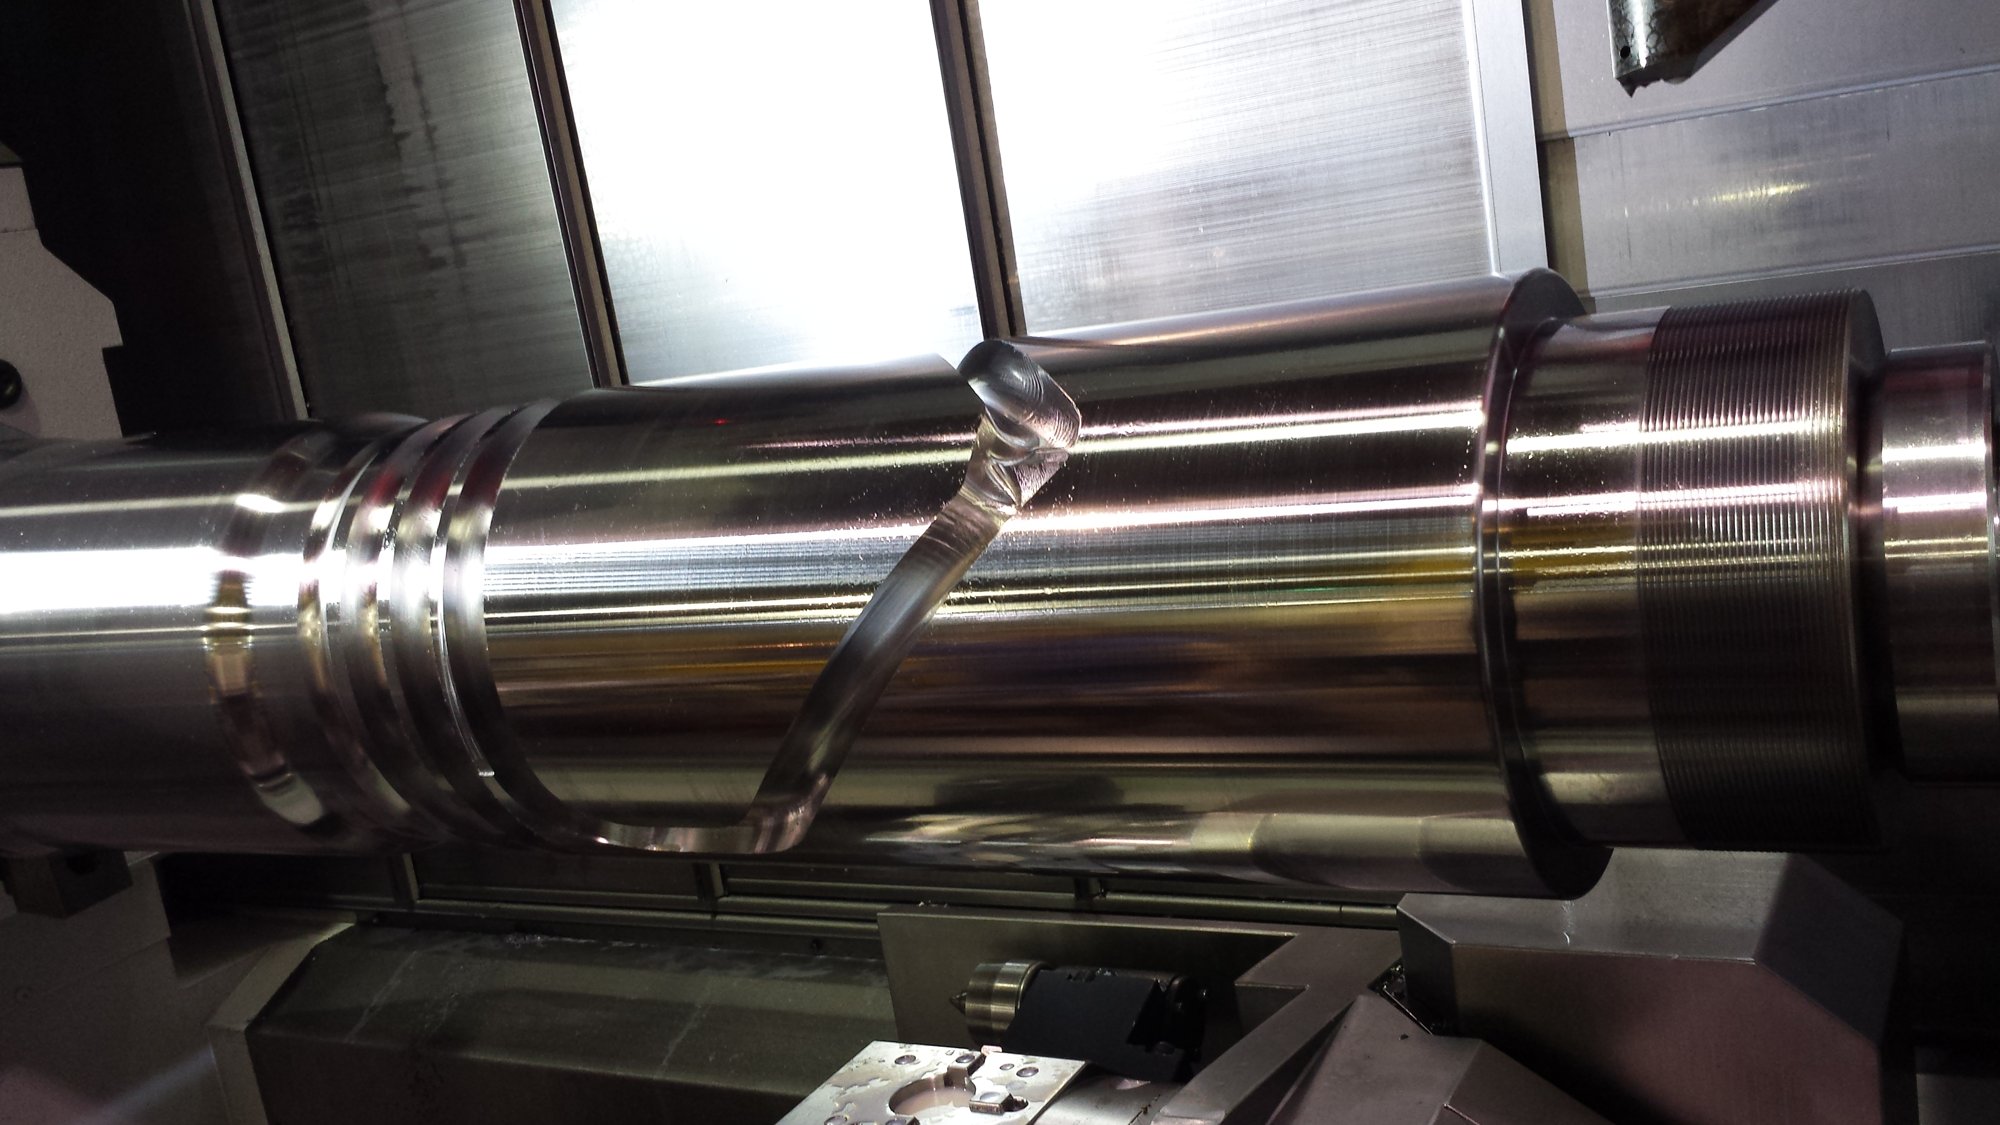
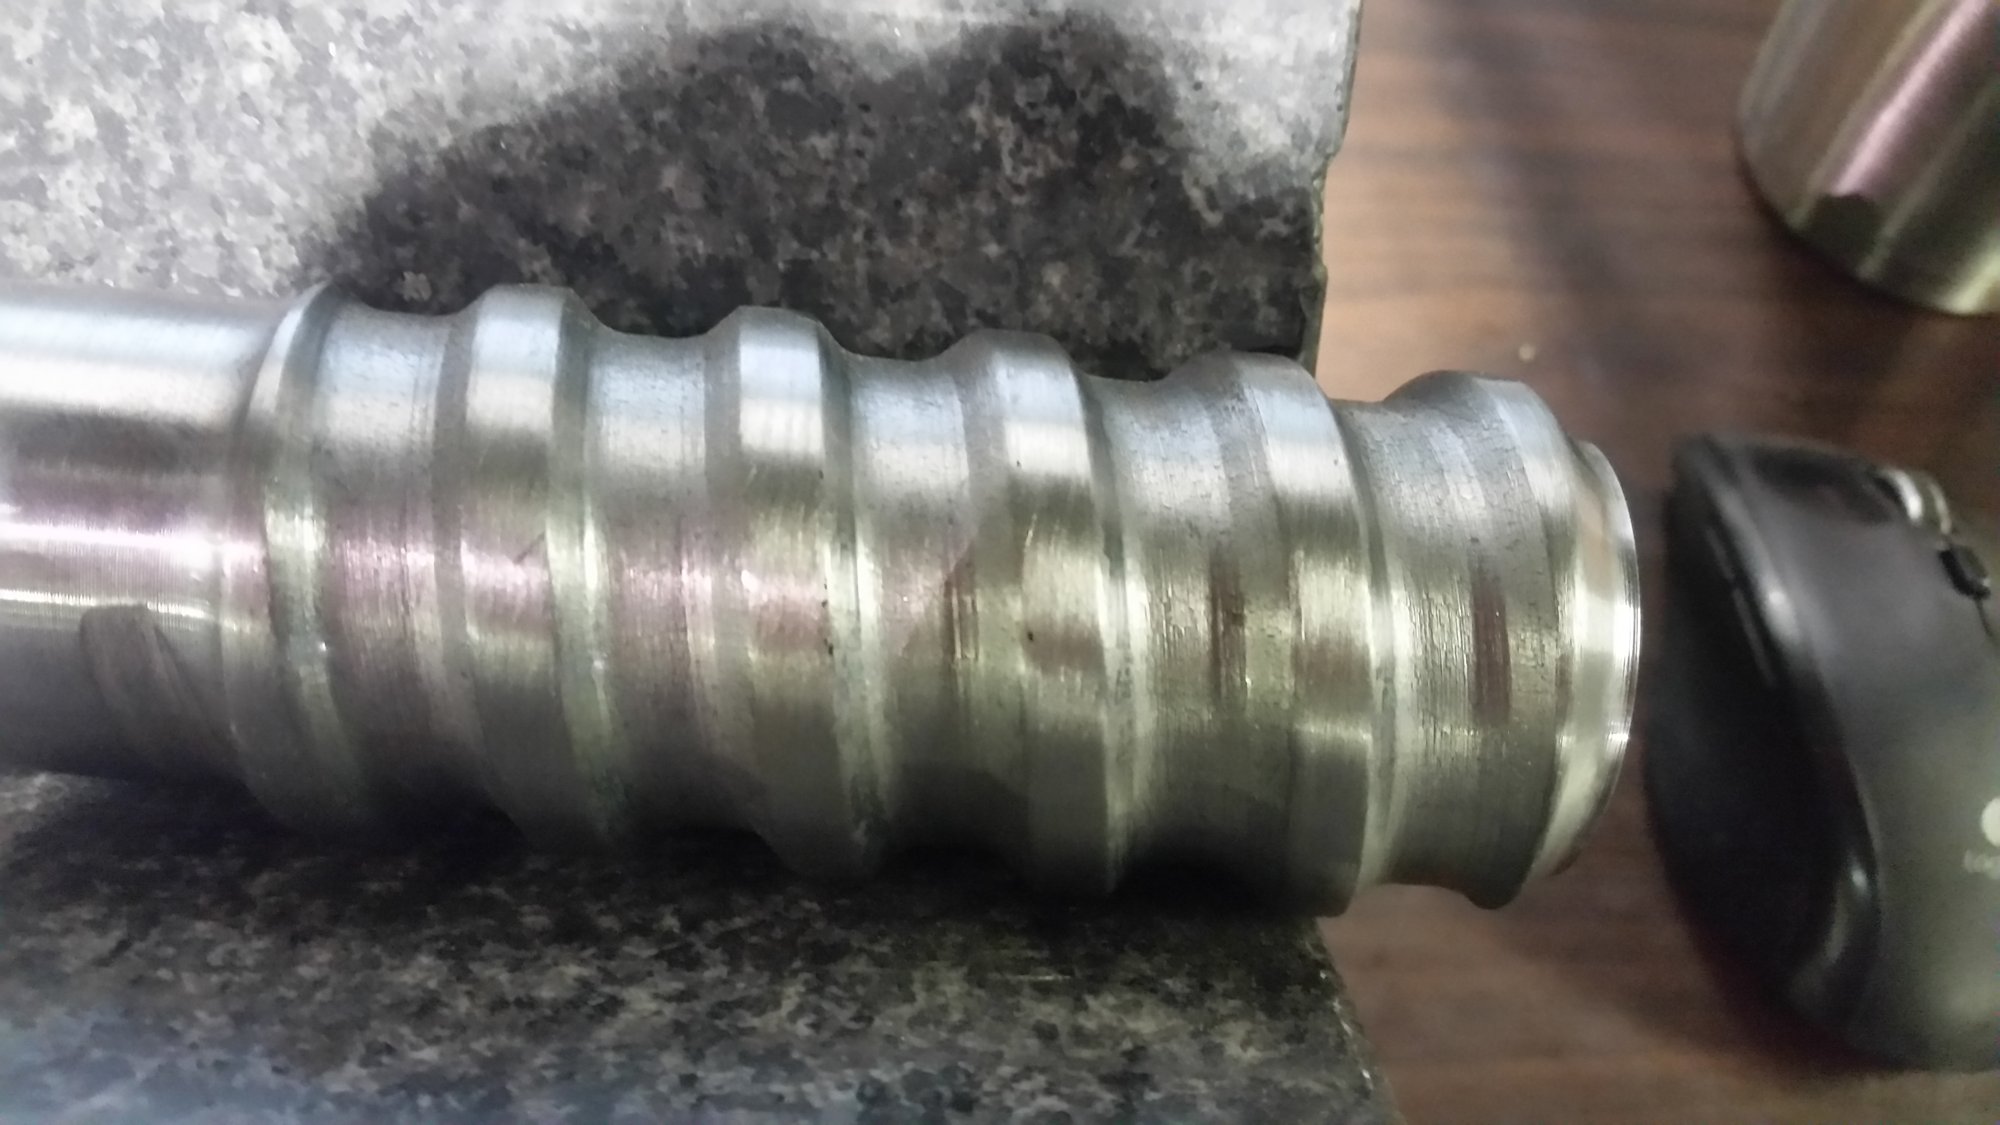
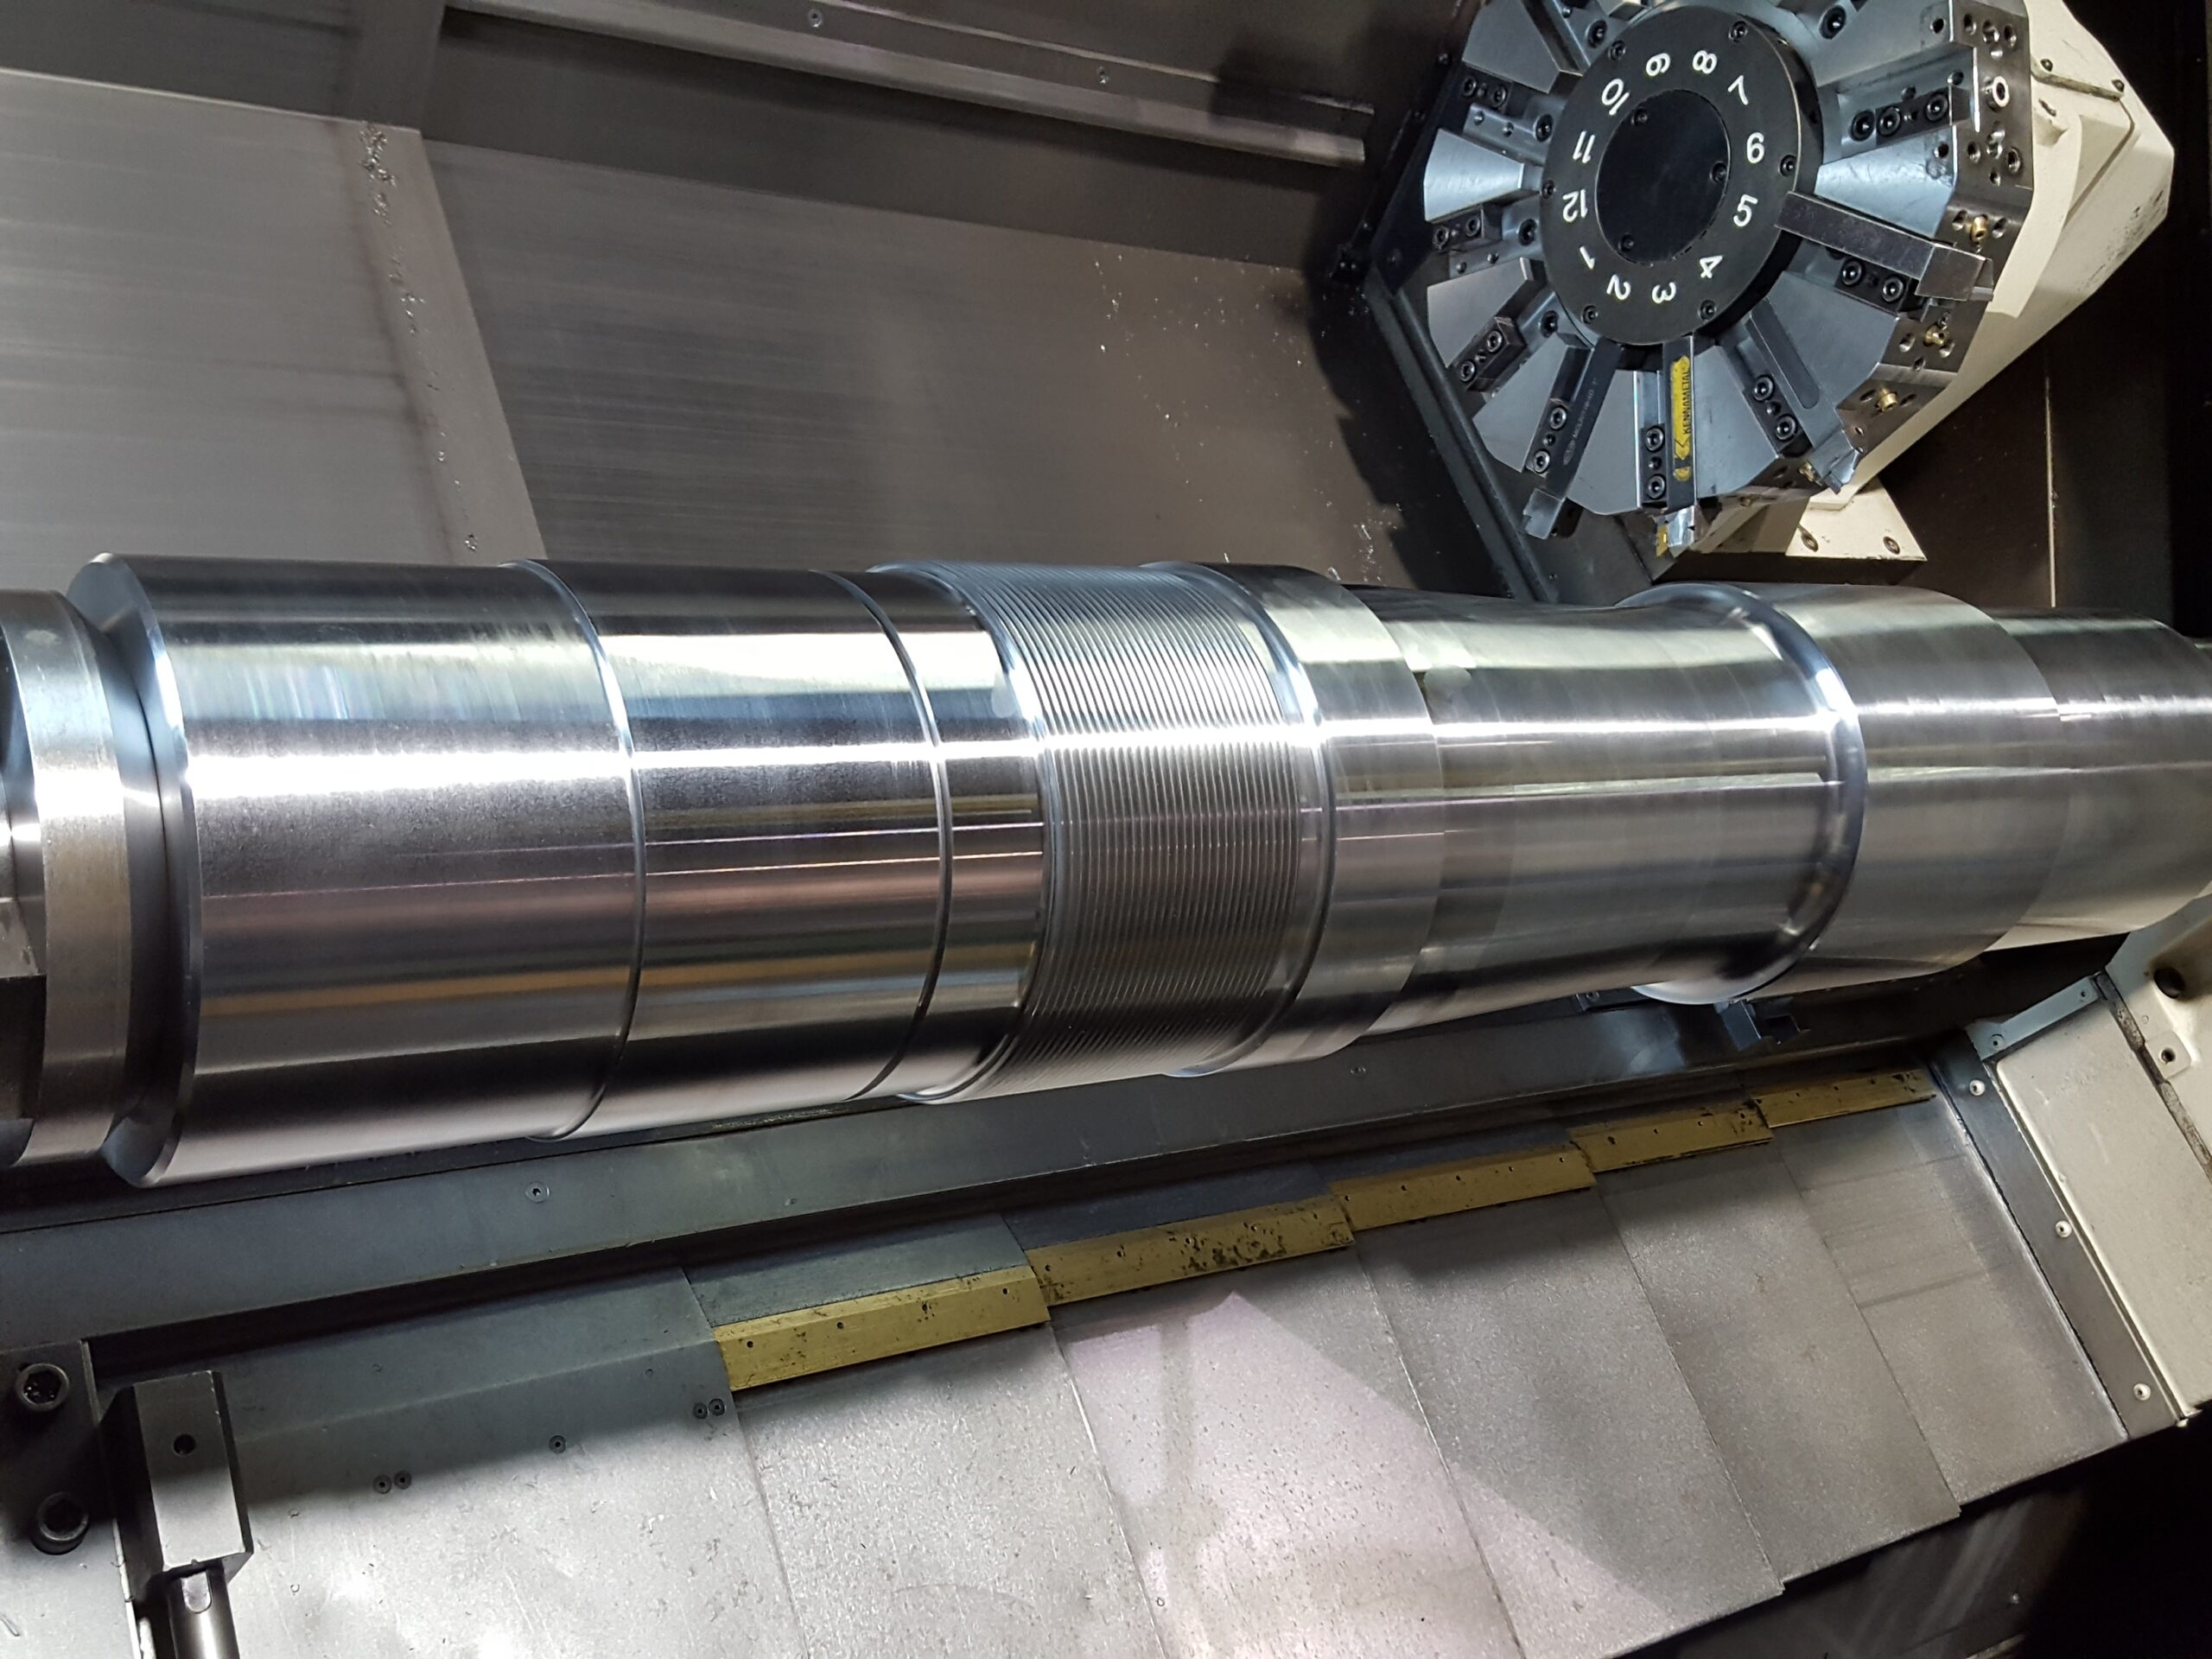
Flight geometry cut into an extruder screw on the machine, mixing groove running into the threaded section
Extruder parts: Flight geometry cut into the screw on the machine
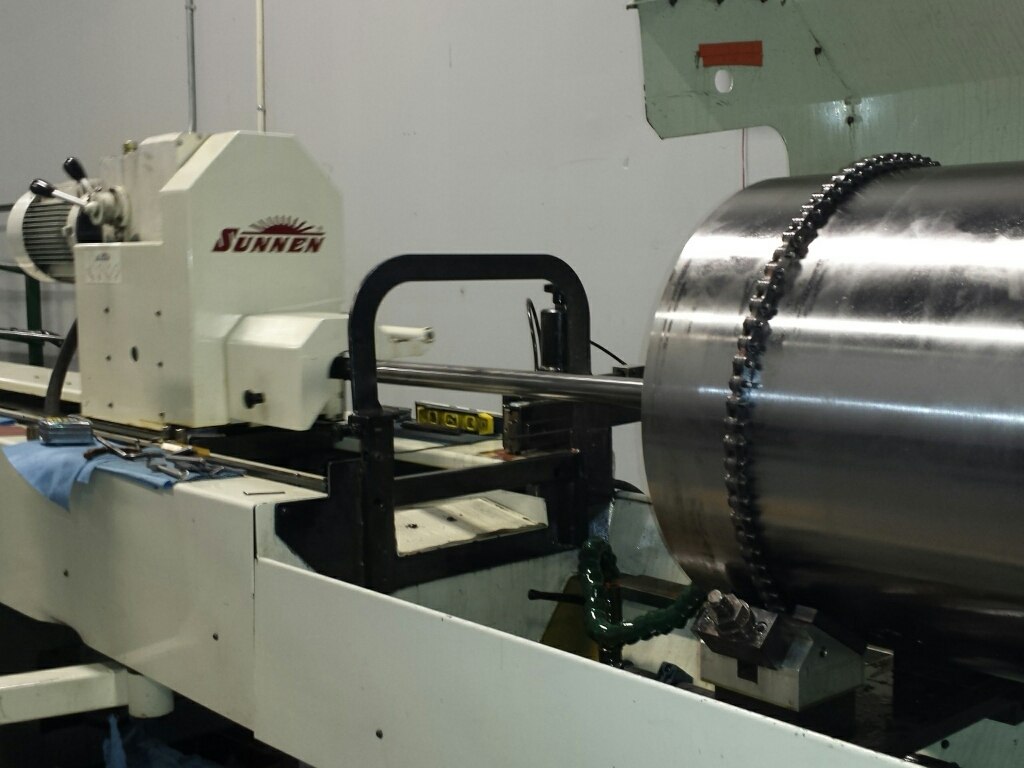
Large cylinder set up on the Sunnen honing machine
Bore honing: Large cylinder set up on the Sunnen honing machine
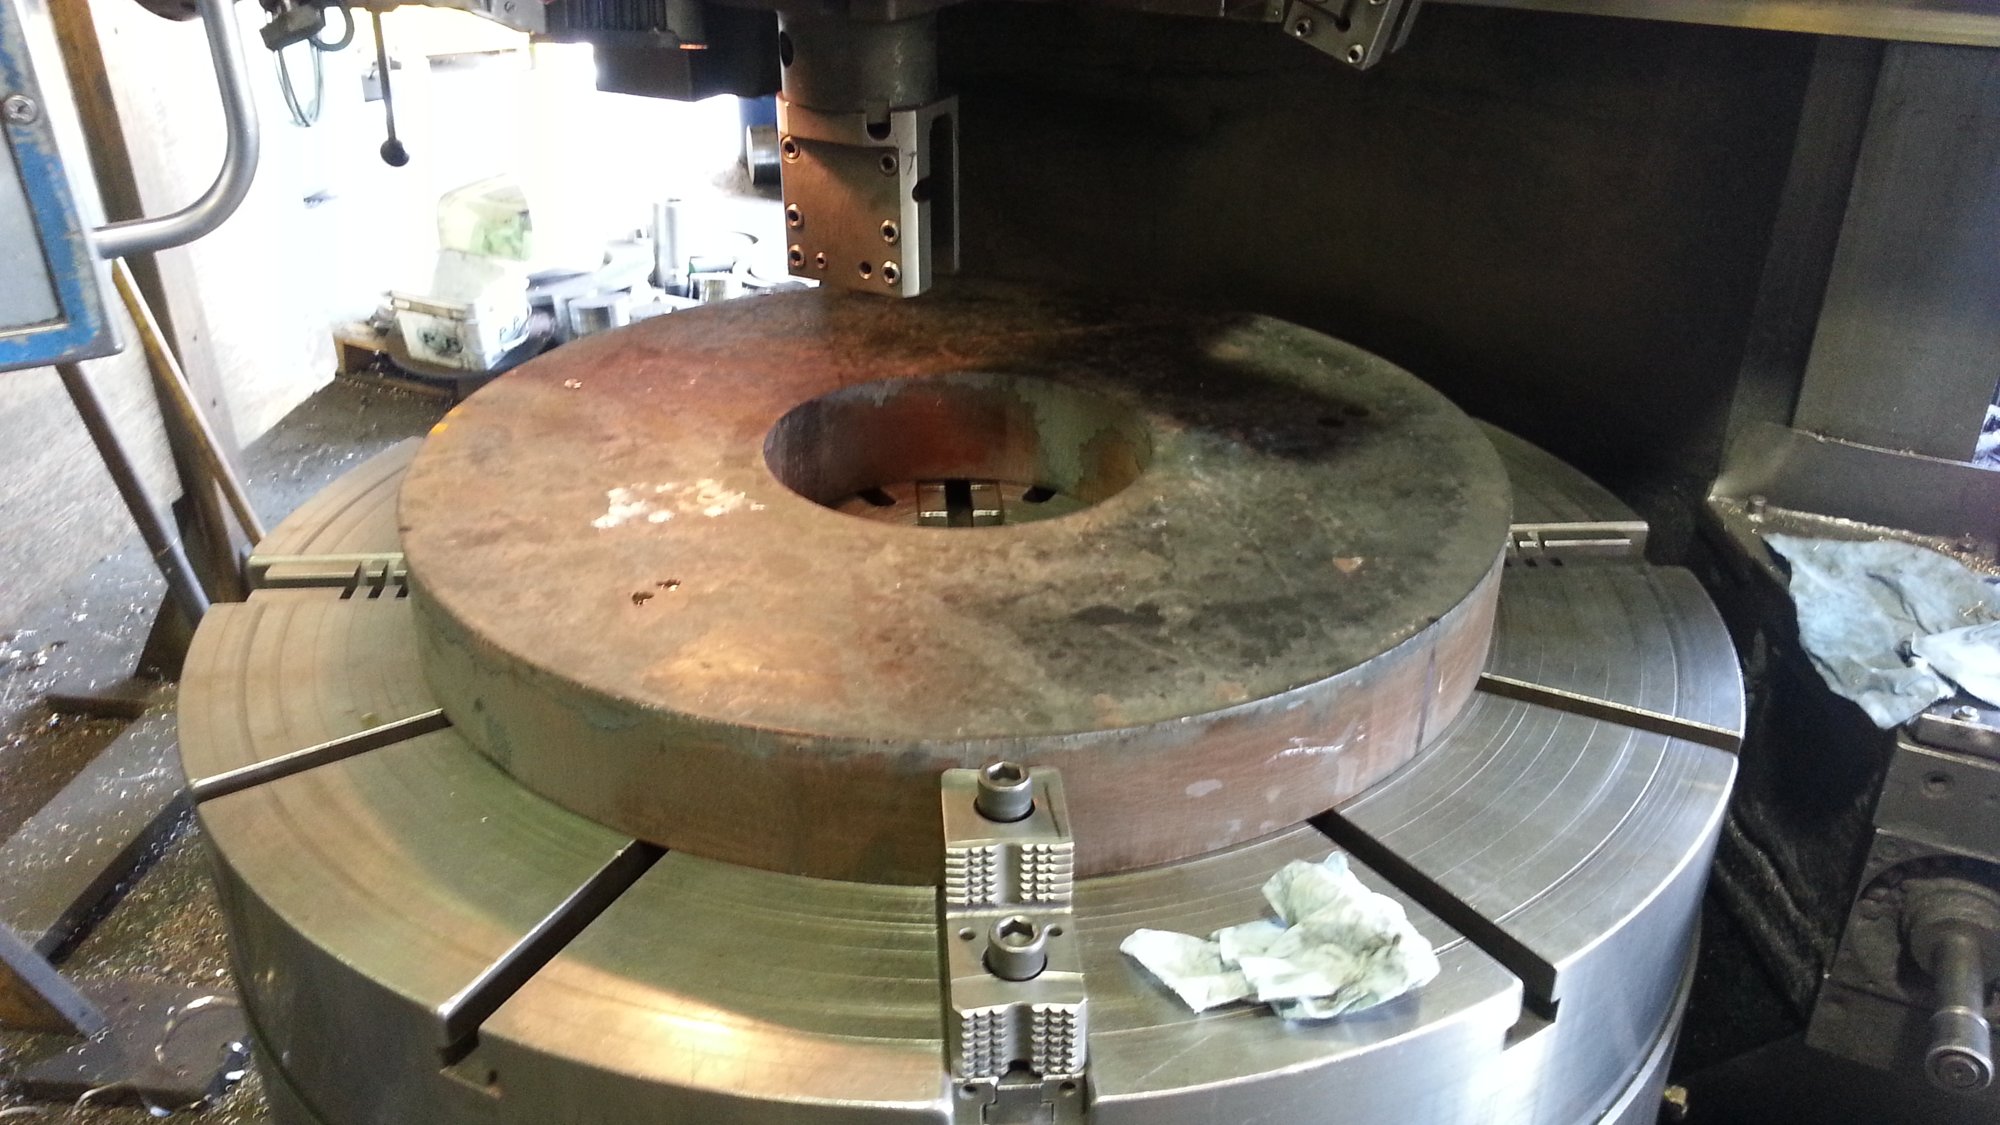
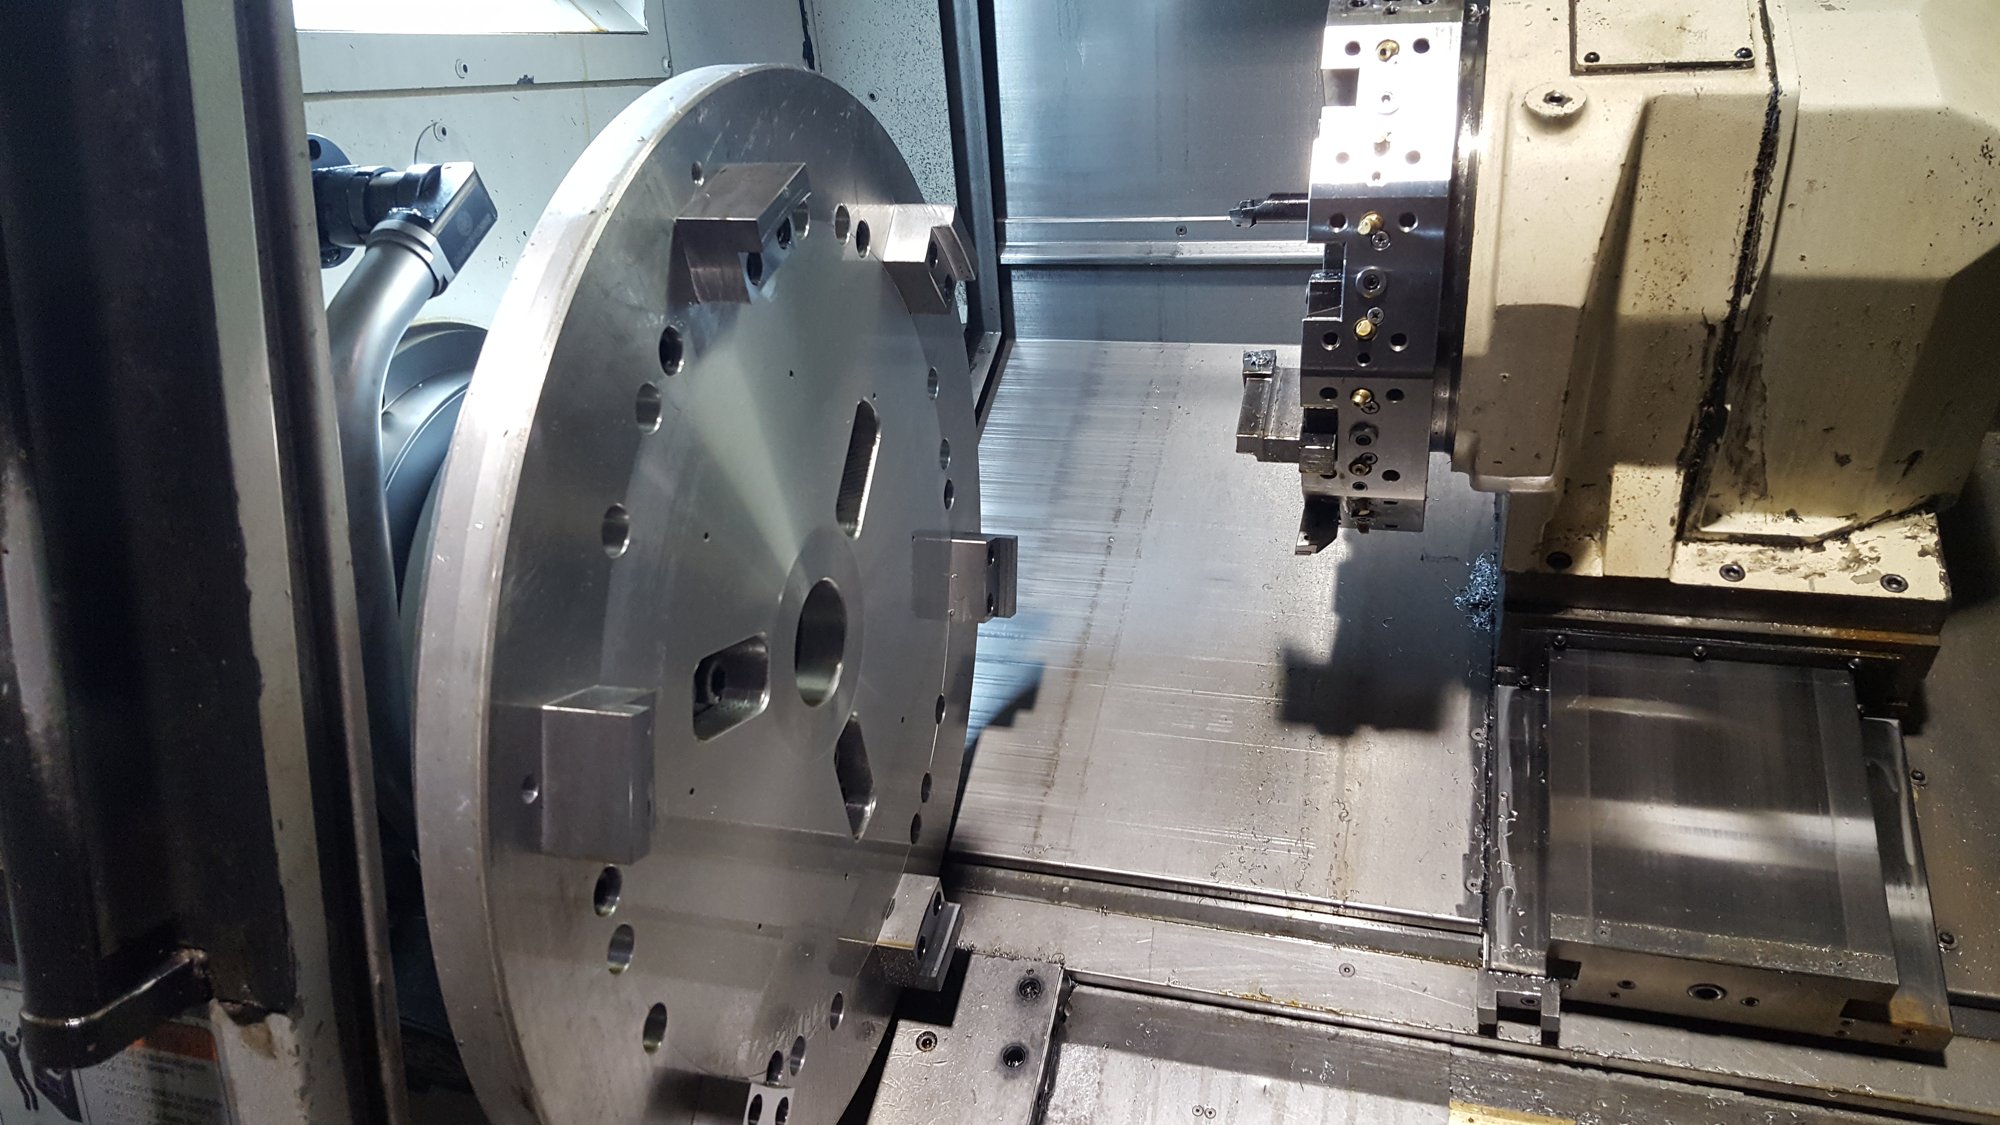
Large disc set on the vertical boring mill table, jaws closed on the rim before turning
Large machining: Disc set on the vertical boring mill table
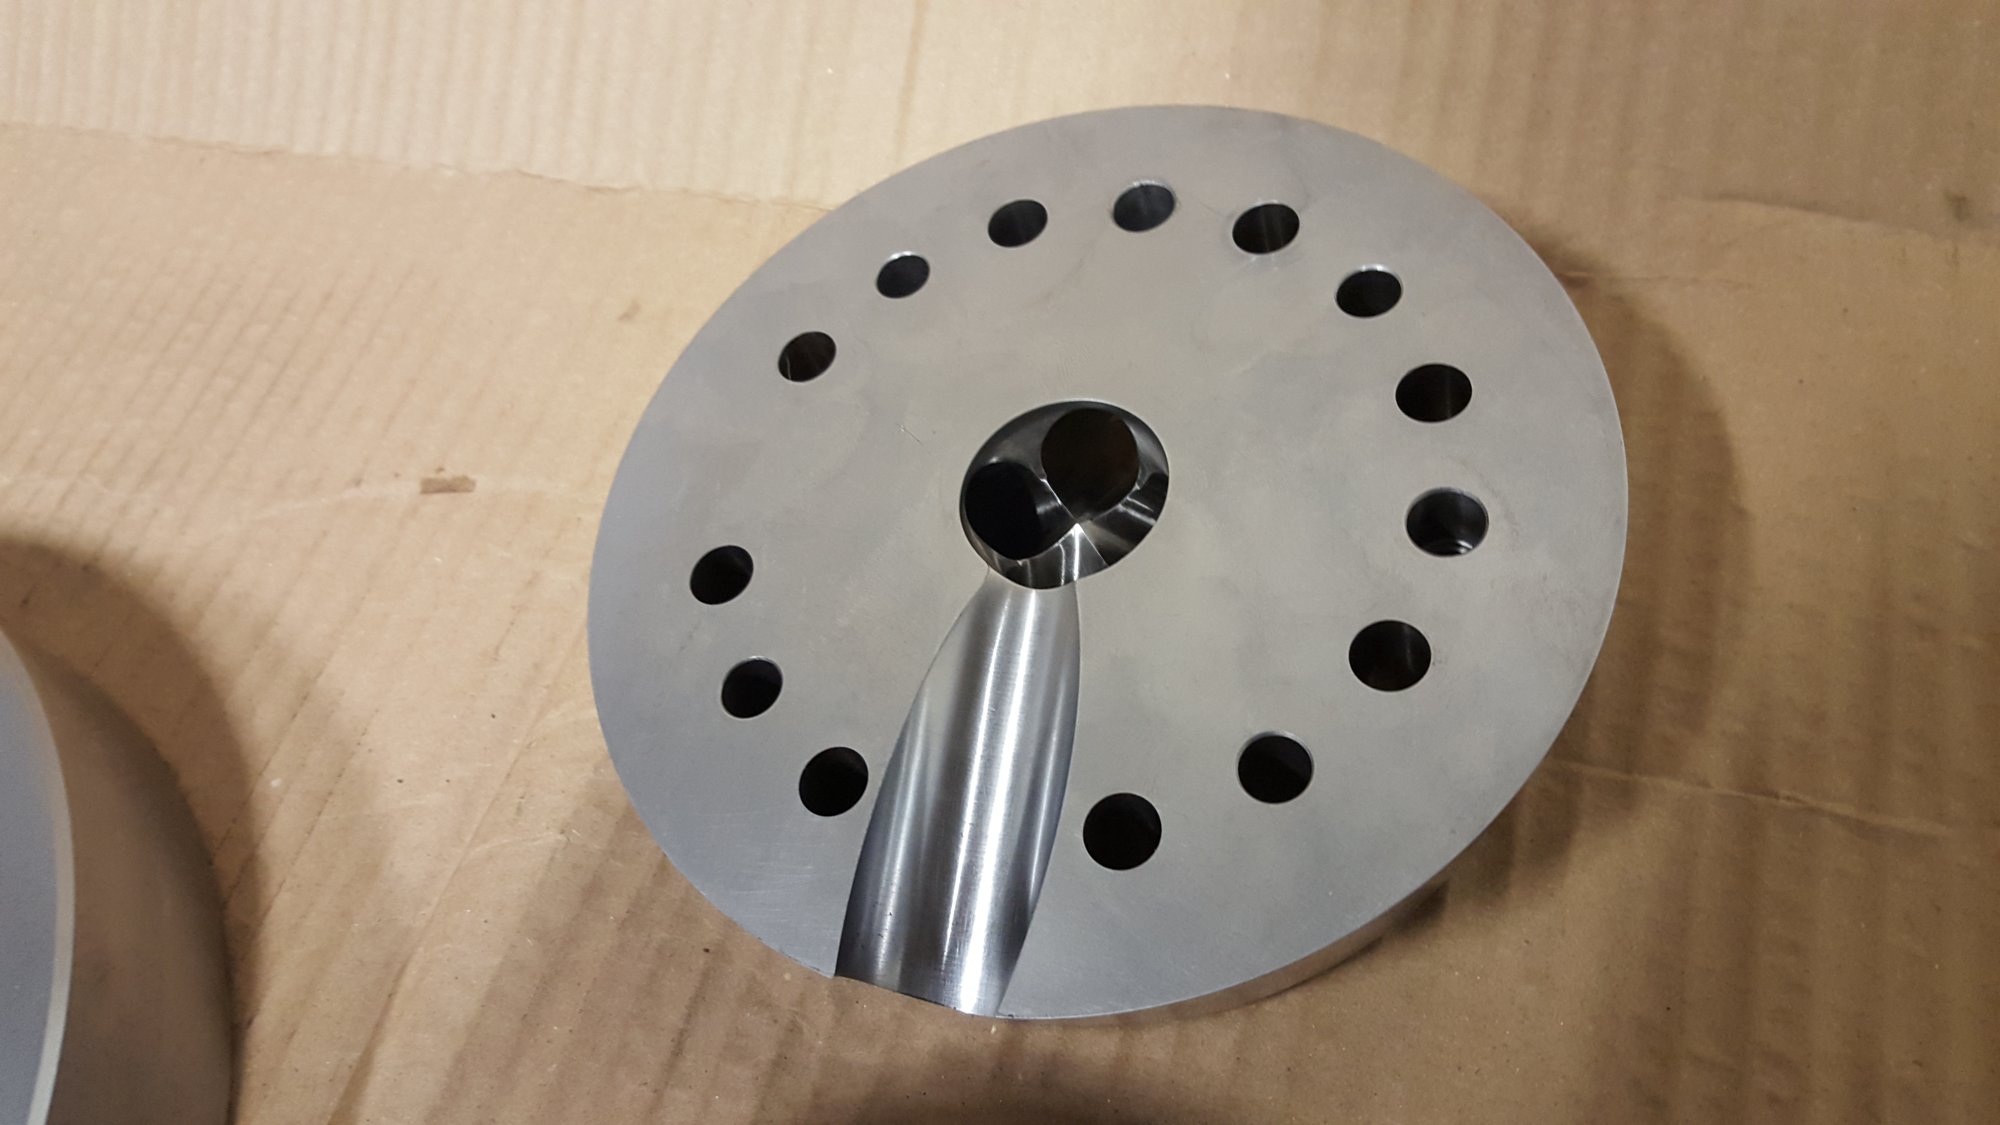
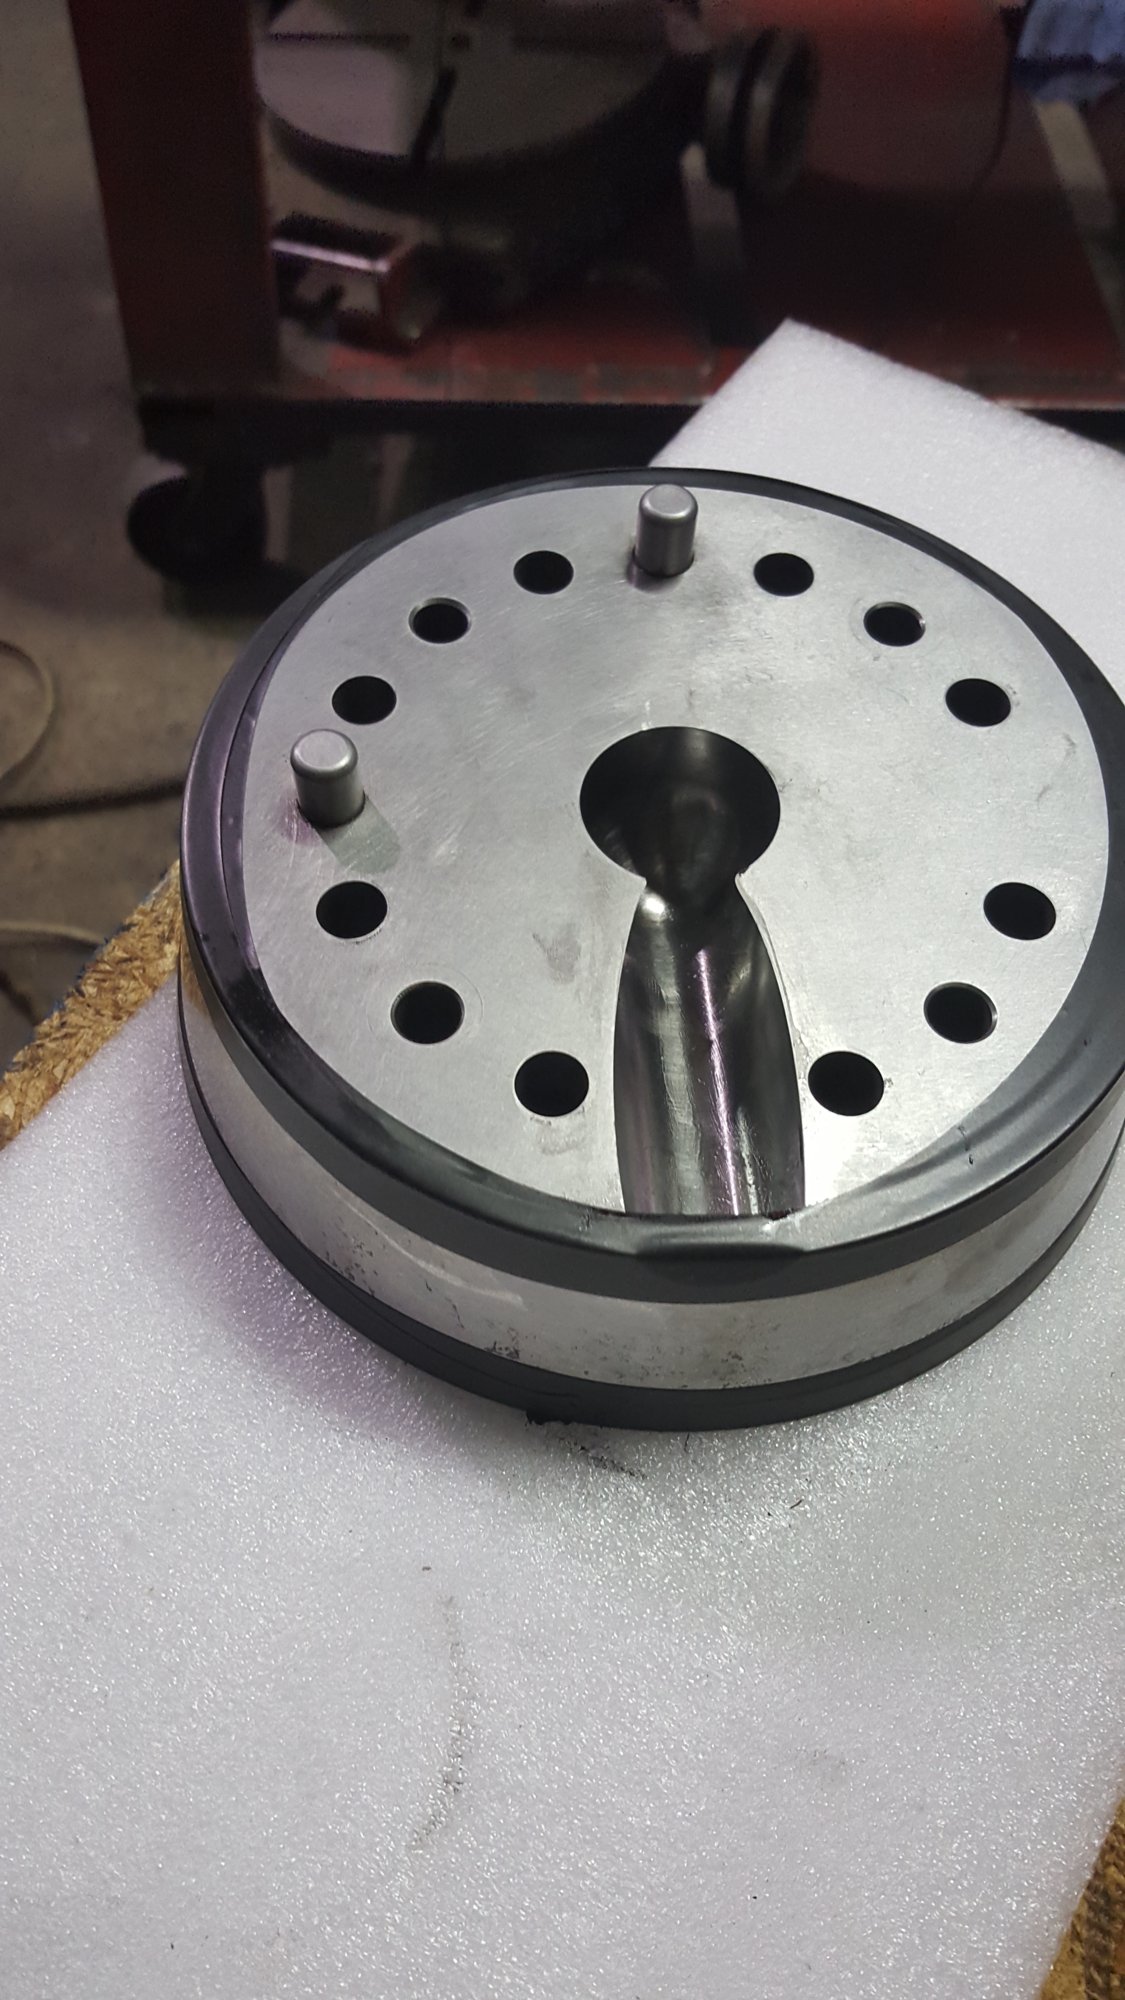
Teardrop melt port polished into the face of a blown film die distribution plate
Blown film dies: Teardrop melt port polished into a distribution plate
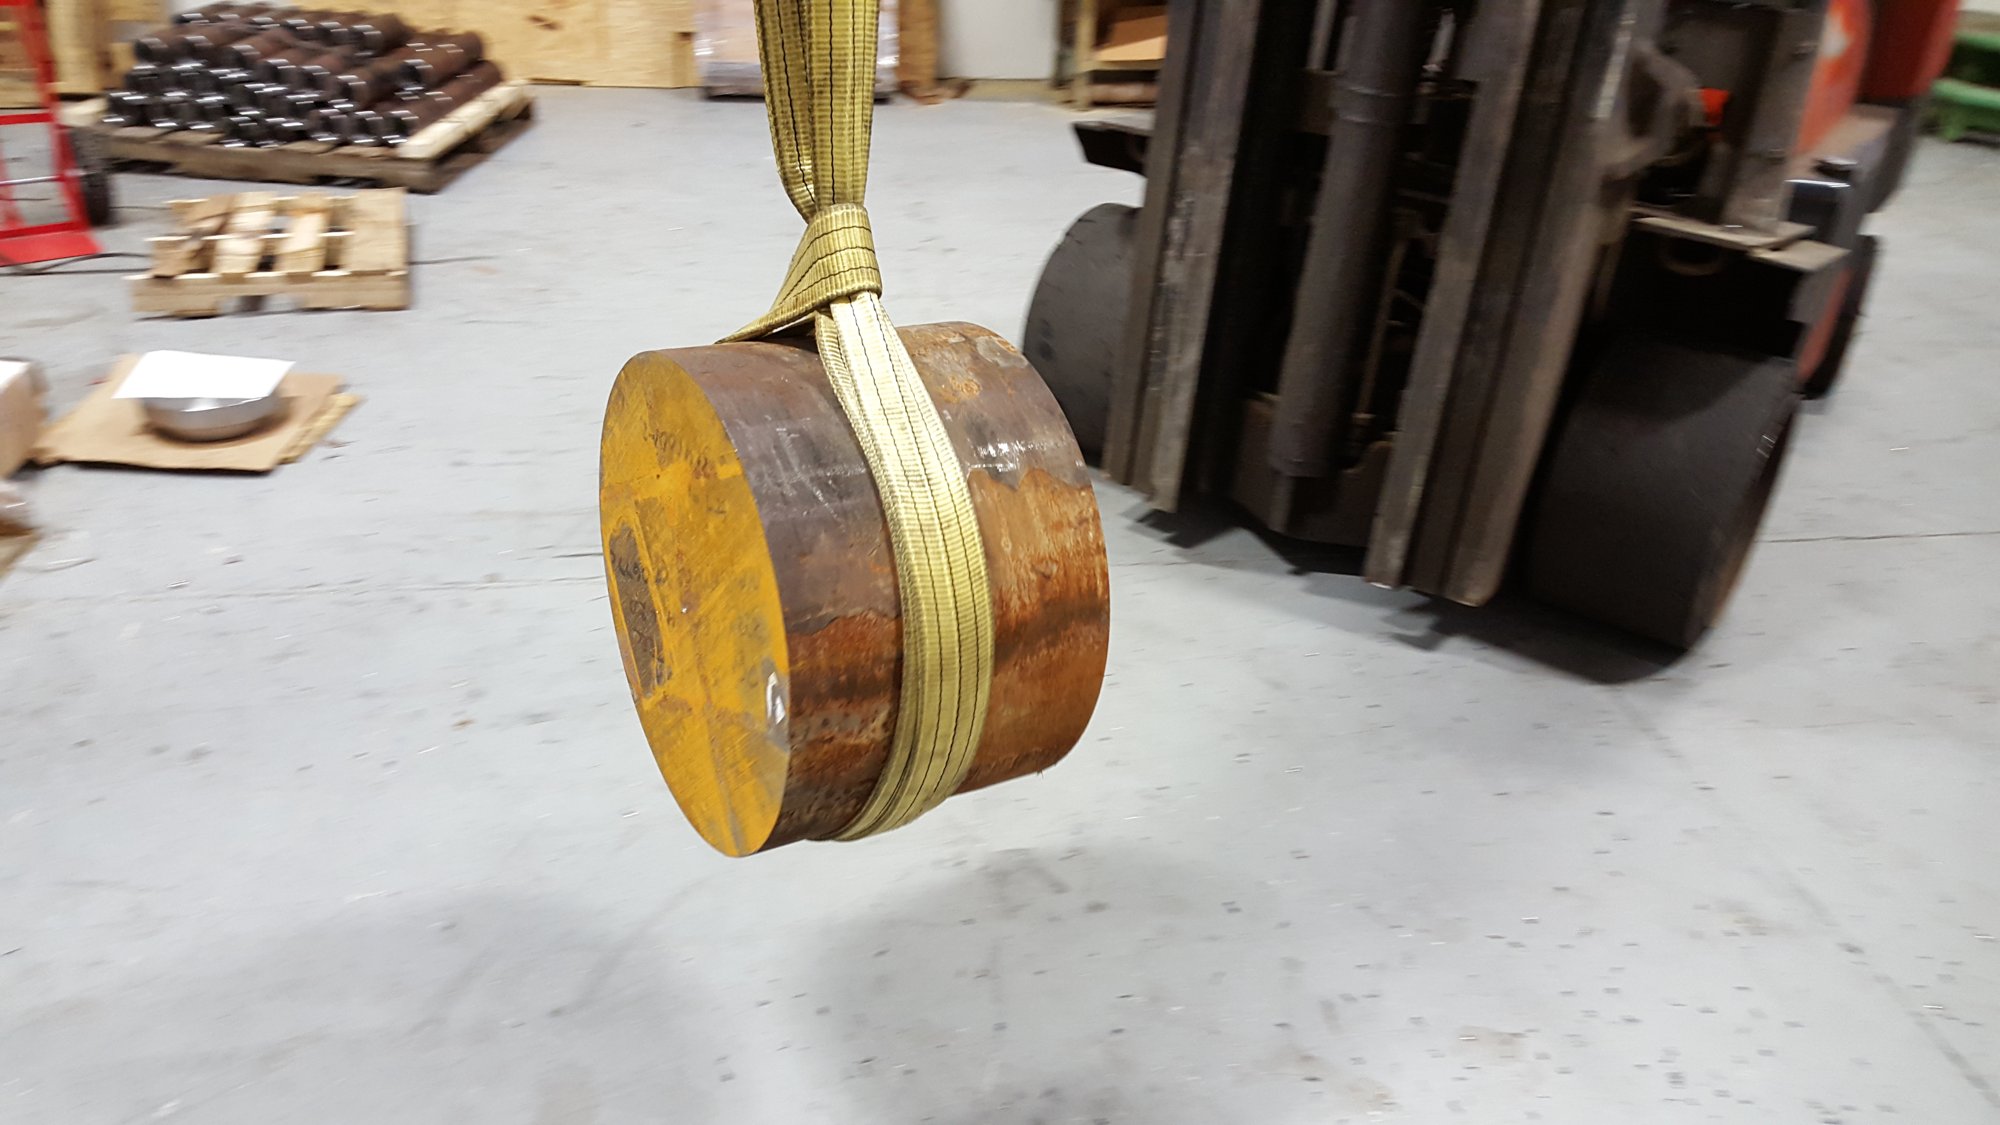
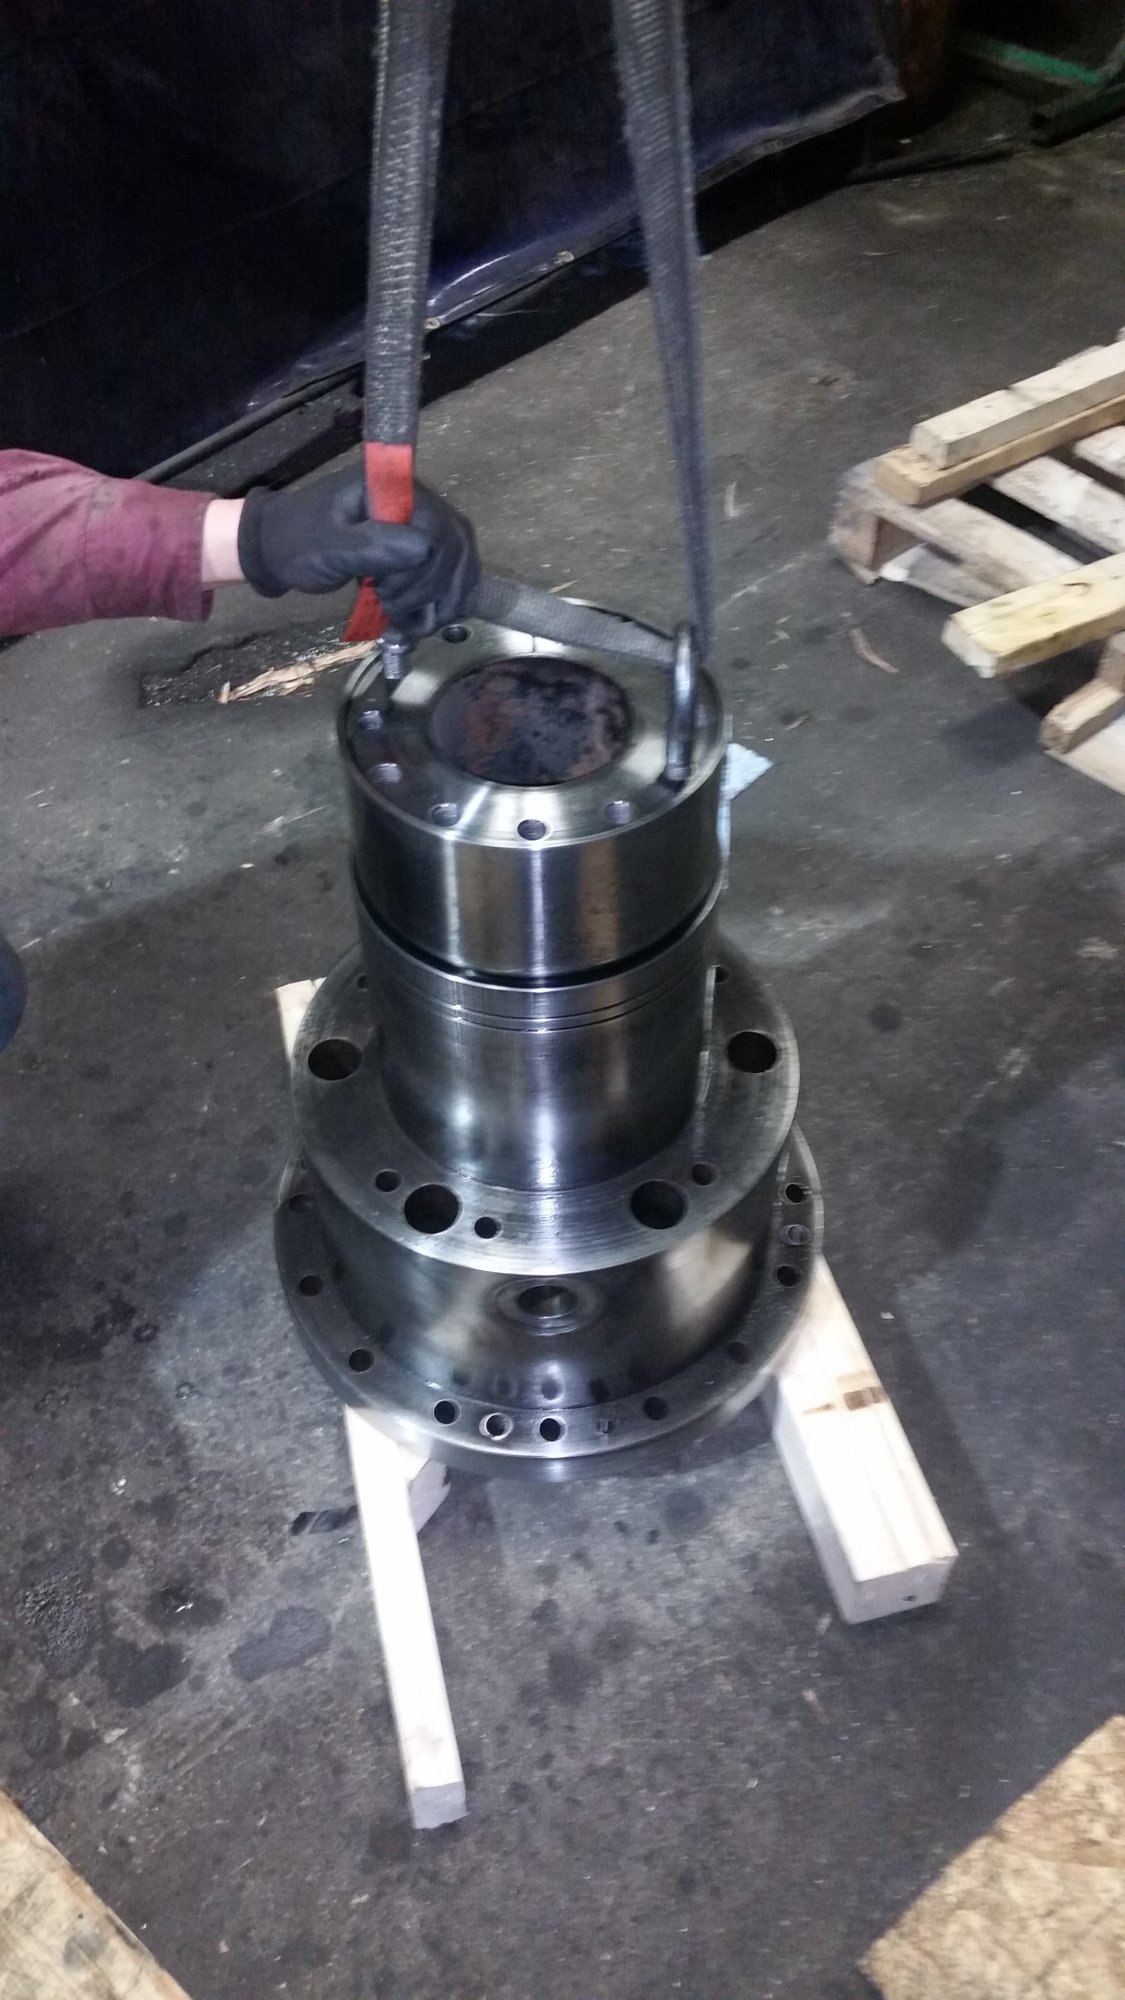
Die block billet slung from the forklift and moved across the shop floor
One die, start to finish (2 of 10): Die block billet moved across the floor on slings
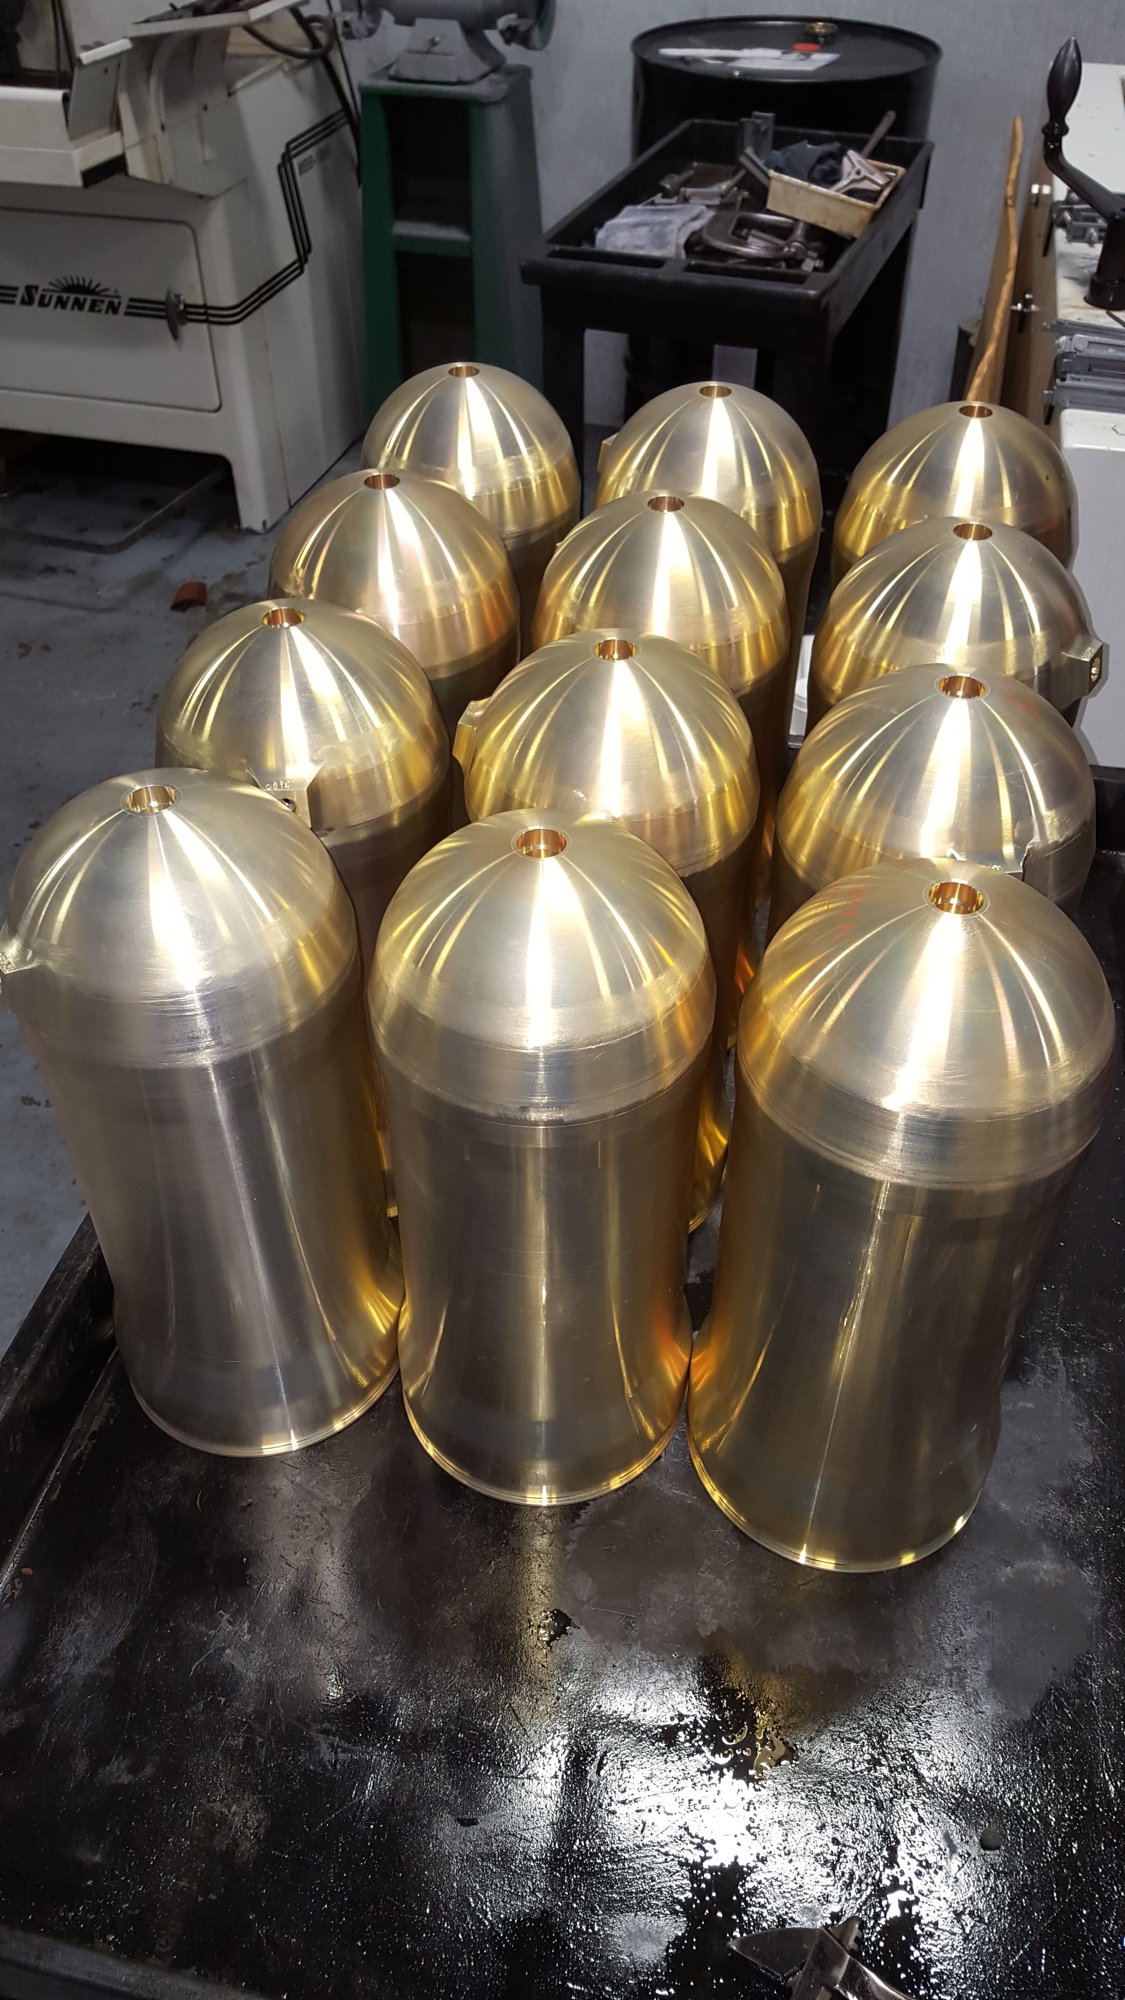
Batch of bronze bullet-nose parts turned and polished, standing together on the bench
Turning and production: Bronze bullet-nose parts, turned and polished
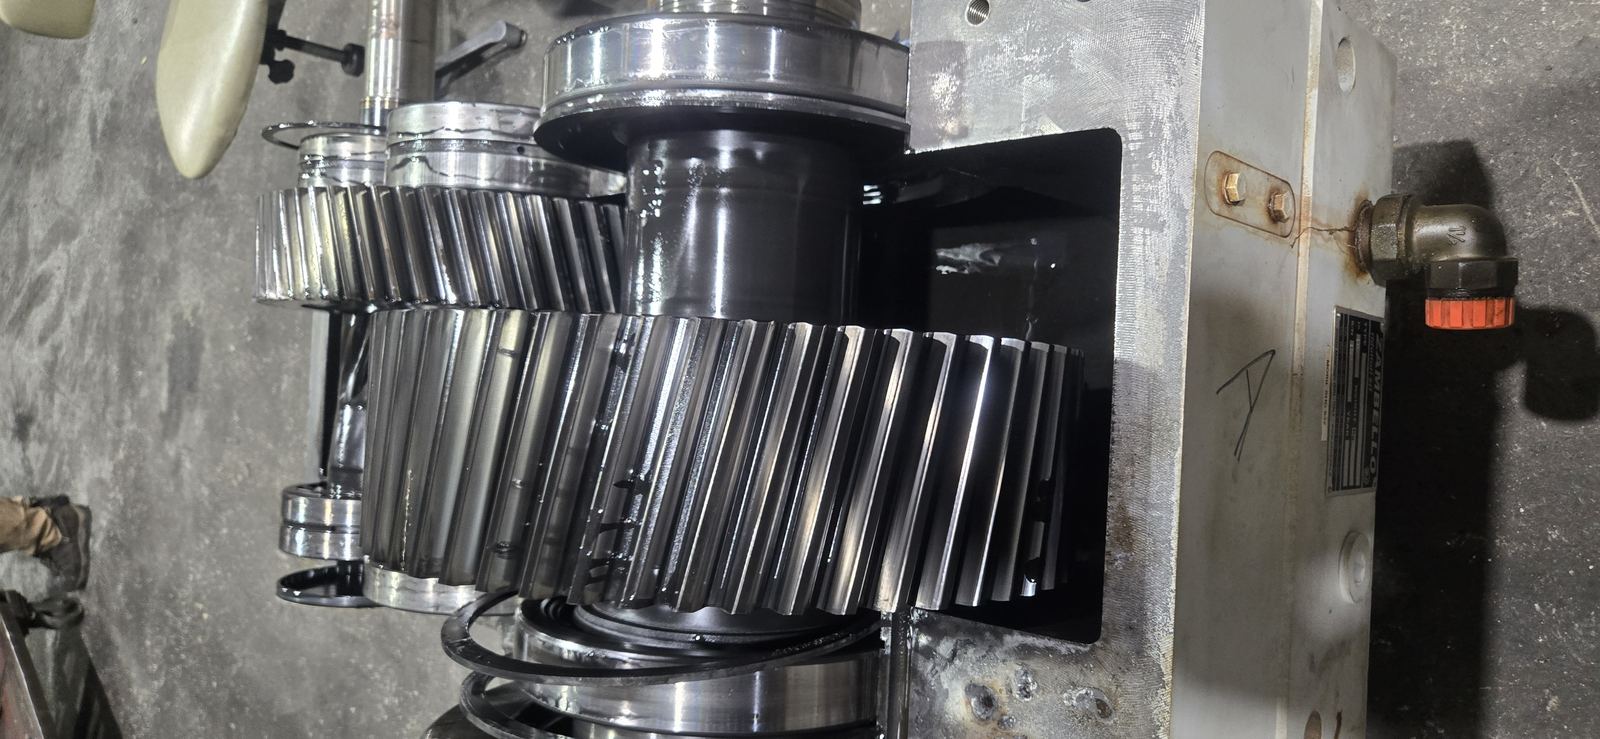
Helical gear stack removed from an extruder gearbox for measurement of tooth contact and journal diameters
Gearbox repair: Helical gear stack lifted out for measurement
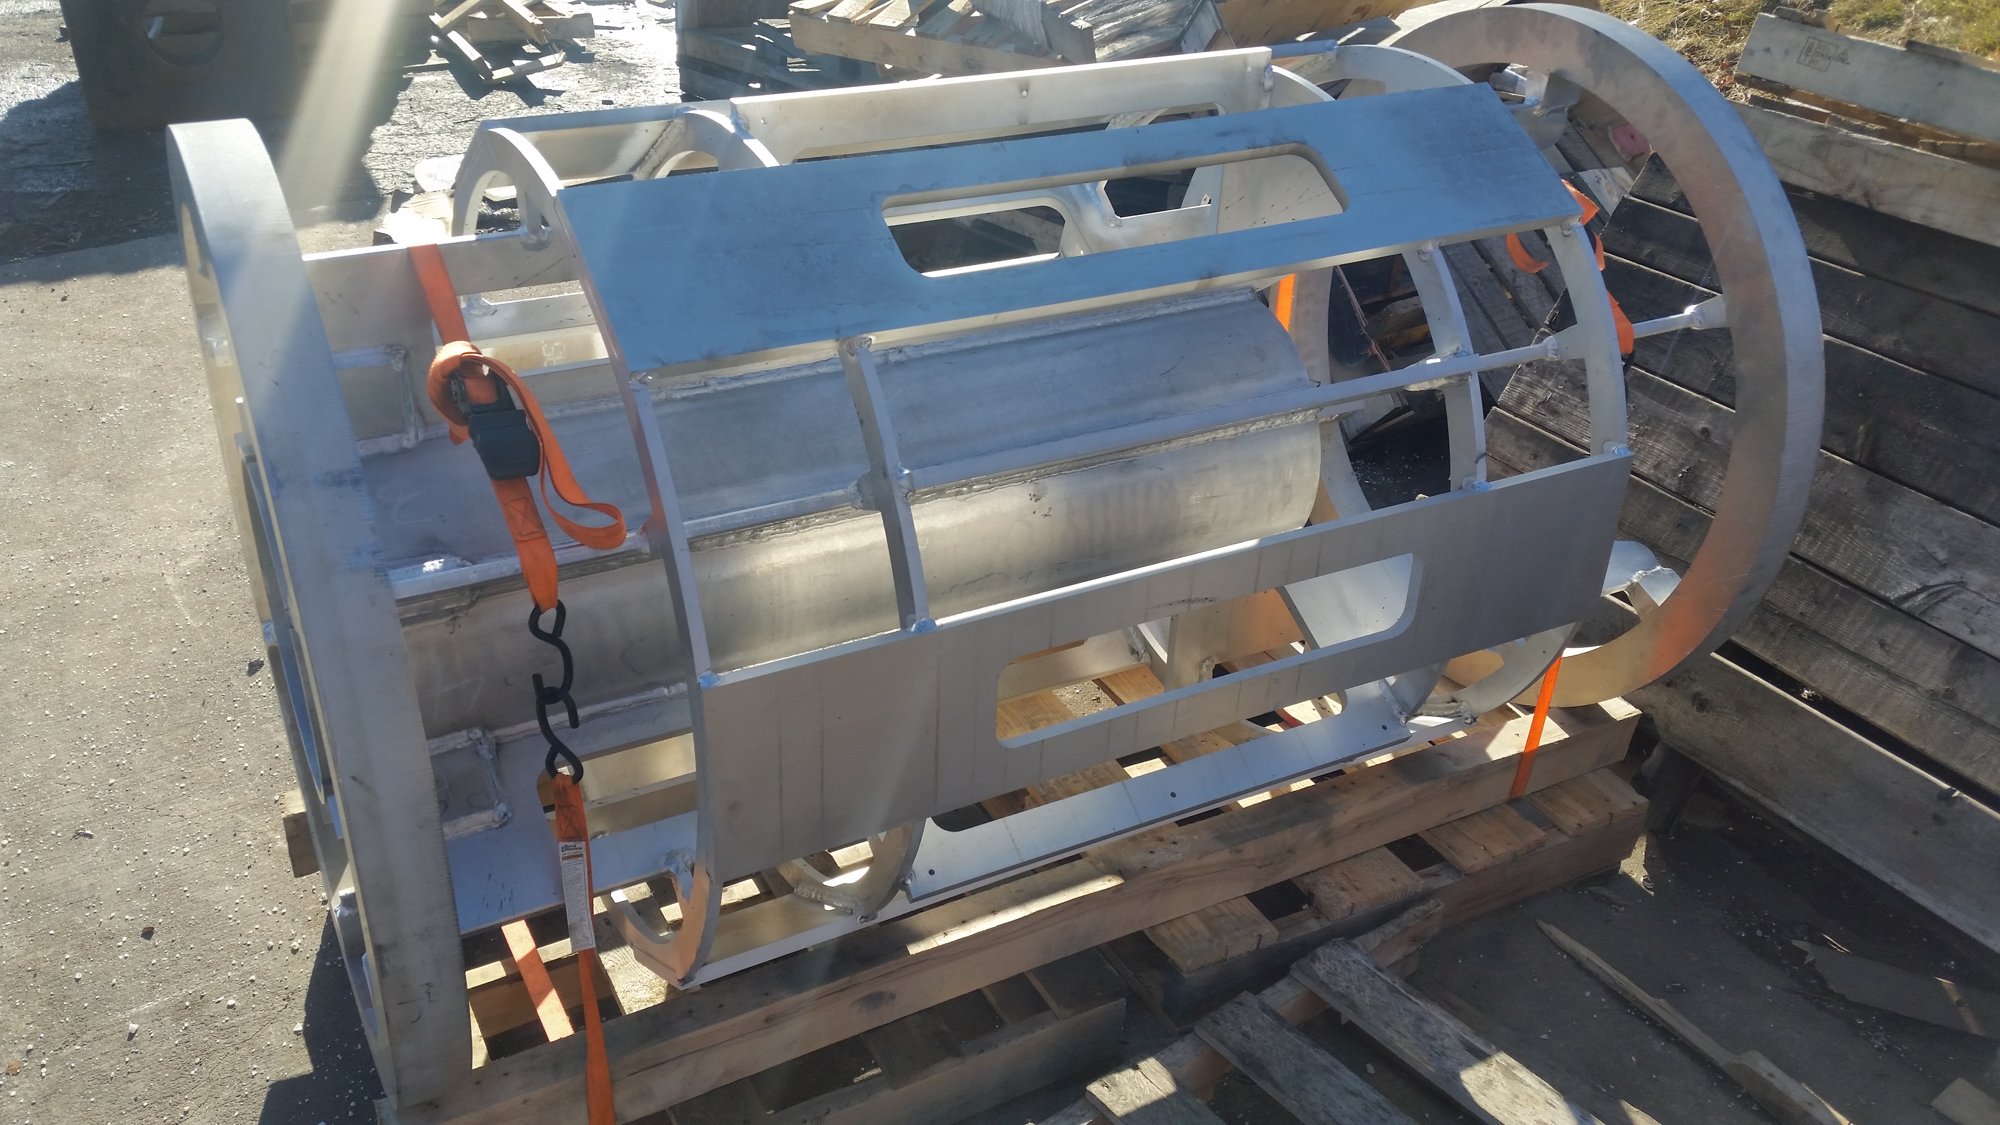
Fabricated cage rotor cylinder strapped on a pallet, slotted body between its end rings
Fabrication and shipping: Fabricated cage rotor between its end rings
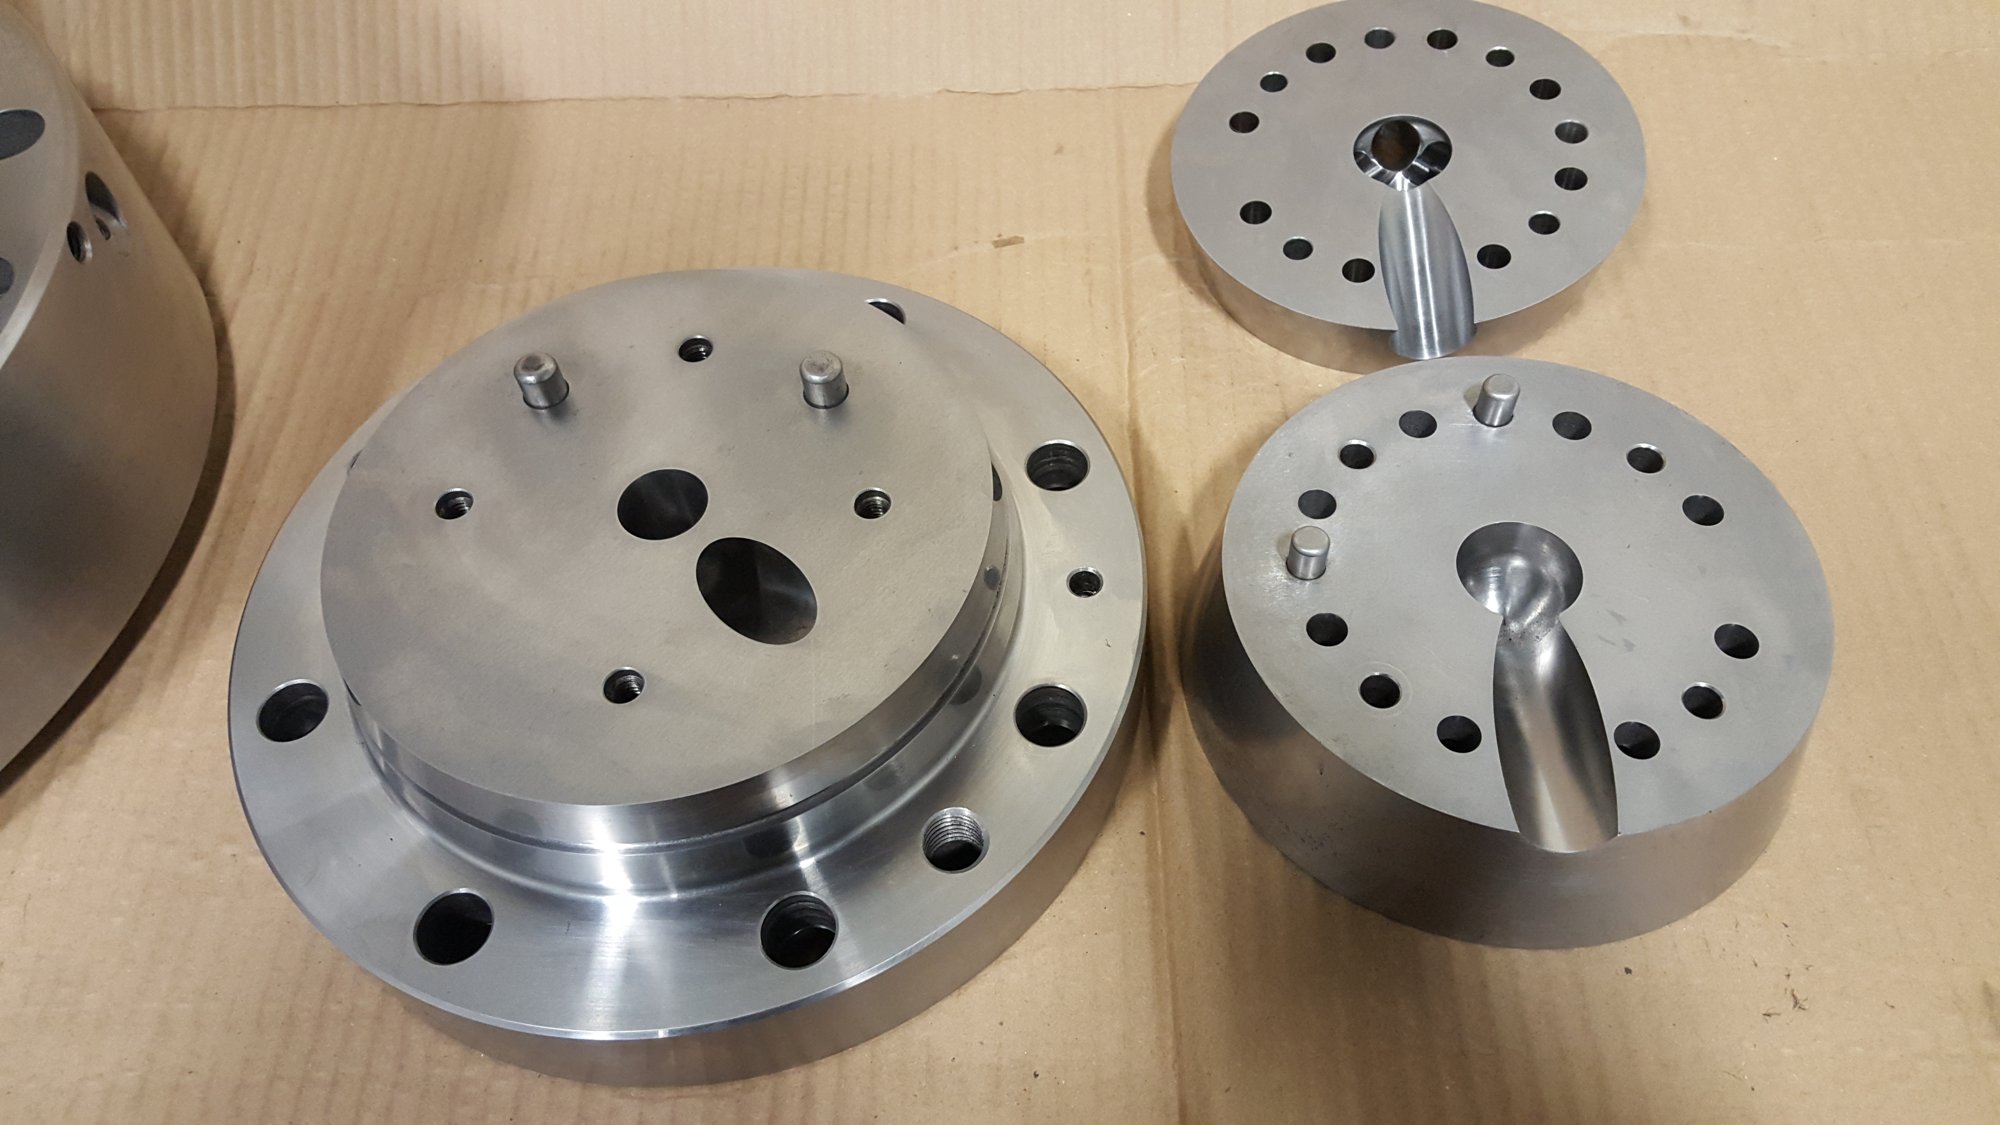
Set of blown film die distribution plates, each with its teardrop melt port and dowelled bolt pattern
Blown film dies: A set of distribution plates, each with its melt port
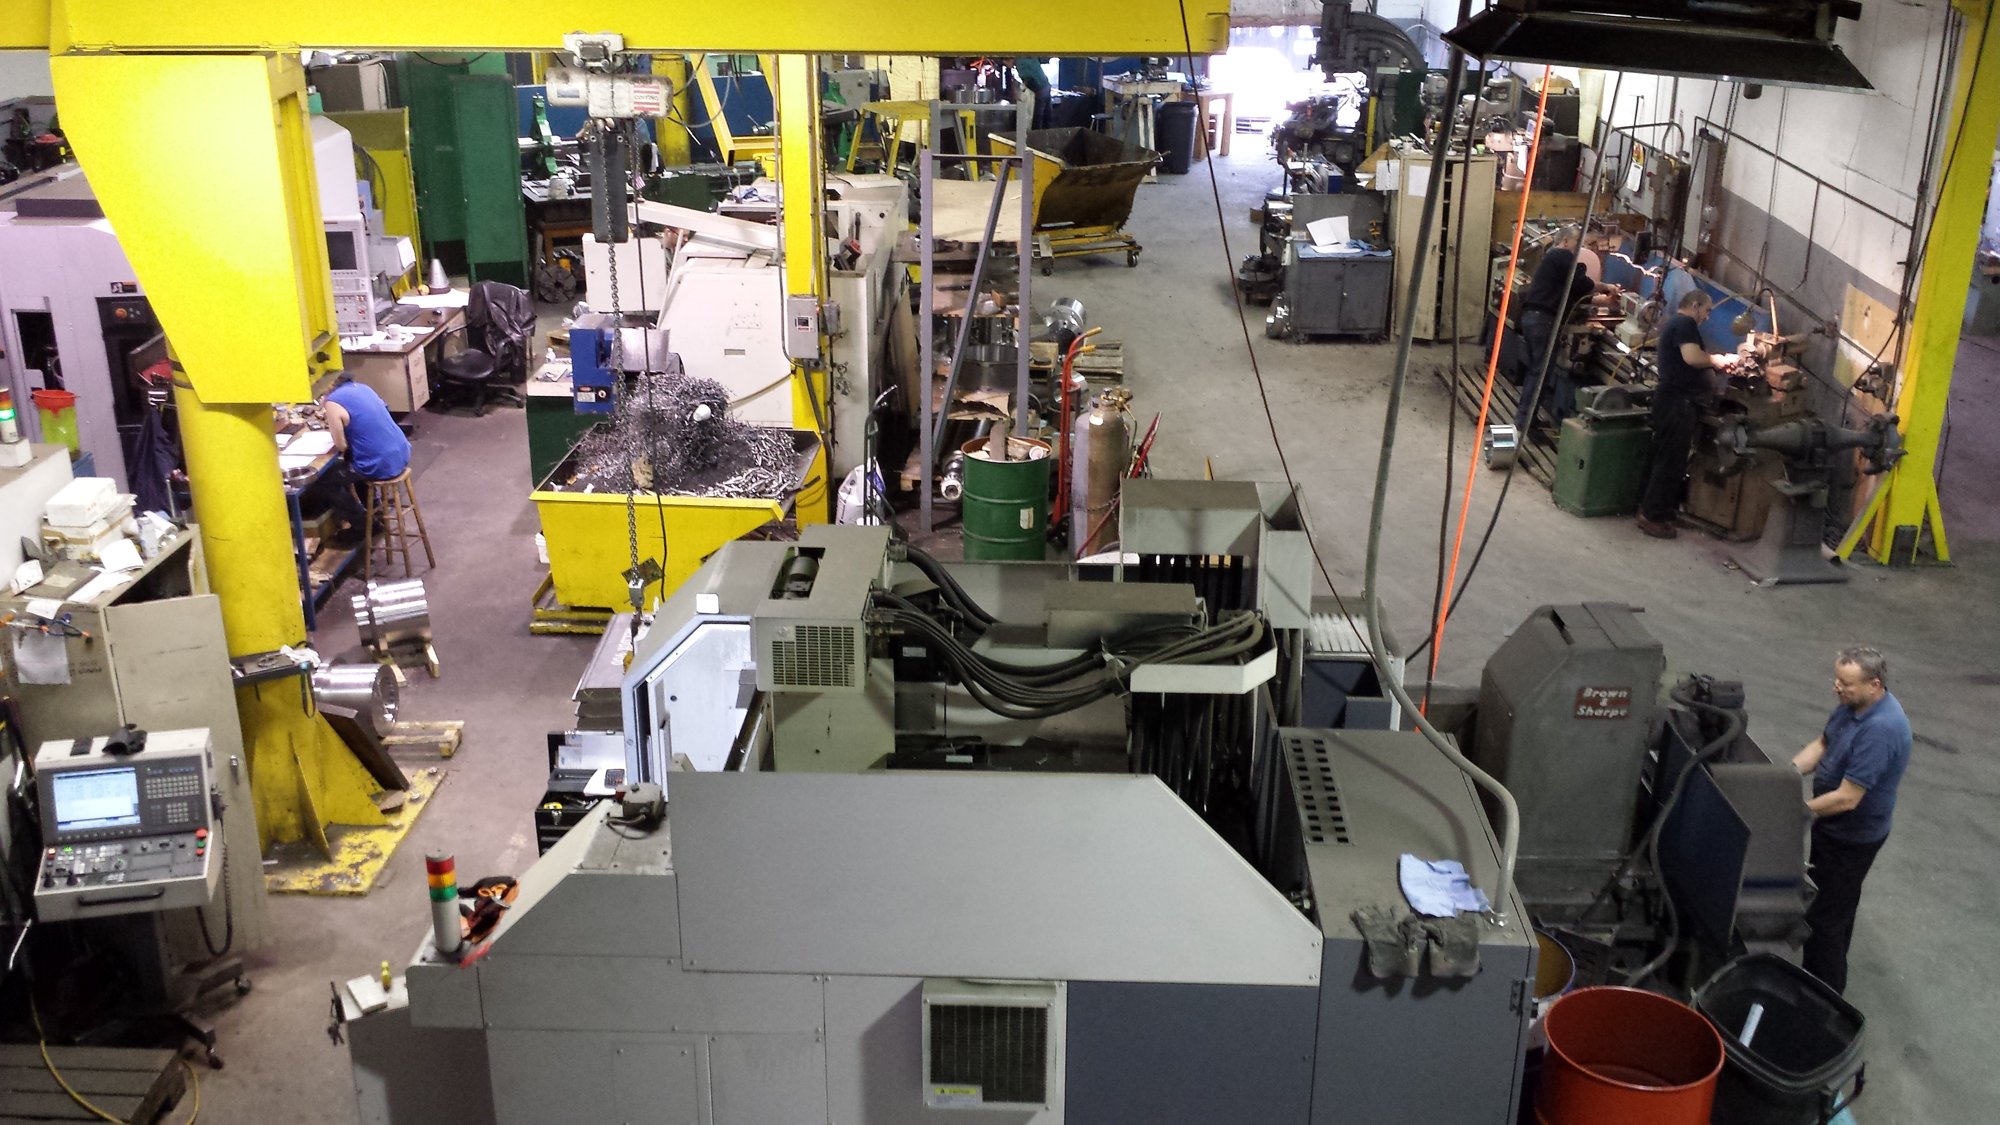
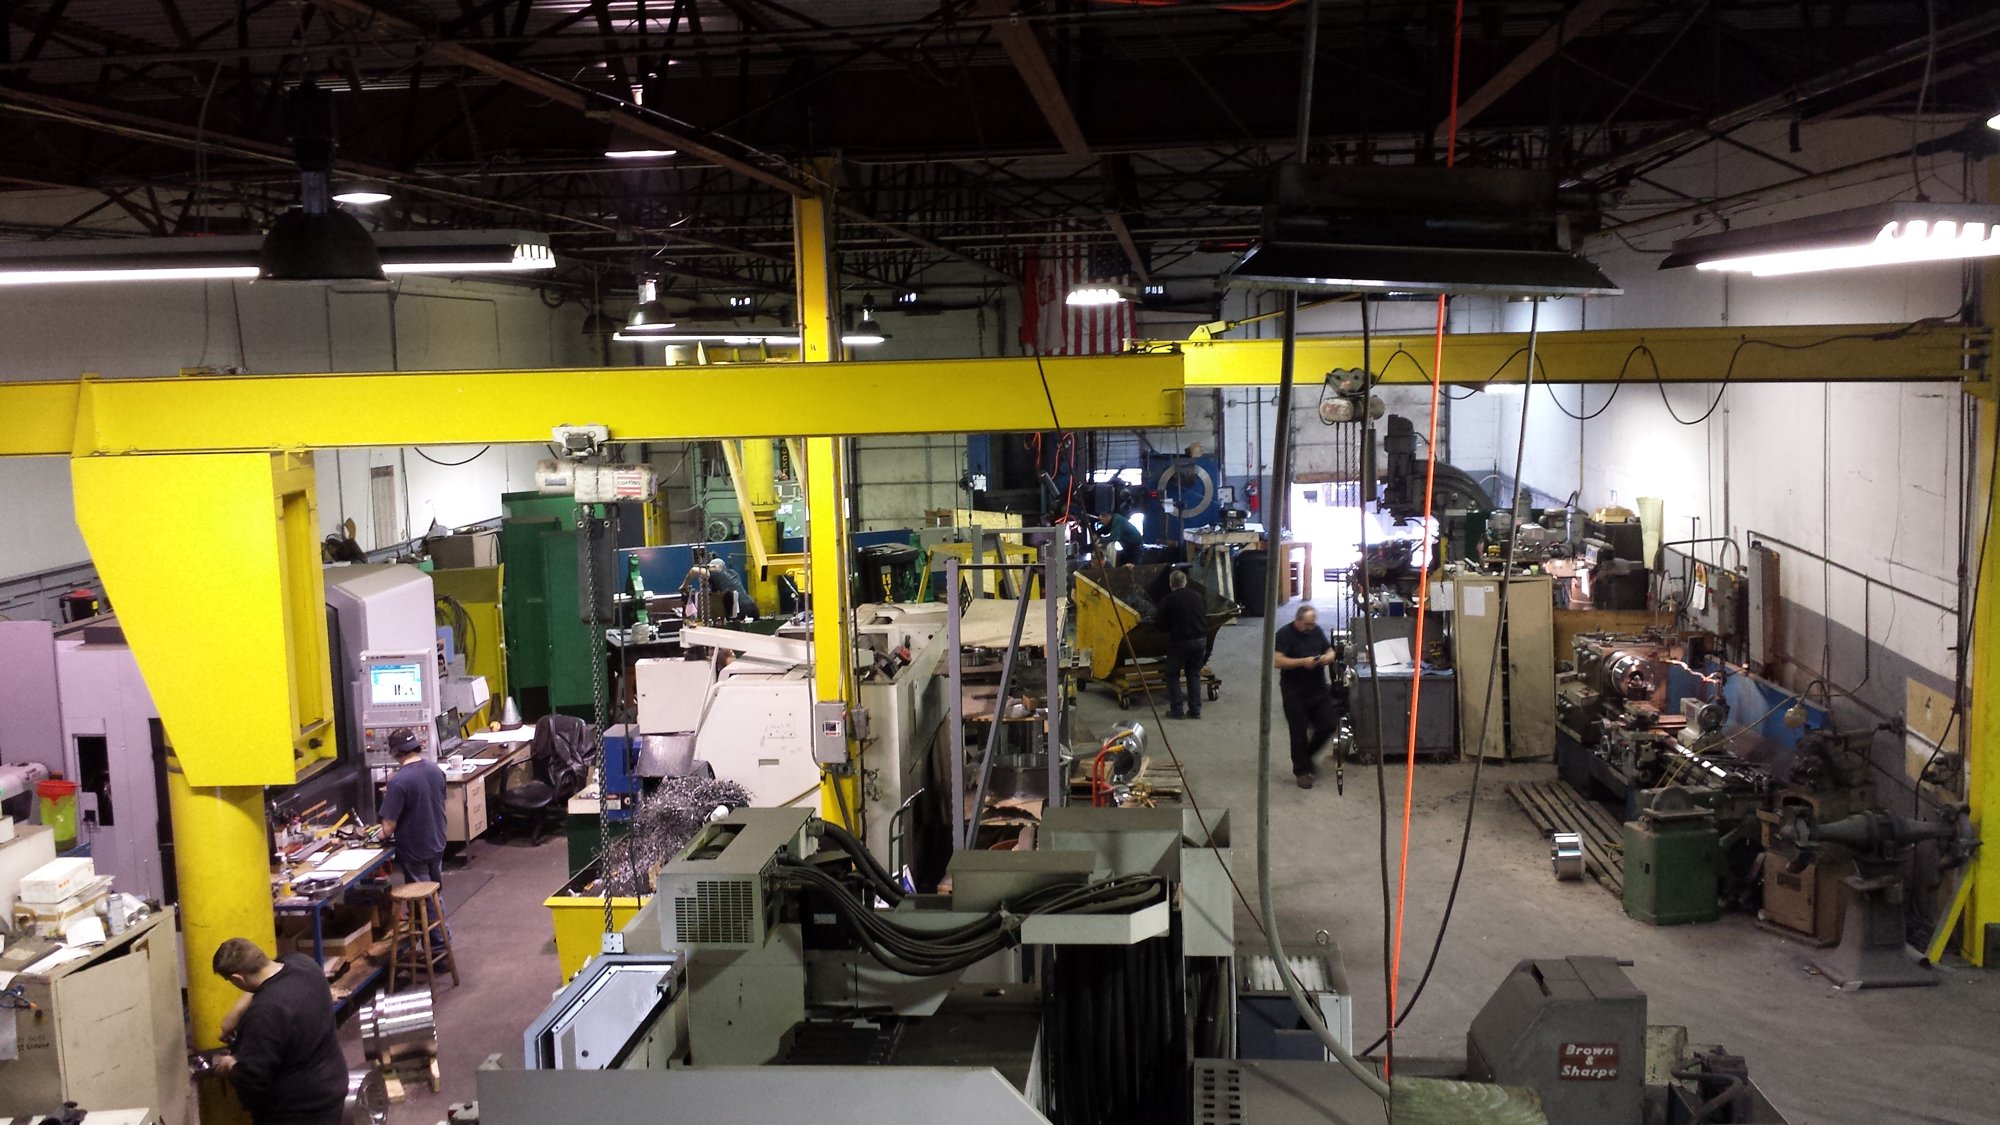
Elevated view across the Zala Machine shop floor, CNC machines and benches under the yellow gantry crane
The shop: Across the shop floor under the gantry crane
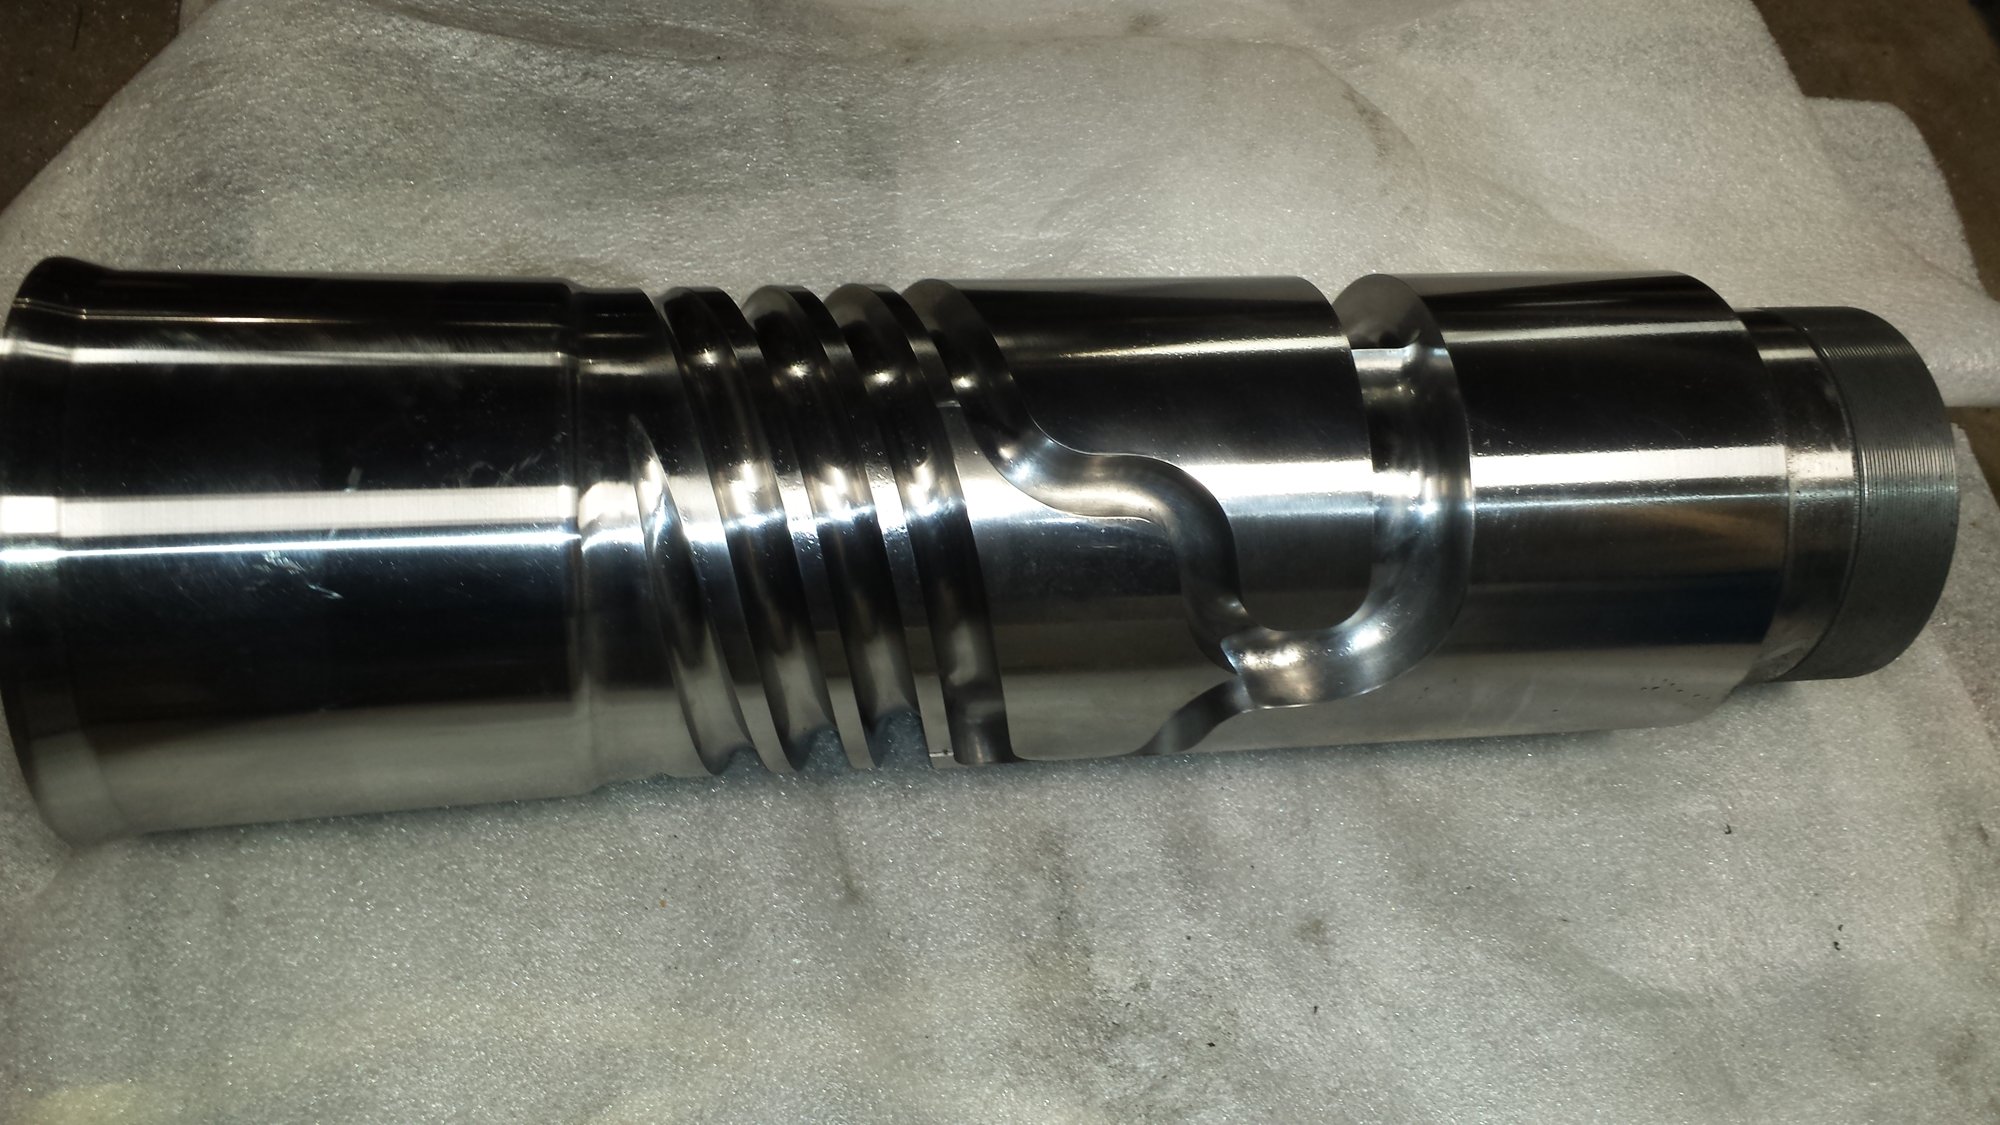
Close view of the deep helical flight cut along an extruder screw's mixing section
Extruder parts: Deep helical flight along the mixing section
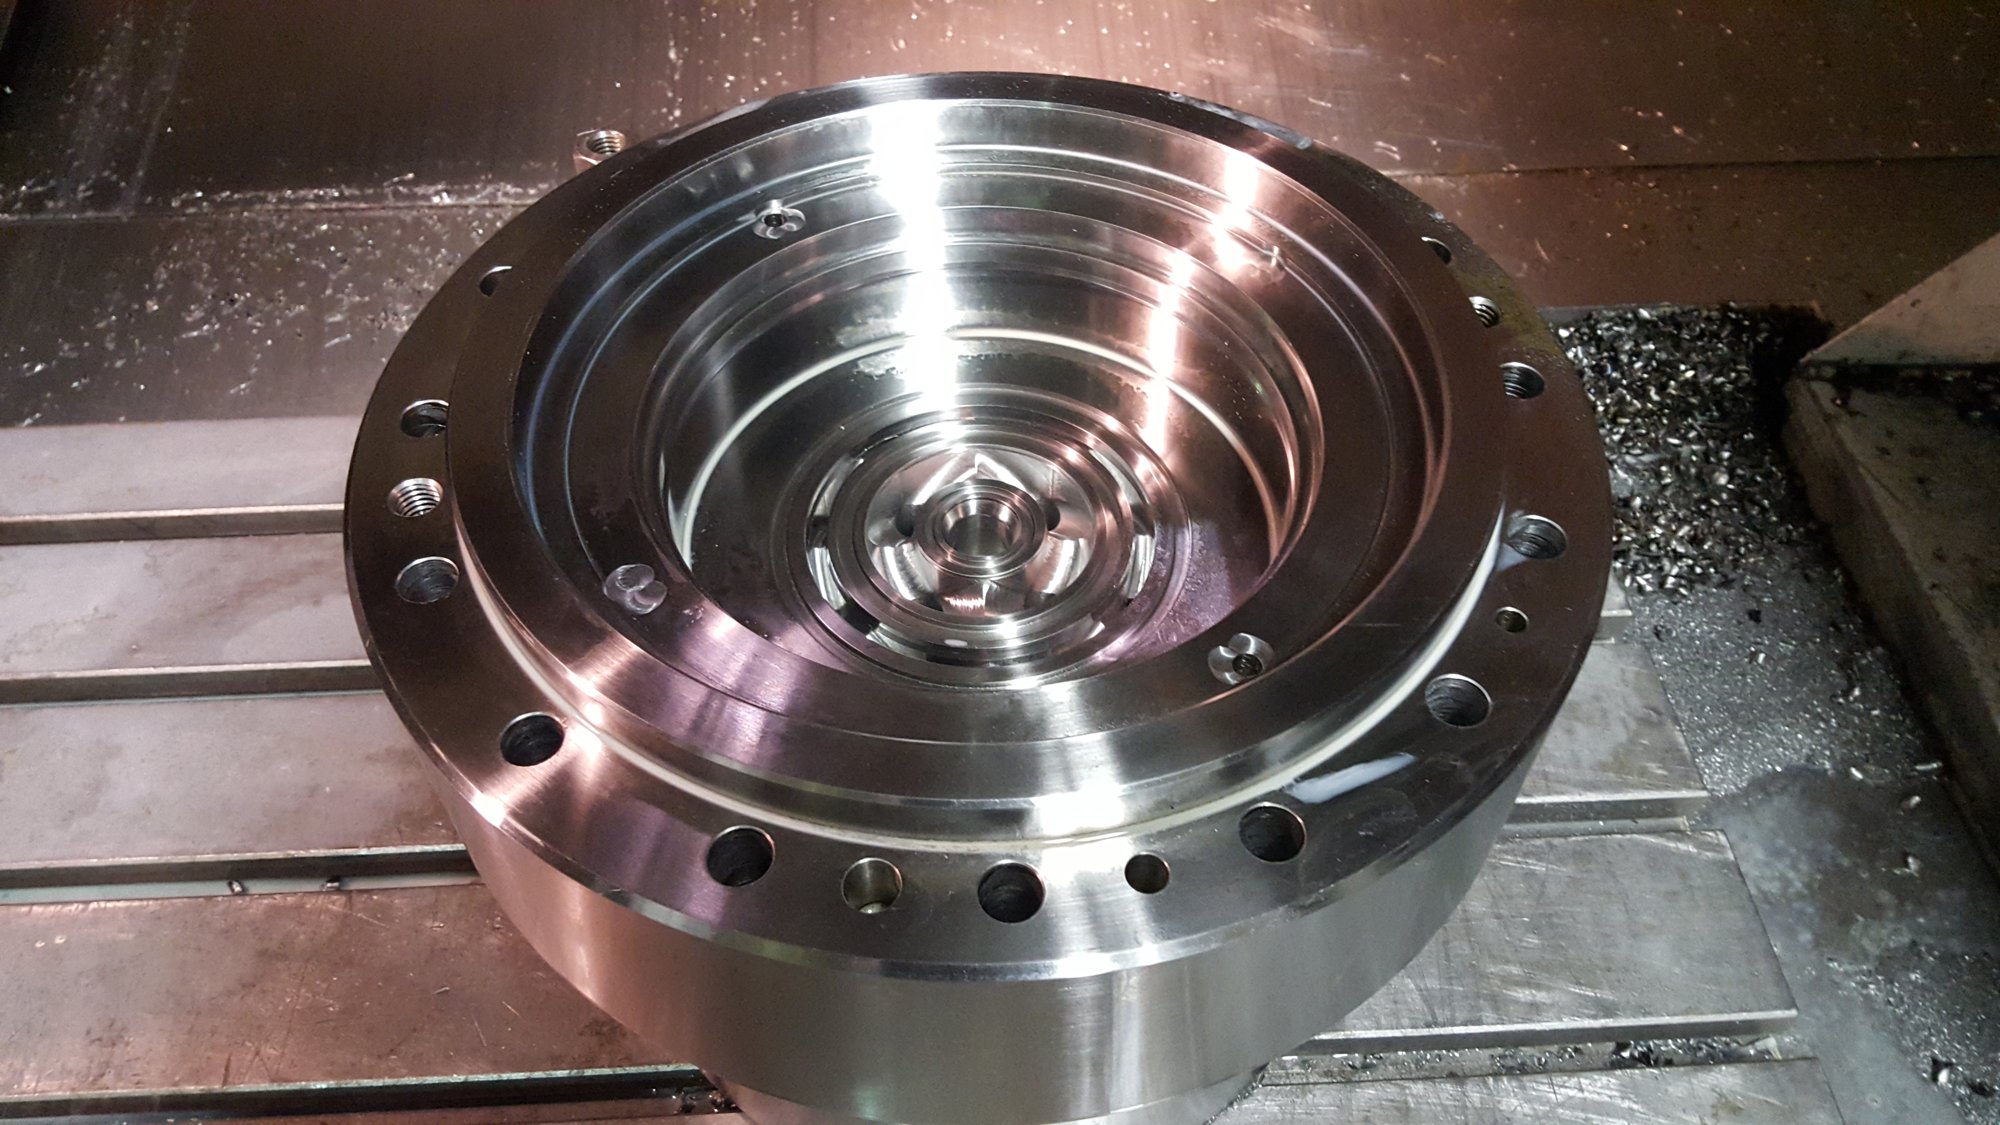
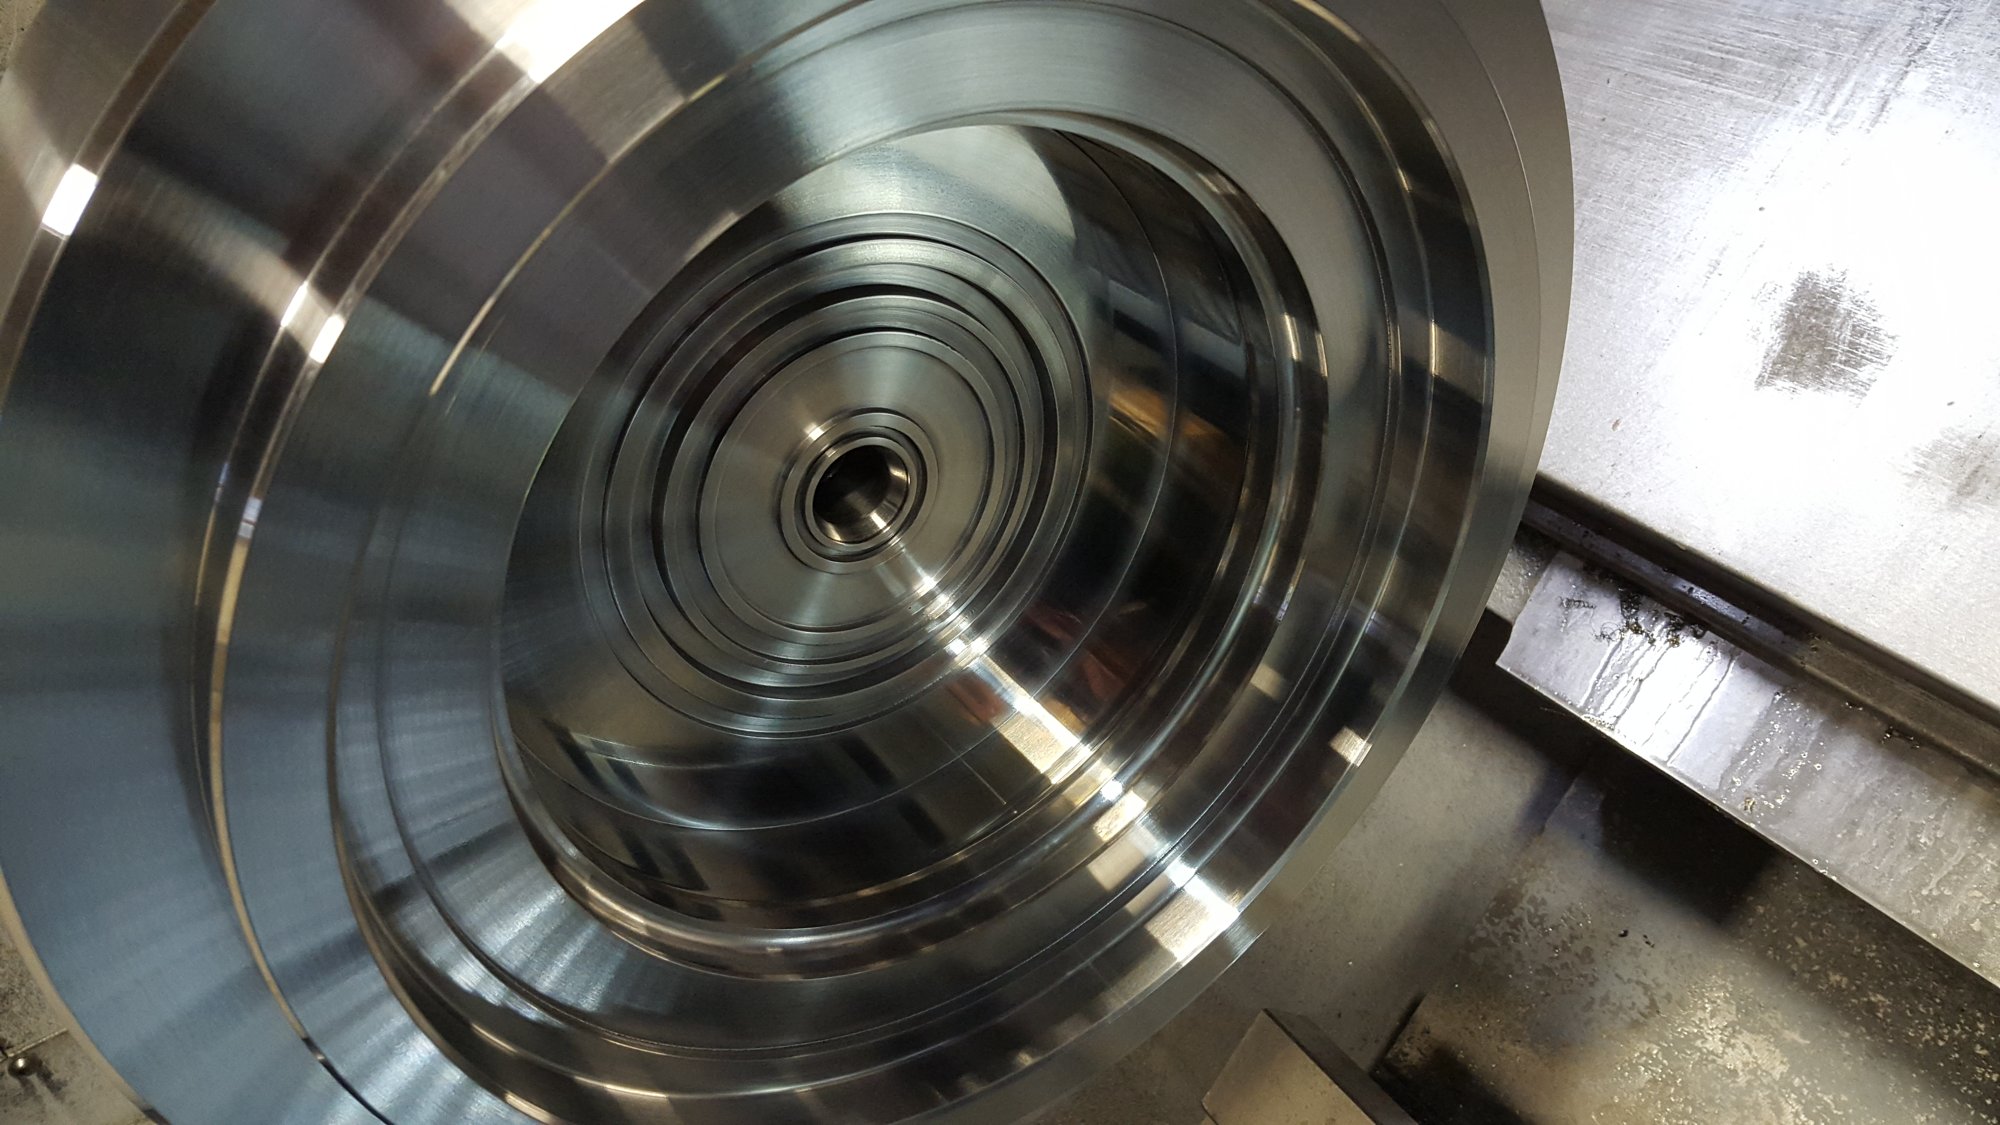
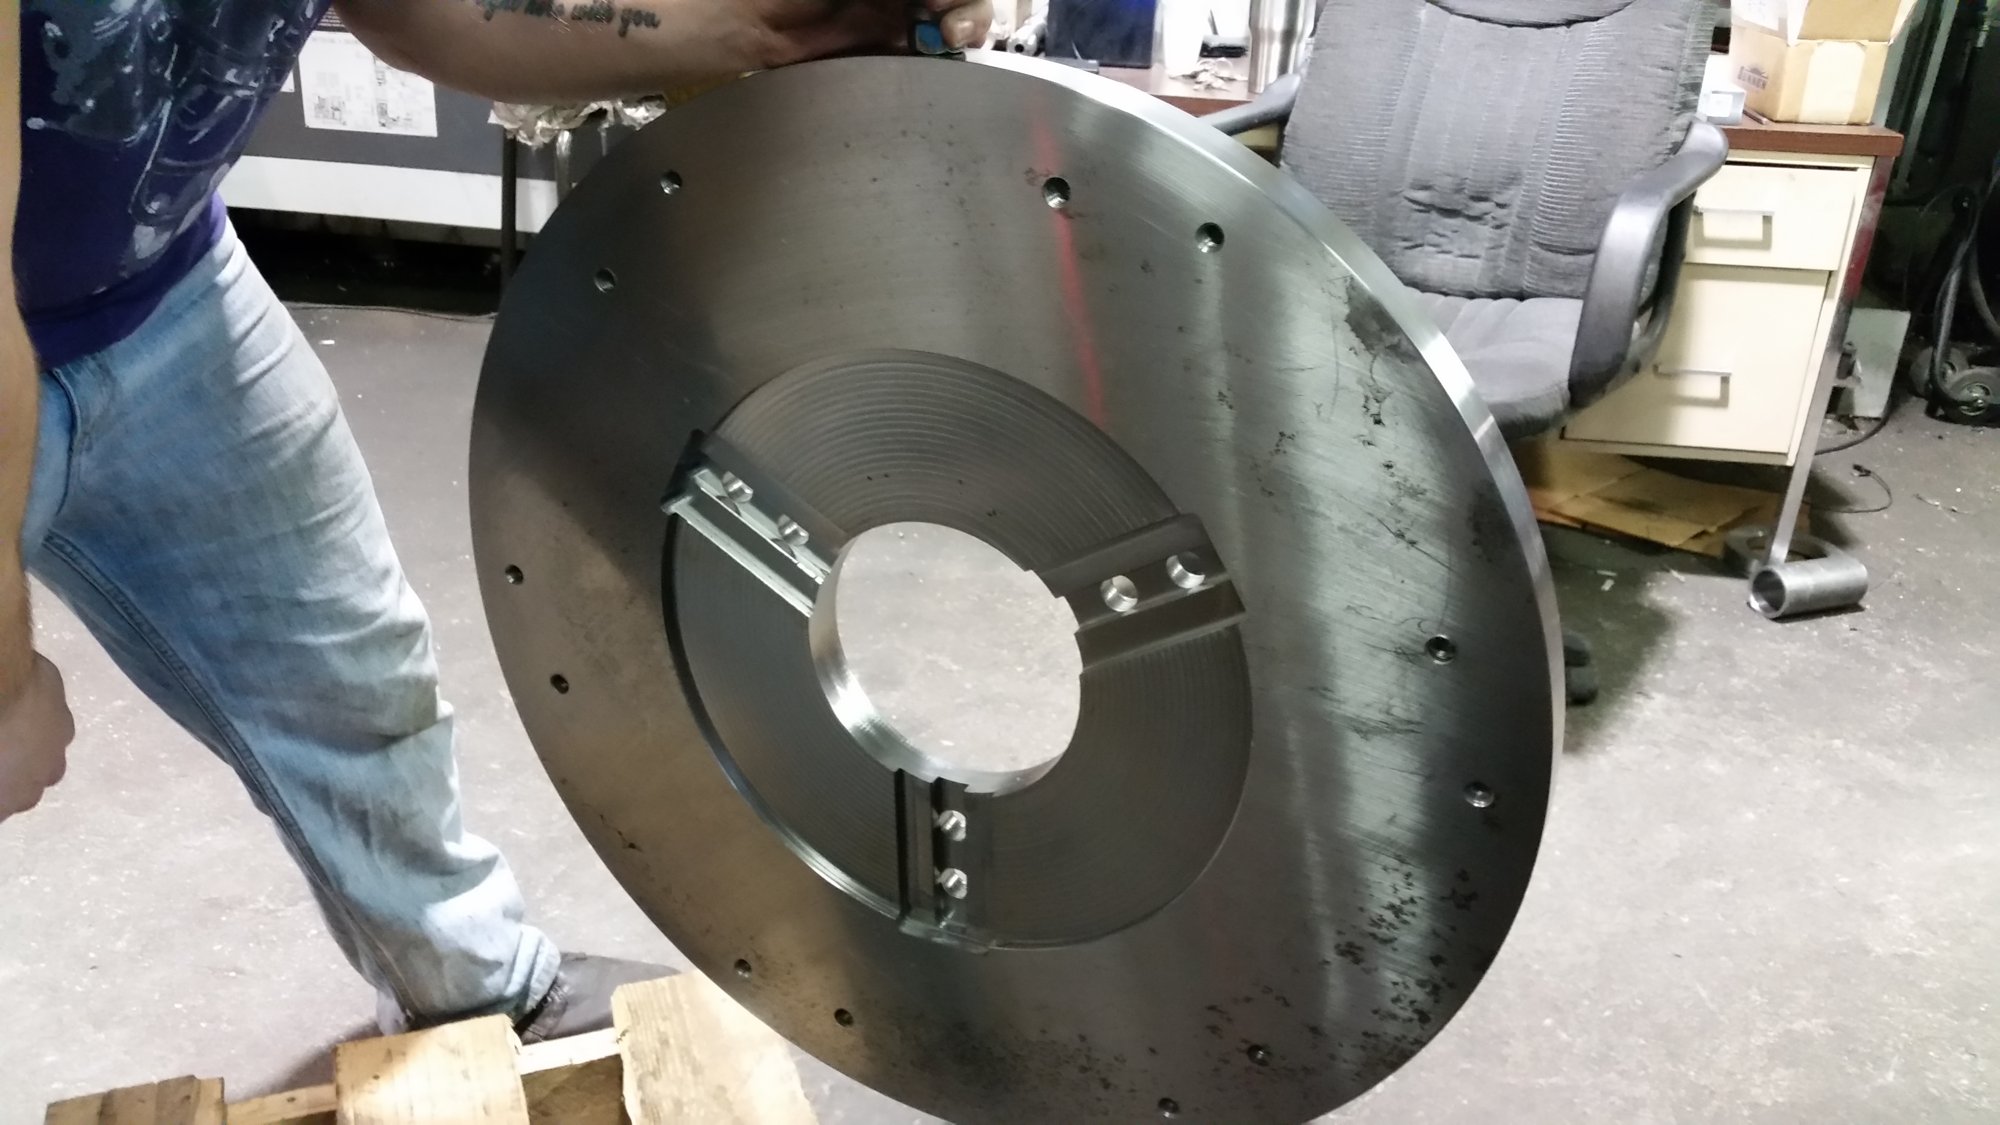
Large flanged plate on the machine table, concentric steps turned into the face inside the bolt circle
Large machining: Concentric steps turned into a large flanged plate
Long shaft turned on the engine lathe, carried in the steady rest to hold it true over the length
Shaft machining: Long shaft carried in the steady rest to hold it true
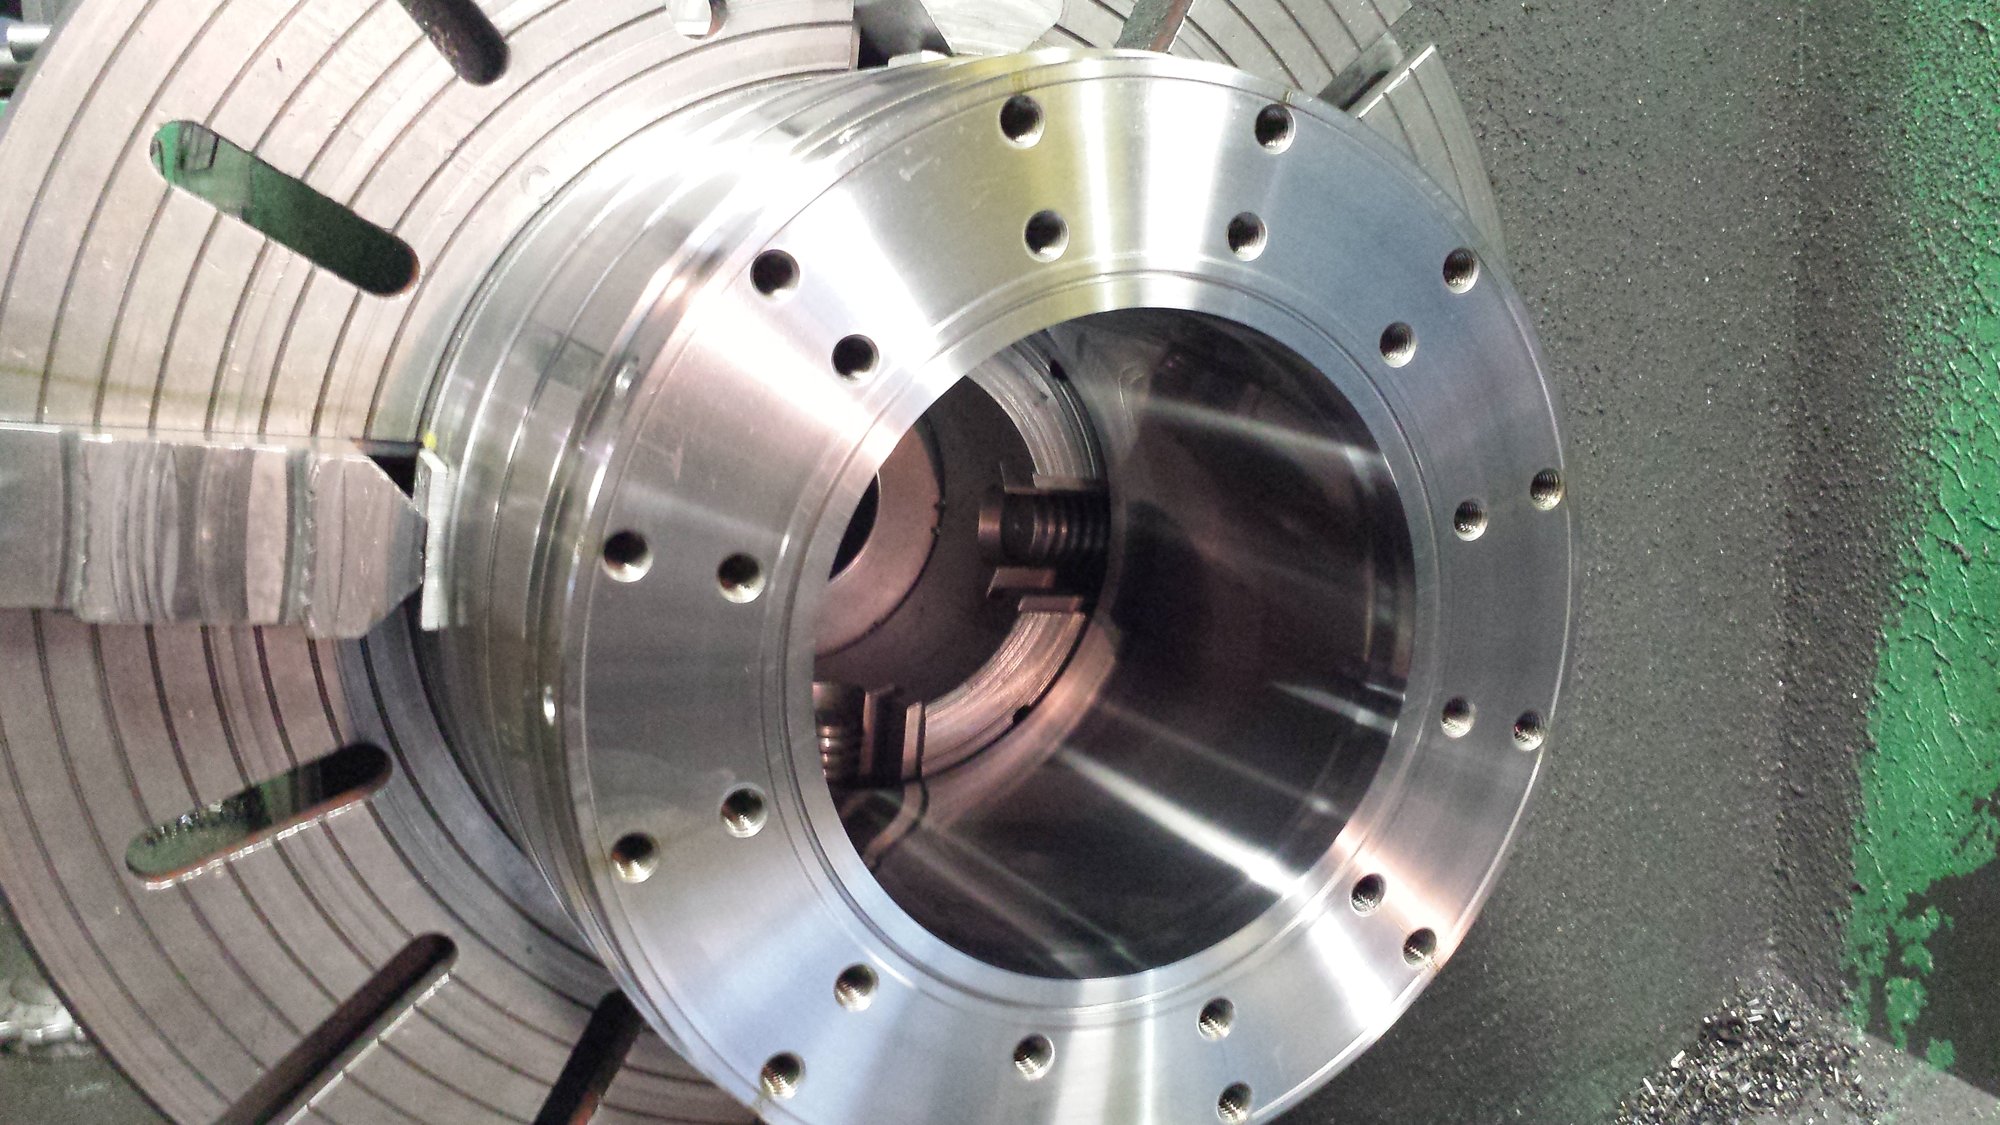
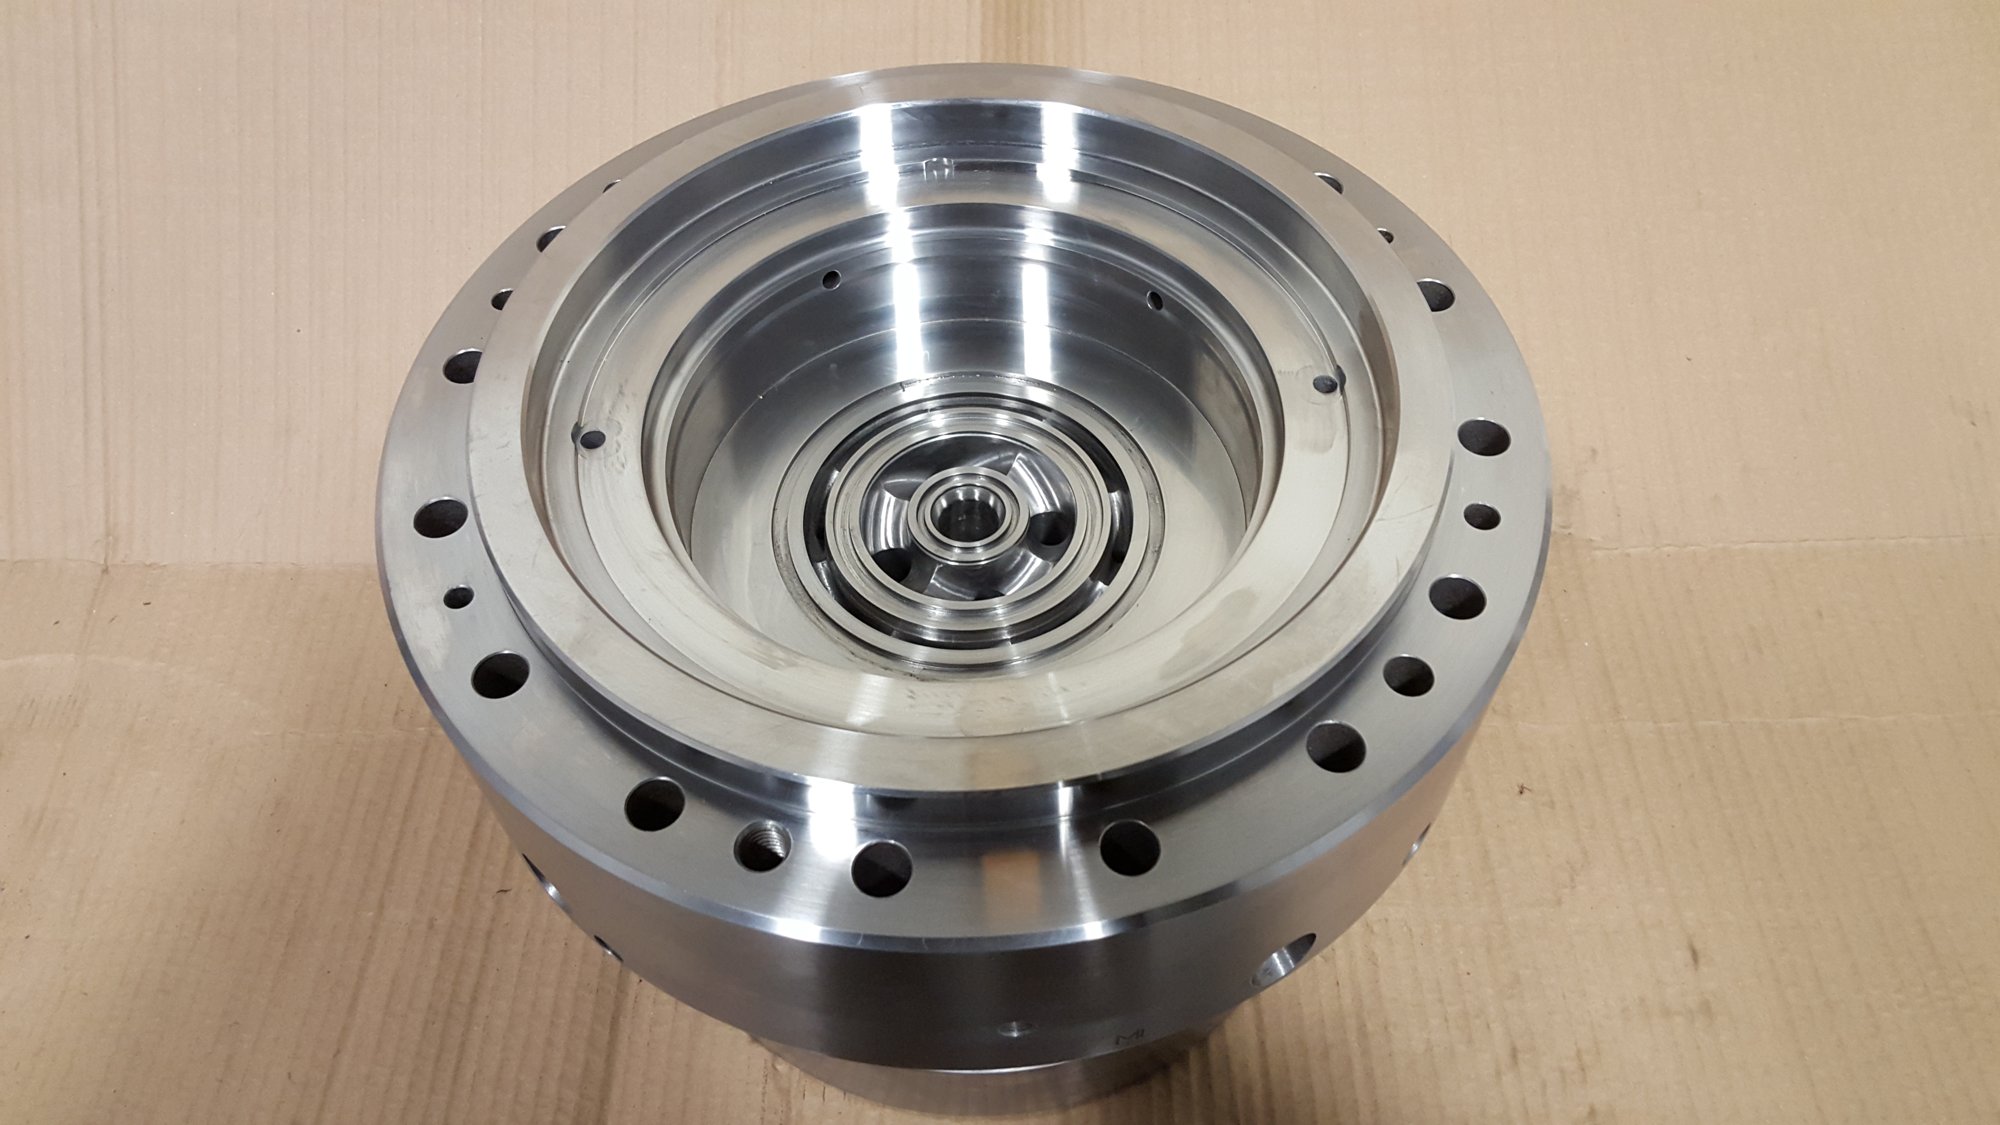
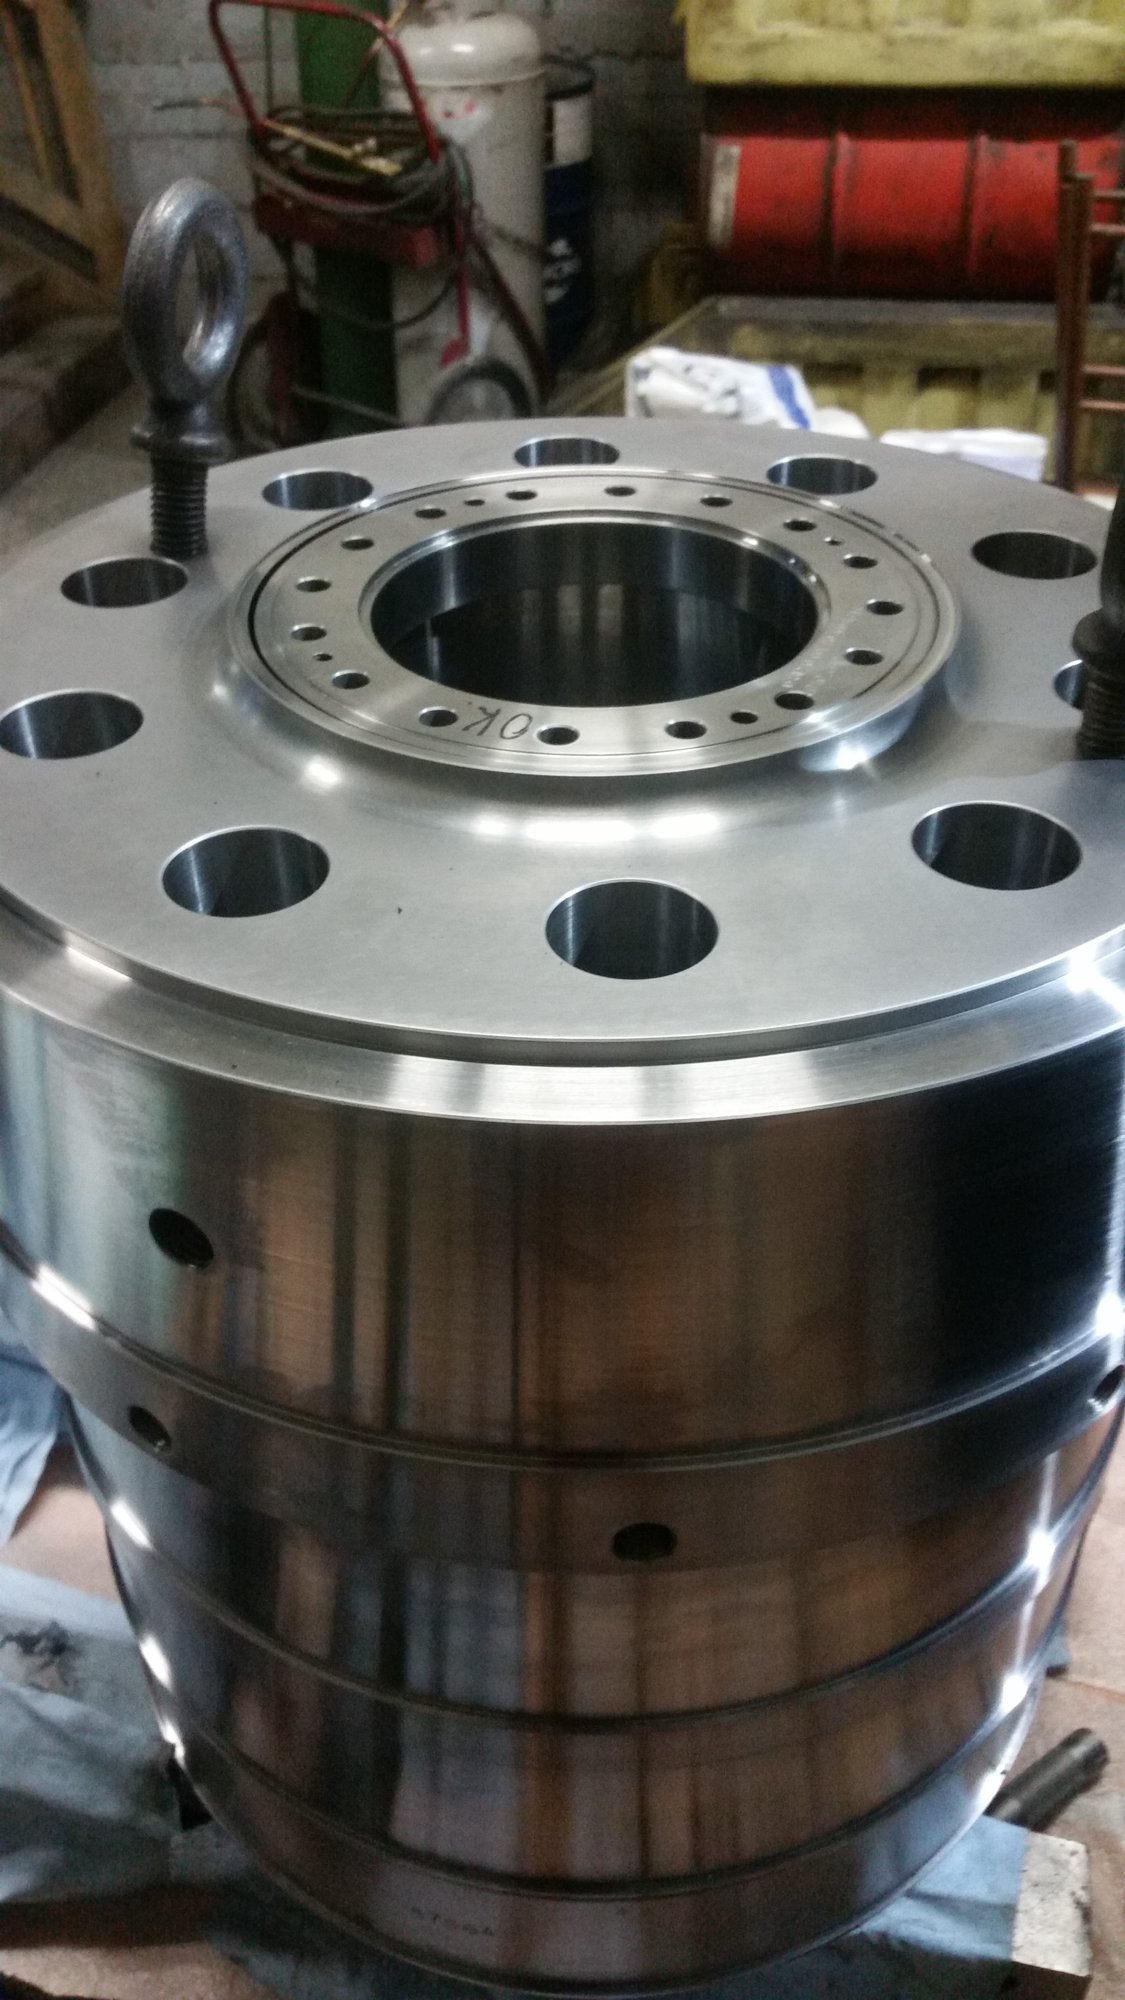
Flanged die assembly showing the bored centre and bolt pattern
Blown film dies: Flanged die assembly, bored centre and bolt pattern
Three machined stepped sleeves with a micrometer alongside, grooved bodies and flanged bases
Turning and production: Stepped sleeves, with the micrometer that checked them
Die block billet chucked in the lathe and supported on a live centre before the first cut
One die, start to finish (3 of 10): Chucked in the lathe and picked up on a live centre
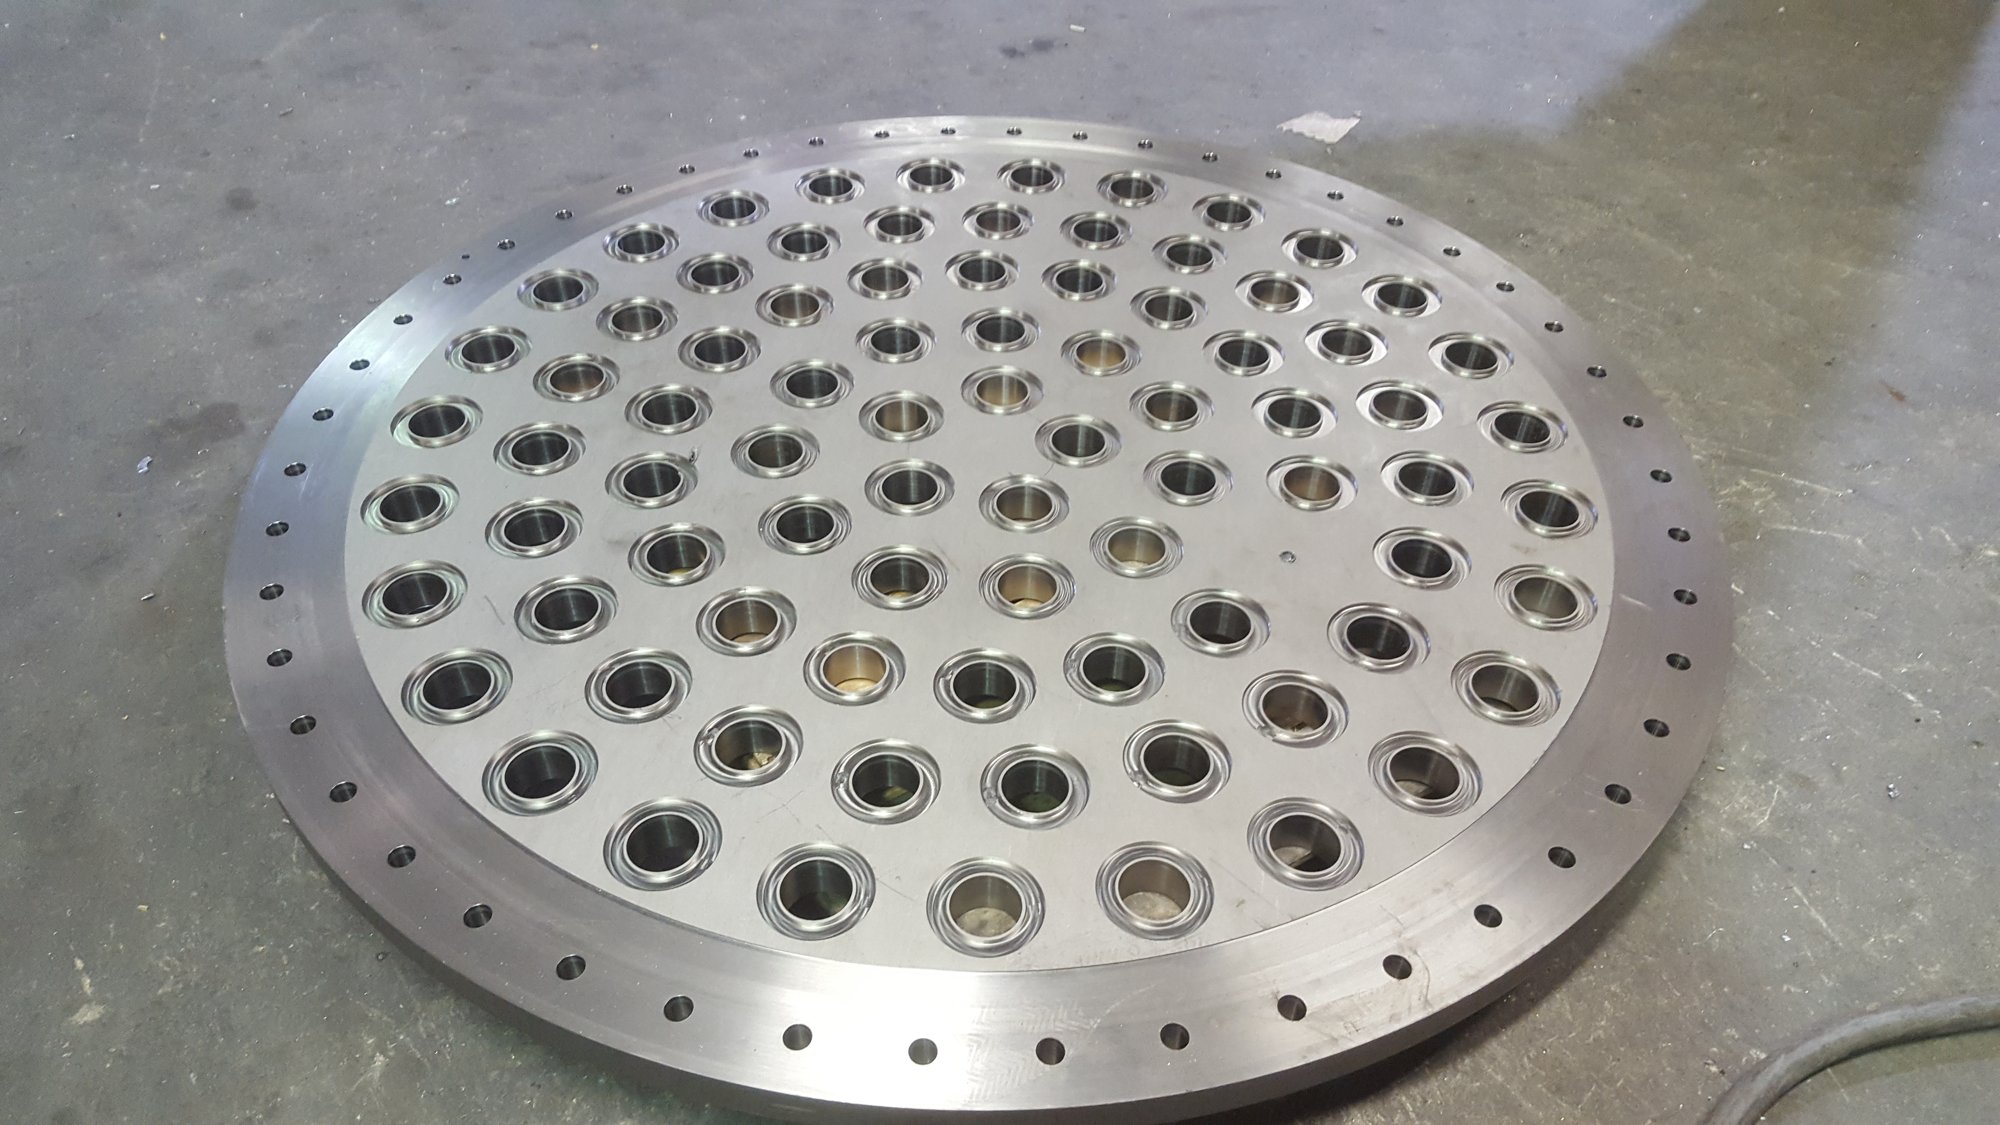
Large drilled tube sheet, every tube hole bored and chamfered inside the outer bolt circle
Large machining: Tube sheet, every hole bored and chamfered
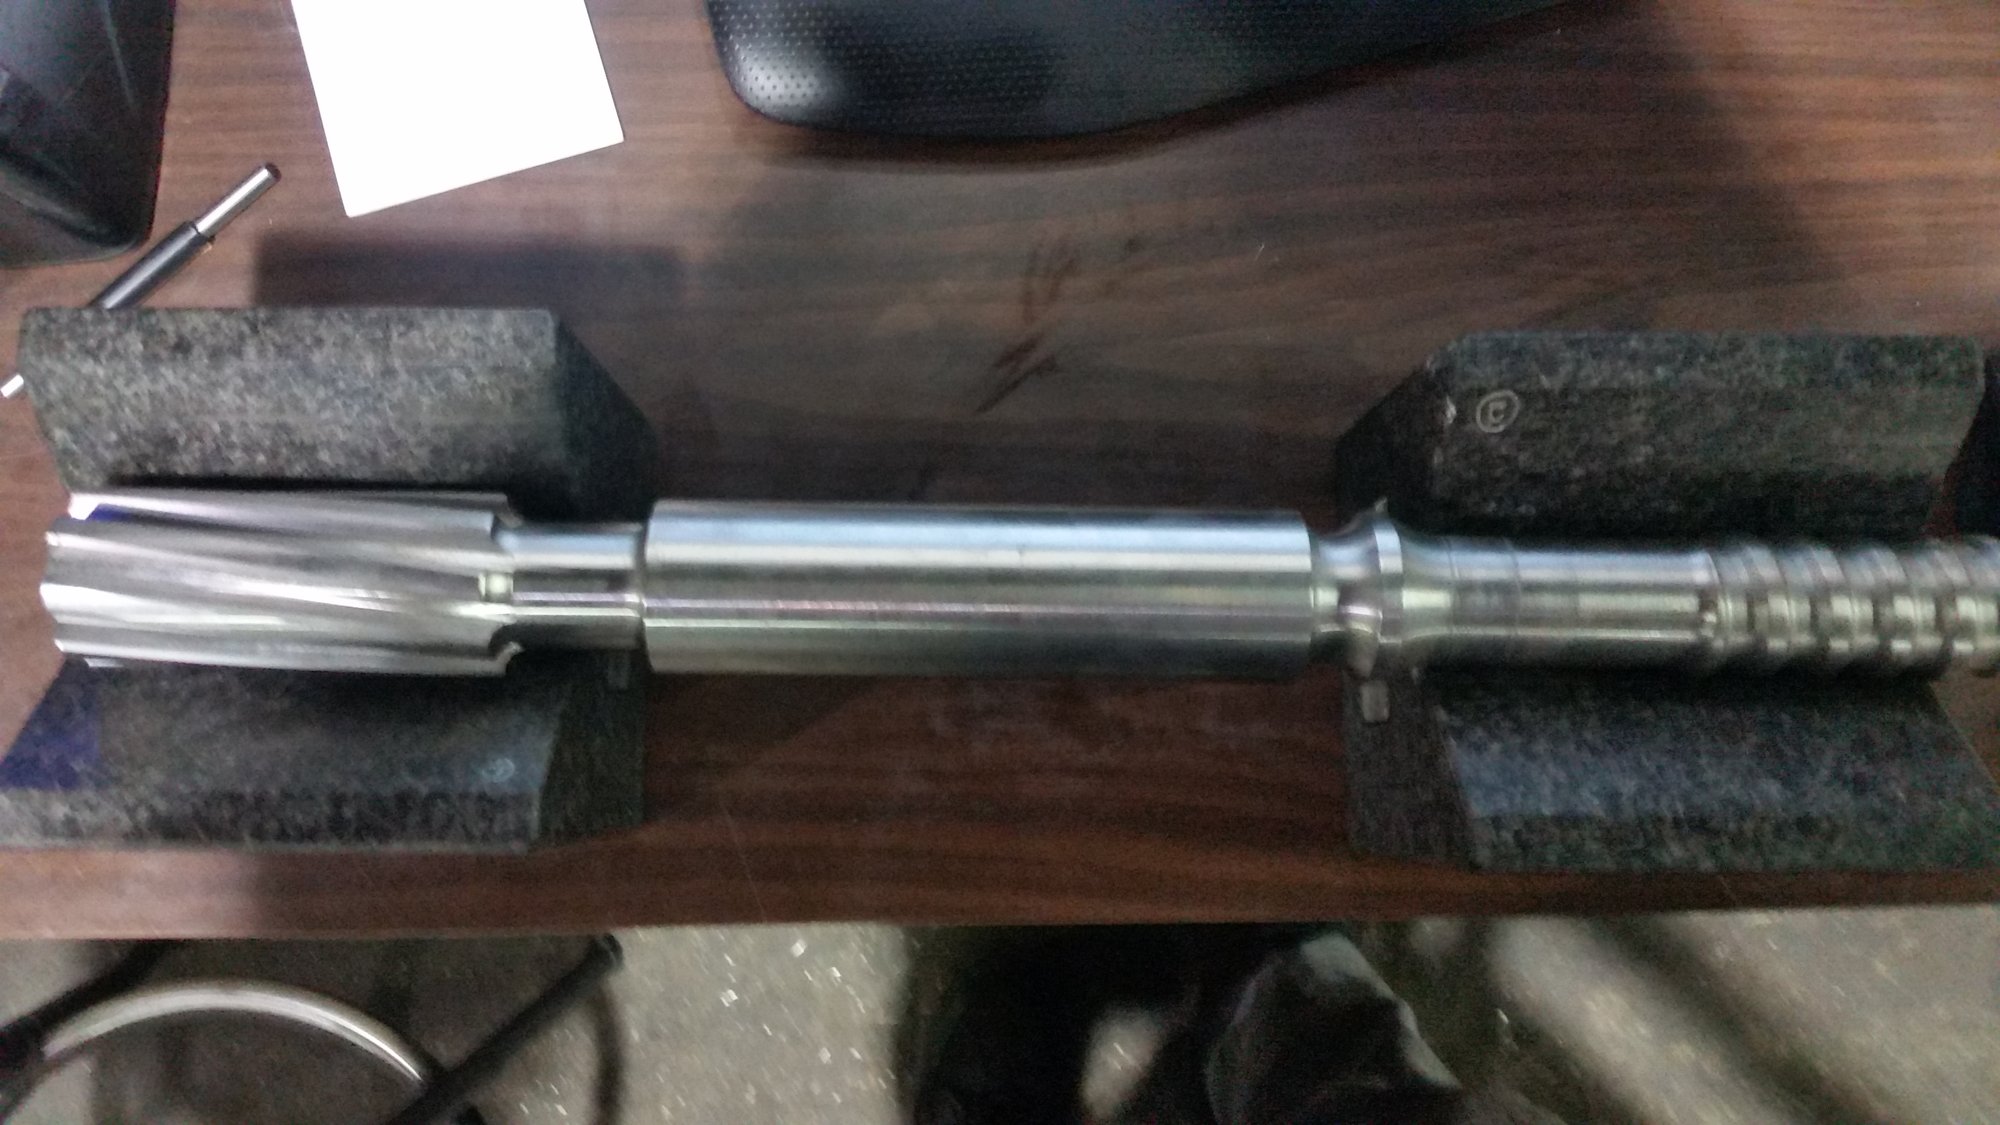
Finished screw shaft set on granite blocks, fluted drive end at one side and the flighted section at the other
Extruder parts: The finished screw, full length, on granite blocks
Large flanged extrusion die assembly on the bench
Blown film dies: Large flanged extrusion die assembly on the bench
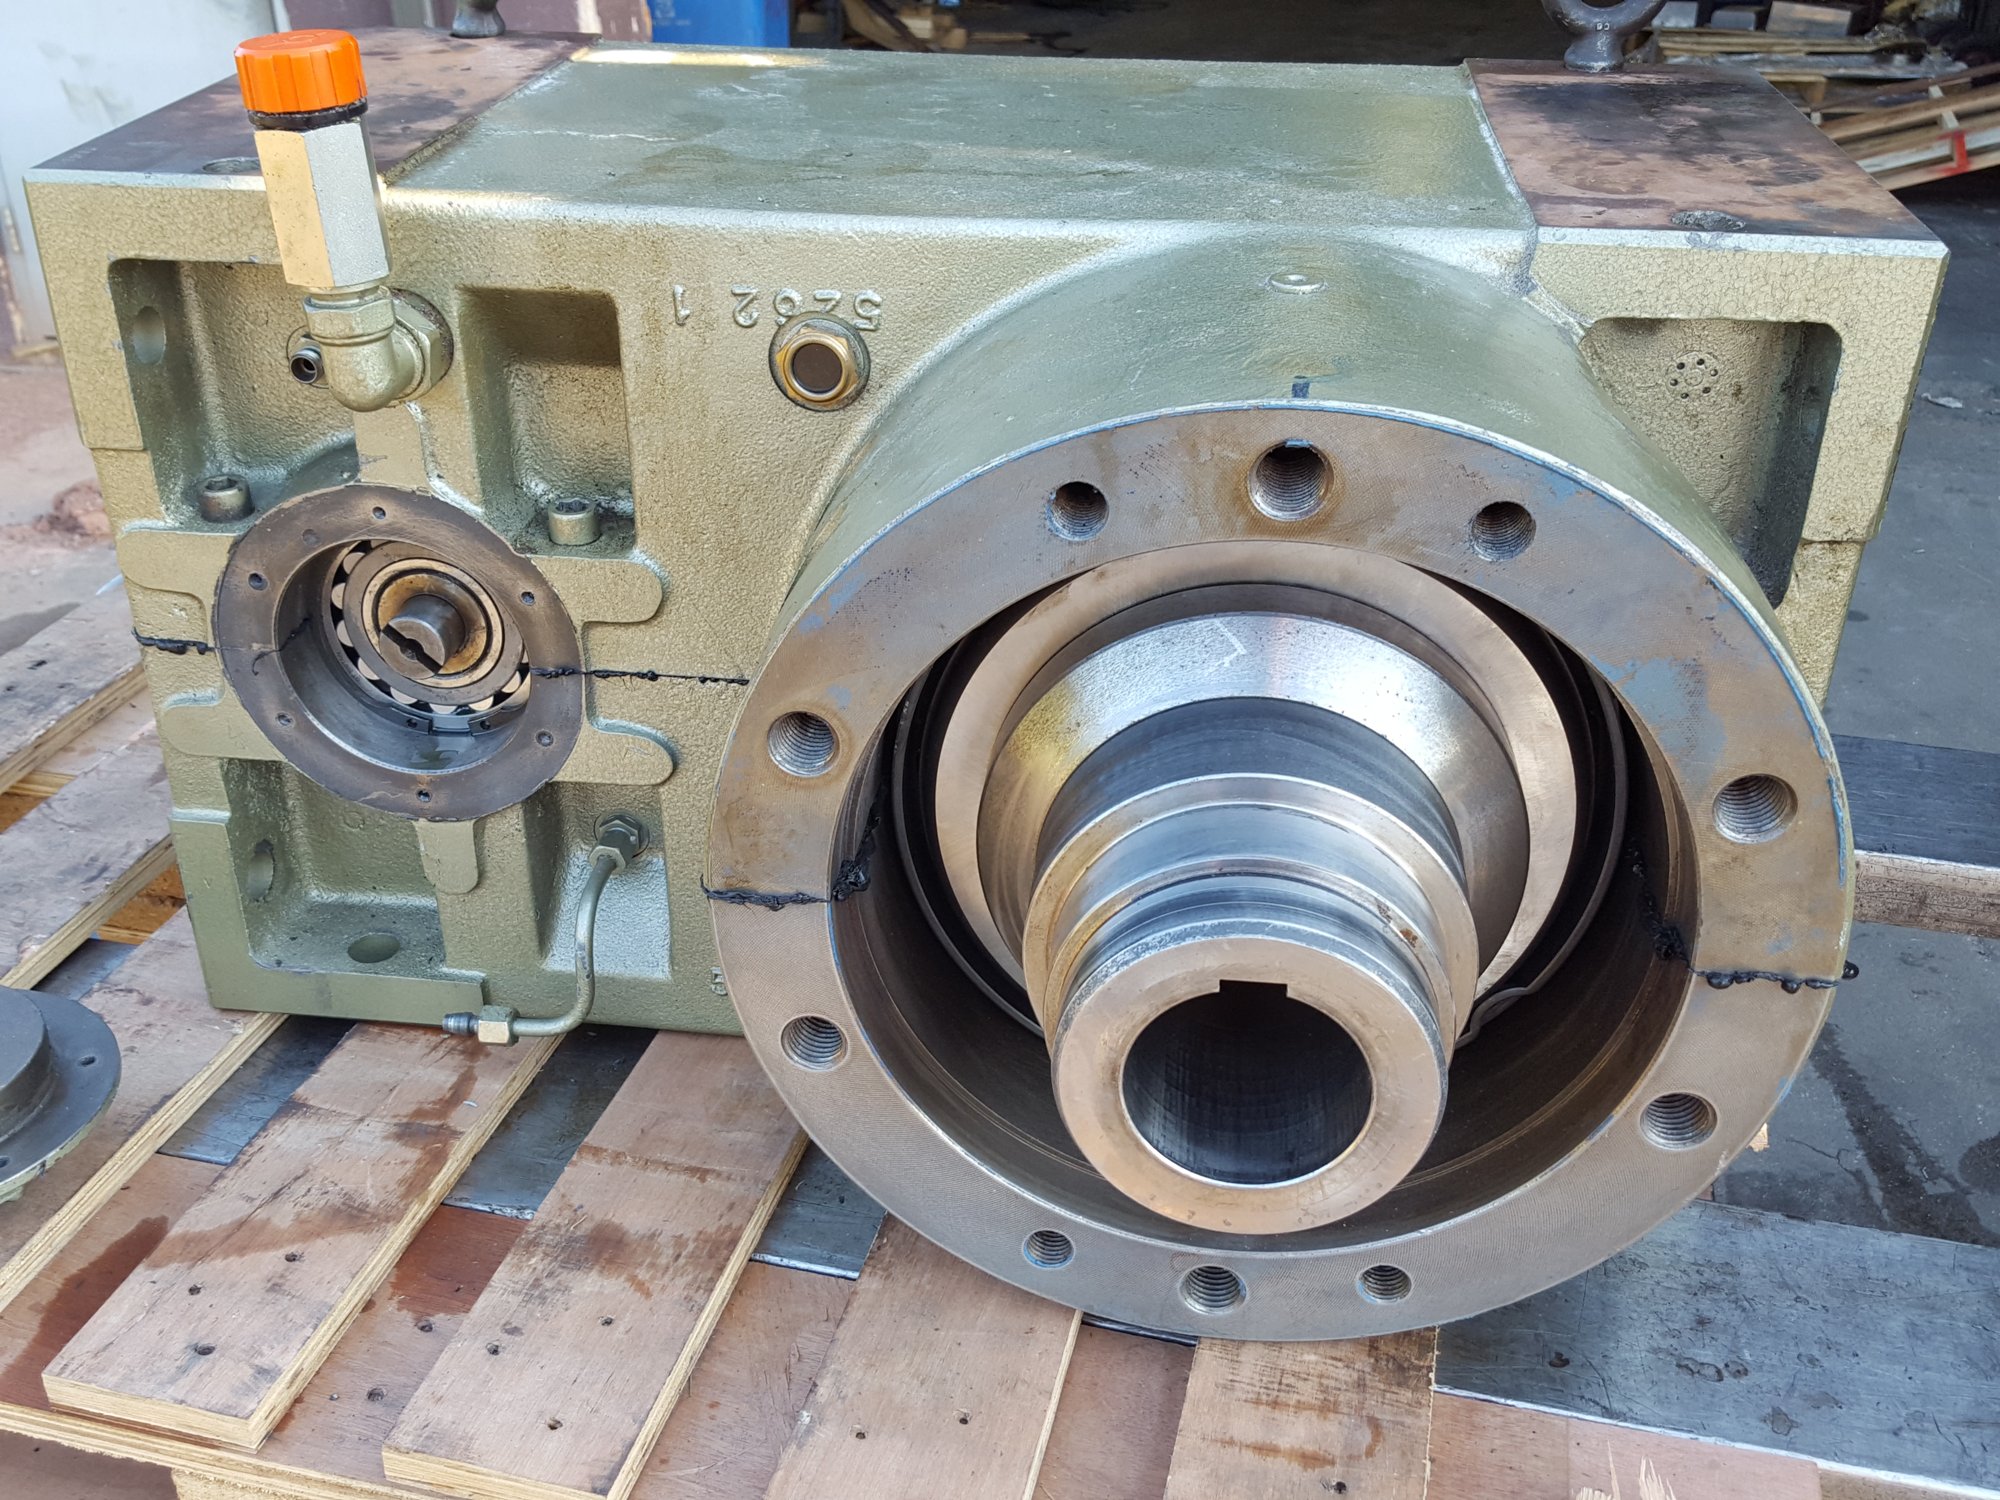
Extruder gearbox housing with the output bearing bore during in-house line boring repair
Gearbox repair: Output bearing bore repaired in house
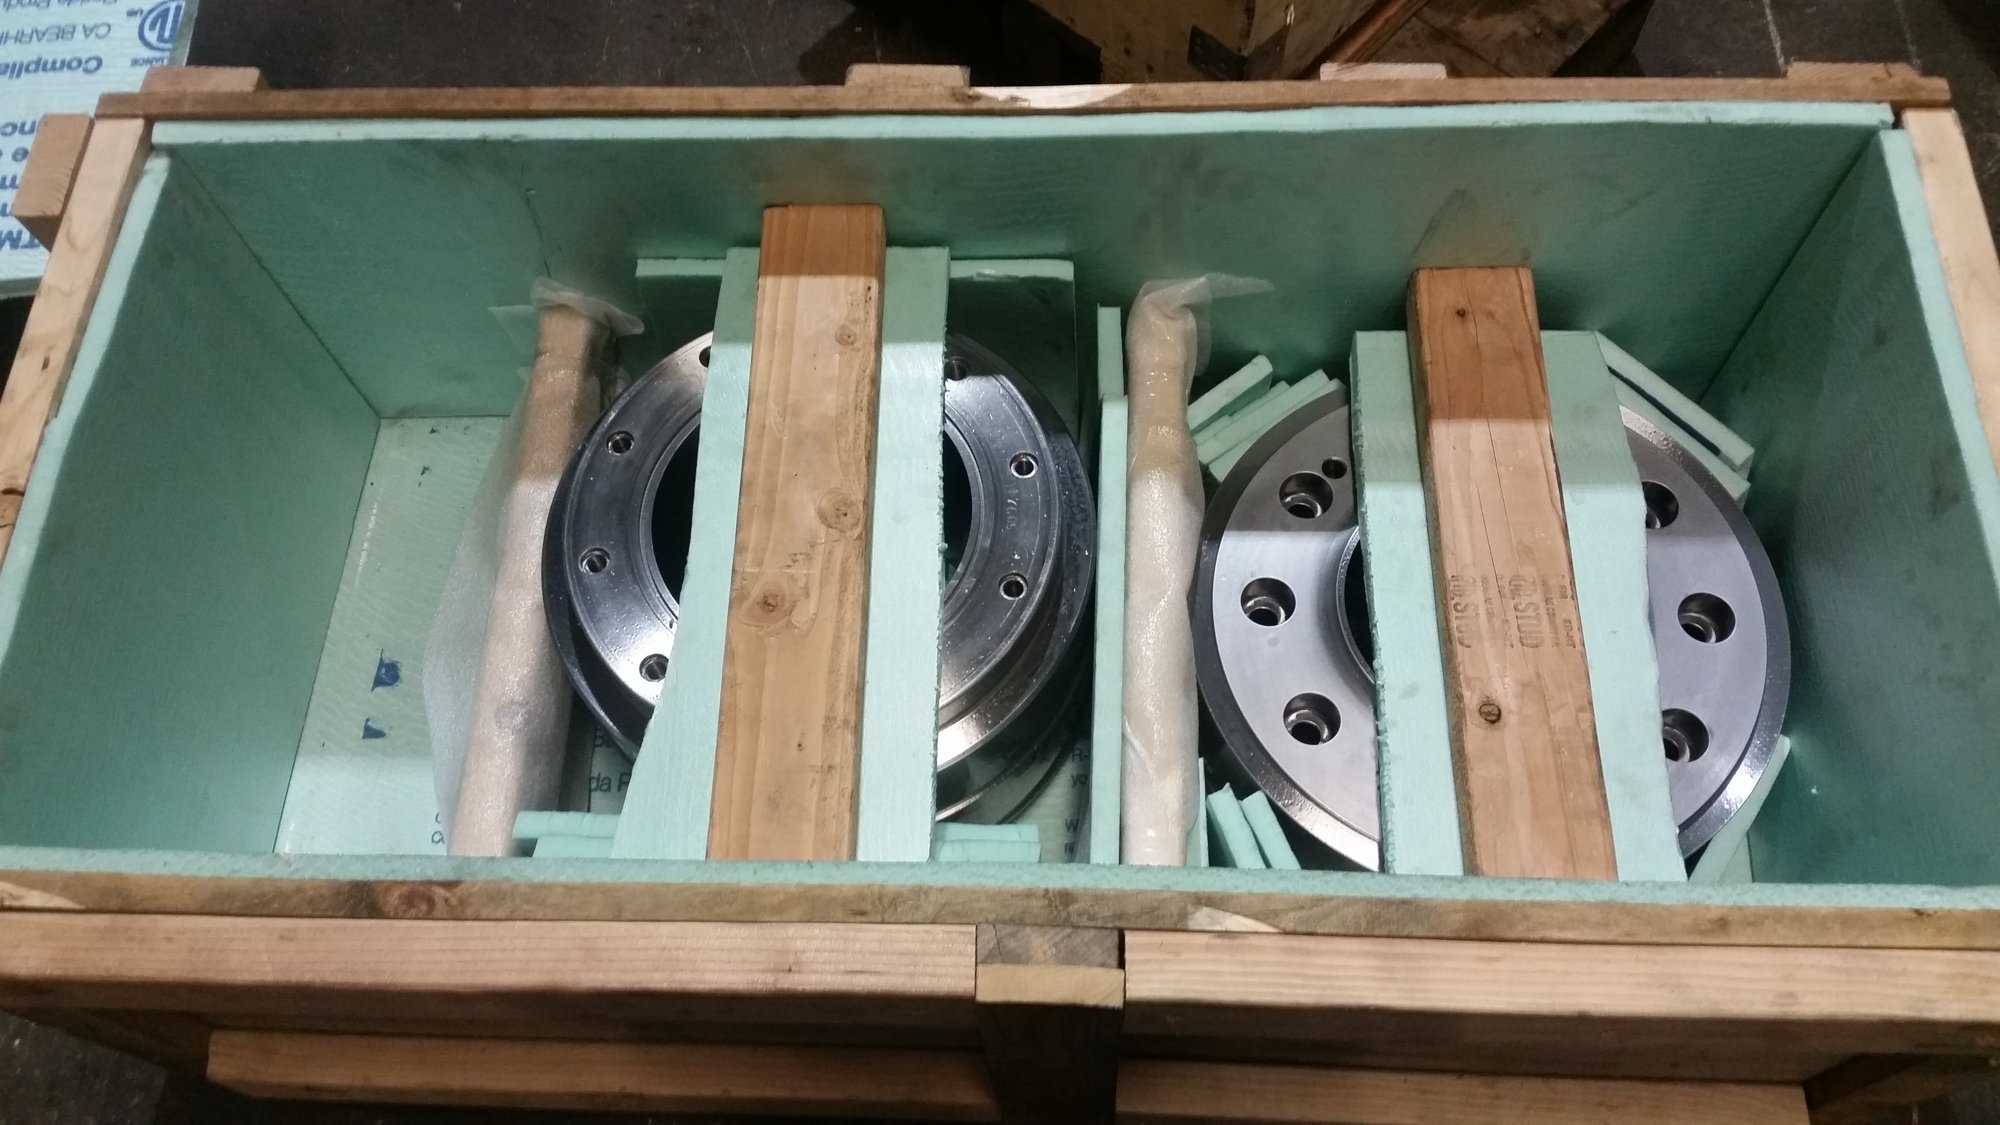
Two machined flange parts blocked upright in a lined crate, braced with timber for shipping
Fabrication and shipping: Flange parts blocked upright in a lined crate
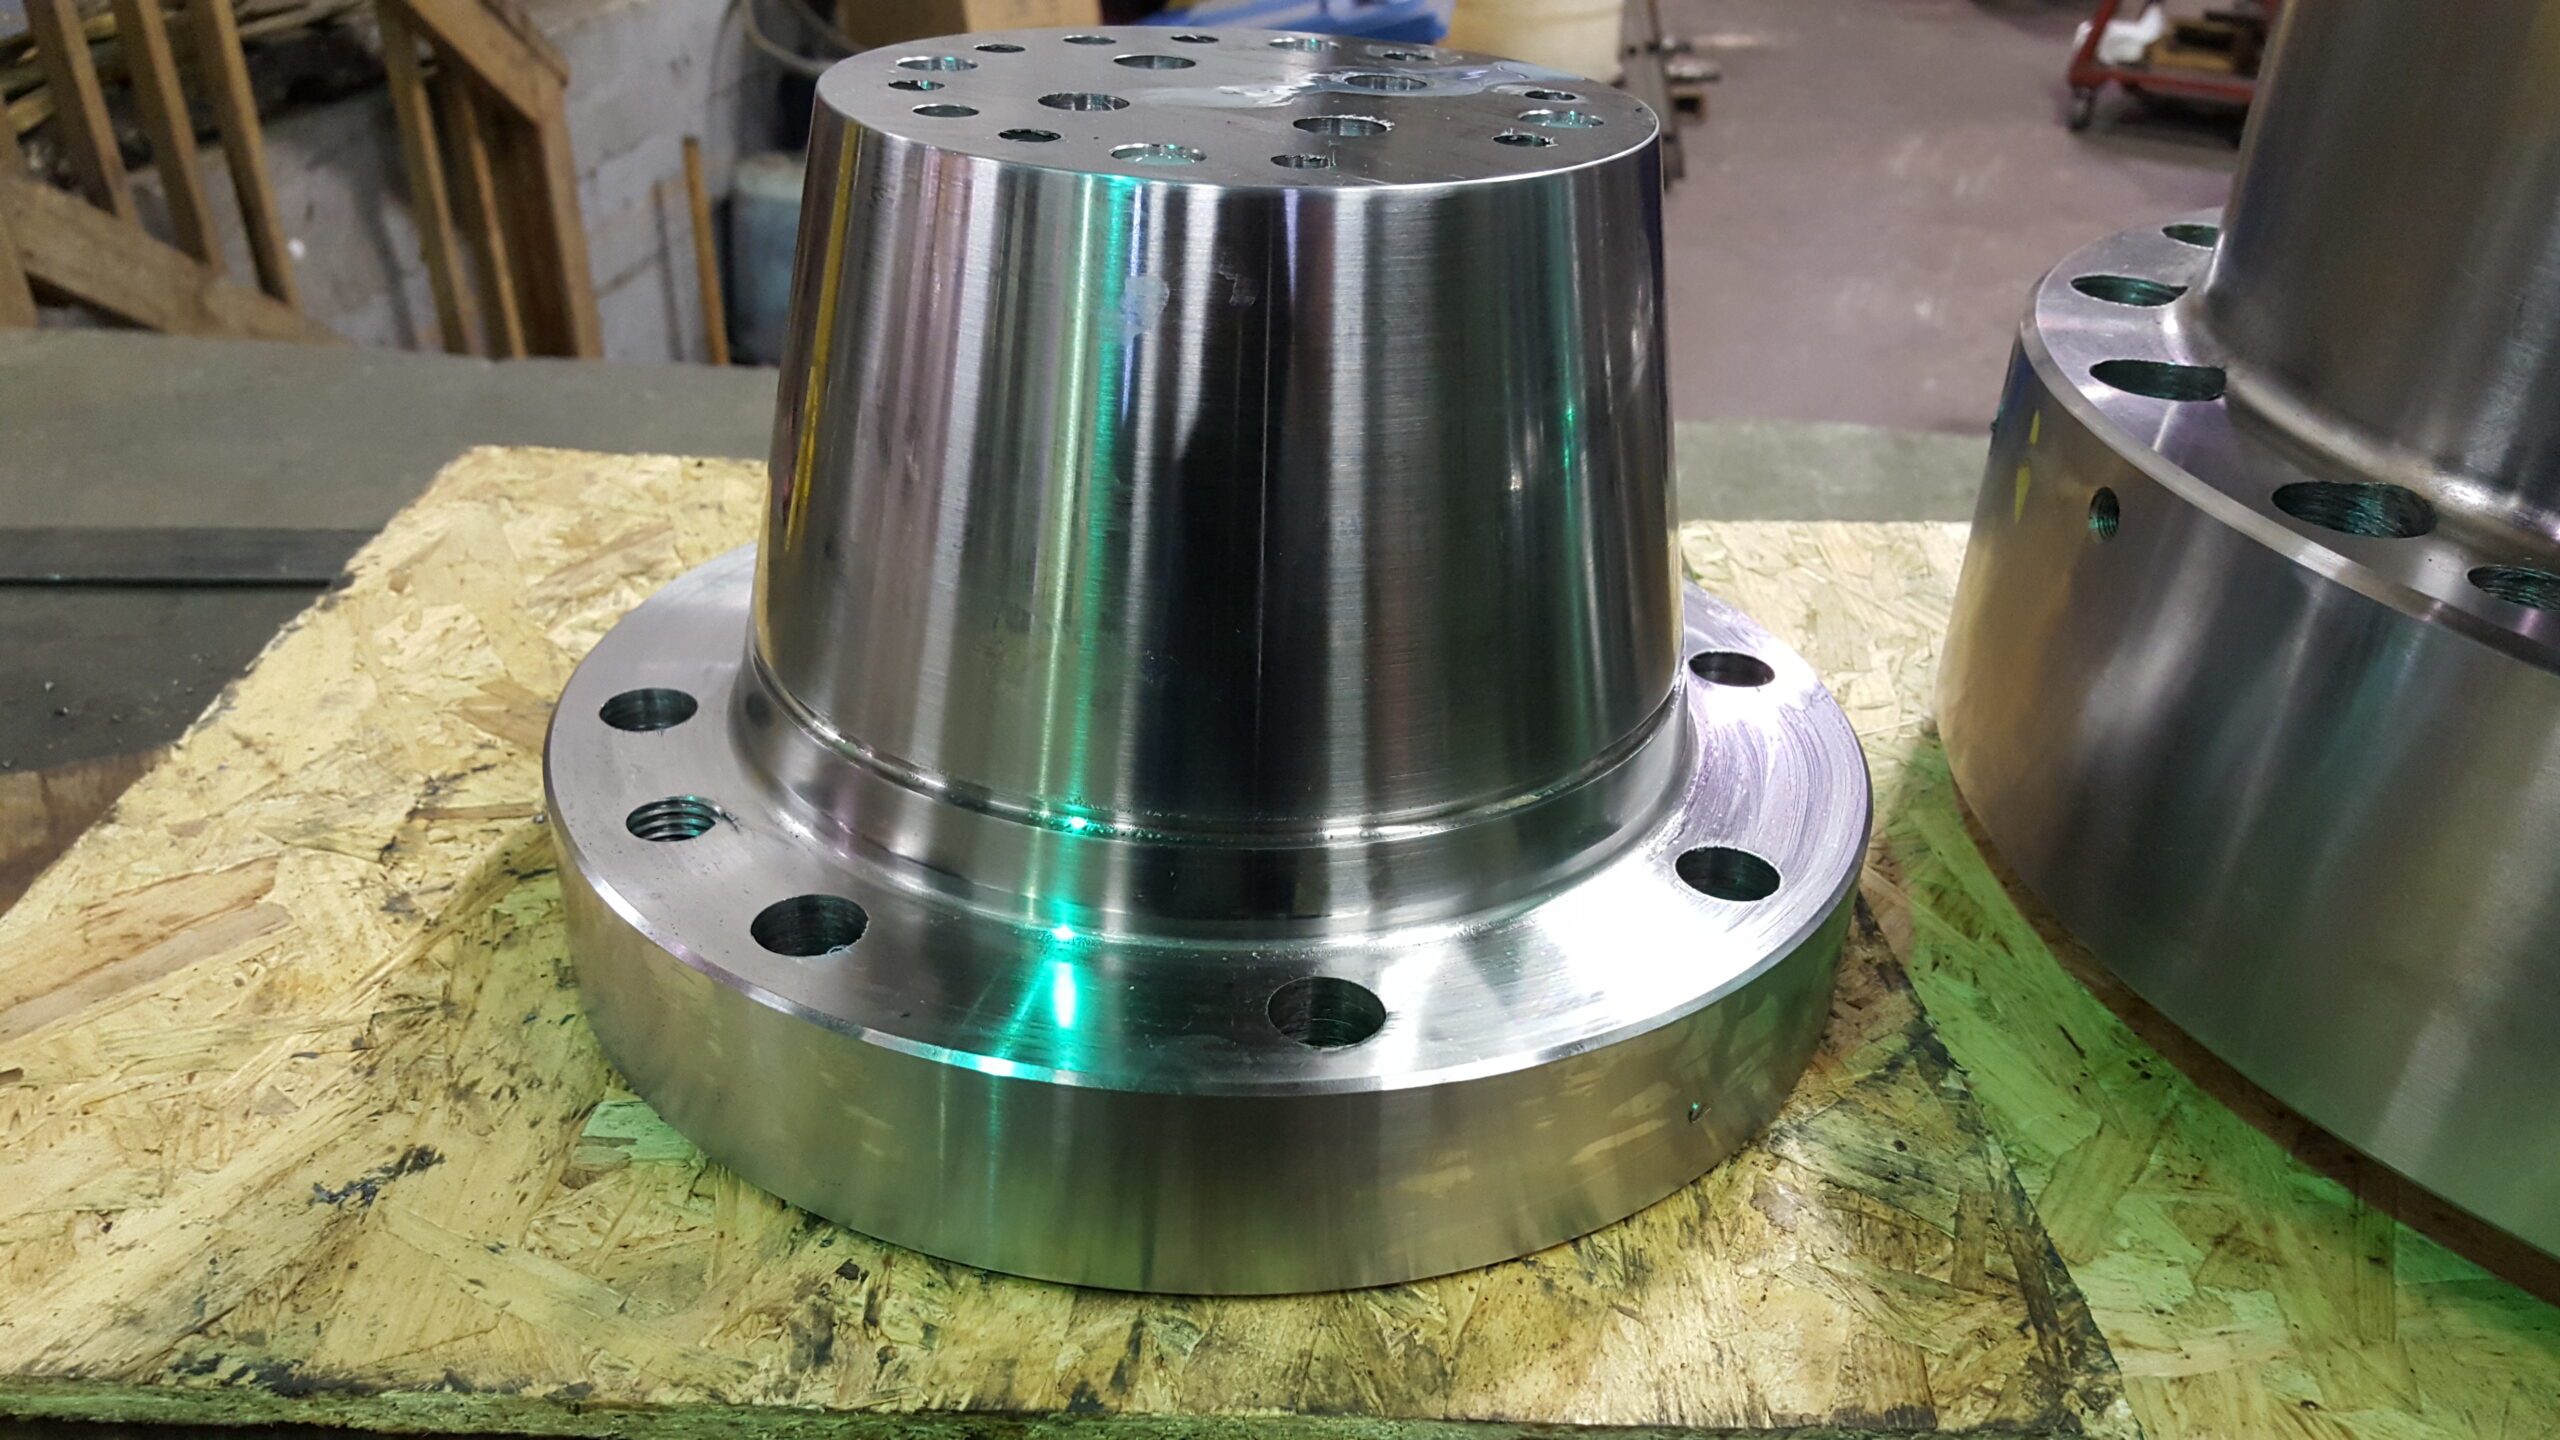
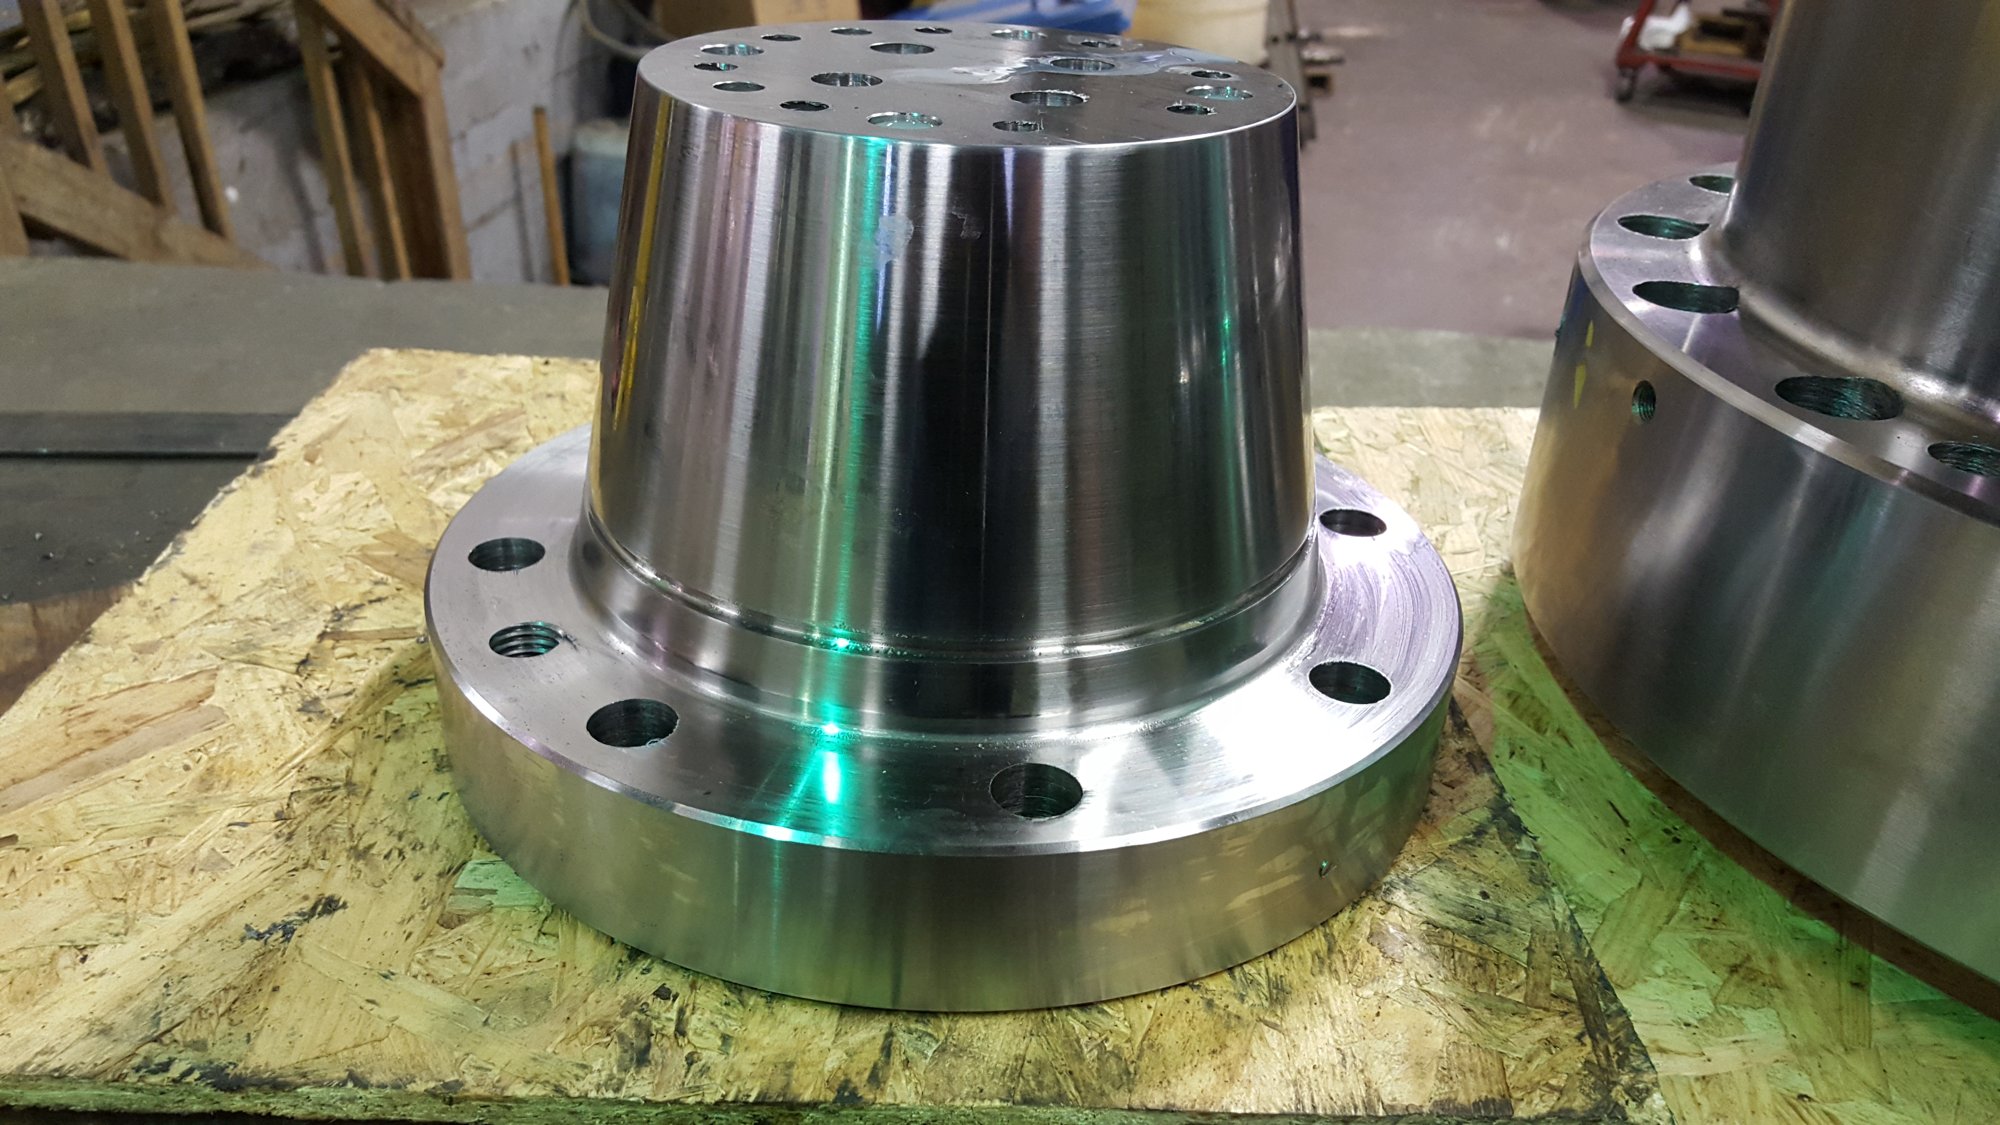
Tapered extrusion die body with mounting flange
Blown film dies: Tapered die body with mounting flange
Machinist working at the bench with parts laid out beside the machine
The shop: At the bench with parts laid out
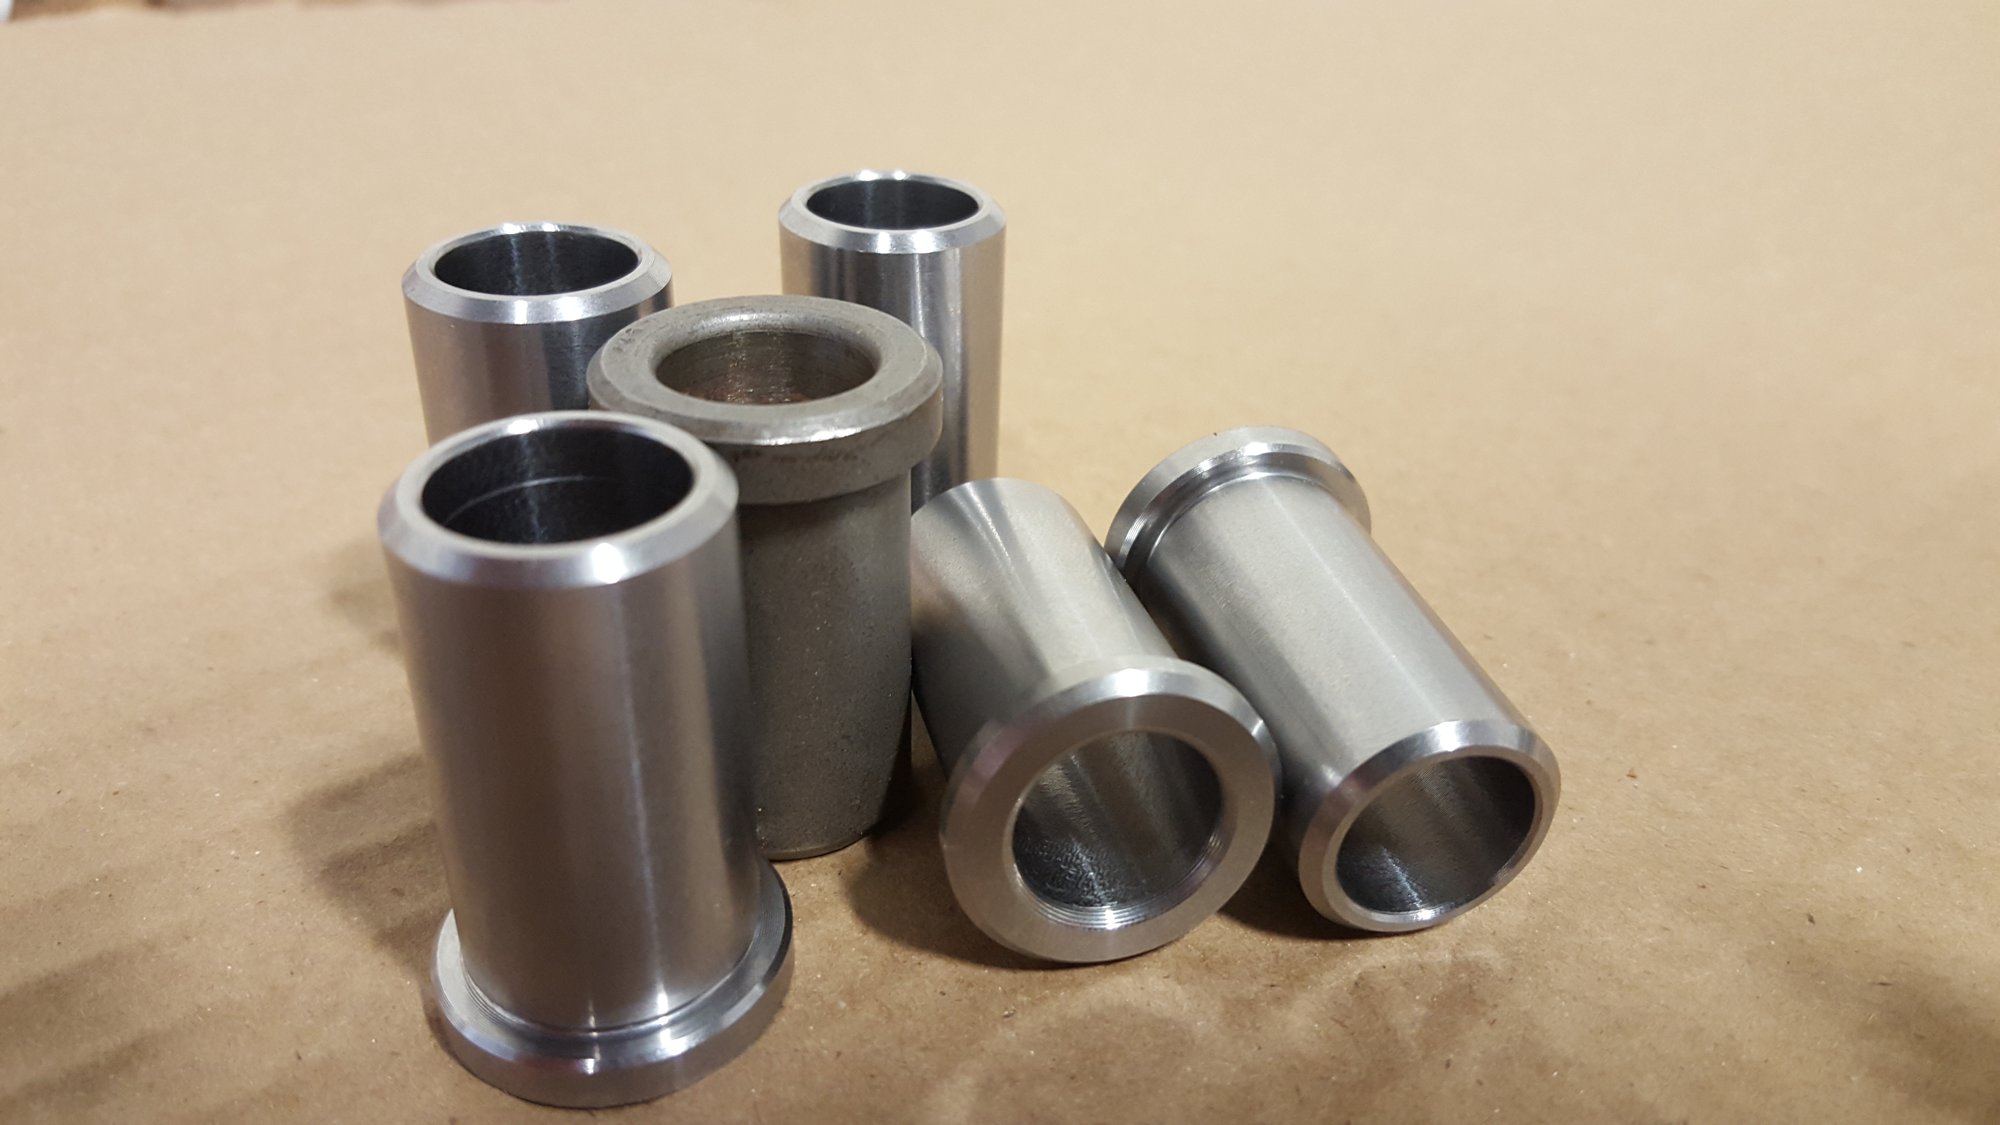
Batch of machined stainless bushings and flanged sleeves grouped on the bench
Turning and production: Stainless bushings and flanged sleeves
Machined bearing plate showing central bore and drilled bolt pattern
Large machining: Bearing plate, central bore and drilled bolt pattern
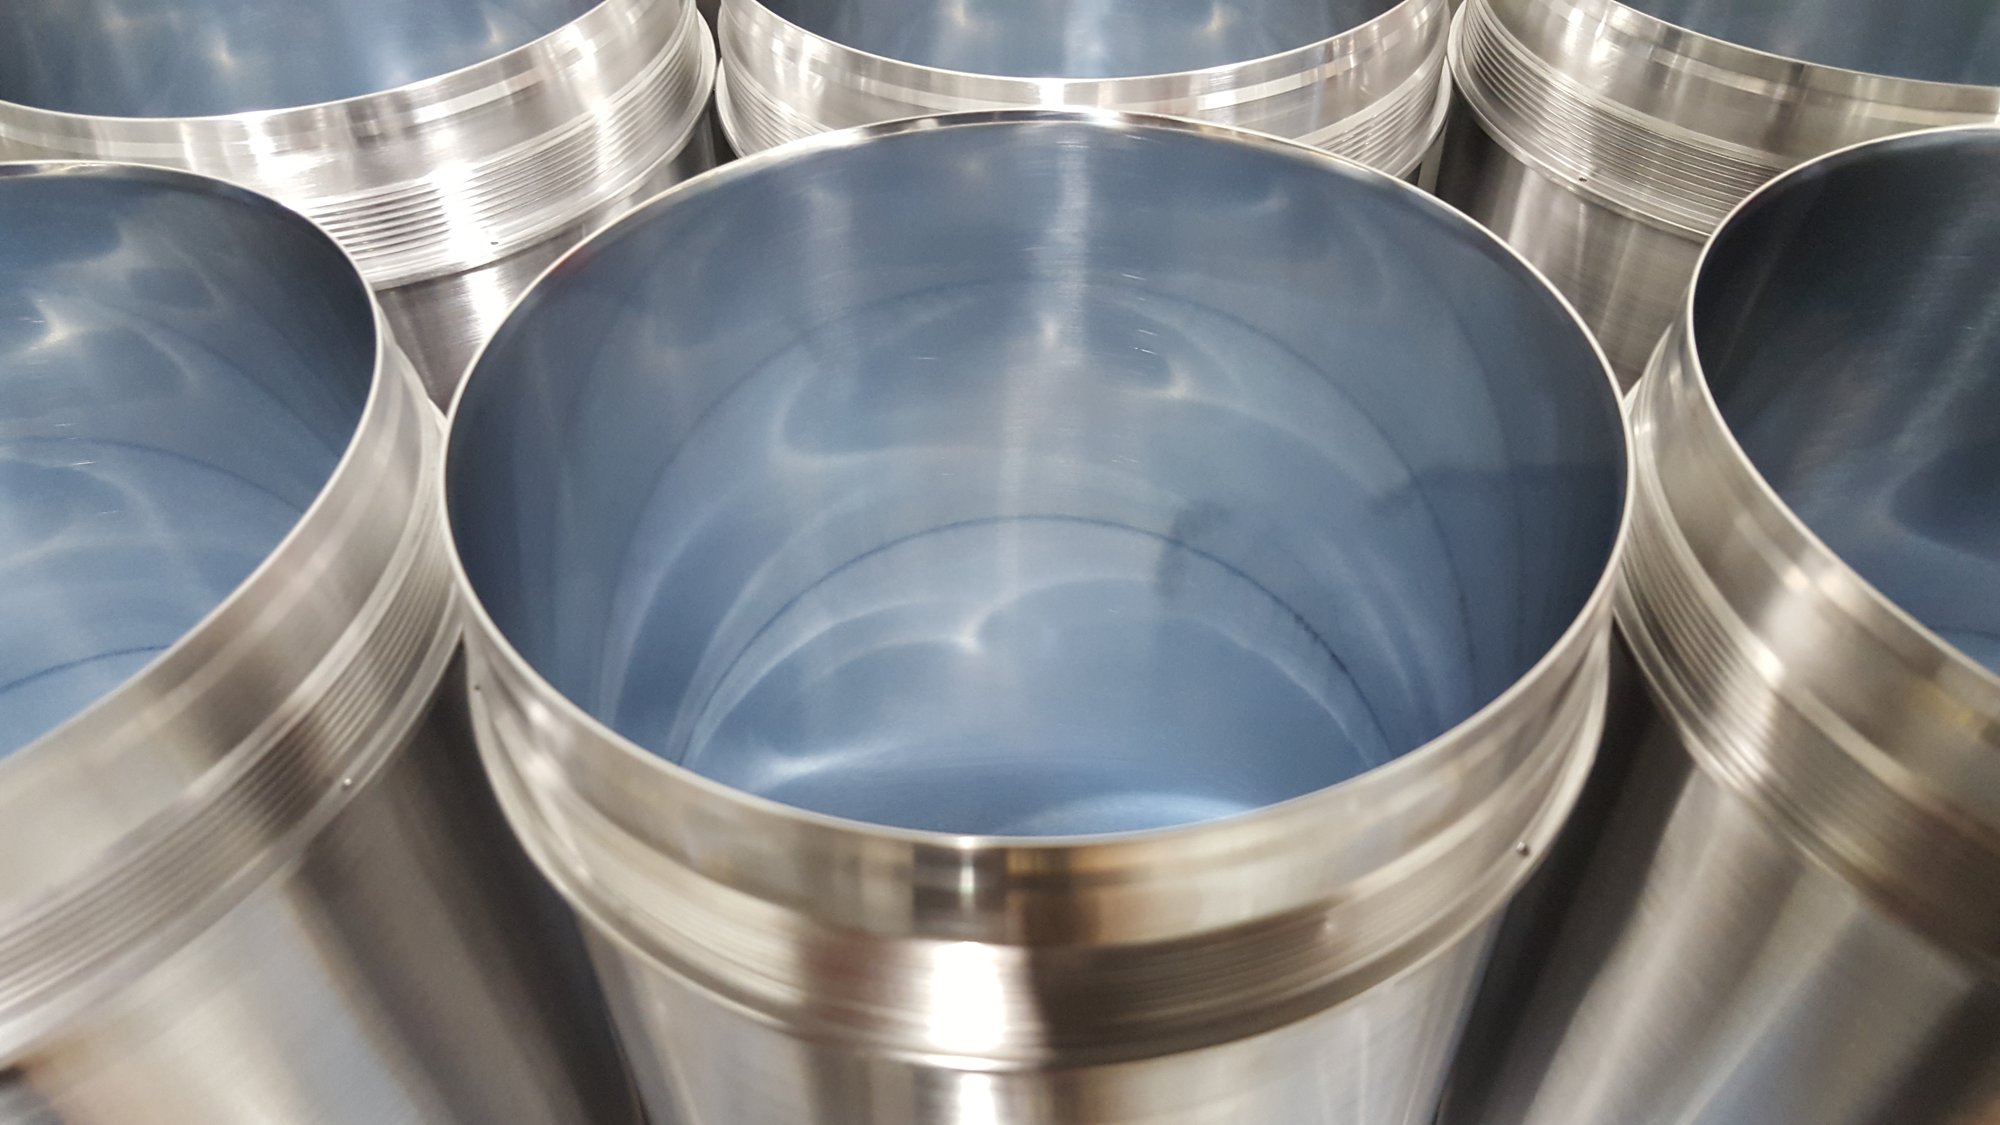
Batch of stainless steel cylinders with honed bores, the finish reflecting straight down the bore
Bore honing: Honed stainless bores, the finish reflecting down the bore
Extrusion die plate with a drilled port pattern for polymer flow
Blown film dies: Die plate with a drilled port pattern for polymer flow
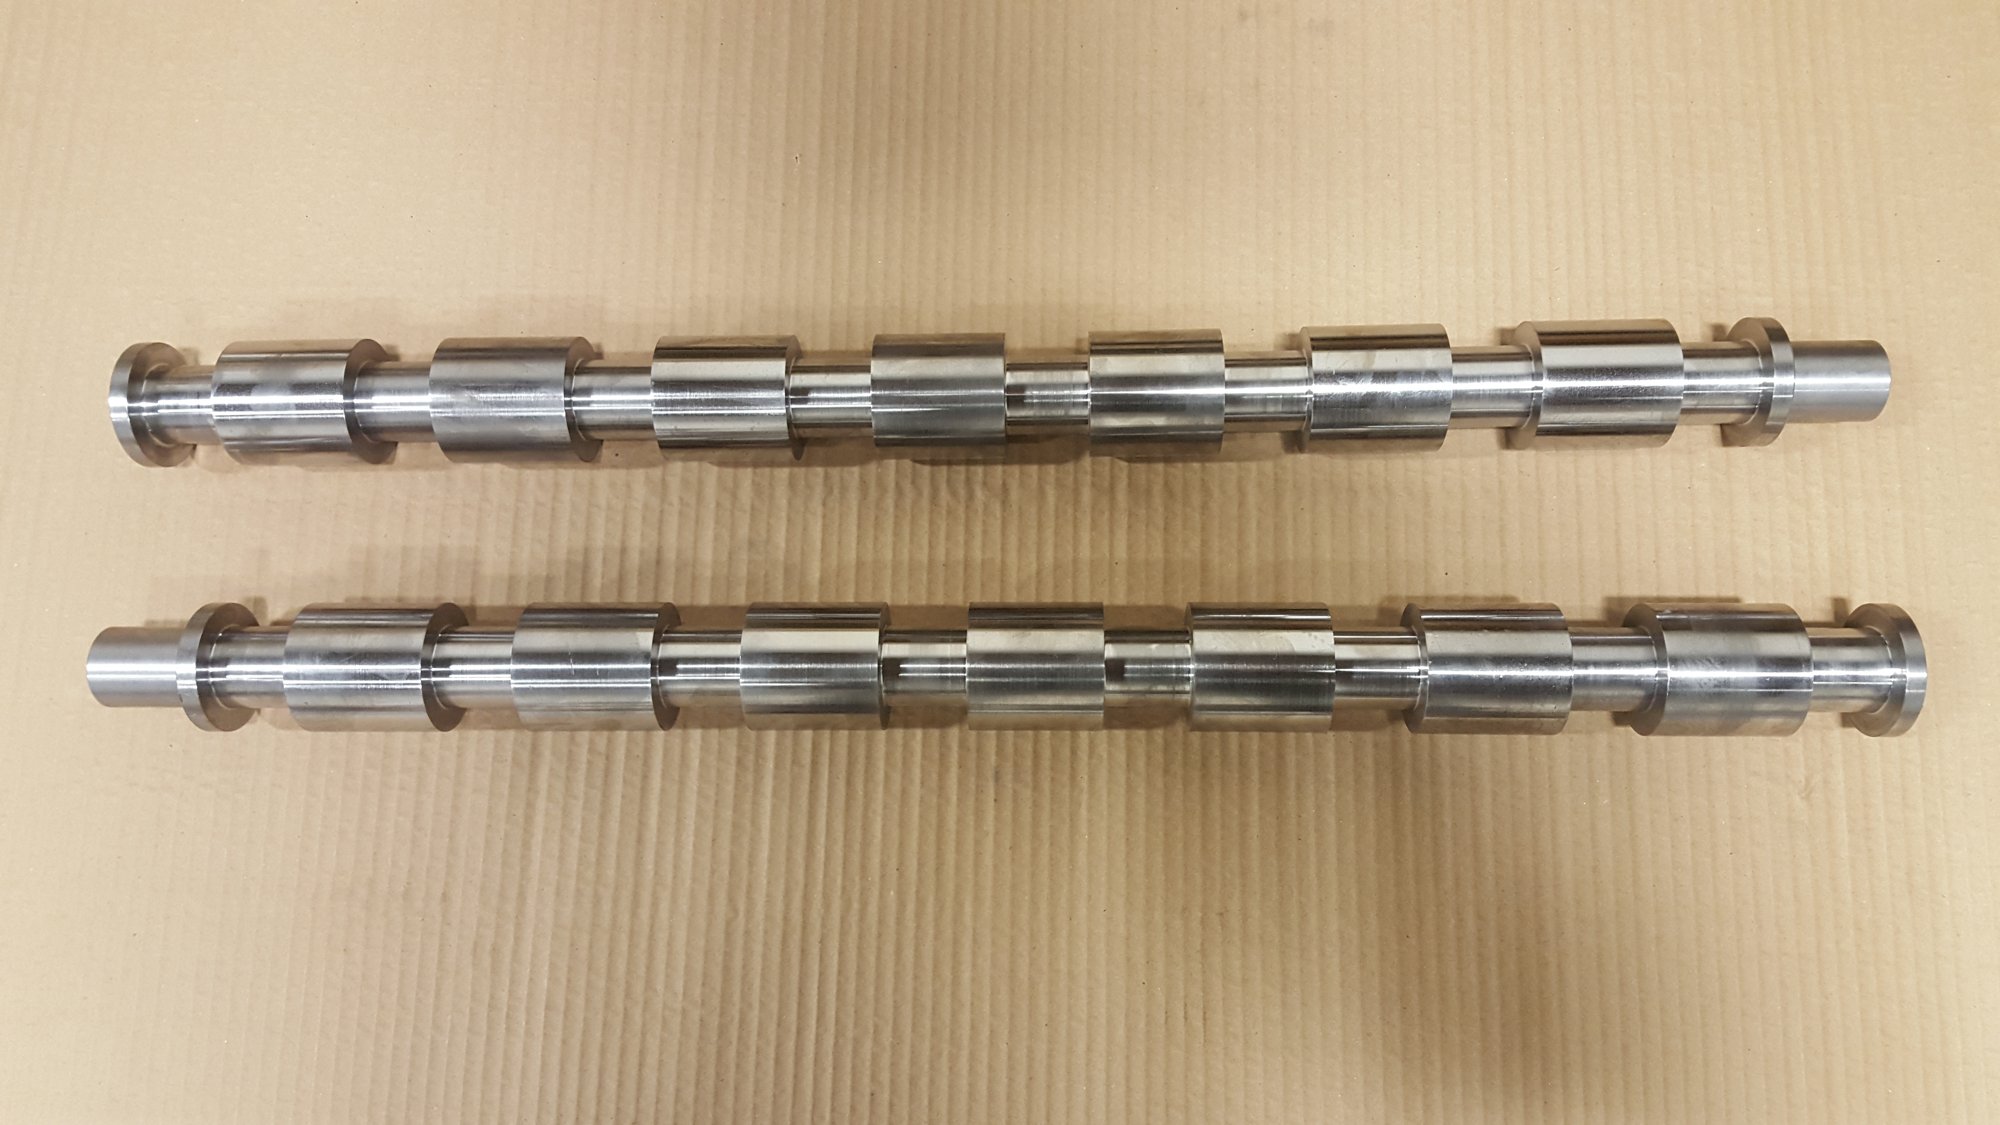
Pair of long shafts machined with splined collars and grooves along the full length
Shaft machining: A matched pair, splined collars along the full length
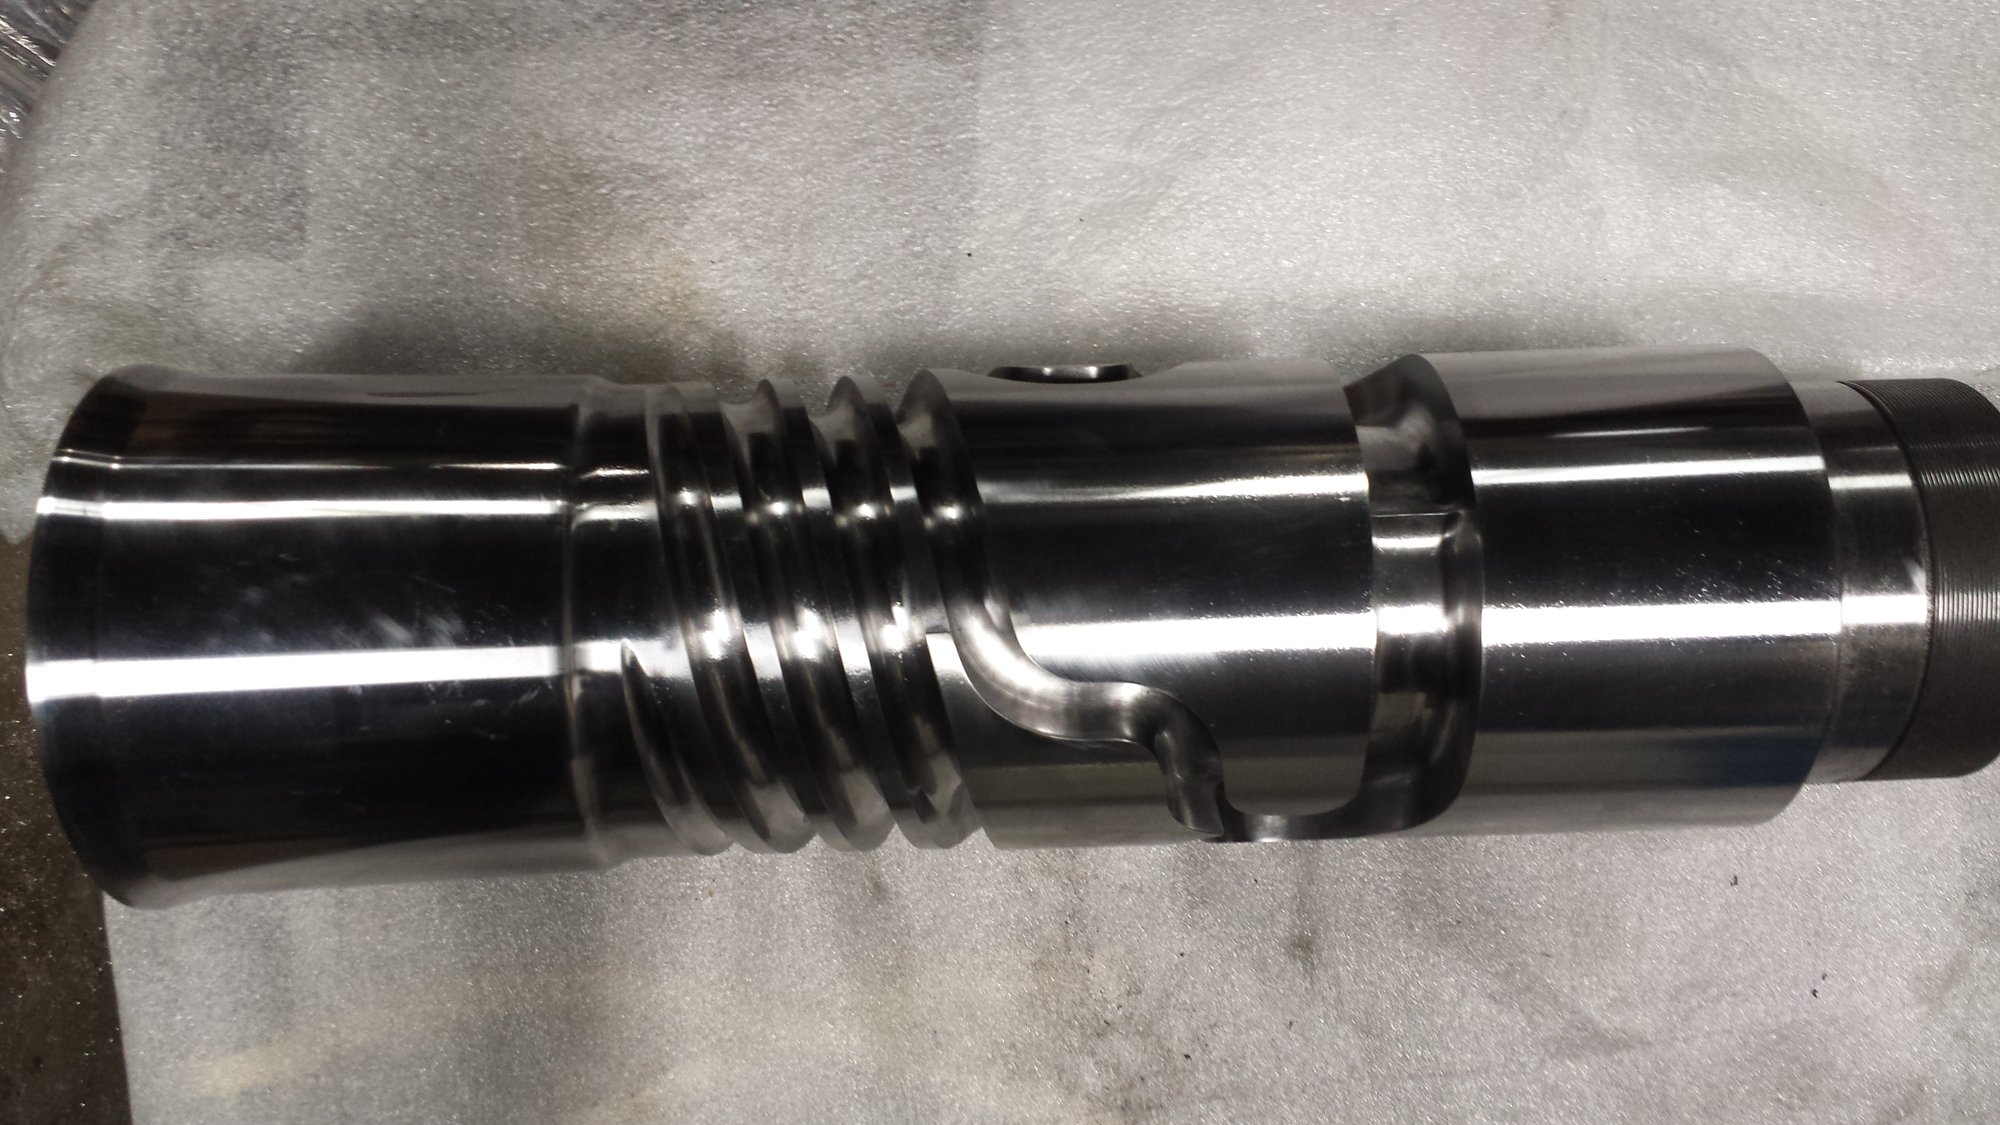
Mixing section of a 4.5in extruder feed screw, barrier flights running into a fluted mixing element
Extruder parts: Mixing section of a 4.5in feed screw
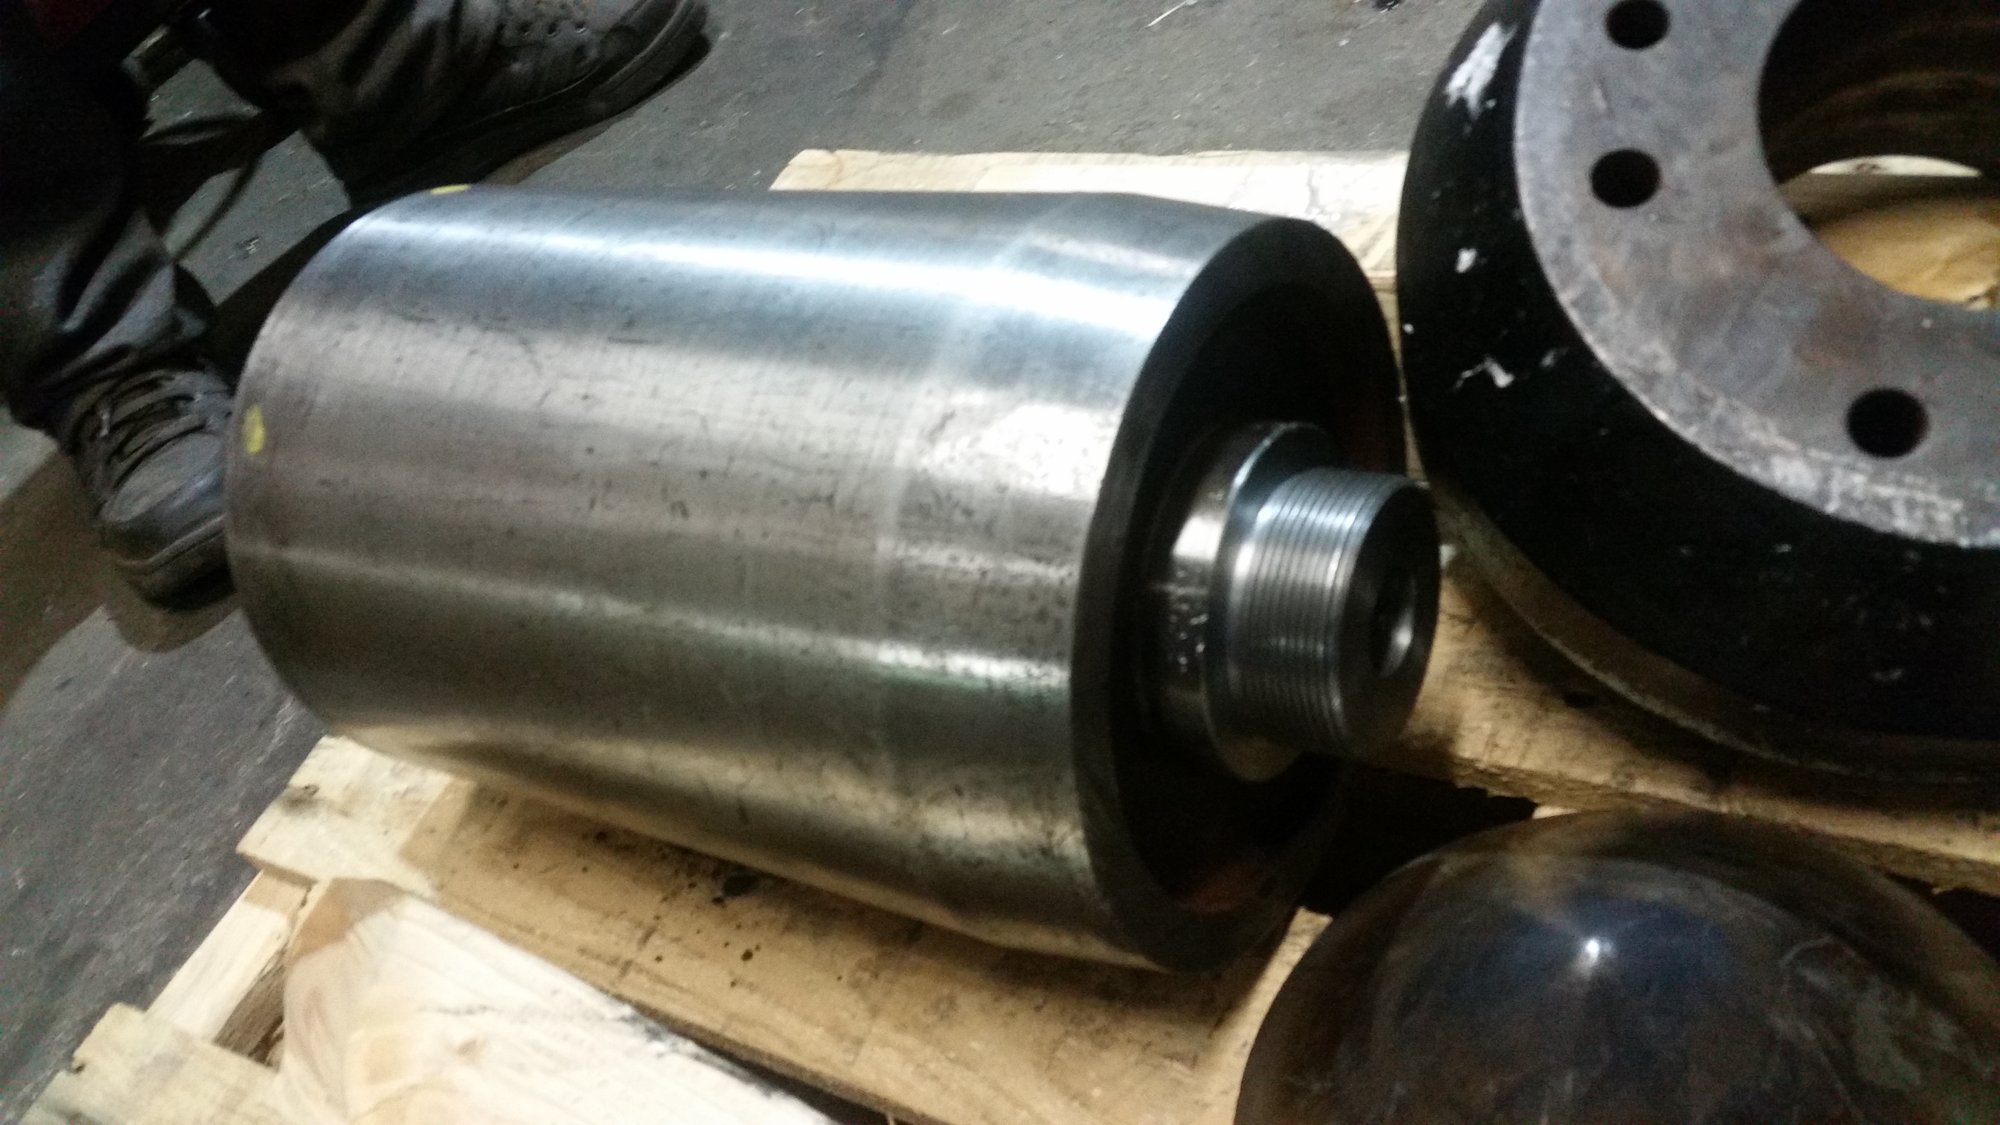
Black die body brought in for reverse engineering, outer bolt circle with a stepped inner flange and a threaded centre bore, measured before new parts were machined
Large machining: Flanged housing, two bolt circles and a splined bore
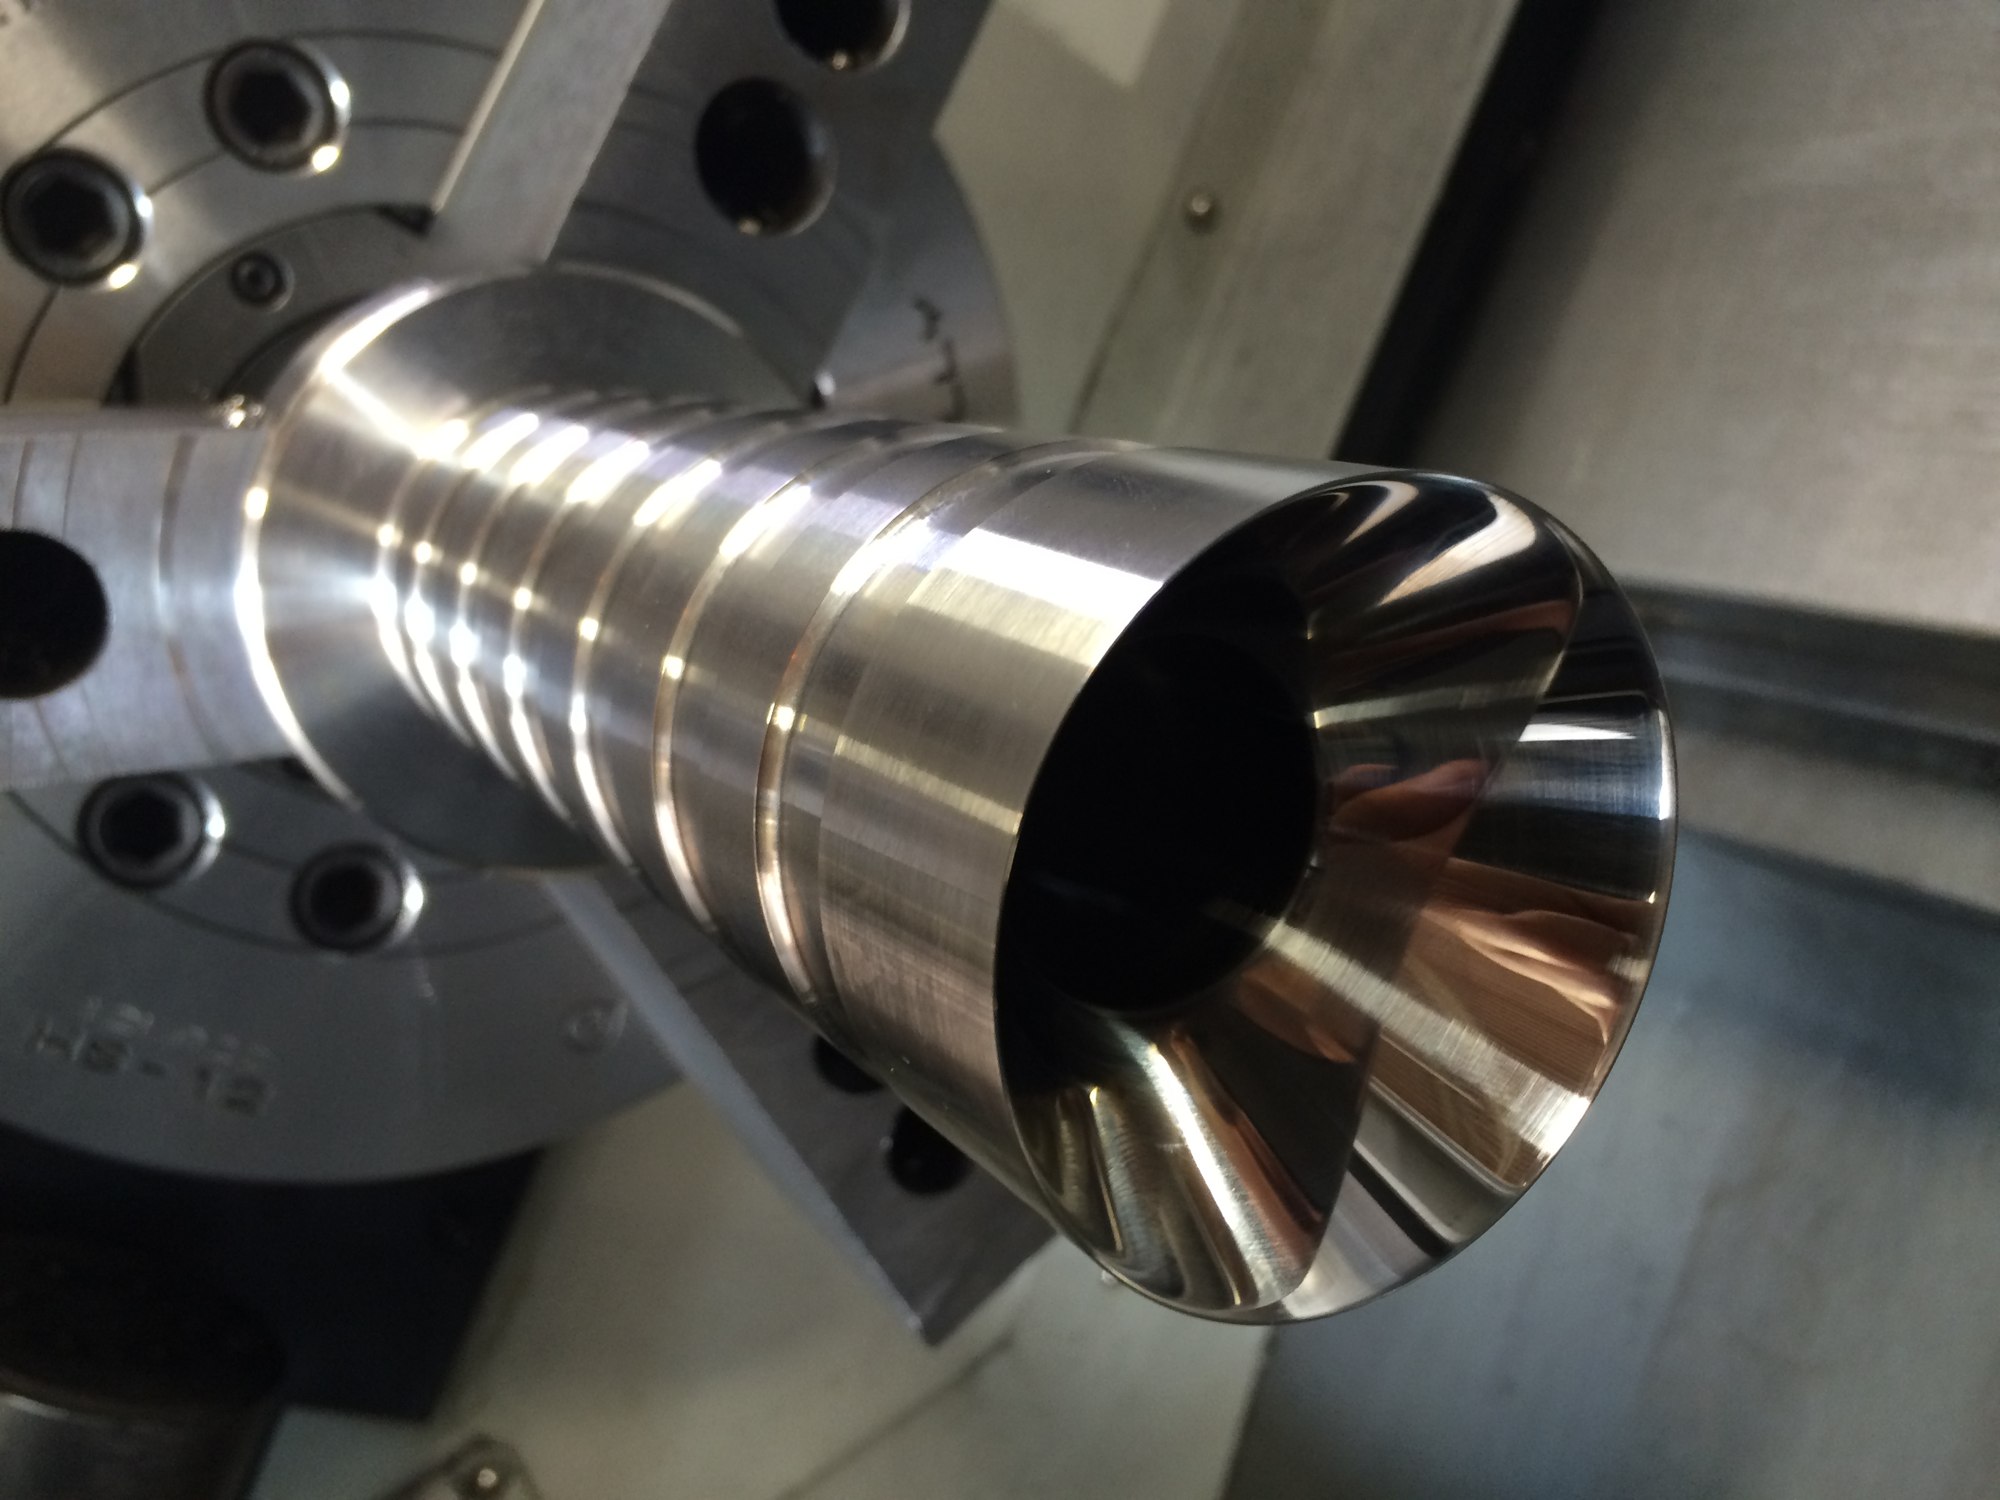
Stainless part in the CNC lathe chuck, tapered bore polished to a mirror finish
Turning and production: Tapered bore polished to a mirror finish
Die body with finished internal bore and mounting flange
Blown film dies: Die body with finished internal bore and mounting flange
First side of the die block finished on the lathe, concentric flow steps turned in to the centre bore
One die, start to finish (4 of 10): First side turned, concentric flow steps in to the bore
Rebuilt extruder gearbox assembled and painted on a pallet at Zala Machine Co.
Gearbox repair: Rebuilt and painted, back on the pallet
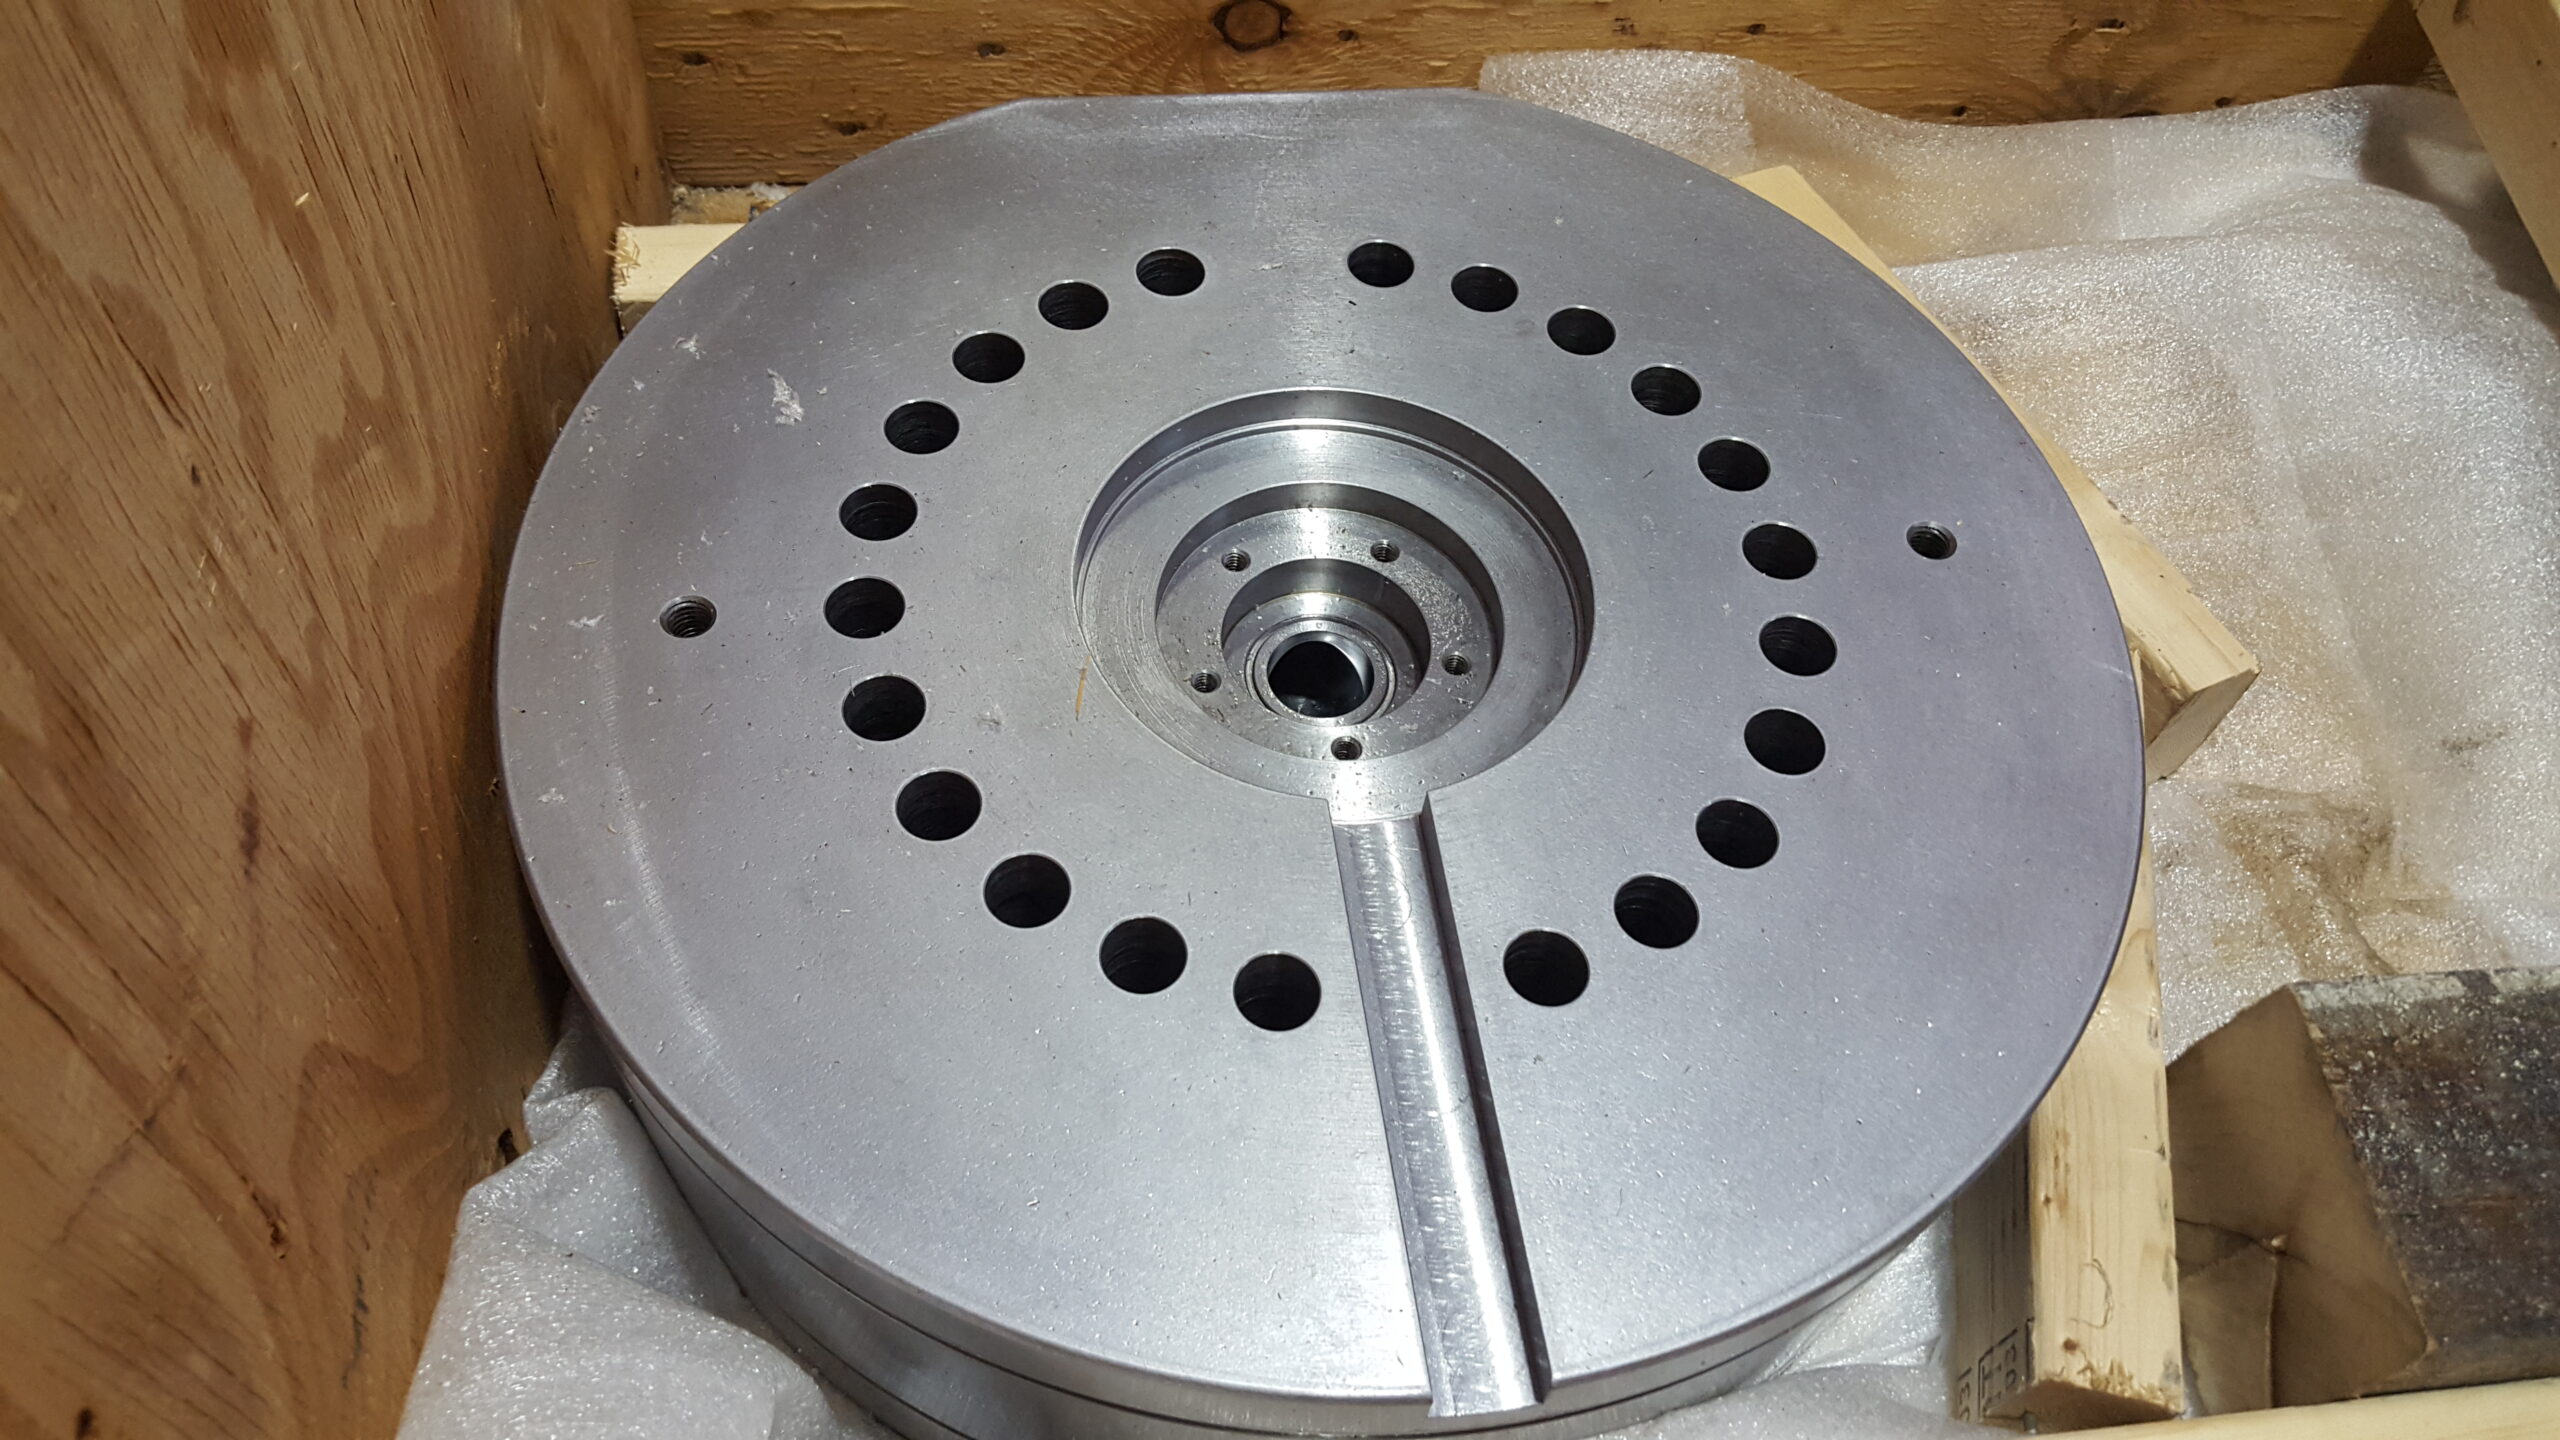
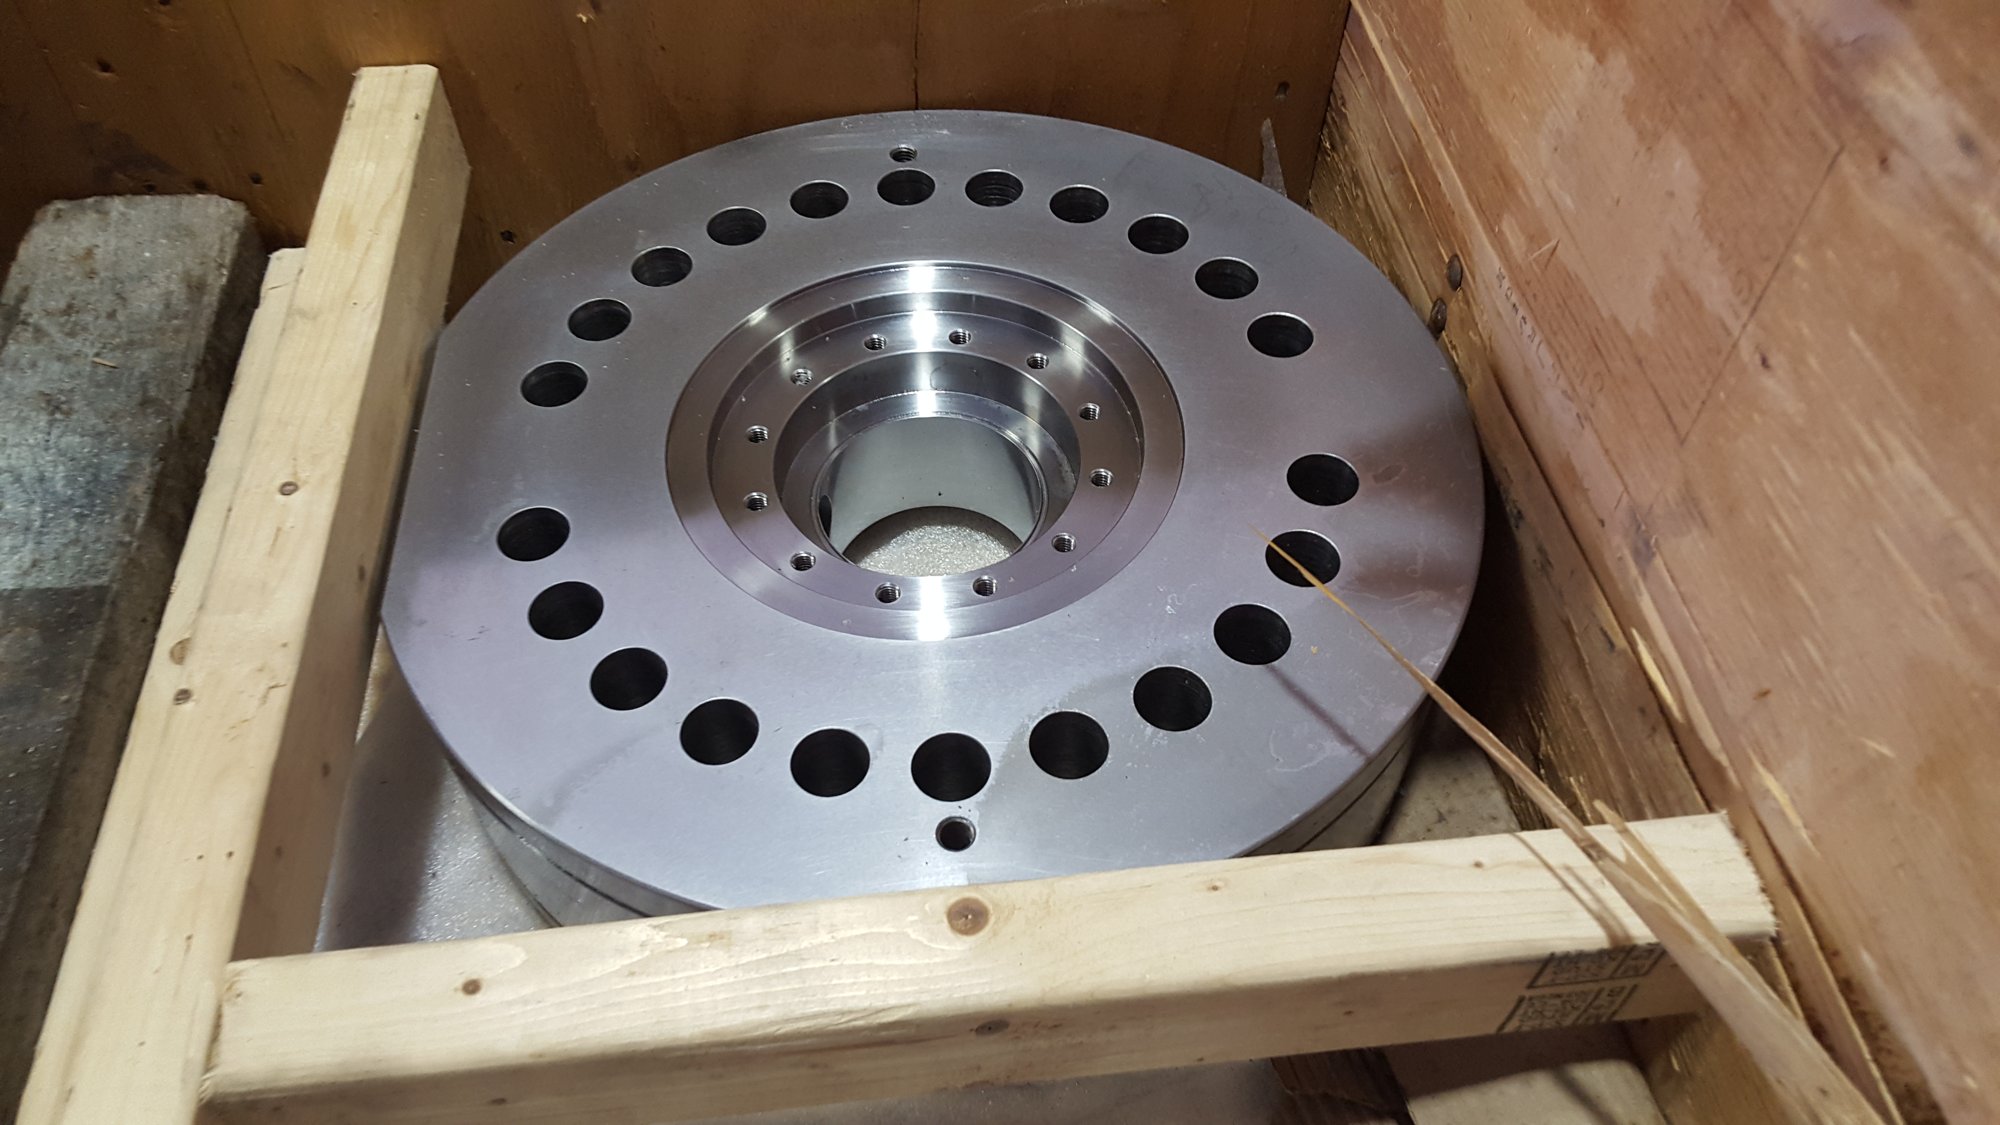
Finished machined disc braced in its crate, bolt circles drilled and the centre hub bored
Fabrication and shipping: Machined disc braced in its crate
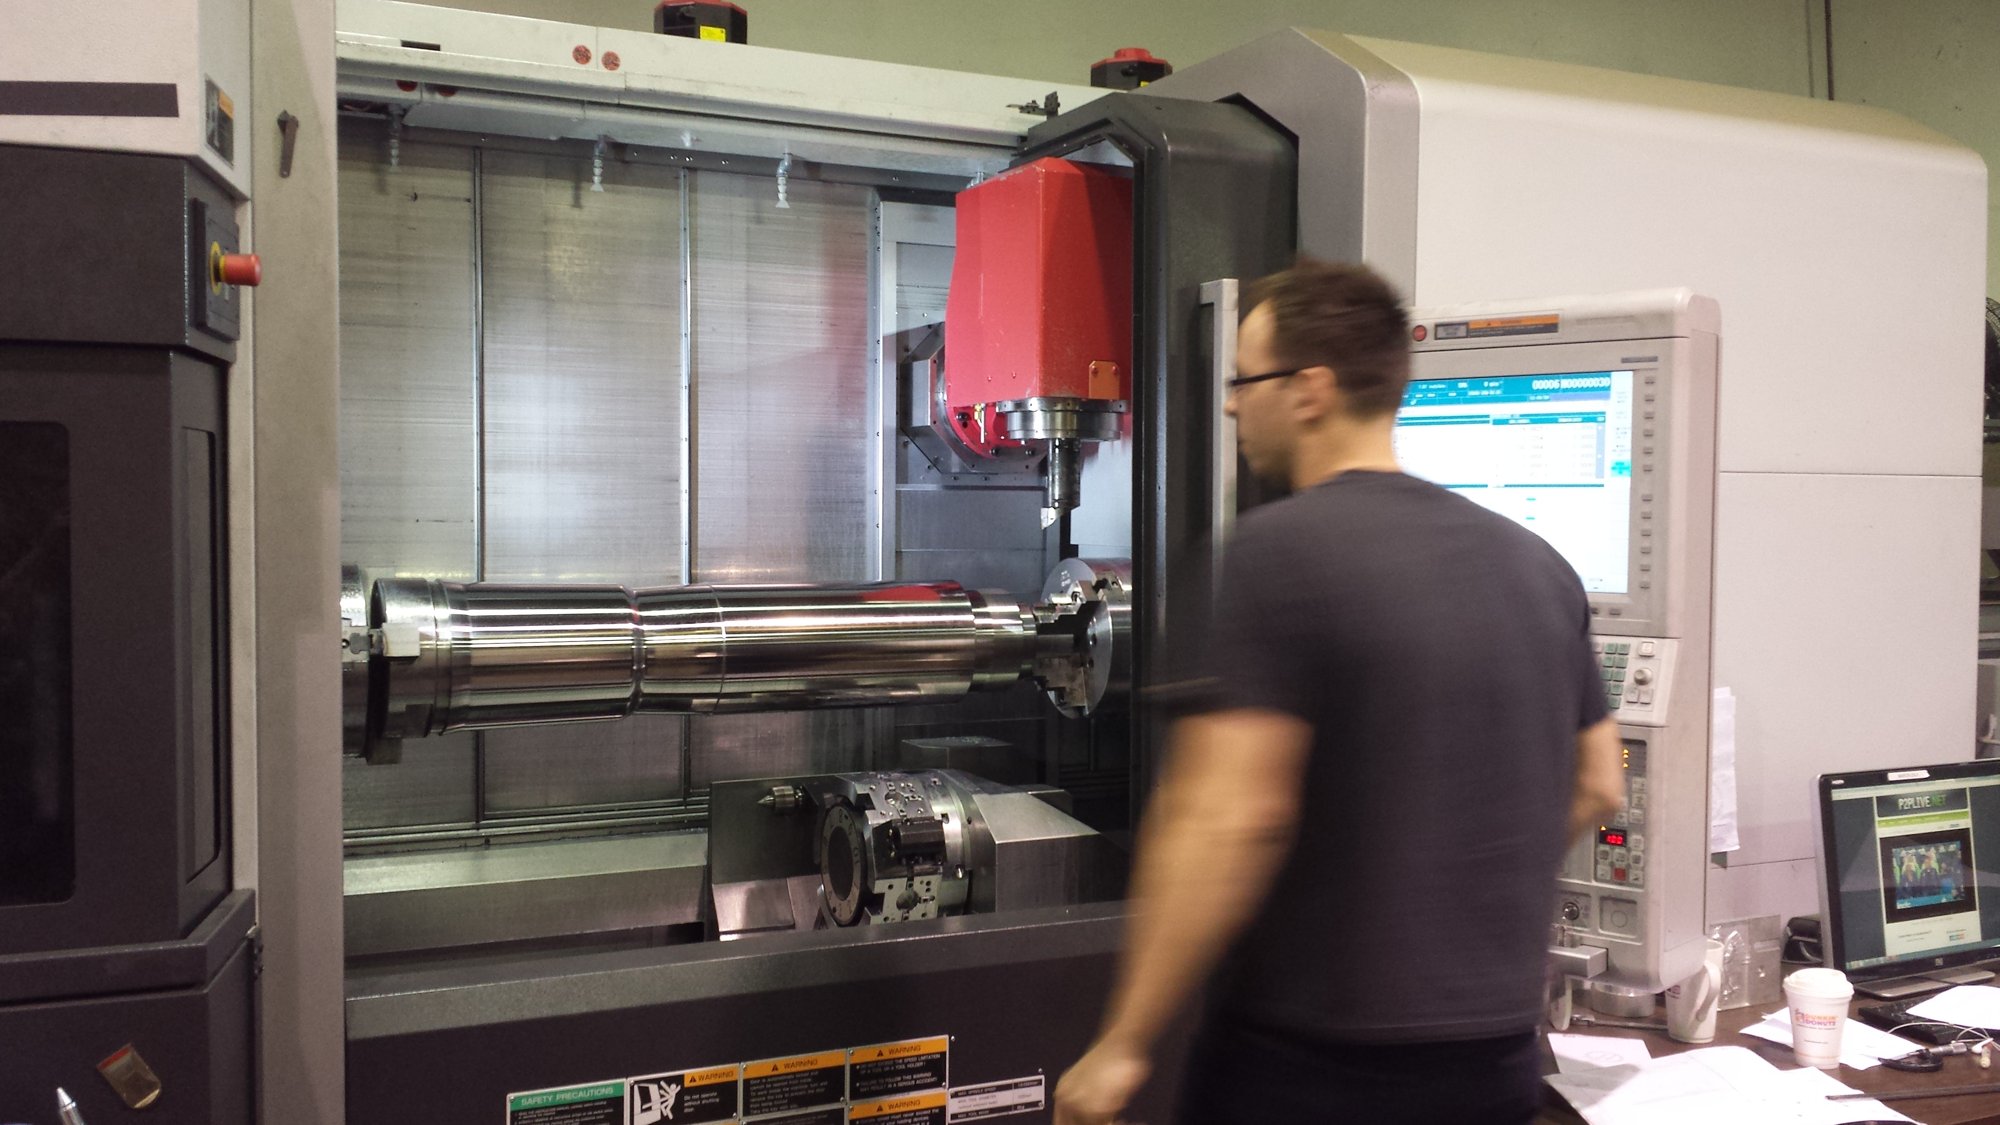
Machinist at the mill-turn control with an extruder screw running in the machine behind him
The shop: At the mill-turn control, a screw running behind
Flanged die body resting on a pallet after machining
Blown film dies: Flanged die body on a pallet after machining
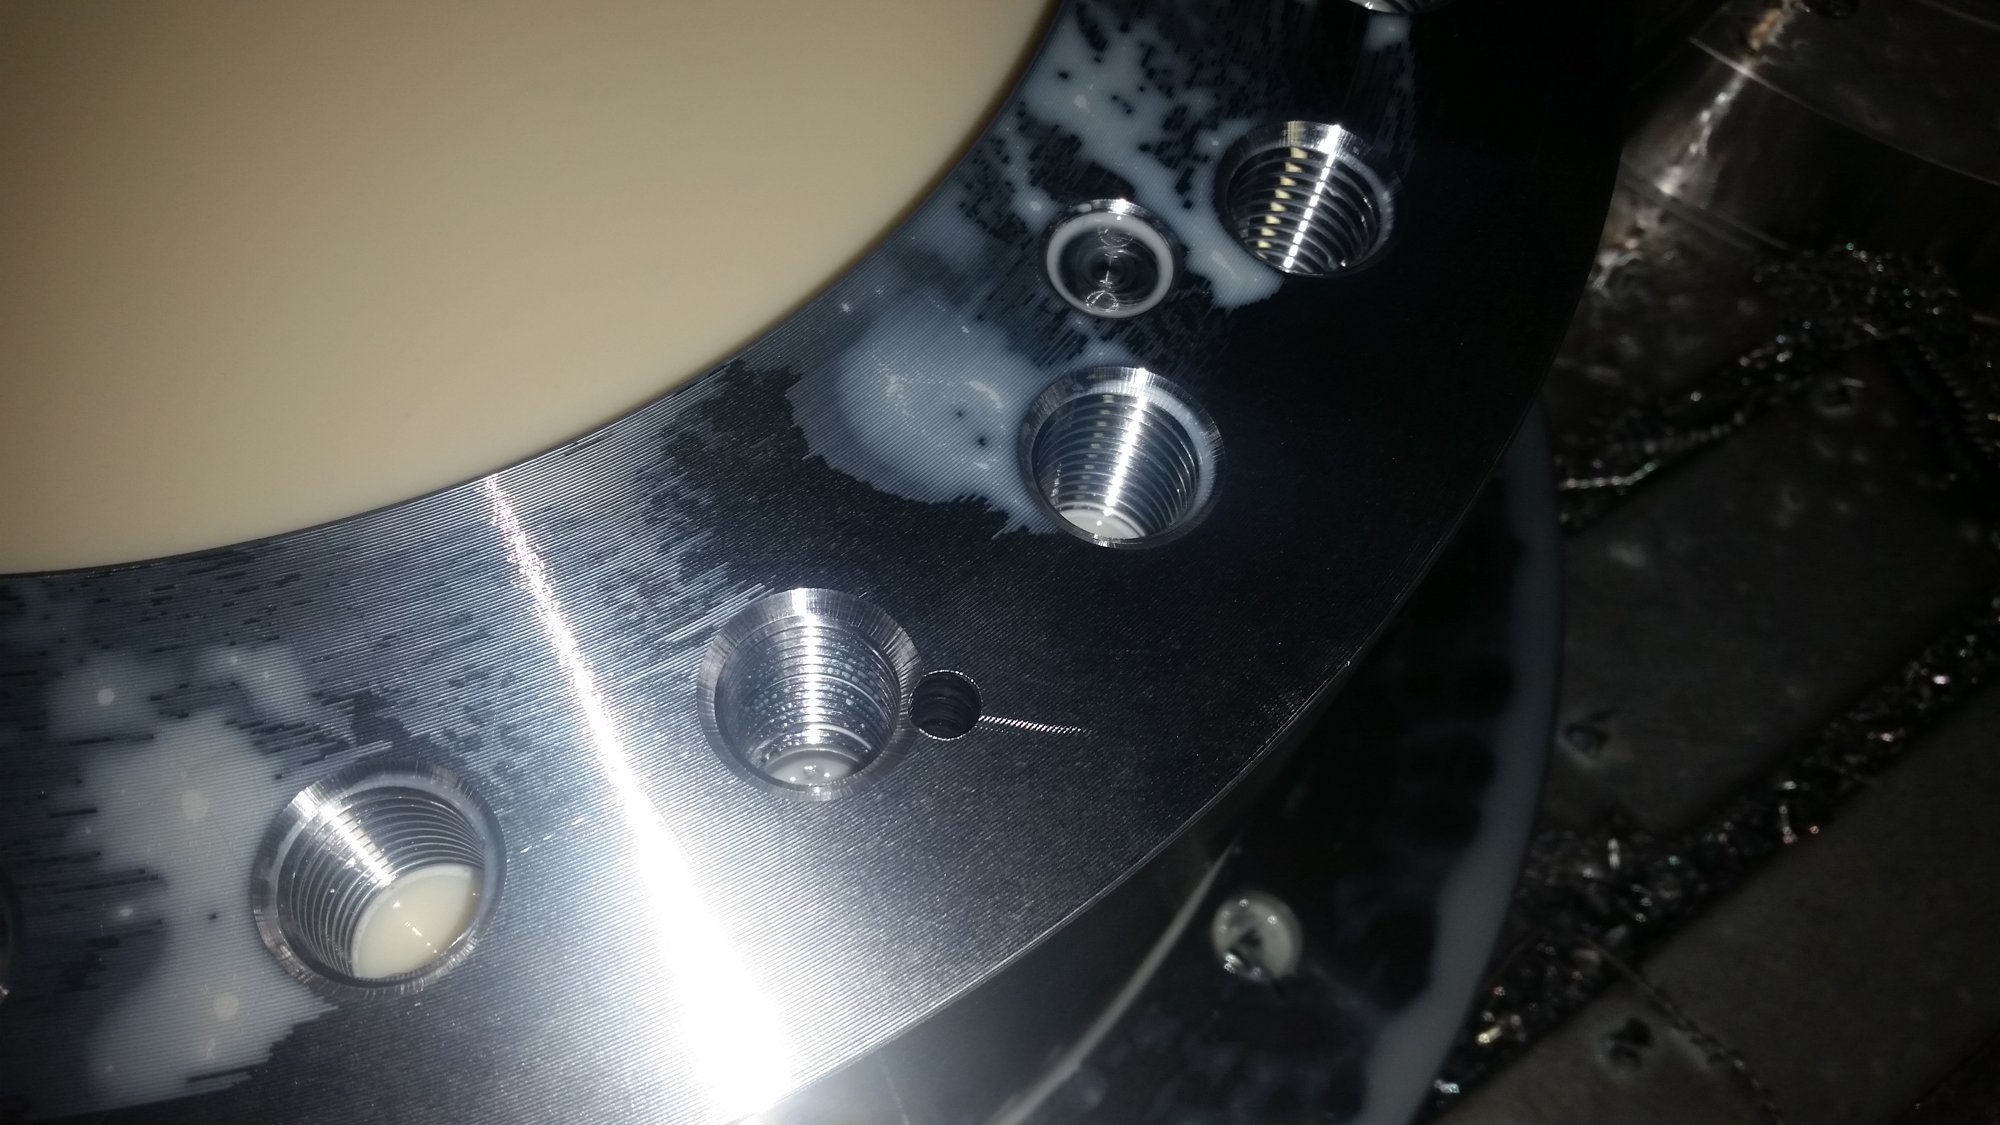
Tapped holes and counterbores machined into a large flange face, coolant still on the part
Large machining: Tapped holes and counterbores in a large flange face
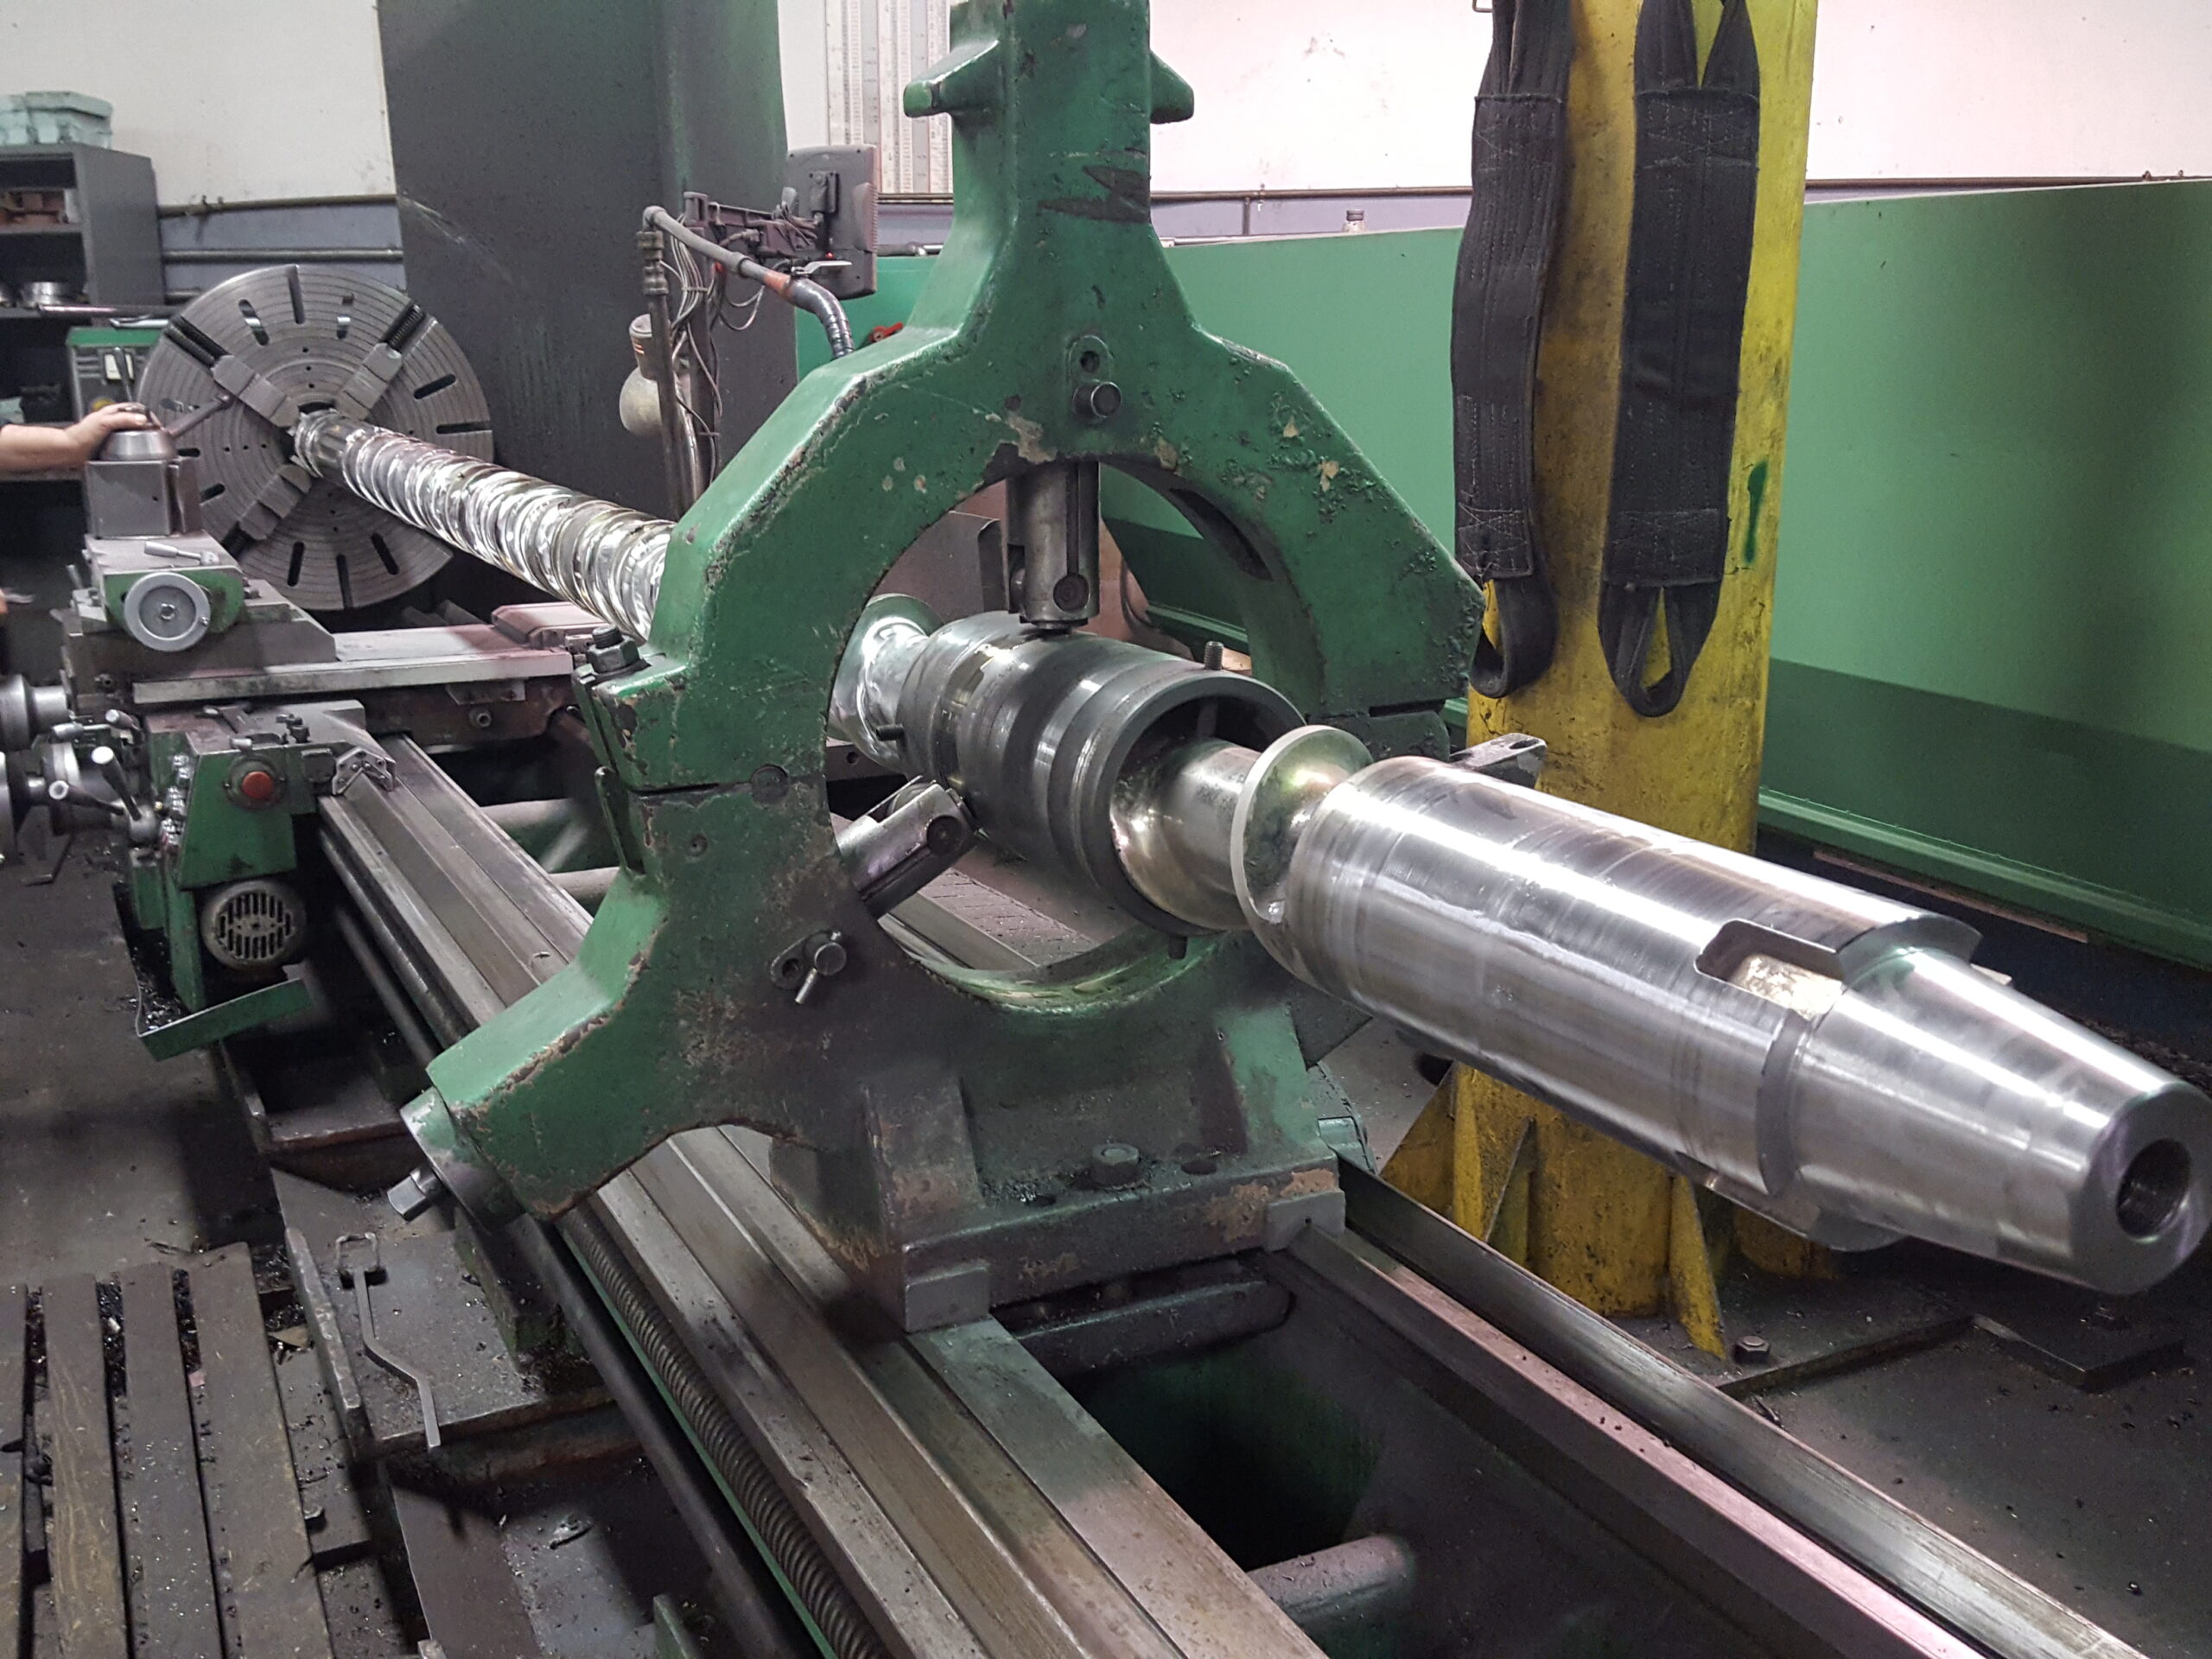
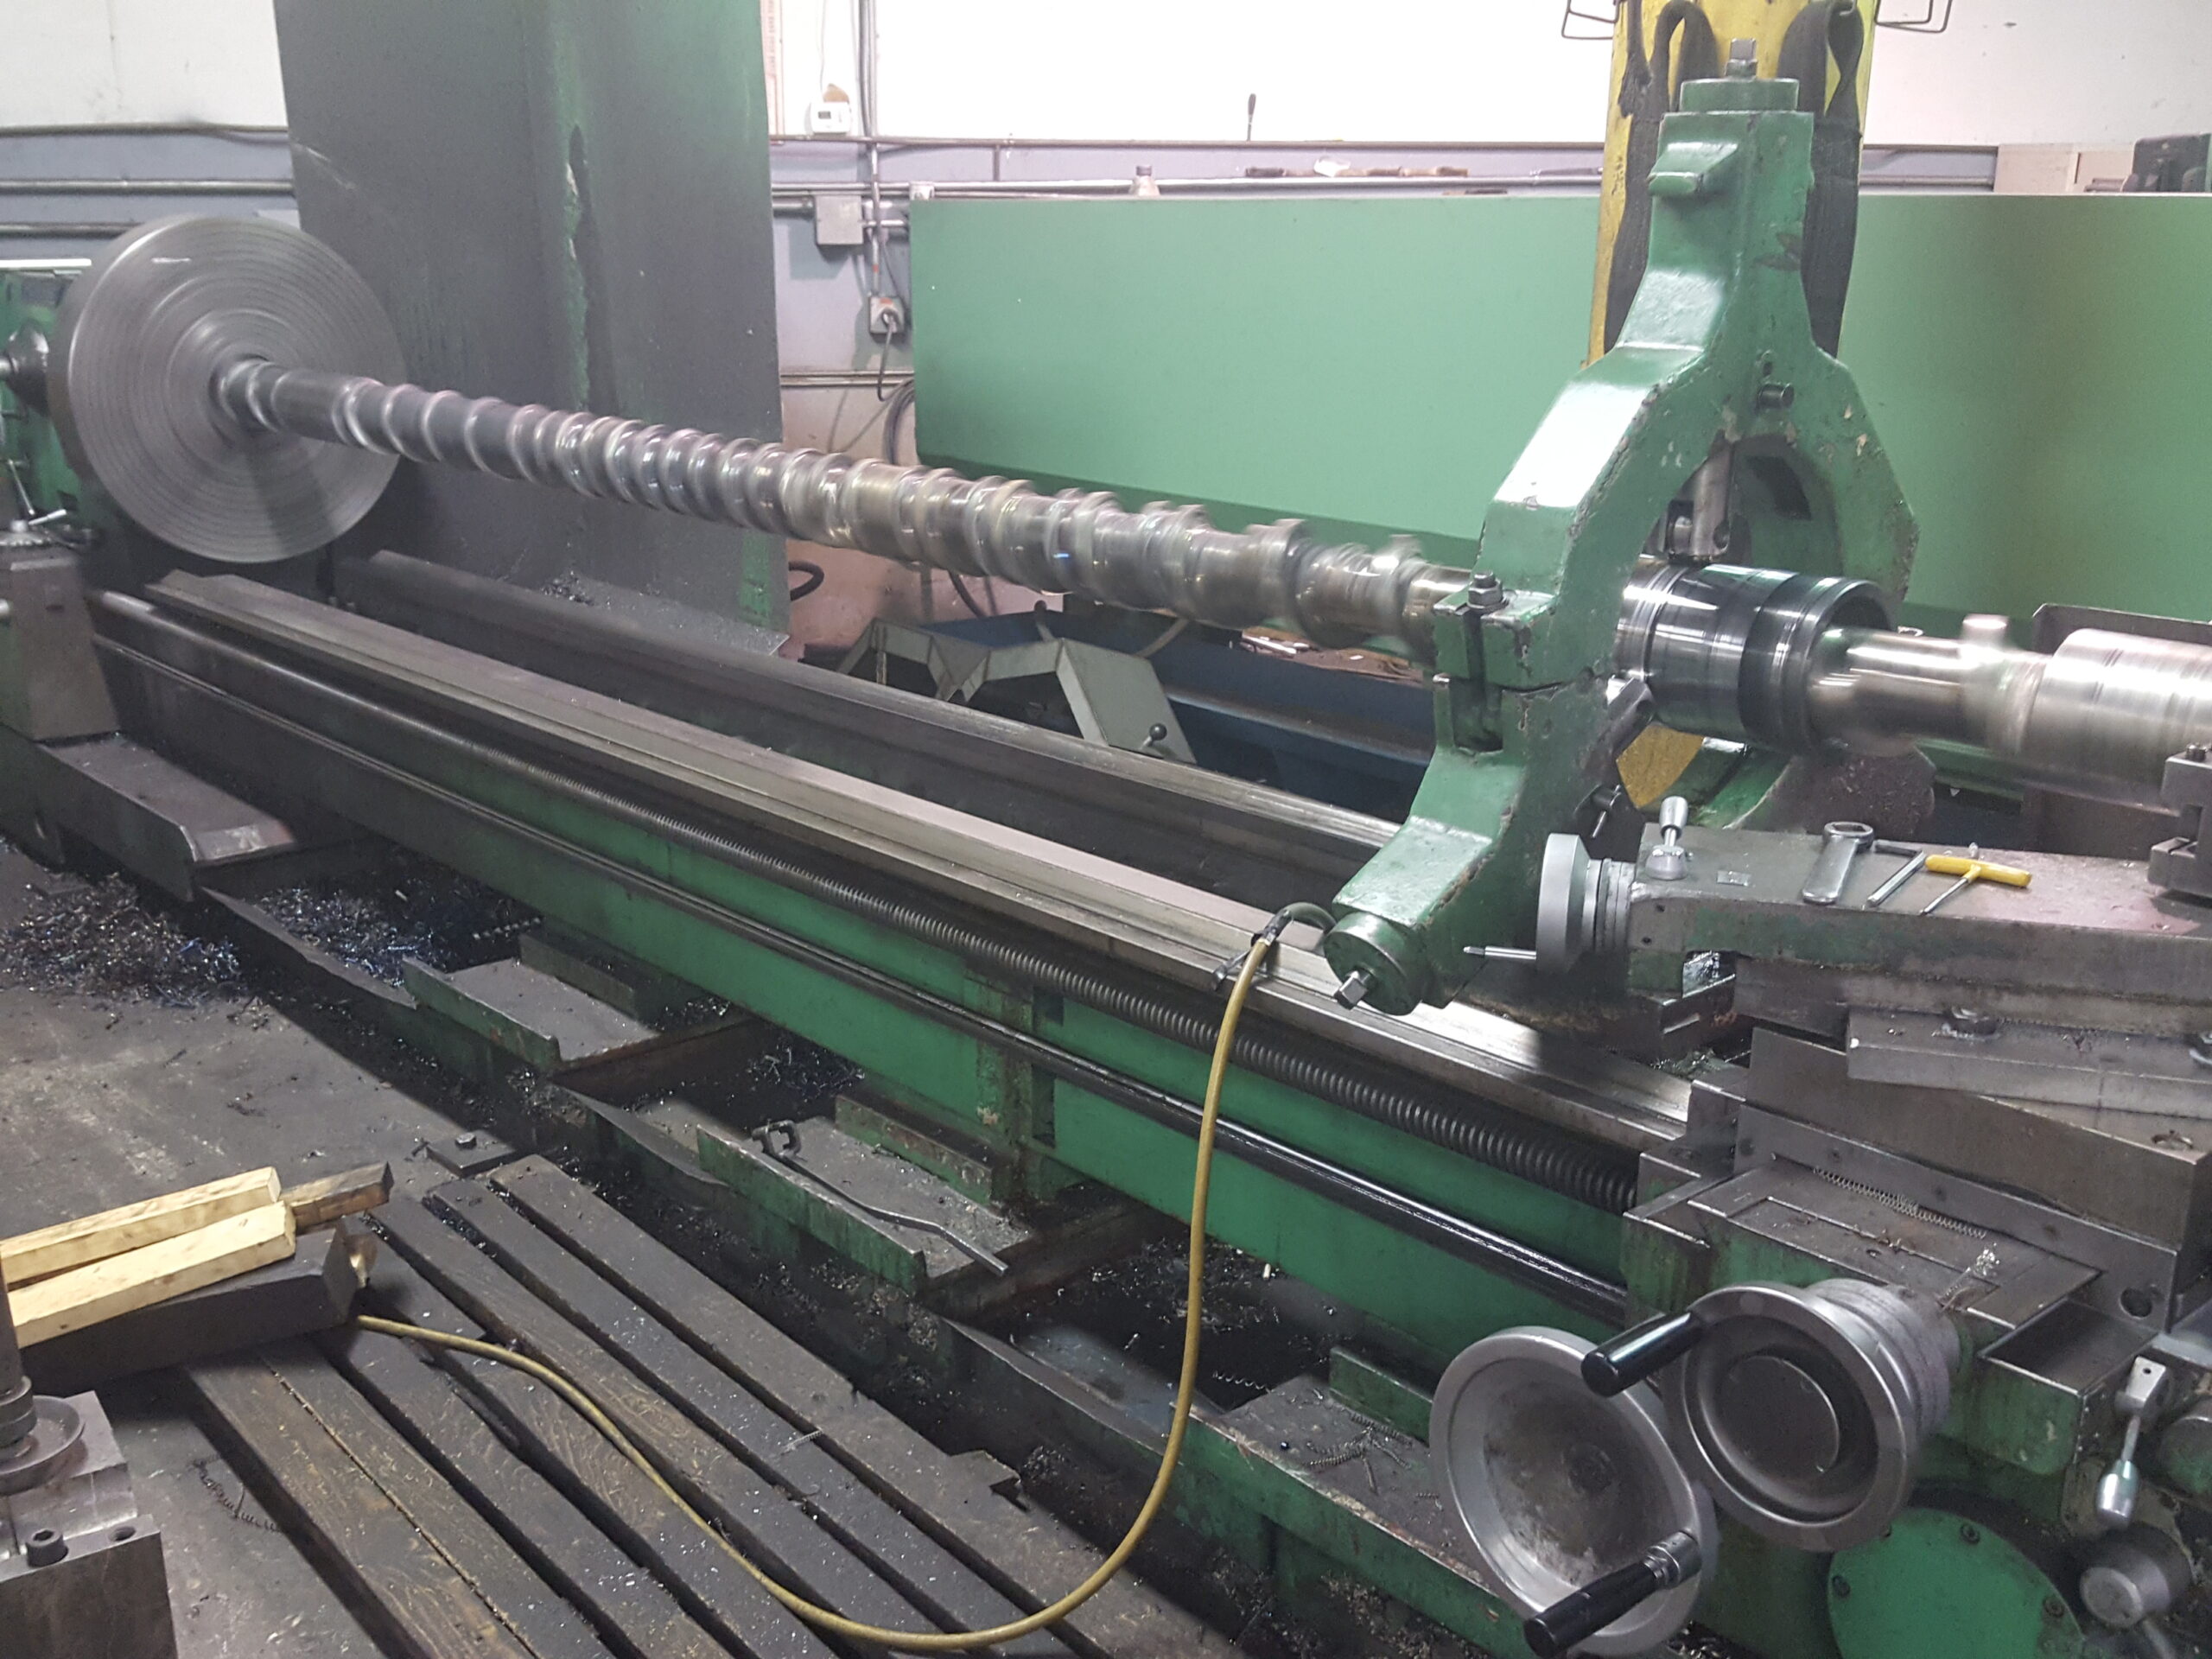
Extruder Screw Modification on the Poreba Engine Lathe
Extruder parts: Screw modification on the Poreba engine lathe
Bronze-faced disc turned in the lathe chuck, fresh cut showing bright against the bore
Turning and production: Bronze-faced disc turned in the chuck
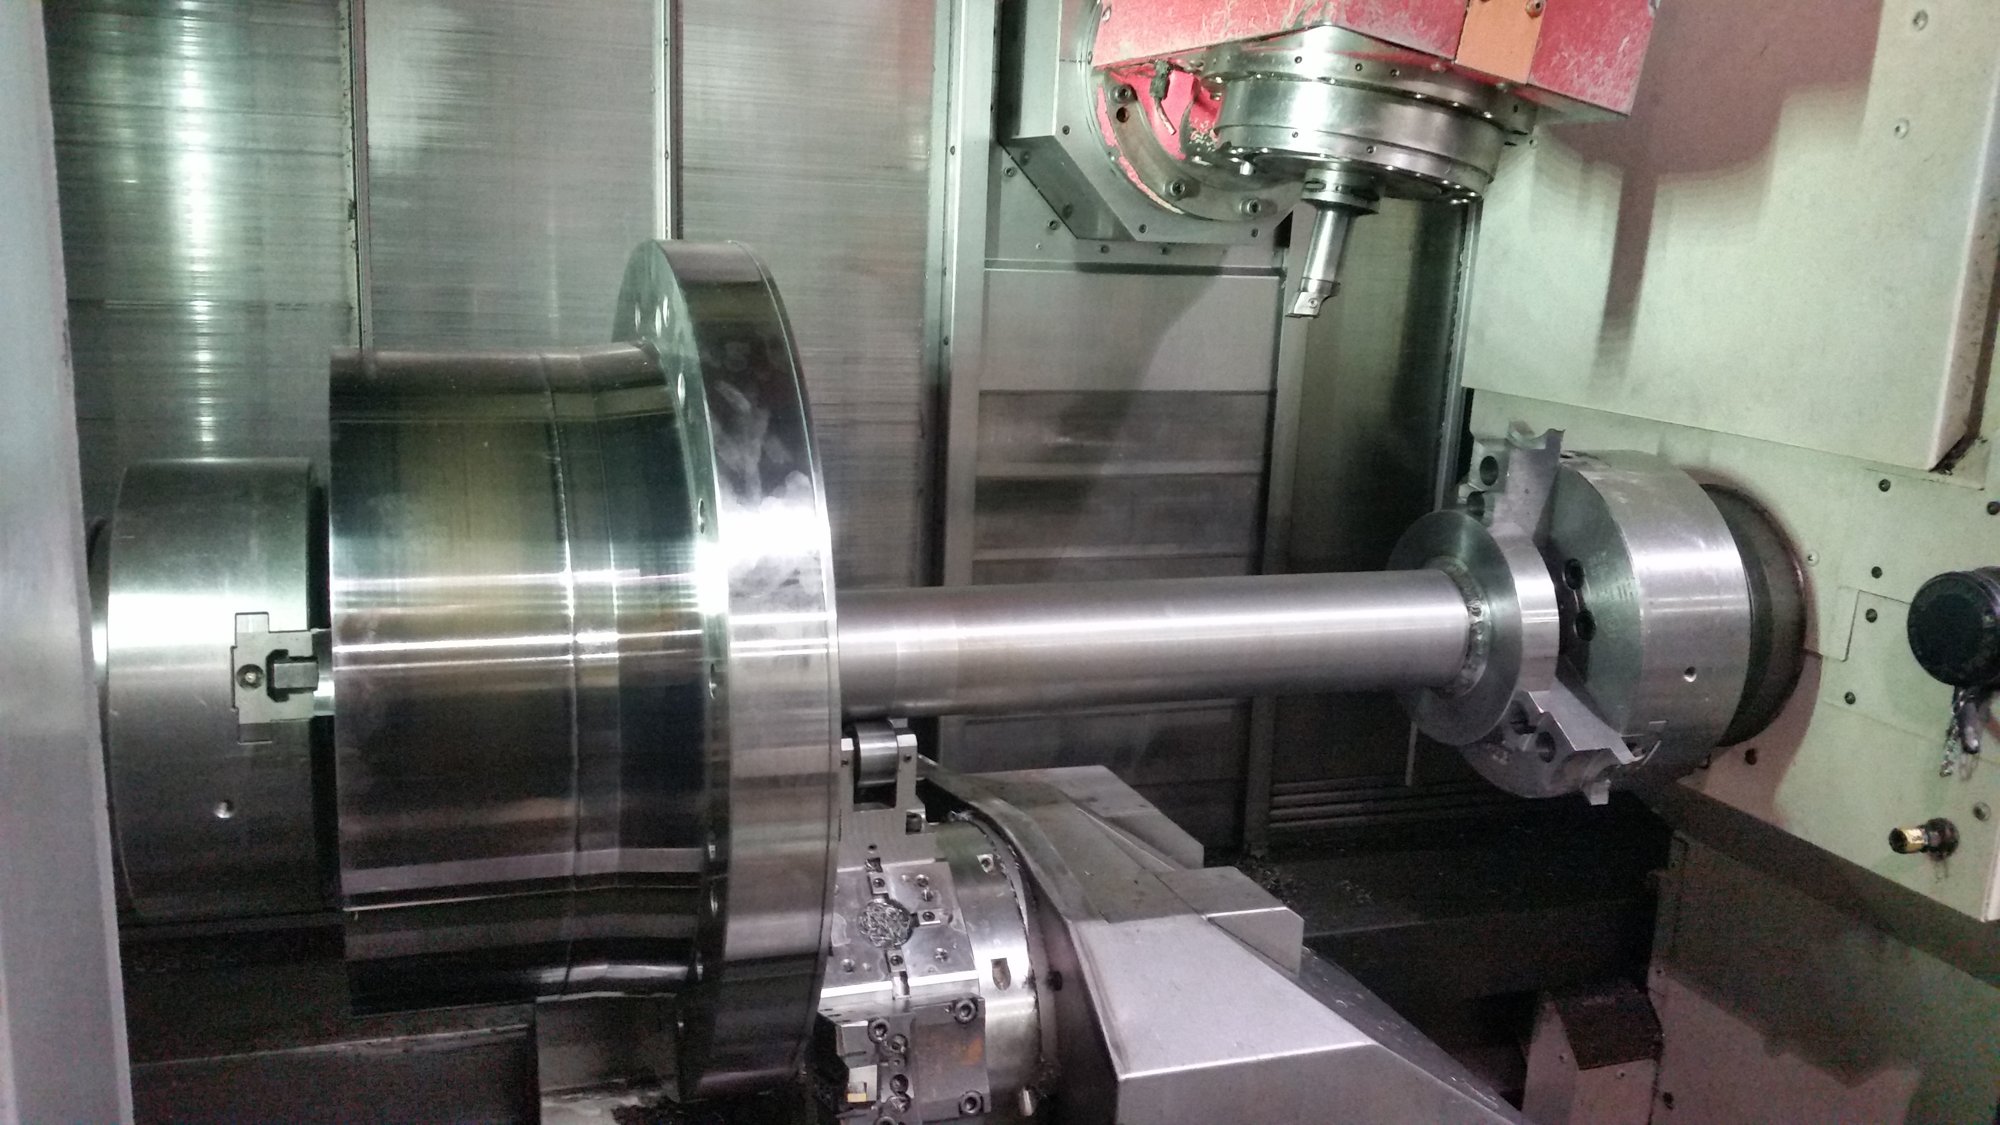
Shaft with a large integral flange machined between centres in the mill-turn
Shaft machining: Shaft with an integral flange, machined between centres
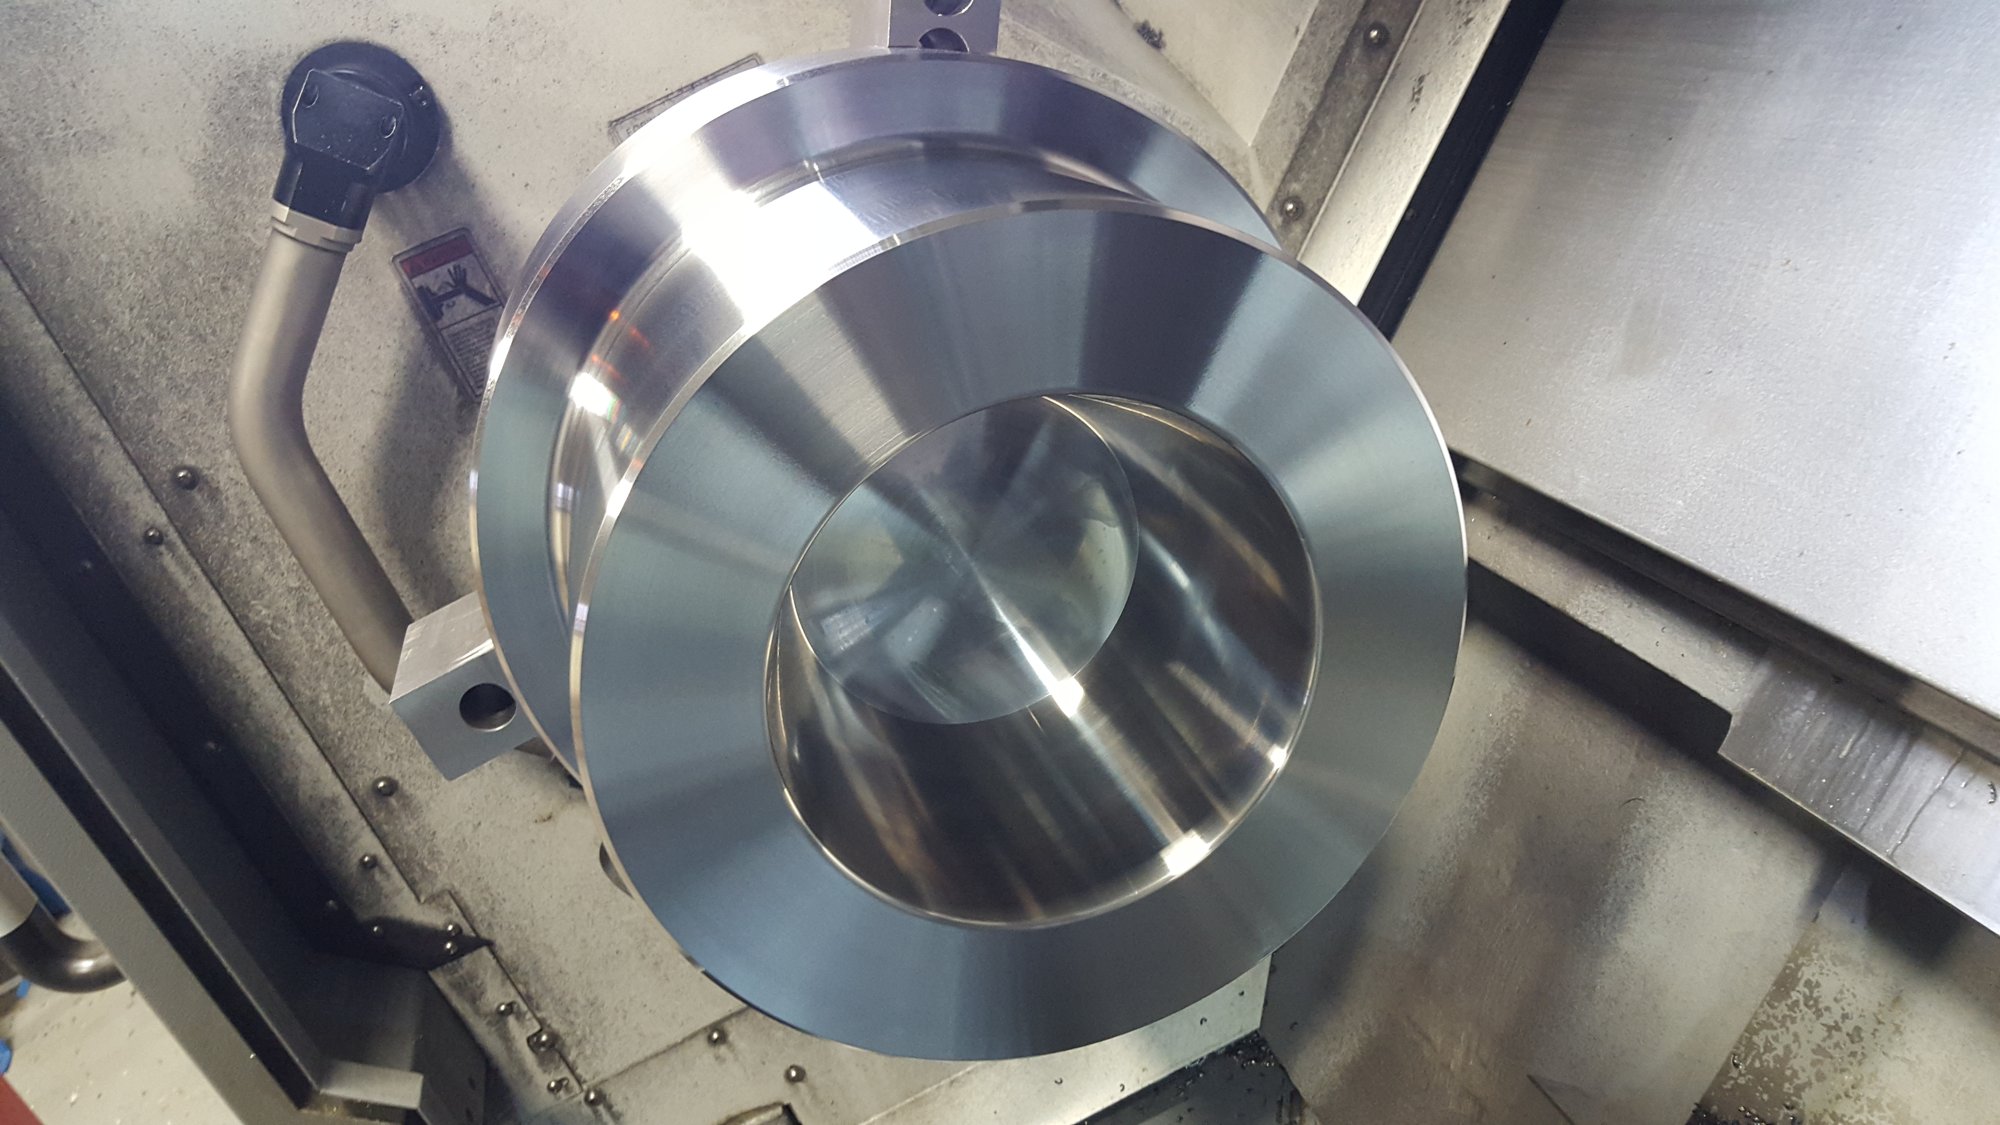
Machined flange ring with bored centre for an extrusion die assembly
Blown film dies: Machined flange ring with bored centre
Second side of the die block finished on the lathe, tapered inner bore turned to size
One die, start to finish (5 of 10): Second side, tapered inner bore cut to size
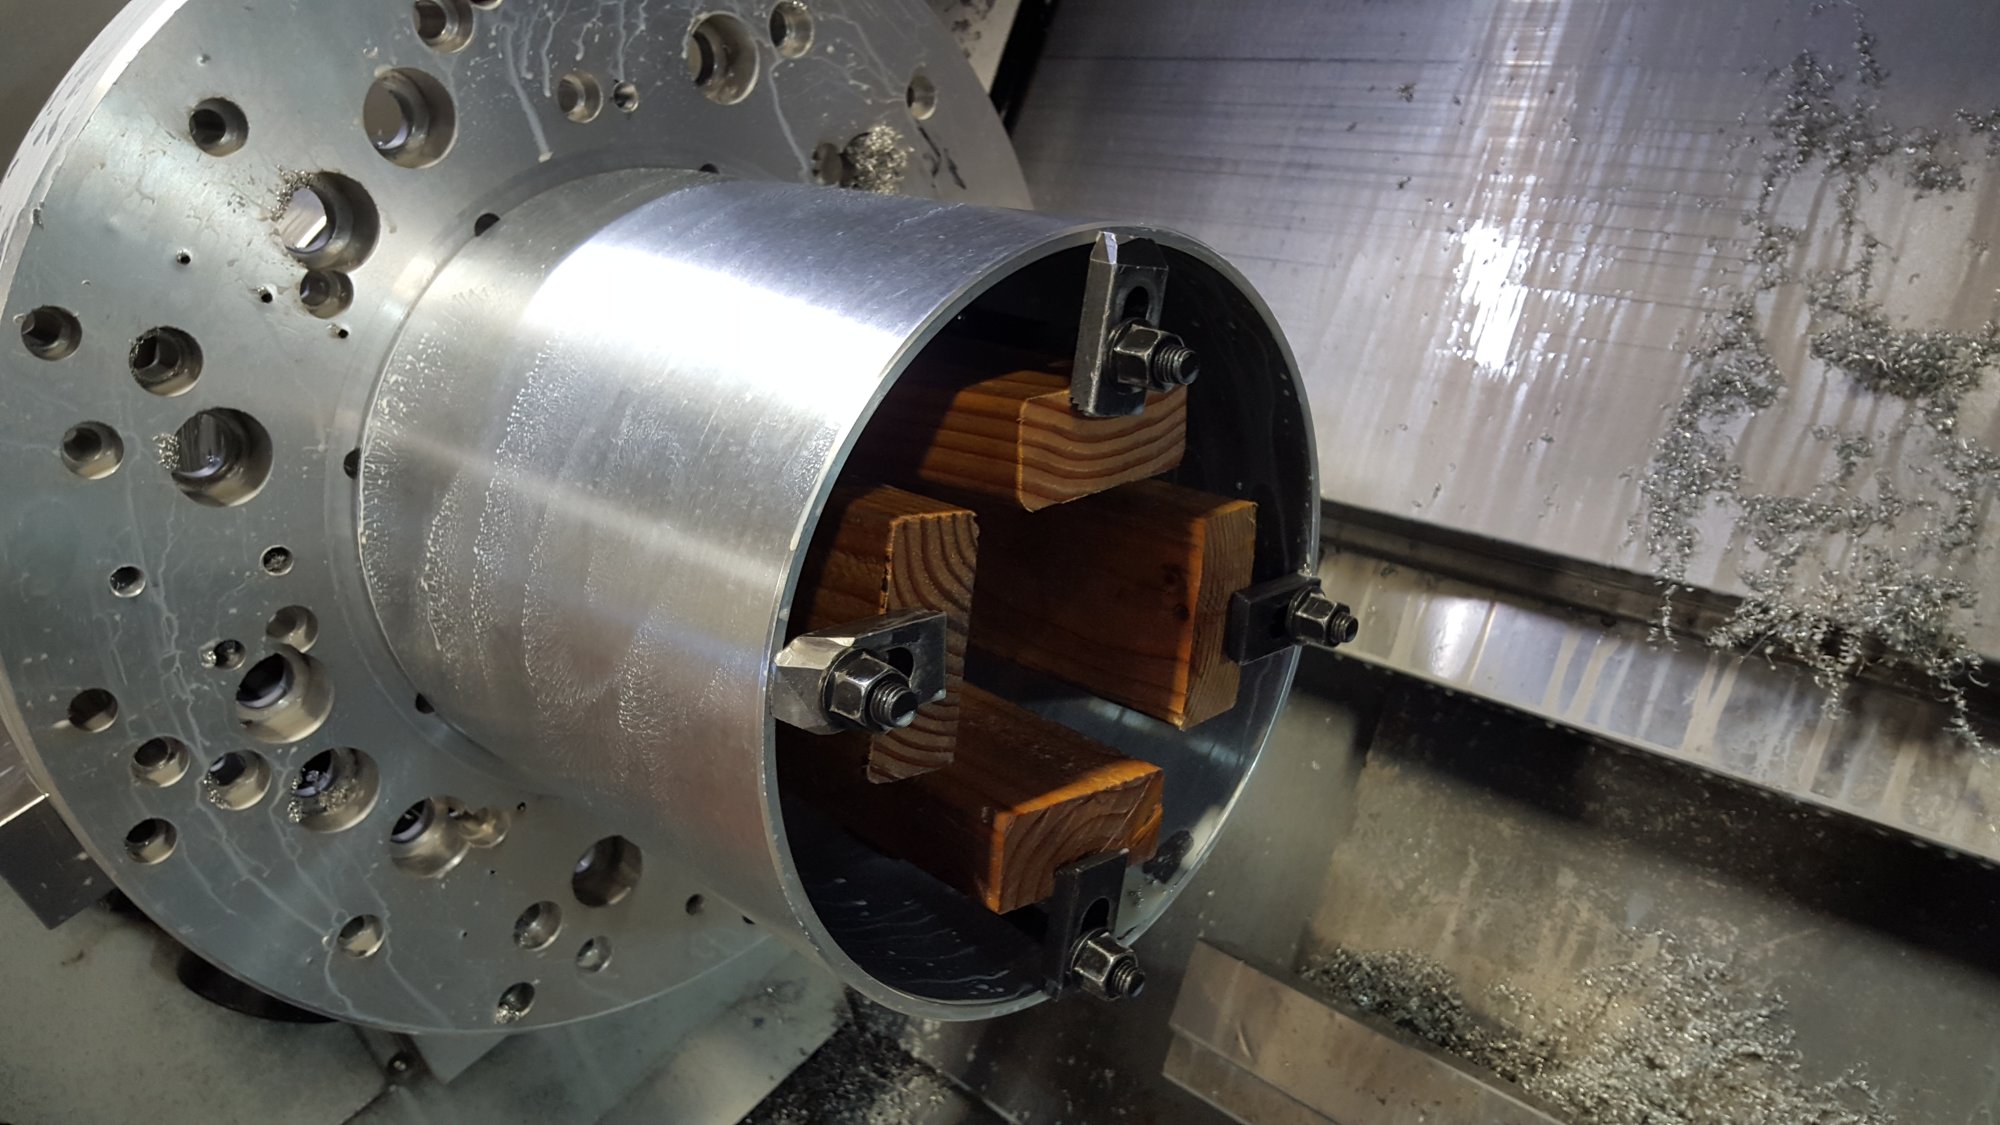
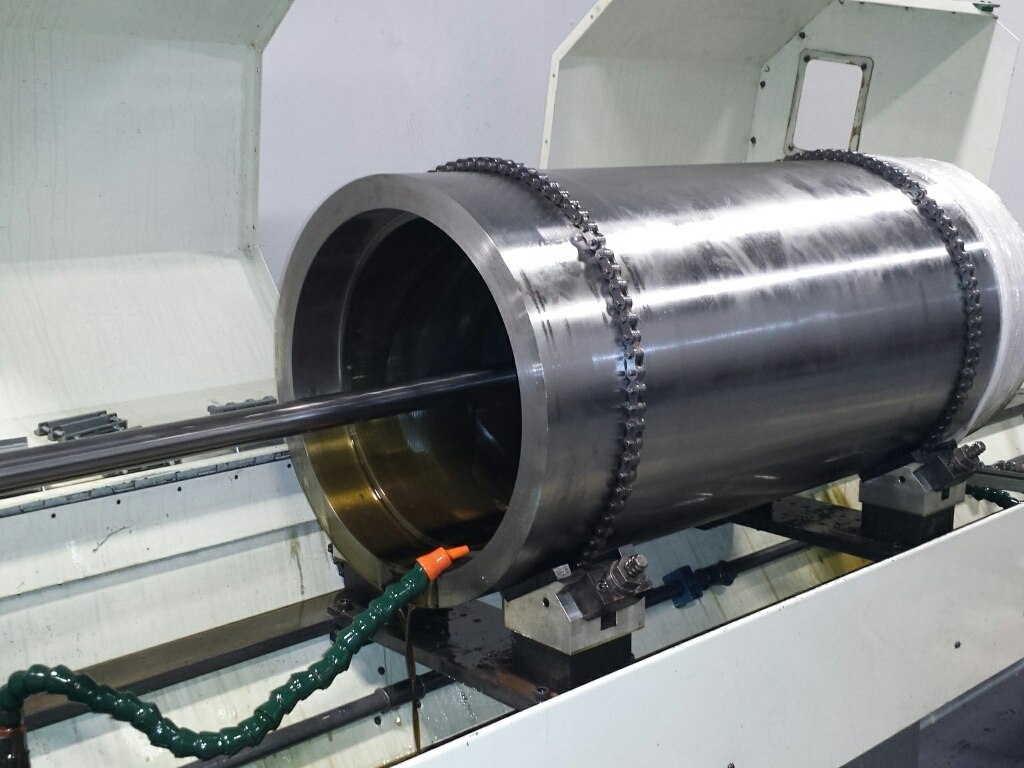
Large cylinder body bored on the lathe, timber packing braced inside to hold it round under the clamps
Large machining: Cylinder body bored, timber packing holding it round
Long shaft supported in a steady rest during turning on the large lathe
Extruder parts: Long shaft carried in the steady rest while turning
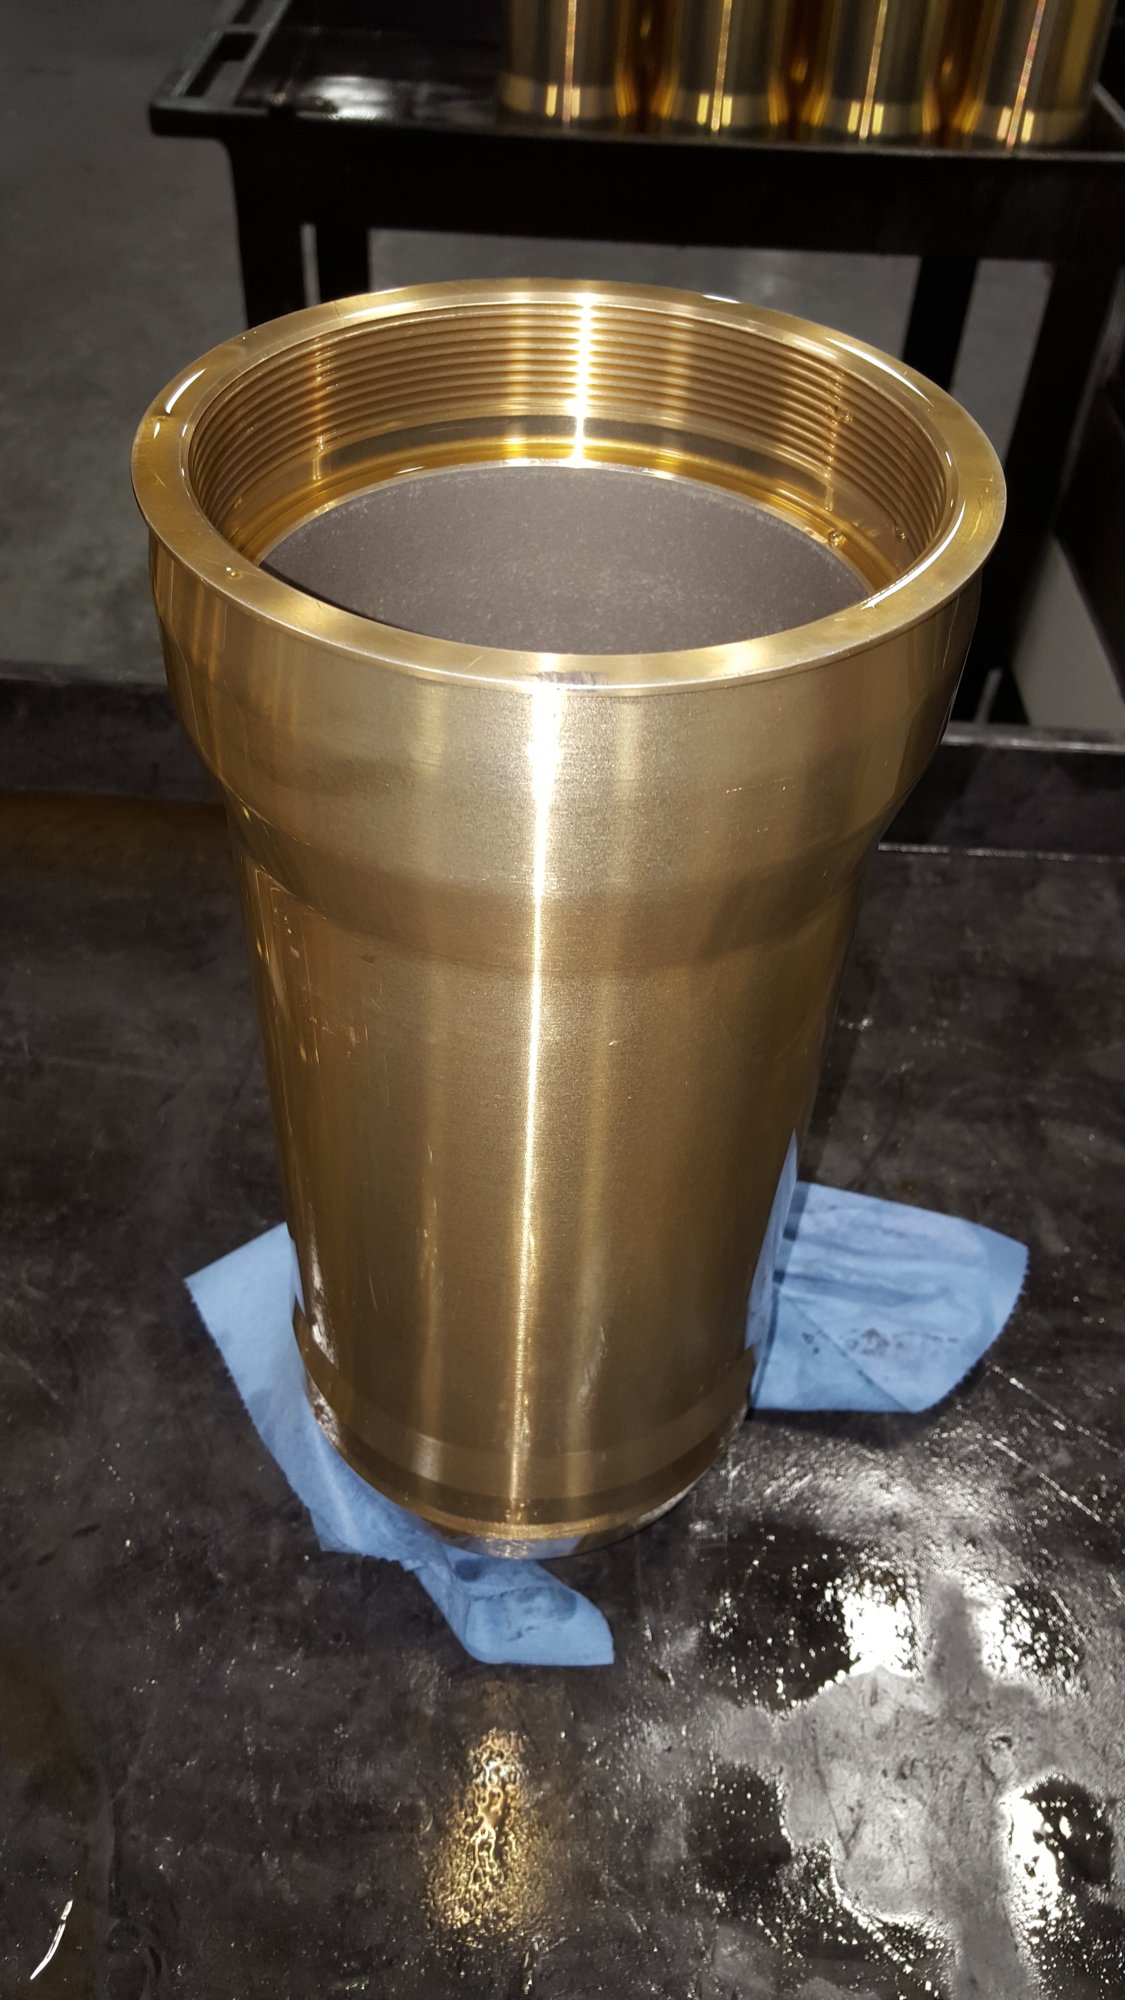
Tapered bronze sleeve bushing, threaded at the top rim and finished on the bench
Turning and production: Tapered bronze sleeve bushing, threaded at the rim
Three-layer blown film die body in the lathe chuck, flange face and bolt circle finish-machined
Blown film dies: Three-layer die body, flange face and bolt circle finished
Large cylinder barrel set up on the honing machine with the hone entering the bore
Bore honing: Cylinder barrel with the hone entering the bore
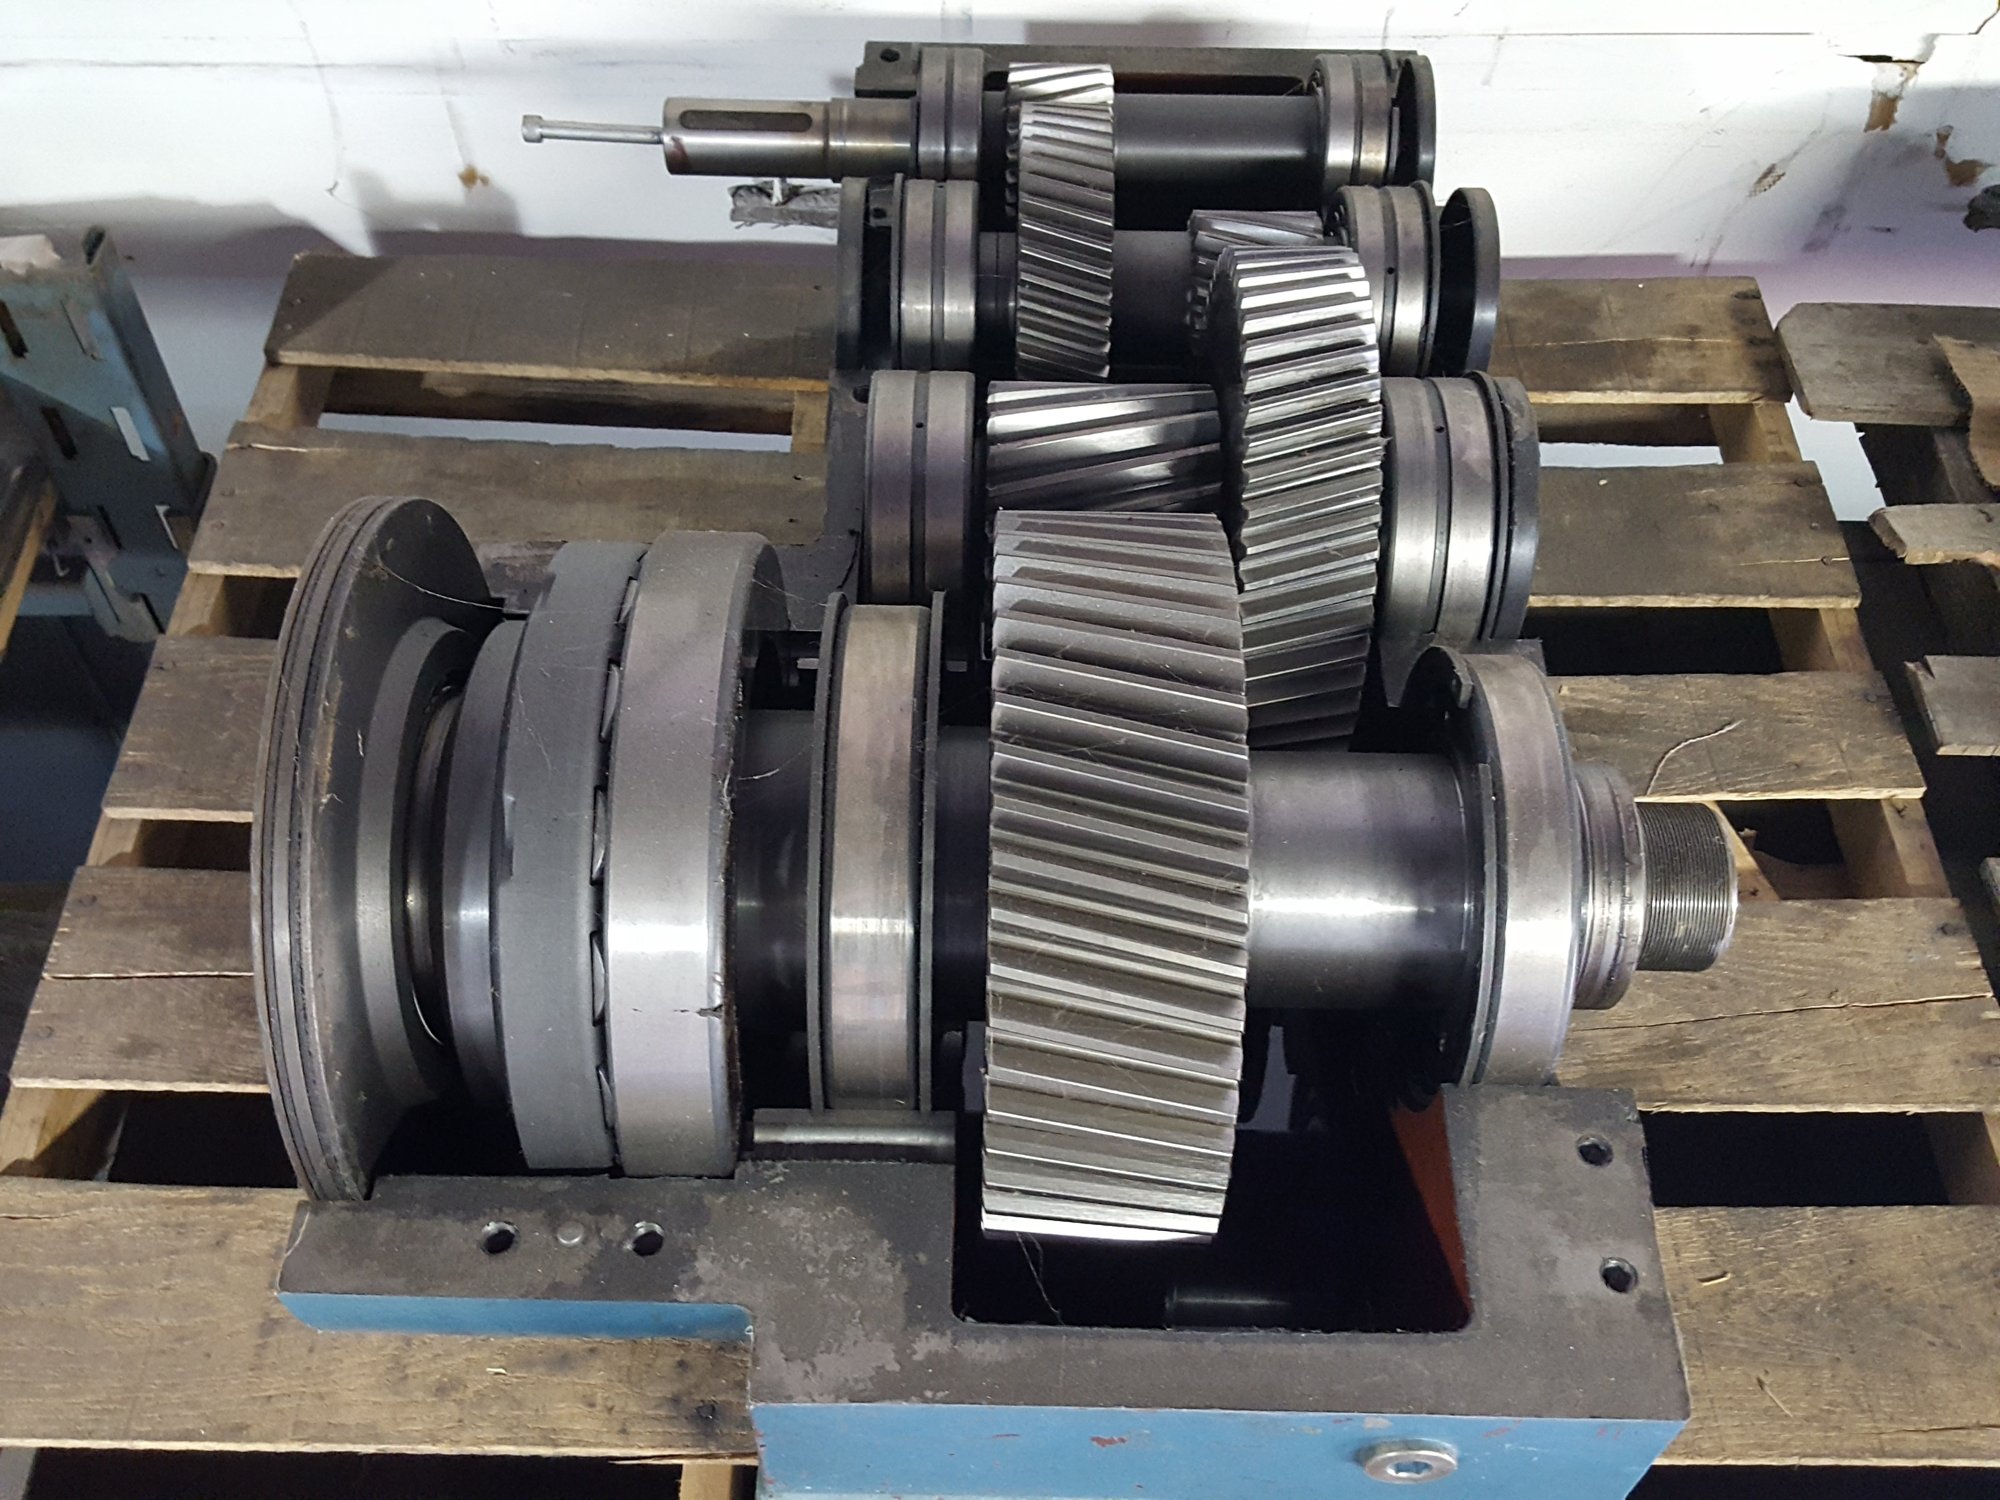
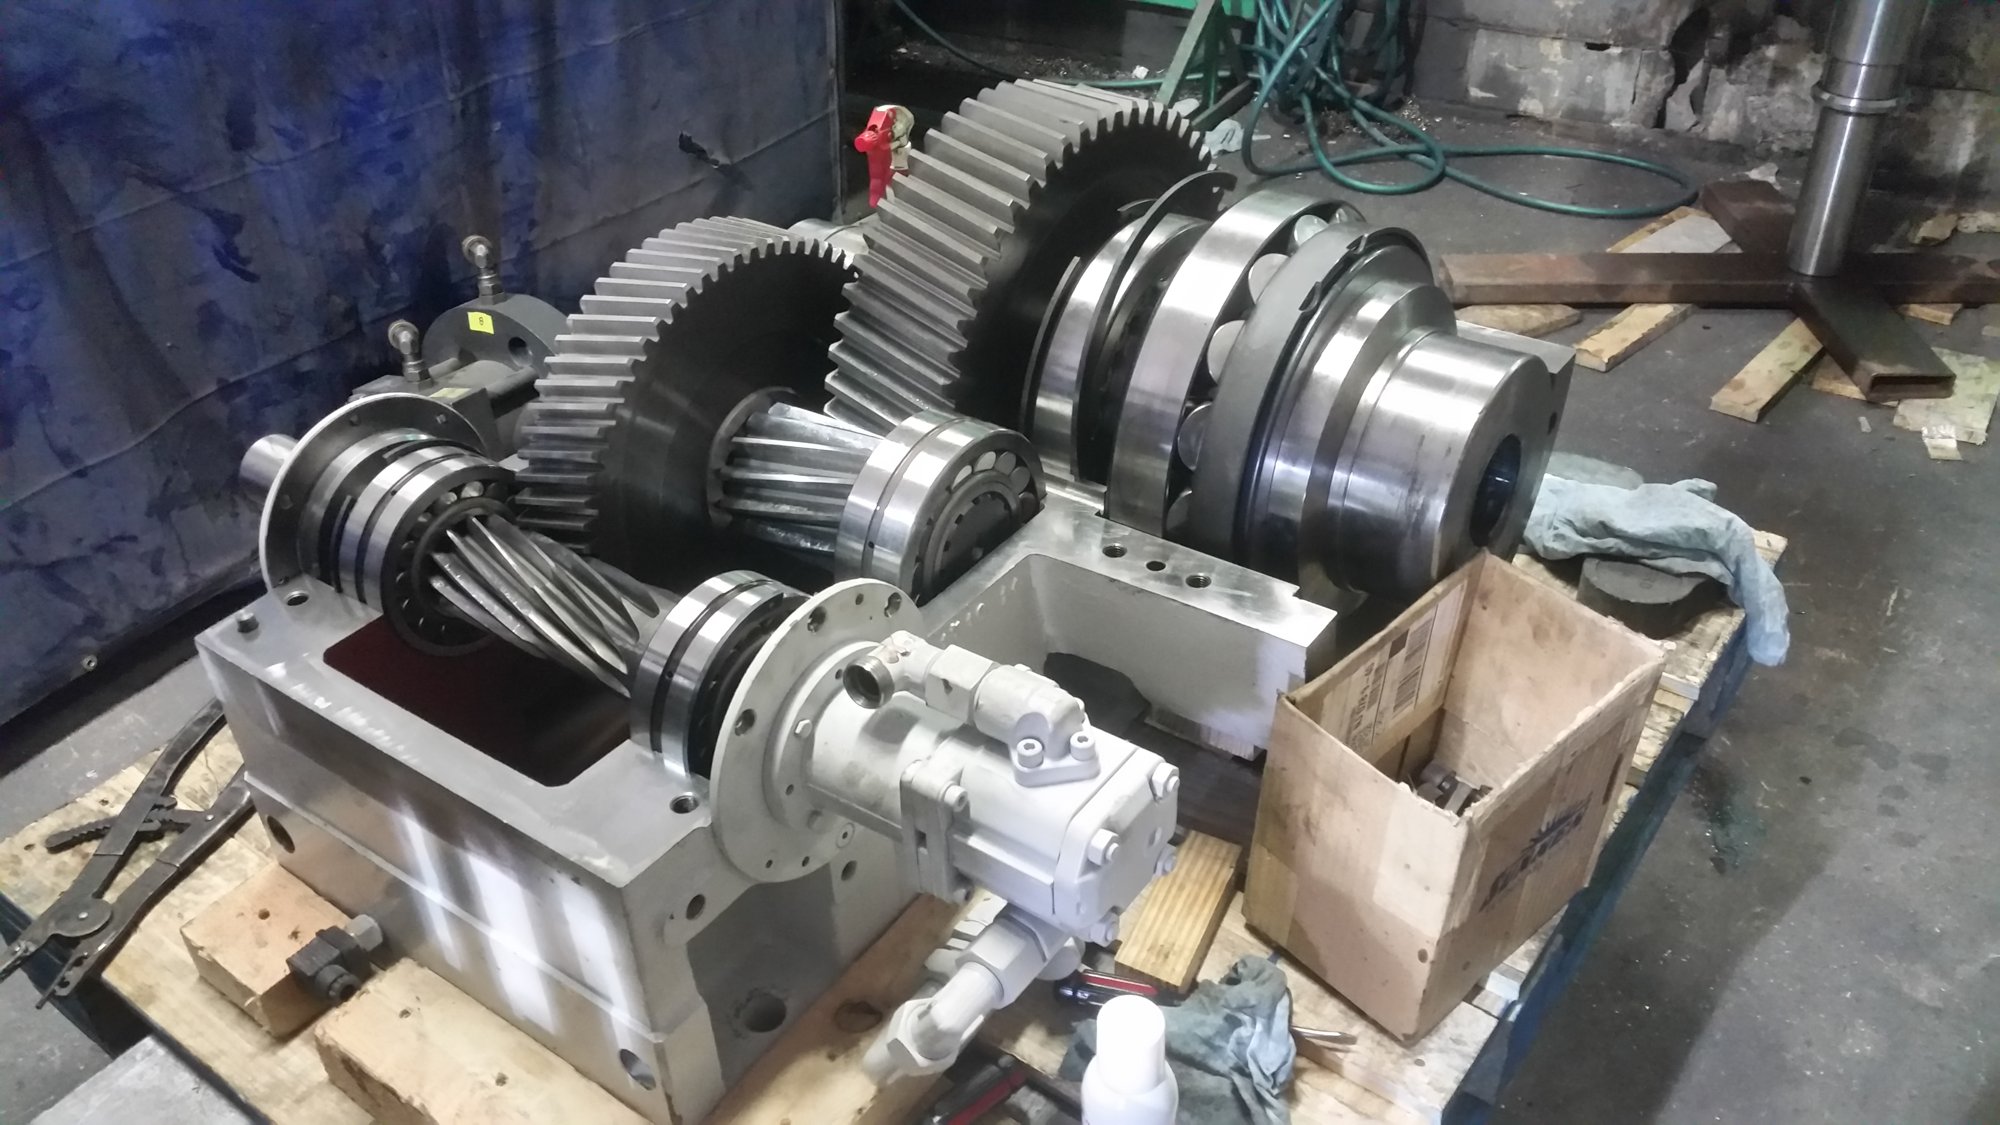
Multi-stage gear drive assembled on its stand, three helical gear sets and shafts stacked out of the case
Gearbox repair: Multi-stage gear drive out of the case
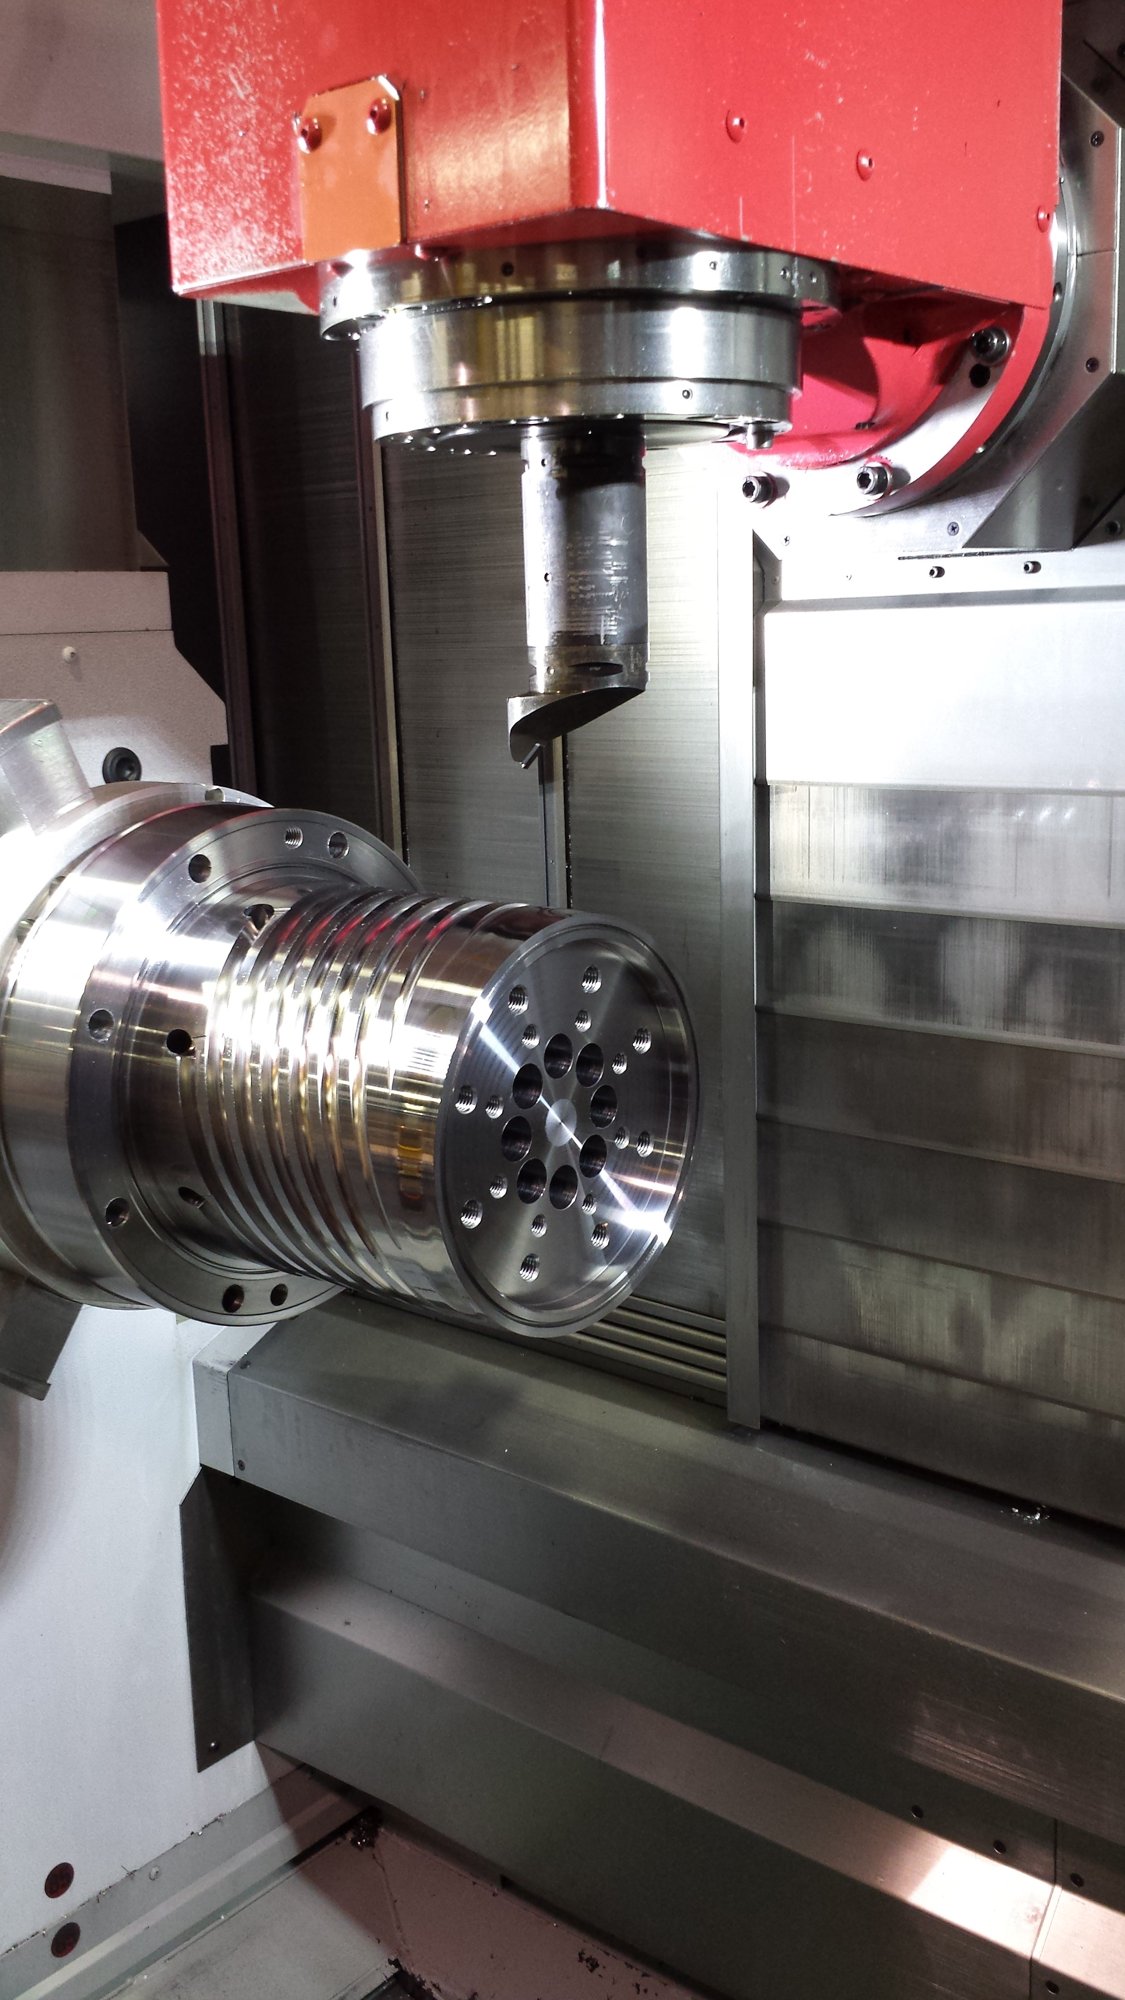
19in spiral mandrel set up under the live tool spindle, drilled port face toward the cutter
Blown film dies: 19in spiral mandrel under the live tool spindle
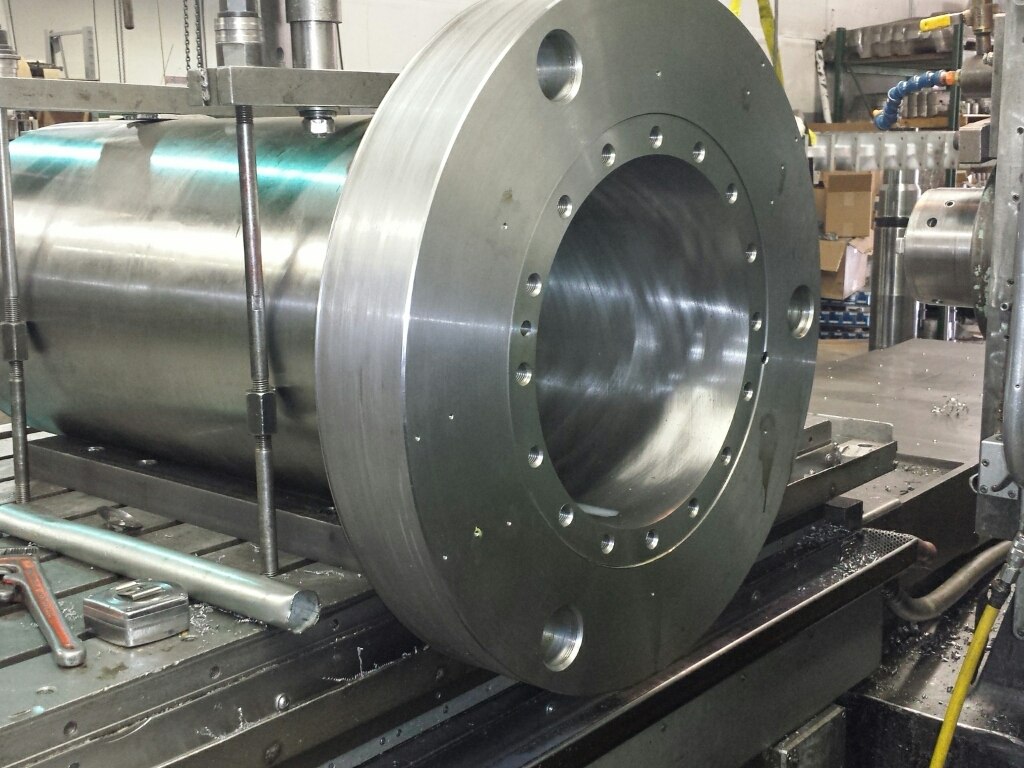
Long cylinder housing clamped on the horizontal boring mill table, flange face toward the spindle
Large machining: Cylinder housing on the horizontal boring mill
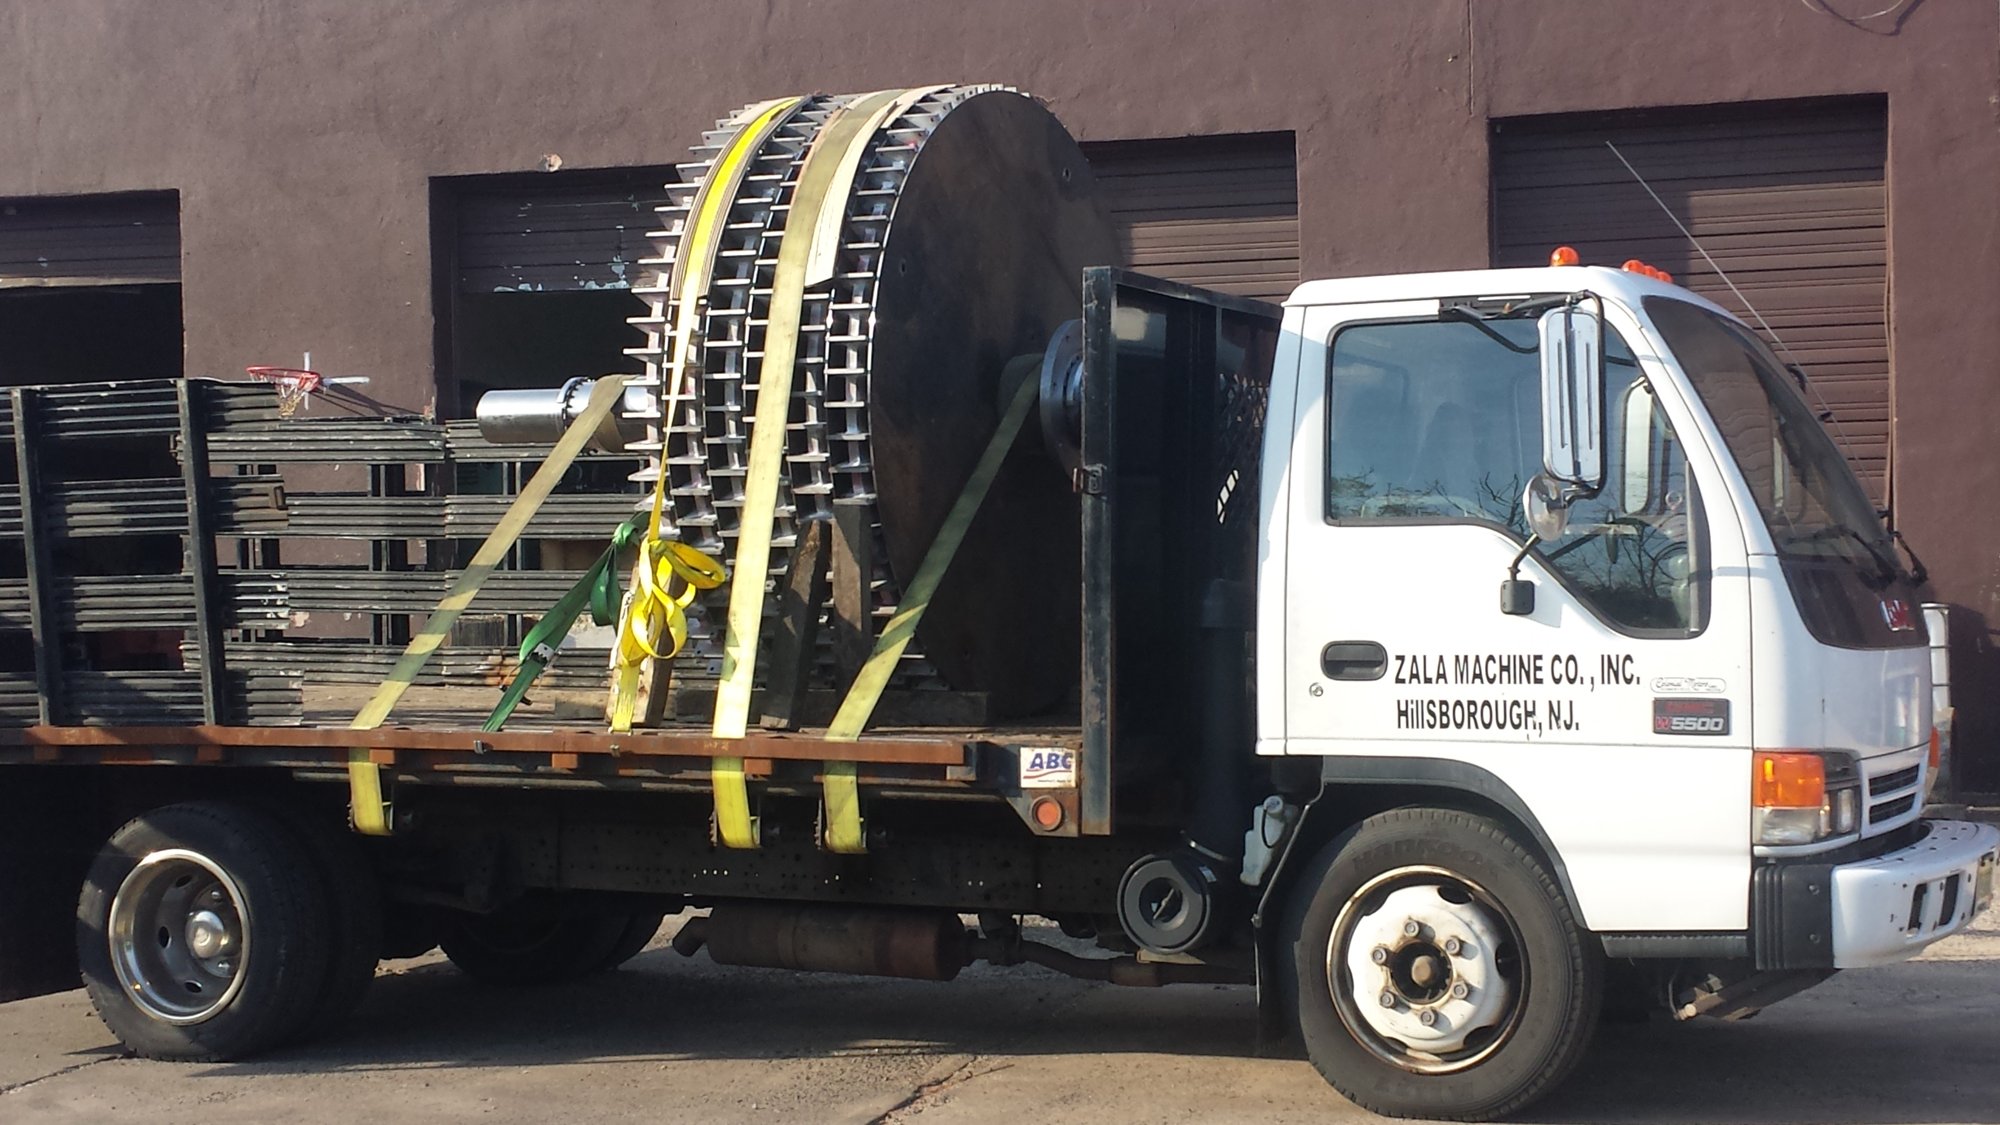
Large spur gear strapped to the Zala Machine flatbed for delivery, Hillsborough NJ lettering on the door
Fabrication and shipping: Loaded on our own truck for delivery
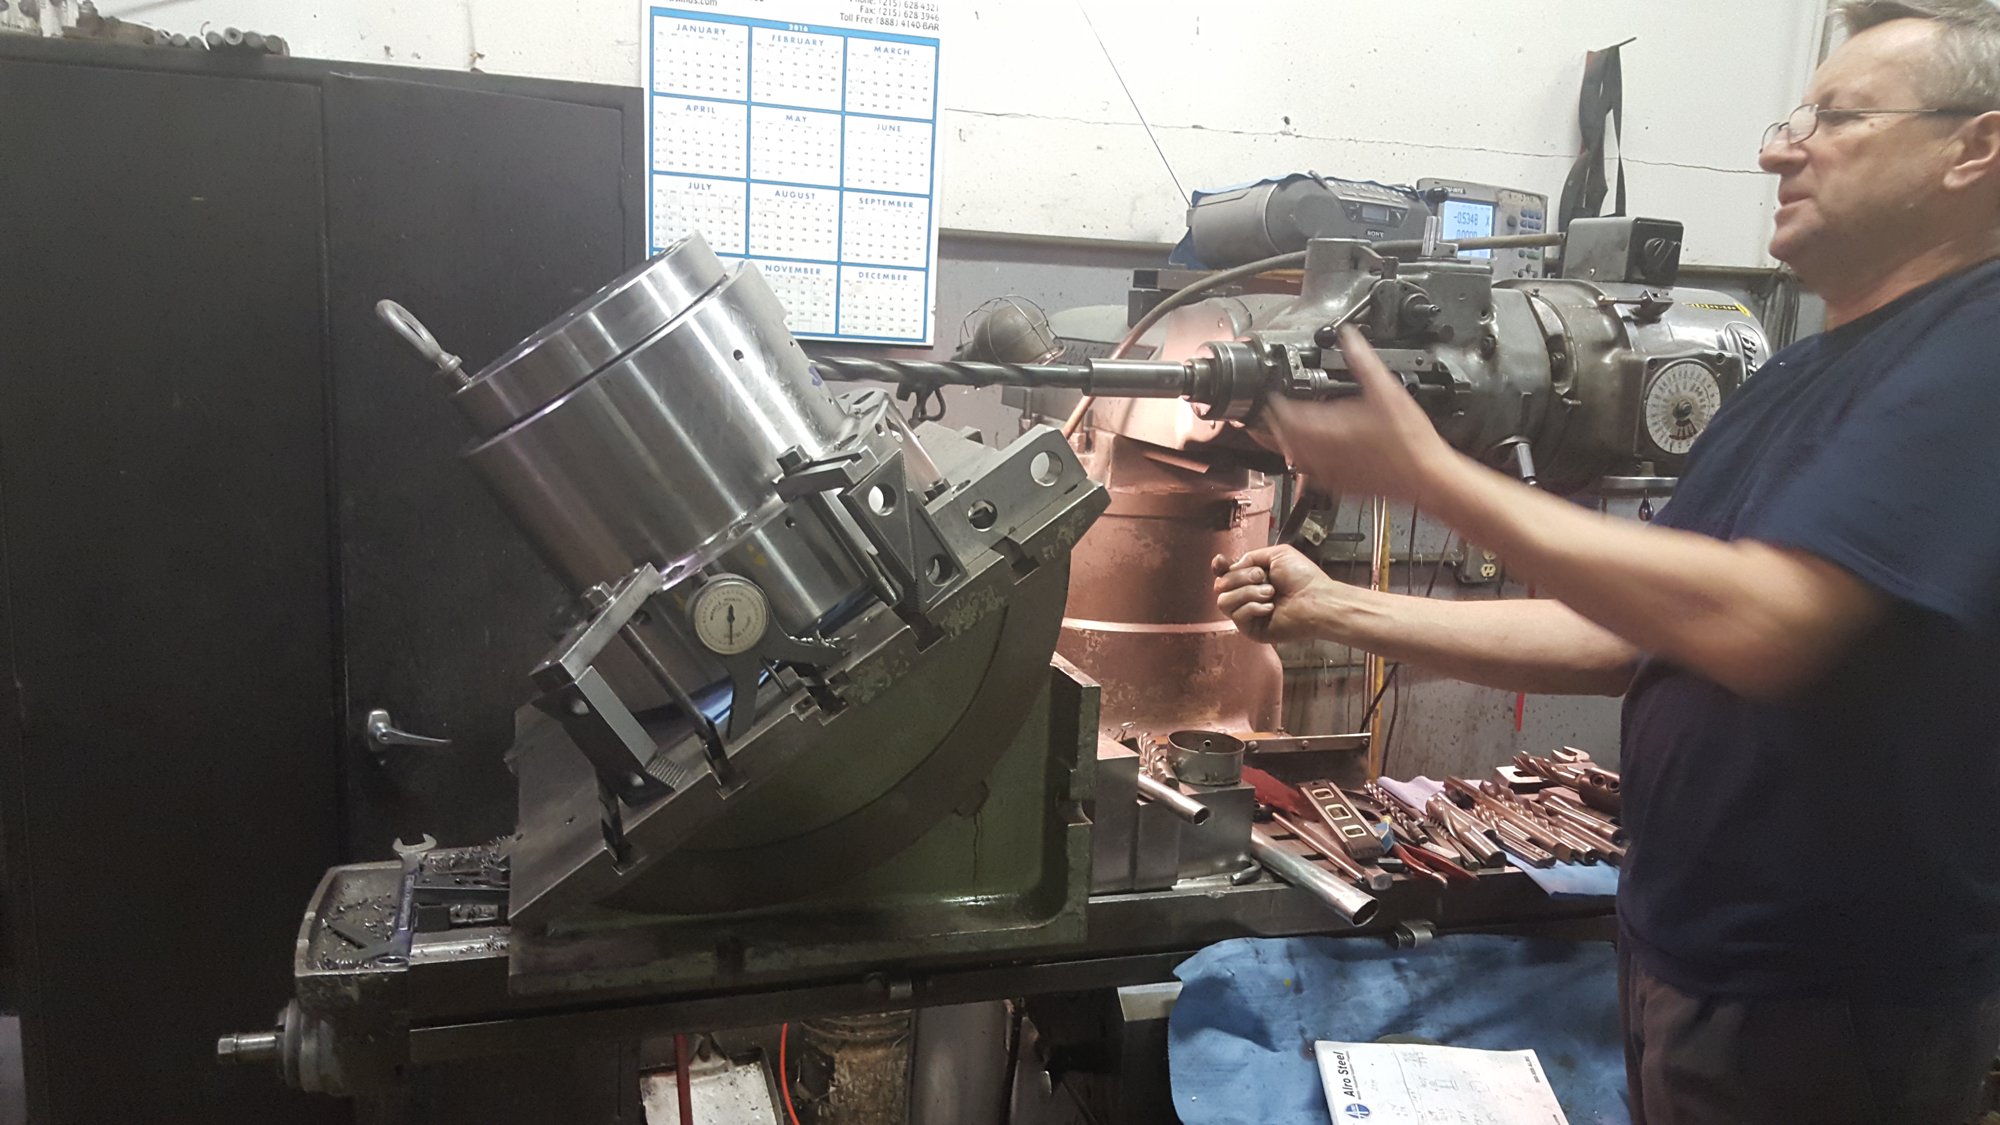
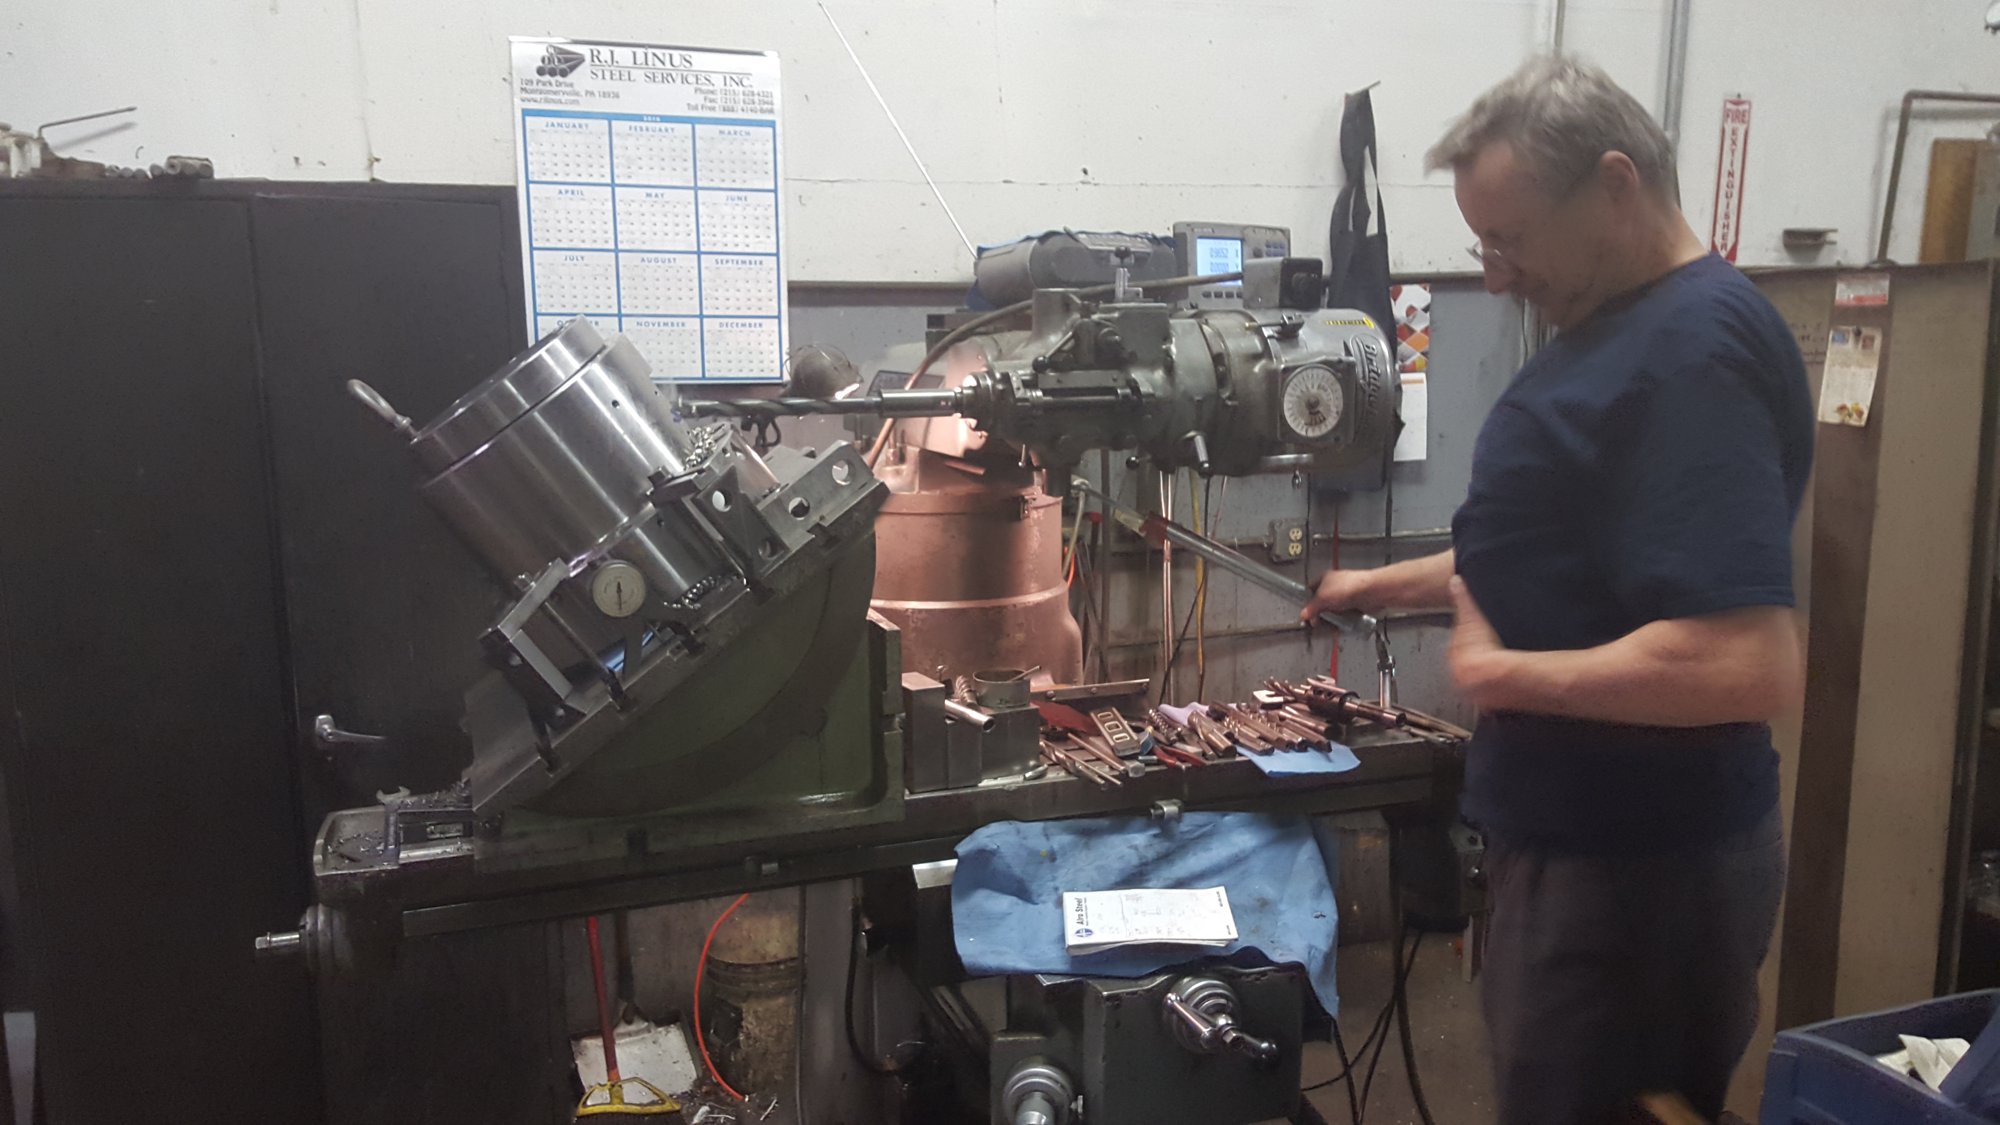
Machinist working on a large die body clamped in the tilting fixture, tooling laid out on the bench
The shop: Working on a die body in the tilting fixture
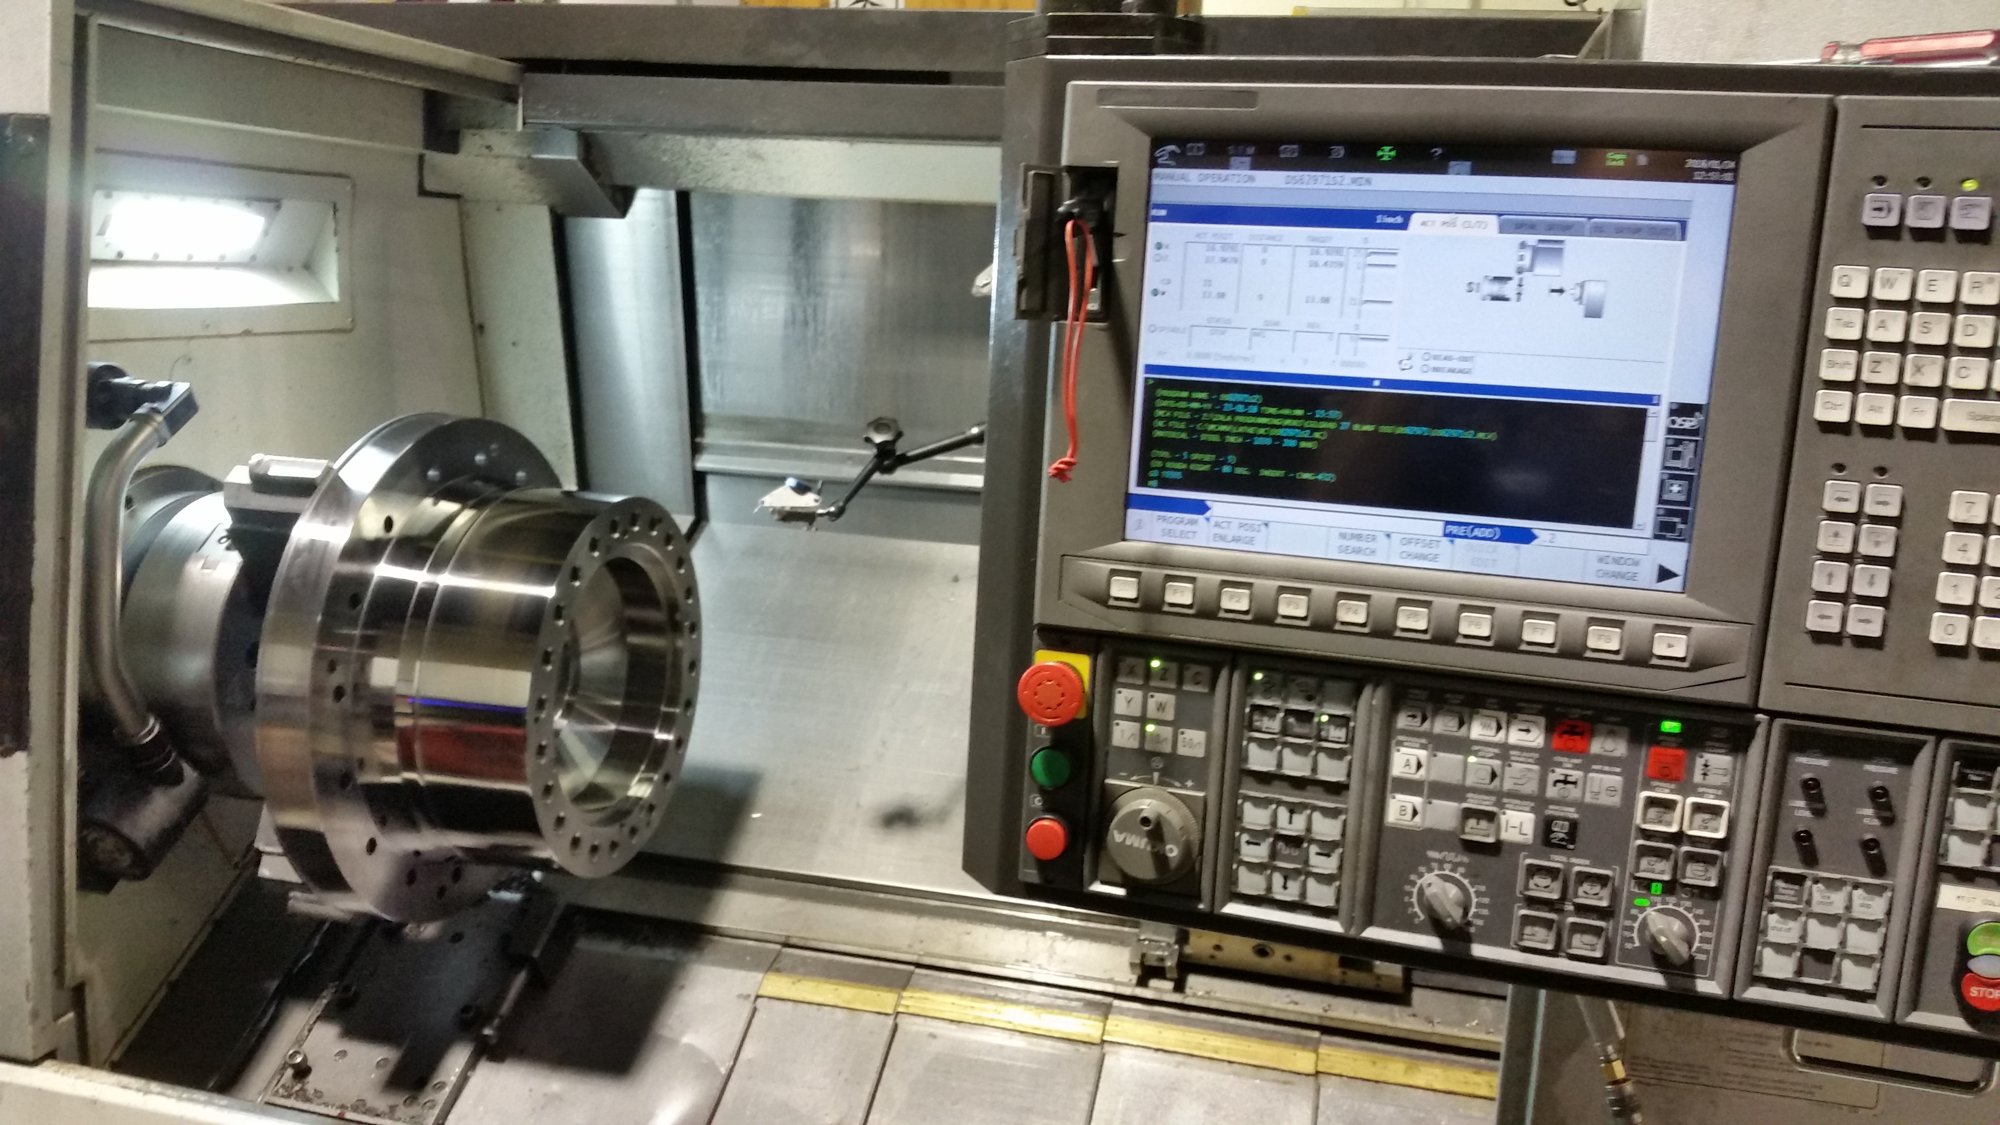
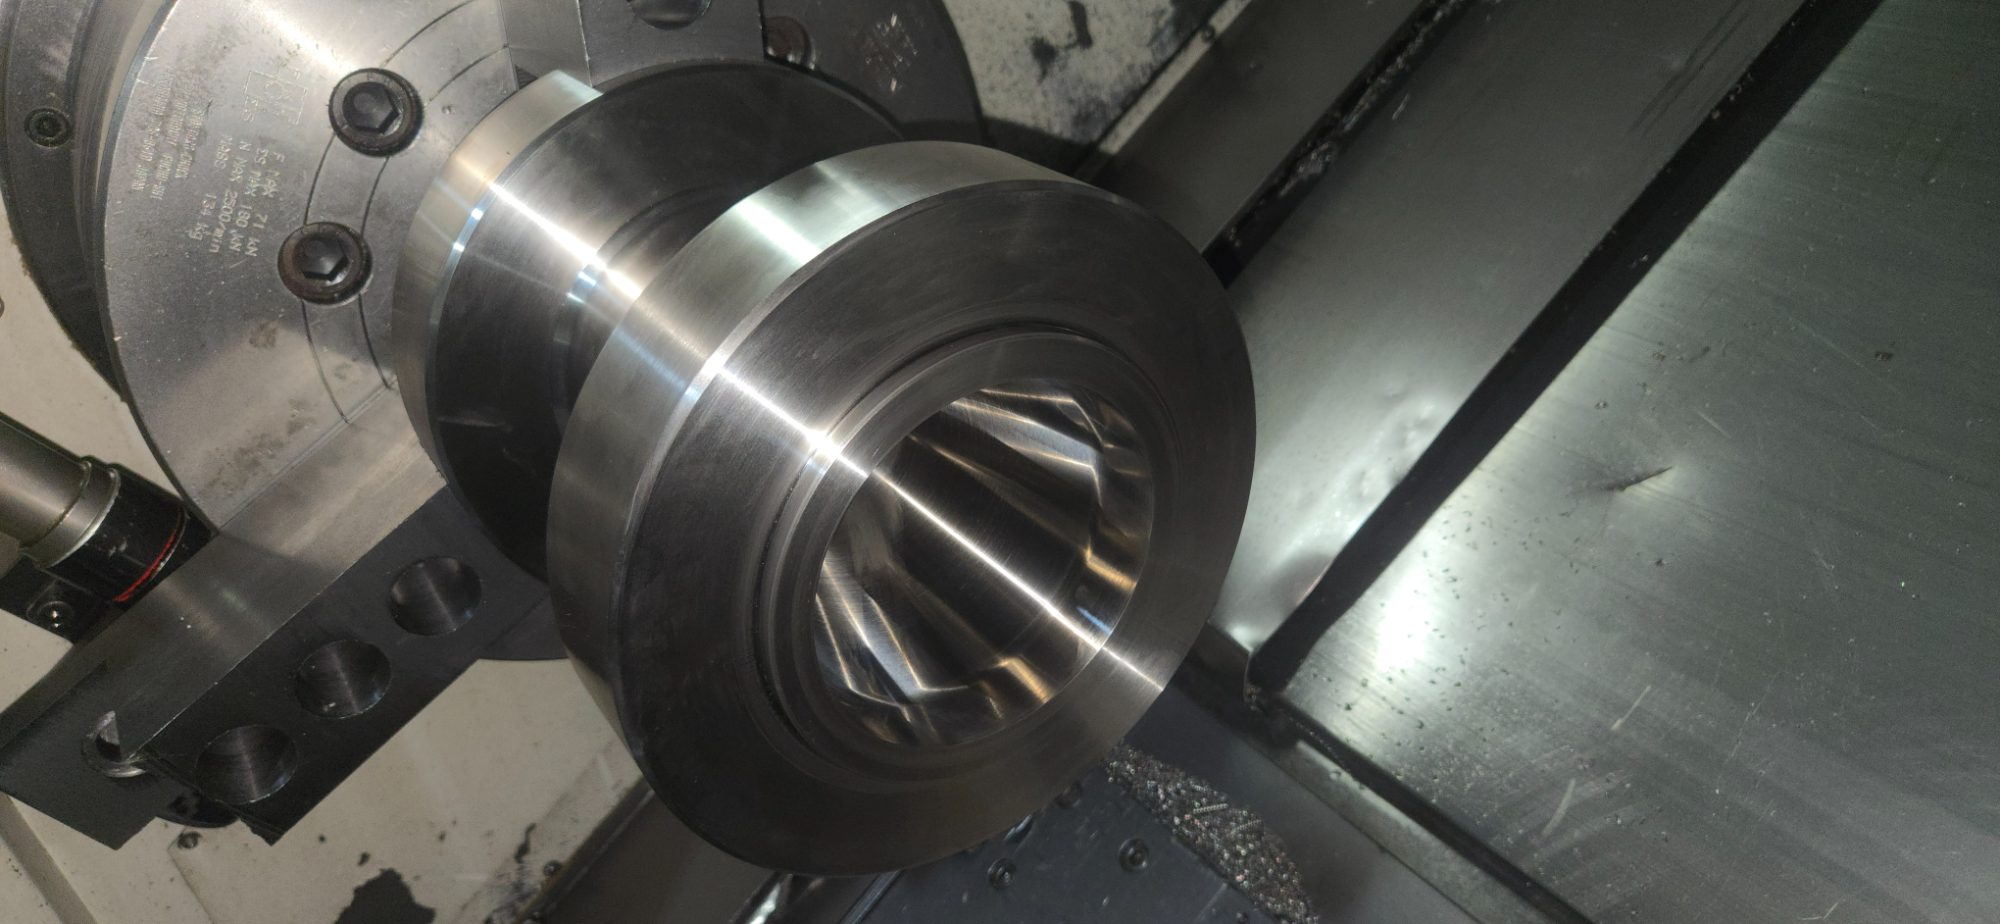
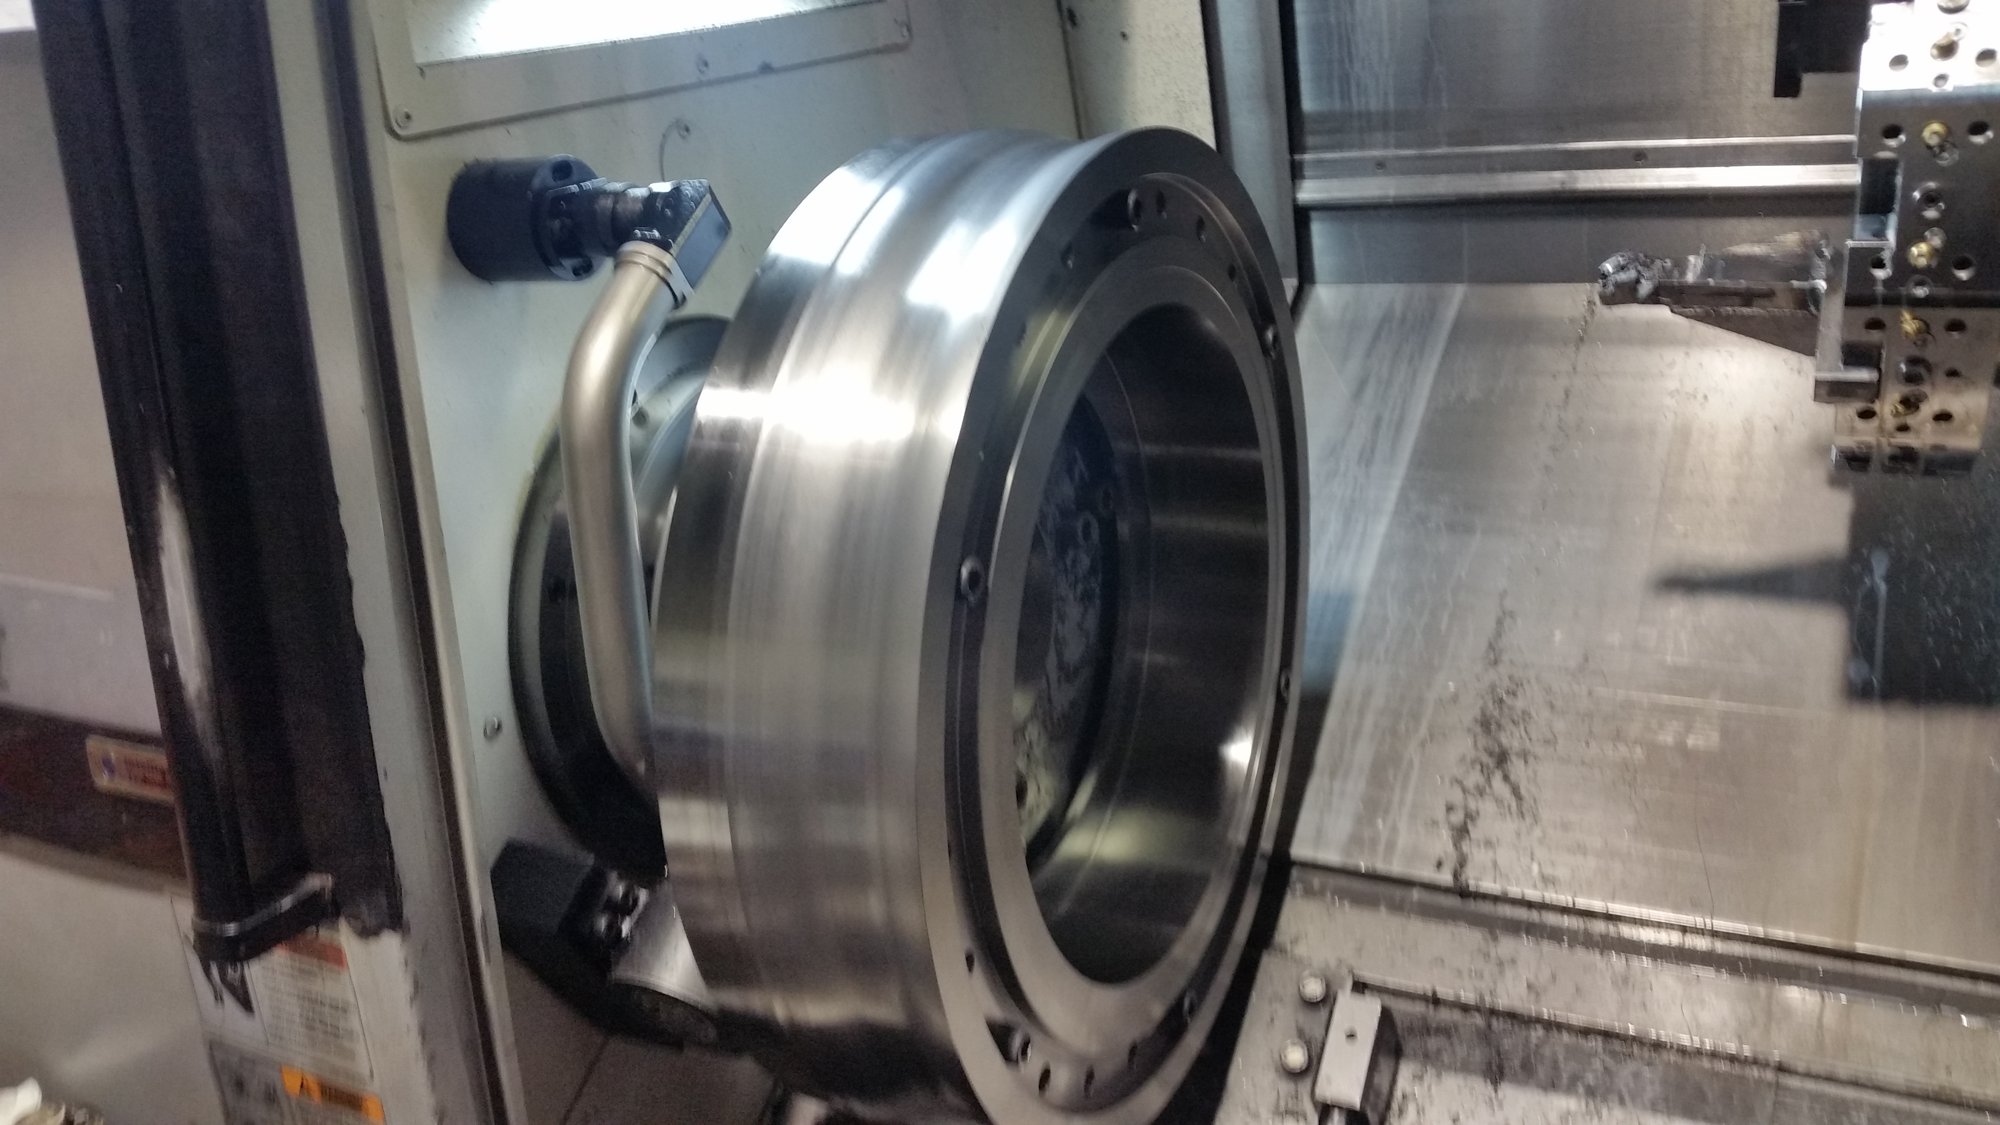
Large flanged hub running in the CNC lathe, program up on the control alongside
Turning and production: Large flanged hub running in the CNC lathe
19in spiral mandrel held in the mill-turn chuck, turret tooling and live spindle in the work envelope
Blown film dies: 19in spiral mandrel held in the mill-turn
Stepped spool with machined flange set up on the lathe
Extruder parts: Stepped spool with machined flange, set up on the lathe
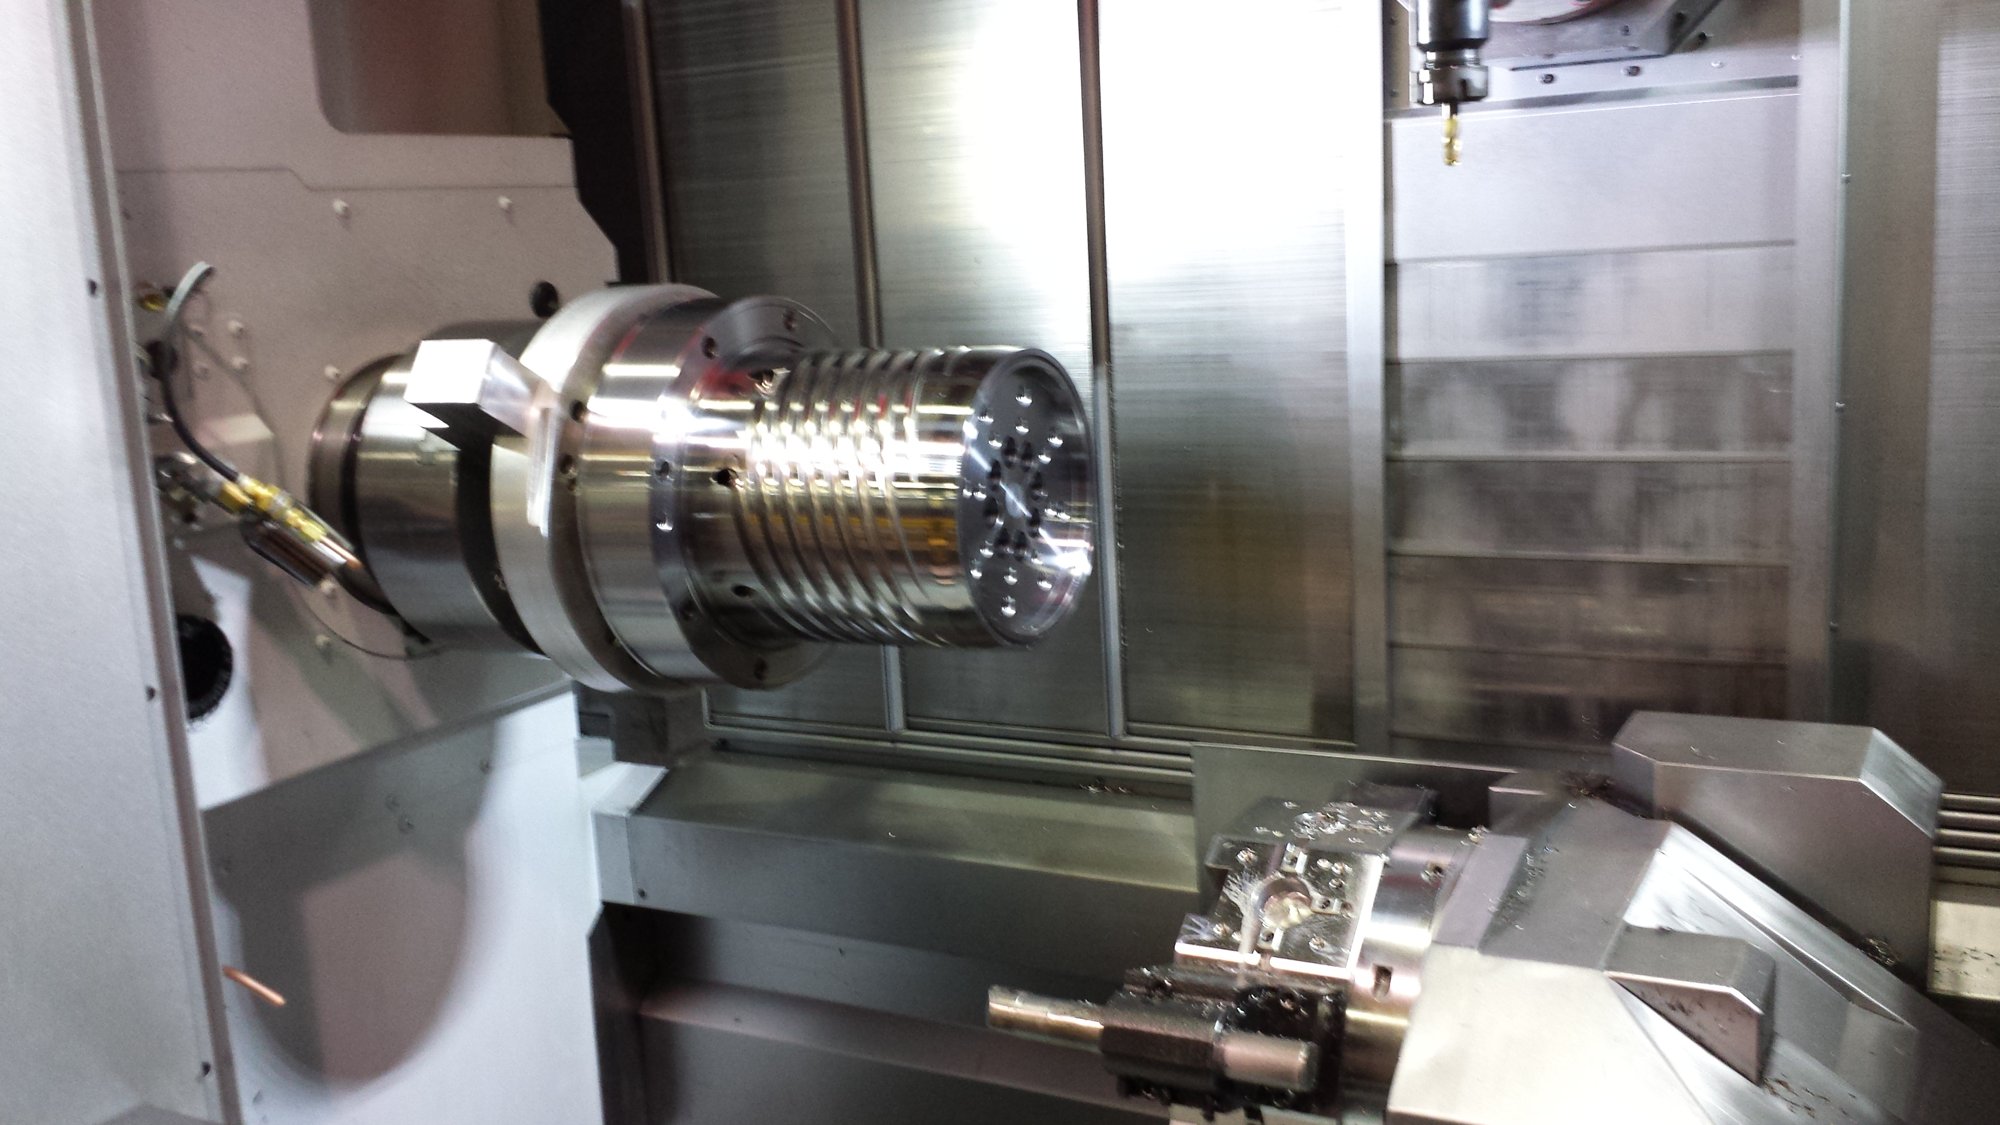
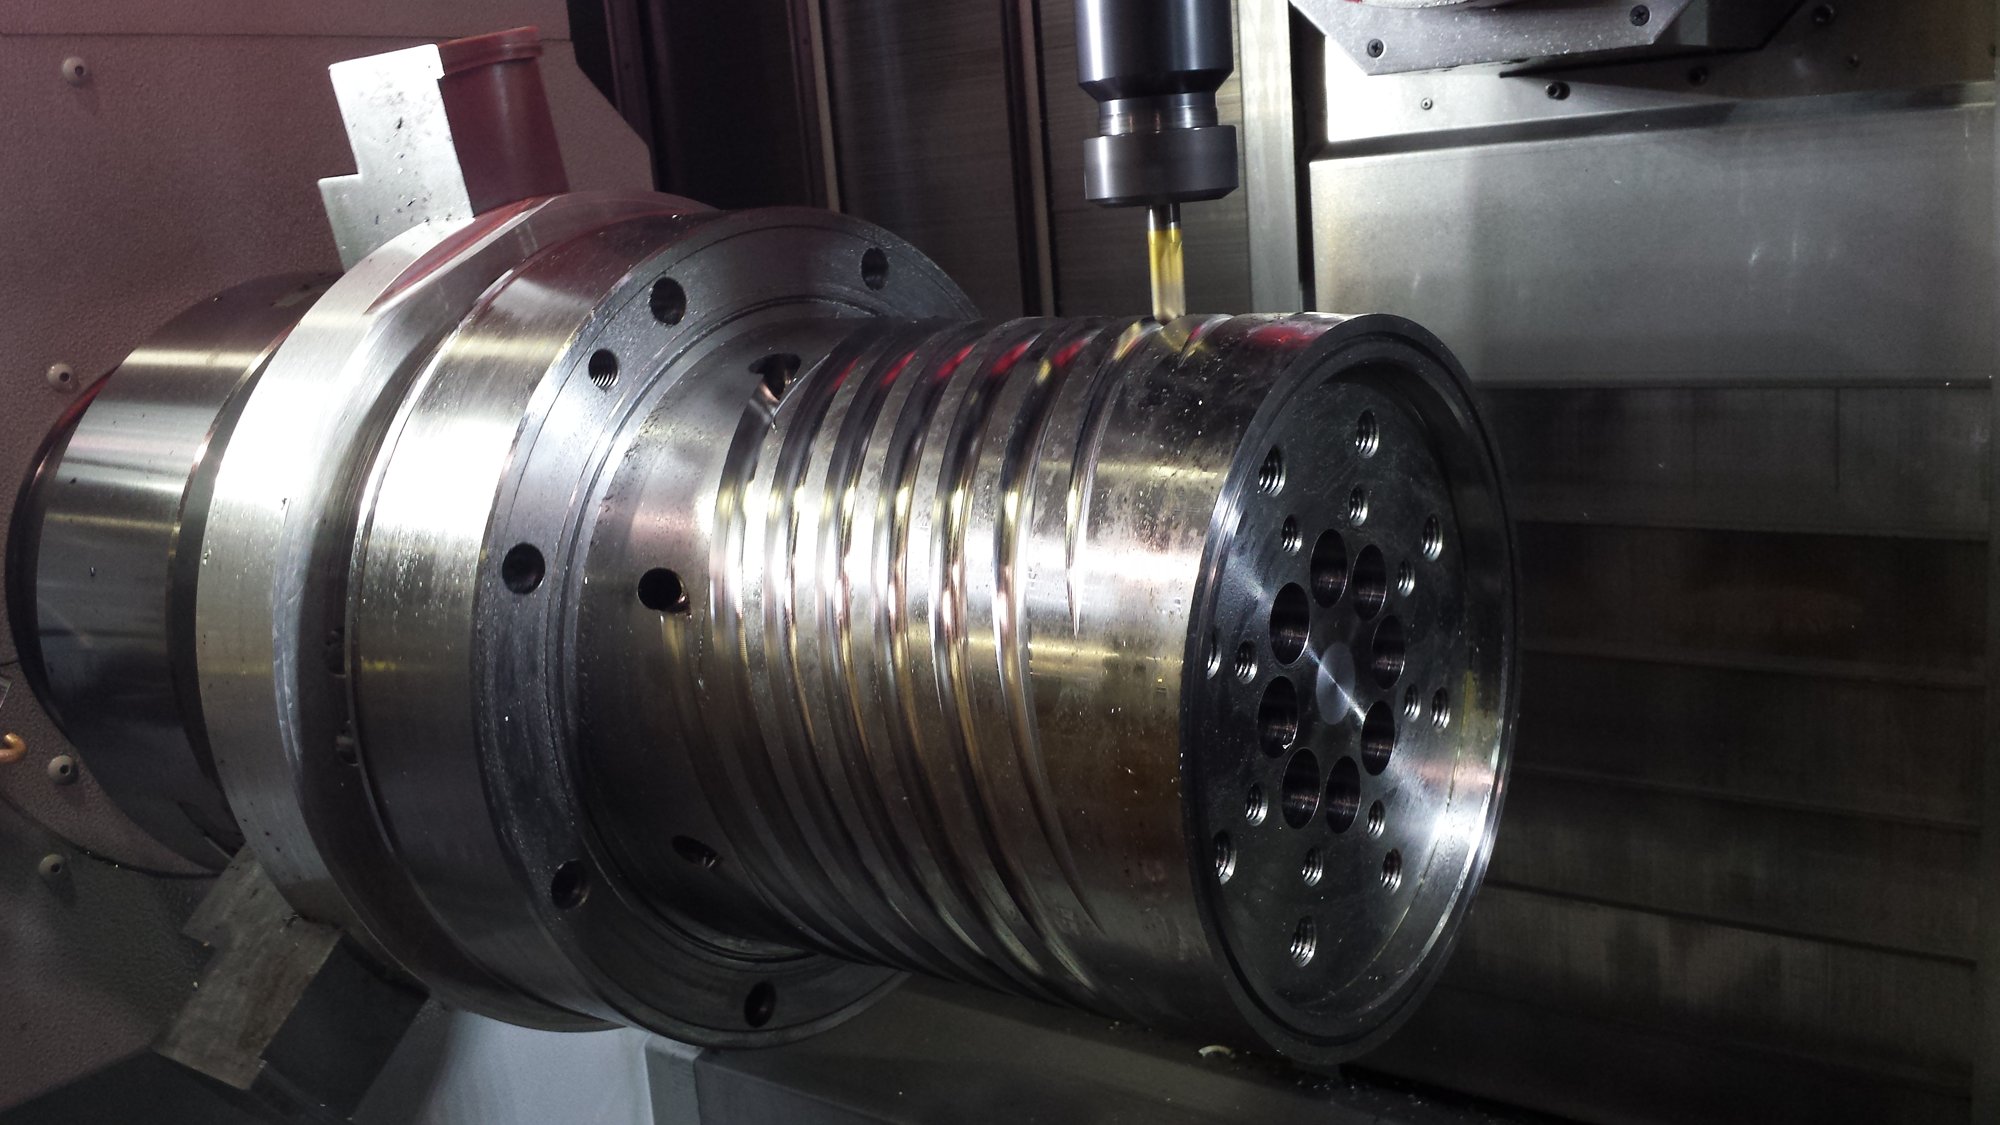
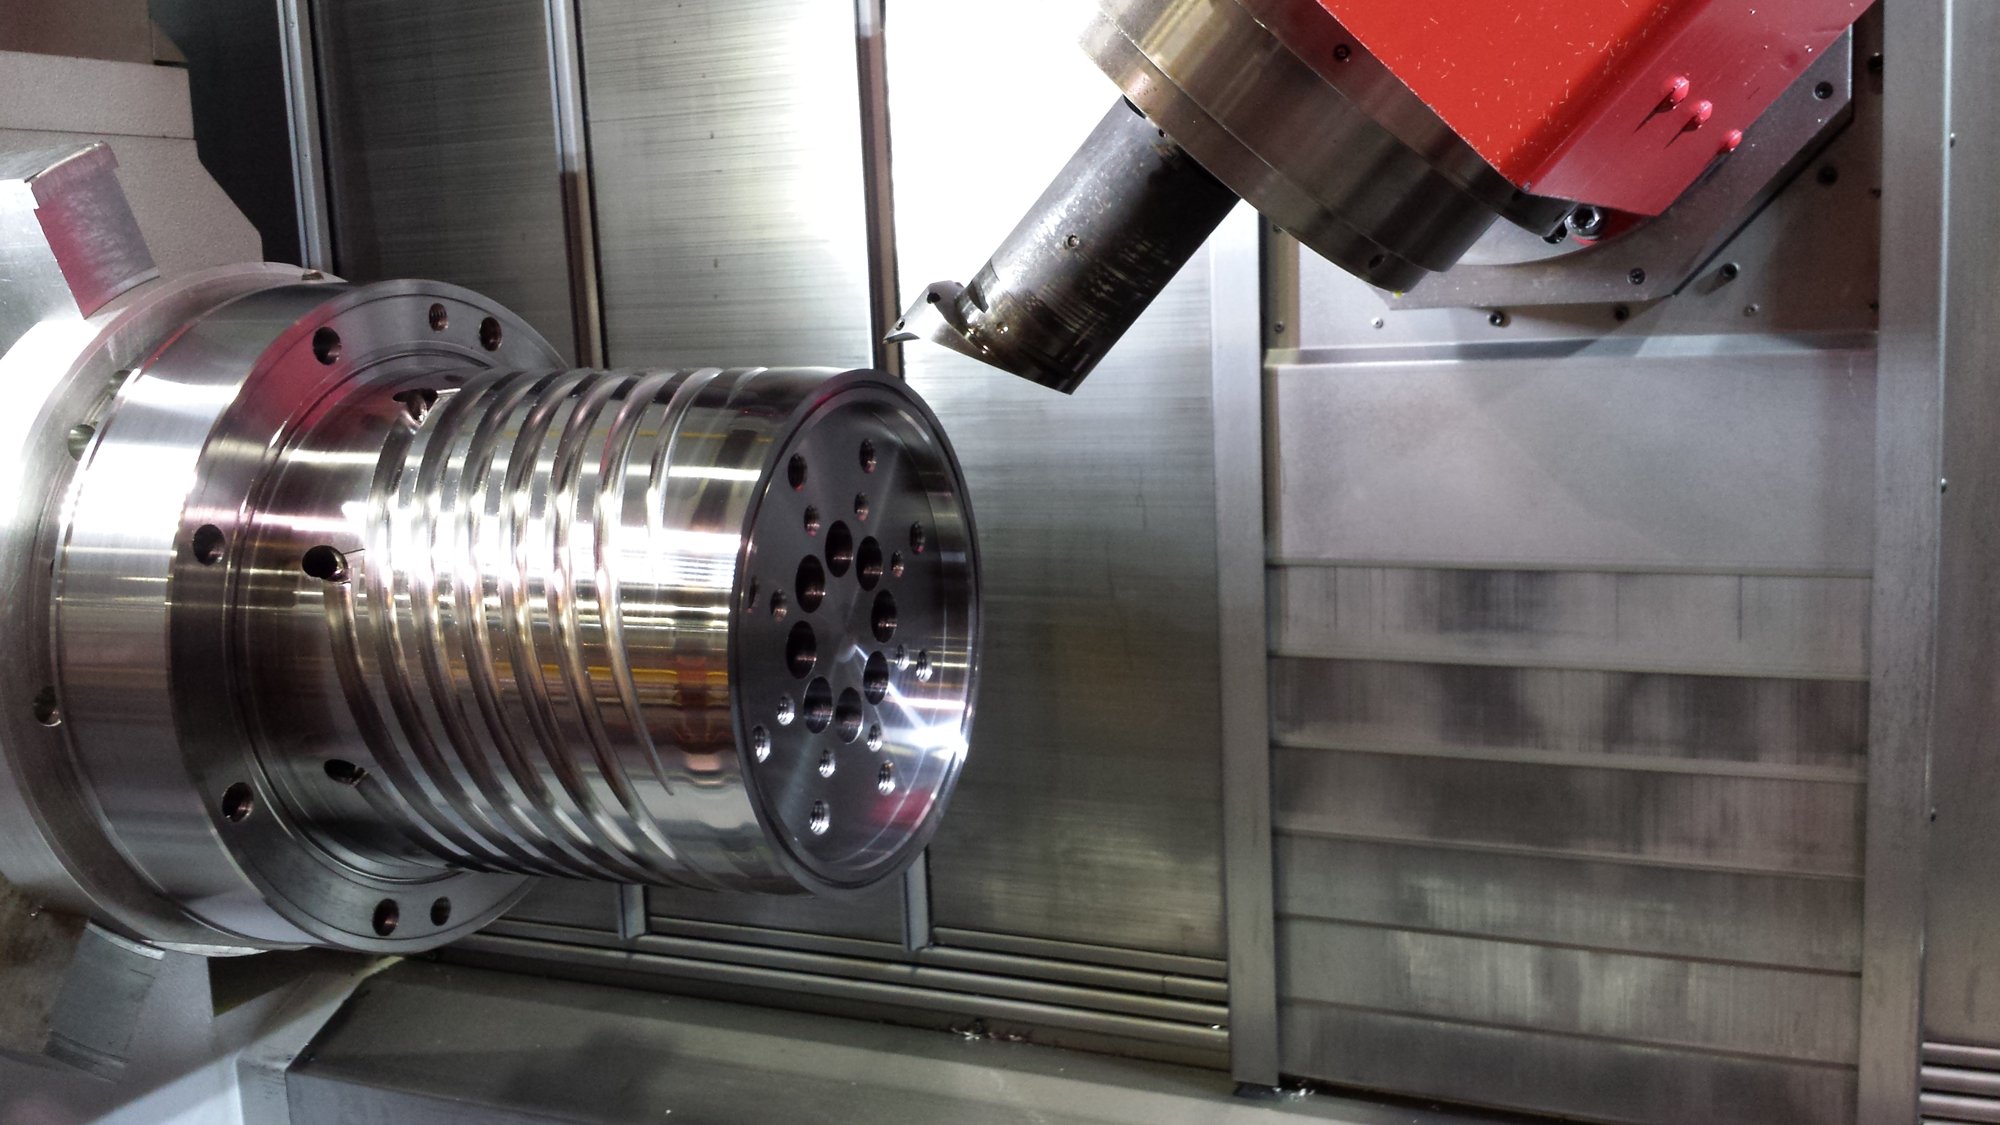
Spiral flow channels being milled into a 19in mandrel for a three-layer blown film die
One die, start to finish (6 of 10): Spiral flow channels milled into the 19in mandrel
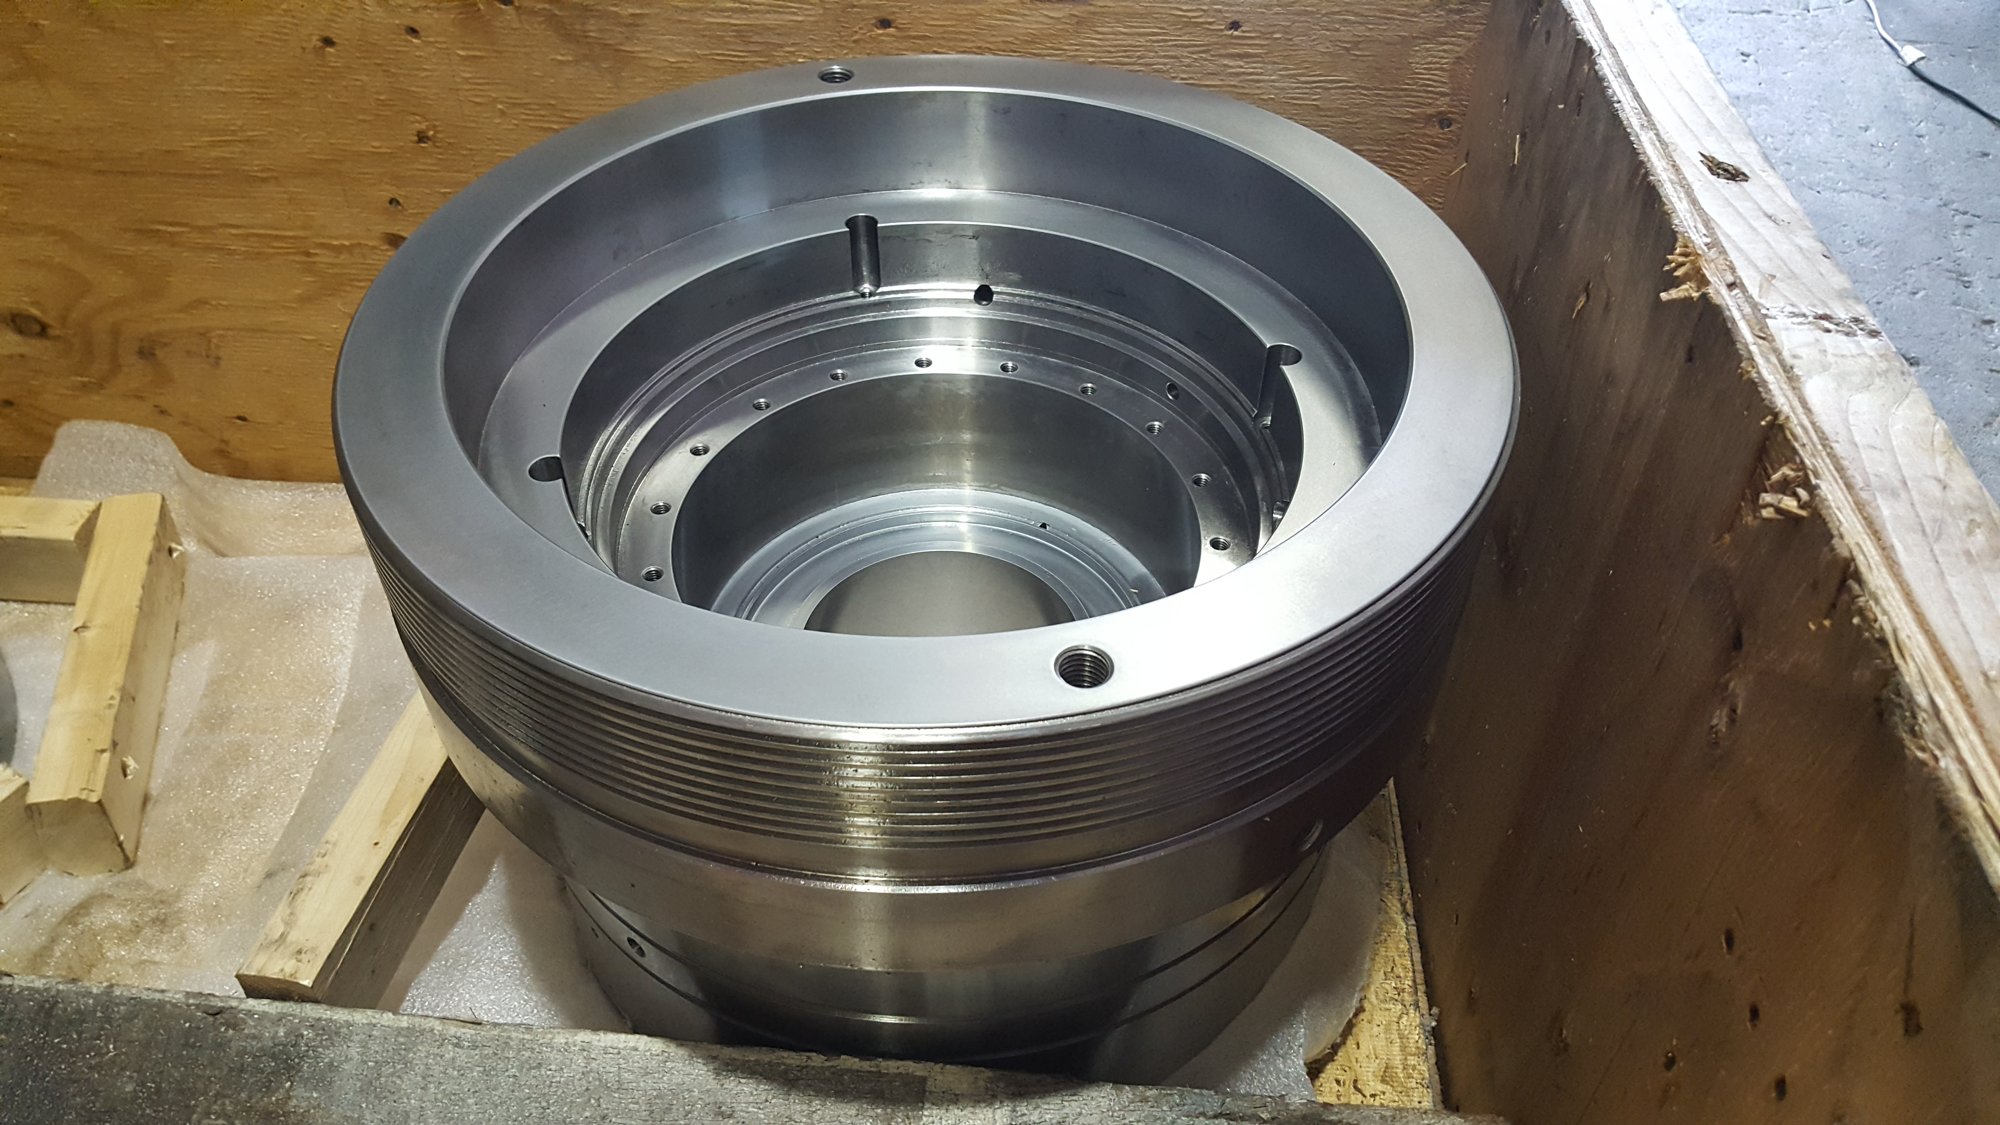
Large barrel housing on the machine, circumferential grooves cut around the body and the flange faced
Large machining: Barrel housing, grooves cut and the flange faced
Splined shaft end held in the lathe chuck during turning
Shaft machining: Splined shaft end held in the lathe chuck
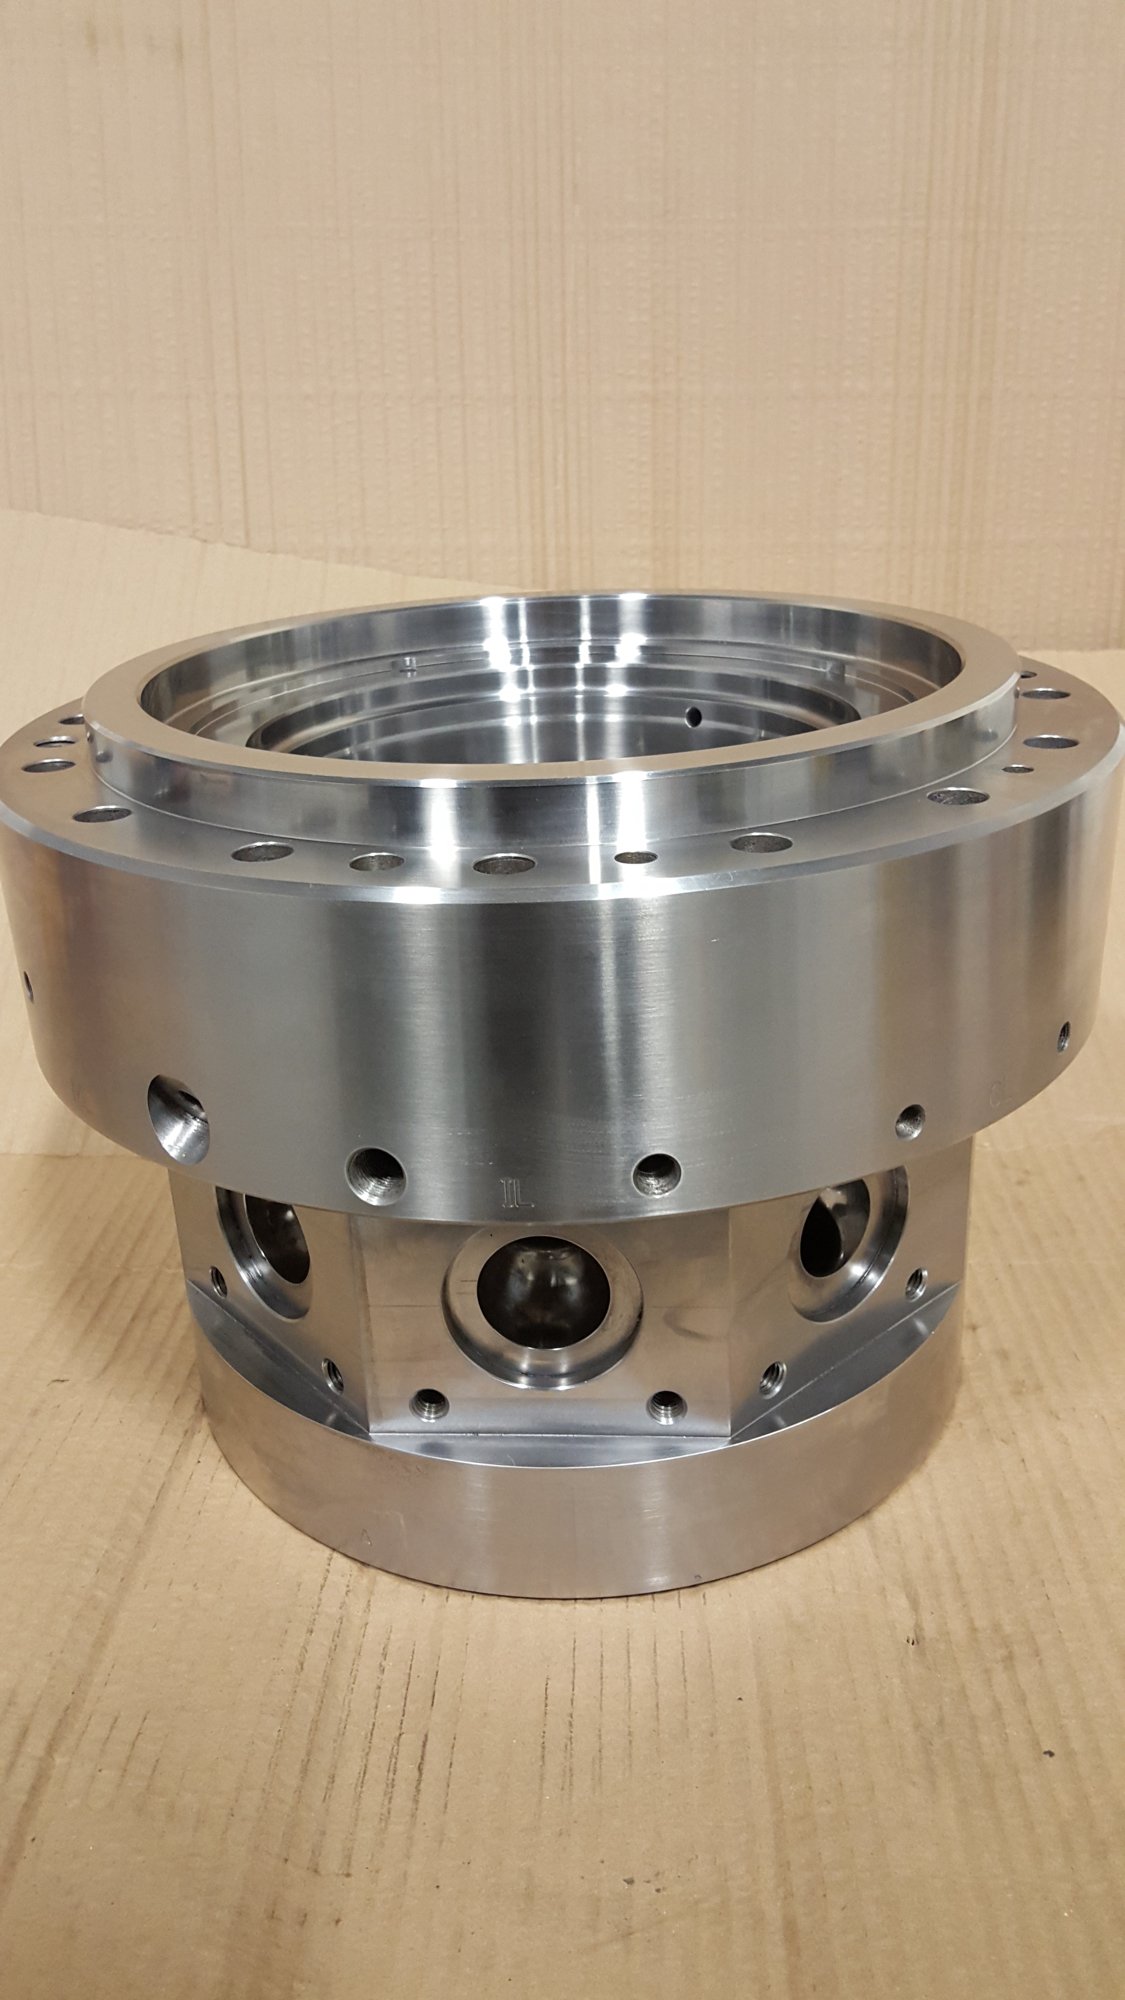
Finished blown film die body, bolt-circle flange above a band of machined side melt ports
Blown film dies: Finished die body, side melt ports below the flange
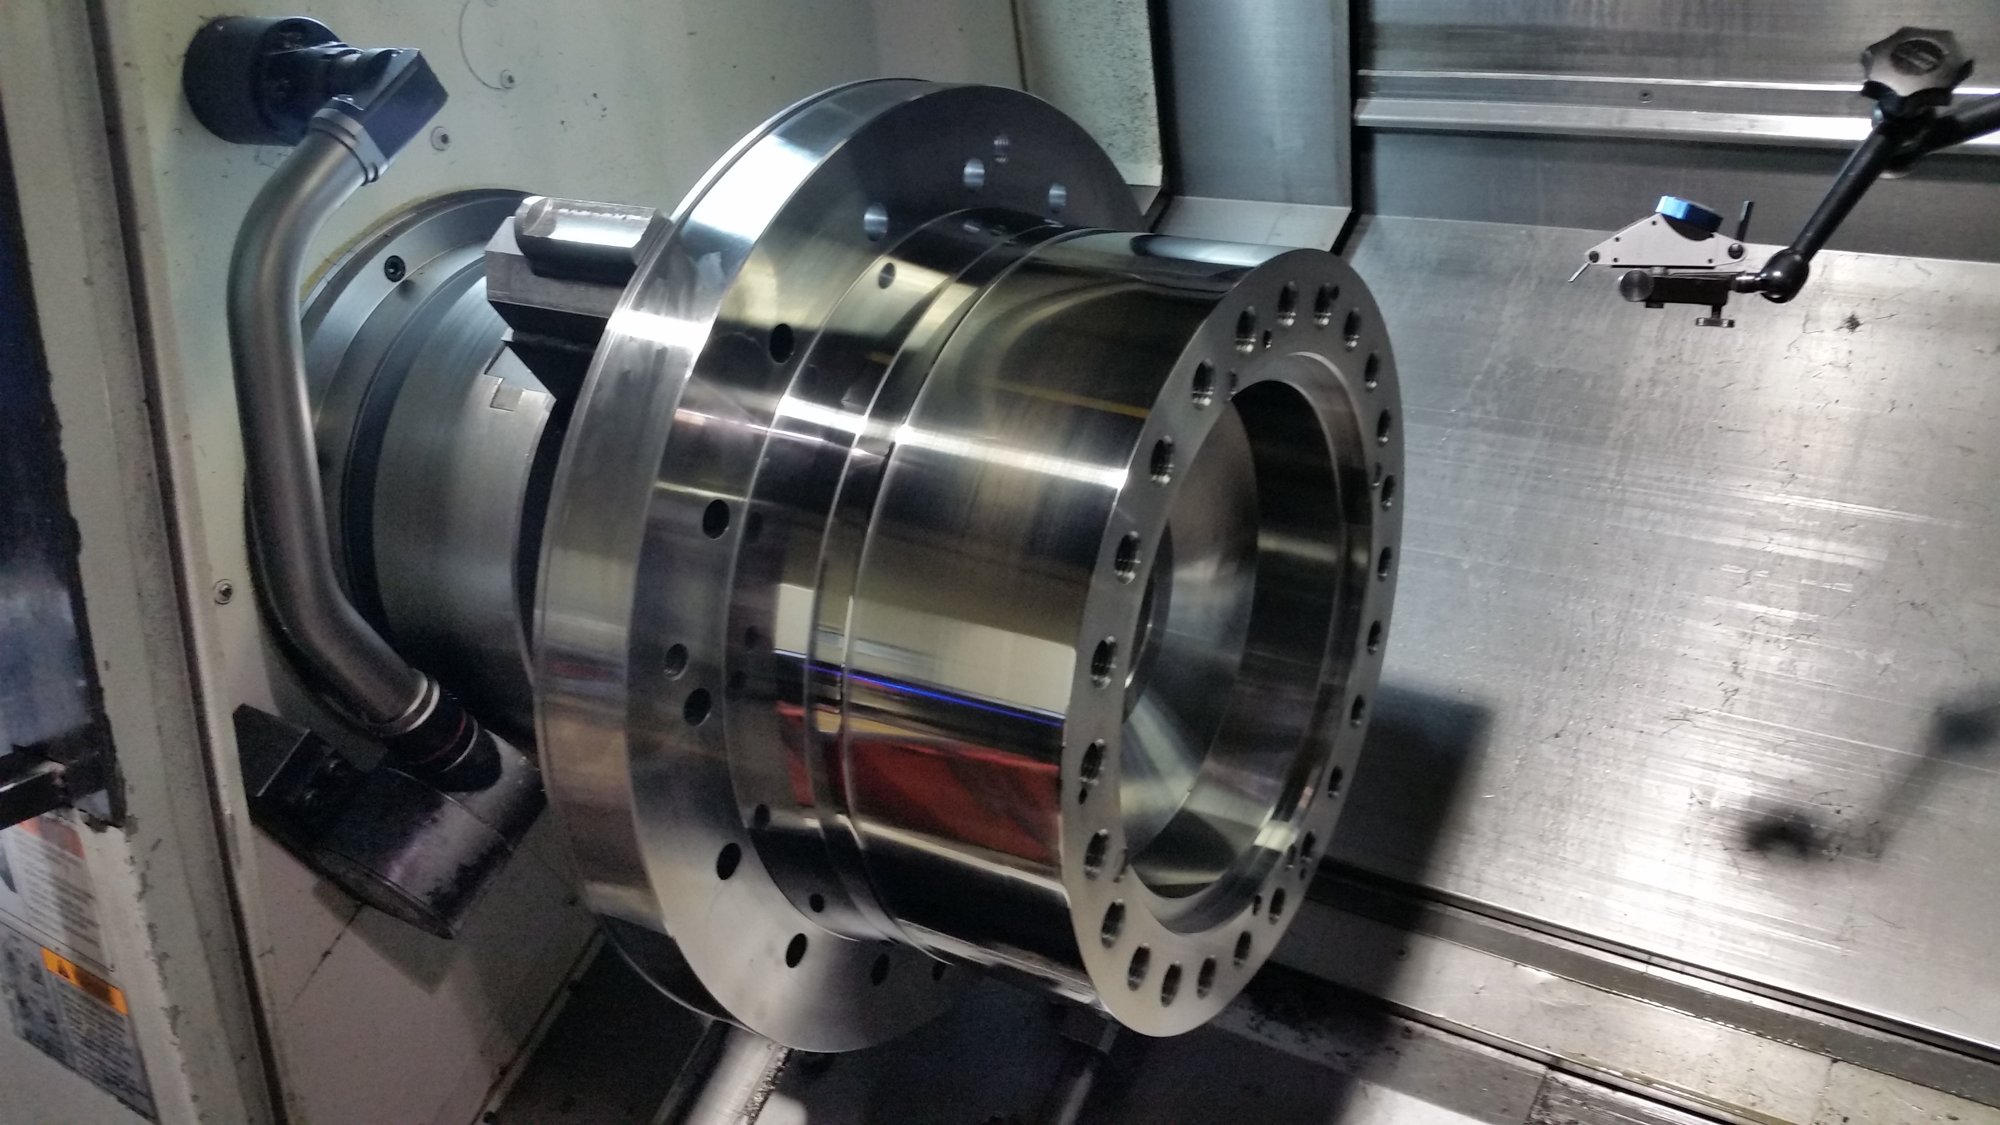
Large flanged housing in the CNC lathe, bolt circle drilled and the bore finish-turned
Turning and production: Flanged housing in the CNC lathe, bore finish-turned
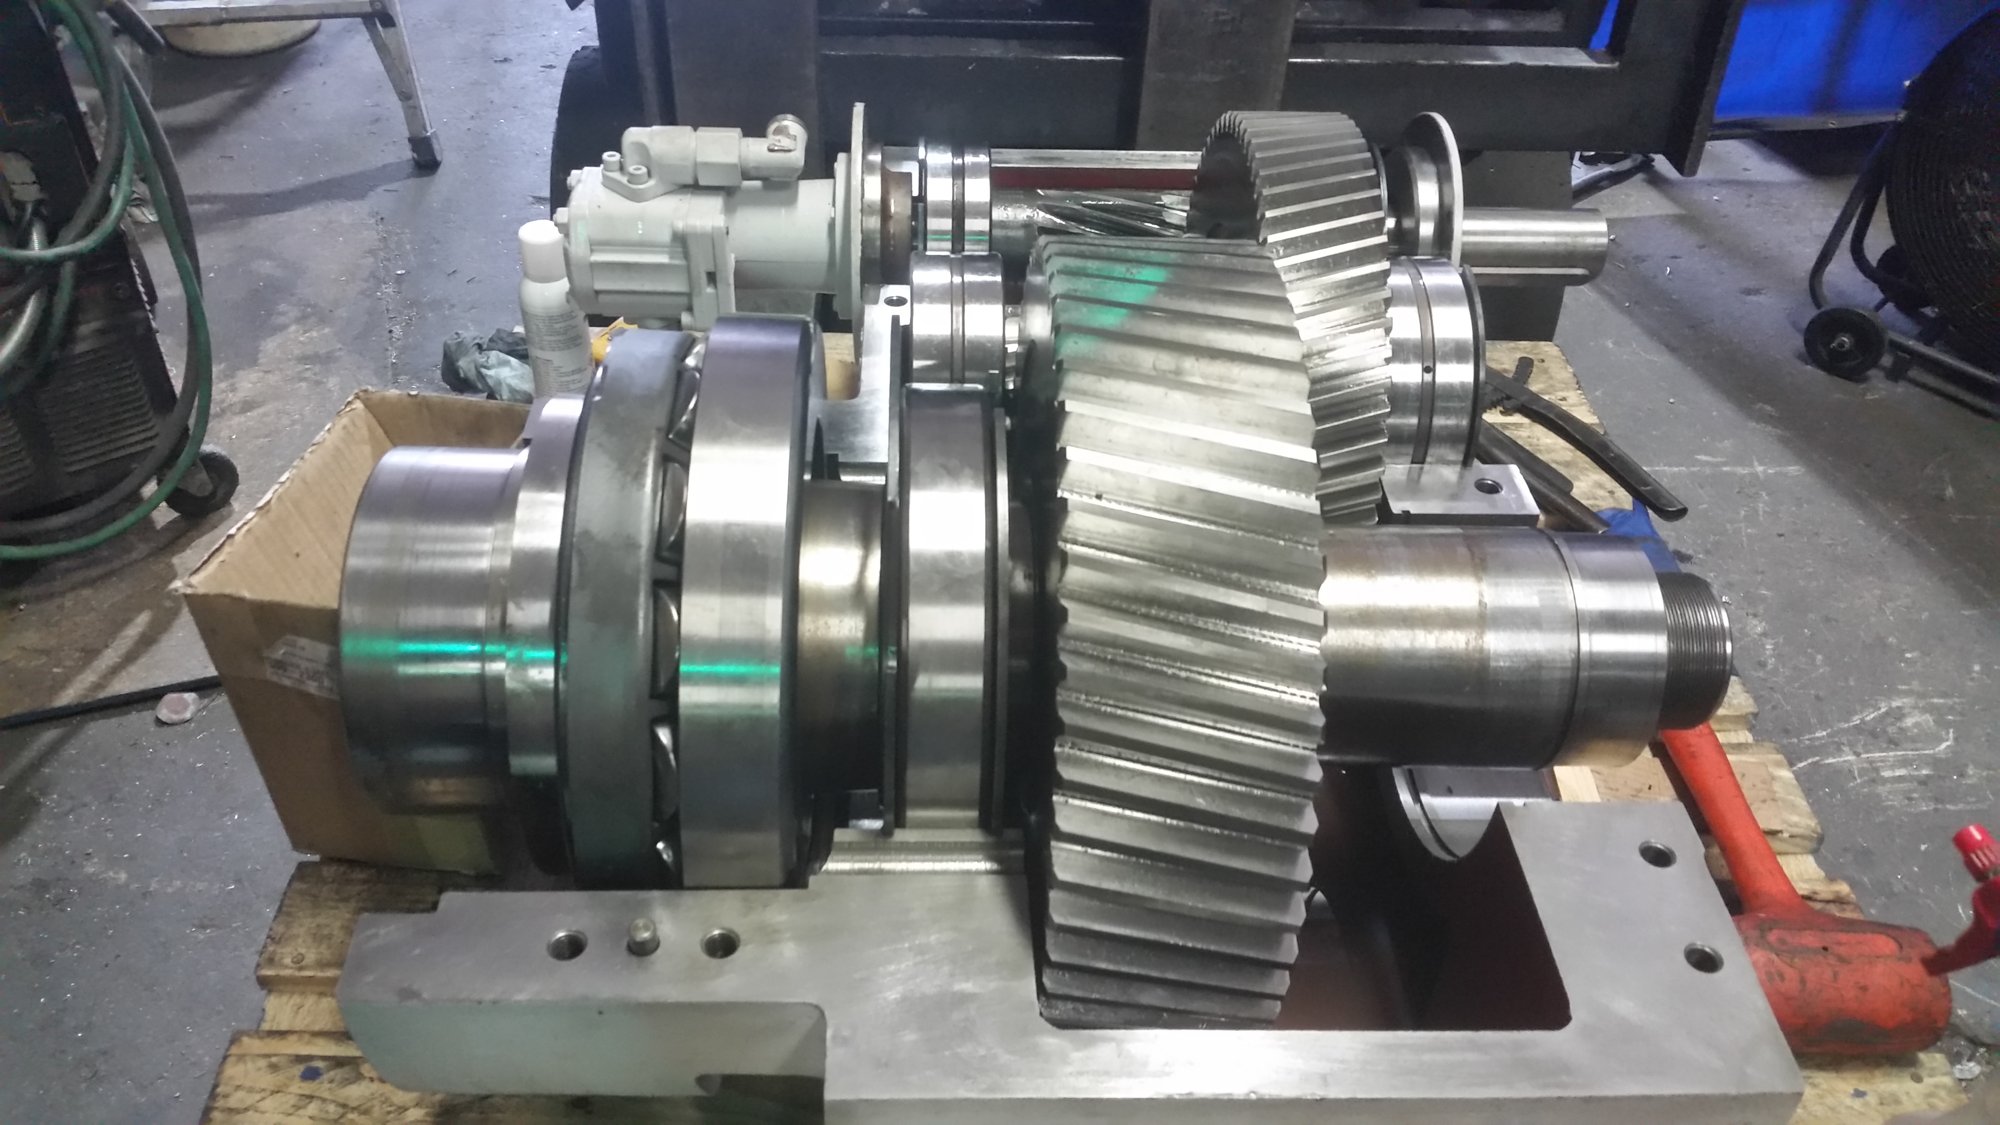
Gearbox gear train assembled on the stand, large helical gear meshed with its pinion shaft and bearing stack
Gearbox repair: Gear train on the stand, helical gear meshed to its pinion
Long housing on the boring mill, flange face and bolt circle finished around the bore
Large machining: Long housing on the boring mill, flange face finished
Flange Adapter for Extruder out of Inconel 718
Extruder parts: Flange adapter for an extruder, Inconel 718
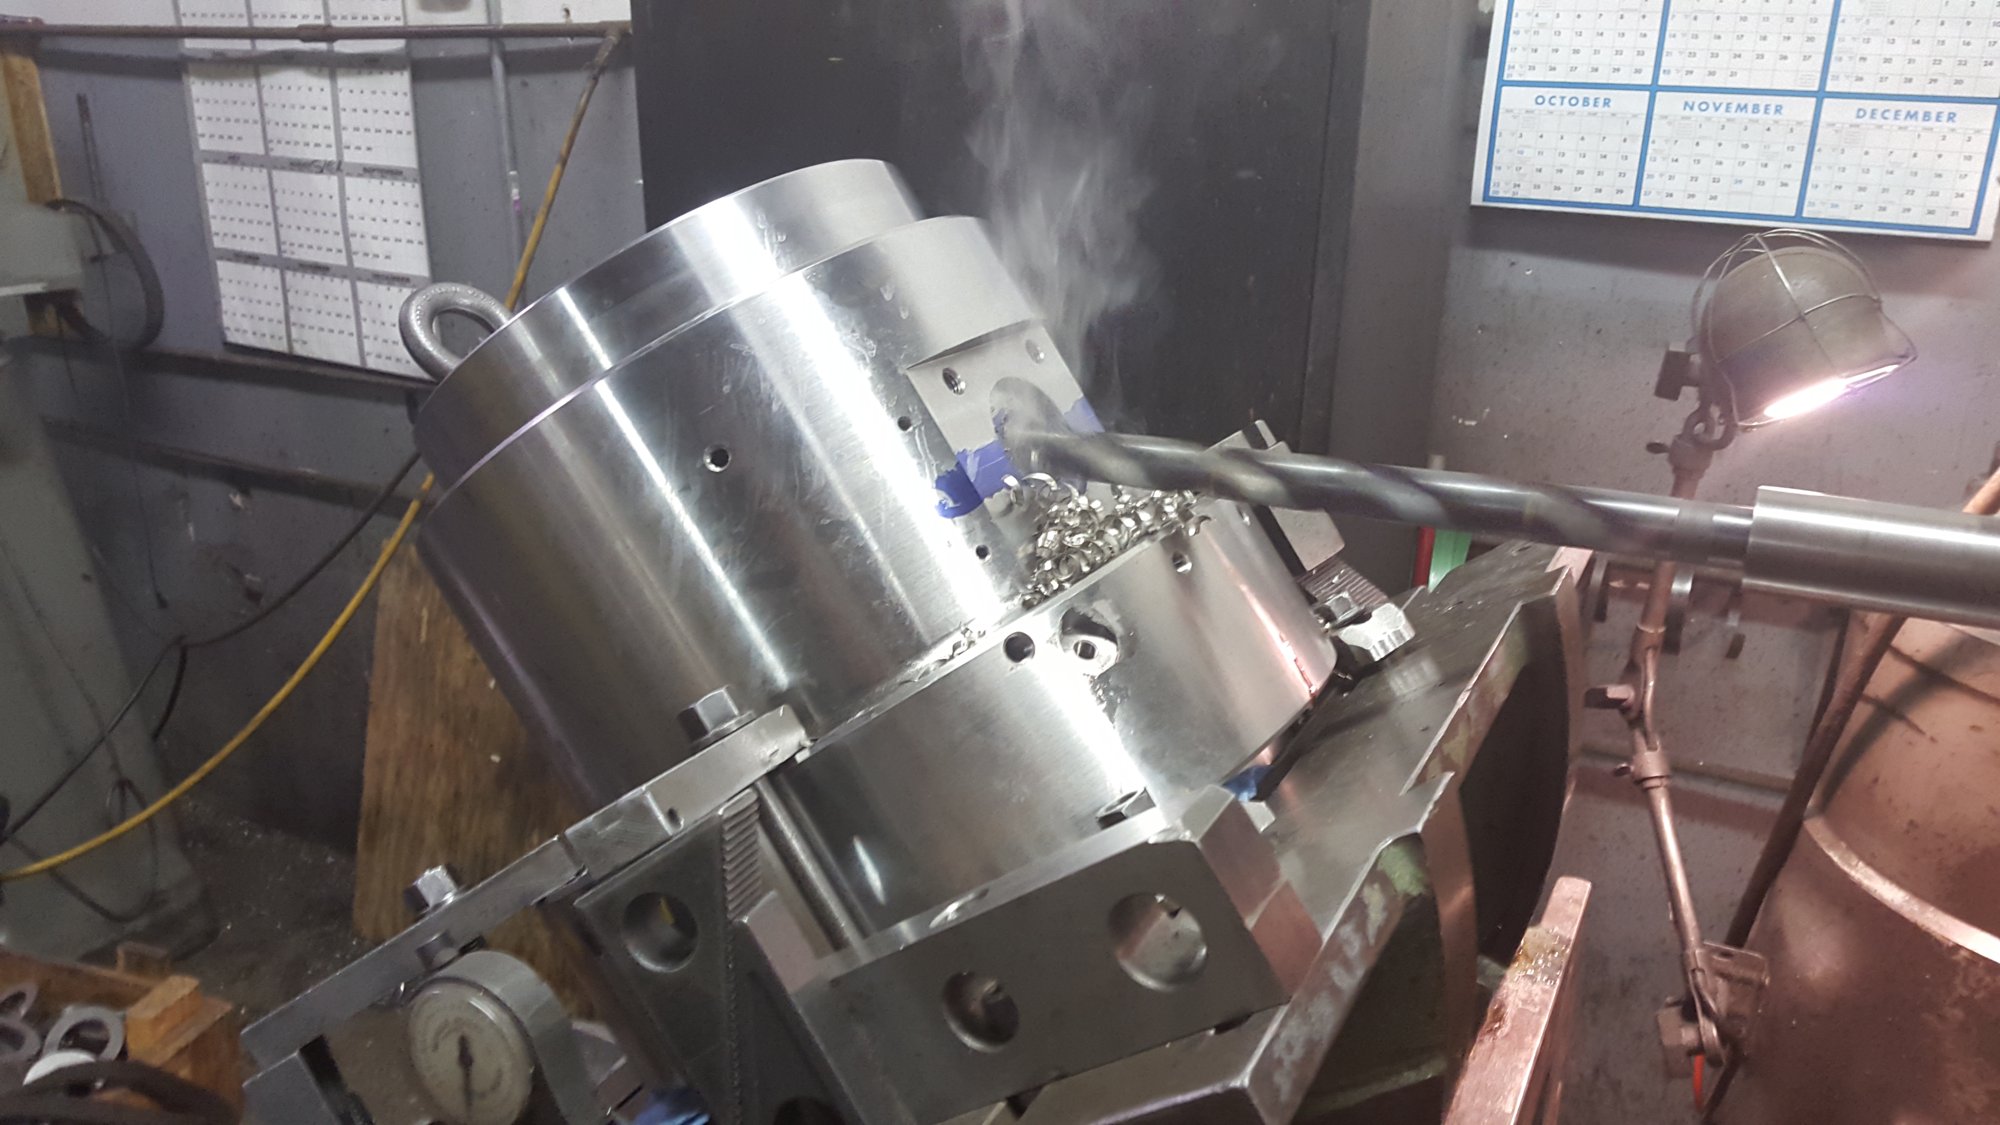
Large die body clamped on the tilting fixture, boring bar cutting with coolant steaming off the work
Blown film dies: Die body on the tilting fixture, boring bar in the cut
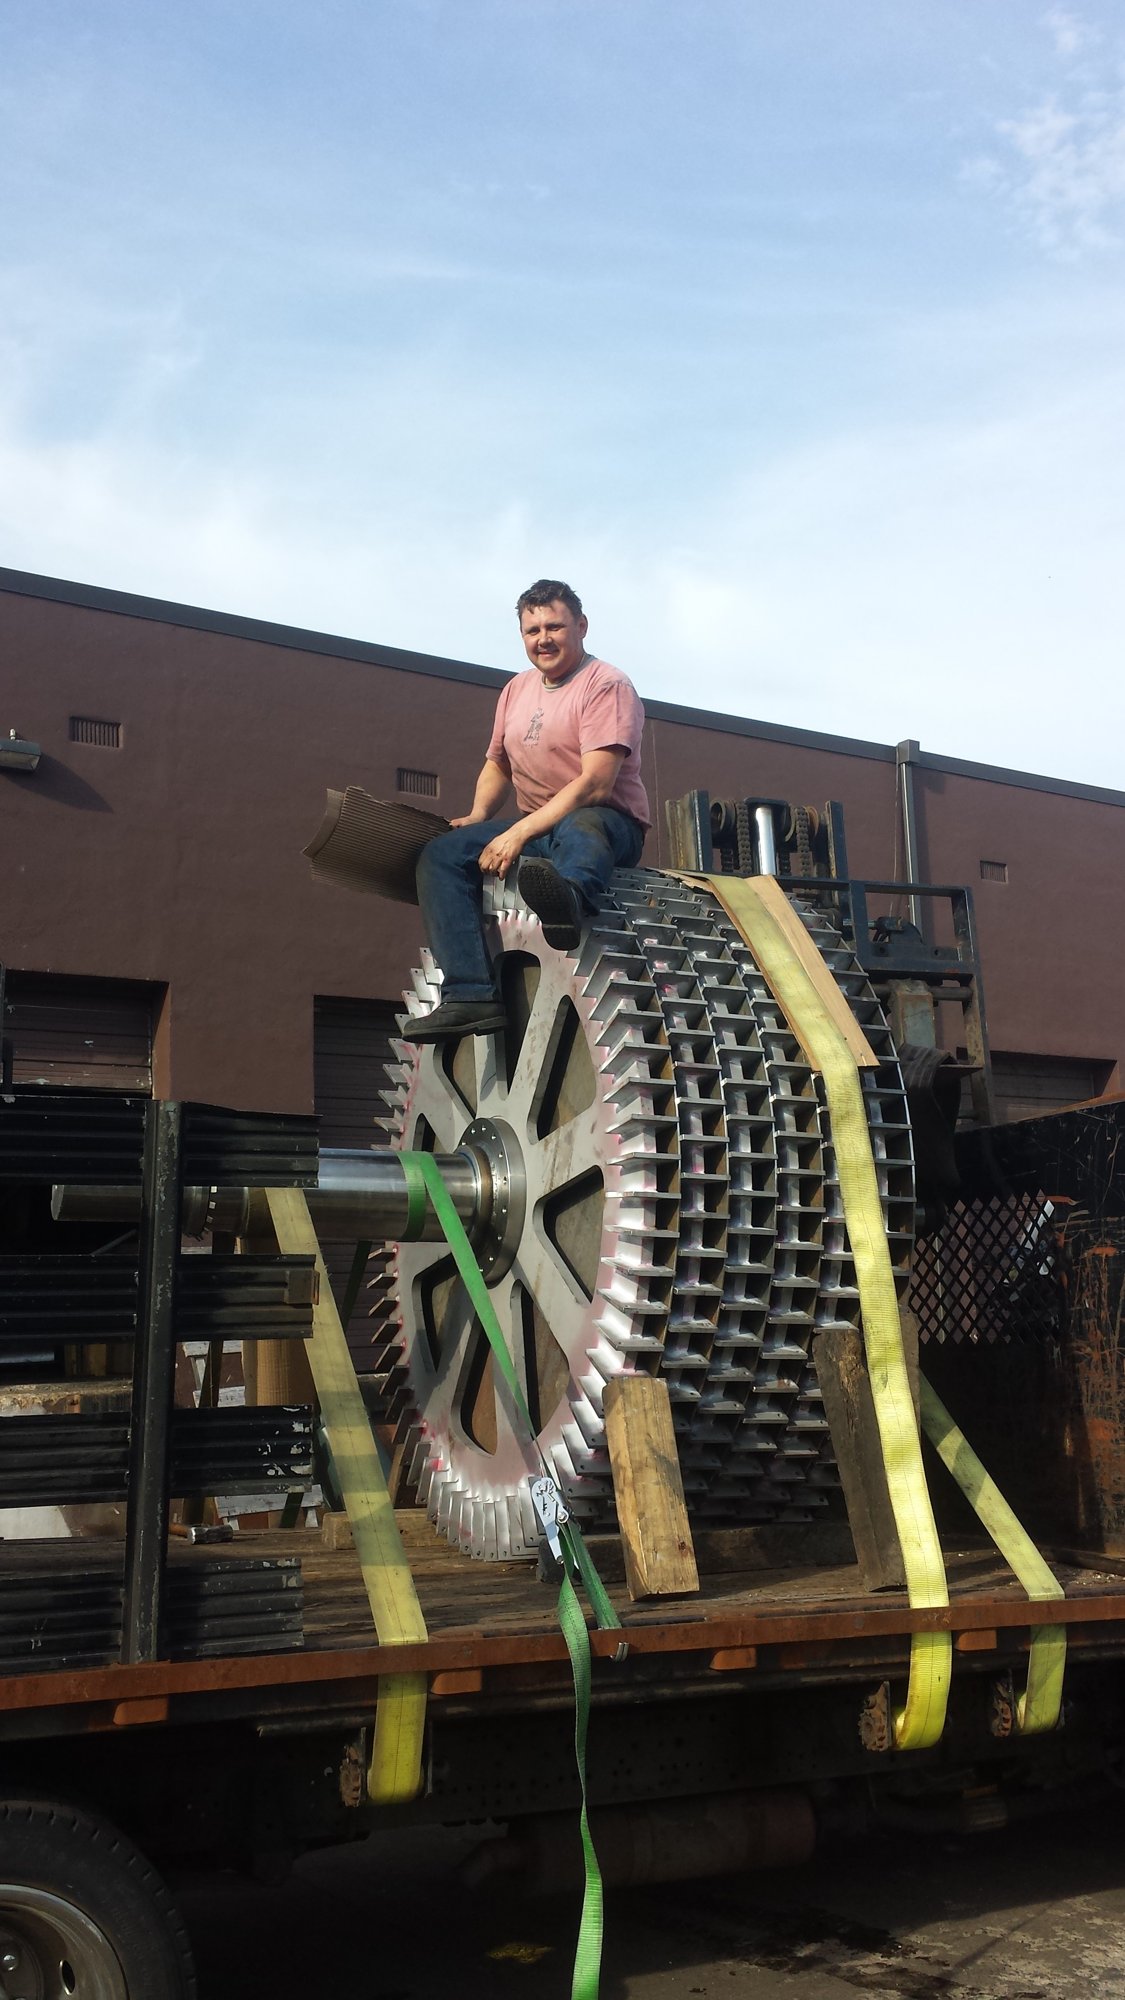
Large spoked spur gear strapped to the flatbed, a man seated on the rim for scale
Fabrication and shipping: The spur gear, with a man on it for scale
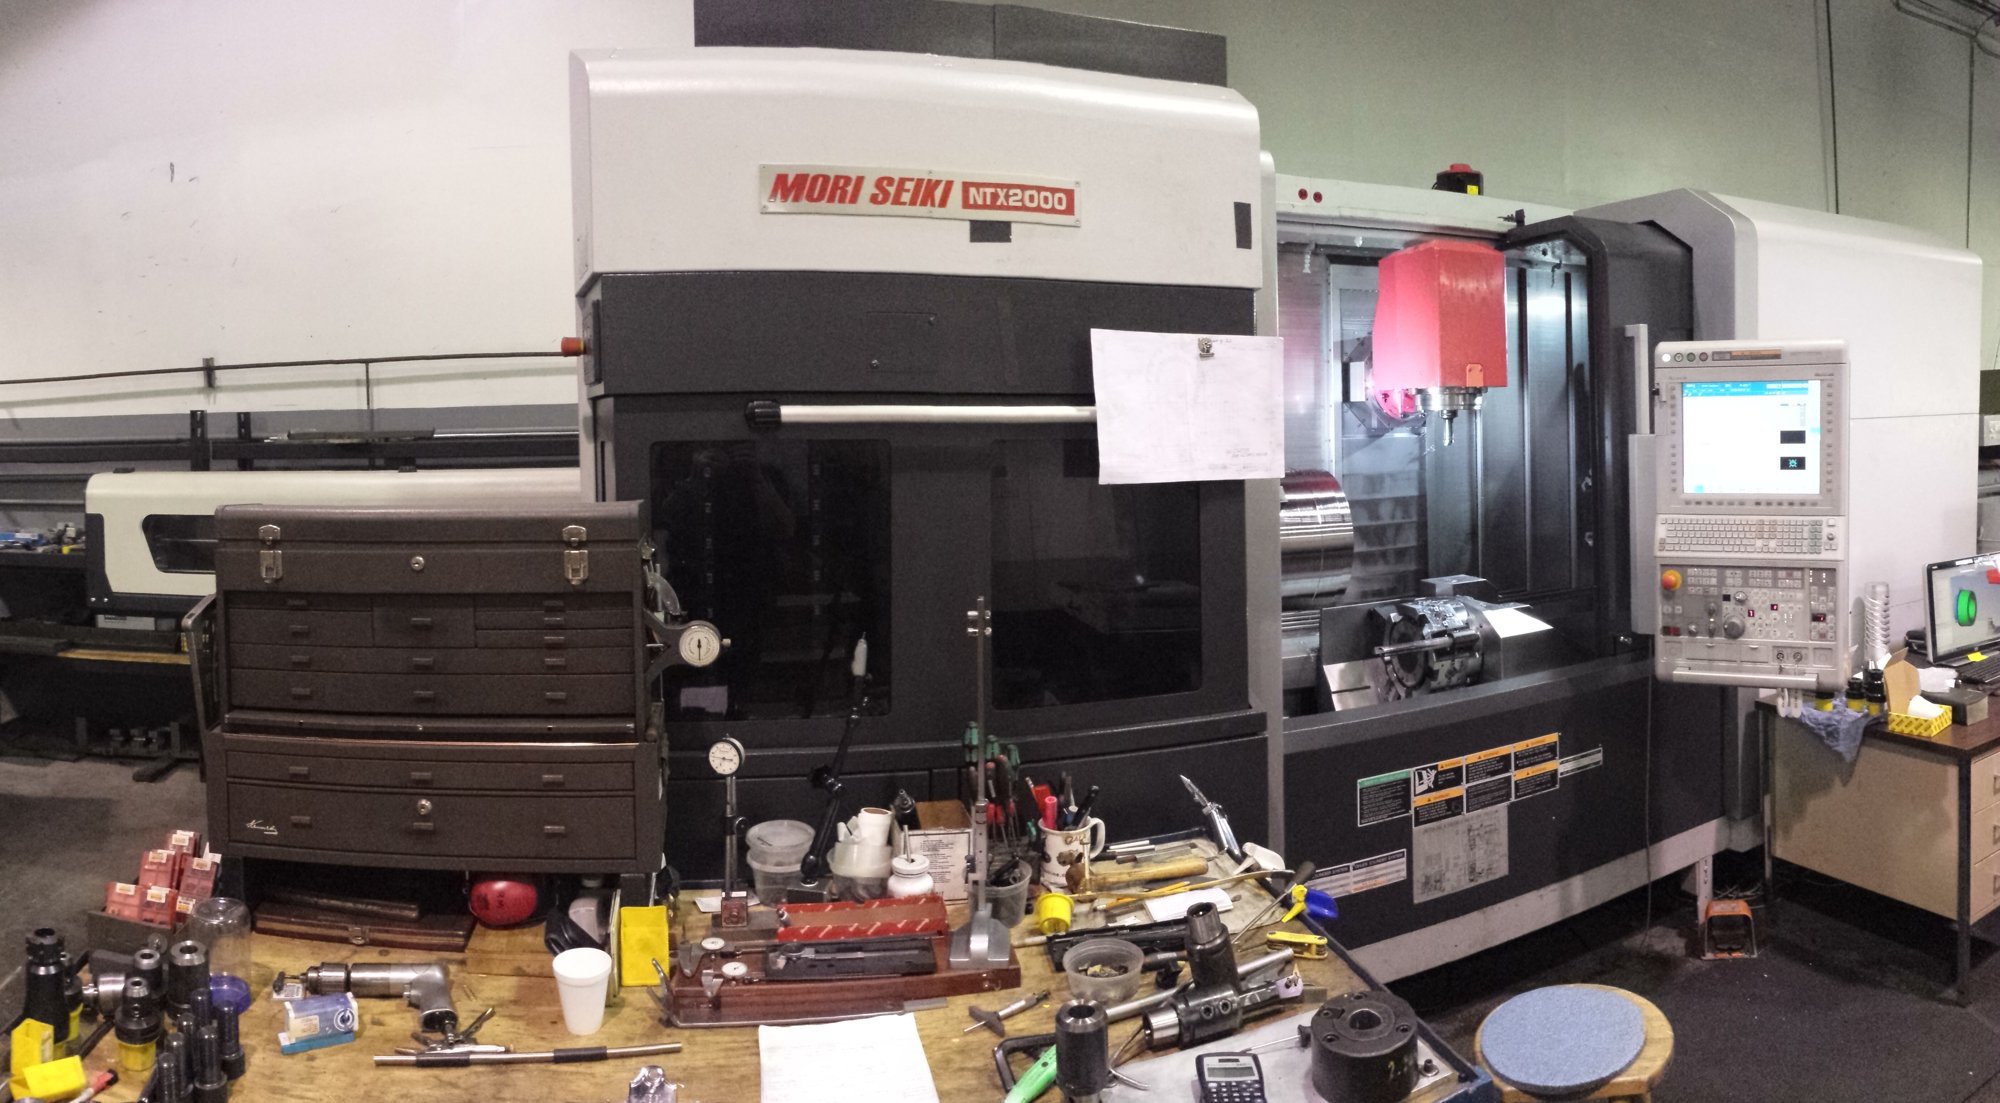
Mori Seiki NTX2000 mill-turn centre on the shop floor with the tool bench alongside
The shop: Mori Seiki NTX2000 mill-turn
Angled milling head cutting the spiral flow channels into a mandrel on the mill-turn
One die, start to finish (7 of 10): The head tilts over to cut the channel geometry
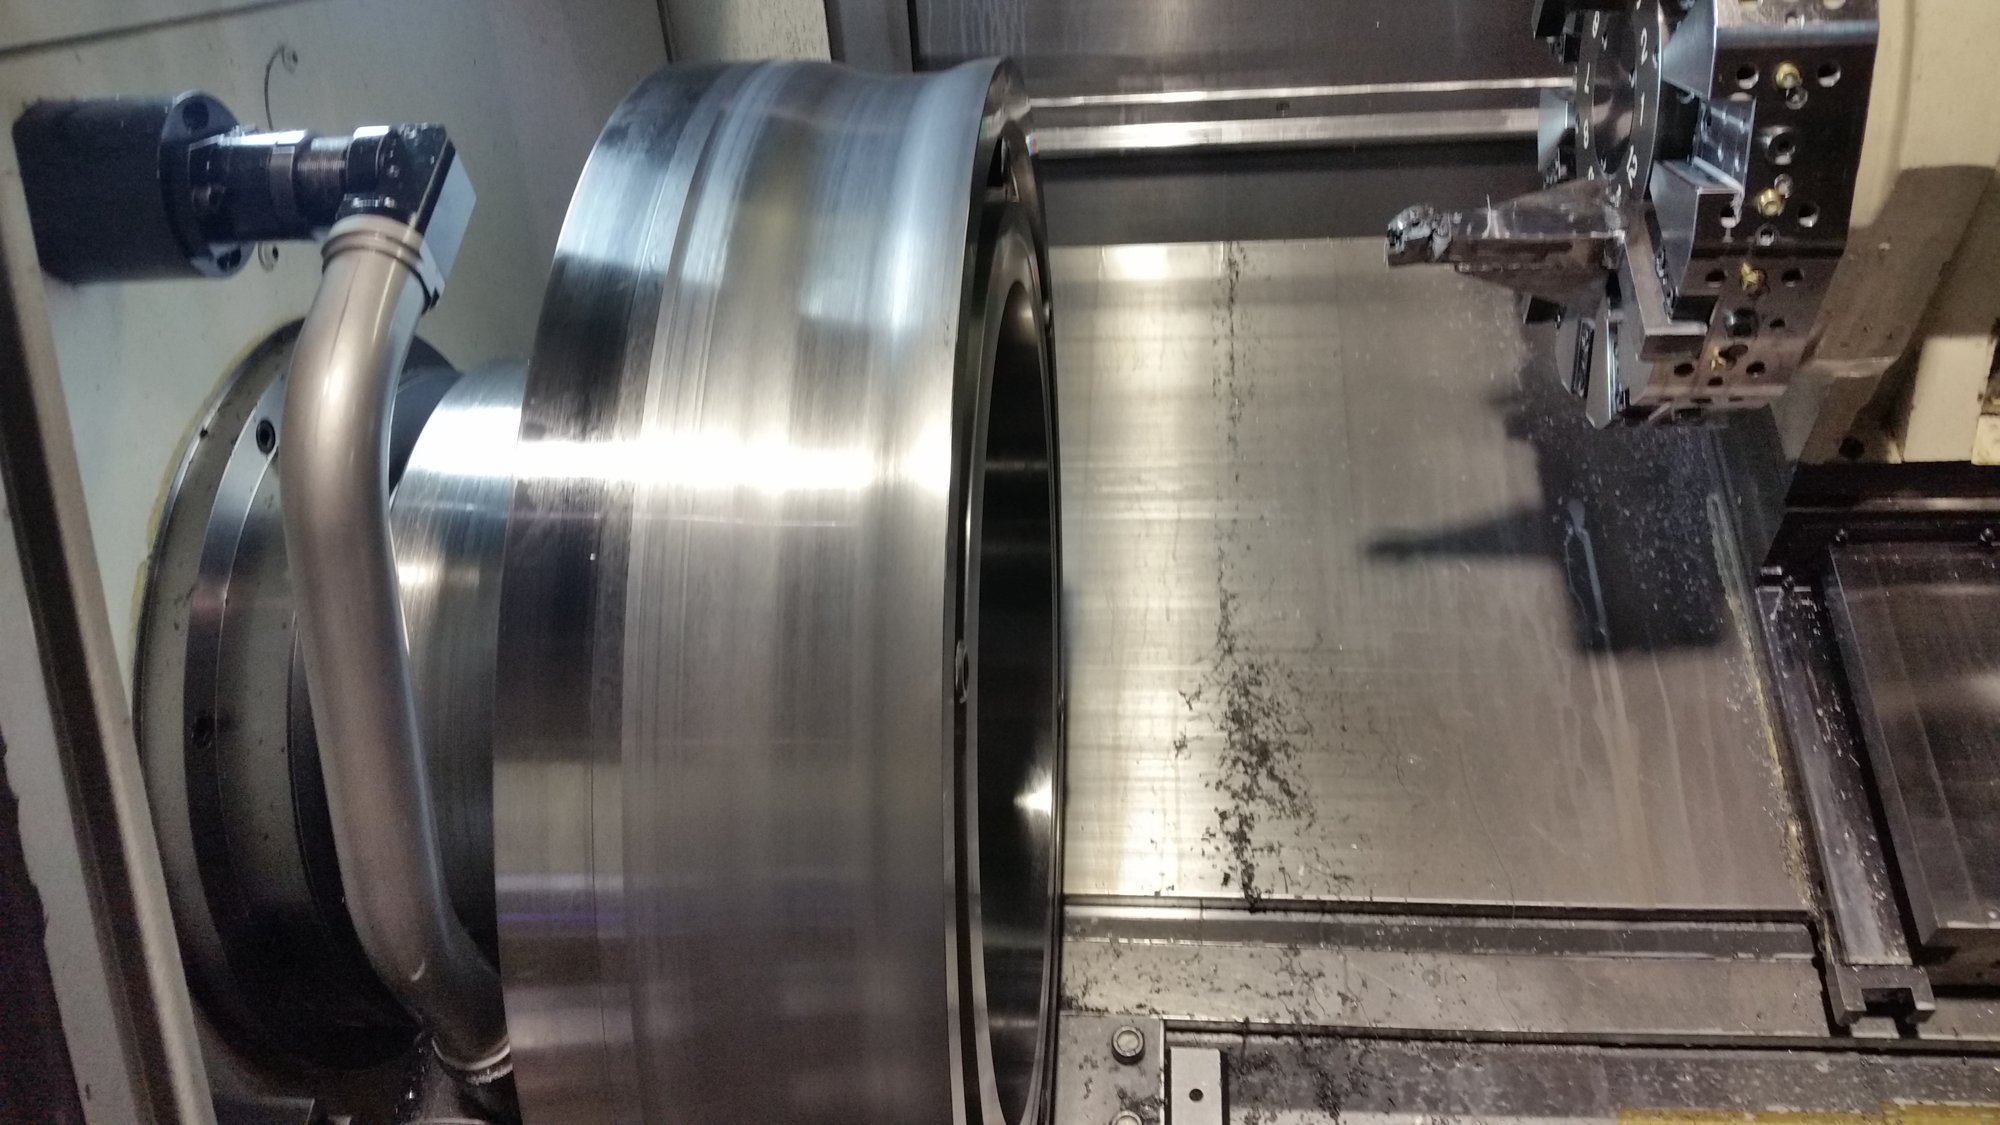
End of a large roll body bored in the CNC lathe, counterbore and face finished
Turning and production: Large roll body, counterbore and face finished
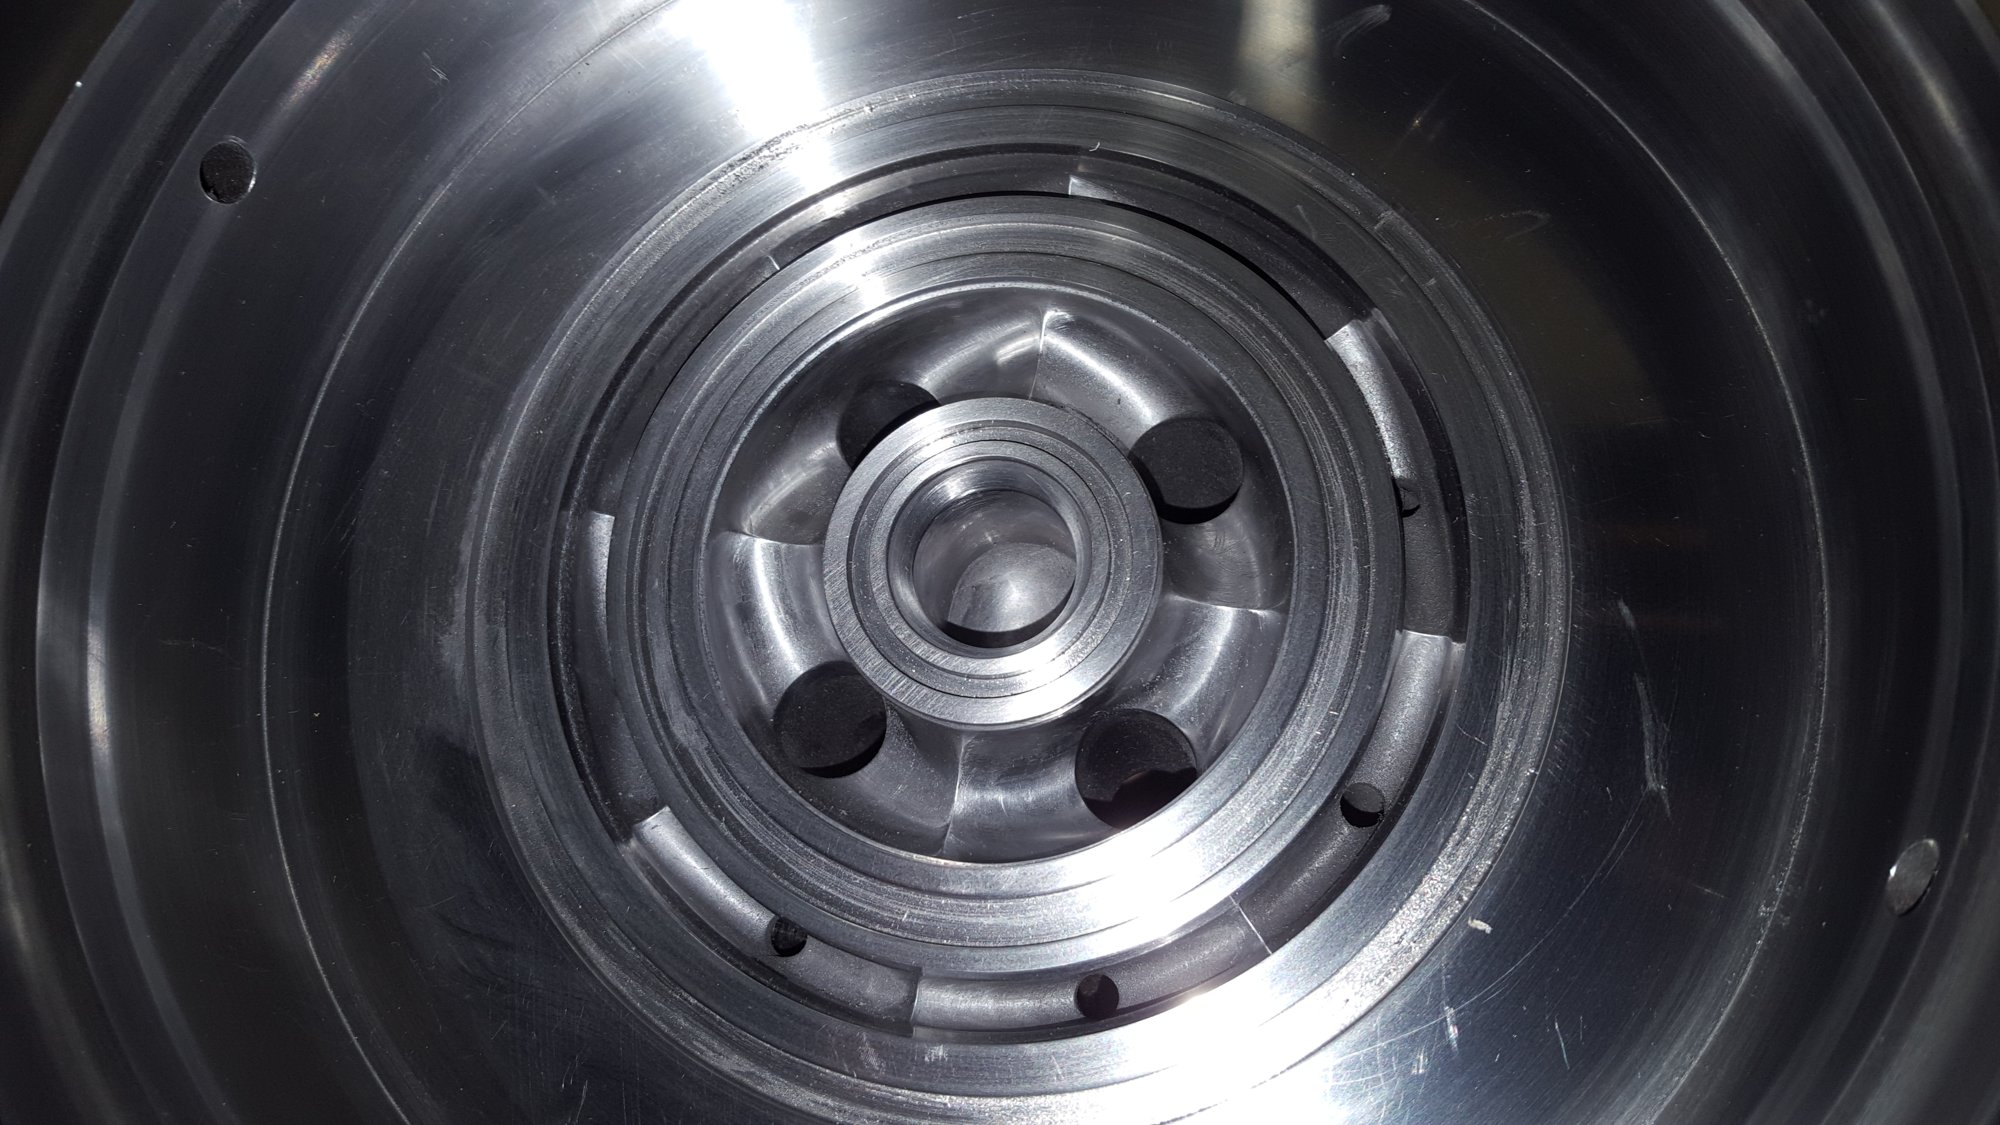
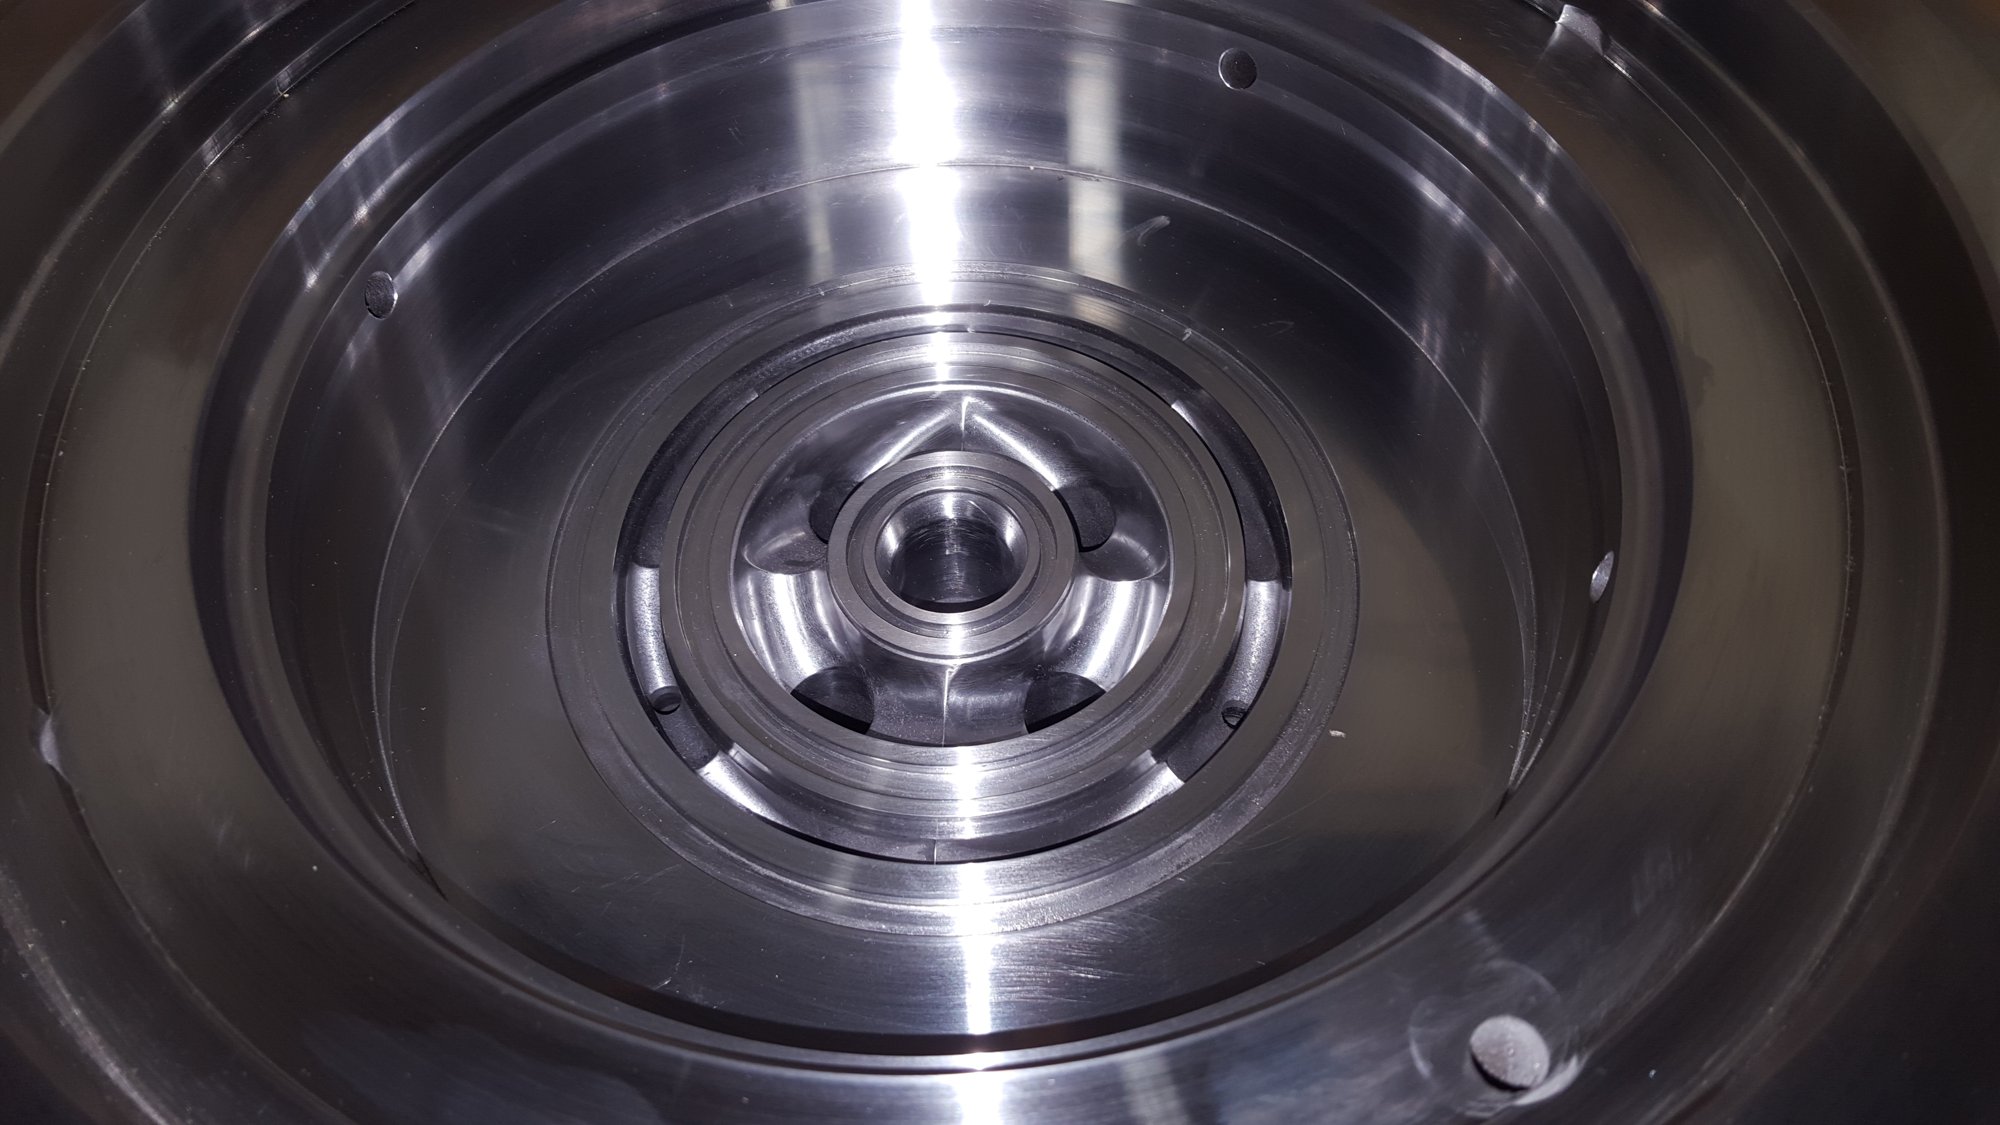
Inside a die flow distributor, radial vanes and ports machined around the concentric centre boss
Blown film dies: Inside a flow distributor, vanes and ports around the boss
Machinist handling a large machined steel plate, centre bore opened and keyed inserts fitted
Large machining: Large plate, centre bore opened and keyed inserts fitted
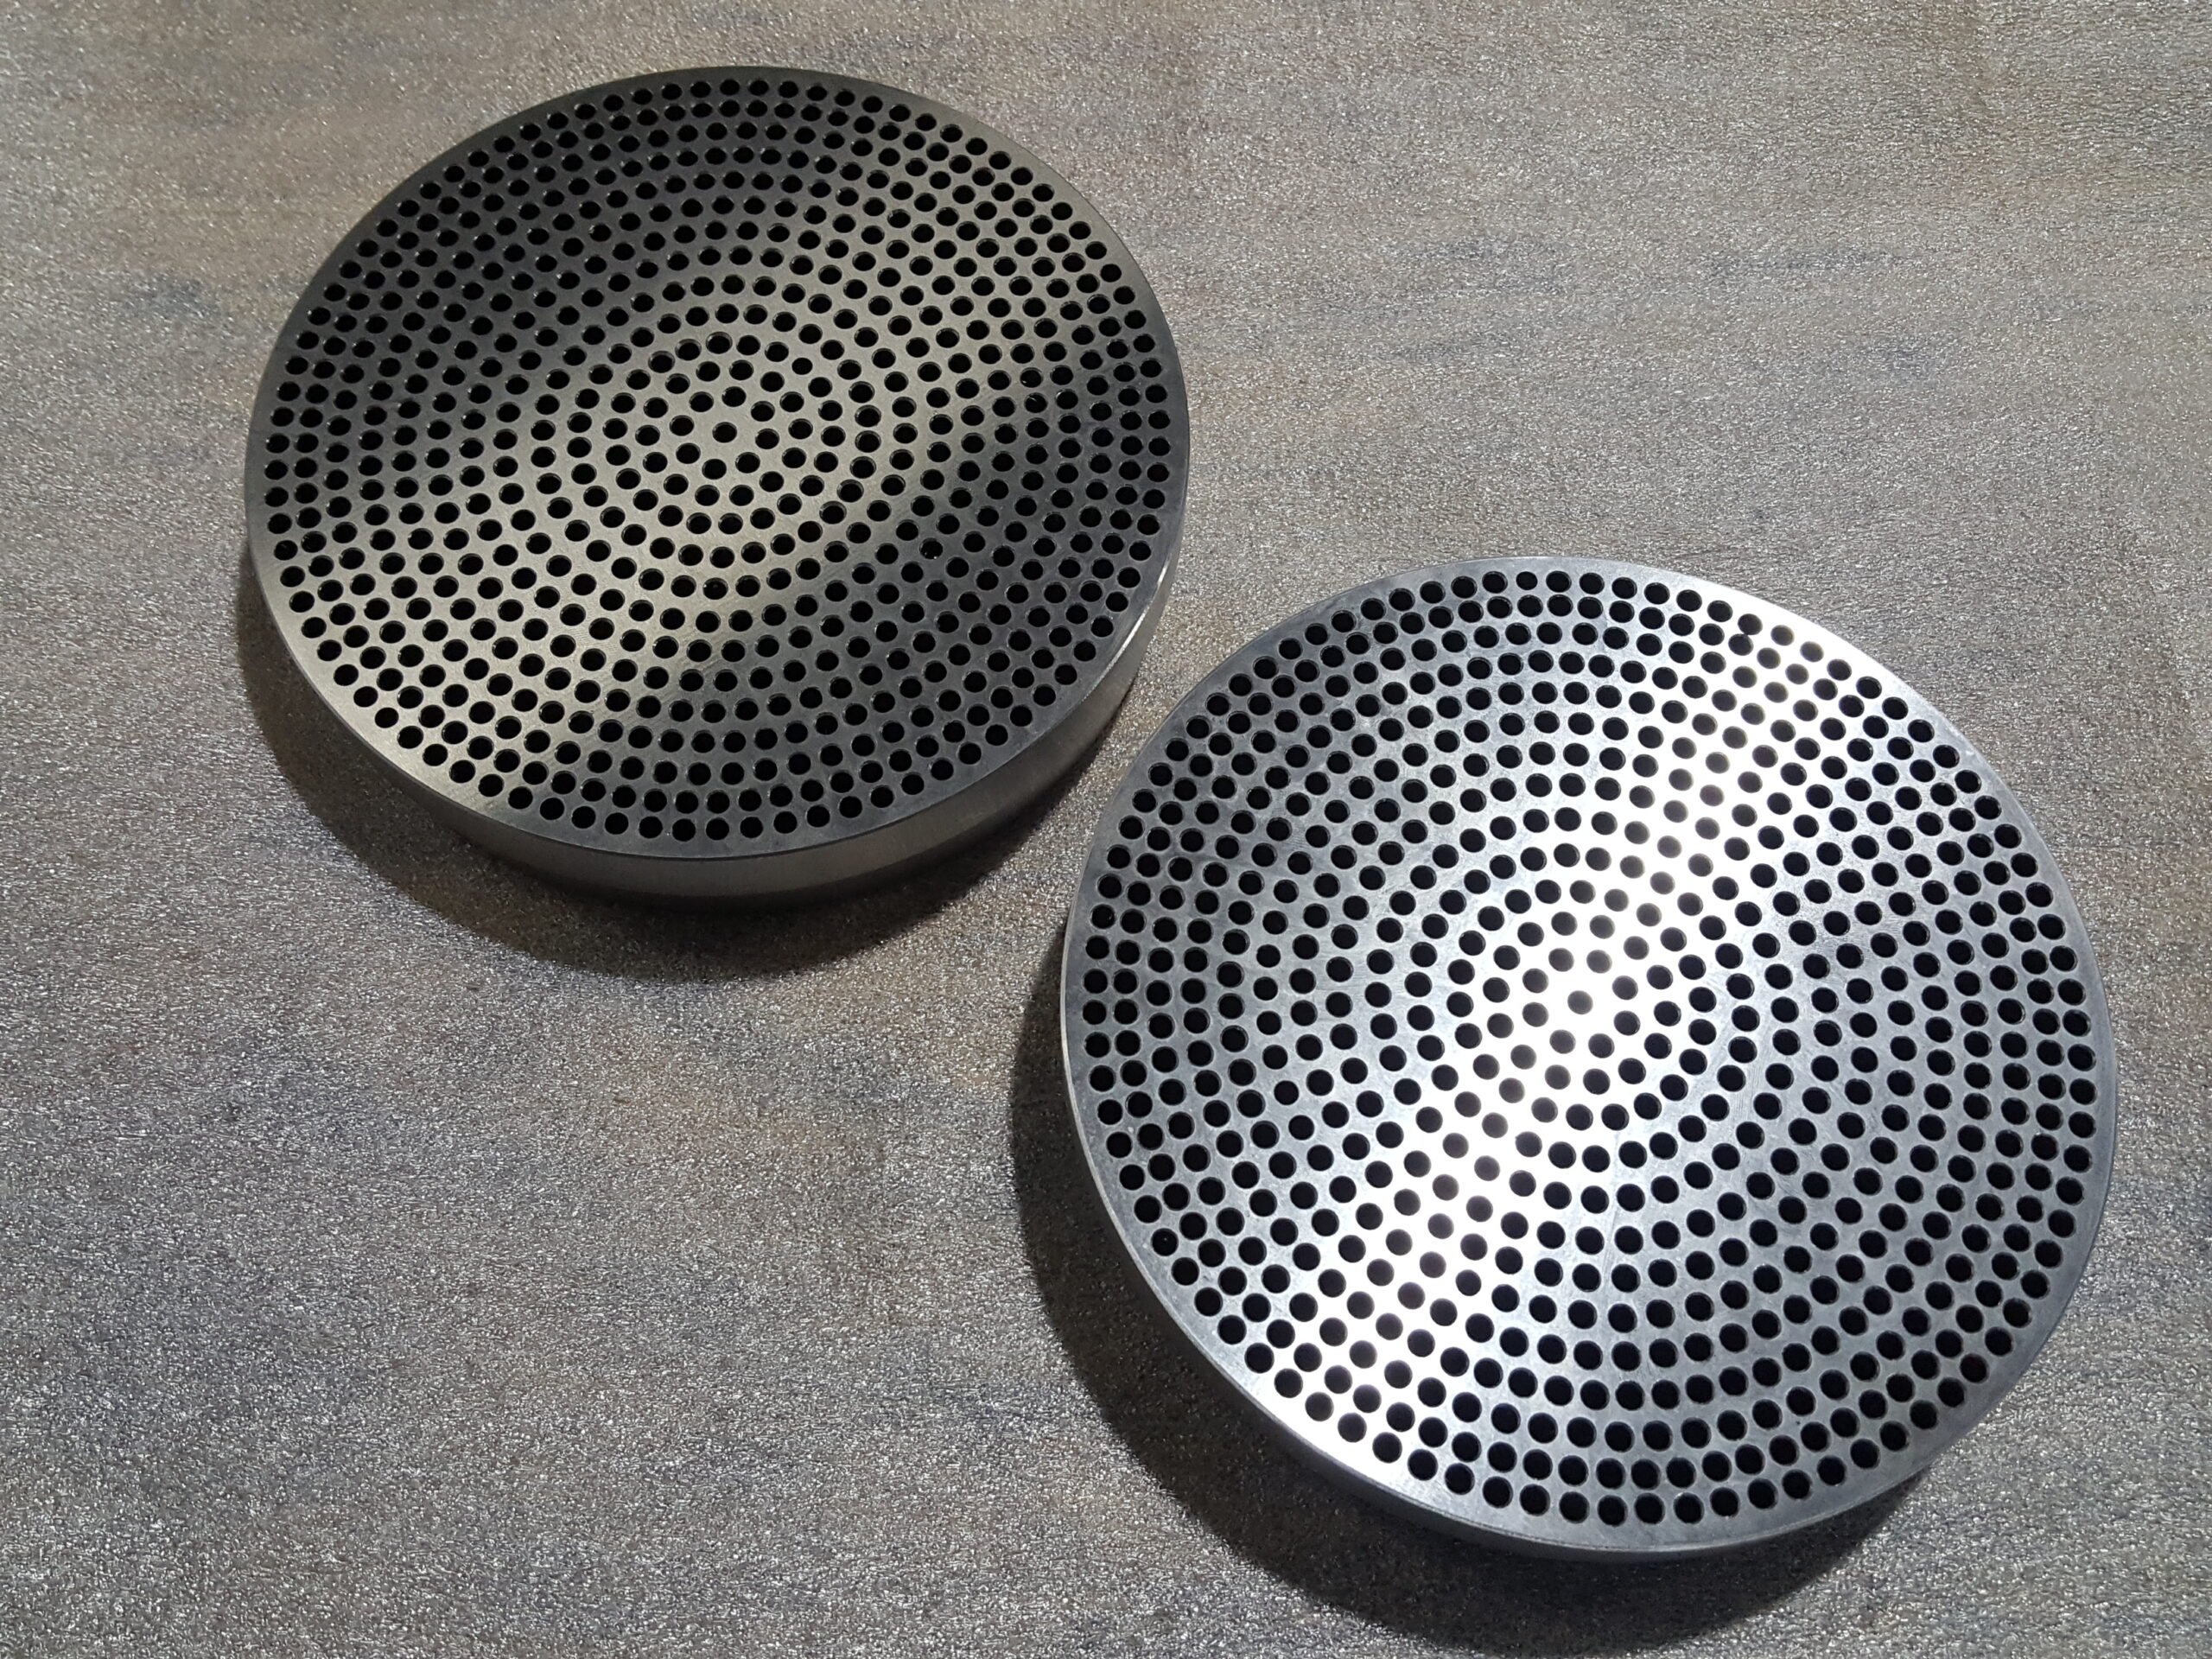
Round Breaker Plate Set out of 15-5 Ph Stainless
Extruder parts: Pair of drilled breaker plates, 15-5 PH stainless
Threaded section cut into a shaft on the manual lathe under the work lamp
Shaft machining: Threading a shaft on the manual lathe
Large cylinder on the honing machine, hone inside the bore working the finish
Bore honing: Hone working the finish inside a large cylinder
Die plate resting on packing foam, teardrop flow port and bolt circle machined into the face
Blown film dies: Die plate with its teardrop flow port and bolt circle
Large plate held in the chuck with pockets and holes milled through, tool head alongside
Large machining: Large plate with pockets and holes milled through
Gear and shaft assembly resting on its housing base, large helical gears and splined coupling
Gearbox repair: Gear and shaft assembly with splined coupling
Large roll body turned on the CNC lathe, outside diameter cut down toward the shoulder
Turning and production: Large roll body turned down toward the shoulder
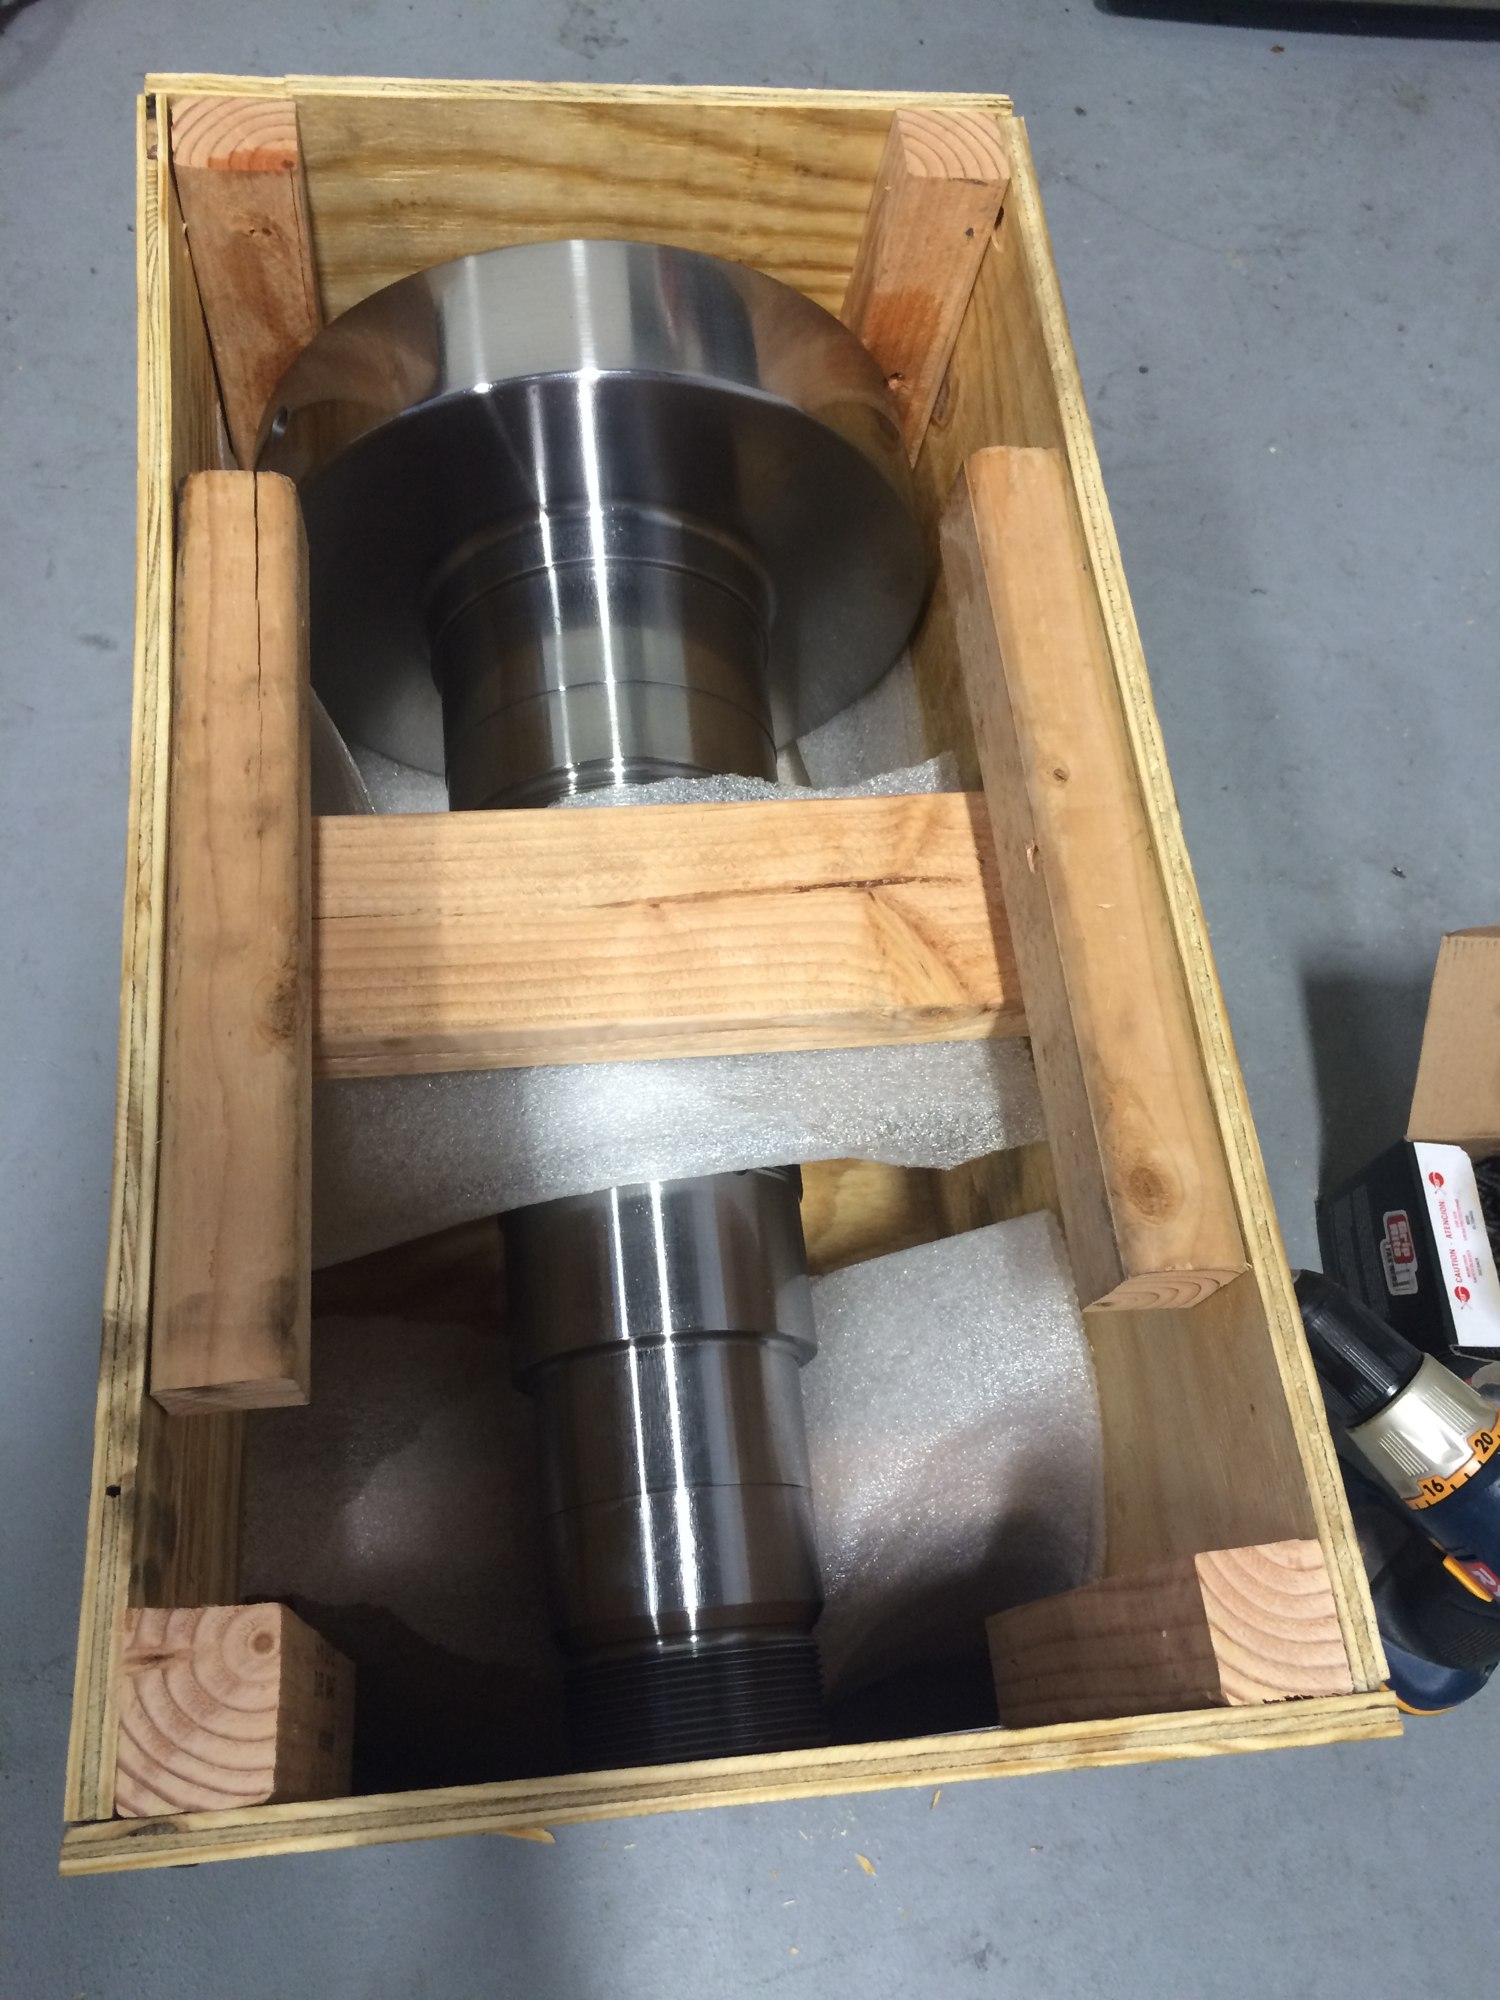
Finished part blocked and braced in its wooden crate, ready to ship
Fabrication and shipping: Finished part braced in its crate, ready to ship
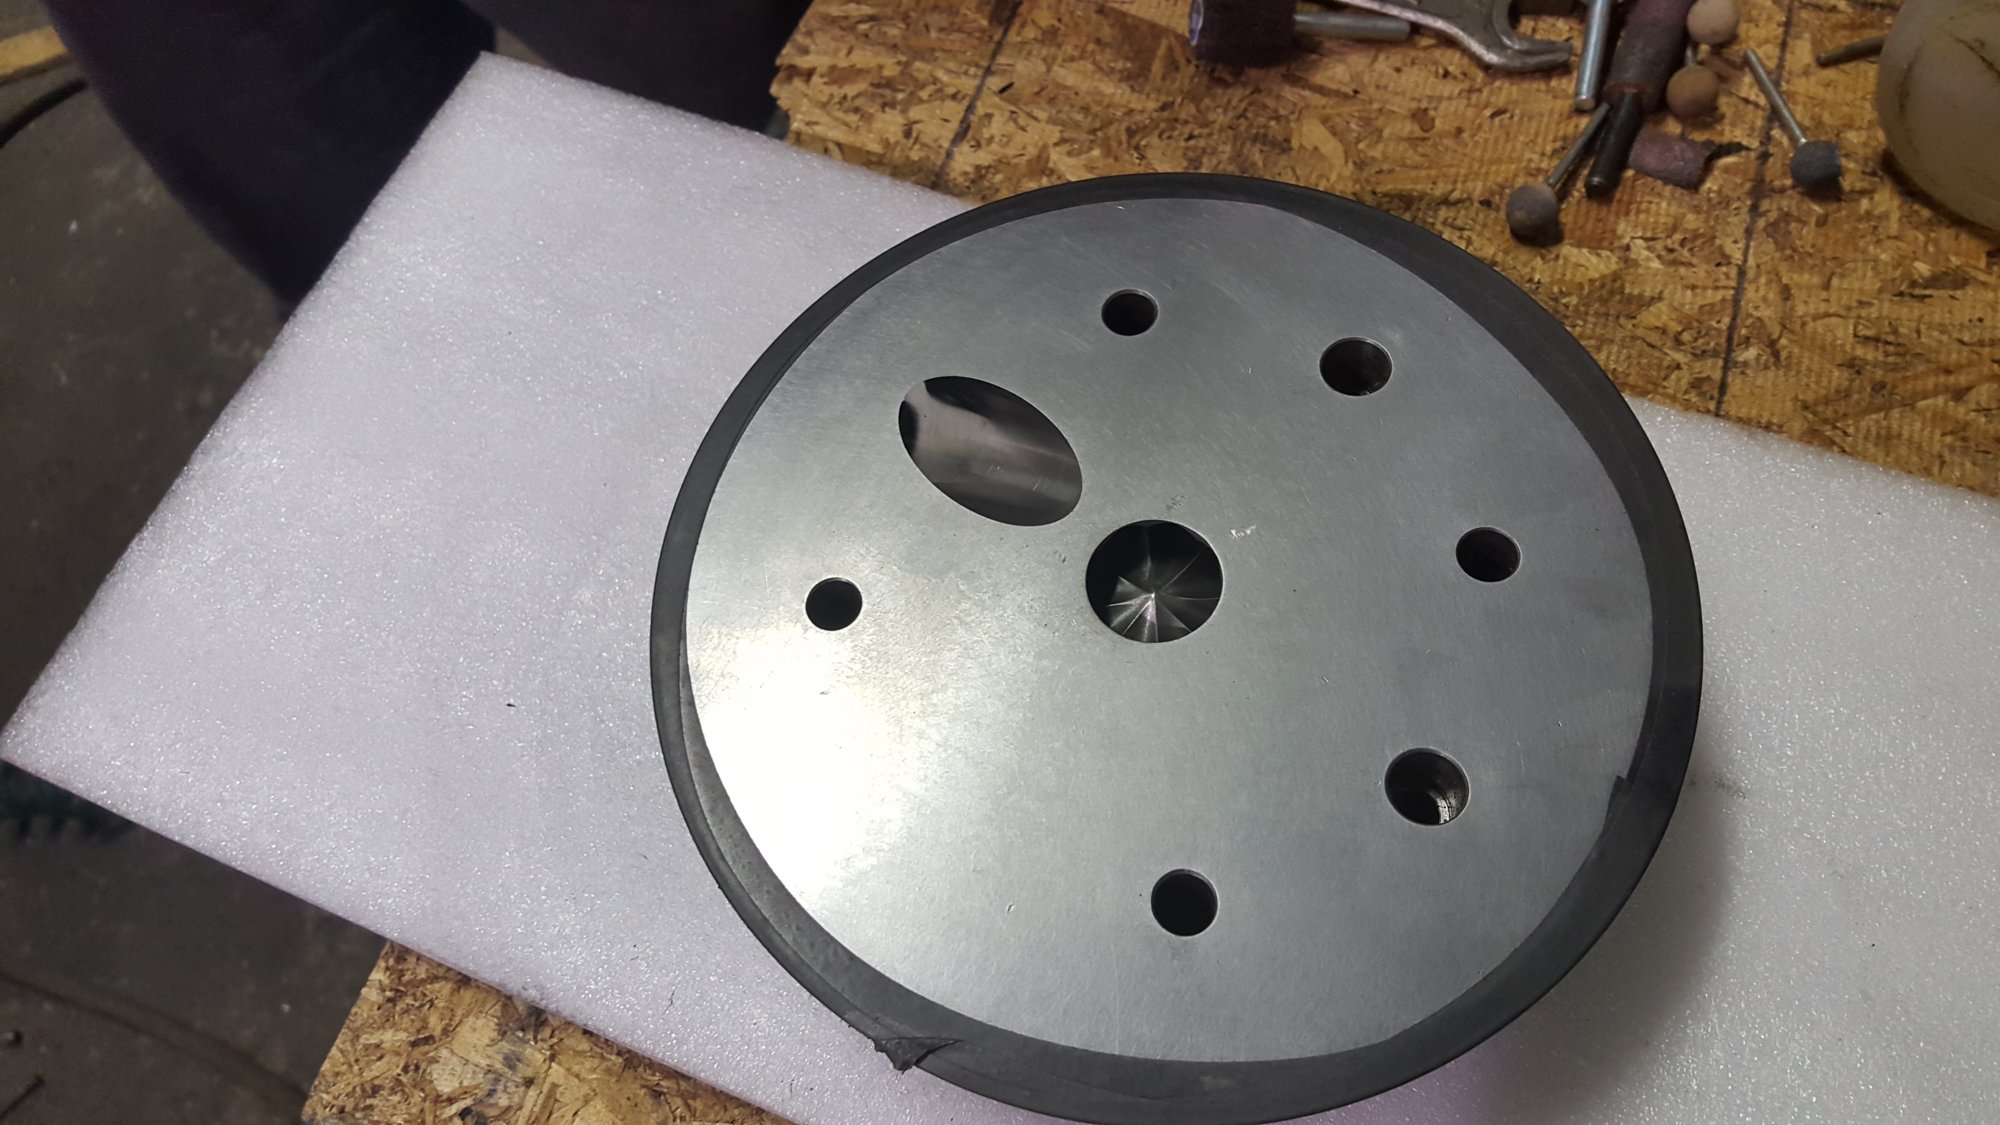
Extrusion die plate with its centre port, bolt holes and elongated melt slot machined through
Blown film dies: Die plate, centre port and elongated melt slot
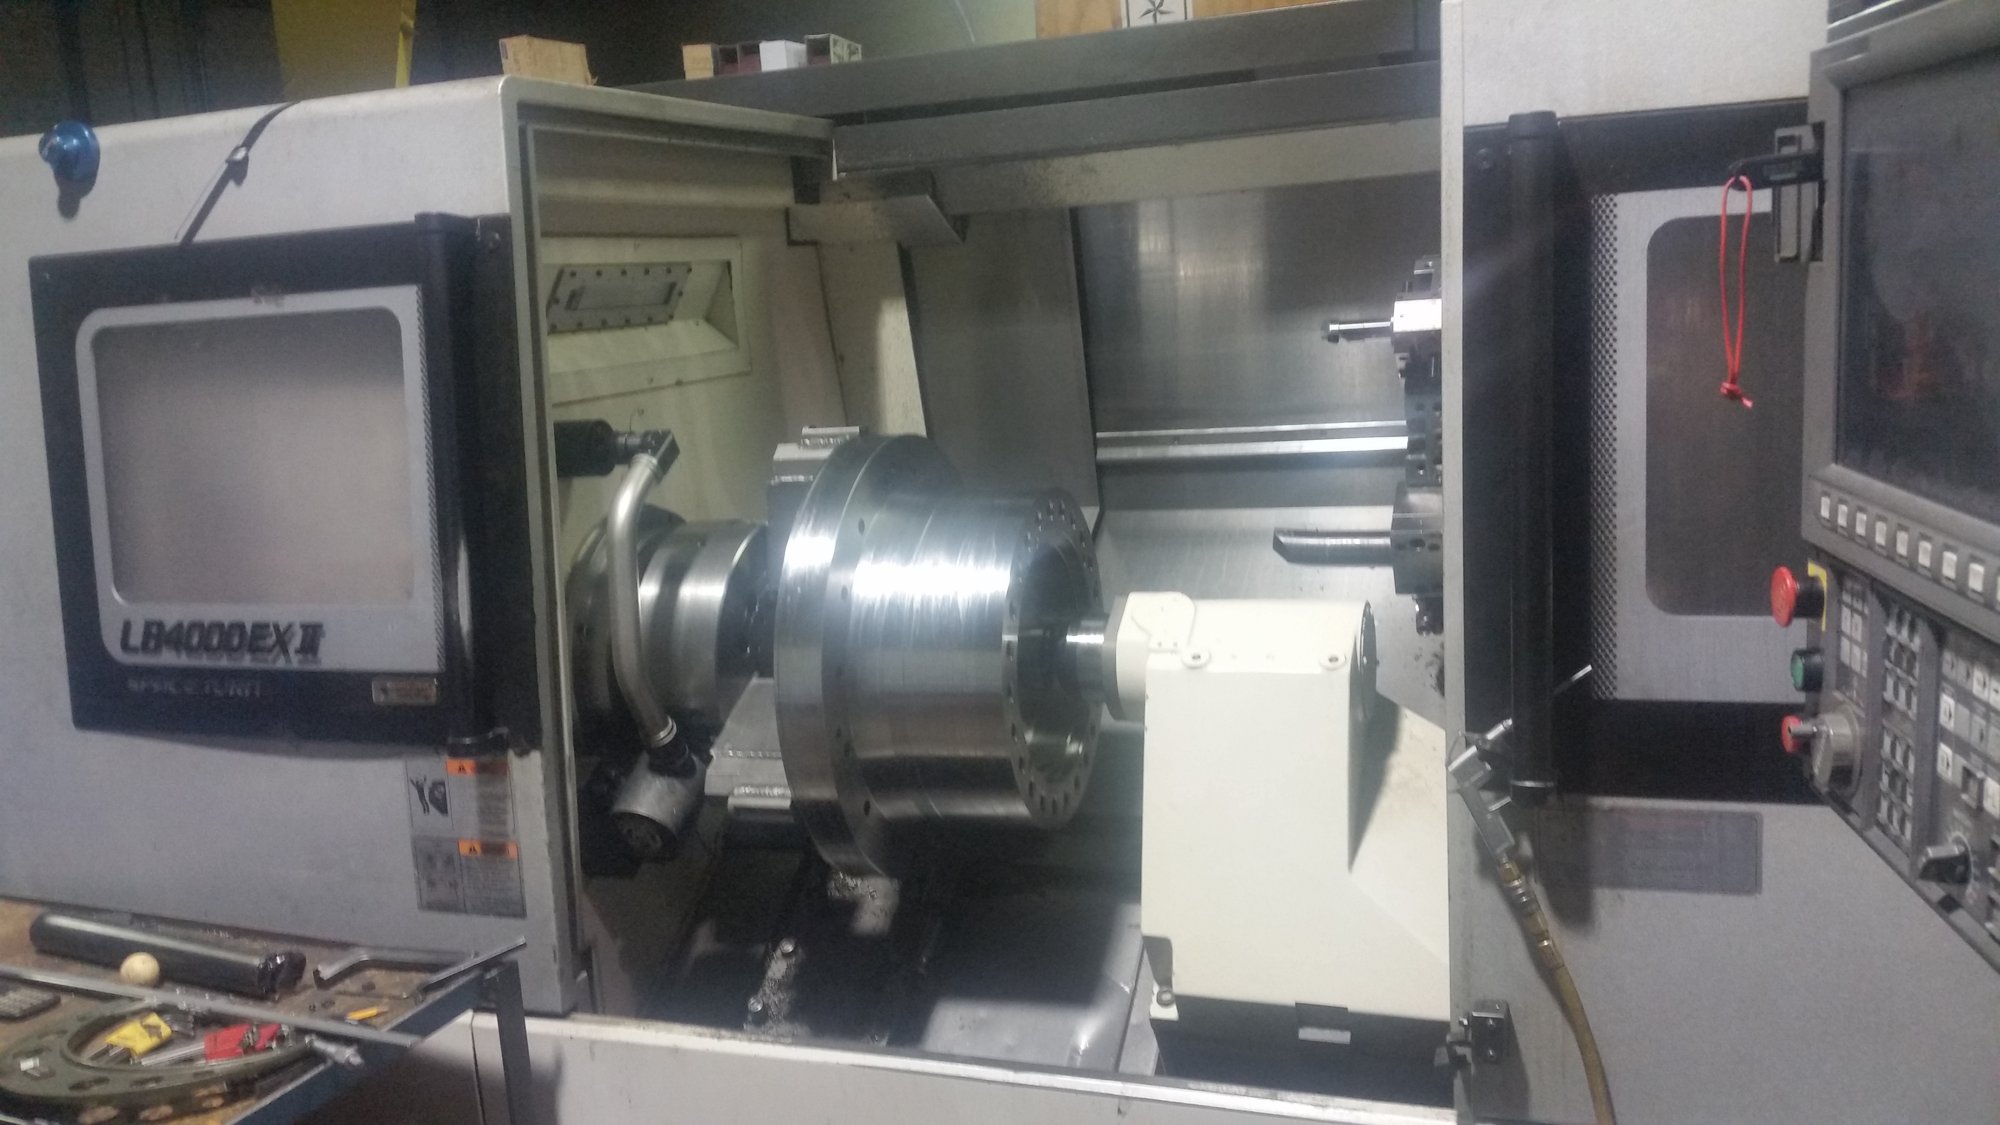
Okuma LB4000EX II turning a flanged part, doors open on the shop floor
The shop: Okuma LB4000EX II turning a flanged part
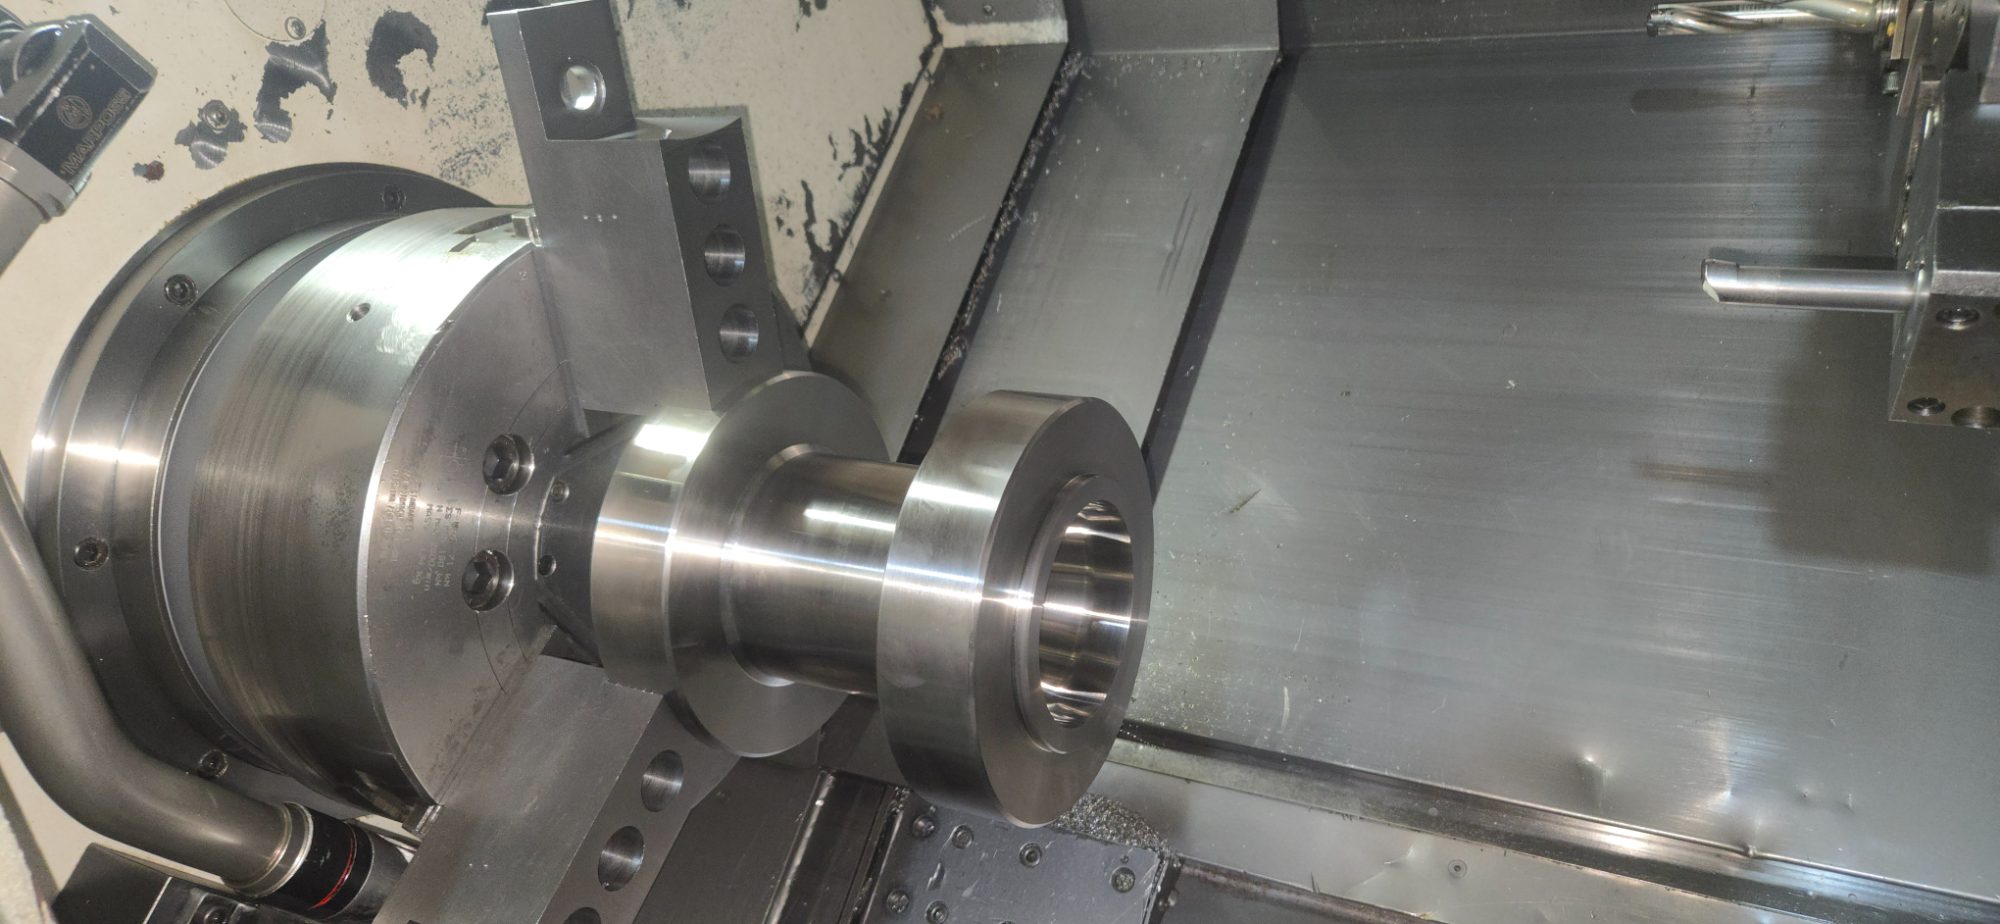
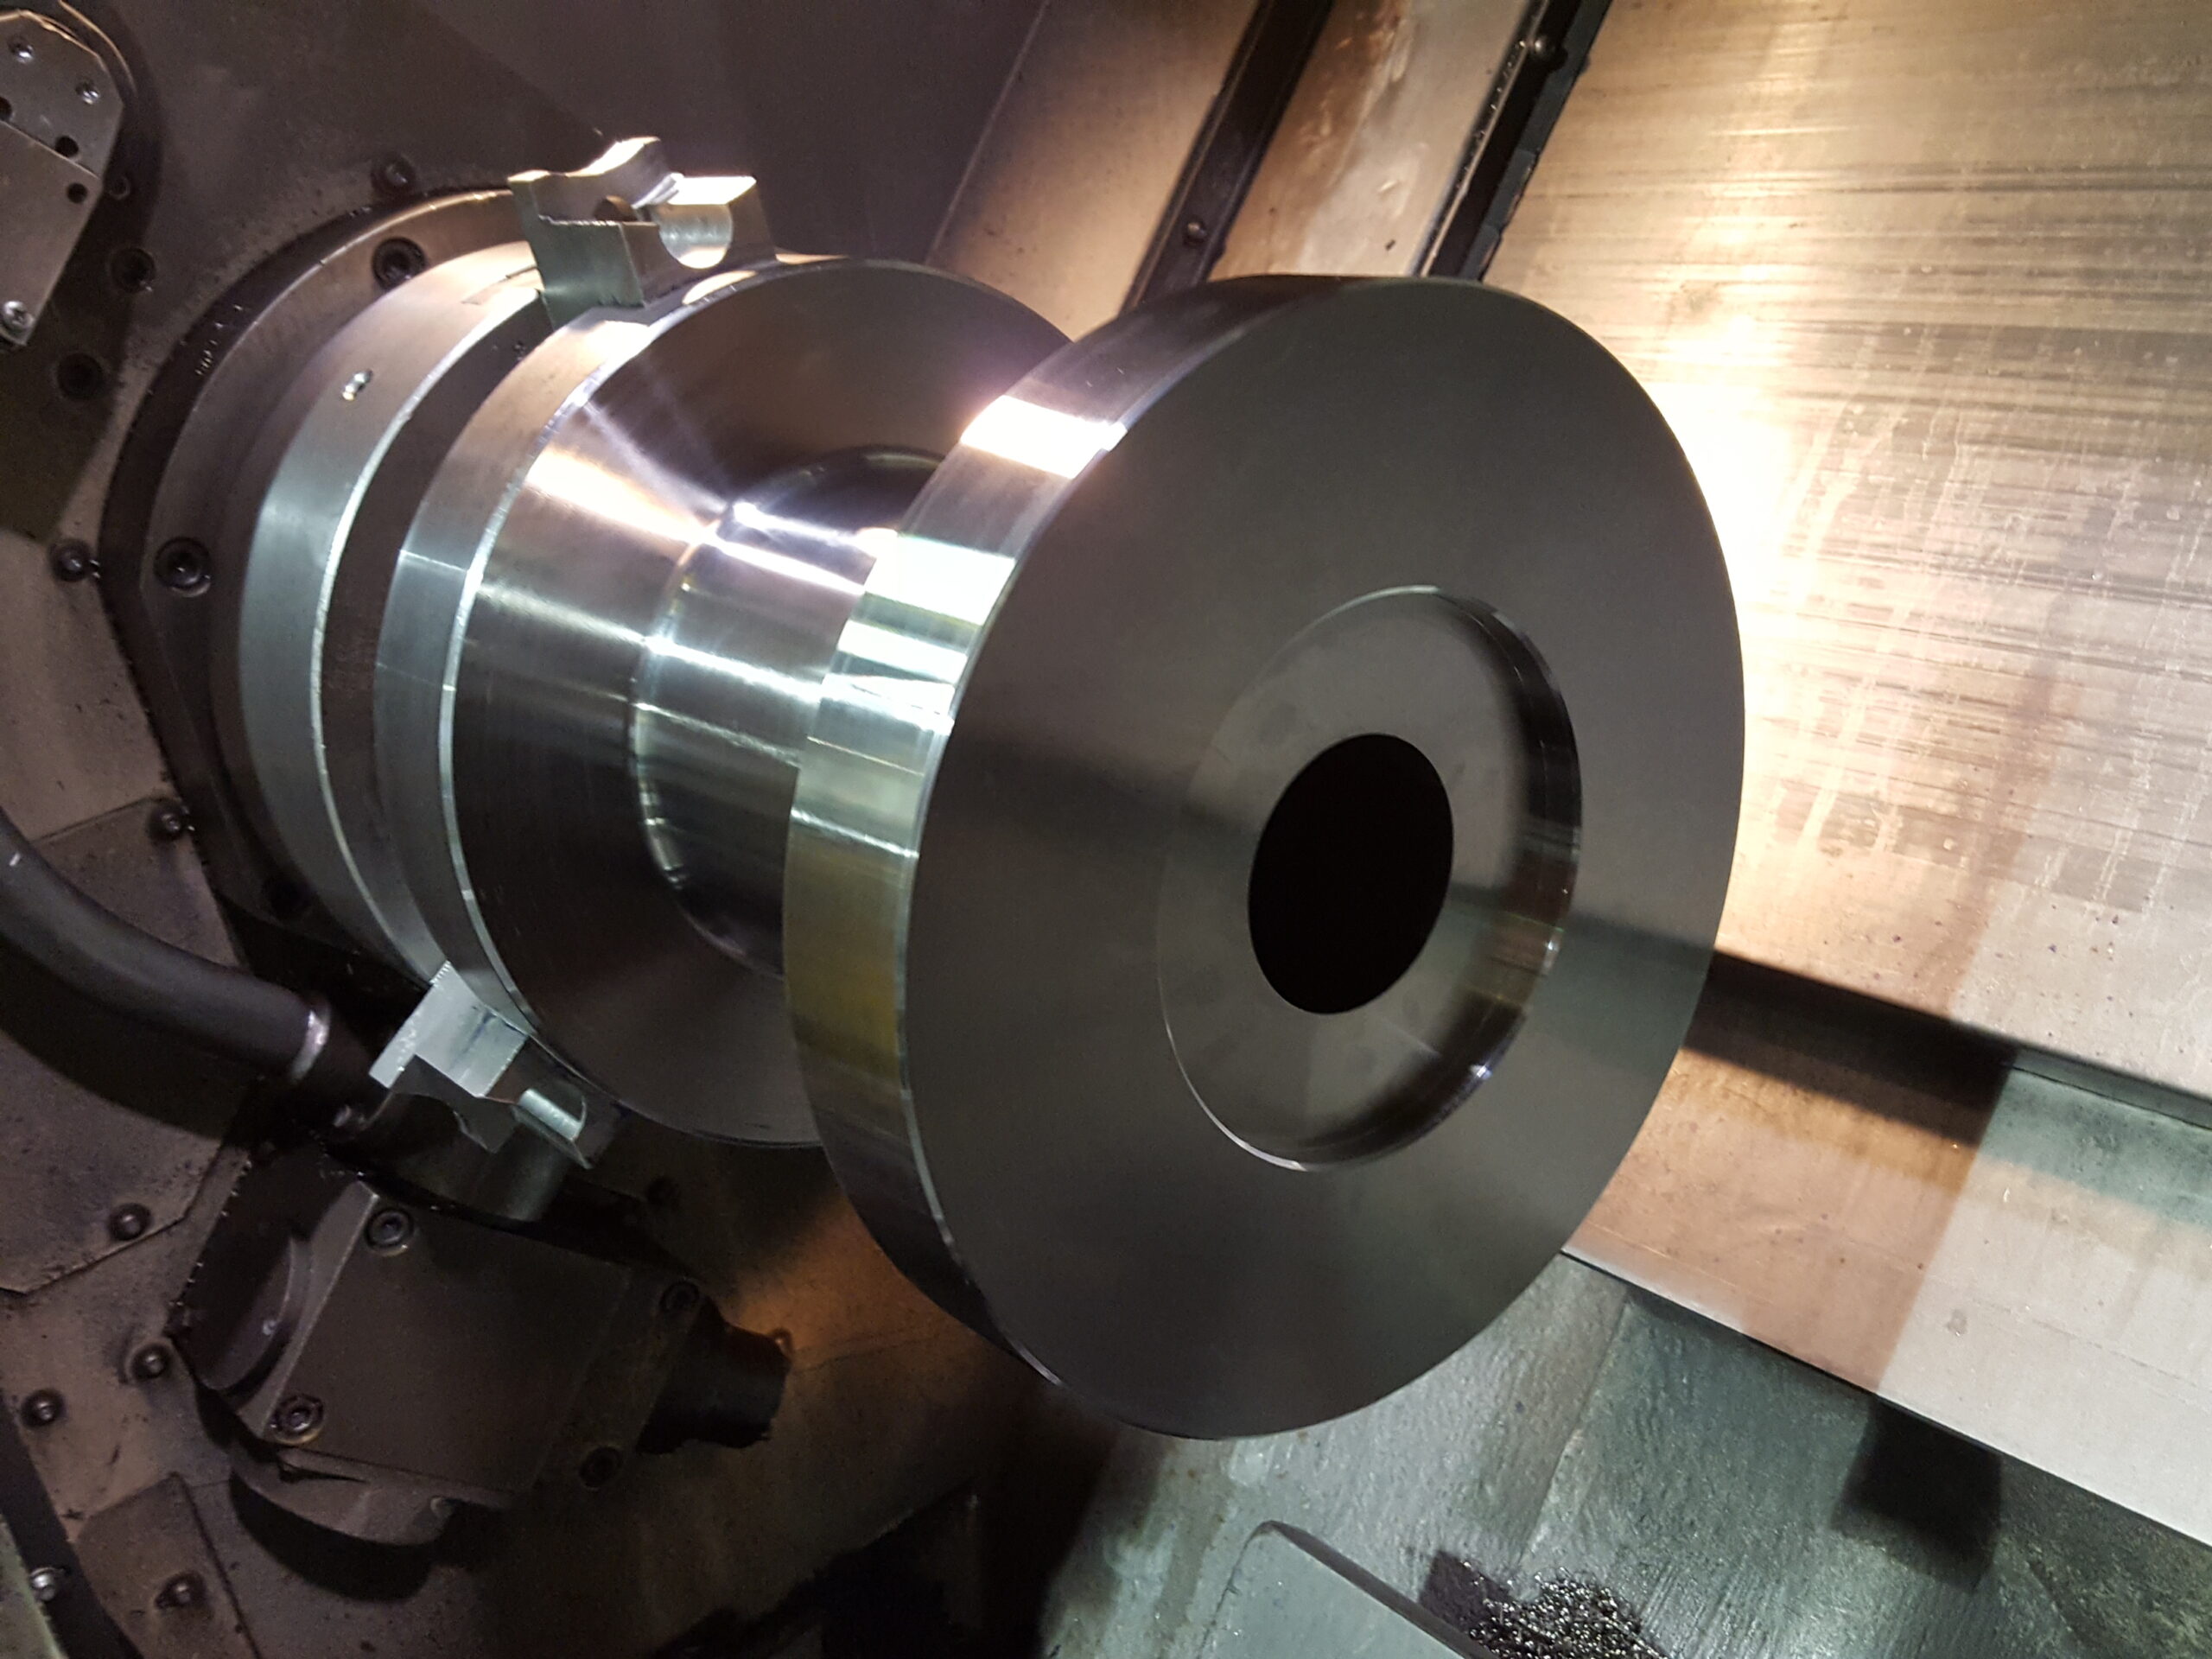
Flange Adapter Turning for Extruder 4140HT Material
Extruder parts: Flange adapter turned from 4140 HT
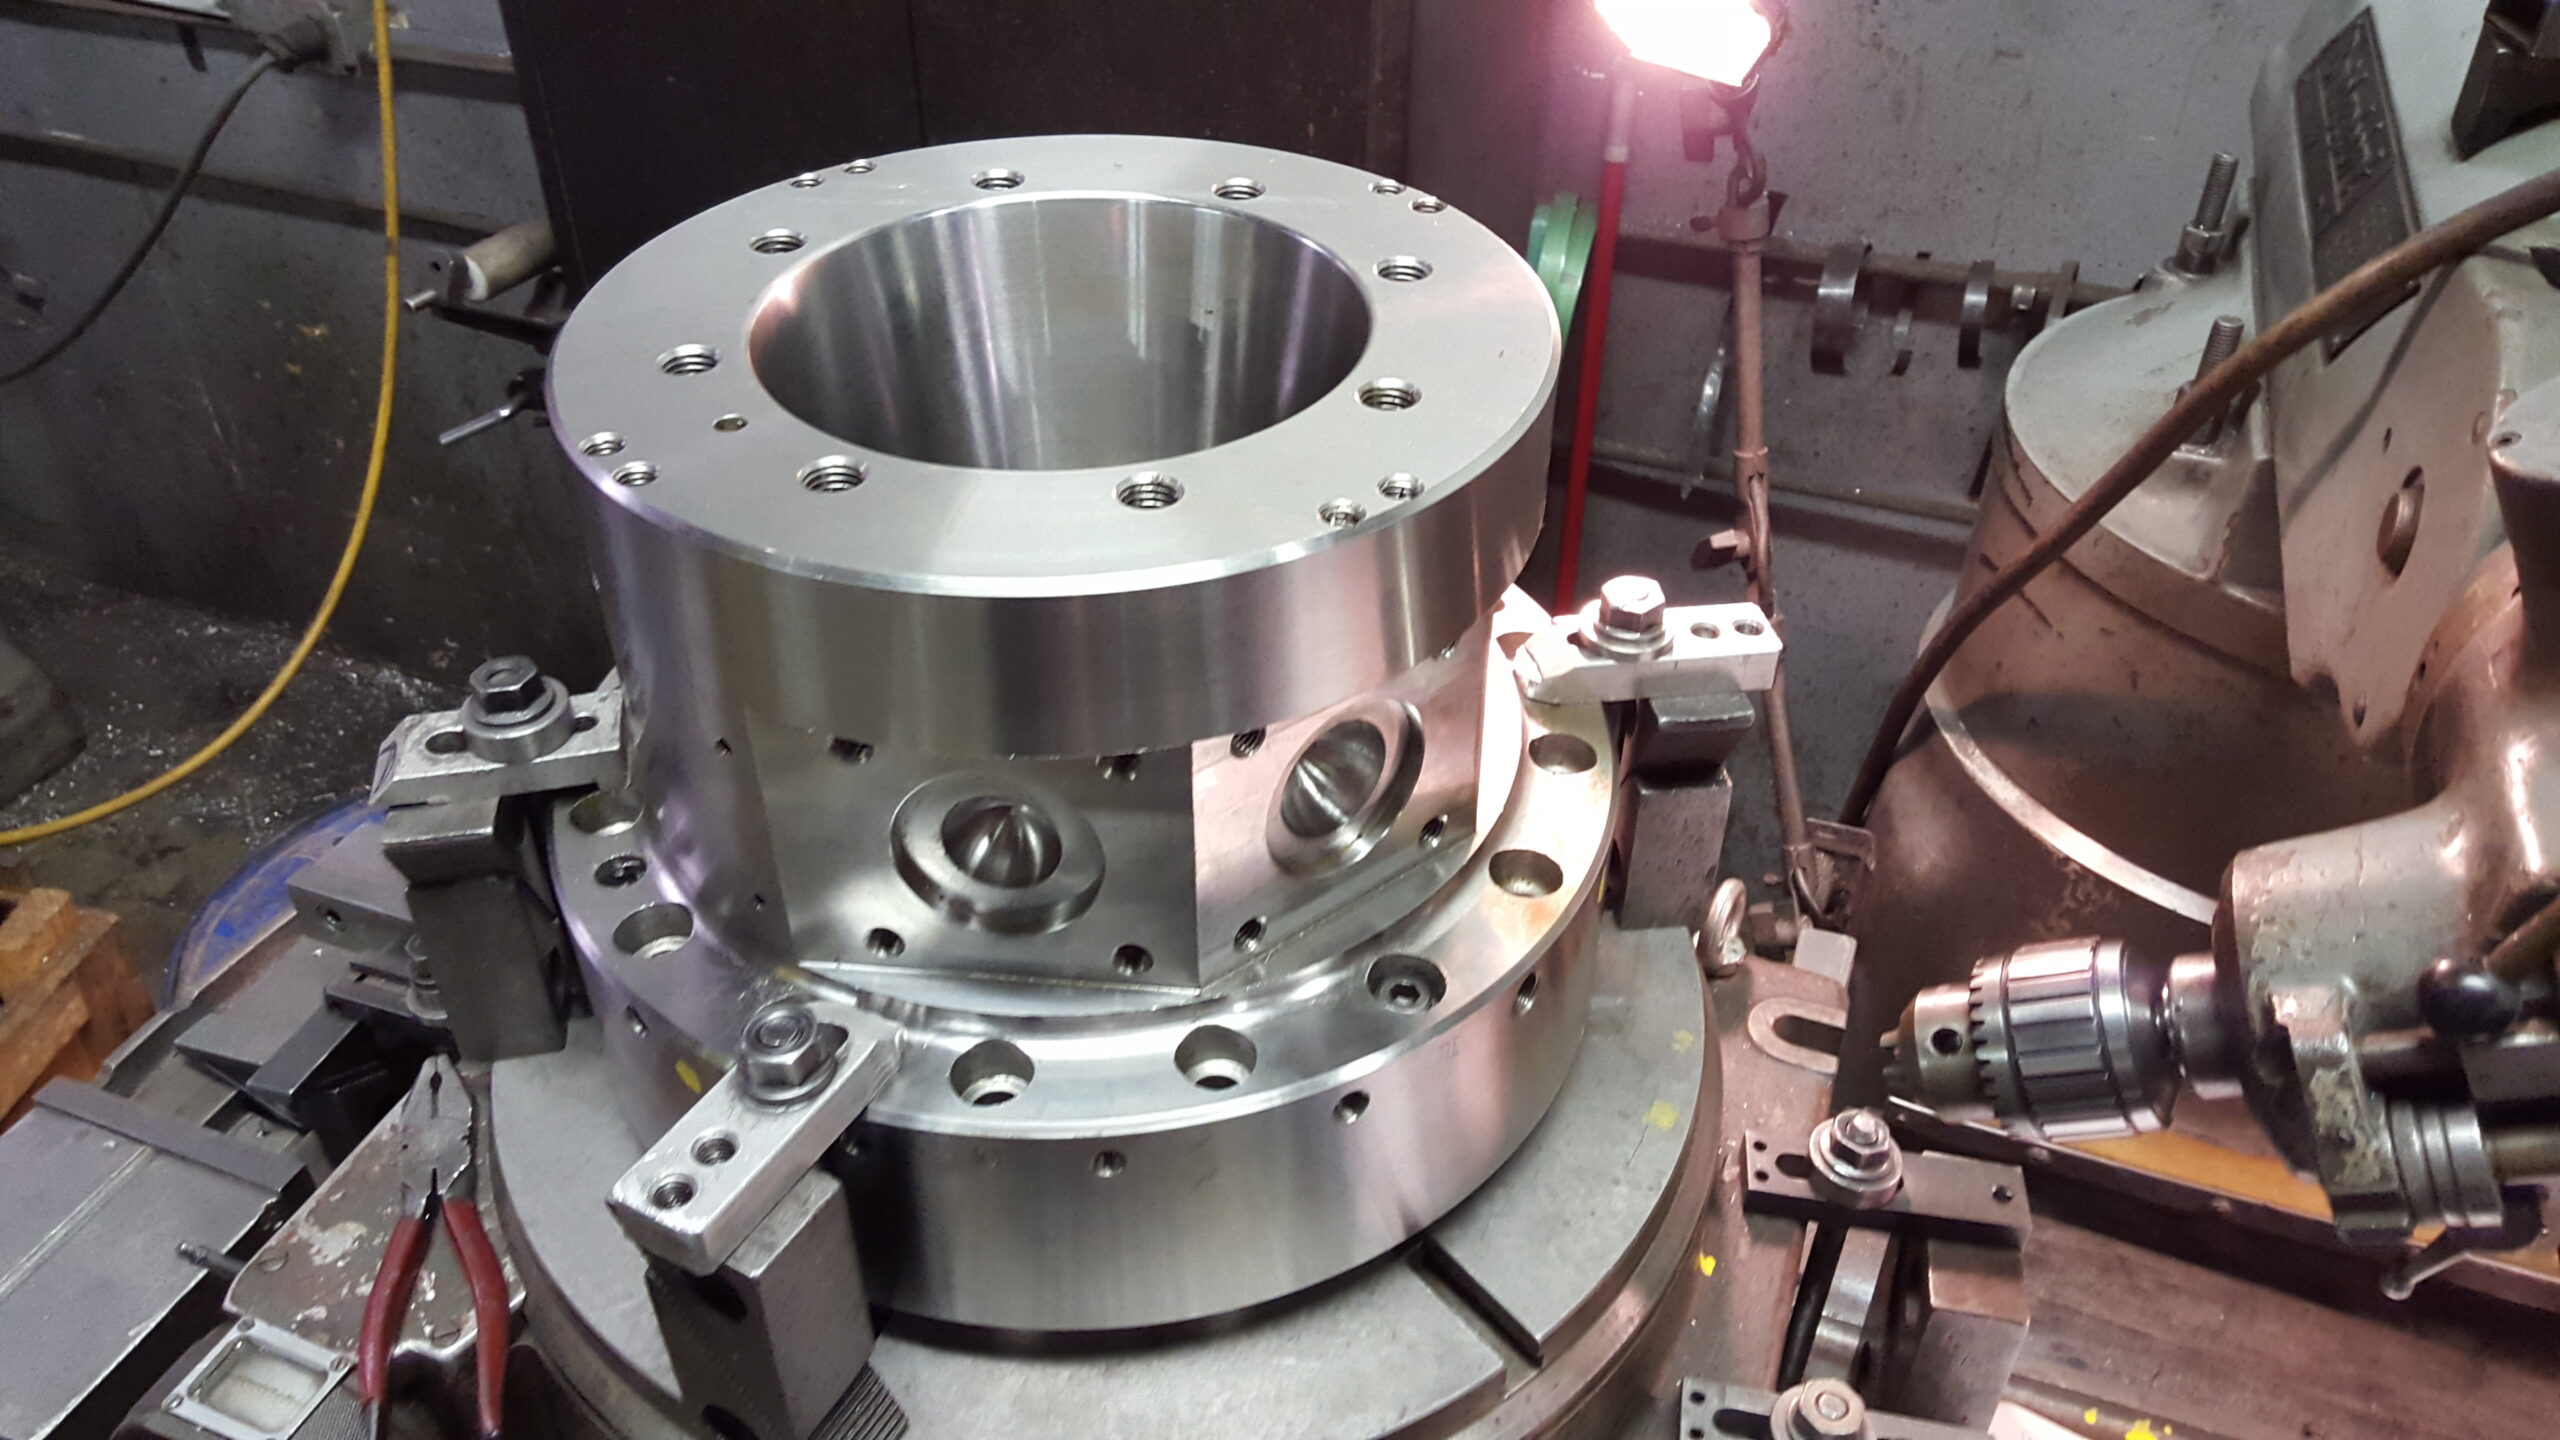
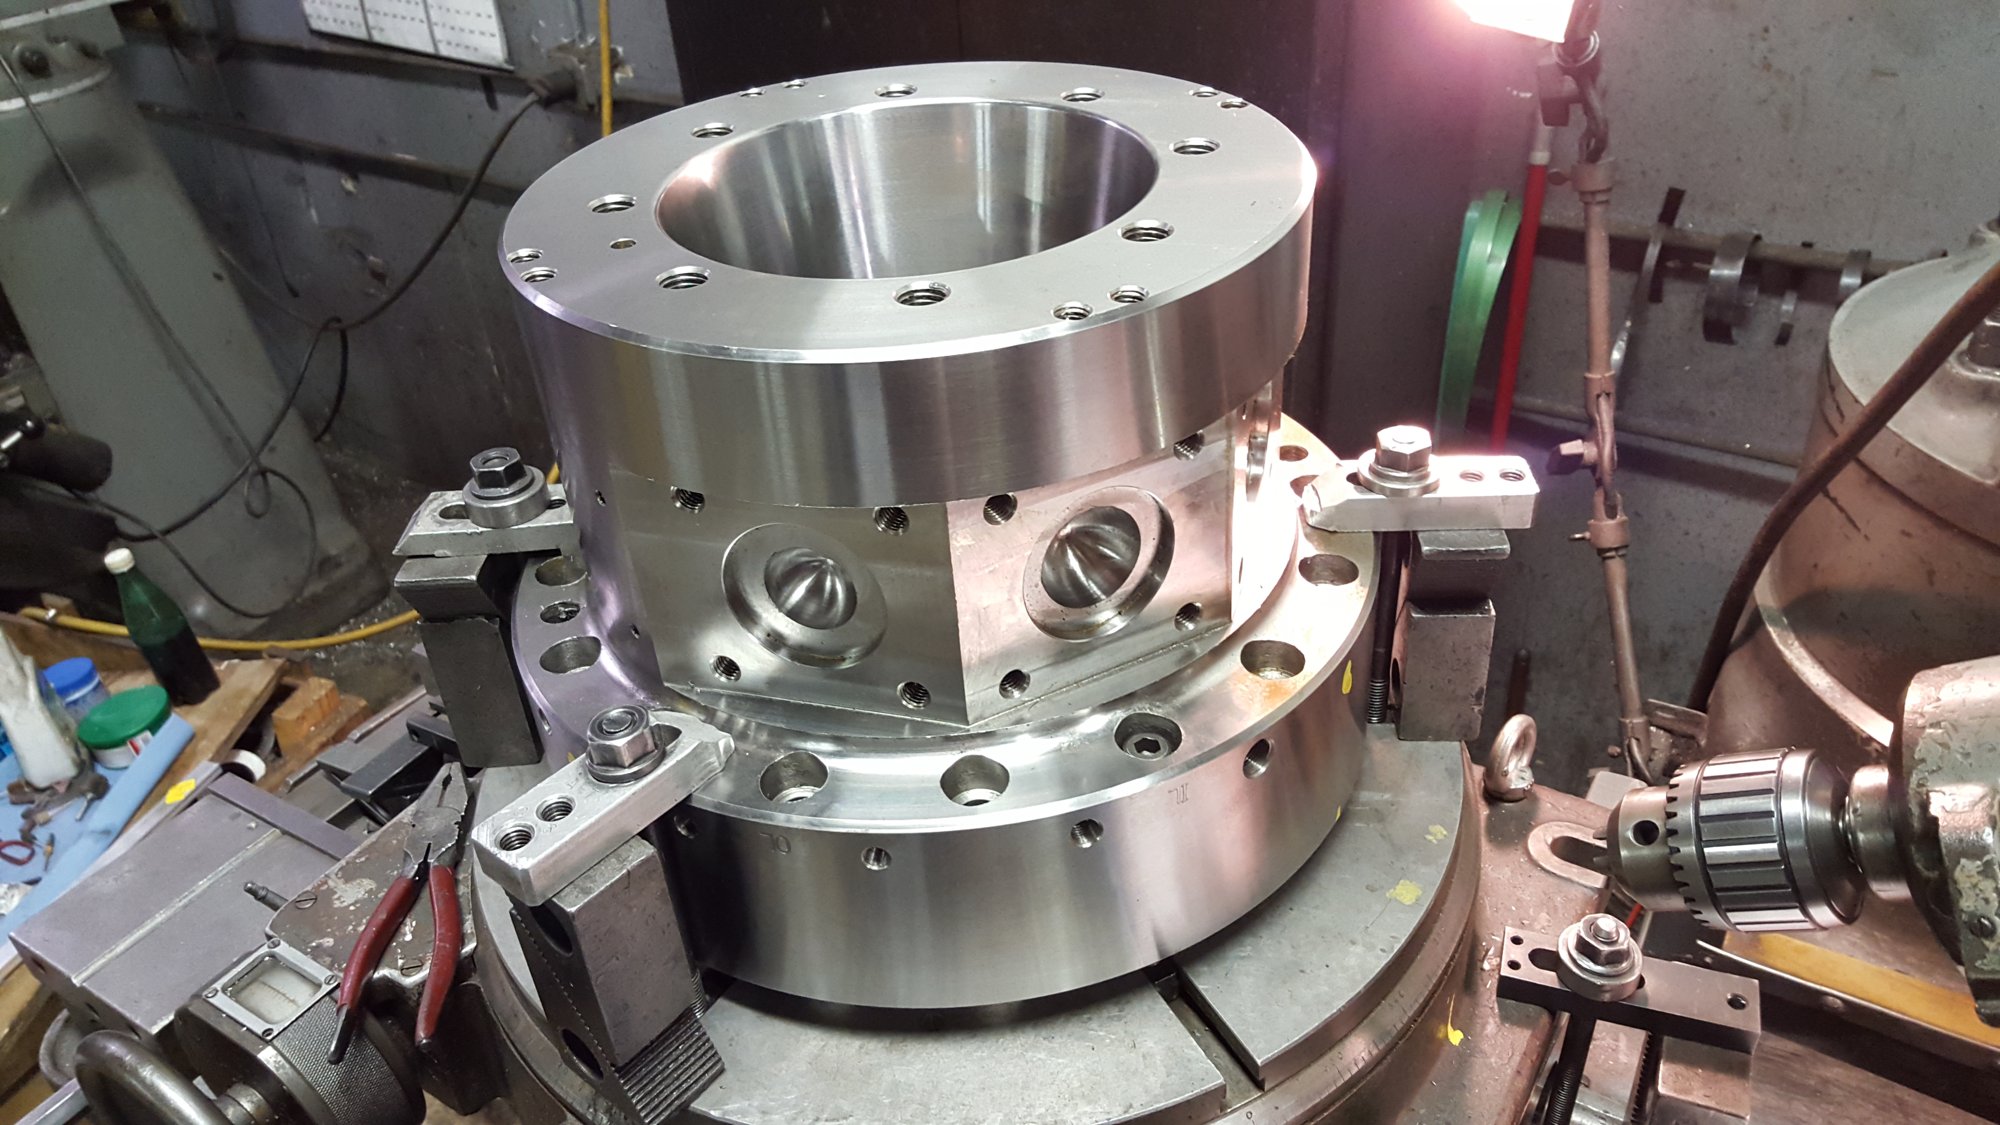
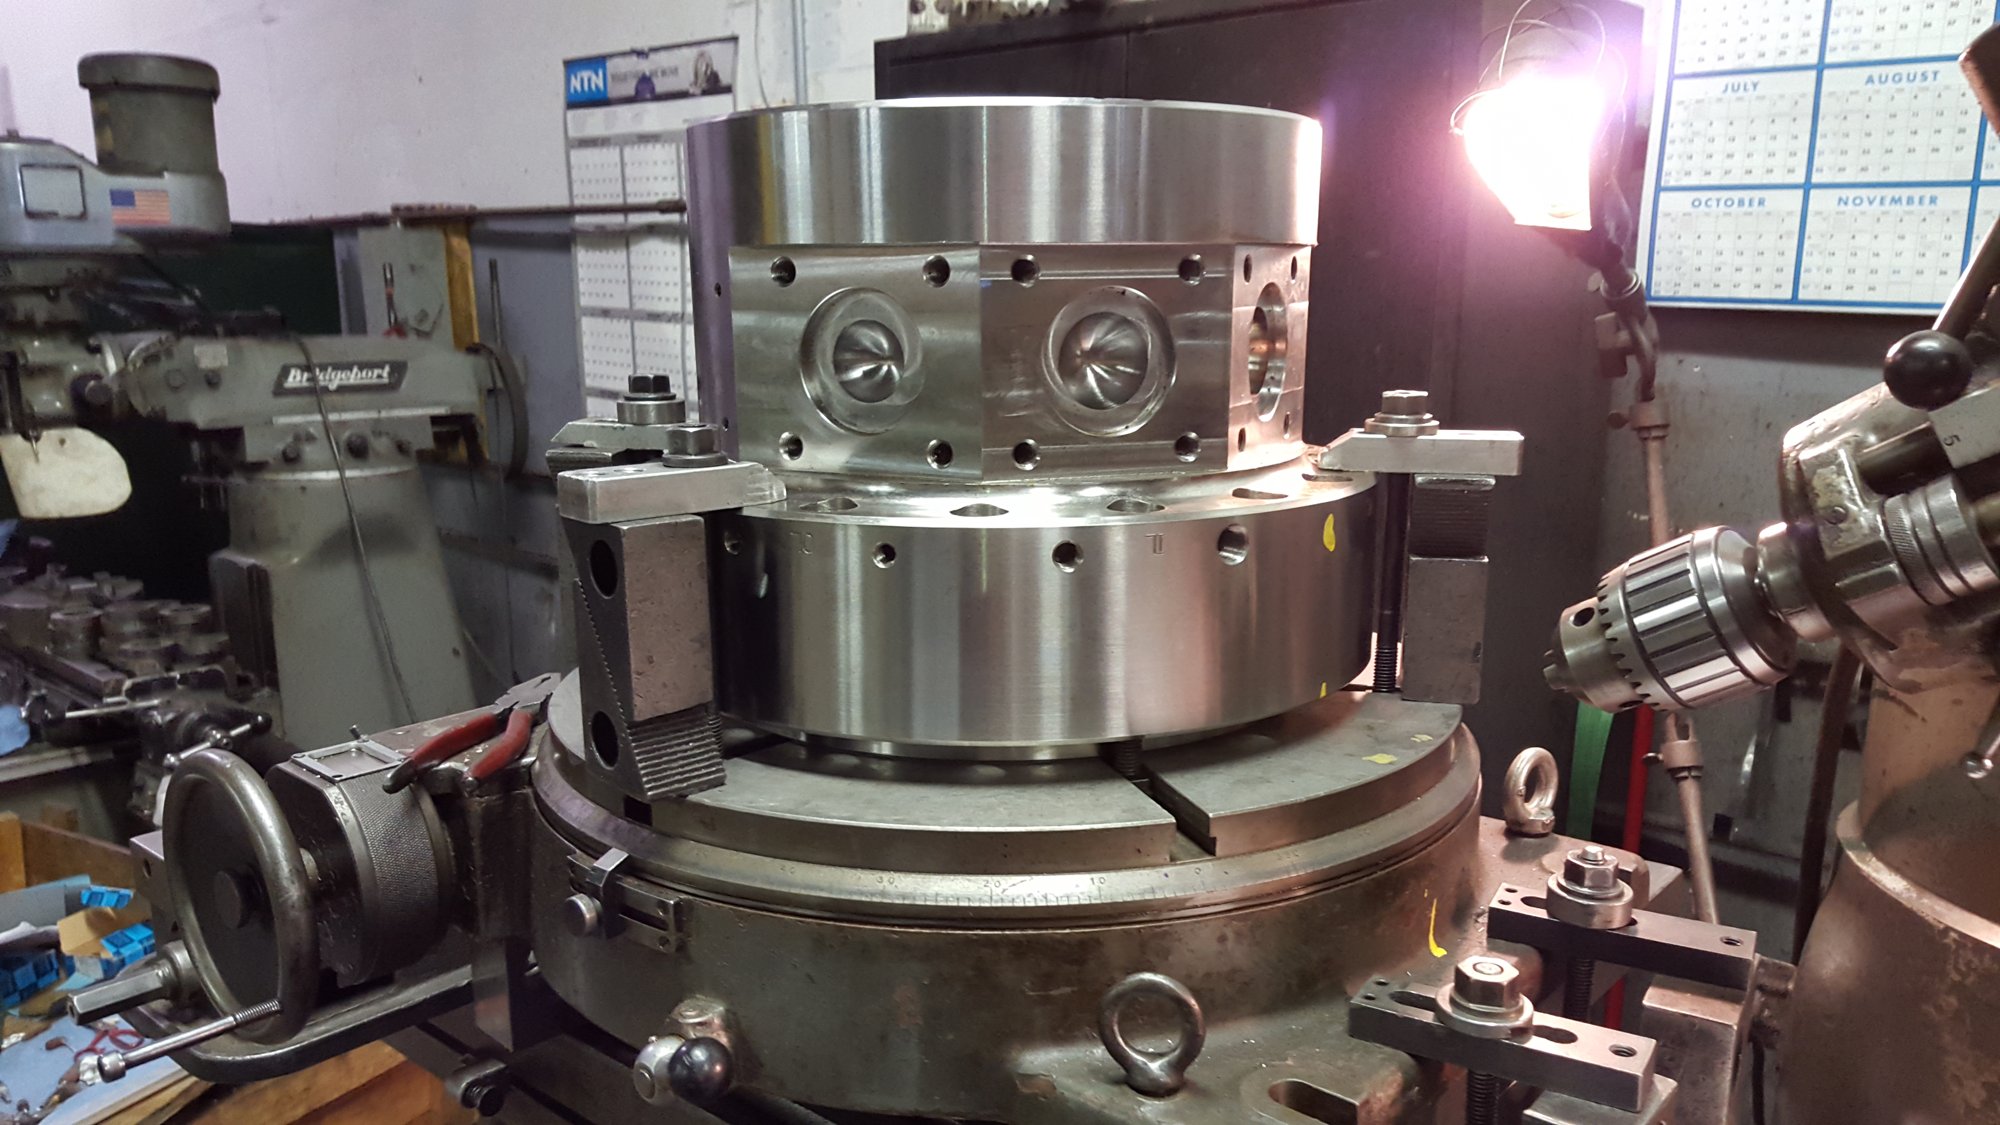
Melt ports bored and tapped into the milled flats of a blown film die body on its base flange
One die, start to finish (8 of 10): Melt ports bored and tapped into the milled flats
Large stainless housing clamped on the machine table, flange bolt circle and side ports machined
Large machining: Stainless housing, bolt circle and side ports machined
Large die body strapped down on the machine table, clamps set before the spindle comes in
Blown film dies: Die body strapped down before the spindle comes in
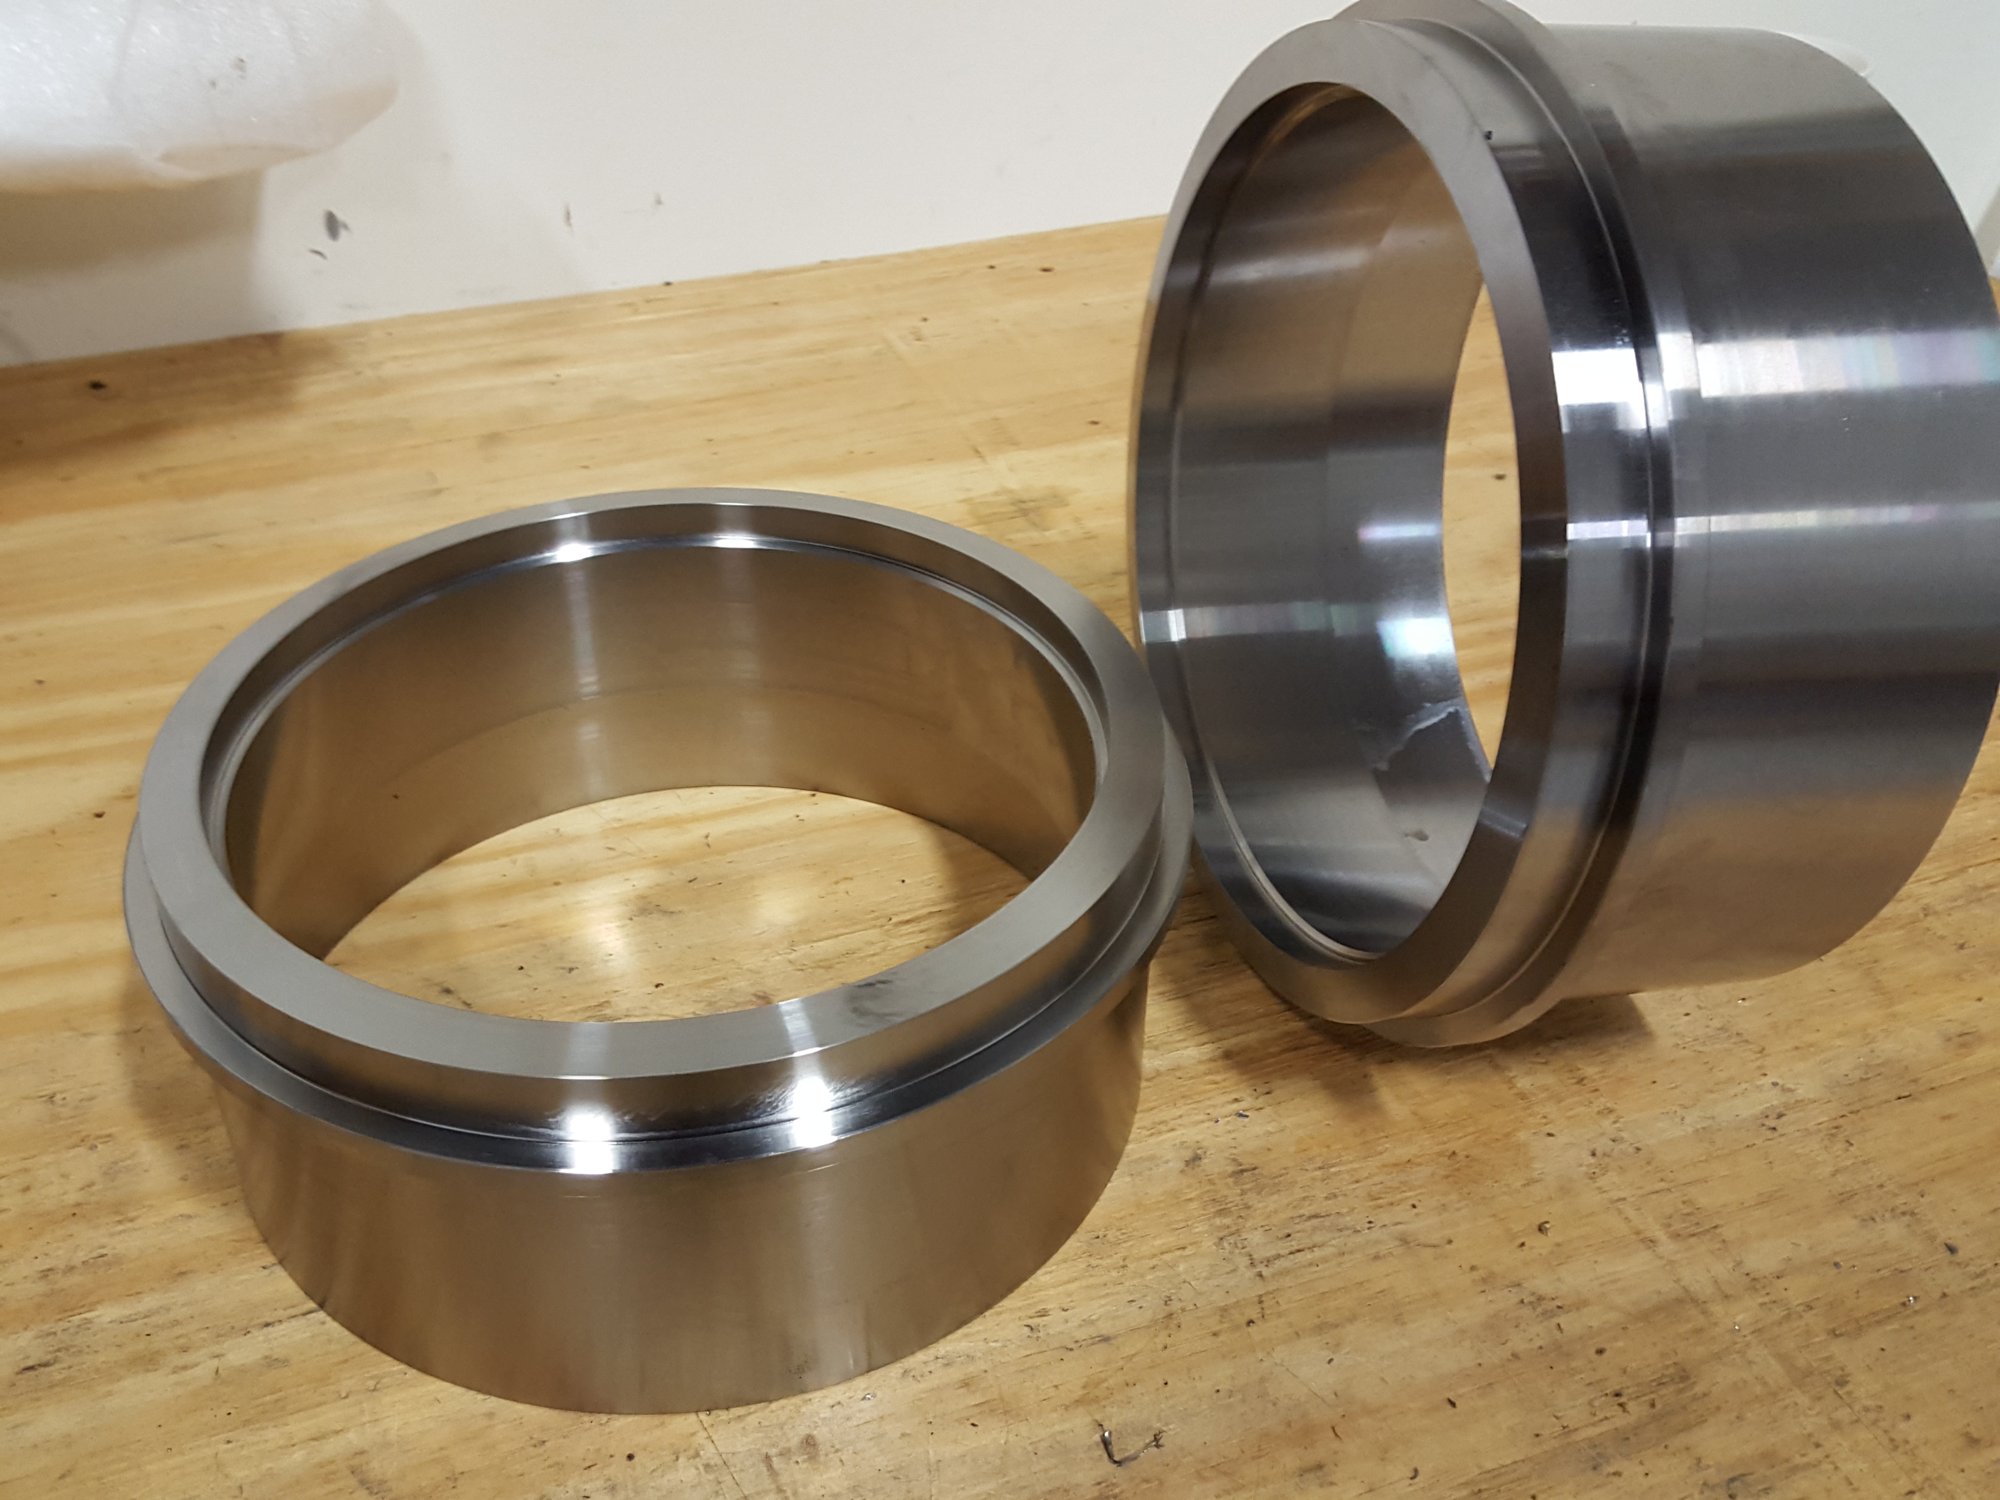
Matched pair of machined steel rings on the bench, bores finished and lips chamfered
Turning and production: Matched pair of rings, bores finished, lips chamfered
Machined shaft with its screw section checked against the customer's drawing at the bench
Shaft machining: Shaft with a screw section checked against the drawing
Die housing on the bench, stepped flanges and the finished bore at the neck
Blown film dies: Die housing, stepped flanges and finished bore
Stainless housing set up on the rotary table for boring, clamps and boring head in place
Large machining: Stainless housing on the rotary table for boring
Close view of the barrier flights and mixing flute on a polished 4.5in extruder screw
Extruder parts: Barrier flights and mixing flute on a 4.5in screw
Gearbox housing with the hollow output shaft in place, bore stepped and keyway cut
Gearbox repair: Housing with the hollow output shaft, bore and keyway cut
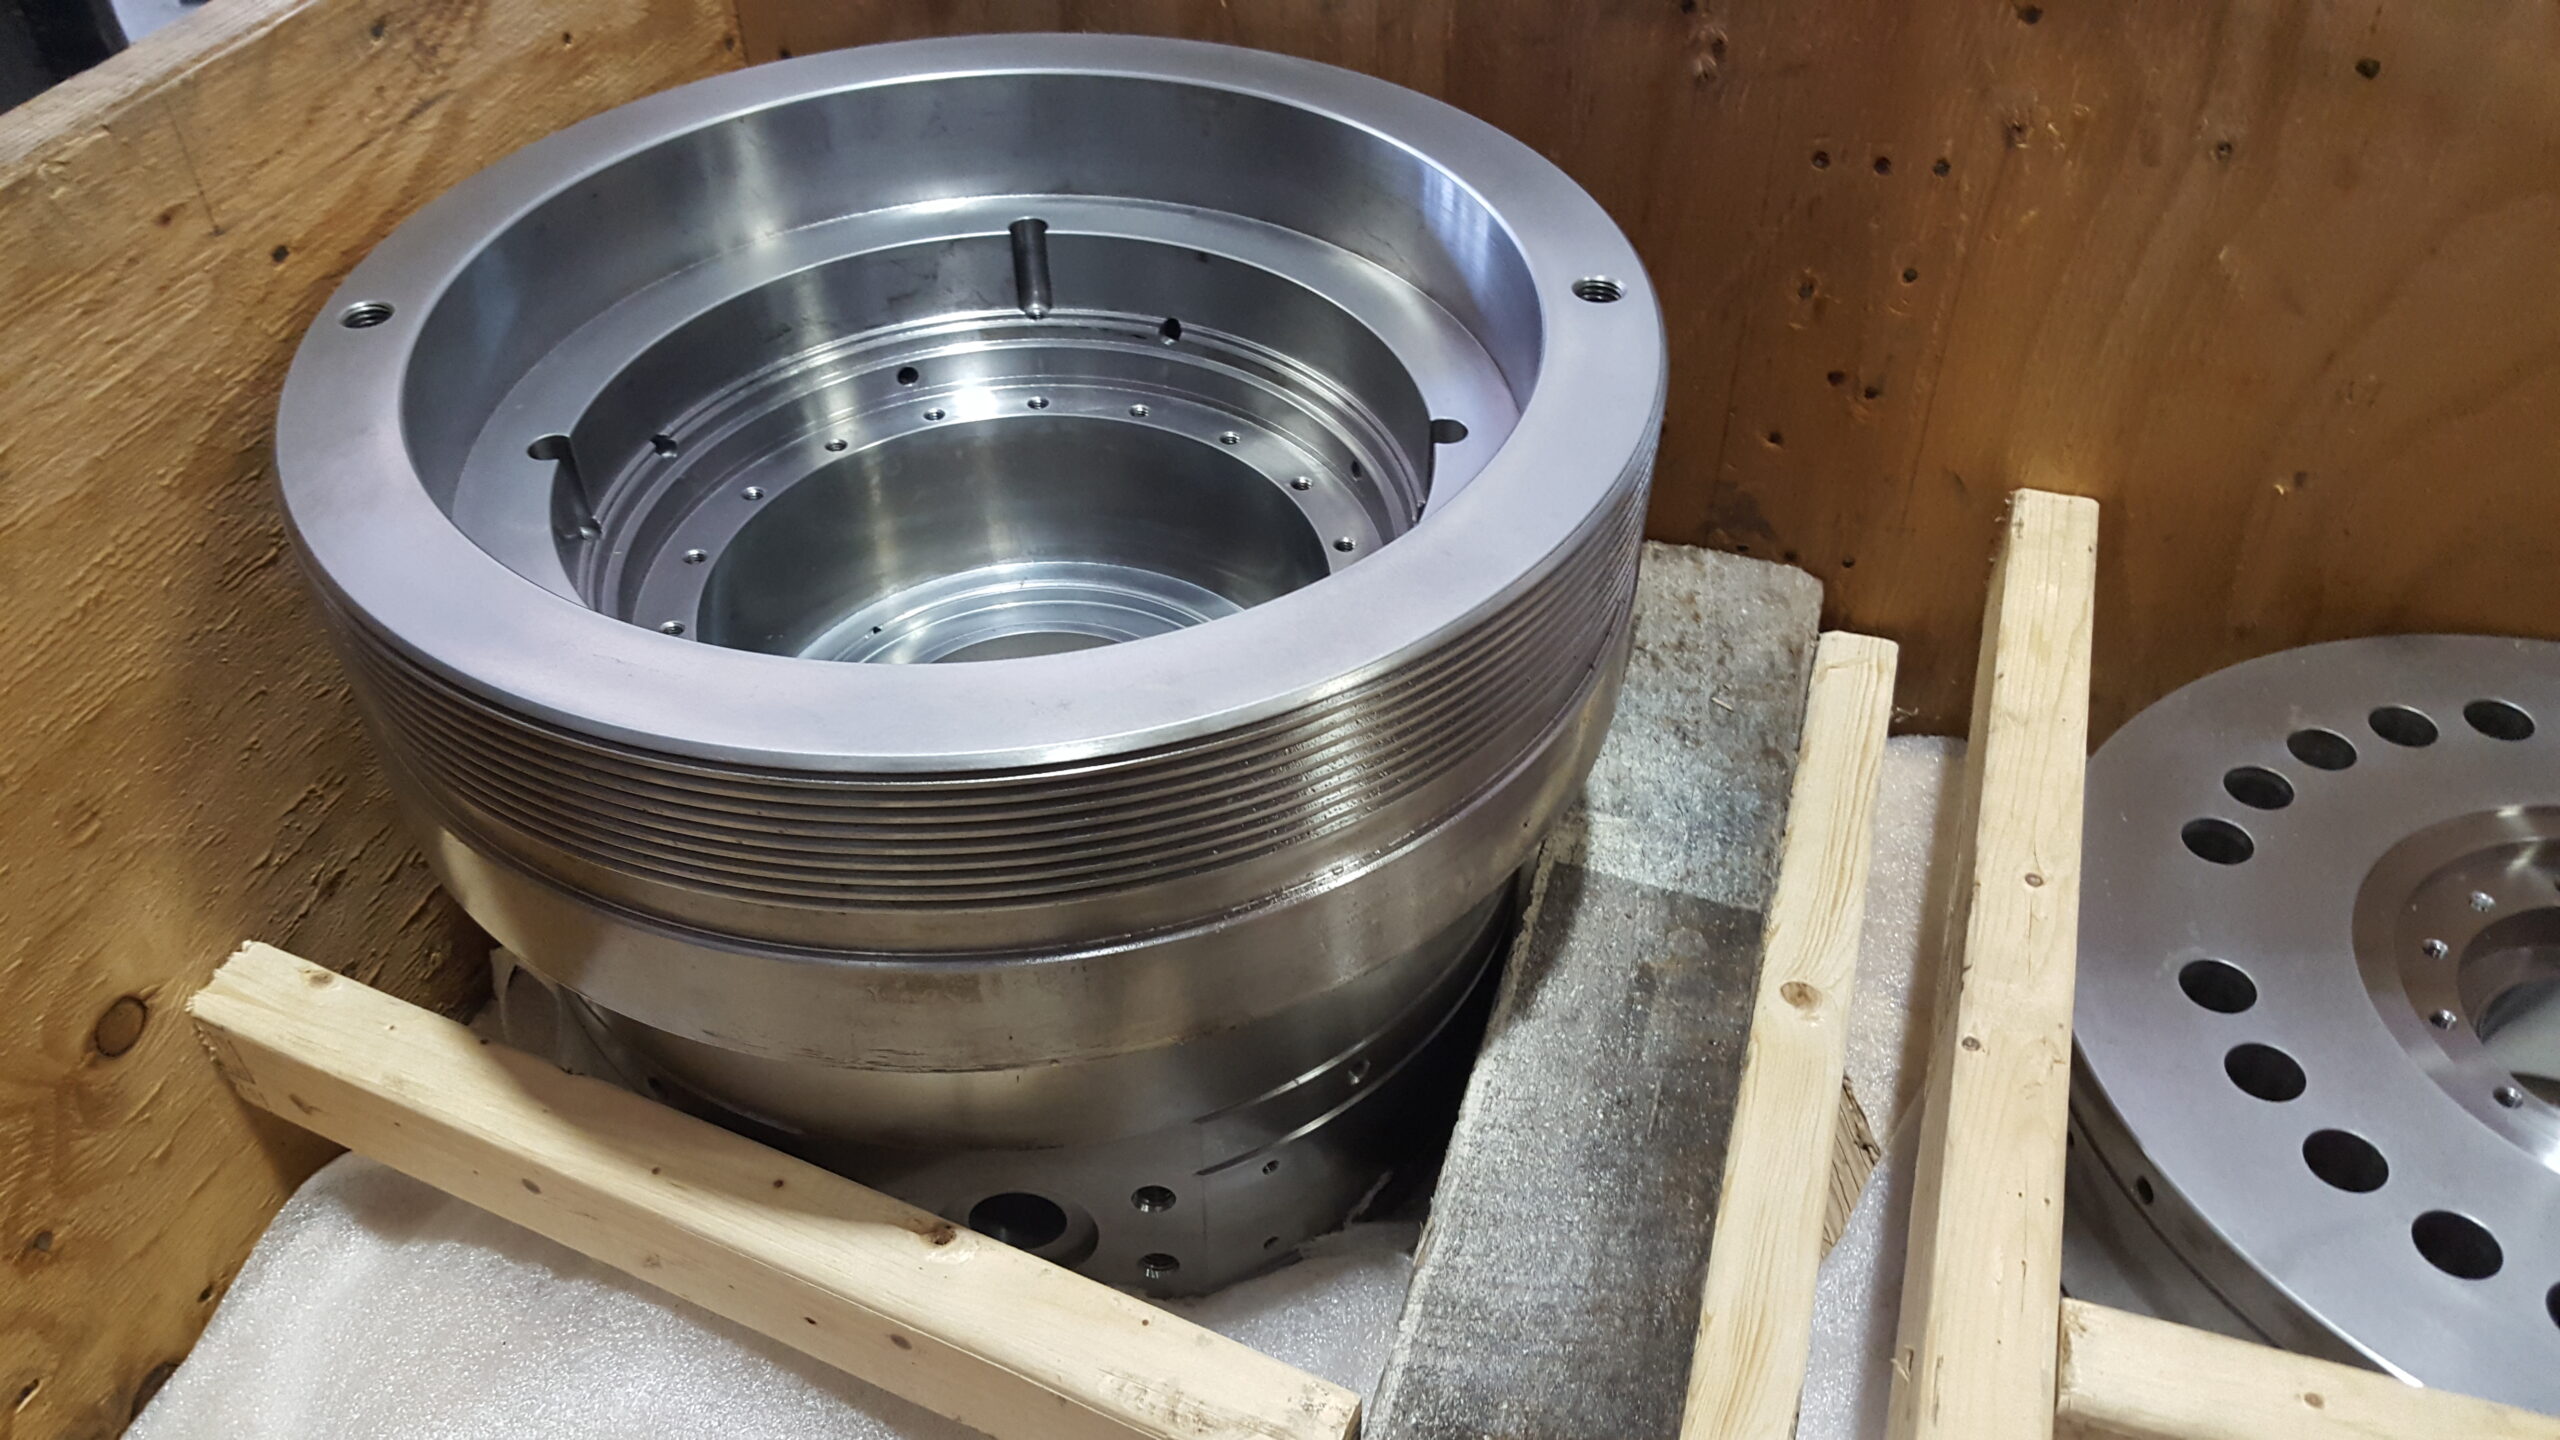
Machined ring housing crated for shipping, stepped bore inside and a threaded band on the outside
Fabrication and shipping: Ring housing crated, threaded band on the outside
Spiral distribution ring with its flow grooves machined into the recessed face
Blown film dies: Spiral distribution ring, flow grooves in the face
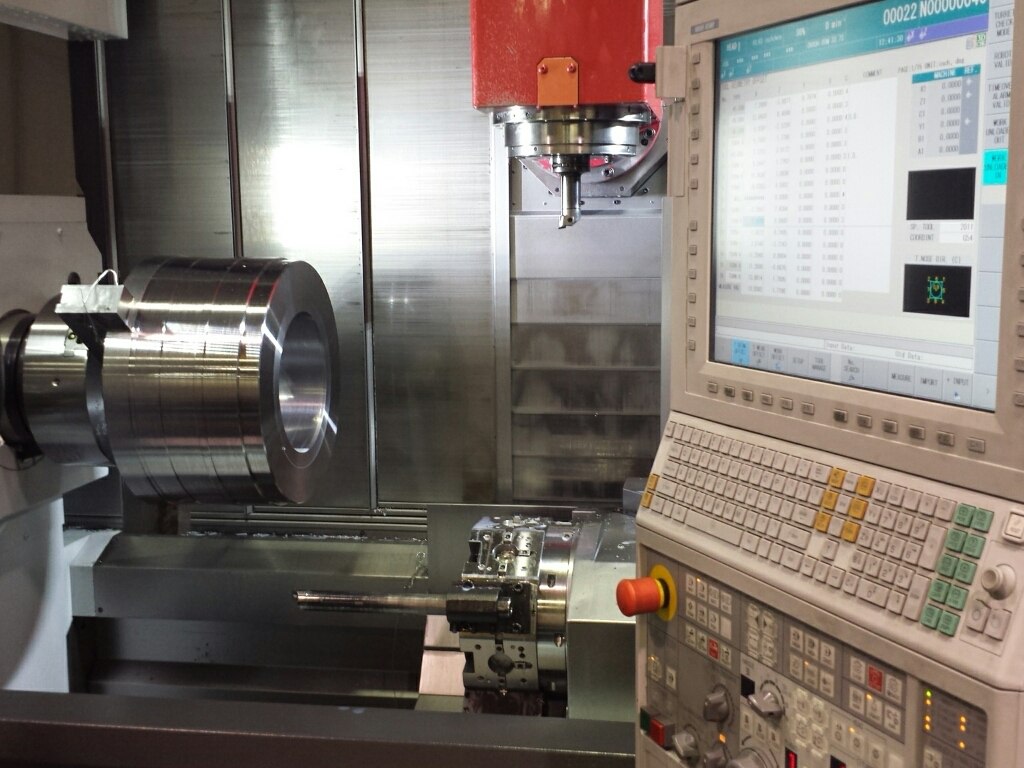
Program running on the control while a cylinder is machined in the mill-turn behind
The shop: Program running while a cylinder is machined
Stepped hub turned in the CNC lathe chuck, diameters and bore cut to size
Turning and production: Stepped hub turned to size in the CNC lathe
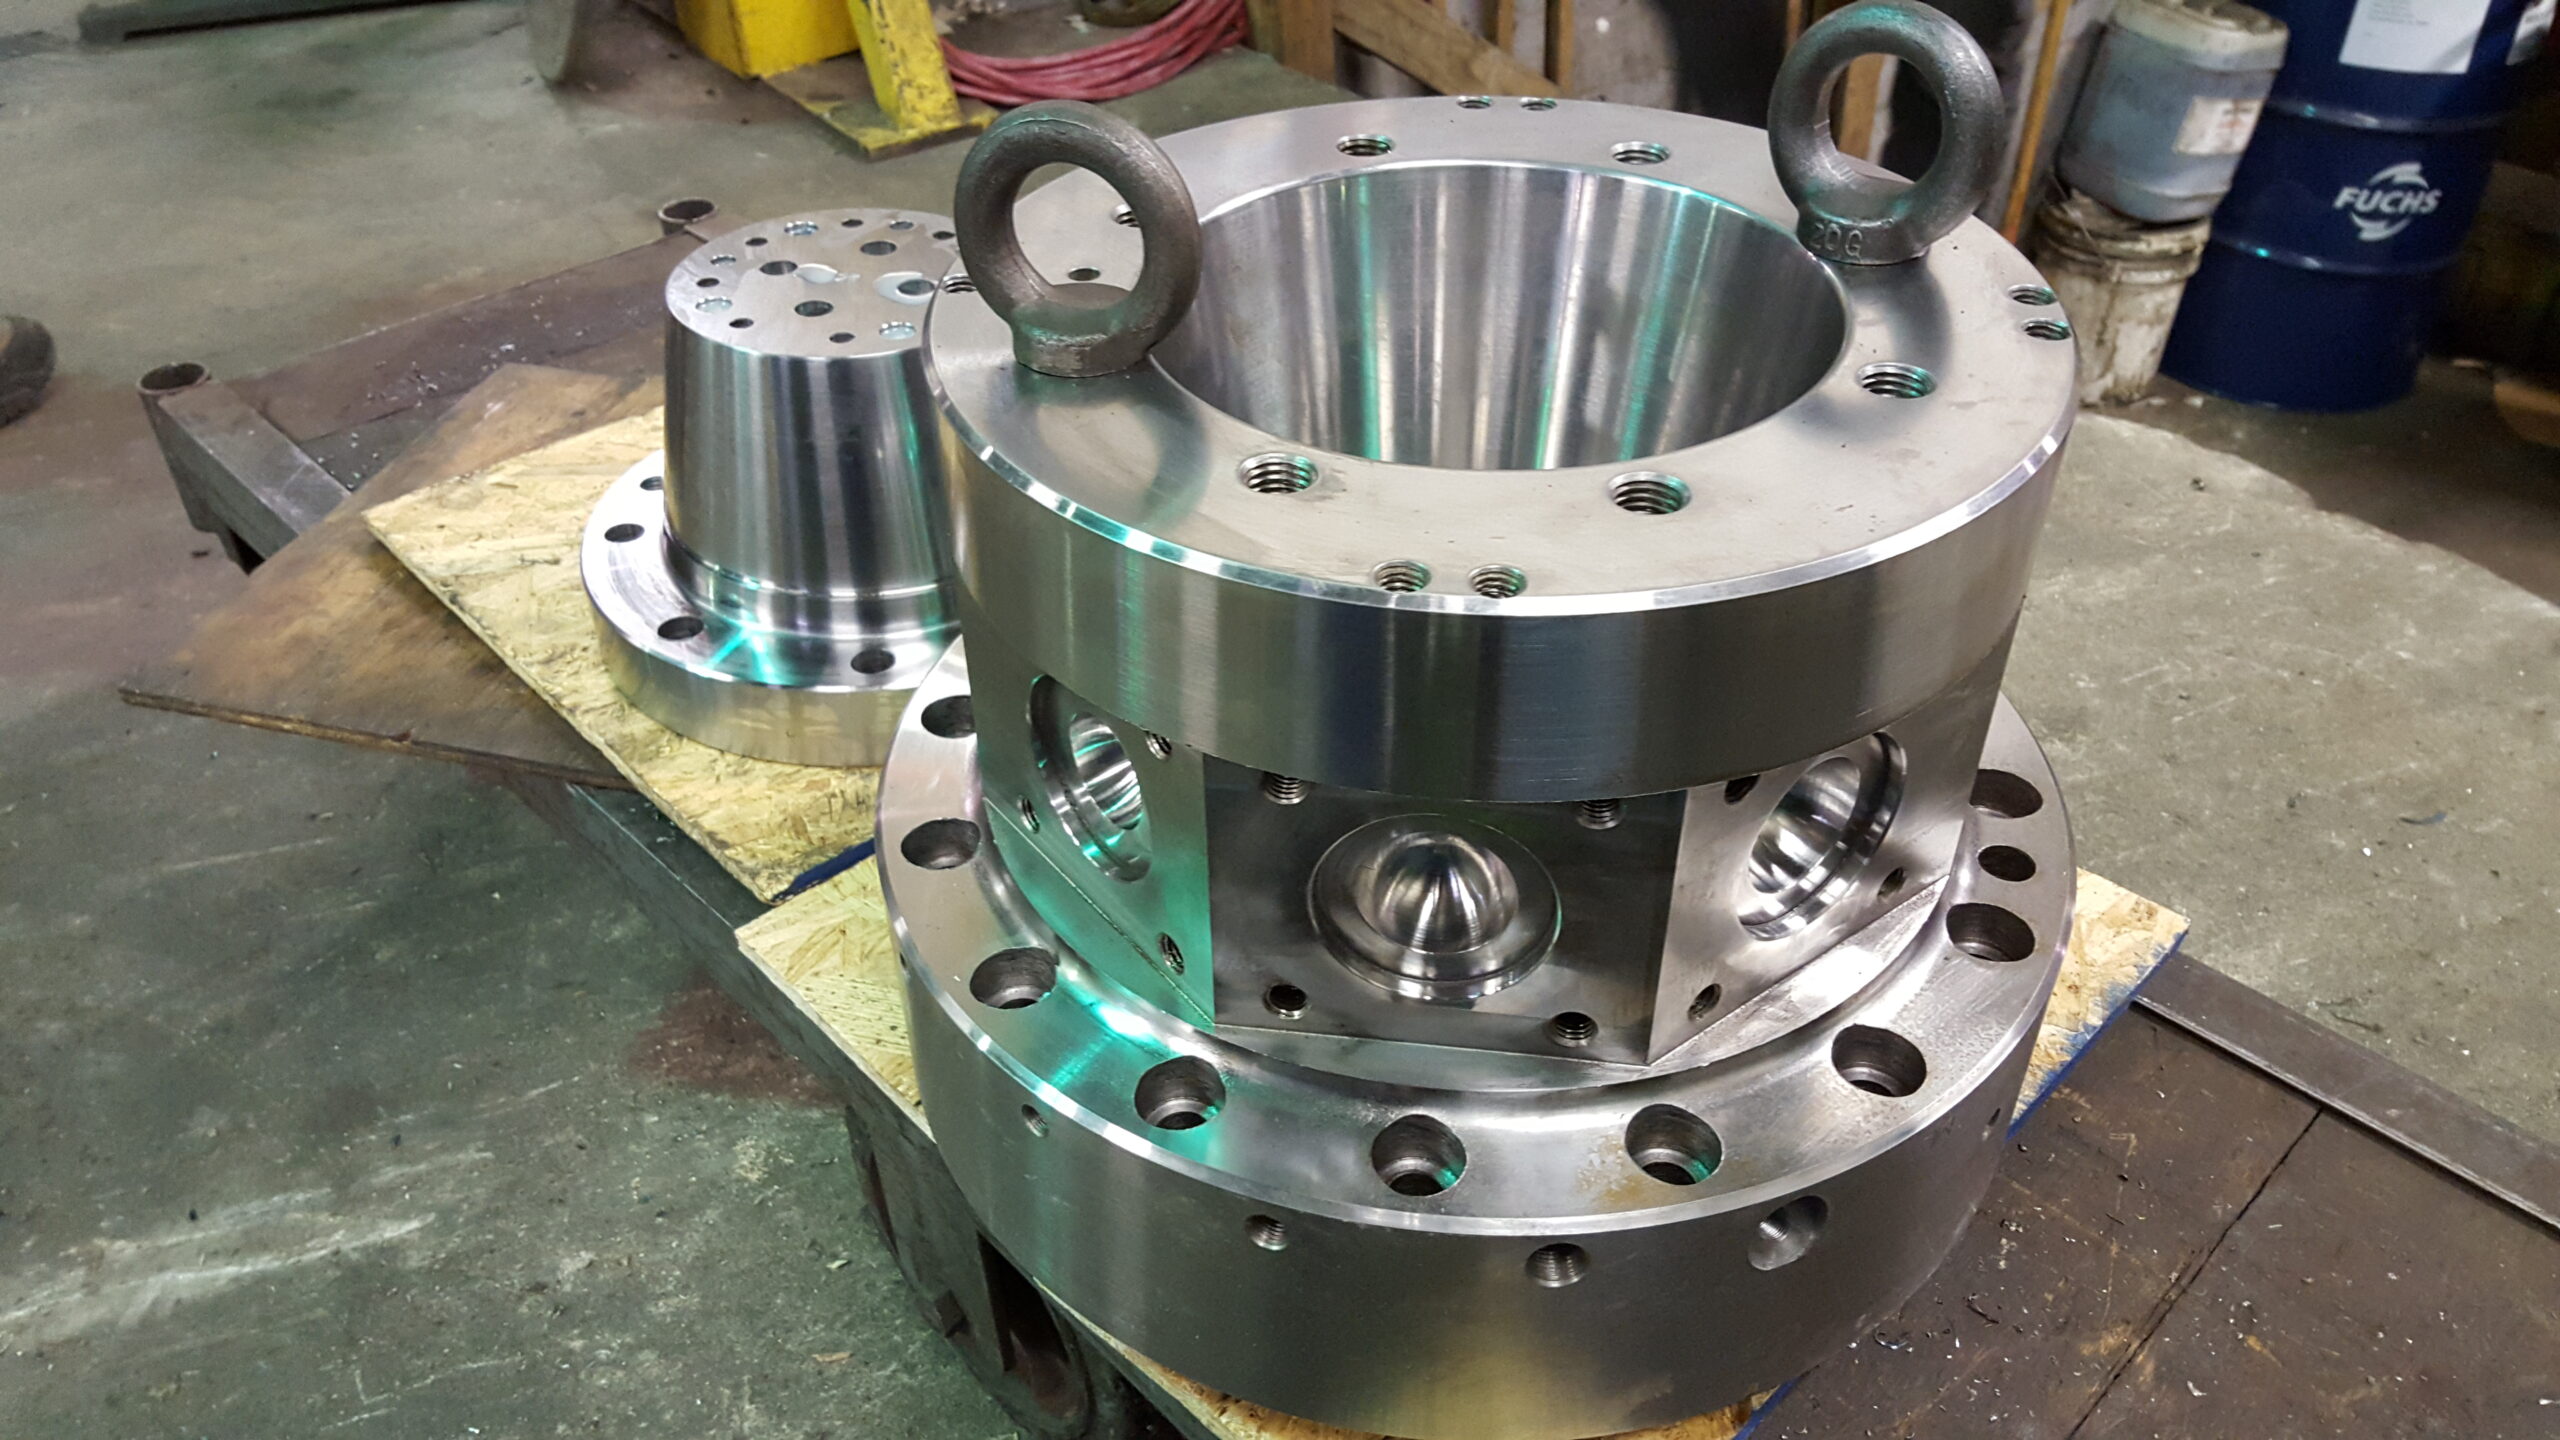
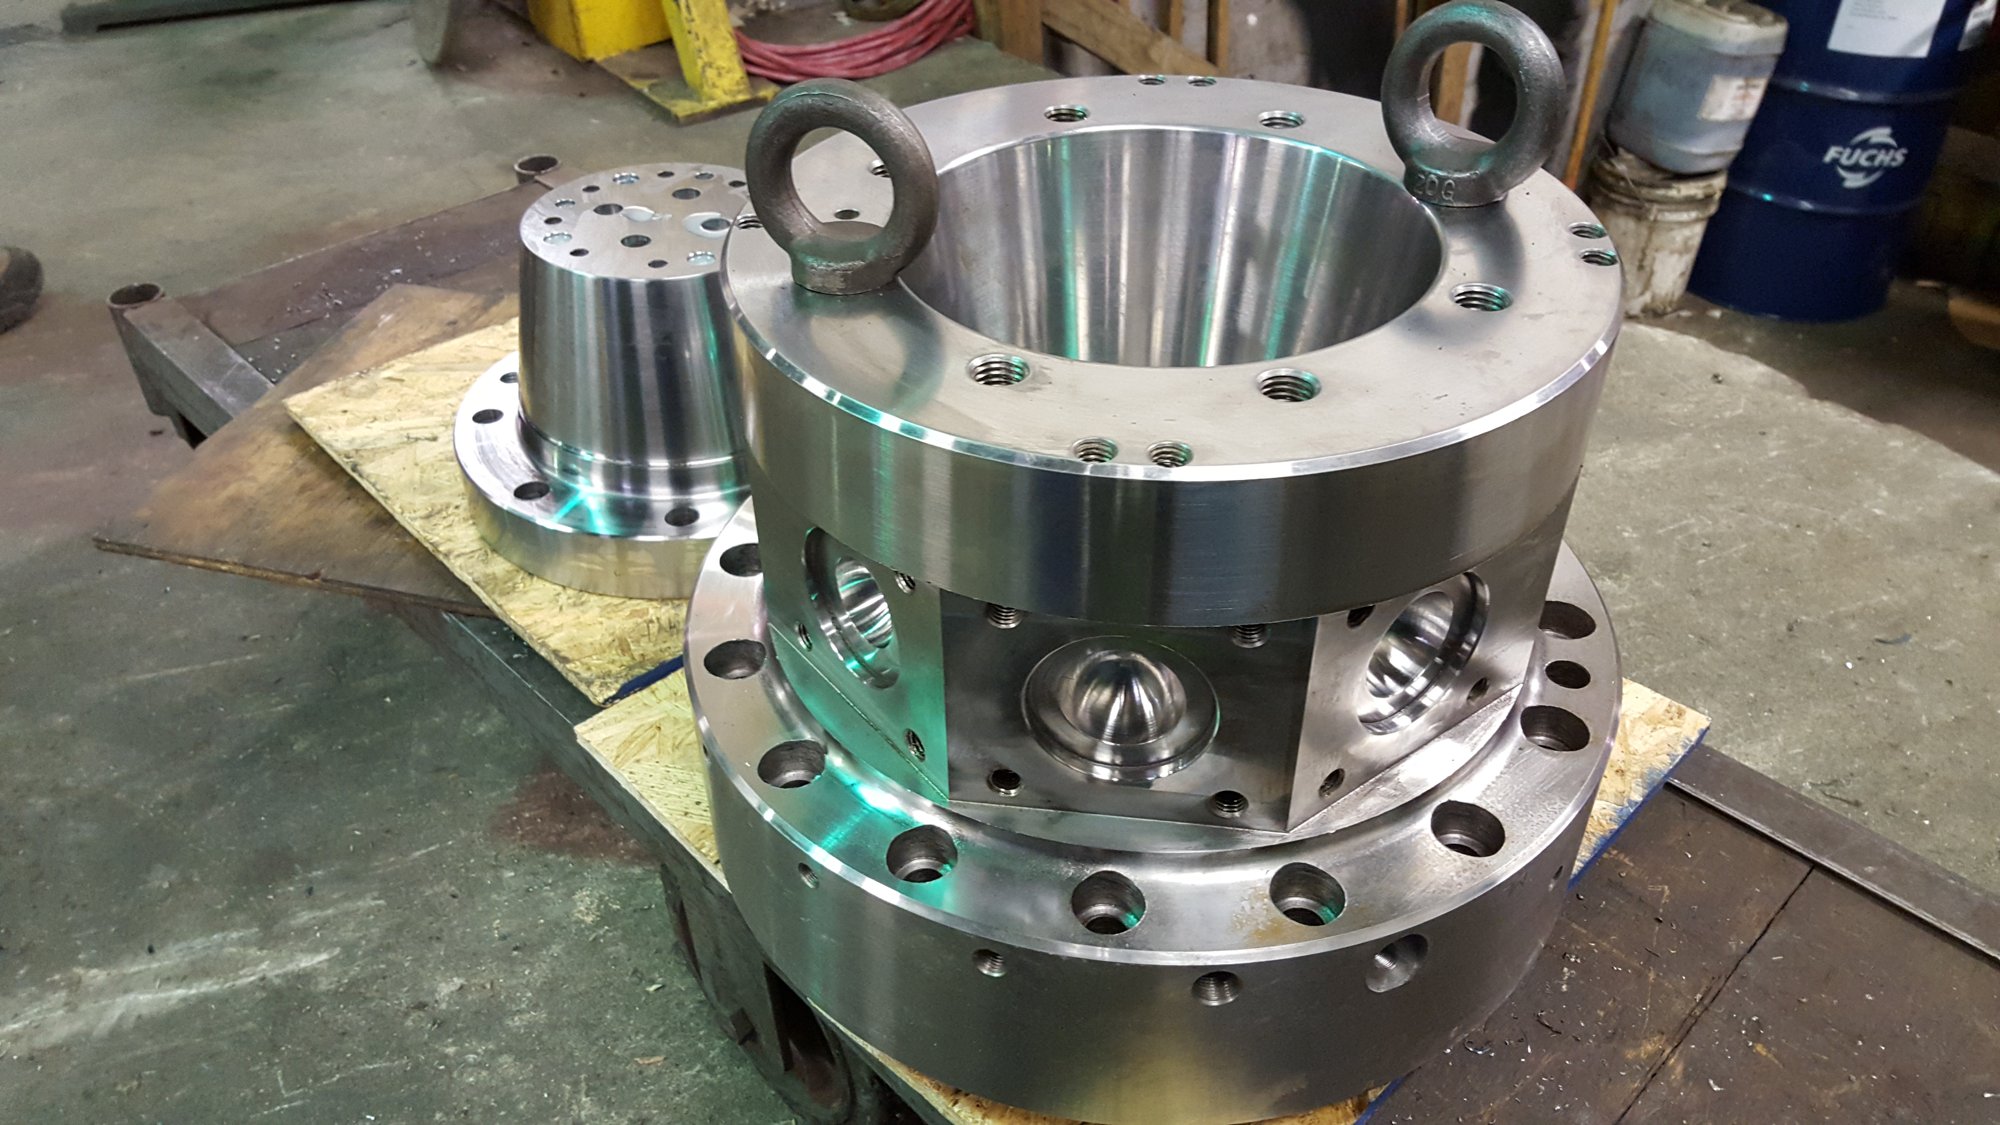
Large flanged die body with lifting eyes fitted, top bore and side ports finished
One die, start to finish (9 of 10): The die body, lifting eyes fitted
Large steel billet faced off on the boring mill table, jaws gripping the outside diameter
Large machining: Billet faced off on the boring mill table
Close detail of the helical spiral flights machined around a mandrel
Blown film dies: Helical flights machined around a mandrel
Extruder screw journal held in the mill-turn chuck, full length supported under the milling head
Extruder parts: Screw journal in the mill-turn, full length supported
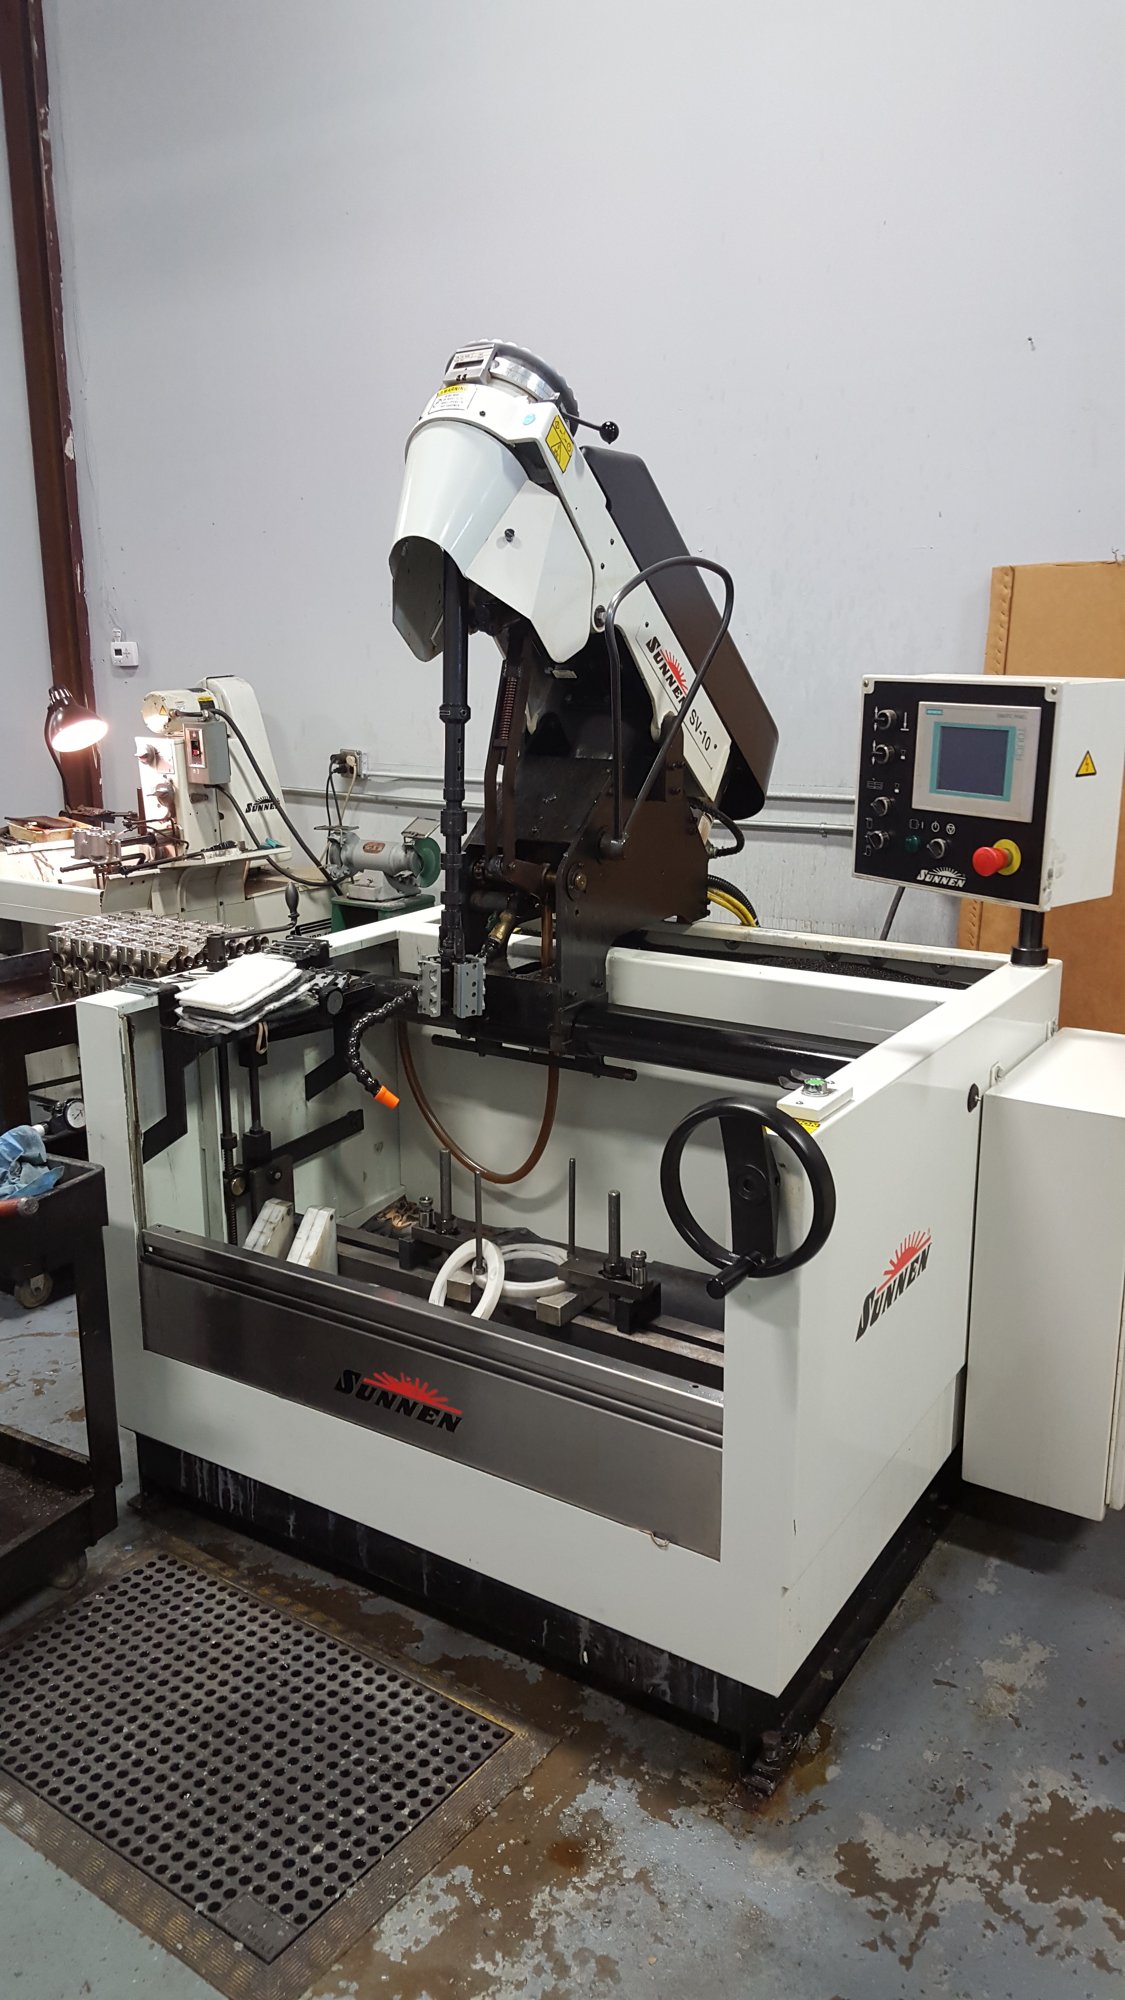
Sunnen honing machine on the shop floor set up for precision bore honing
Bore honing: The Sunnen honing machine
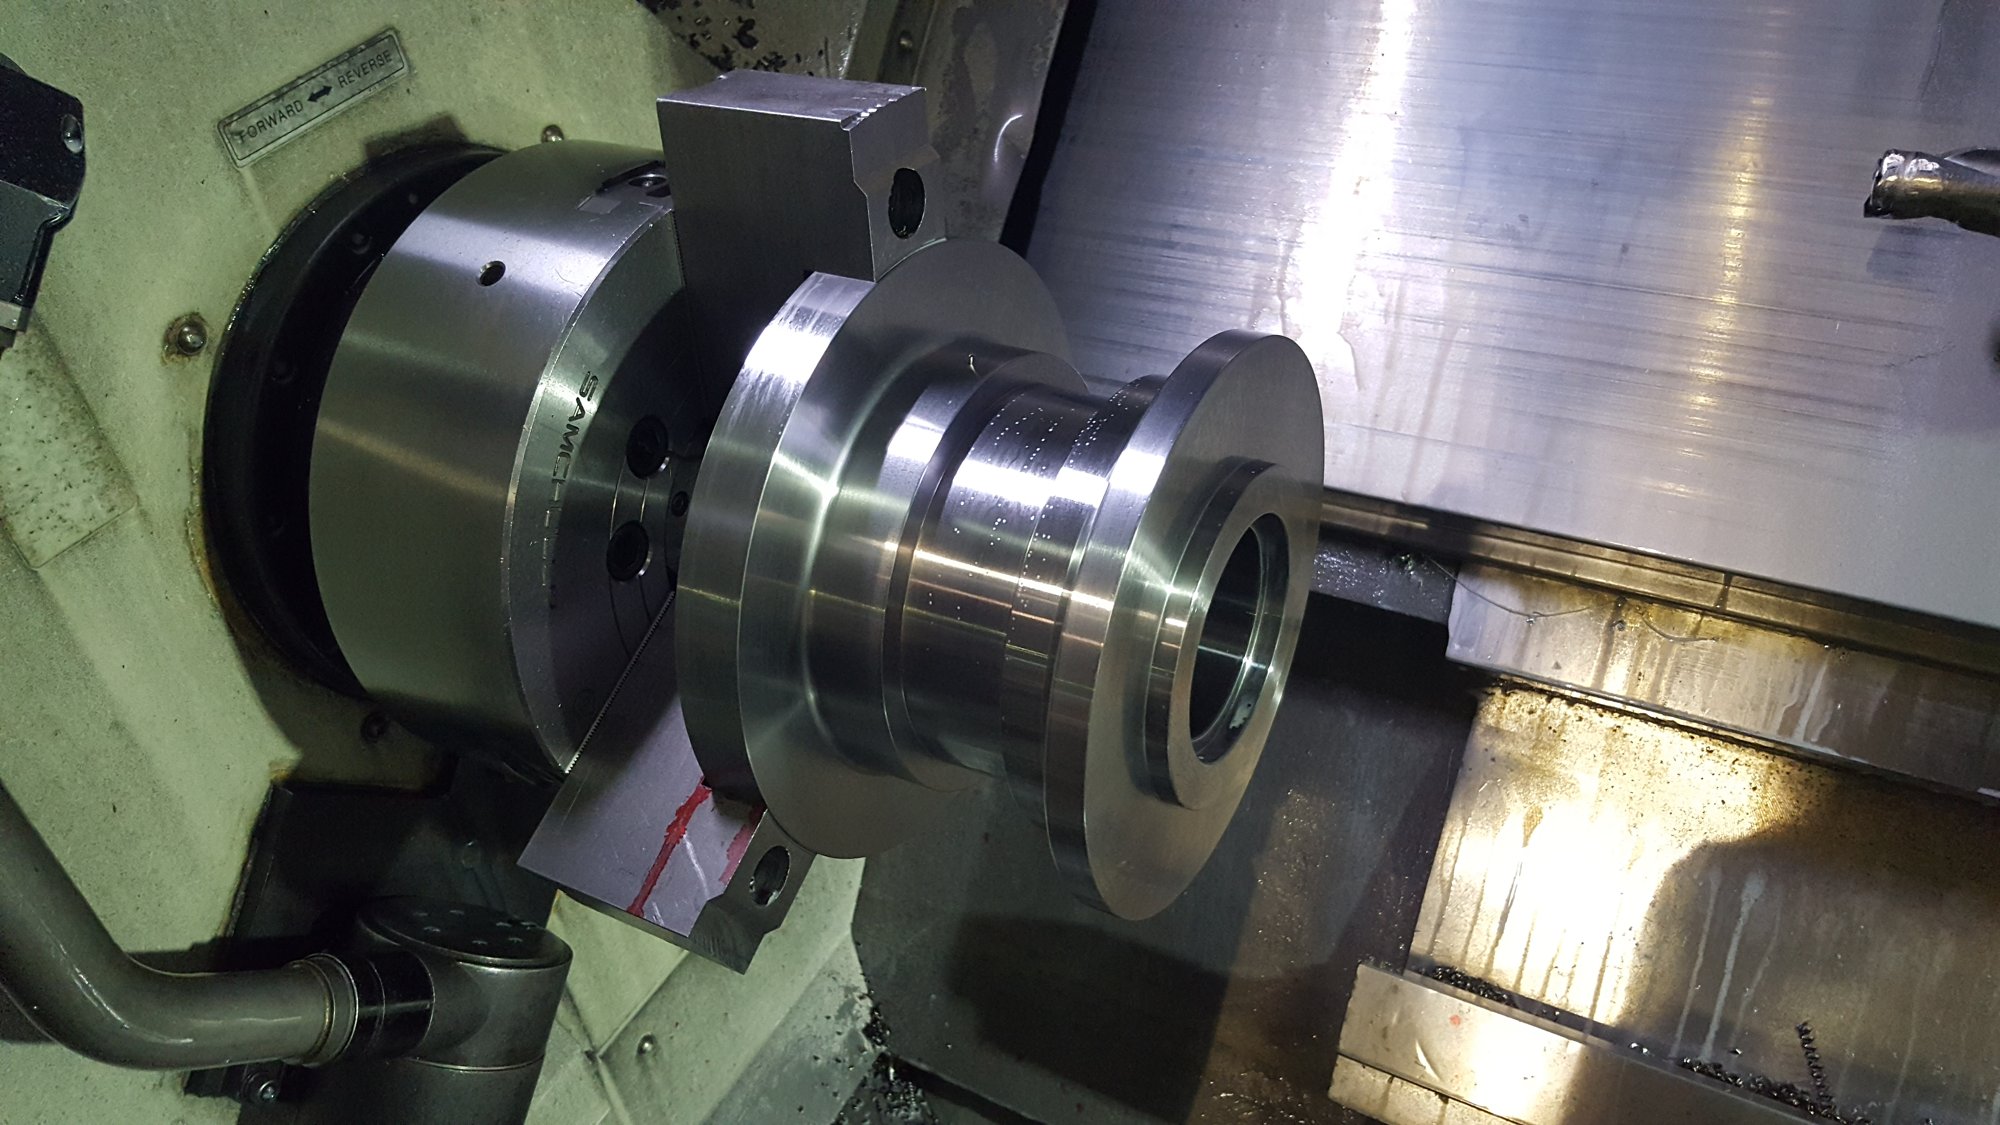
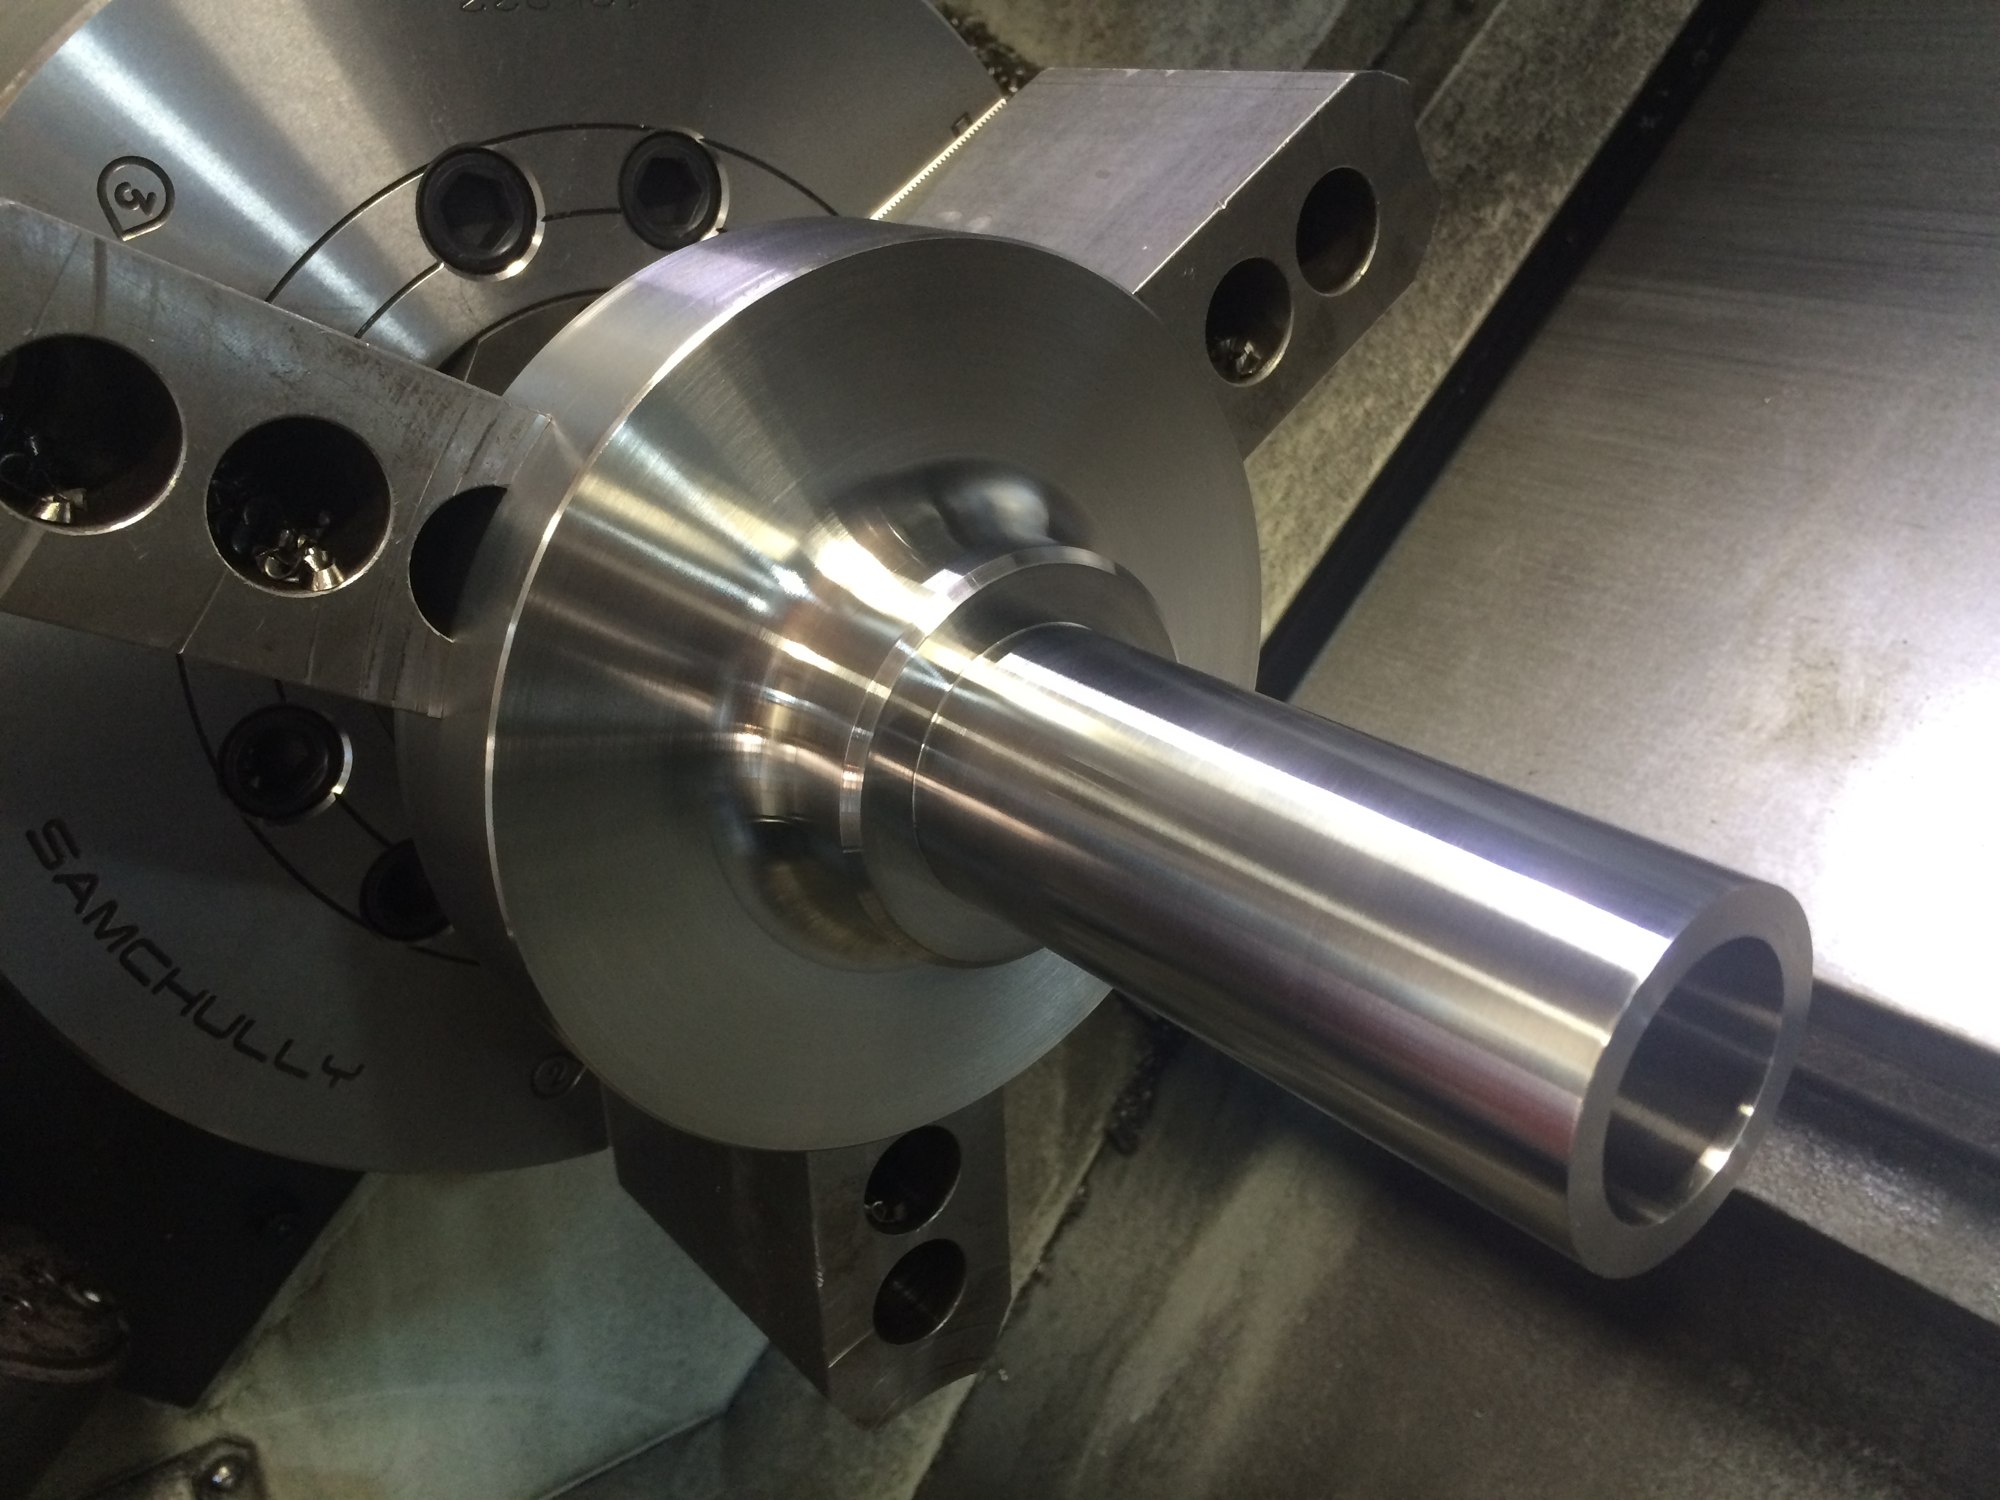
Stepped sleeve bored and turned in the Samchully chuck
Turning and production: Stepped sleeve bored and turned in the Samchully chuck
Machined cylindrical housing finished on the bench, stacked sections bolted at the top flange
Large machining: Stacked housing sections bolted at the top flange
Inner face of a spiral mandrel, flow channels cut around the central hub
Blown film dies: Inner face of a spiral mandrel, channels round the hub
Long steel shaft set up between centres on the manual engine lathe
Shaft machining: Long shaft between centres on the engine lathe
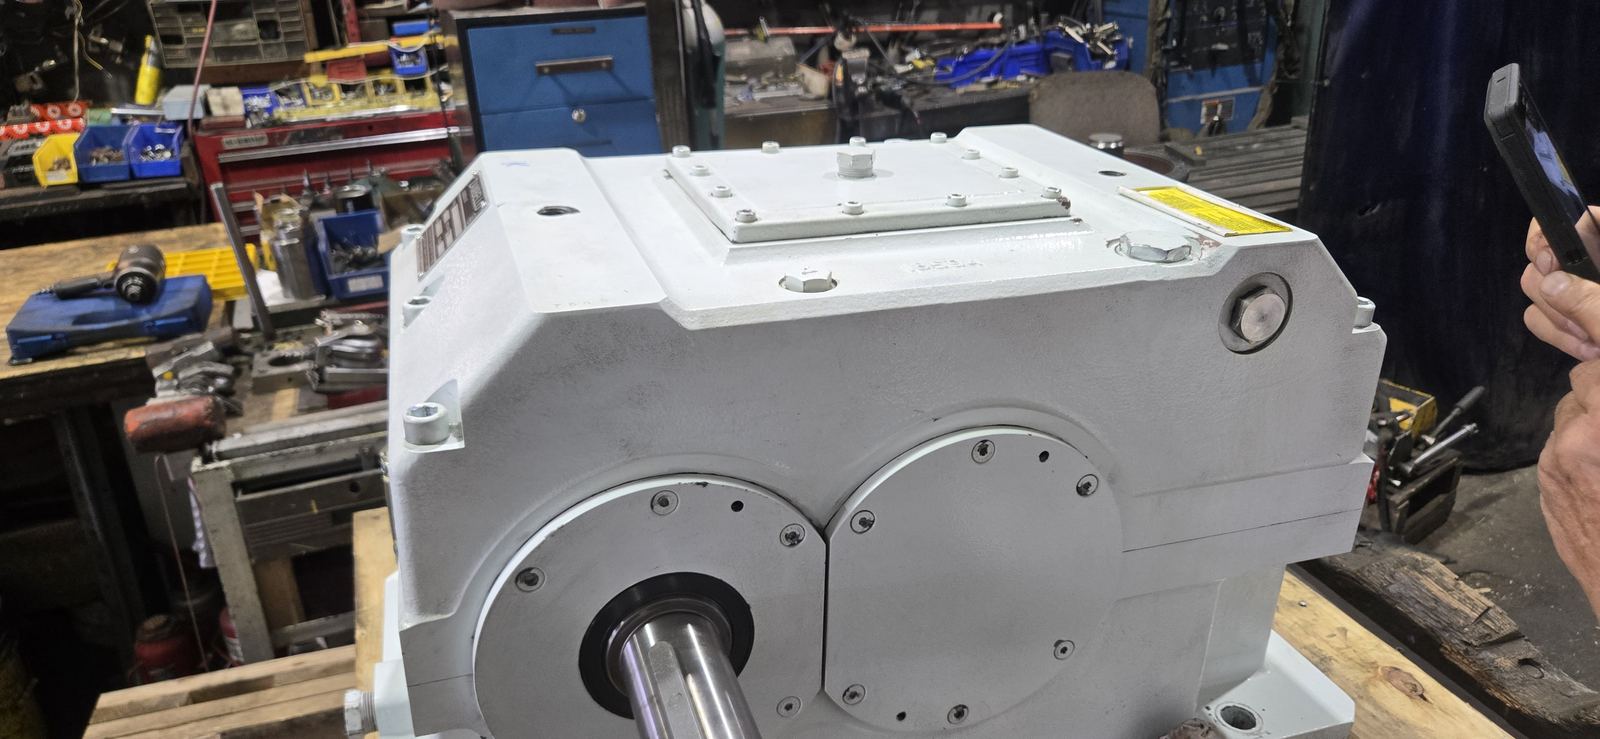
Assembled industrial gearbox on the pallet with its output shafts and bearing in place
Gearbox repair: Assembled gearbox with its output shafts in place
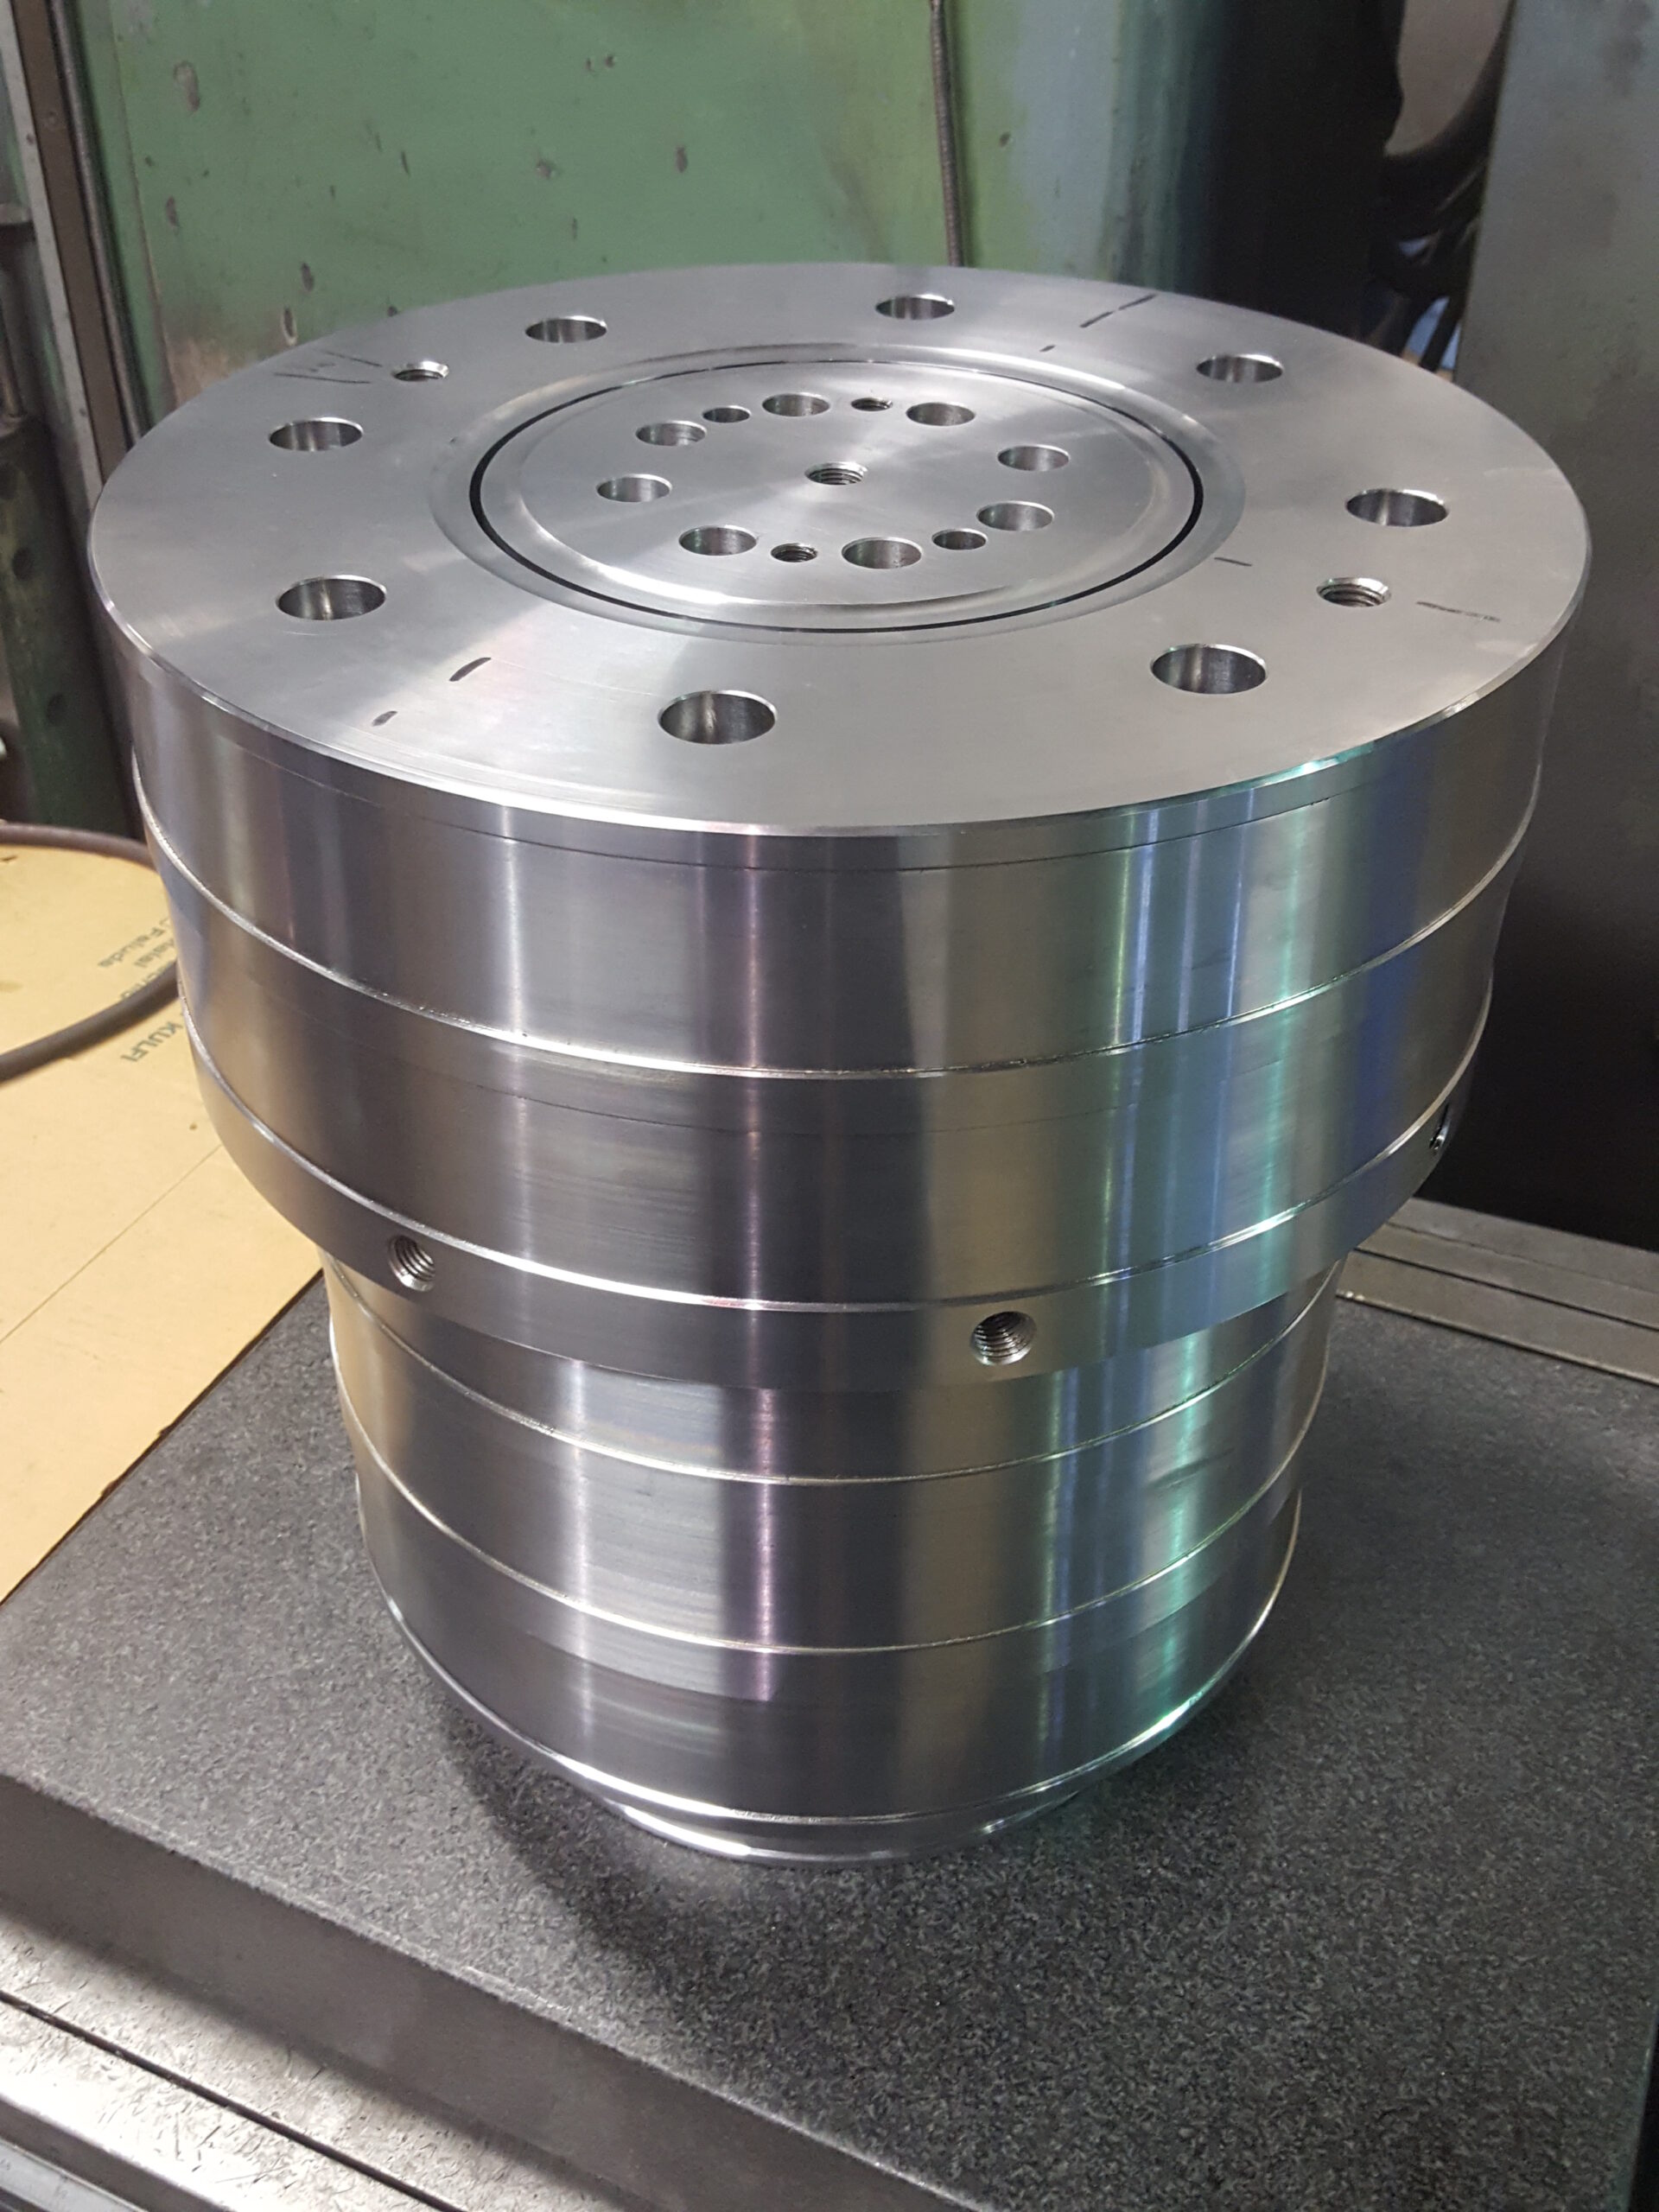
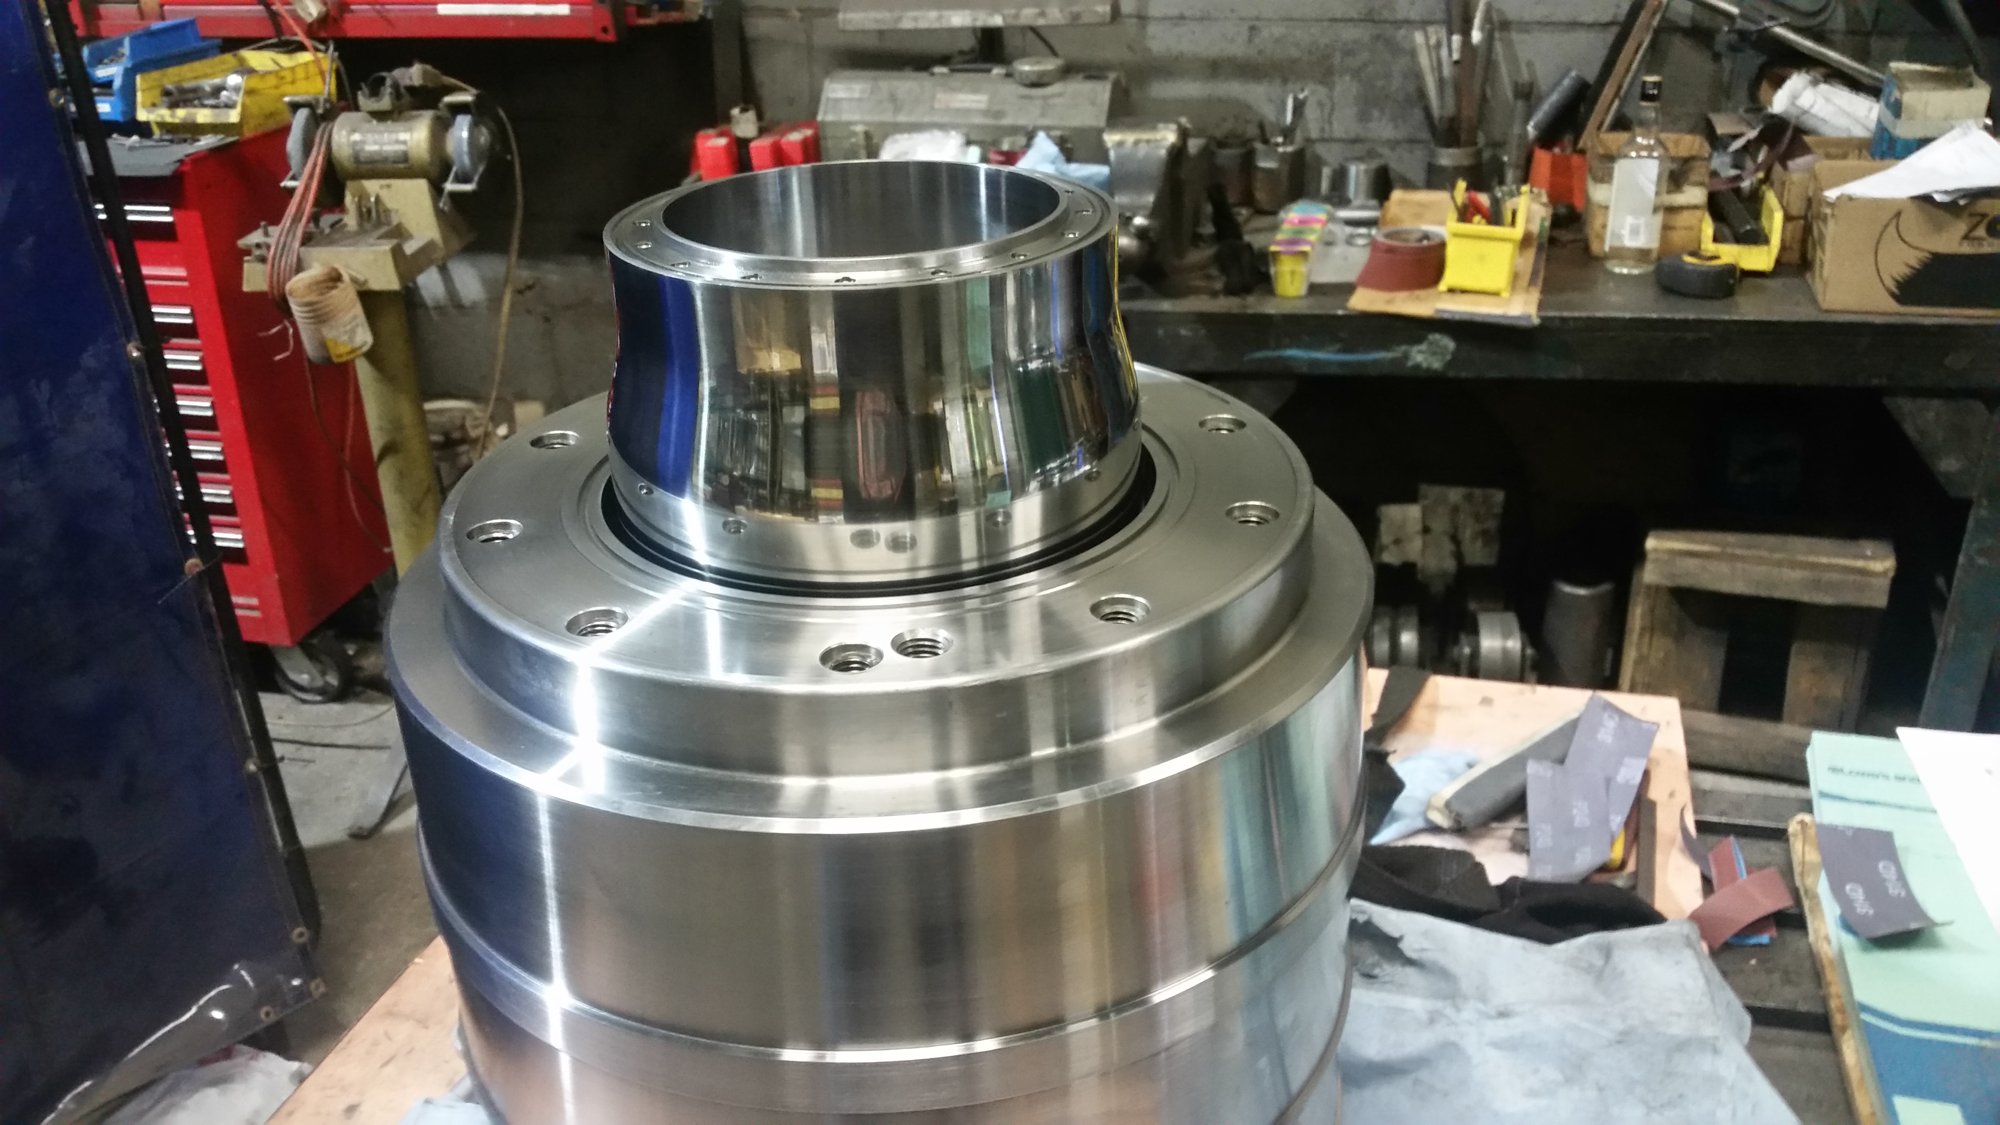
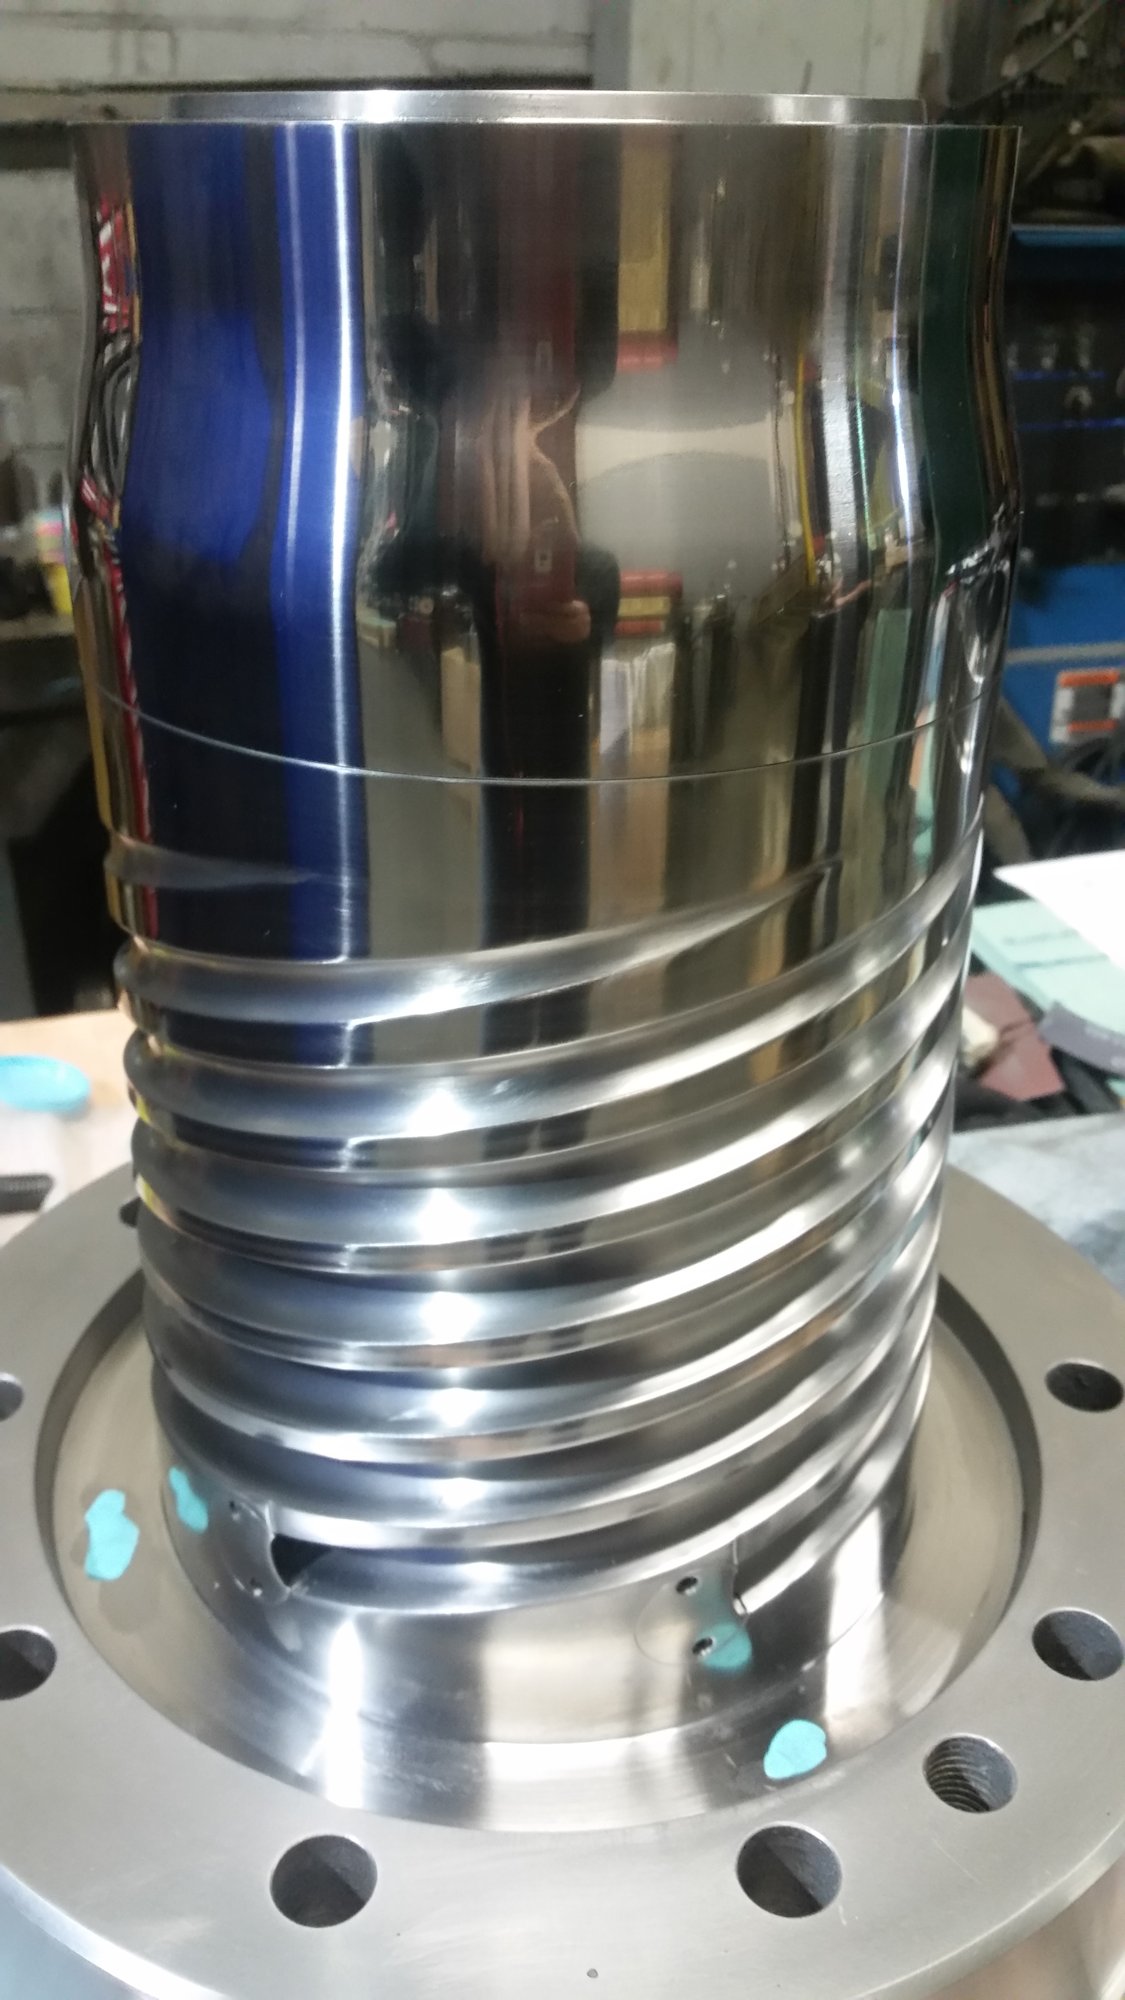
Spiral mandrel standing upright on its bolted mounting flange, flights spiralling up to the polished body
Blown film dies: Spiral mandrel upright on its bolted flange
Machined body lifted on slings from its lifting eye, timber blocks set to land it on
Fabrication and shipping: Machined body lifted on slings, landing on timber
The Zala Machine shop floor in Hillsborough, New Jersey, machines and gantry cranes across the bay
The shop: The shop floor in Hillsborough, New Jersey
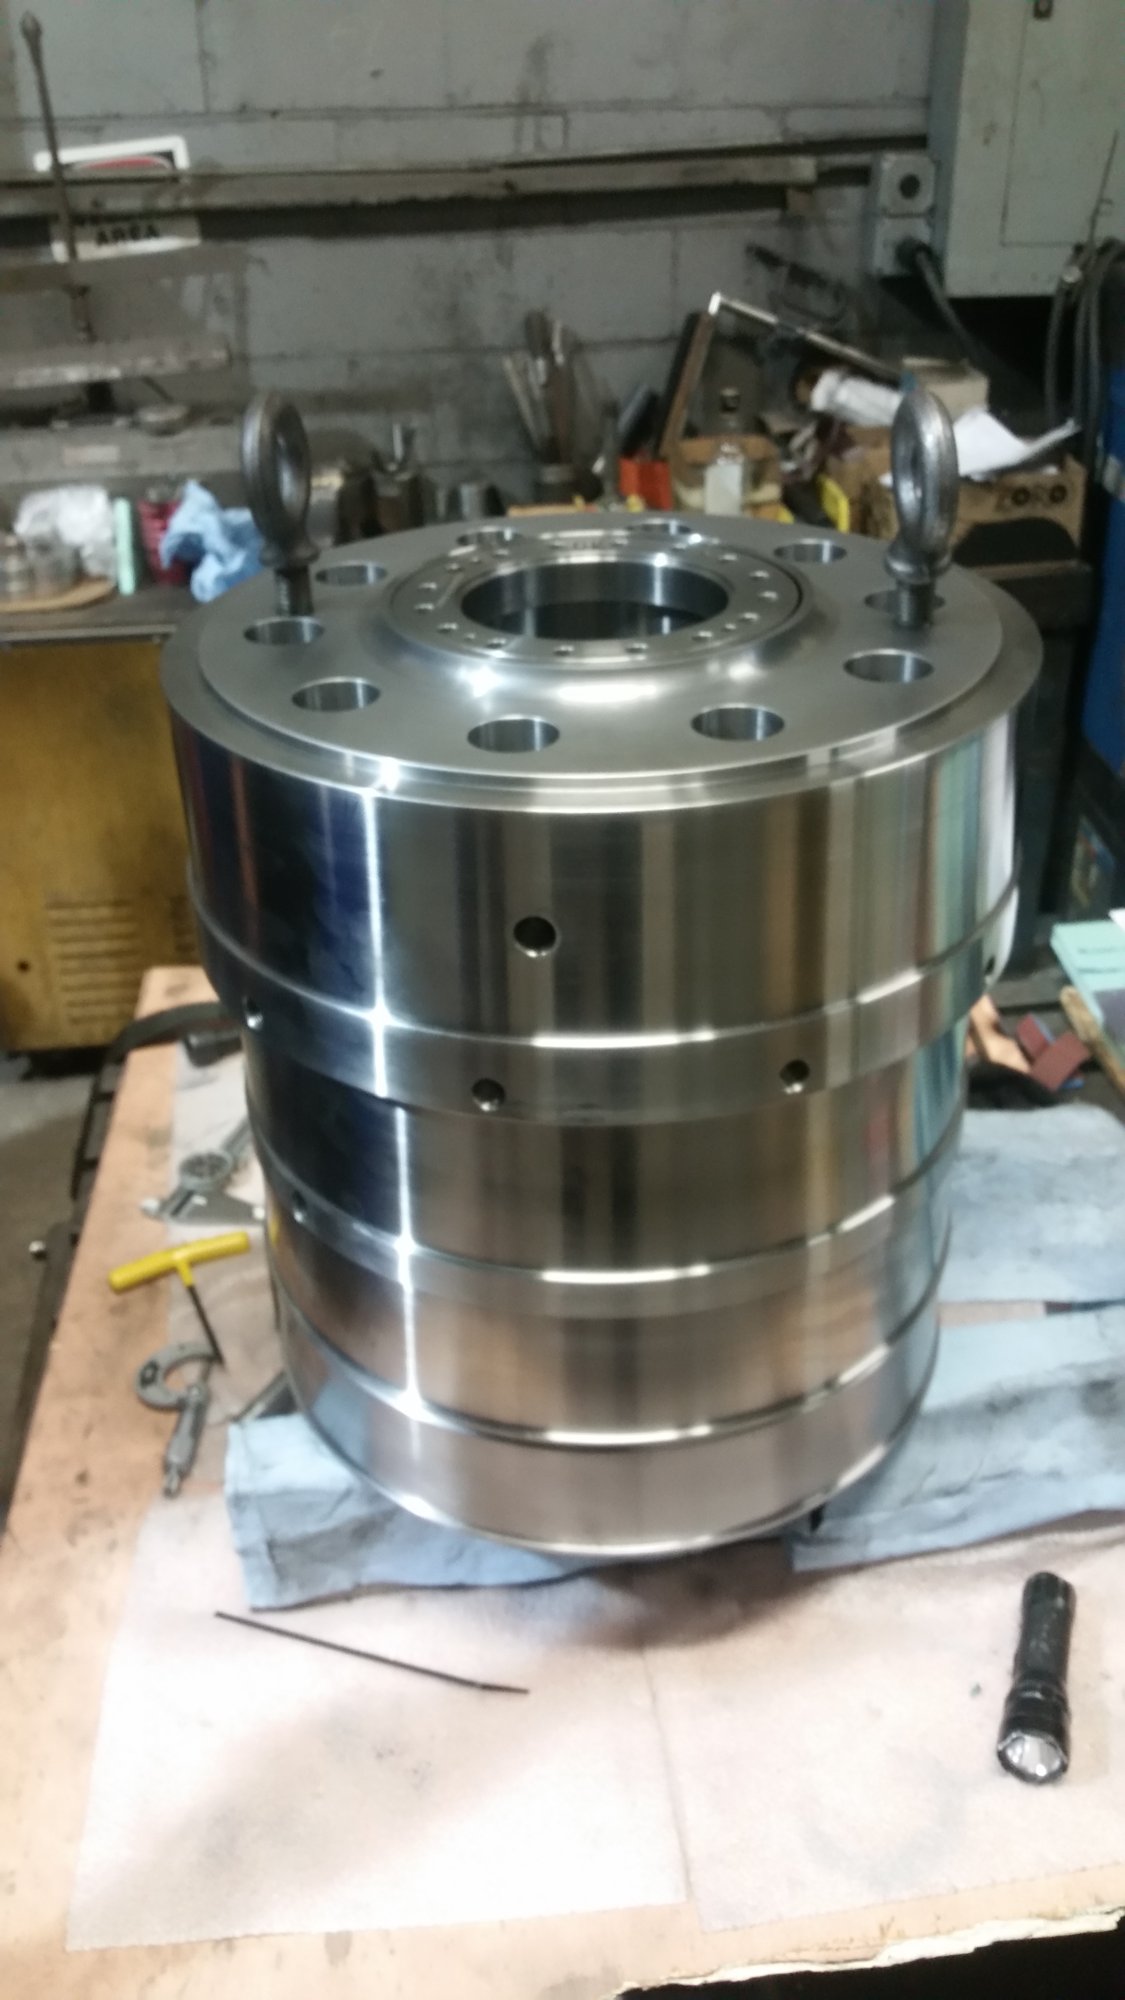
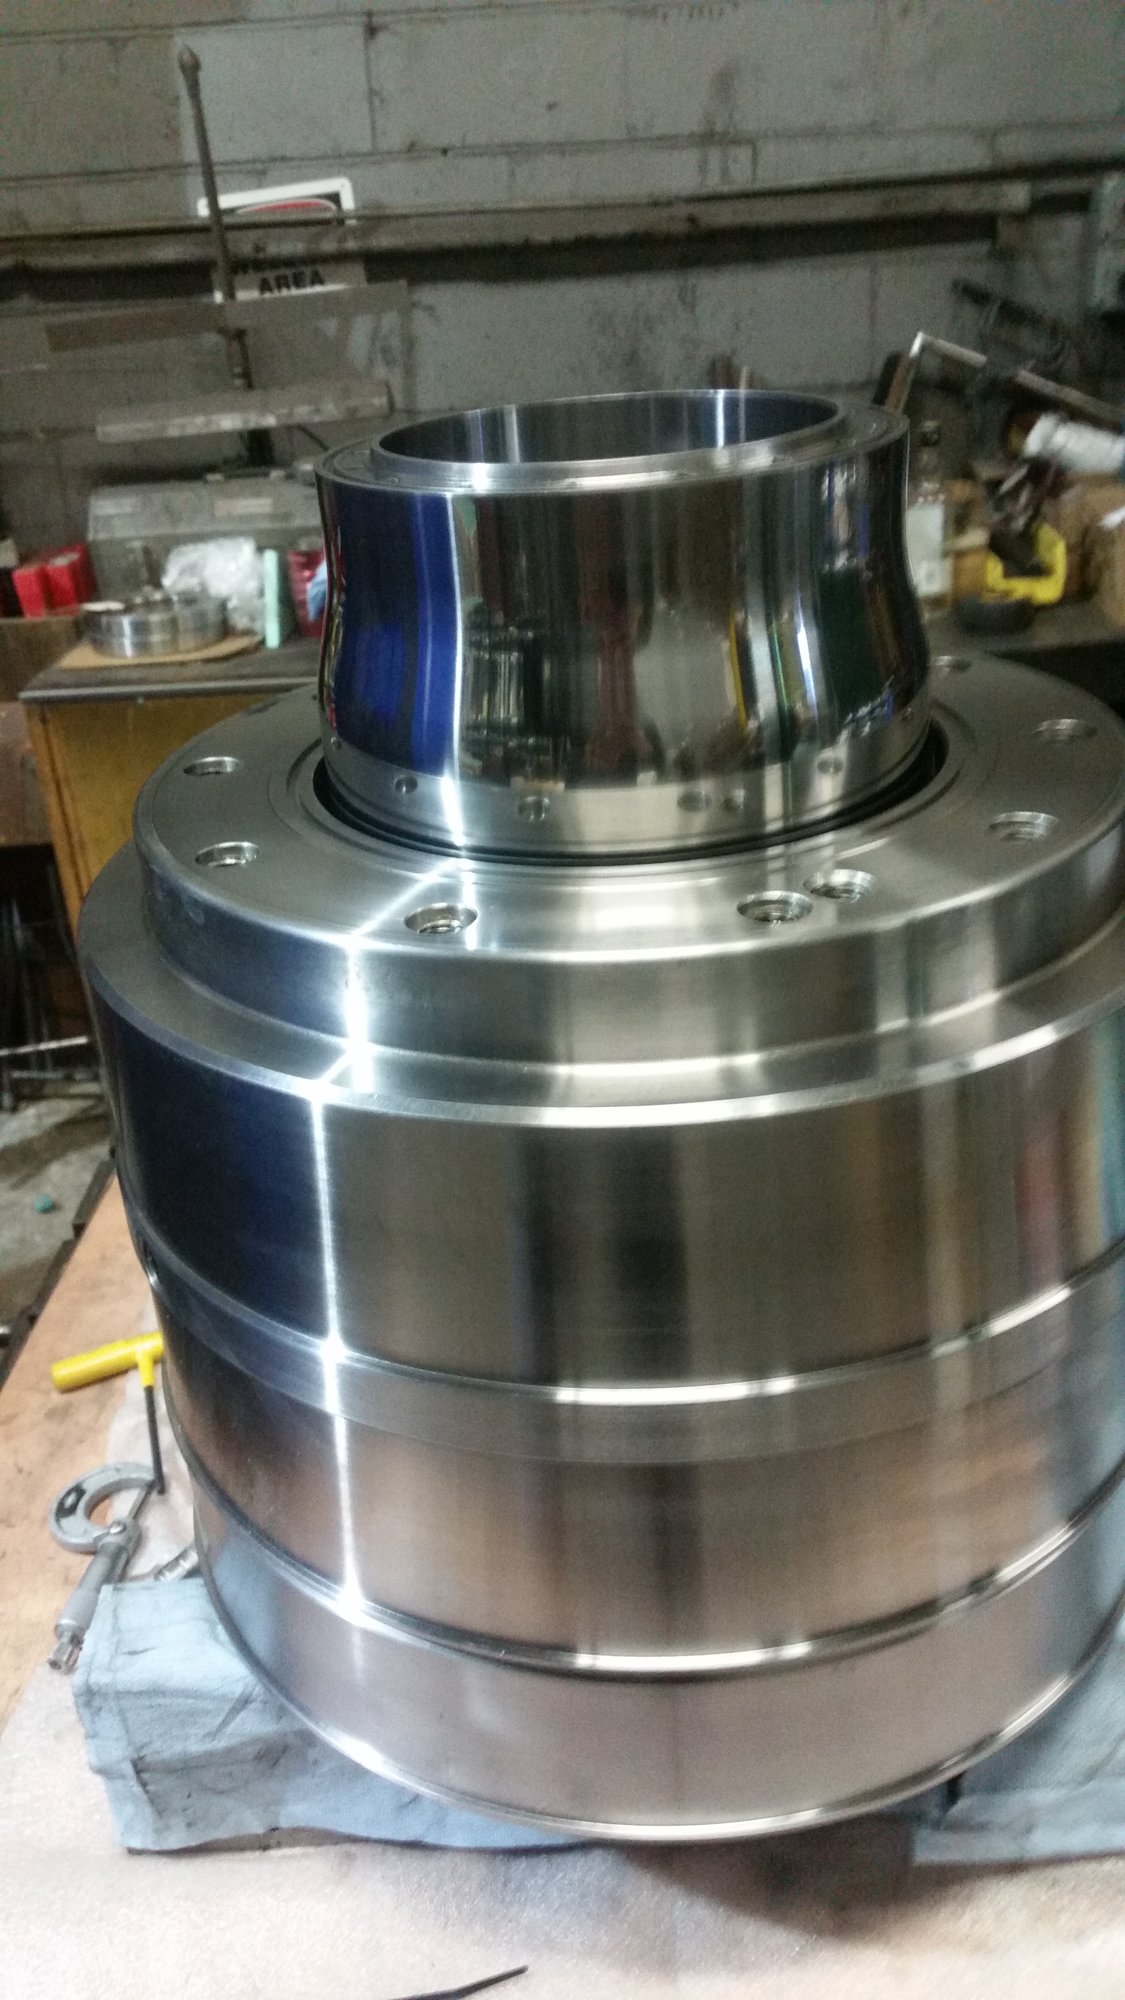
Blown film die housing assembled from its stacked machined sections, polished neck at the top
One die, start to finish (10 of 10): Assembled and stacked, ready to go back
Extruder screw tip and flight run-out finished on the mill-turn, chuck holding the drive end
Extruder parts: Screw tip and flight run-out finished on the mill-turn
Turned steel roll on the pallet, threaded journal machined at the end
Turning and production: Turned roll with a threaded journal
Top of the machined housing body, outer bolt flange and inner bolt circle around the bore
Large machining: Housing top, outer flange and inner bolt circle
Tapered die bodies finished on their mounting flanges, bolt circles drilled
Blown film dies: Tapered die bodies finished on their mounting flanges

What's in the gallery

One Die, Start to Finish

A three-layer blown film die block, from the billet that came in on a pallet to the assembled die. One job, nine photographs, in order. More on extruder components.

Blown Film Dies, Mandrels and Distribution Plates

Spiral mandrels, die bodies, flange rings and distribution plates machined from 4140HT and stainless for blown film and sheet extrusion lines. More on extruder components.

Extruder Screws, Adapters and Breaker Plates

Feed screw modification, adapters and journal work for single and twin screw extruders, cut on the mill-turn in one setup where the geometry allows. Breaker plates drilled in 15-5 PH stainless. More on extruder components.

Gearbox Repair and Rebuild

Gearboxes stripped, measured, line-bored in house and re-timed. Bearings and seals run one to two weeks; a full rebuild four to eight. More on industrial gearbox repair.

Large Machining and Boring

Boring, facing and drilling on parts too big for a lathe — we lift to 10 tons and line-bore to 20in diameter across a 50in span. More on large part machining.

Turning and Production Runs

Production runs, small batches and one-offs machined to a customer’s drawings, every piece the same as the last. More on CNC turning.
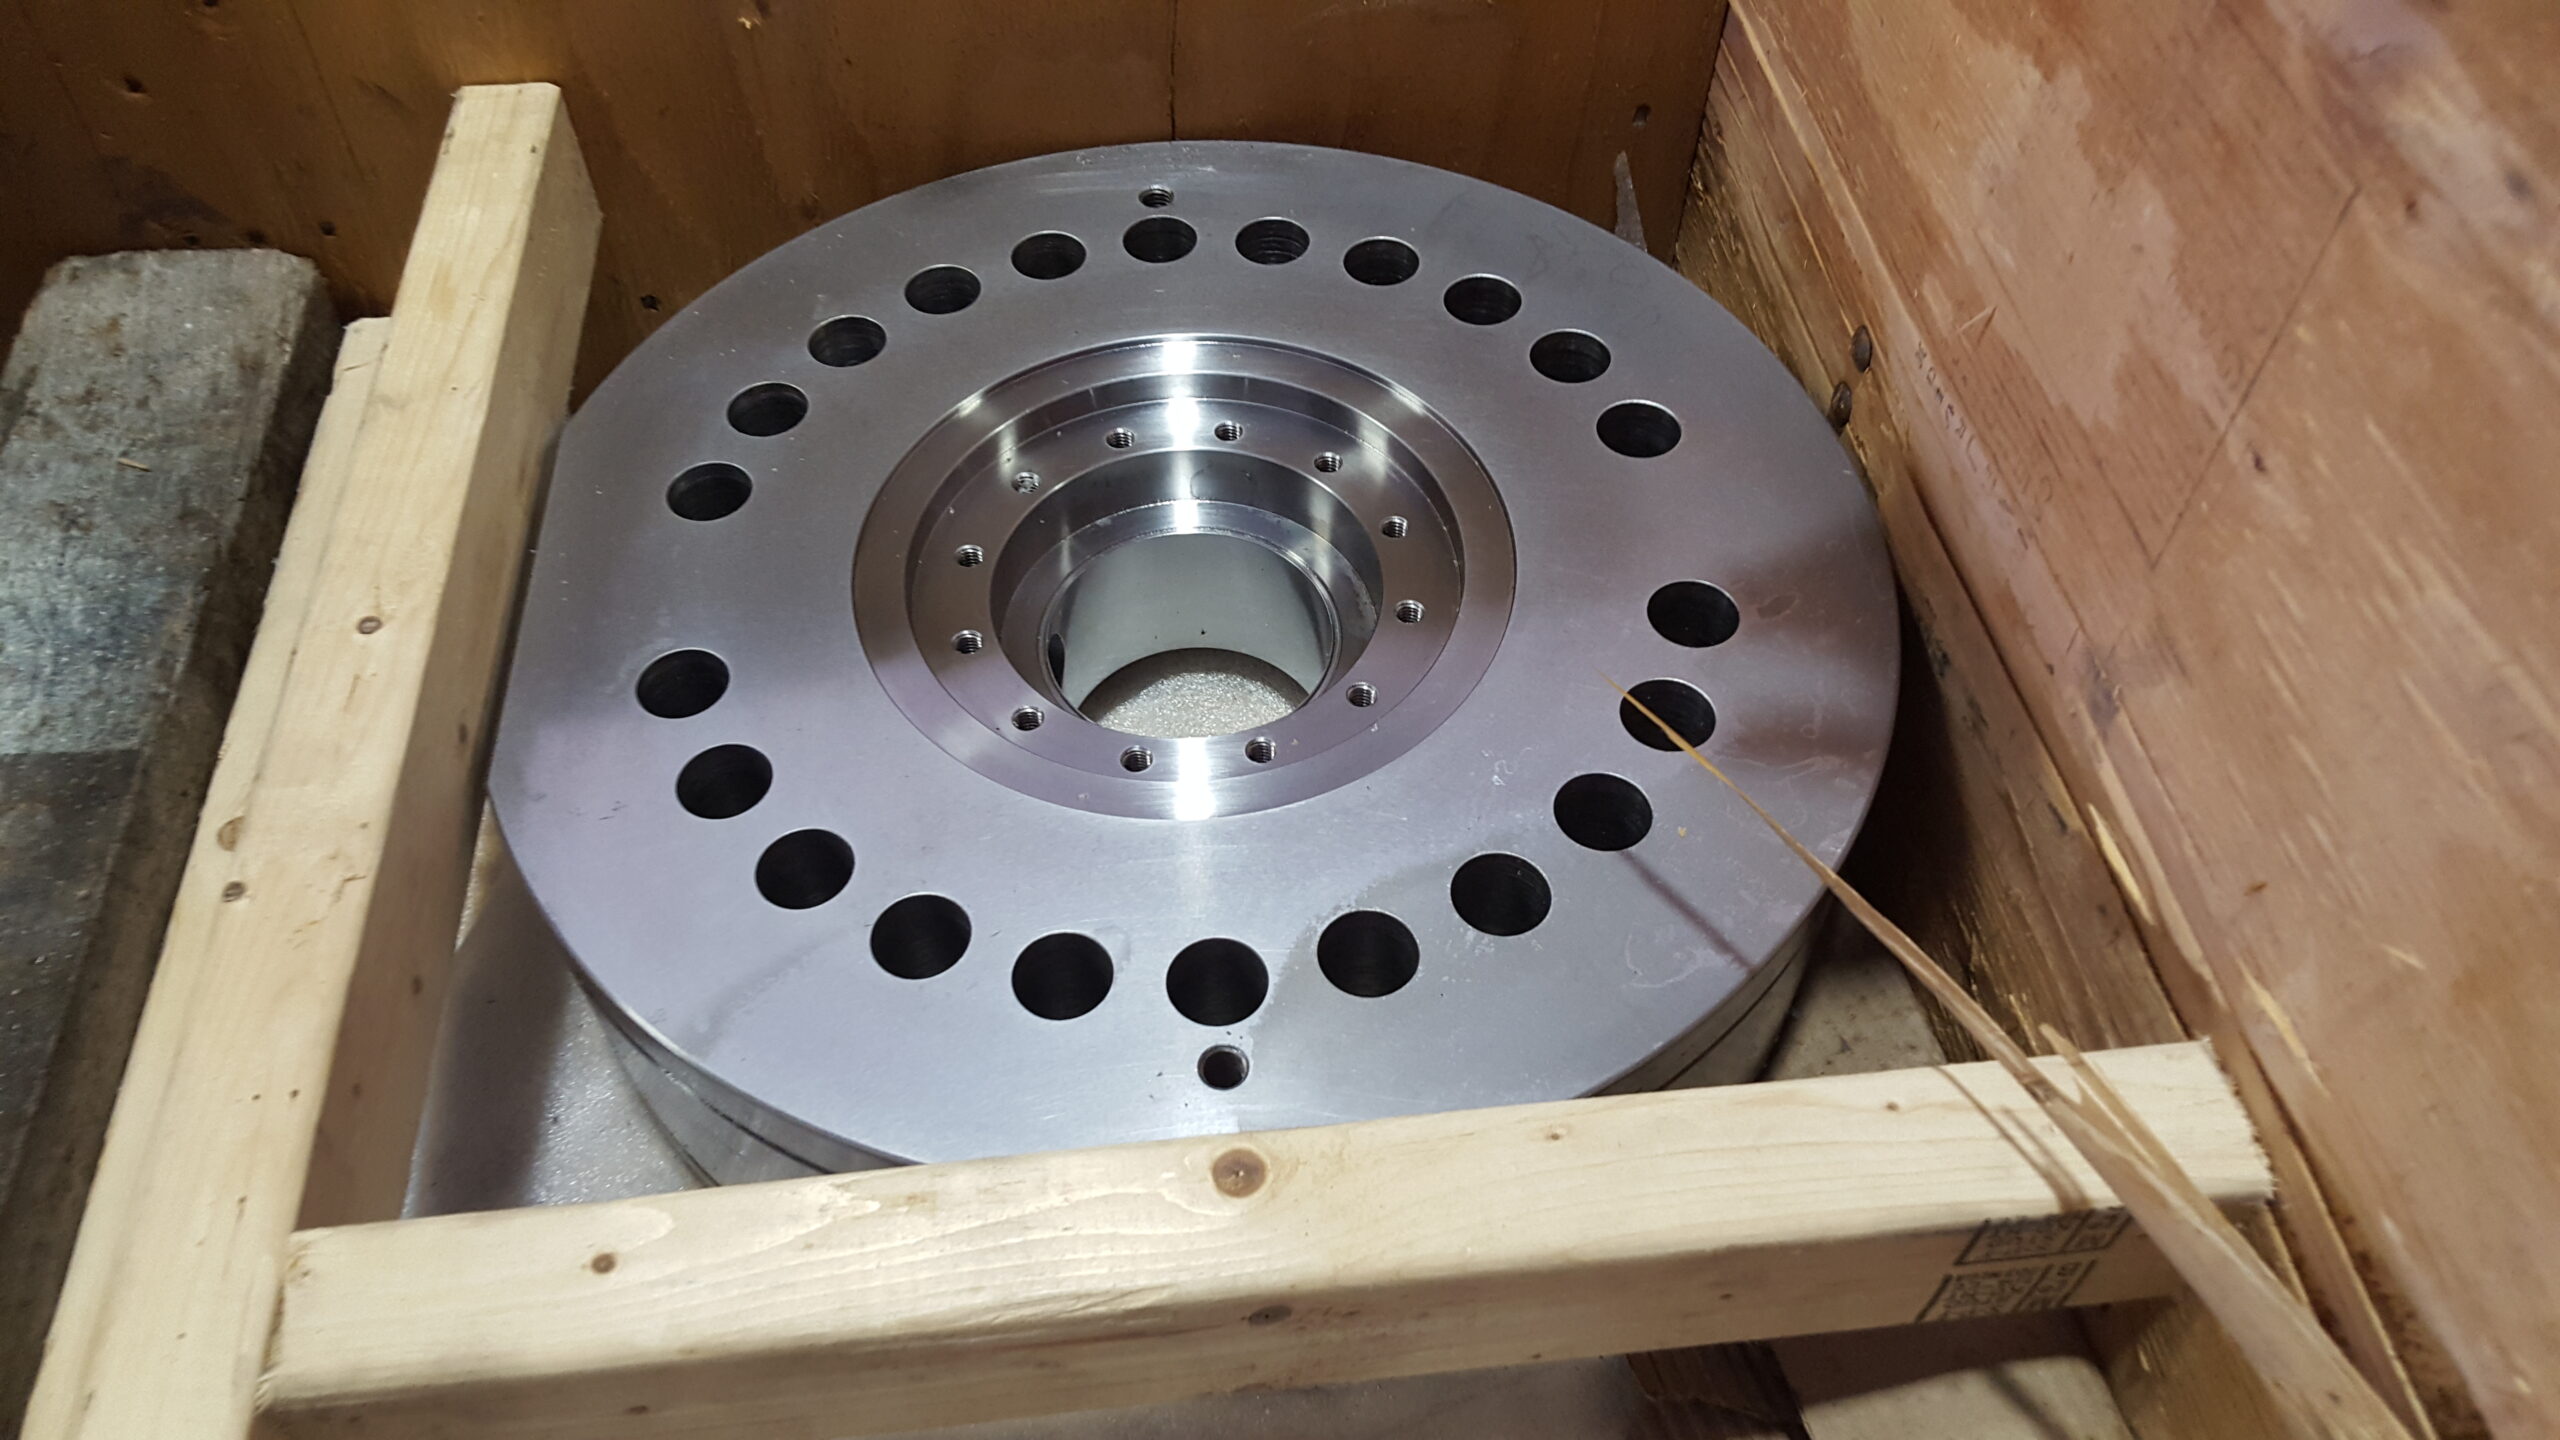
Shaft Machining

Shafts turned between centres and carried in the steady rest, with keyways, splines and threads cut on the same setup. More on shaft machining.
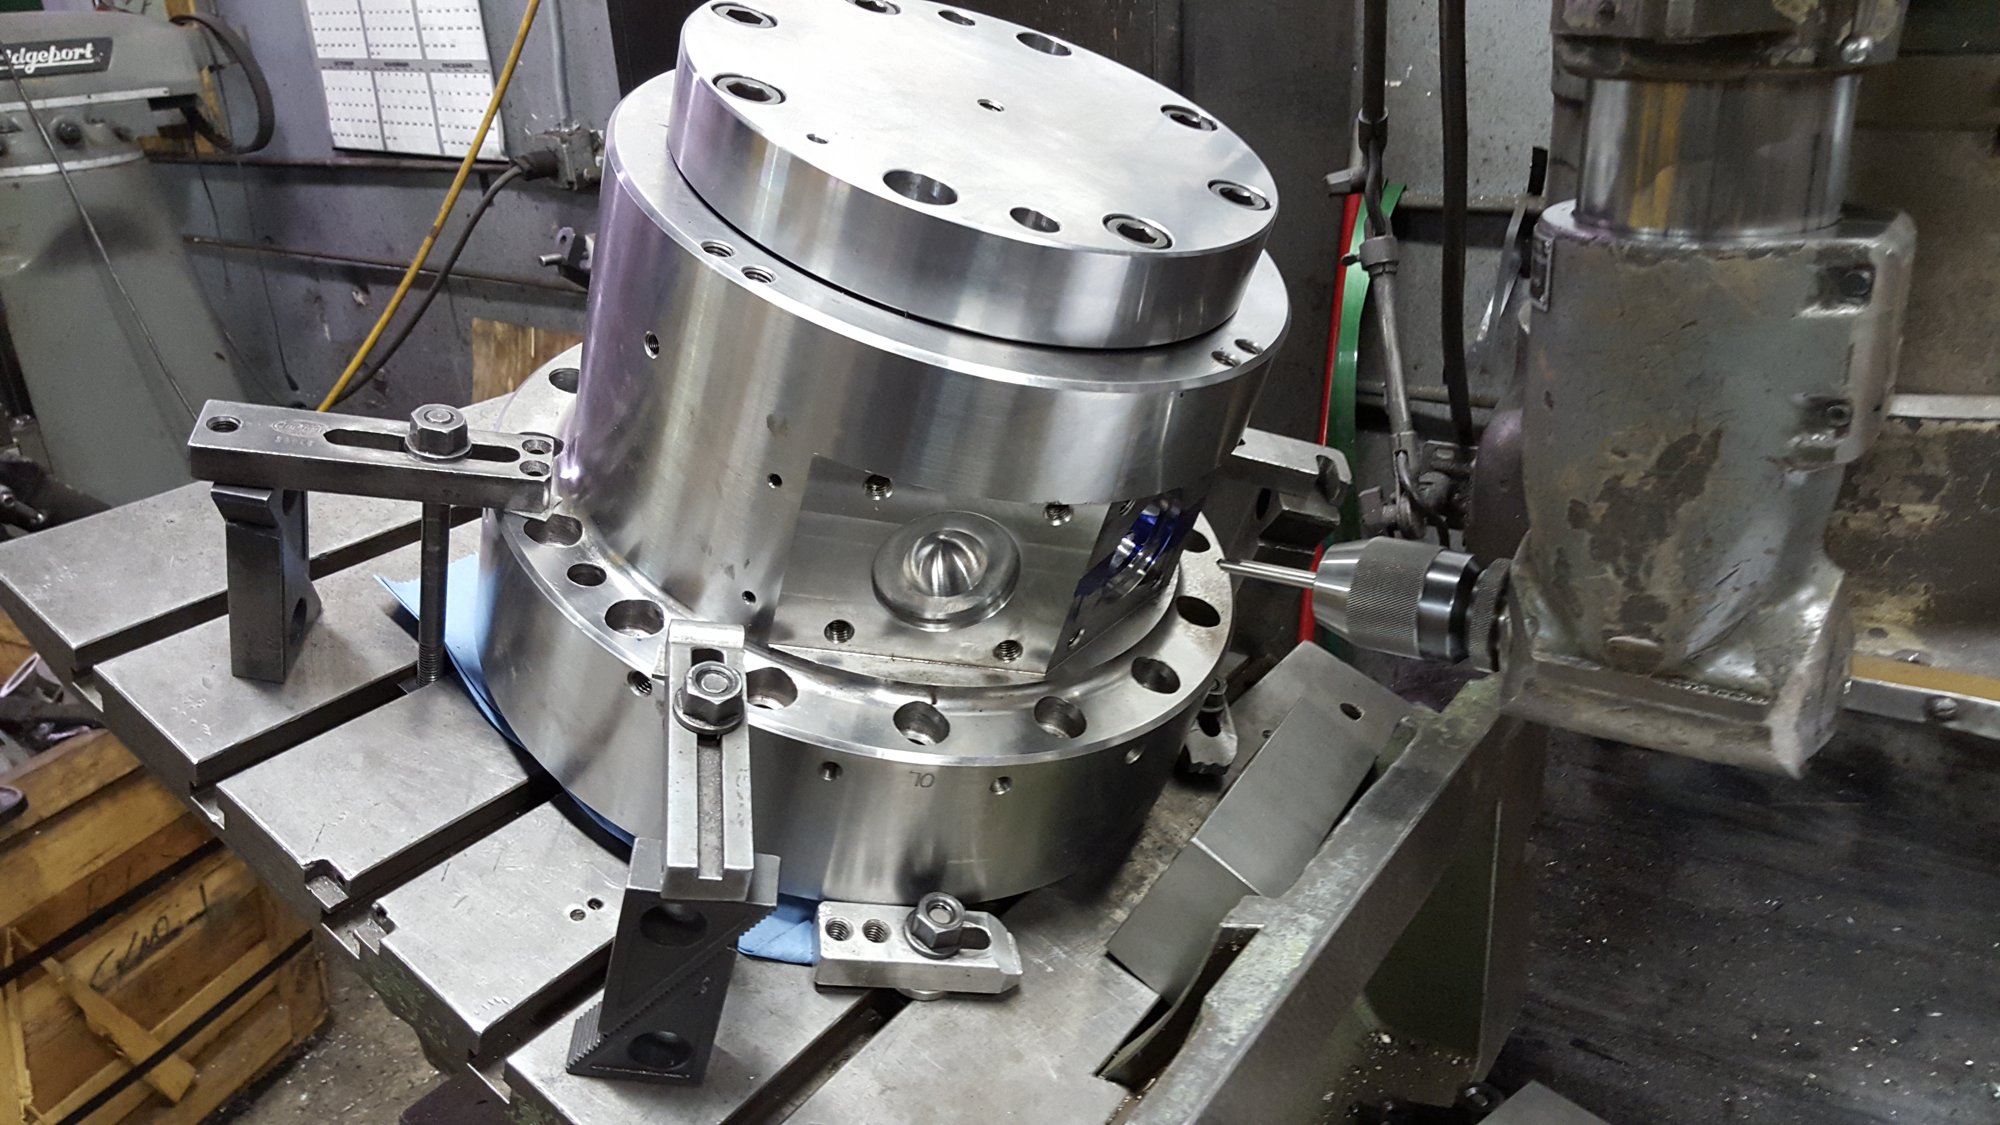
Bore Honing

Bore honing on the Sunnen, for finish and size on cylinders, sleeves and liners. More on bore honing.

Fabrication, and Out the Door

Weldments machined after welding, and finished parts crated and delivered on our own truck. More on large fabrication.

The Shop

The floor in Hillsborough, New Jersey: the machines, the programs and the people running them. See the facility list.