Home / Extruder Components
Machined, repaired and polished in Hillsborough, New Jersey, by a shop that learned extrusion from the inside. Tap a component to jump to it.
Stanley Zala spent his career at one of the major extruder OEMs — a company that builds the extruders, dies and processing lines this page is about. He machined their parts and learned the equipment from the inside: which tolerances matter in a feed section, and how melt actually moves through the metal.
In 2002 he opened Zala Machine Co. in Hillsborough to support the plants nearby. What he learned did not stay with him. He taught it to his son Martin, who runs the shop today, and to his grandson Gabriel, who has been on the floor since he was old enough to help. Just as much of it went to the machinists who work beside them. When one of them sets up a die body or checks a breaker plate, they are working to a standard that came off an extruder builder’s shop floor — and we have kept machining for the major extruder OEMs ever since.
Most of it is made to your drawing. When there is no drawing, we measure the worn part and make the new one from that. Replacement and spare parts for single and twin-screw extruders are the bulk of this work — including parts for lines the original builder no longer supports.
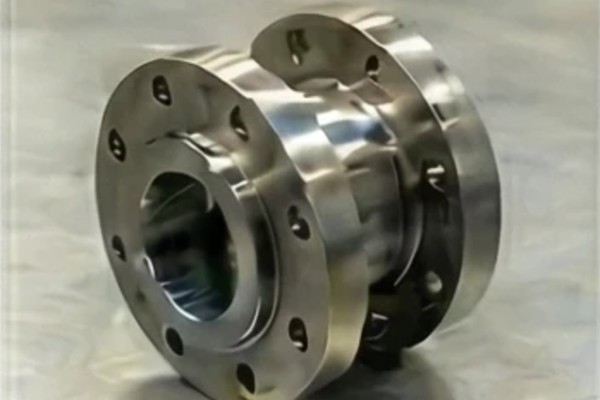
The adapter that joins the gearbox to the extruder, bored and faced so the gearbox output and the screw stay concentric.
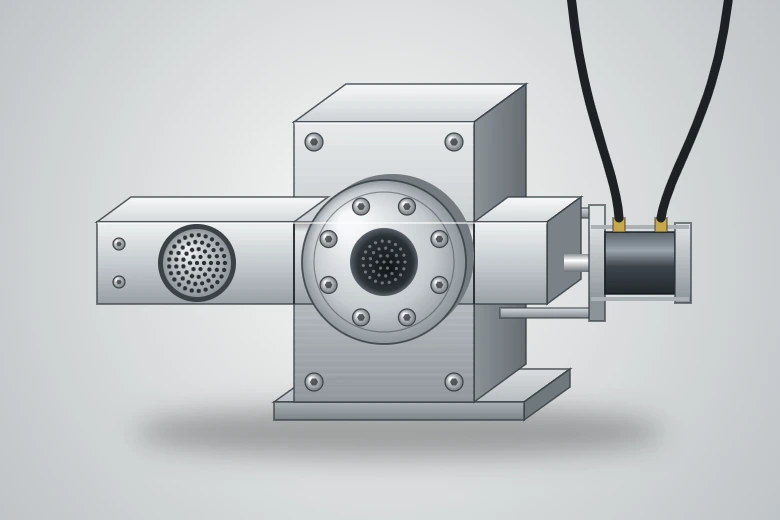
Screen changer bodies, slide plates and screen carriers, machined to your drawing or measured from the worn part.
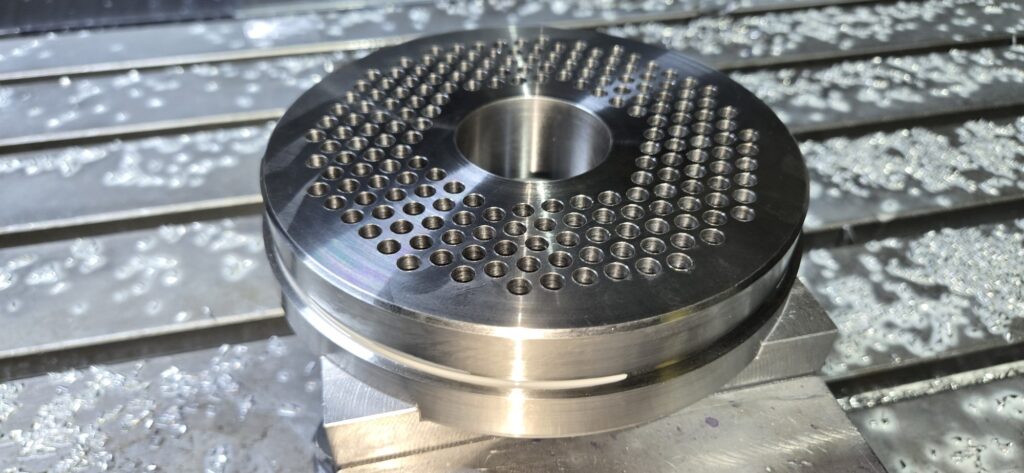
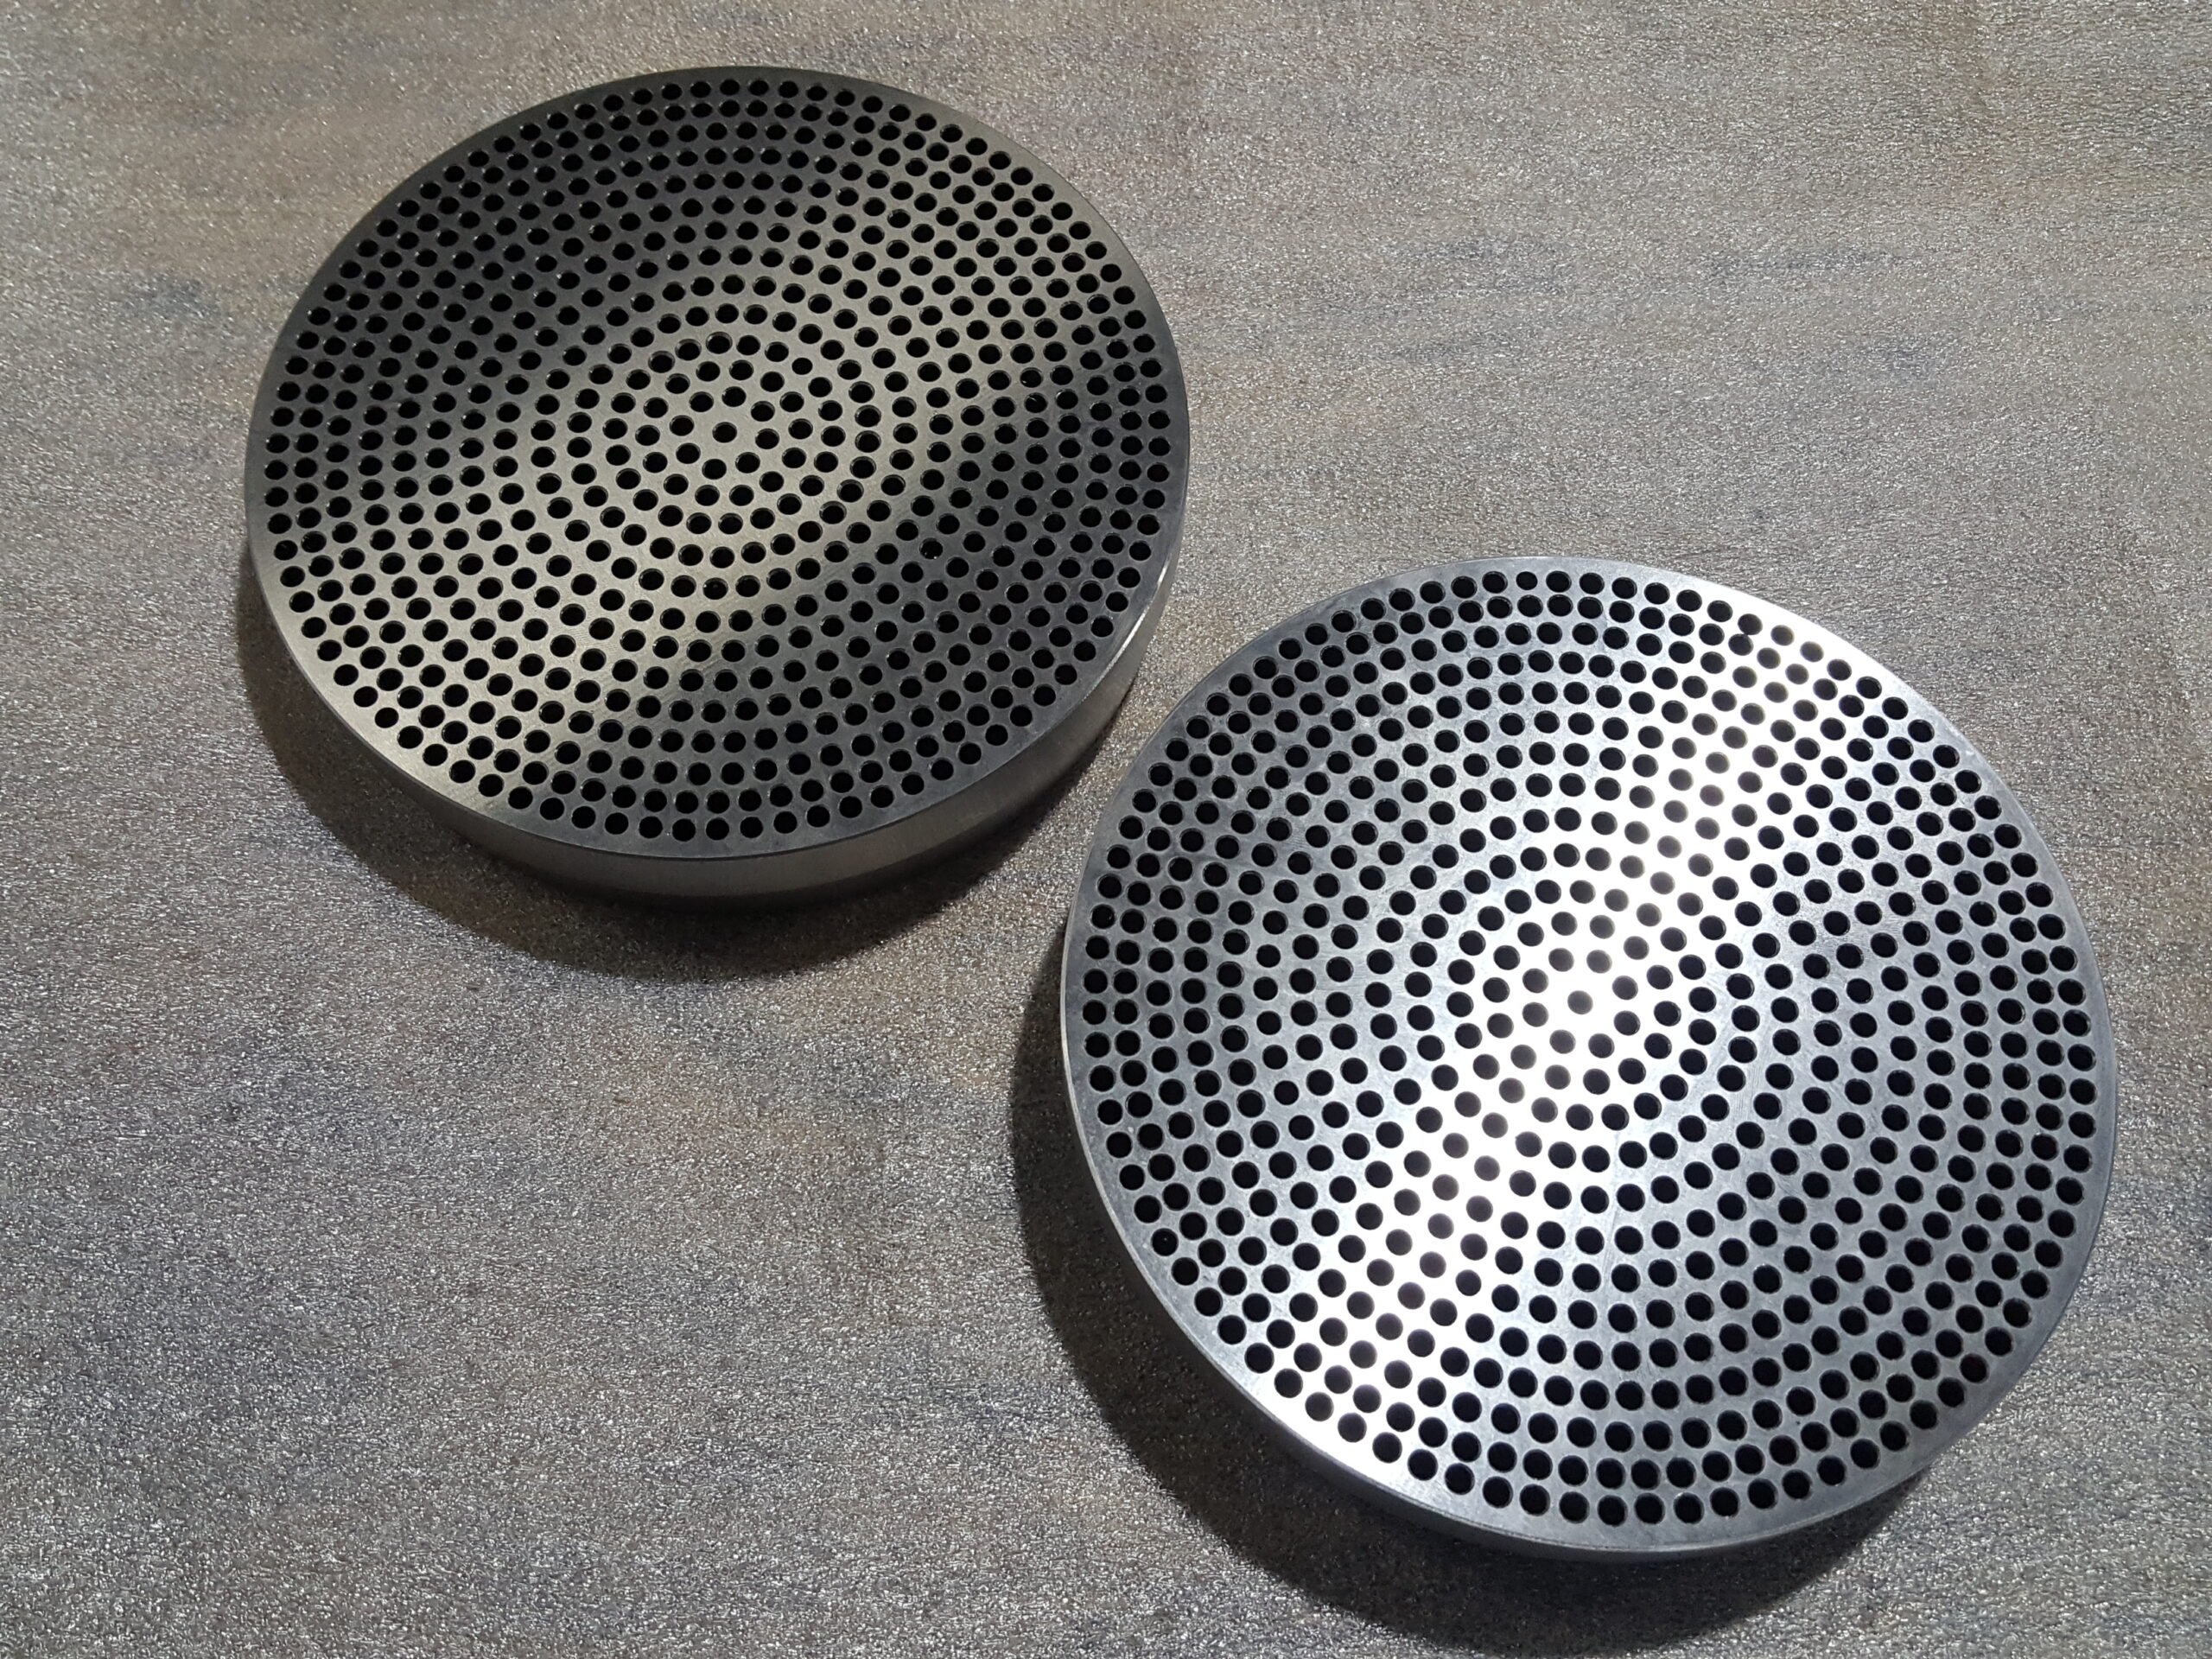
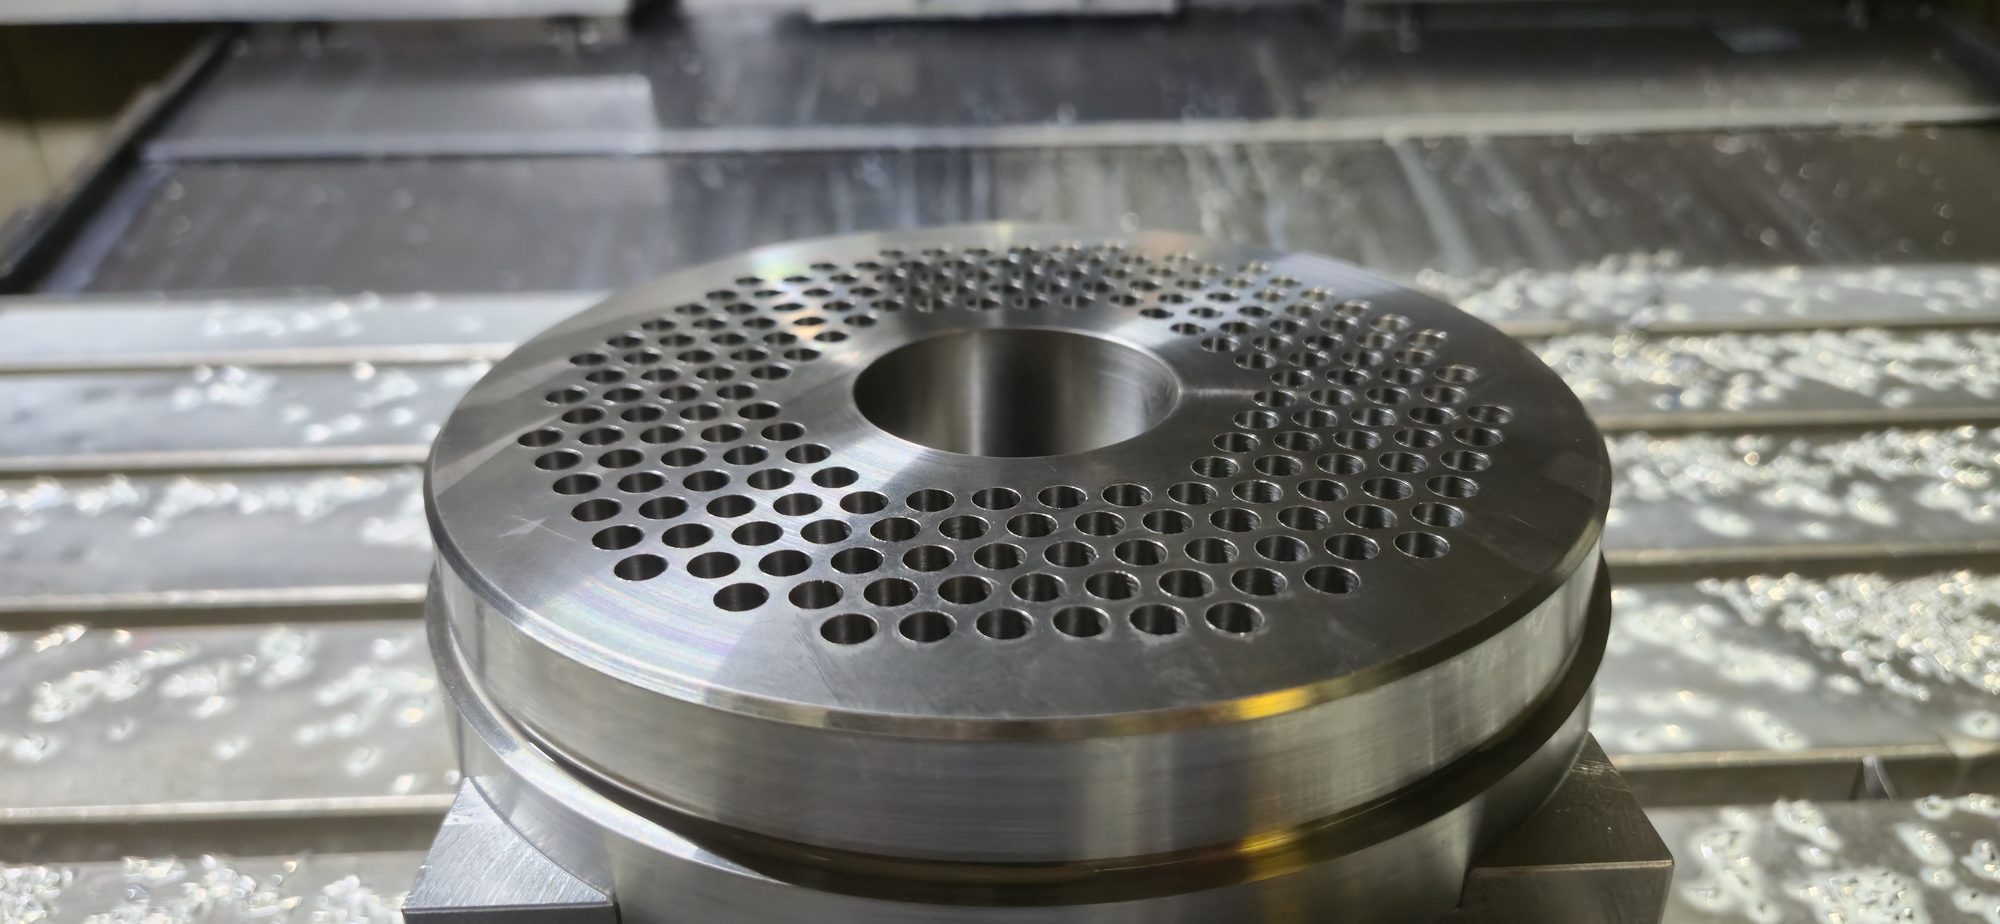
Drilled breaker plates in 15-5 PH stainless, with the hole pattern and counterbores to your drawing.
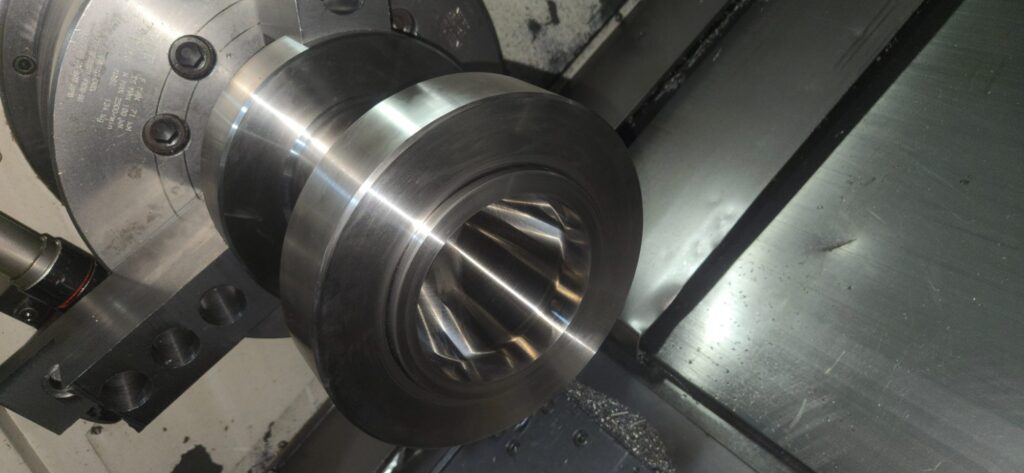
Flange and transition adapters between barrel, screen changer, pipe and die, in 4140 HT and Inconel 718.
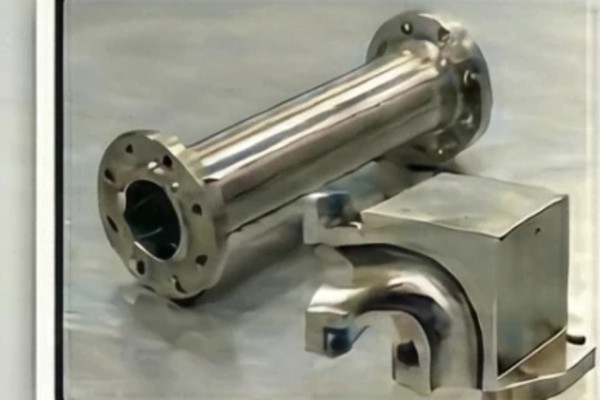
Heavy-wall melt pipes gundrilled to 4″ diameter and 96″ deep, then honed. Elbows and transition bends with the flow bore machined and polished to line up with the pipe on either side. ID transitions, tapered and sealing ends, and flanges machined from solid, welded or threaded on. Full details on melt pipes, long-neck elbows and honed tube.
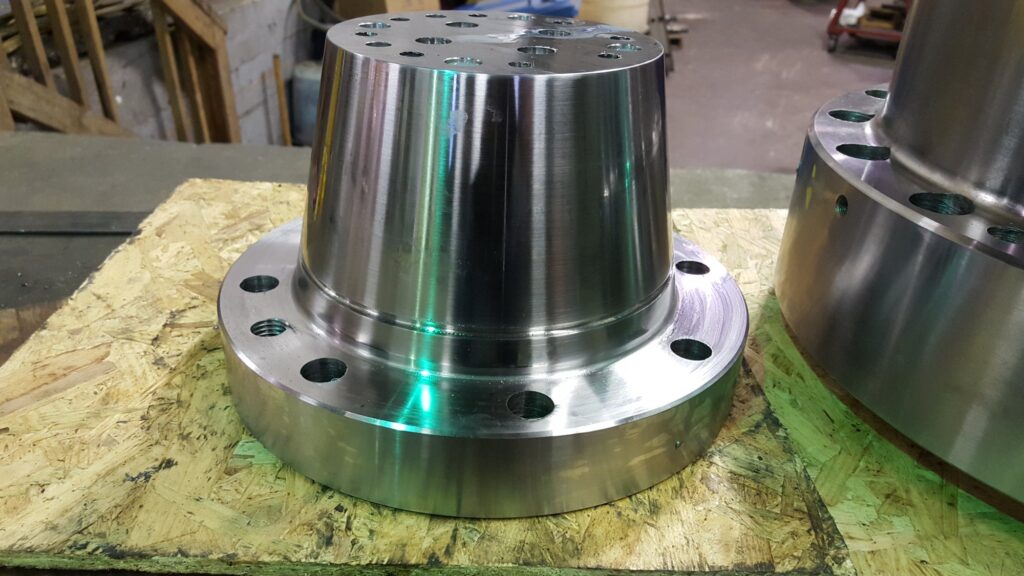
Die adapters and mounting flanges between the melt line and the die, with bores, bolt circles and sealing faces machined to your drawing.
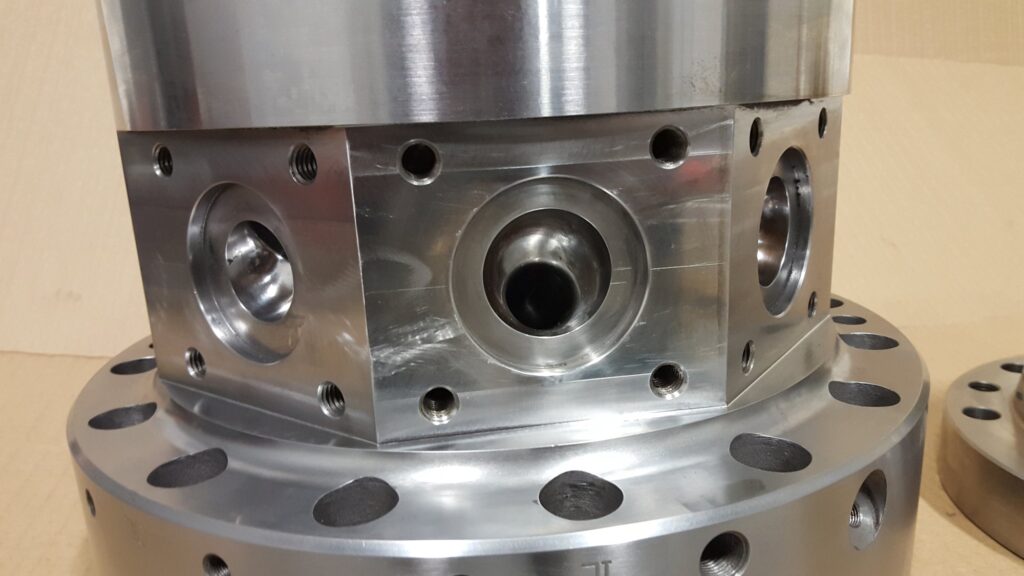
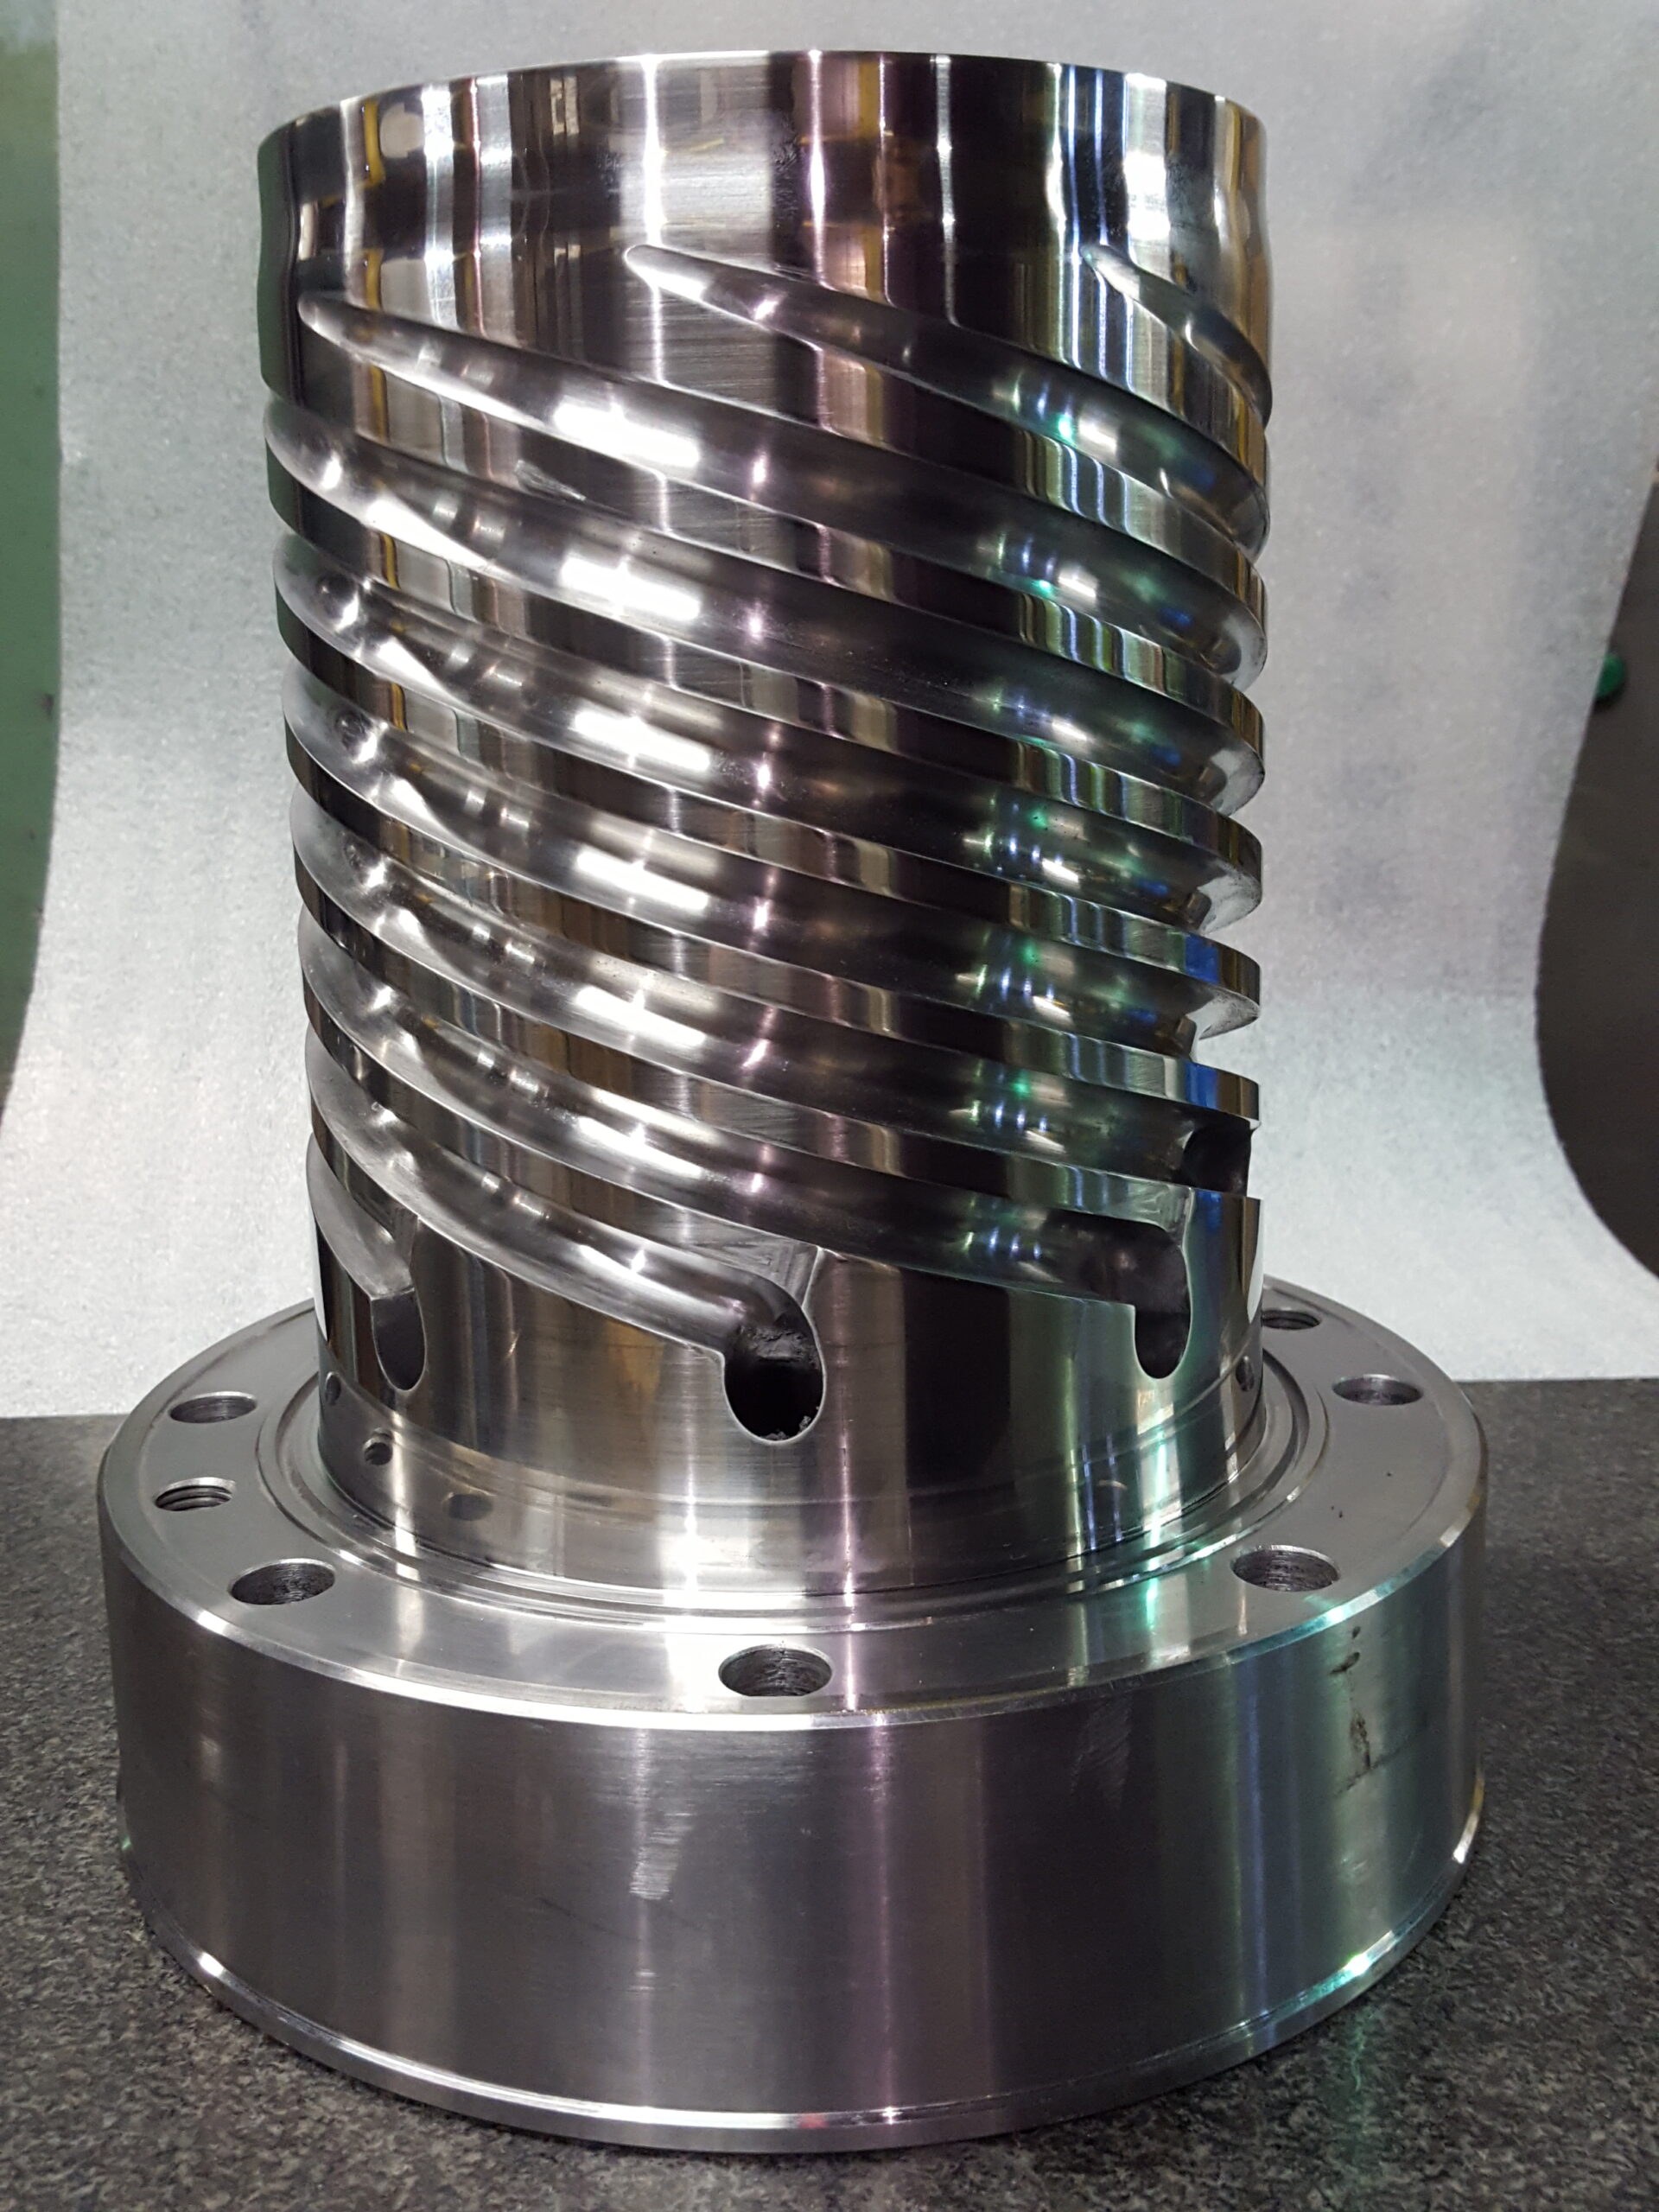
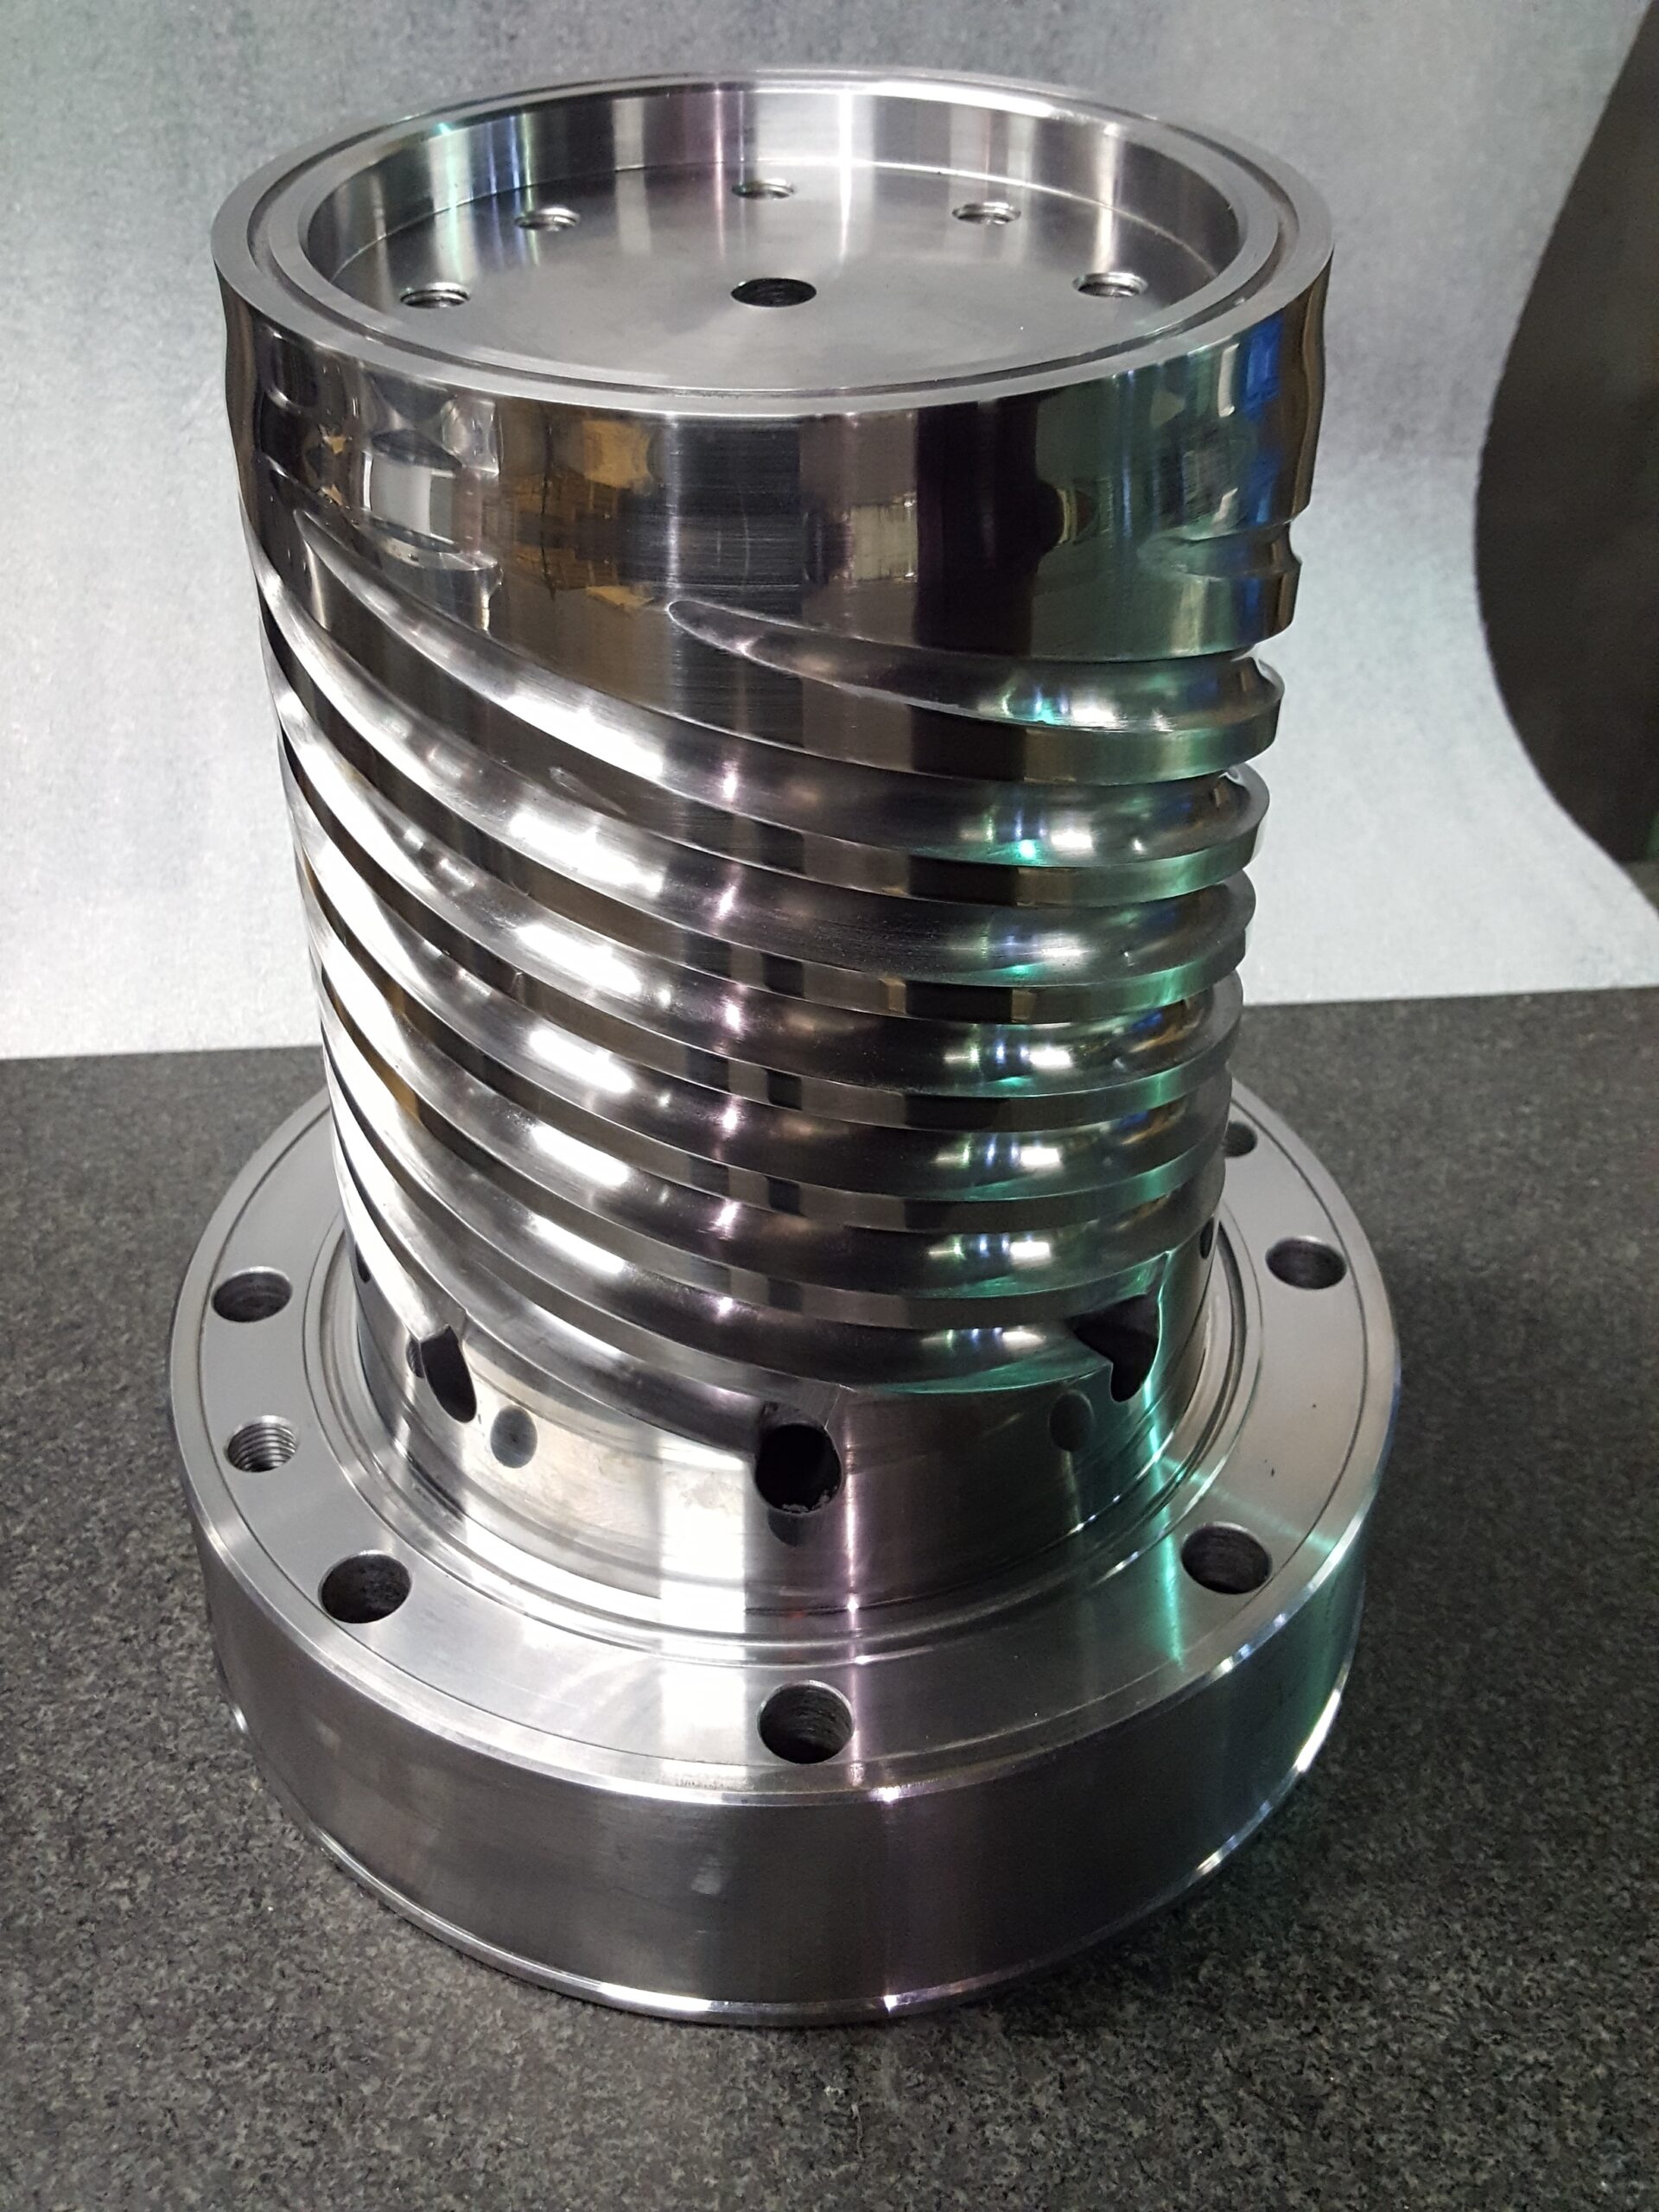
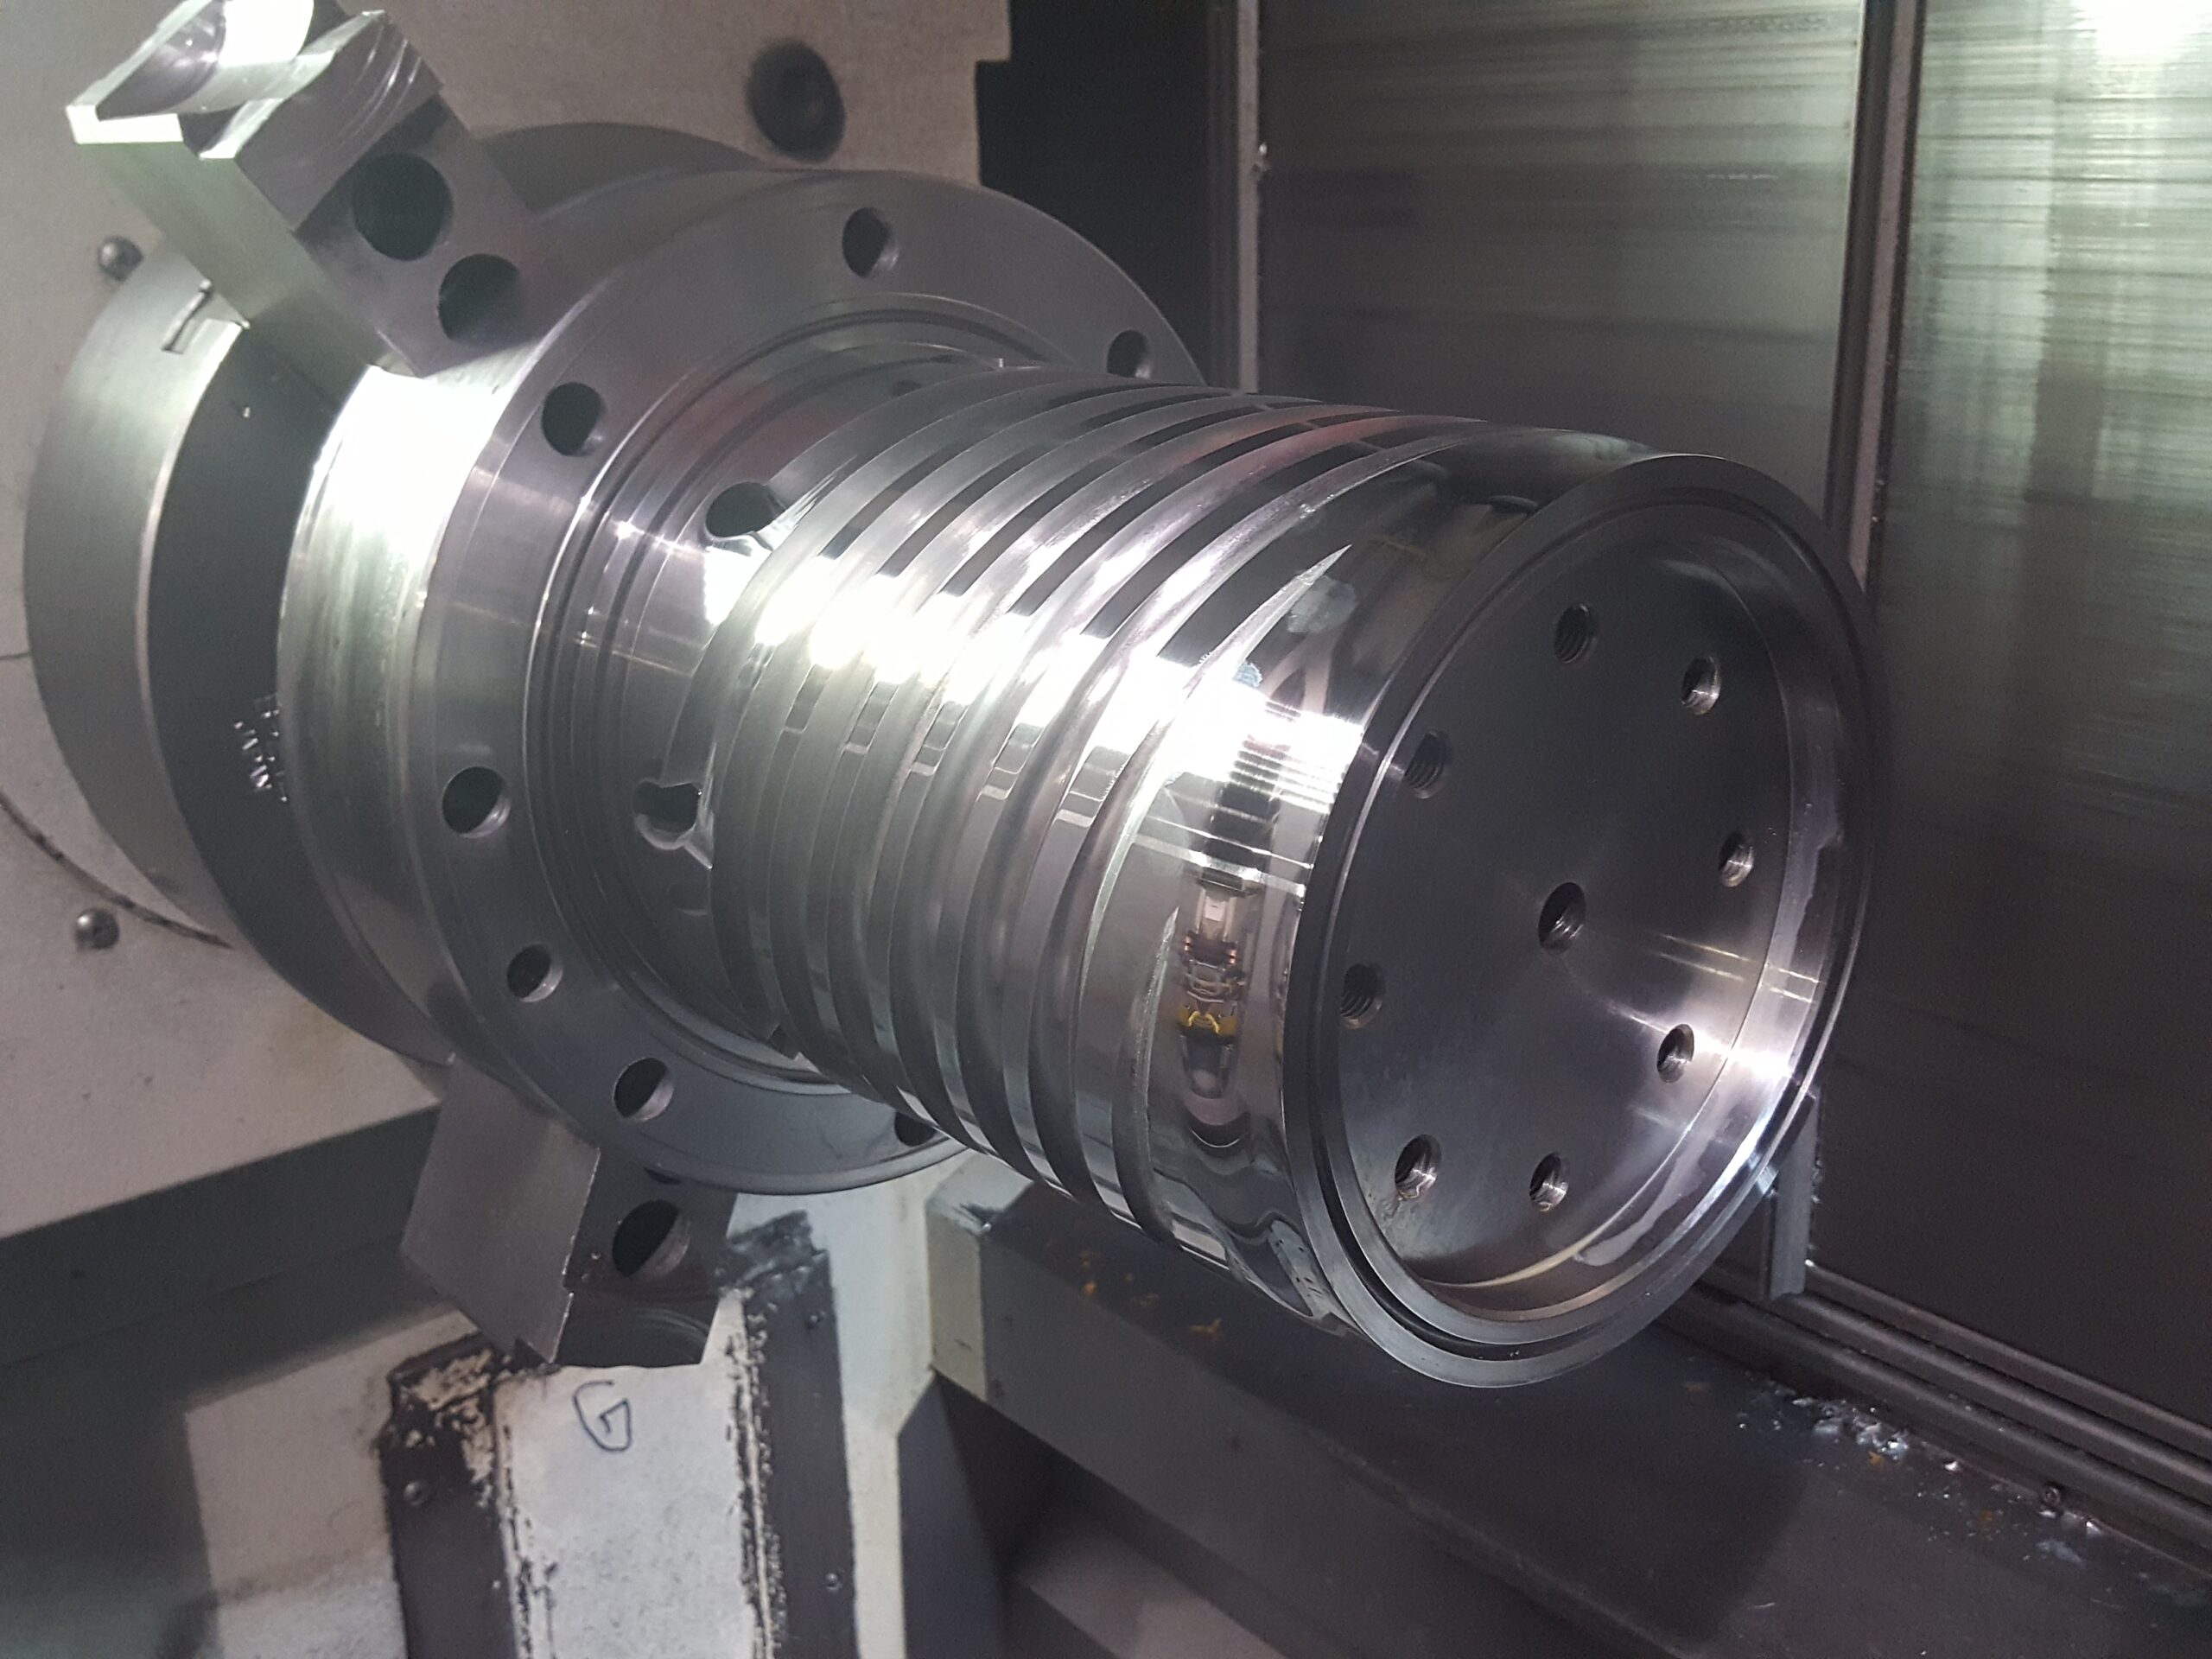
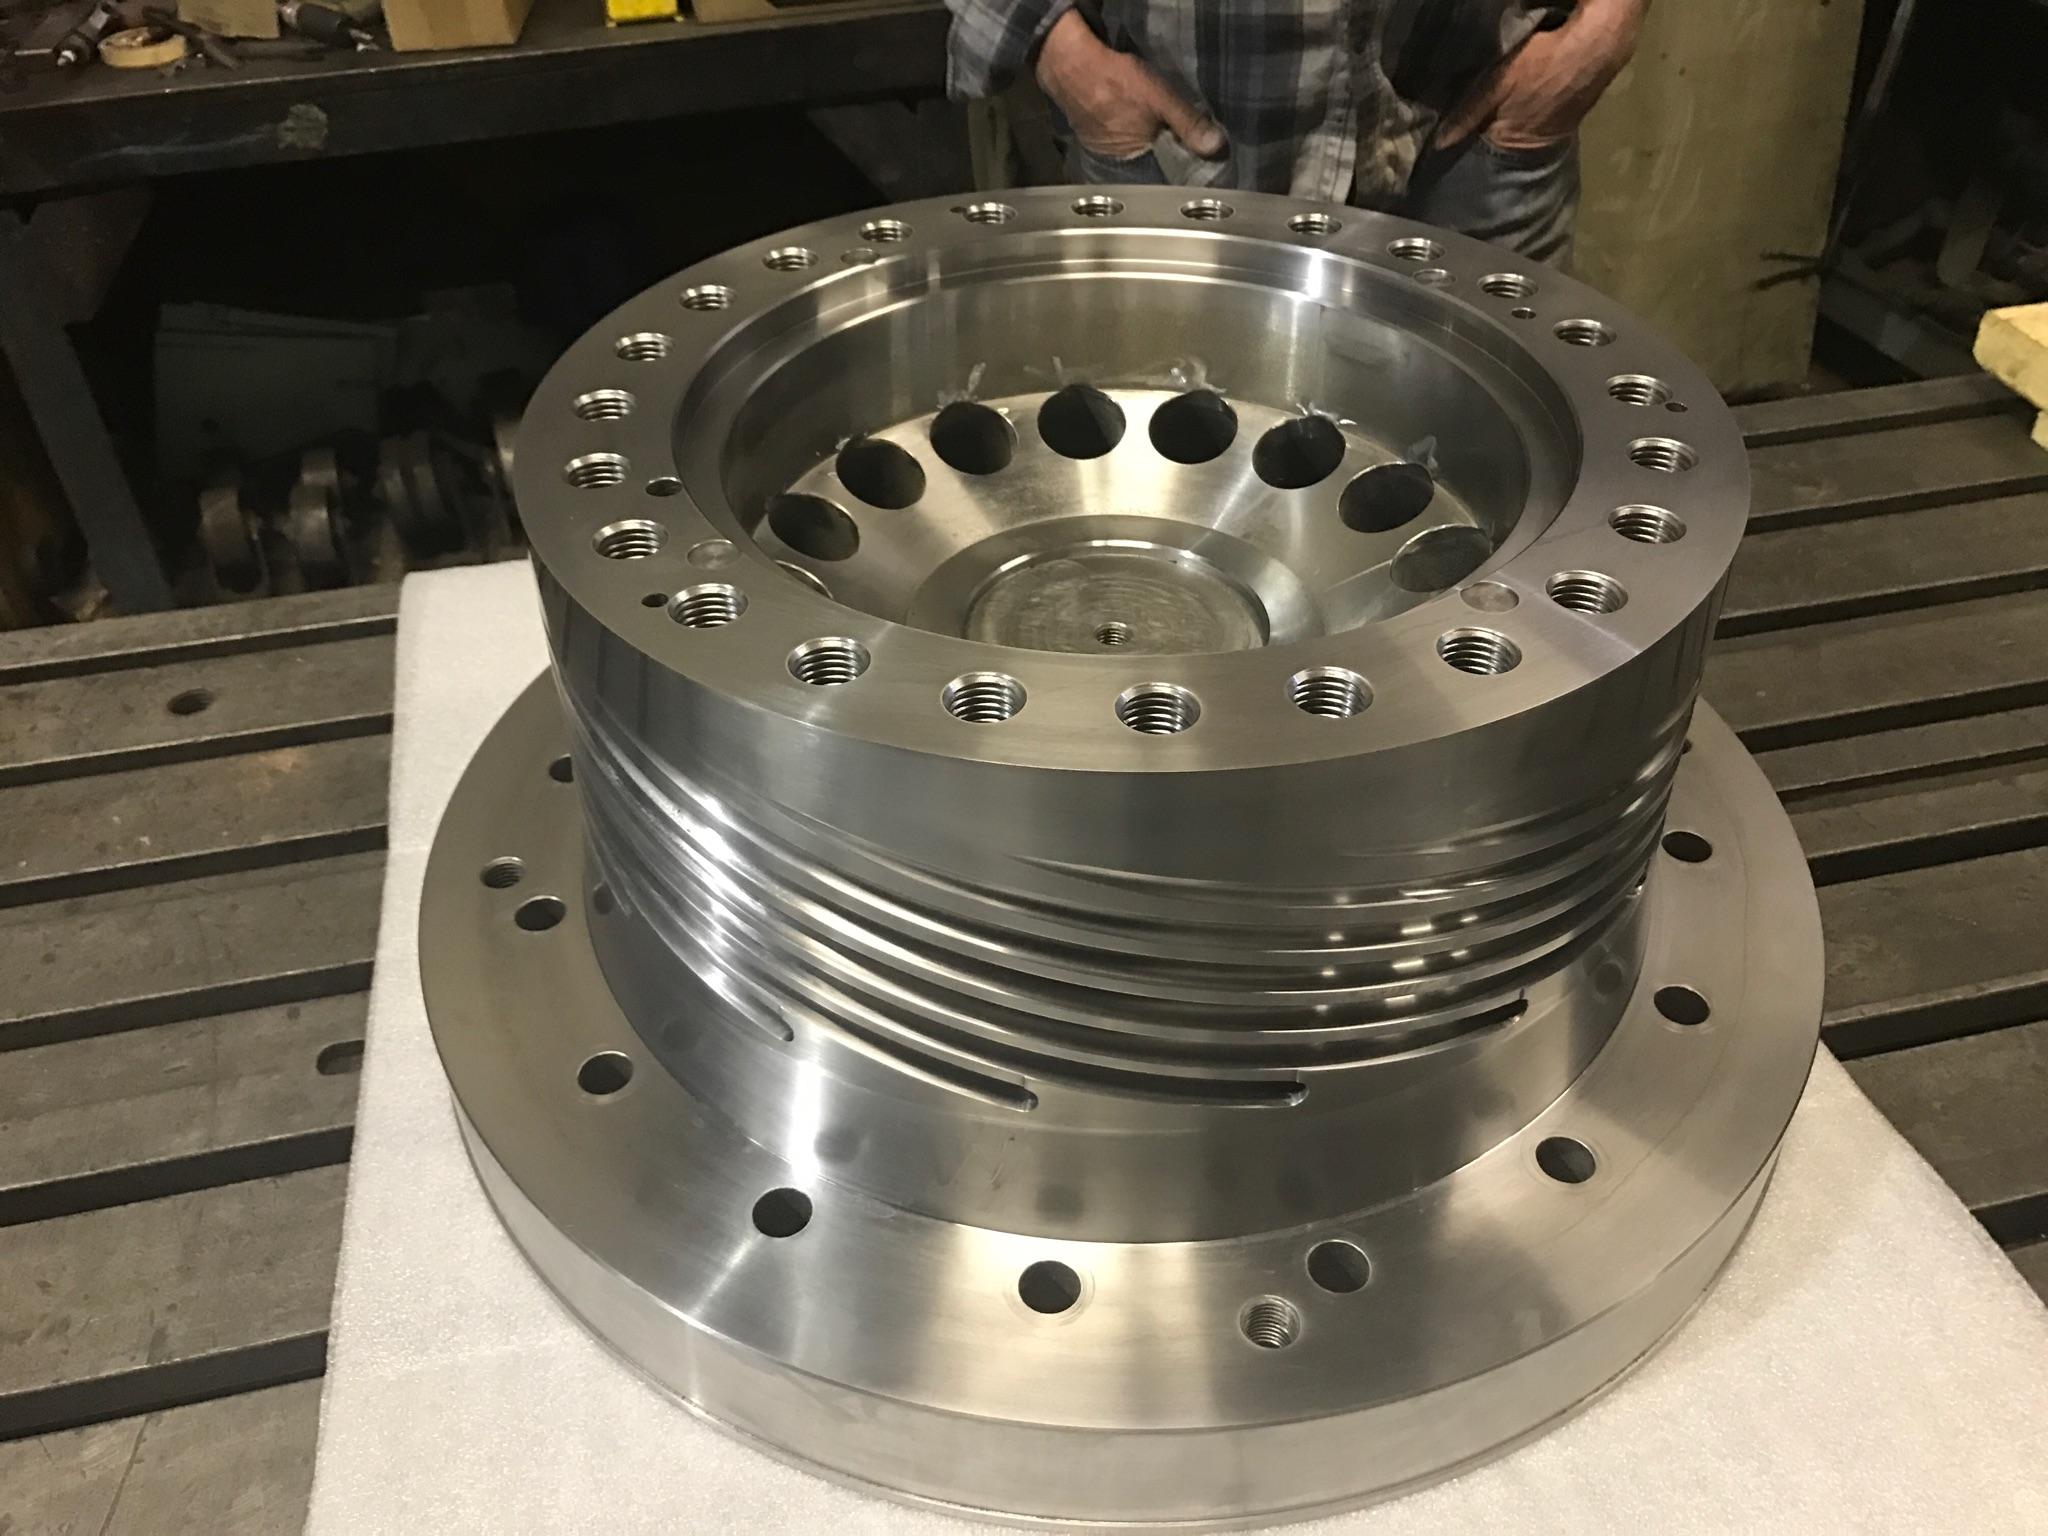
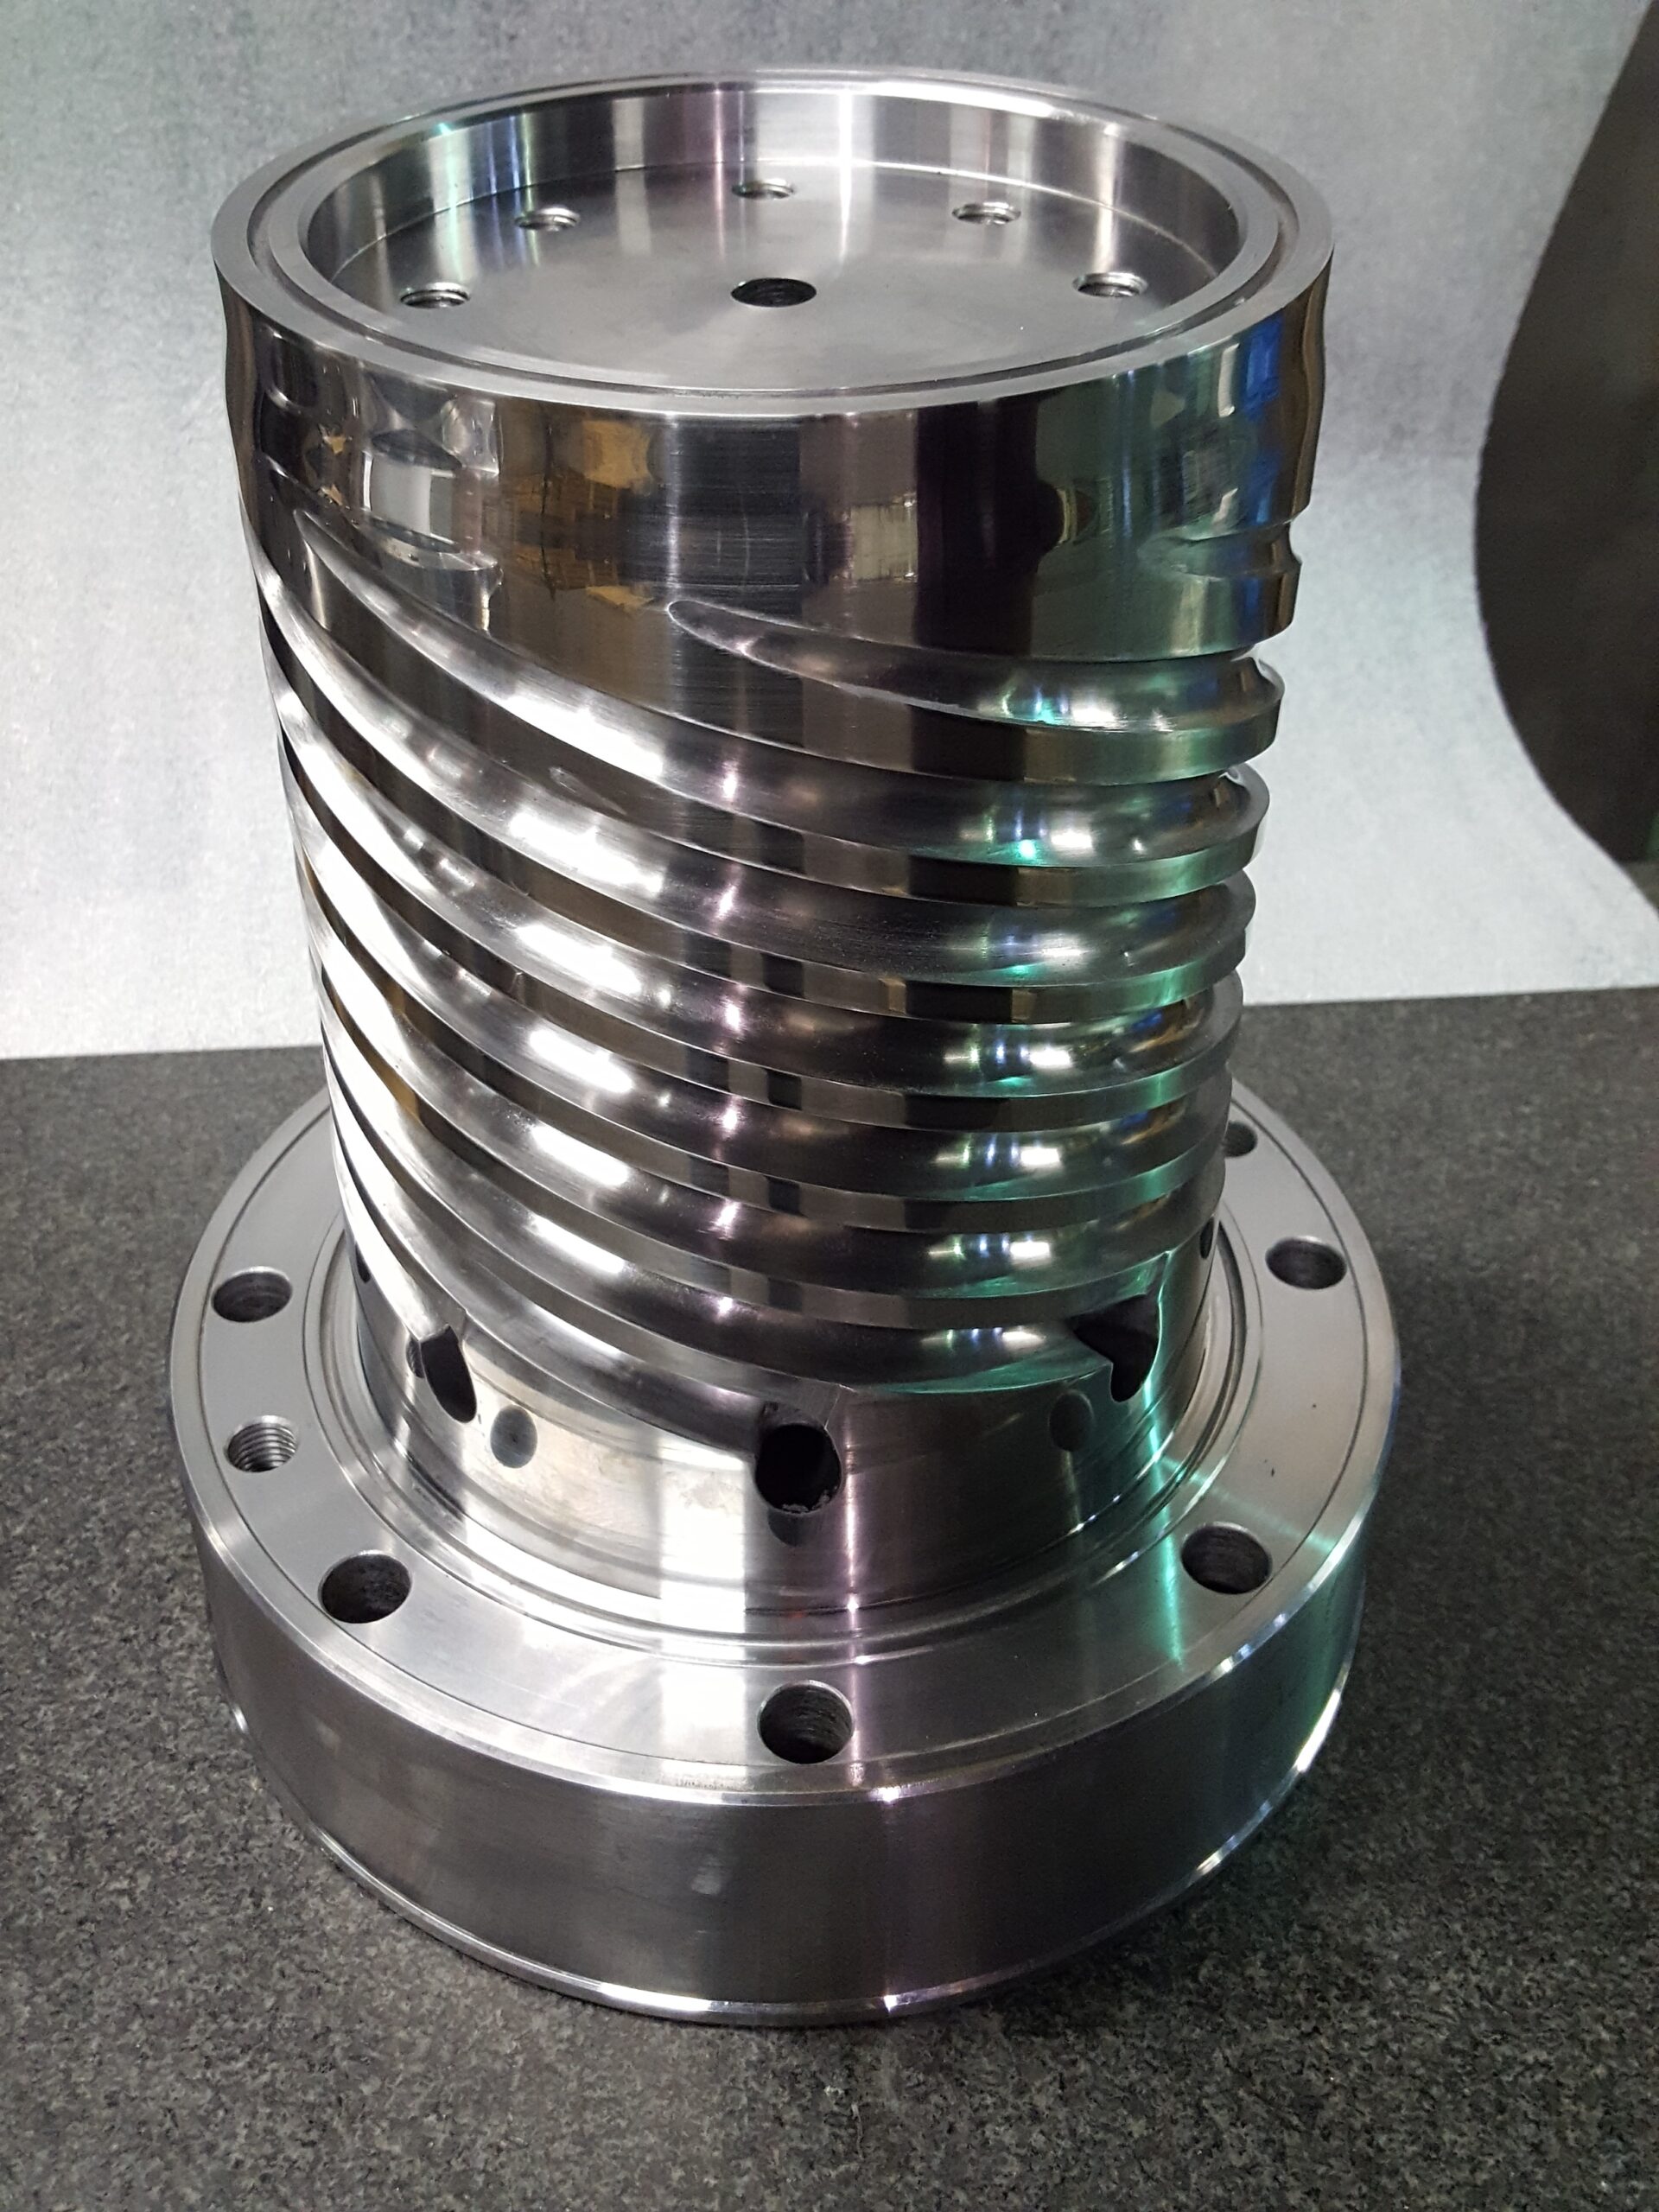
Blown film die bodies, spiral mandrels and distribution plates, and flat and profile die sections. Die sections to 50″ diameter, spiral mandrels to 20″.
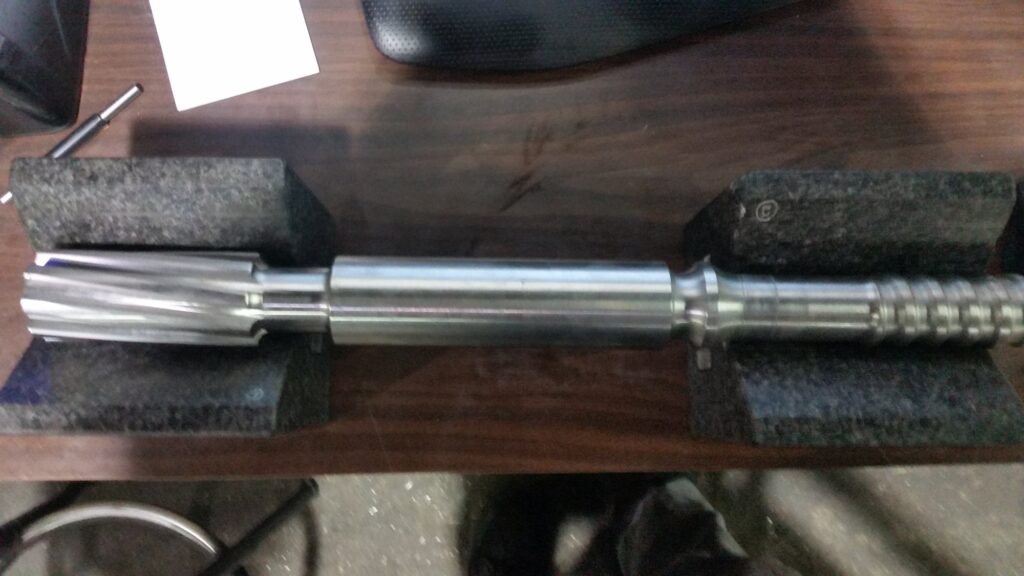
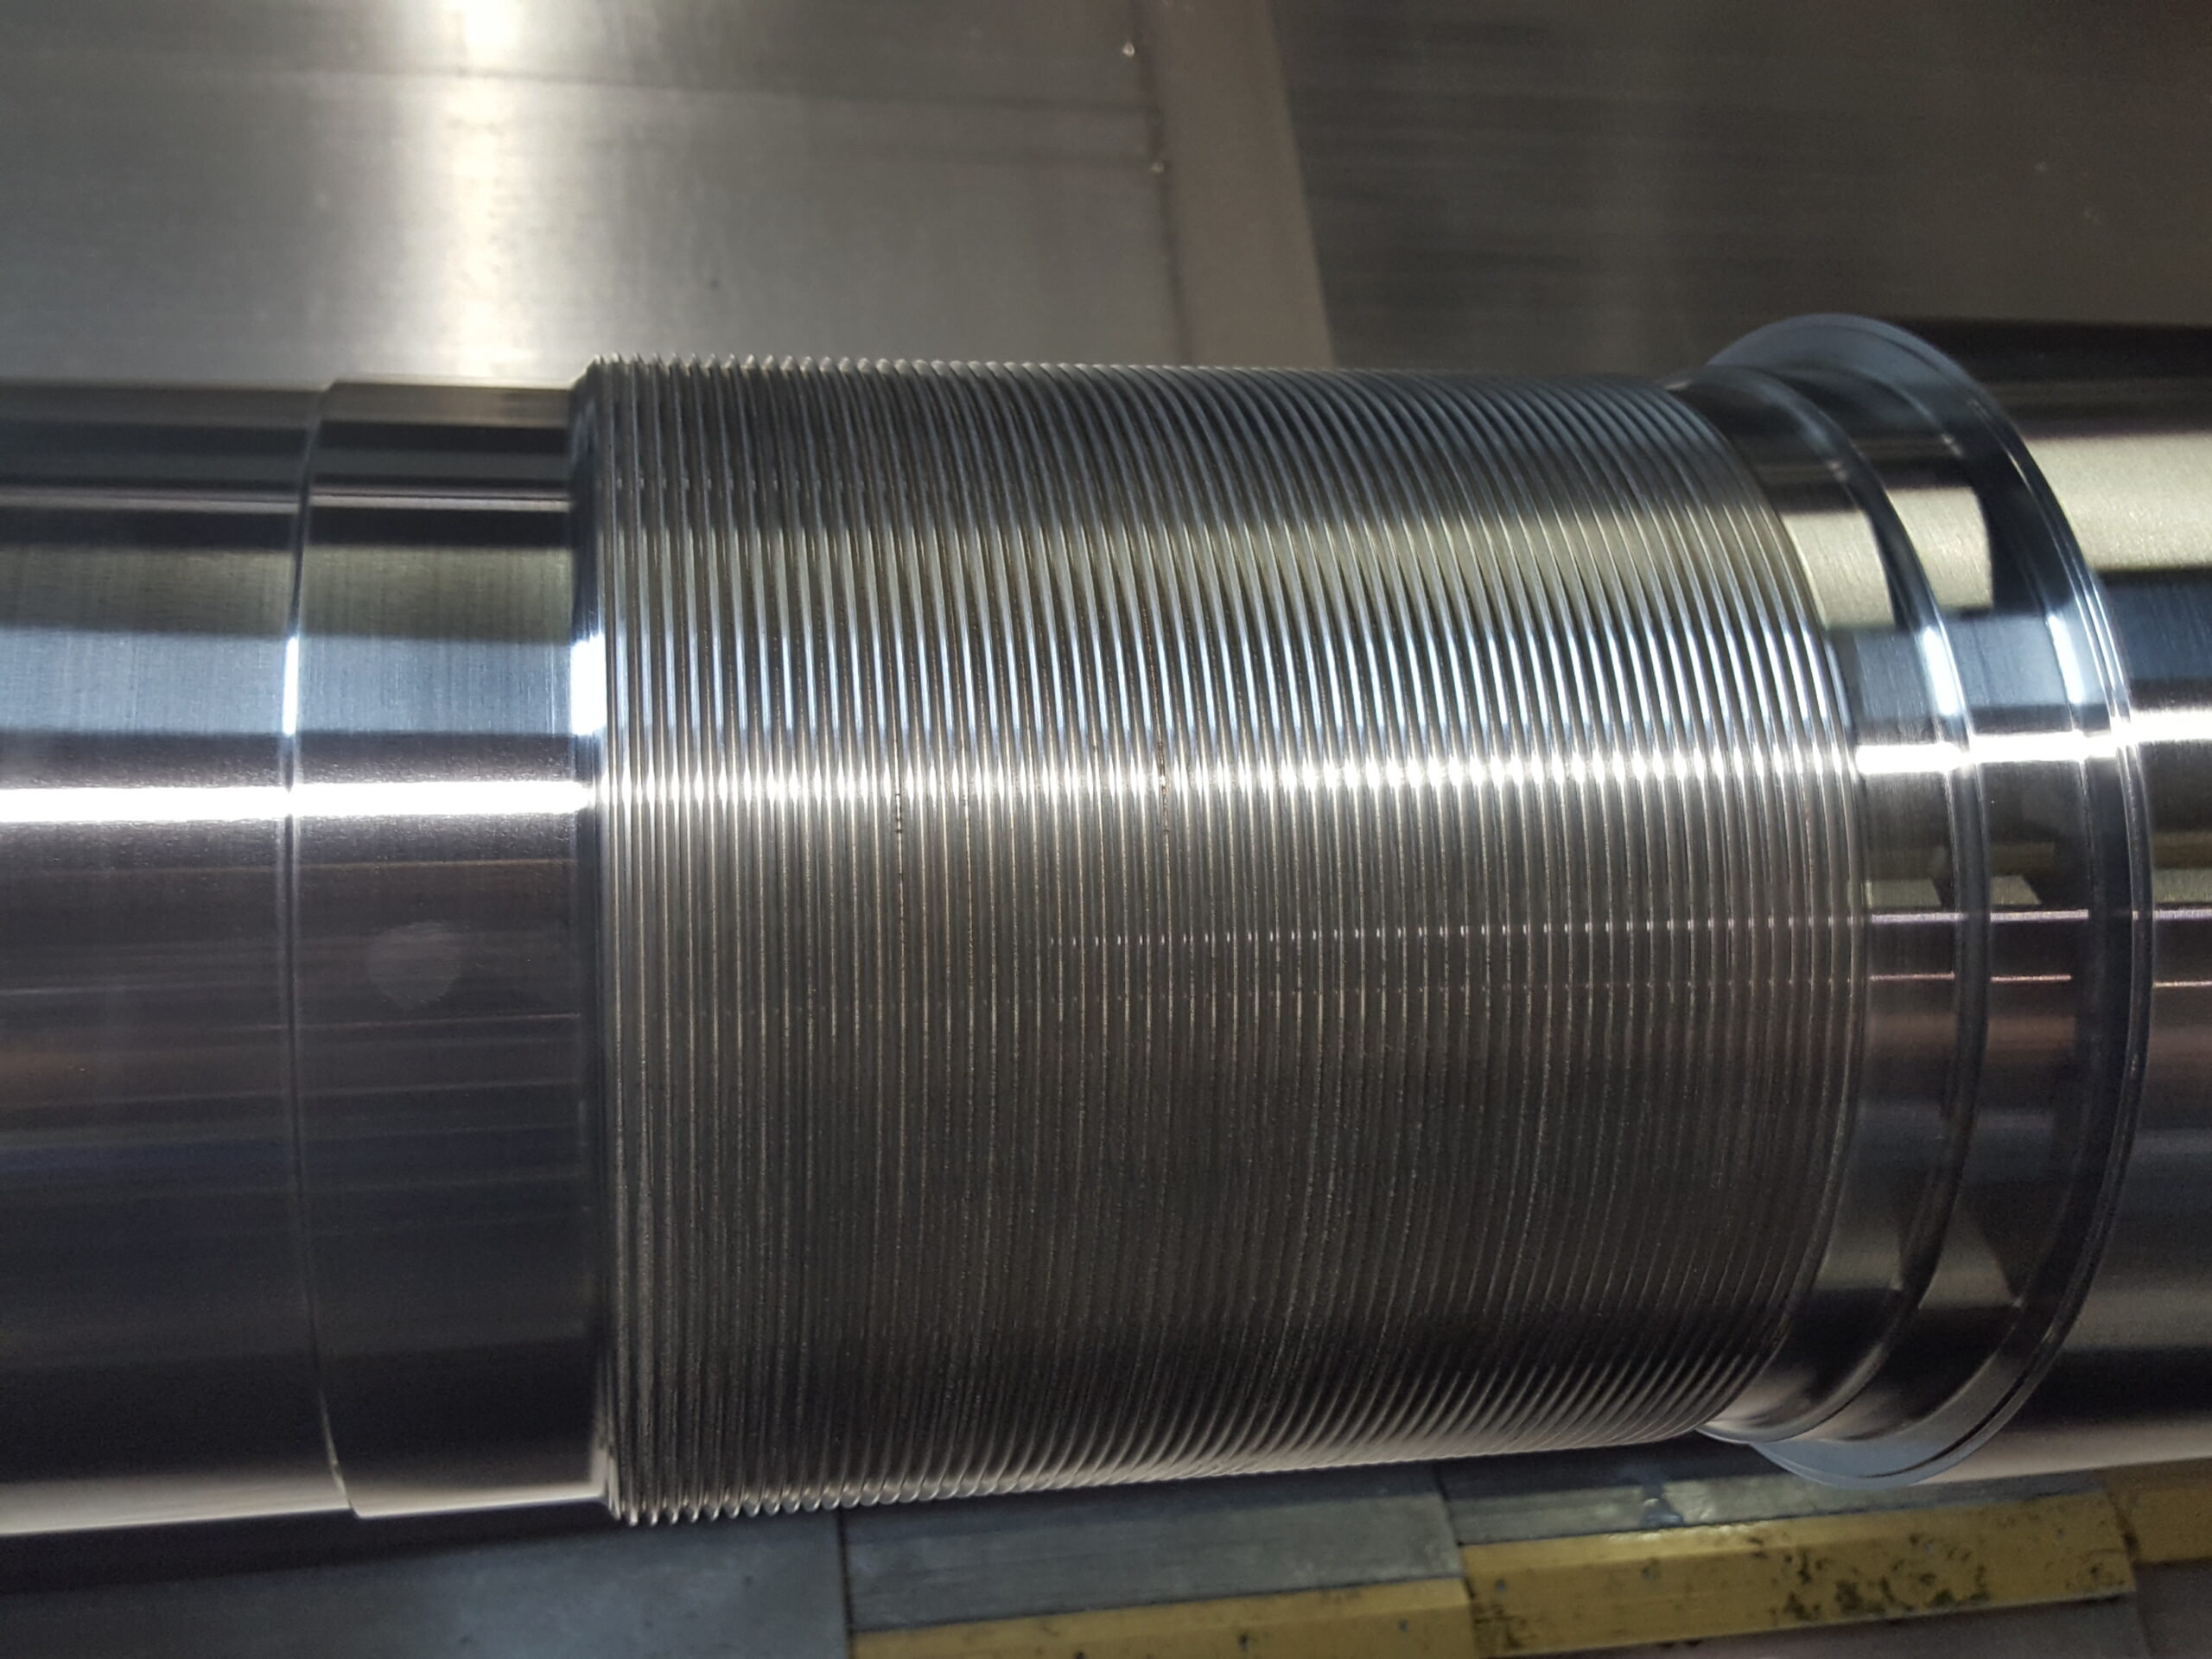
Worn flights re-cut and repaired, bent screws straightened. Hard-surfaced flights come back from our vendor and are machined to size here.
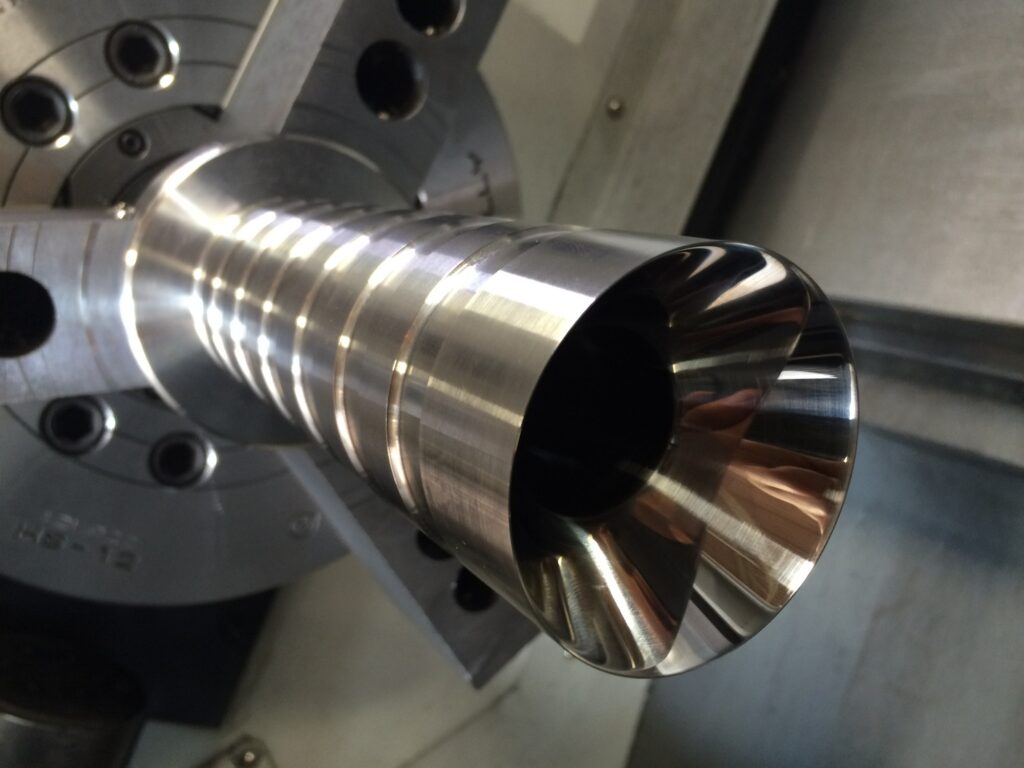
Flow channels, lands and bores polished after machining, to the finish on your print.
Extruder gearboxes have a page of their own: extruder gearbox repair and rebuild →
If it bolts onto the line, we can usually make it or fix it: feed throat parts, barrel flanges, housings, drive and support shafts. Extruder barrel bores are honed here, to 26″ diameter and 120″ long. Downstream, we make winder shafts and chucks, slitter knife holders and nip rollers.
Hard surfacing, nitriding and plating go to our vendors and come back to us for final machining, so the finished size is still ours.
Extrusion plants are thick on the ground in this part of the country, and most of these parts go out to them: across New Jersey — Bridgewater, Somerville, Flemington, Edison, Piscataway and Trenton, and the corridor through Newark, Elizabeth, Jersey City and Paterson — and into eastern Pennsylvania, New York and New England. Extruder parts travel well, so plenty also go by truck across the United States, Canada and Mexico; we regularly ship replacement parts to plants in Texas and the Midwest. Tell us the machine, the part and how fast you need it.
If your part sits outside these, send it anyway. We will tell you straight whether it is ours.
| Blown film die sections | to 50″ diameter |
| Spiral mandrels | to 20″ diameter |
| 5-axis mill-turn | Mori Seiki NTX2000 |
| Gundrilling | 4″ diameter × 96″ deep |
| Bore honing | 26″ diameter × 120″ long |
| CNC turning | 28″ × 60″ long (Okuma LB4000EX); 14″ × 83″ long (Doosan Puma 300XLY) |
| Manual turning | 60″ diameter vertical; 32″ × 170″ long horizontal |
| Milling | to 157″ — Zayer |
| Materials | 4140 HT, 15-5 PH and other stainless, Inconel 718, titanium |
Everything between the gearbox and the die, and a good deal downstream of it: gearbox-to-extruder adapters, screen changer bodies and slide plates, breaker plates, barrel and transition adapters, melt pipes and elbows, die adapters and flanges, blown film die bodies, spiral mandrels and die sections, and screw repair. Downstream, winder shafts and chucks, slitter knife holders and nip rollers.
Yes, and it is one of the most common jobs here. Send the worn part, or a photo and the dimensions you can measure, and we will reverse engineer it and make the new one. Obsolete lines are kept running this way all the time.
Yes. Single and twin-screw. The gearbox side of twin-screw machines is covered on the gearbox page; the adapters, screen changers, breaker plates, melt piping and dies are covered here.
Yes. Worn flights are re-cut and repaired and bent screws are straightened here. Hard surfacing goes to our vendor and the screw comes back to us to be machined to final size, so the finished dimension is still ours.
Yes. Barrel bores are honed here to 26″ diameter and 120″ long, to ±.0001″ and a finish from 32 down to 8 RMS.
4140 HT for most bodies and adapters, 15-5 PH and 17-4 PH stainless for breaker plates and corrosion-exposed parts, Inconel 718 where the polymer or the temperature demands it, and tool steels for die sections. Nitriding, hard surfacing and plating go to our vendors and come back for final machining.
Yes — gundrilled, honed, flanged or threaded, with ID transitions and sealing ends. They have a page of their own with the full detail.
Hillsborough, New Jersey, in Somerset County. Most extruder parts go to plants across New Jersey, eastern Pennsylvania, New York and New England, and plenty ship by truck across the United States, Canada and Mexico. Send the print and we will quote it with a lead time.
Spiral mandrels, breaker plates and feed screws machined for polymer extrusion and blown film lines — cut from 4140HT, 15-5 PH stainless and Inconel in our New Jersey shop.